
In my extensive study of automotive engineering and manufacturing, I have delved deeply into the realm of turbocharger shell castings, recognizing their pivotal role in enhancing engine performance and meeting global environmental standards. The drive for节能减排 and green initiatives has intensified focus on automotive exhaust emissions, prompting innovations in components like turbochargers. As an air compressor, a turbocharger increases进气量 by compressing ambient air, thereby boosting engine power, improving emissions, providing altitude compensation, and enhancing fuel economy. The shell castings, particularly the压壳 or housing, are critical to these functions, as they house key components and withstand high temperatures and pressures. In this article, I will explore the casting processes for these shell castings, analyze prevalent defects, and propose改进 measures, all while emphasizing the importance of precision in shell castings for automotive applications.
The turbocharger’s structure fundamentally comprises two main parts: the compressor and the turbine. To summarize, the compressor includes a diffuser, a single-stage centrifugal compressor, and a compressor housing, while the turbine consists of a turbine wheel, turbine housing, and a single-stage radial flow design. Internally, components like internally supported rotors, full-floating bearings in the intermediate body, and thrust ball bearings manage axial forces. Externally, sealing rings are installed at both ends, with additional挡油罩 on the compressor side to prevent oil leakage. Understanding these elements is essential for appreciating the casting demands of shell castings, which must achieve high dimensional accuracy and material integrity. Below, I present a table summarizing the key components and their functions in turbocharger shell castings:
| Component | Function | Relevance to Shell Castings |
|---|---|---|
| Compressor Housing | Directs compressed air into the engine | Primary shell casting requiring smooth internal surfaces |
| Turbine Housing | Channels exhaust gases to drive the turbine | Shell casting exposed to high thermal stresses |
| Intermediate Body | Supports bearings and seals | Complex shell casting with precision channels |
| Sealing Rings | Prevents leakage of fluids | Integrated into shell casting design |
The advantages of turbochargers are quantitatively significant. For instance, they can increase engine output power by up to 30% without altering displacement, contributing to节能减排. This performance boost is often modeled using thermodynamic principles. The compression ratio, a key parameter, can be expressed as: $$ \text{CR} = \frac{P_2}{P_1} $$ where \( P_1 \) is the inlet pressure and \( P_2 \) is the outlet pressure. The efficiency of the compressor in shell castings affects this ratio, highlighting the need for optimal casting quality. Another formula relevant to shell castings is the heat transfer during operation: $$ Q = h A \Delta T $$ where \( Q \) is heat flux, \( h \) is the heat transfer coefficient, \( A \) is the surface area of the shell casting, and \( \Delta T \) is the temperature difference. This underscores the importance of material properties and casting integrity in managing thermal loads.
Moving to the casting process for turbocharger shell castings, it involves several meticulous stages: mold selection, mold preheating, pouring, and cooling. In mold preheating, I emphasize the use of模温机 to steadily supply heat, maintaining模具 temperatures around 300°C. During pouring, metal liquid is introduced into the cavity, where repeated heat exchange occurs until thermal equilibrium is achieved. This balance can be described by: $$ m_c C_c \frac{dT_c}{dt} = k A (T_m – T_c) $$ where \( m_c \) is the mold mass, \( C_c \) is specific heat, \( T_c \) is mold temperature, \( k \) is thermal conductivity, \( A \) is interface area, and \( T_m \) is metal temperature. For shell castings, this equation guides preheating protocols to prevent defects. The melting of铝合金 for these castings includes steps like配料,加料,熔化,精炼,变质处理, and成分分析. To ensure quality, measures such as drying炉料 and tools, removing impurities, and controlling temperatures are critical. The table below outlines the melting stages for铝合金 shell castings:
| Stage | Description | Key Considerations for Shell Castings |
|---|---|---|
| 配料 | Weighing and mixing alloy elements | Ensures material consistency for shell casting properties |
| 加料 | Adding materials to the furnace | Avoids contamination that could weaken shell castings |
| 熔化 | Melting the alloy to liquid state | Temperature control prevents defects in shell castings |
| 精炼 | Removing impurities and gases | Enhances density and strength of shell castings |
| 变质处理 | Modifying microstructure | Improves mechanical properties of shell castings |
| 成分分析 | Verifying chemical composition | Ensures shell castings meet specifications |
To visualize a typical casting setup for shell castings, I include the following image link that illustrates the process:
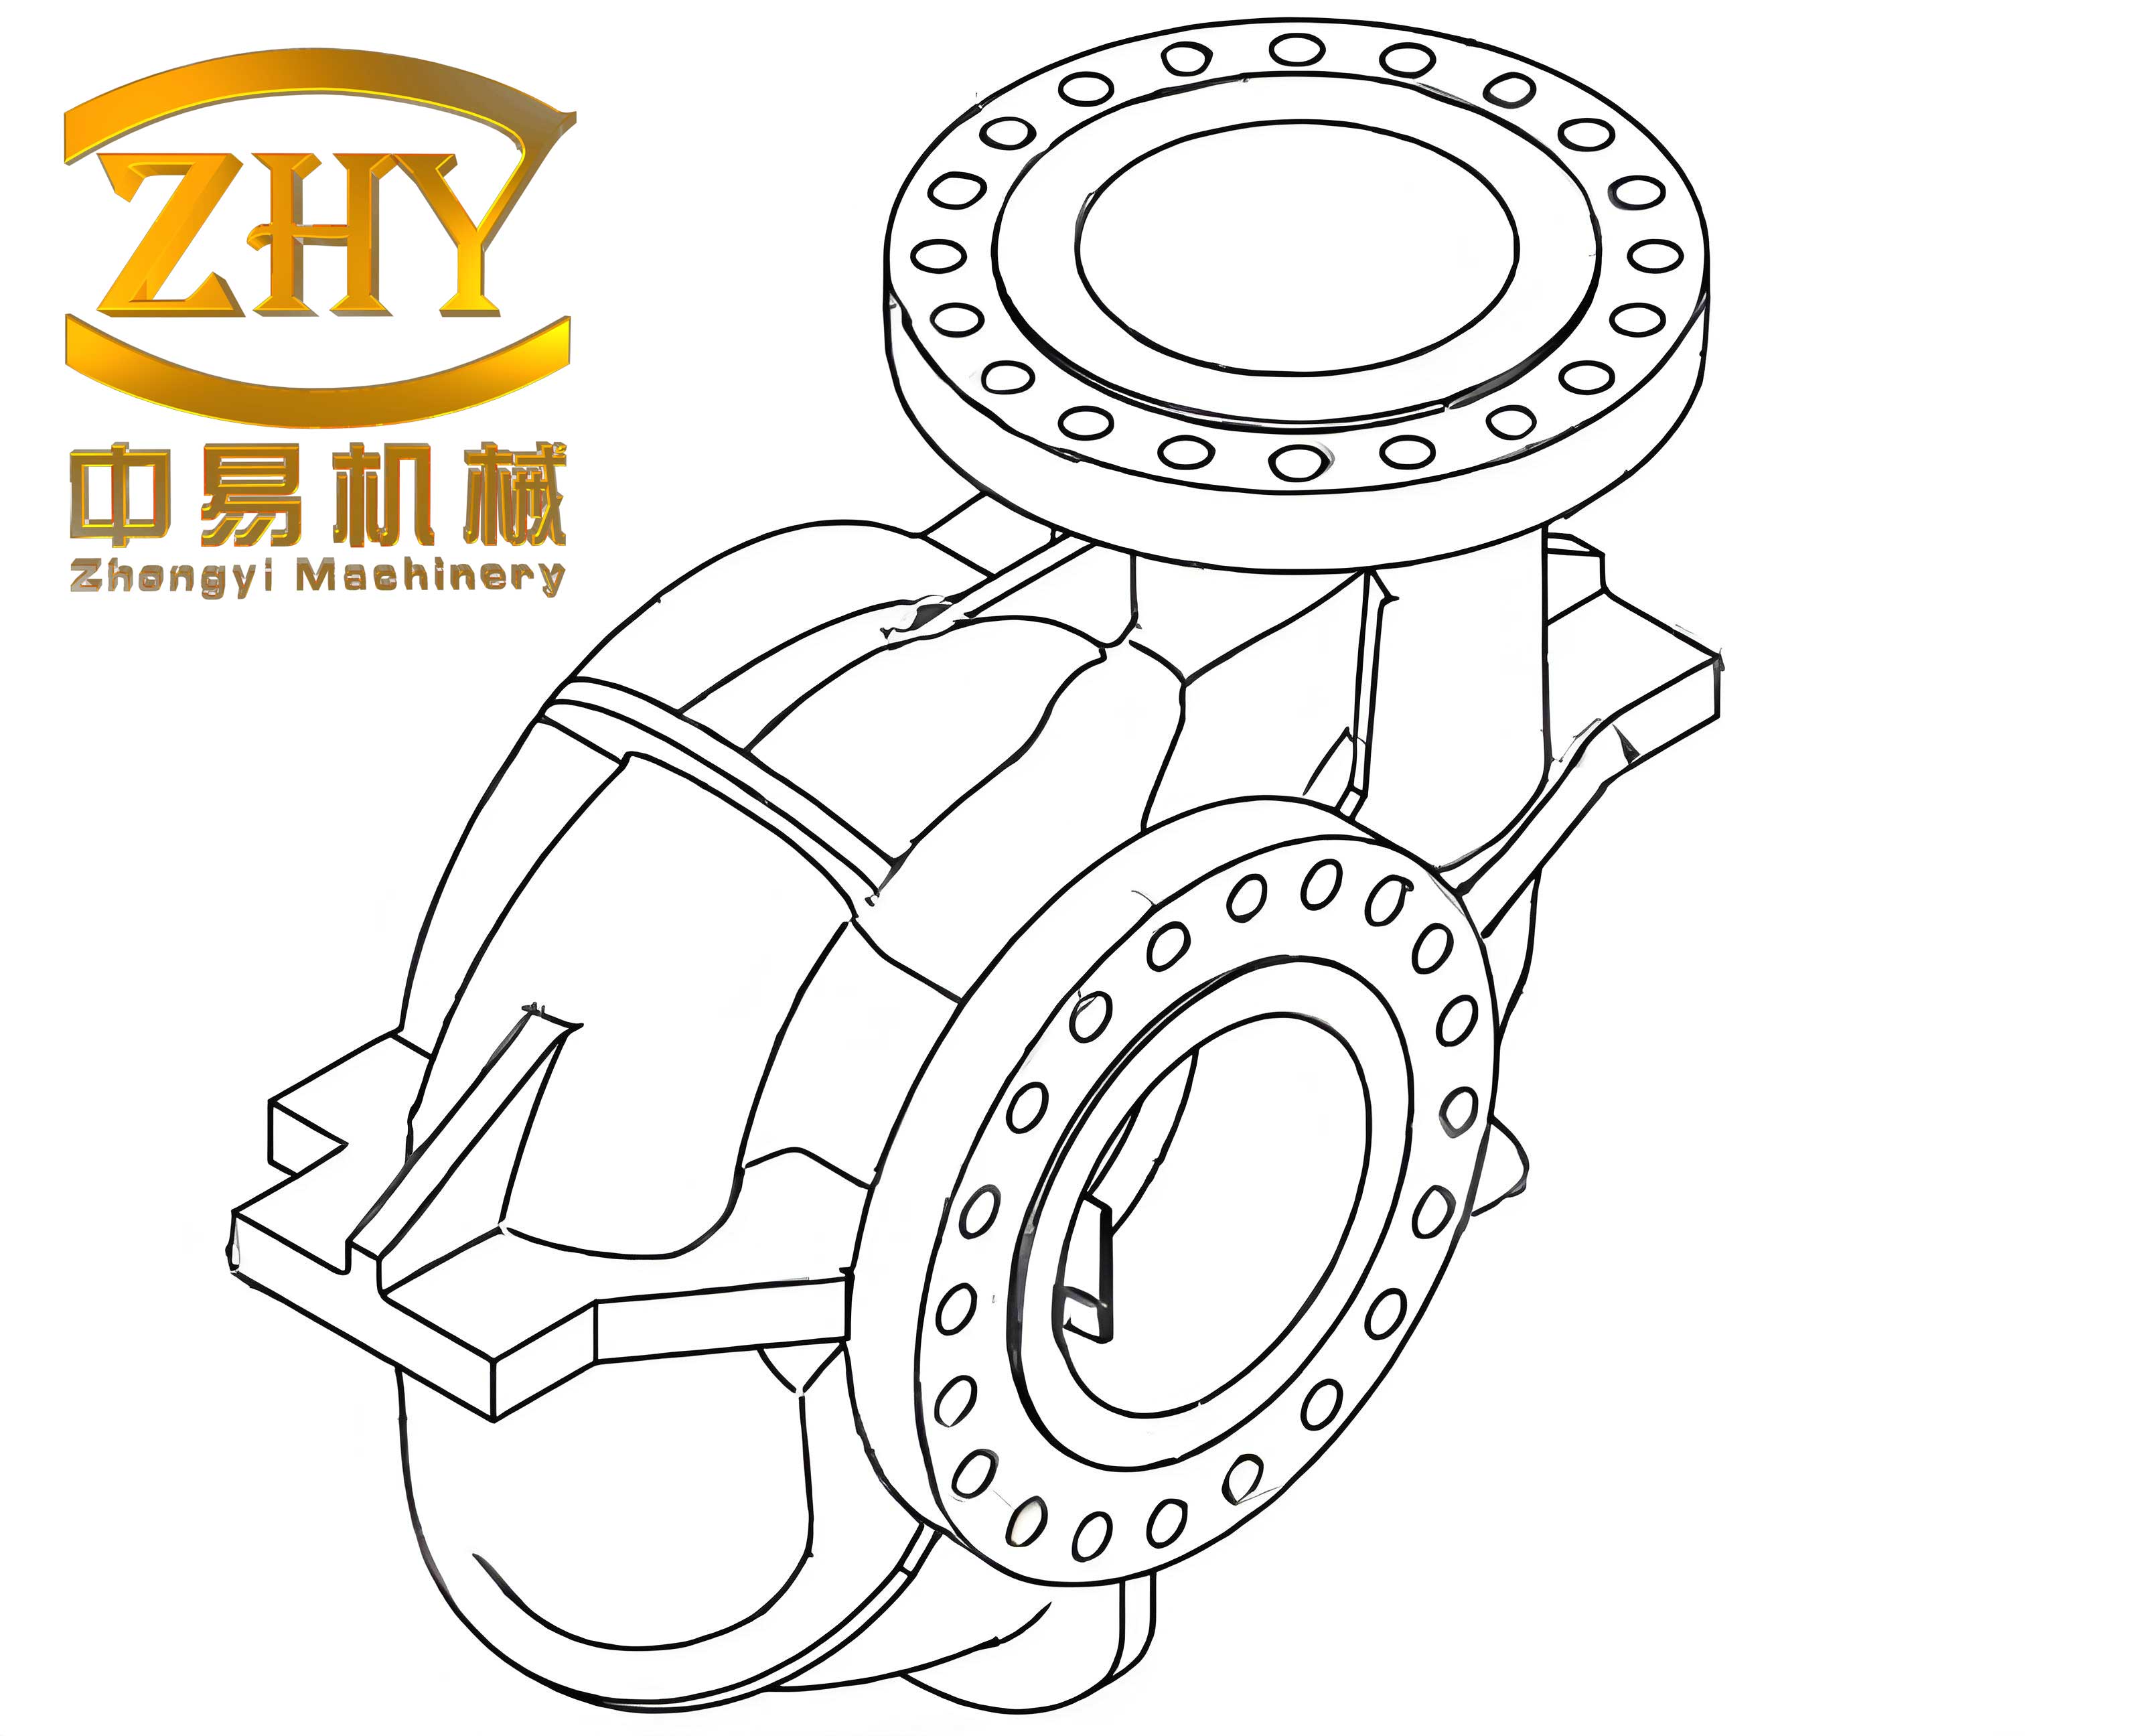
This depiction aids in understanding the complexity involved in producing high-quality shell castings for turbochargers.
However, the casting process for shell castings is prone to defects that compromise quality. Based on my analysis, common issues include large flash on mold parting lines, as well as pores and shrinkage in certain areas. Flash not only damages the casting quality but also prolongs machining time, increases costs, and wastes material, adversely affecting the production efficiency of shell castings. Pores and shrinkage, often resulting from trapped gases or improper cooling, reduce the precision and durability of shell castings, leading to不合格 turbochargers. The formation of shrinkage cavities can be modeled using solidification dynamics: $$ V_s = \beta V_0 (1 – f_s) $$ where \( V_s \) is shrinkage volume, \( \beta \) is shrinkage coefficient, \( V_0 \) is initial volume, and \( f_s \) is solid fraction. For shell castings, this highlights the need for controlled cooling. The table below summarizes defects in shell castings:
| Defect Type | Causes | Impact on Shell Castings |
|---|---|---|
| Flash (溢边) | Poor mold clamping or excessive pressure | Increases machining effort and cost for shell castings |
| Pores (气孔) | Gas entrapment during pouring | Weakens structural integrity of shell castings |
| Shrinkage (缩松) | Inadequate feeding during solidification | Reduces density and performance of shell castings |
| Hot Tears | Thermal stresses during cooling | Causes cracks in shell castings under stress |
These defects often arise from “hot spots” or thermal imbalances during casting, where localized散热不良 disrupts solidification sequences. In shell castings, this is critical because uneven cooling can lead to residual stresses and dimensional inaccuracies. The heat transfer equation for such scenarios is: $$ \nabla \cdot (k \nabla T) + \dot{q} = \rho C_p \frac{\partial T}{\partial t} $$ where \( \dot{q} \) is internal heat generation, \( \rho \) is density, and \( C_p \) is specific heat. Solving this for shell castings requires numerical methods to predict defect formation.
To address these challenges, I propose several改进 measures for enhancing the casting of shell castings. The primary goal is to manage thermal节 effectively, ensuring orderly solidification and模具 stability. Methods include water cooling, air cooling, indirect cooling via chill inserts, mold cavity modification, use of保温 coatings, heat pipe technology, and temperature control systems. Each method has its merits and drawbacks for shell castings. For instance, water cooling involves creating channels in the mold, which complicates design but offers rapid cooling. The cooling rate can be expressed as: $$ \frac{dT}{dt} = \frac{h (T – T_{\infty})}{\rho C_p L} $$ where \( T_{\infty} \) is ambient temperature and \( L \) is characteristic length. For shell castings, this formula helps optimize cooling parameters. Air cooling, while easier to implement, has lower efficiency, making it suitable for less critical areas of shell castings. Indirect cooling using chill inserts enhances heat extraction, with effectiveness modeled by: $$ Q_{\text{chill}} = k_{\text{chill}} A_{\text{chill}} \frac{\Delta T}{d} $$ where \( k_{\text{chill}} \) is thermal conductivity of the chill, \( A_{\text{chill}} \) is contact area, and \( d \) is thickness. This is particularly beneficial for thick sections in shell castings. Modifying mold cavities, within machining allowances, can reduce hot spots by improving geometry.保温 coatings, such as发热覆盖剂, slow solidification in risers to aid feeding, crucial for sound shell castings. Heat pipes, based on phase change principles, transfer heat with minimal loss, ideal for精细温度控制 in shell castings. Finally, temperature工控 devices enable regional模具 temperature management, ensuring uniformity. The table below compares these methods for shell castings:
| Method | Mechanism | Advantages for Shell Castings | Disadvantages for Shell Castings |
|---|---|---|---|
| Water Cooling | Circulating water through mold channels | Fast cooling; precise for critical shell casting areas | Complex mold design; higher cost |
| Air Cooling | Using compressed air to dissipate heat | Easy implementation; suitable for shell castings with limited access | Low efficiency; slower cooling rates |
| Indirect Cooling | Inserting chills or heat sinks | Effective for localized hot spots in shell castings | Requires additional components; potential for冷铁 interaction |
| Mold Modification | Redesigning cavity geometry | Prevents defects at source in shell castings | Limited by machining constraints |
| 保温 Coatings | Applying insulating materials | Controls solidification; improves feeding in shell castings | May increase cycle time |
| Heat Pipes | Phase-change heat transfer | Efficient with small temperature gradients in shell castings | High initial cost; design complexity |
| Temperature Control | Automated systems for模具 heating/cooling | Ensures thermal stability for consistent shell castings | Requires sophisticated equipment |
In my view, integrating these methods can significantly enhance the quality of shell castings. For example, combining water cooling for high-heat areas with保温 coatings for risers optimizes the solidification pattern. Mathematical modeling, such as finite element analysis (FEA), supports this by simulating temperature fields: $$ \rho C_p \frac{\partial T}{\partial t} = \nabla \cdot (k \nabla T) + Q_{\text{latent}} $$ where \( Q_{\text{latent}} \) accounts for latent heat release during solidification of shell castings. This allows预测 of defect-prone zones and tailored improvements.
Furthermore, material science plays a key role in shell castings. The use of铝合金 like Al-Si alloys requires careful control of composition to balance strength and castability. The phase diagram for Al-Si systems, often represented by equations like: $$ T_{\text{eutectic}} = 577^\circ \text{C}, \quad \text{Si\%} = 12.6\% $$ guides alloy selection for shell castings. Additionally, the mechanical properties of shell castings can be related to microstructure via the Hall-Petch equation: $$ \sigma_y = \sigma_0 + \frac{k_y}{\sqrt{d}} $$ where \( \sigma_y \) is yield strength, \( \sigma_0 \) is friction stress, \( k_y \) is a constant, and \( d \) is grain size. Refining grains through变质处理 improves the performance of shell castings under engine stresses.
Another aspect I explore is the economic and environmental impact of improving shell castings. By reducing defects, we minimize material waste and energy consumption, aligning with节能减排 goals. The lifecycle assessment of shell castings can be quantified using metrics like carbon footprint: $$ \text{CF} = \sum_{i} E_i \times \text{EF}_i $$ where \( E_i \) is energy input at stage \( i \) and \( \text{EF}_i \) is emission factor. Enhanced casting processes for shell castings lower this footprint by improving yield and reducing rework.
In conclusion, my analysis of turbocharger shell castings underscores the importance of advanced casting techniques. Through detailed process understanding, defect analysis, and targeted改进 measures, we can elevate the quality of shell castings, ensuring reliable turbocharger performance. The integration of tables and formulas, as presented, provides a comprehensive framework for optimizing shell castings. As automotive demand grows, continued innovation in shell castings will drive节能减排 efforts, enhance fuel economy, and contribute to a sustainable future. I am confident that by focusing on these aspects, shell castings will see wider adoption and further development in the automotive industry.
To recap, the casting of shell castings involves complex interactions between thermal management, material properties, and mold design. By employing methods like cooling systems and temperature control, we mitigate defects such as flash and porosity, leading to superior shell castings. The mathematical models and comparative tables offered here serve as tools for practitioners. Ultimately, refining shell castings is not just a technical endeavor but a commitment to environmental stewardship and industrial progress. I encourage ongoing research into shell castings to unlock new potentials in turbocharger technology and beyond.