
In the production of white cast iron grinding balls, it was observed that the use of local pig iron with high phosphorus content led to a significant decline in mechanical properties, particularly impact toughness. Additionally, internal shrinkage porosity increased drastically, resulting in product rejection. Given that many regional pig iron sources in our country exhibit elevated phosphorus levels, often exceeding 0.2%, exploring the feasibility of utilizing such high-phosphorus raw materials for manufacturing white cast iron components became imperative. This study investigates the state of phosphorus within white cast iron, its effects on impact toughness and hardness, and proposes methodologies to mitigate its adverse influences through casting techniques and heat treatment processes.
Our research was primarily conducted in a laboratory setting. The molten iron was prepared in a medium-frequency induction furnace, with chemical composition controlled within the typical range for white cast iron, specifically focusing on varying phosphorus levels. For each distinct phosphorus content, specimens were cast, and their impact toughness and Rockwell hardness were measured. Microstructural examination was performed using standard optical microscopy, with specific staining techniques employed to reveal phosphide networks. Furthermore, electron probe microanalysis (EPMA) was utilized to scrutinize the distribution and morphology of phosphorus within the microstructure.
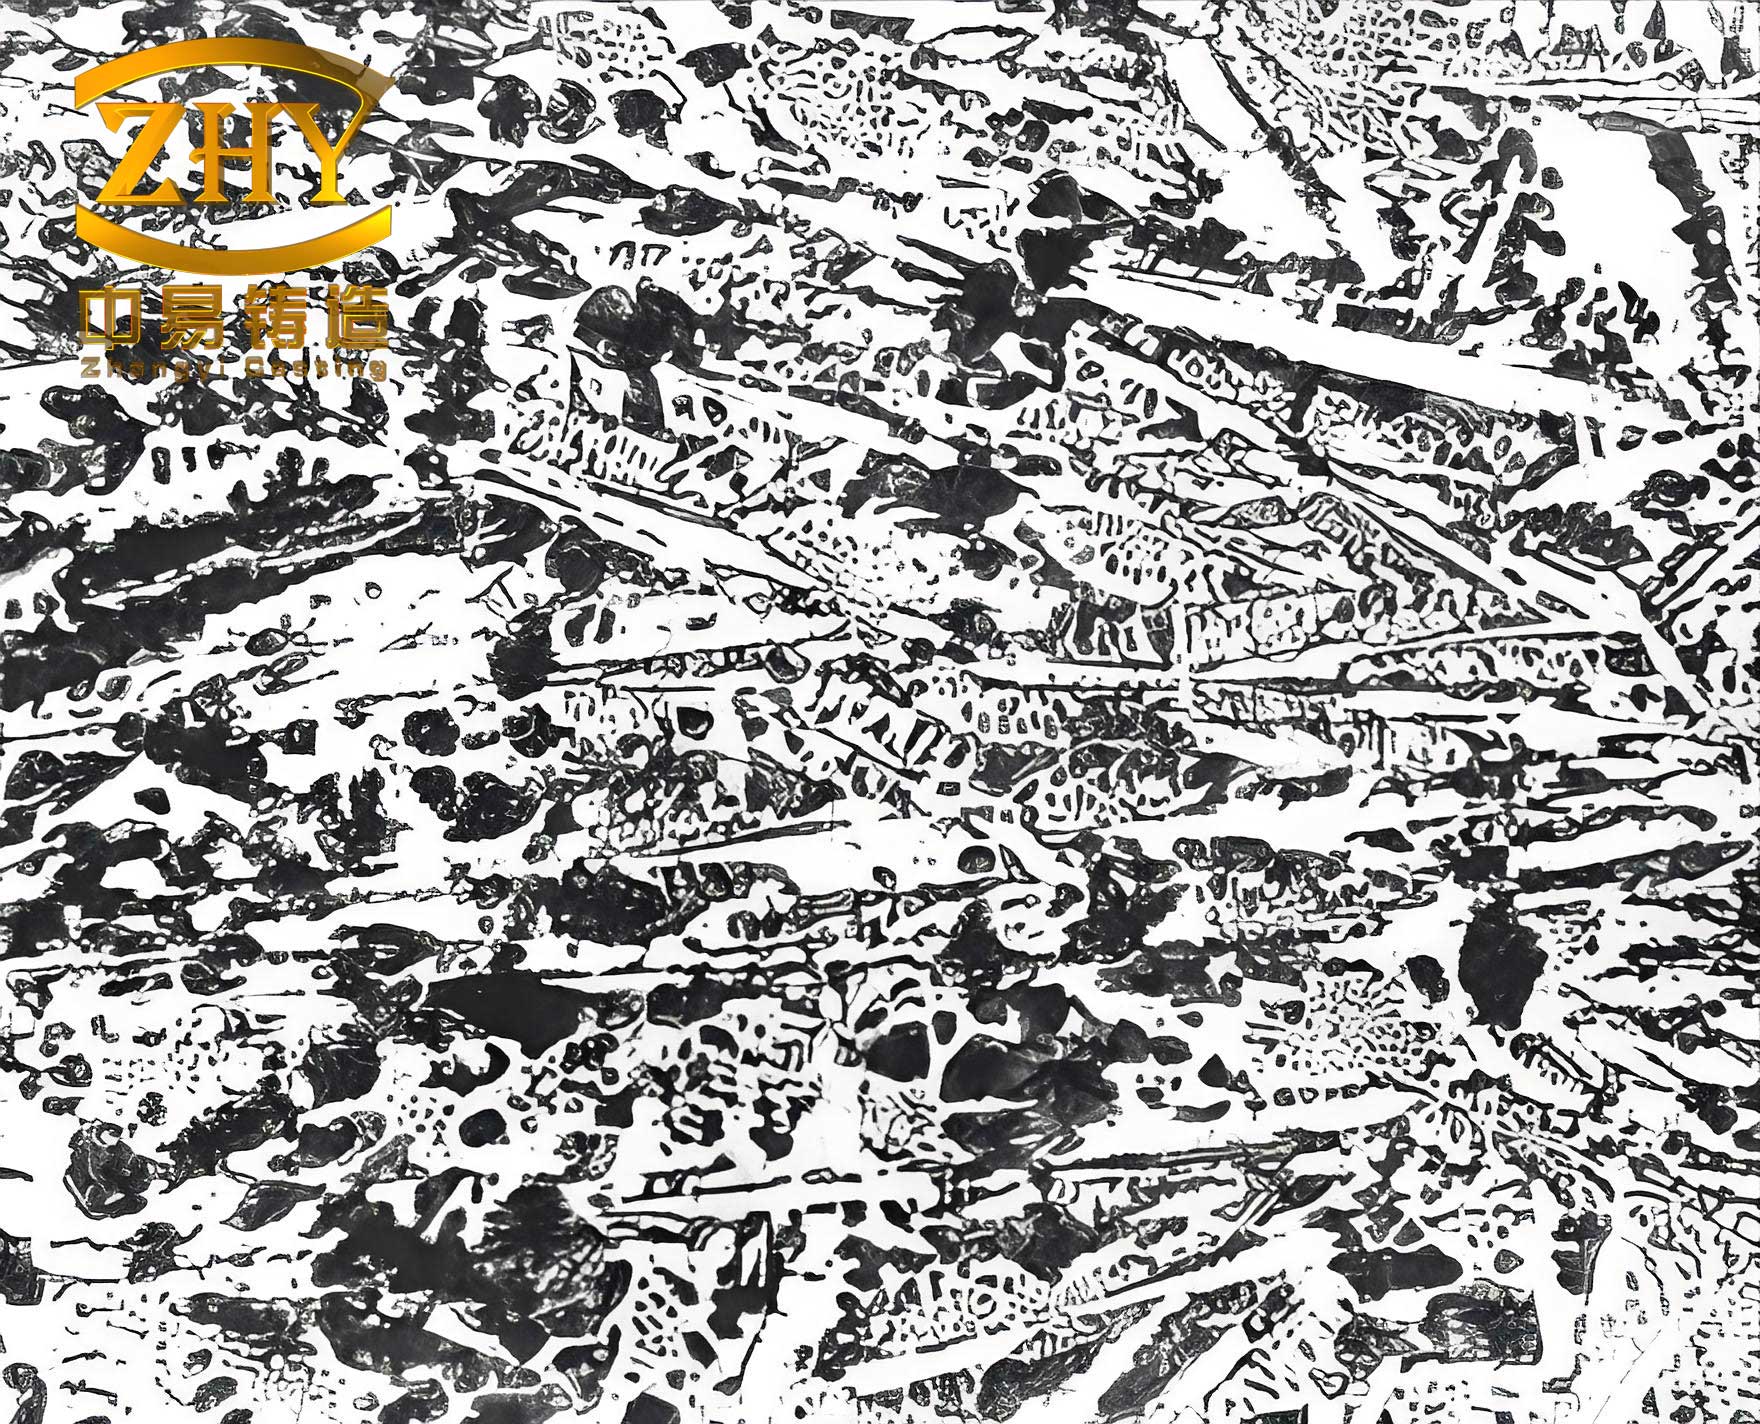
The experimental matrix involved phosphorus contents ranging from 0.03% to 0.45%. The base composition of the white cast iron was maintained as follows: Carbon (C) between 2.8% and 3.2%, Silicon (Si) between 0.6% and 1.0%, Manganese (Mn) between 0.8% and 1.2%, Chromium (Cr) between 1.5% and 2.0%, Molybdenum (Mo) between 0.3% and 0.6%, and Copper (Cu) between 0.8% and 1.2%. The variation in phosphorus (P) was the primary independent variable. The properties measured included Charpy impact toughness (a_k, in J/cm²) and Rockwell hardness (HRC). Each data point represents the average of three specimens to ensure statistical reliability.
| Phosphorus Content (wt.%) | As-Cast Impact Toughness, a_k (J/cm²) | As-Cast Hardness (HRC) | Observations (Microstructure) |
|---|---|---|---|
| 0.03 | 4.8 | 58.5 | Fine carbide network, minimal porosity |
| 0.12 | 4.2 | 58.0 | Increased central micro-shrinkage |
| 0.25 | 3.5 | 57.8 | Pronounced shrinkage porosity, no phosphide eutectic observed |
| 0.45 | 2.9 | 57.5 | Severe shrinkage defects, phosphorus uniformly distributed |
The relationship between phosphorus content and the as-cast properties of white cast iron can be summarized by the following empirical correlations derived from our data. For impact toughness:
$$ a_k(P) = a_{k0} – k_1 \cdot P – k_2 \cdot P^2 $$
where $a_{k0}$ is the impact toughness at negligible phosphorus, $k_1$ and $k_2$ are constants related to shrinkage and matrix embrittlement. For hardness, the variation was minimal, approximated by:
$$ HRC(P) = HRC_0 – \alpha \cdot P $$
with $\alpha$ being a small coefficient, indicating that phosphorus has a limited direct effect on hardness in the as-cast state.
Microstructural analysis revealed that increasing phosphorus content did not alter the fundamental matrix constitution or the distribution morphology and quantity of carbides. Even at 0.45% P, no classical phosphorus eutectic (such as steadite) was detected under optical microscopy. However, the volume of shrinkage porosity, particularly in the specimen centers, escalated markedly with rising phosphorus. This suggests that the deterioration in impact toughness is primarily attributable to the augmentation of shrinkage defects. Additionally, phosphorus dissolved in the austenite matrix enhances its inherent brittleness, contributing to the decline in toughness. The hardness remains relatively stable because the hard carbide phases dominate the hardness response, and phosphorus does not significantly affect their volume fraction.
To address the issue of shrinkage porosity, we investigated the effect of casting method. Identical melts were poured into both sand molds and metal molds. The comparative results are presented below.
| Casting Method | Phosphorus Content (wt.%) | Impact Toughness, a_k (J/cm²) | Hardness (HRC) | Notable Microstructural Features |
|---|---|---|---|---|
| Sand Mold | 0.03 | 4.8 | 58.5 | Coarser grains, some porosity |
| 0.45 | 2.9 | 57.5 | Extensive shrinkage, larger austenite grains | |
| Metal Mold | 0.03 | 5.5 | 56.0 | Refined grains, reduced porosity, higher retained austenite |
| 0.45 | 4.2 | 55.8 | Significantly less shrinkage, fine microstructure |
The metal mold casting process, due to its higher cooling rate, refines the primary crystallization, leading to finer grains. Moreover, the accelerated cooling suppresses the precipitation of carbon and alloying elements from supersaturated austenite, increasing its stability and lowering the martensite start (M_s) temperature. Consequently, the as-cast structure retains a greater amount of retained austenite. This results in a universal improvement in impact toughness for metal mold specimens compared to sand cast ones, albeit with a slight reduction in hardness. For instance, at 0.45% P, the impact toughness of metal mold white cast iron reached 4.2 J/cm², approximately 45% higher than its sand-cast counterpart. This demonstrates that metal mold casting is an effective technique to alleviate shrinkage defects and enhance the toughness of high-phosphorus white cast iron.
A critical aspect of this study was elucidating the state of phosphorus in white cast iron. Contrary to gray cast iron, where phosphorus eutectic typically appears at levels around 0.1%, our high-phosphorus white cast iron (up to 0.45% P) showed no such eutectic under optical examination. Electron probe microanalysis provided deeper insights. The EPMA scanning images indicated that phosphorus was uniformly distributed across both the matrix and the carbide phases. Only in isolated, last-to-solidify regions was minor phosphorus enrichment observed, but these areas were minuscule and not resolvable with conventional microscopy.
This behavior can be explained by considering solubility limits. In white cast iron, particularly alloyed white cast iron, the carbon and silicon contents are lower than in gray iron. Furthermore, alloying elements shift the eutectic point, reducing the carbon solubility in primary austenite. This allows phosphorus to remain in solution within both austenite and carbides during solidification. The solubility of phosphorus in austenite in the Fe-C-P system can be described by an empirical relation:
$$ C_P^{\gamma}(C, T) = C_{P0} \cdot \exp\left(-\frac{Q}{RT}\right) – \beta \cdot C_C $$
where $C_P^{\gamma}$ is the phosphorus solubility in austenite, $C_{P0}$ is a constant, $Q$ is an activation energy, $R$ is the gas constant, $T$ is temperature, $C_C$ is the carbon content, and $\beta$ is a coefficient. The lower carbon and silicon in white cast iron, combined with alloying effects, increase $C_P^{\gamma}$, preventing phosphorus rejection and subsequent eutectic formation. Thus, phosphorus in white cast iron exists primarily in solid solution, with negligible formation of detrimental phosphides at grain boundaries.
Given that the metal mold as-cast white cast iron exhibited higher toughness but lower hardness due to retained austenite, heat treatment was explored to optimize the performance. Instead of the energy-intensive austempering or quenching processes often used for white cast iron, we investigated direct tempering of the as-cast metal mold specimens. The tempering temperatures ranged from 200°C to 500°C, with holding times of 2 hours. Both single and double tempering cycles were evaluated.
The effect of single tempering temperature on the properties of high-phosphorus (0.45% P) white cast iron is graphically and quantitatively summarized. The response can be divided into three regimes:
- Low-Temperature Regime (Below 300°C): Insufficient driving force for transformation; properties remain near as-cast levels.
- Intermediate Regime (300°C to 450°C): Retained austenite decomposes into fine martensite or lower bainite; hardness increases, toughness decreases initially then may recover slightly as stress is relieved.
- High-Temperature Regime (Above 450°C): Over-tempering occurs; carbides coarsen, and transformed products become softer, leading to hardness drop.
The optimal single tempering for balancing hardness and toughness was found around 400°C. However, double tempering (e.g., 400°C for 2 hours, twice) yielded superior results by more completely eliminating casting and transformation stresses, allowing further transformation of retained austenite.
| Material Condition (0.45% P White Cast Iron) | Heat Treatment Process | Impact Toughness, a_k (J/cm²) | Hardness (HRC) | Microstructure Description |
|---|---|---|---|---|
| As-Cast (Metal Mold) | None | 4.2 | 55.8 | Martensite, retained austenite, carbides, minimal porosity |
| Tempered | 400°C × 2h (Single) | 3.8 | 58.5 | Tempered martensite, reduced retained austenite |
| Double Tempered | 400°C × 2h, twice | 4.1 | 59.0 | Fine tempered martensite, minimal retained austenite, carbides |
| Reference Low-P (0.03% P) | Austempered: 950°C quench + 250°C temper | 4.5 | 60.0 | Bainite/martensite matrix, carbides |
The performance of high-phosphorus white cast iron after metal mold casting and double tempering closely approximates that of low-phosphorus white cast iron subjected to conventional austempering. This indicates that high-phosphorus white cast iron is viable for applications like grinding balls. Moreover, the white cast iron exhibited high tempering stability; even after double tempering at 450°C, hardness remained around 58 HRC, suggesting potential for tooling applications where extreme toughness is not paramount.
The mechanisms underlying the tempering response involve the decomposition of retained austenite. The transformation kinetics can be modeled using an Avrami-type equation:
$$ f = 1 – \exp(-k t^n) $$
where $f$ is the fraction transformed, $t$ is time, $k$ is a rate constant dependent on temperature and composition, and $n$ is an exponent. For high-phosphorus white cast iron, the presence of phosphorus in solid solution likely alters $k$, enhancing stability. The final hardness after tempering is a function of the matrix hardness and carbide dispersion, expressible as:
$$ HRC_{final} = HRC_{matrix} + \Delta HRC_{carbides} – \Delta HRC_{over-tempering} $$
where each term depends on tempering parameters.
In conclusion, our investigation into phosphorus in white cast iron reveals several key findings. Firstly, phosphorus, up to 0.45%, does not form classical phosphide eutectics in alloyed white cast iron. Instead, it dissolves uniformly in the matrix and carbides. The primary detriment of phosphorus to as-cast properties is the exacerbation of shrinkage porosity and a contribution to matrix embrittlement, leading to reduced impact toughness. Hardness is less affected. Secondly, metal mold casting effectively mitigates shrinkage defects, refines microstructure, and enhances toughness by promoting retained austenite, though at a slight hardness cost. Thirdly, a direct tempering treatment, particularly double tempering in the range of 300-450°C, can transform retained austenite, relieve stresses, and yield a balanced combination of hardness and toughness. This process is more energy-efficient than traditional quenching methods.
Therefore, the utilization of high-phosphorus local pig iron for producing white cast iron components is technically feasible when combined with metal mold casting and appropriate tempering. The resulting white cast iron exhibits properties comparable to low-phosphorus grades, offering a cost-effective and sustainable alternative for anti-wear applications. Furthermore, the high tempering stability of this white cast iron opens avenues for its use in certain tooling contexts. Future work could explore the wear resistance under various conditions and the effects of other residual elements commonly found in local pig irons on the performance of white cast iron.
The study underscores the importance of process adaptation in materials engineering. By understanding the specific role of phosphorus in white cast iron and implementing tailored casting and heat treatment strategies, the limitations imposed by raw material impurities can be overcome, expanding the applicability of white cast iron in diverse industrial sectors.