
The inherent brittleness of white cast iron has historically restricted its application to wear-resistant components subjected to minimal or no impact. The primary source of this brittleness is widely attributed to the continuous, brittle network of eutectic carbides within its microstructure. This network effectively segments the metallic matrix, providing easy paths for crack initiation and propagation under stress, leading to catastrophic failure with negligible macroscopic plastic deformation. Therefore, the key to enhancing the toughness of white cast iron lies in modifying the morphology, size, and distribution of these carbides to disrupt their continuous network.
Traditional approaches to address this issue have included alloying, melt inoculation, and post-casting heat treatments. While these methods can offer some improvements, their effectiveness in achieving a significant breakthrough in toughness has often been limited. A paradigm-shifting concept is the application of thermomechanical processing—forging—to white cast iron, a material traditionally deemed “unforgeable.” Recent exploratory work has demonstrated that certain compositions of white cast iron possess unexpected forgeability, with reports of single-pass deformation exceeding 80% under suitable conditions. This revelation opens a new frontier for dramatically enhancing the comprehensive mechanical properties of white cast iron through controlled deformation and subsequent heat treatment, a process broadly termed thermomechanical treatment.
This work systematically investigates a multi-stage processing route for medium-manganese white cast iron, combining melt inoculation, forging, and post-forging heat treatment. The objective is to comprehensively analyze the influence of each processing step on the microstructure evolution and the resulting mechanical properties, with the ultimate goal of developing an effective methodology for the strengthening and toughening of white cast iron.
1. Material Preparation and Experimental Procedures
1.1 Melting and Casting
The medium-manganese white cast iron was melted in a coreless medium-frequency induction furnace. The target chemical composition of the cast material is detailed in Table 1.
| Element | C | Si | Mn | P | S | Fe |
|---|---|---|---|---|---|---|
| Content | 2.8 – 3.2 | 1.5 – 2.0 | 5.0 – 6.0 | < 0.1 | < 0.05 | Bal. |
To modify the as-cast carbide structure, a manganese-based inoculant was employed. The inoculation process involved two stages: the first addition was made approximately 10 minutes before tapping the furnace, and the second addition was made in the ladle during tapping. The melt was poured at a temperature of 1380°C ± 20°C into green sand molds. The dimensions of the cast specimens for mechanical testing are listed in Table 2.
| Specimen Type | Dimensions (mm) |
|---|---|
| Bending (Cast) | φ20 x 250 |
| Impact (Cast) | 10 x 10 x 55 (unnotched) |
1.2 Forging Process
The cast specimens were subjected to hot forging. The pre-forging heating was conducted in a box-type furnace following the thermal cycle shown in Figure 1 (conceptual), ensuring uniform heating and minimizing thermal shock. Forging was performed using an air hammer, with the goal of achieving a significant reduction in a single forging pass. The dimensions of specimens before and after forging are summarized in Table 3.
Conceptual Forging Heating Cycle: The heating profile involved a slow ramp to 600°C for stress relief, followed by a faster ramp to the forging temperature of 1050°C – 1100°C, holding for sufficient time to achieve temperature homogeneity throughout the cross-section.
| Specimen Type | Pre-forging Dimensions | Post-forging Dimensions | Approx. Reduction |
|---|---|---|---|
| Bending | φ20 mm | φ14 mm | ~50% |
| Impact | 15 x 15 mm cross-section | 10 x 10 mm cross-section | ~55% |
1.3 Heat Treatment Processes
Various heat treatment sequences were applied to the forged white cast iron to optimize the final microstructure. The specific schedules investigated are listed in Table 4.
| Schedule No. | Heat Treatment Process Description |
|---|---|
| 1 | Direct quenching after forging + 280°C temper. |
| 2 | Air cooling after forging, reheat to 850°C, quench + 280°C temper. |
| 3 | Air cooling after forging, reheat to 950°C, quench + 280°C temper. |
| 4 | Air cooling after forging, reheat to 1000°C, quench + 280°C temper. |
| 5 (Reference) | As-cast state + 950°C normalizing. |
2. Experimental Results and Microstructural Analysis
2.1 Effect of Inoculation on As-Cast Structure
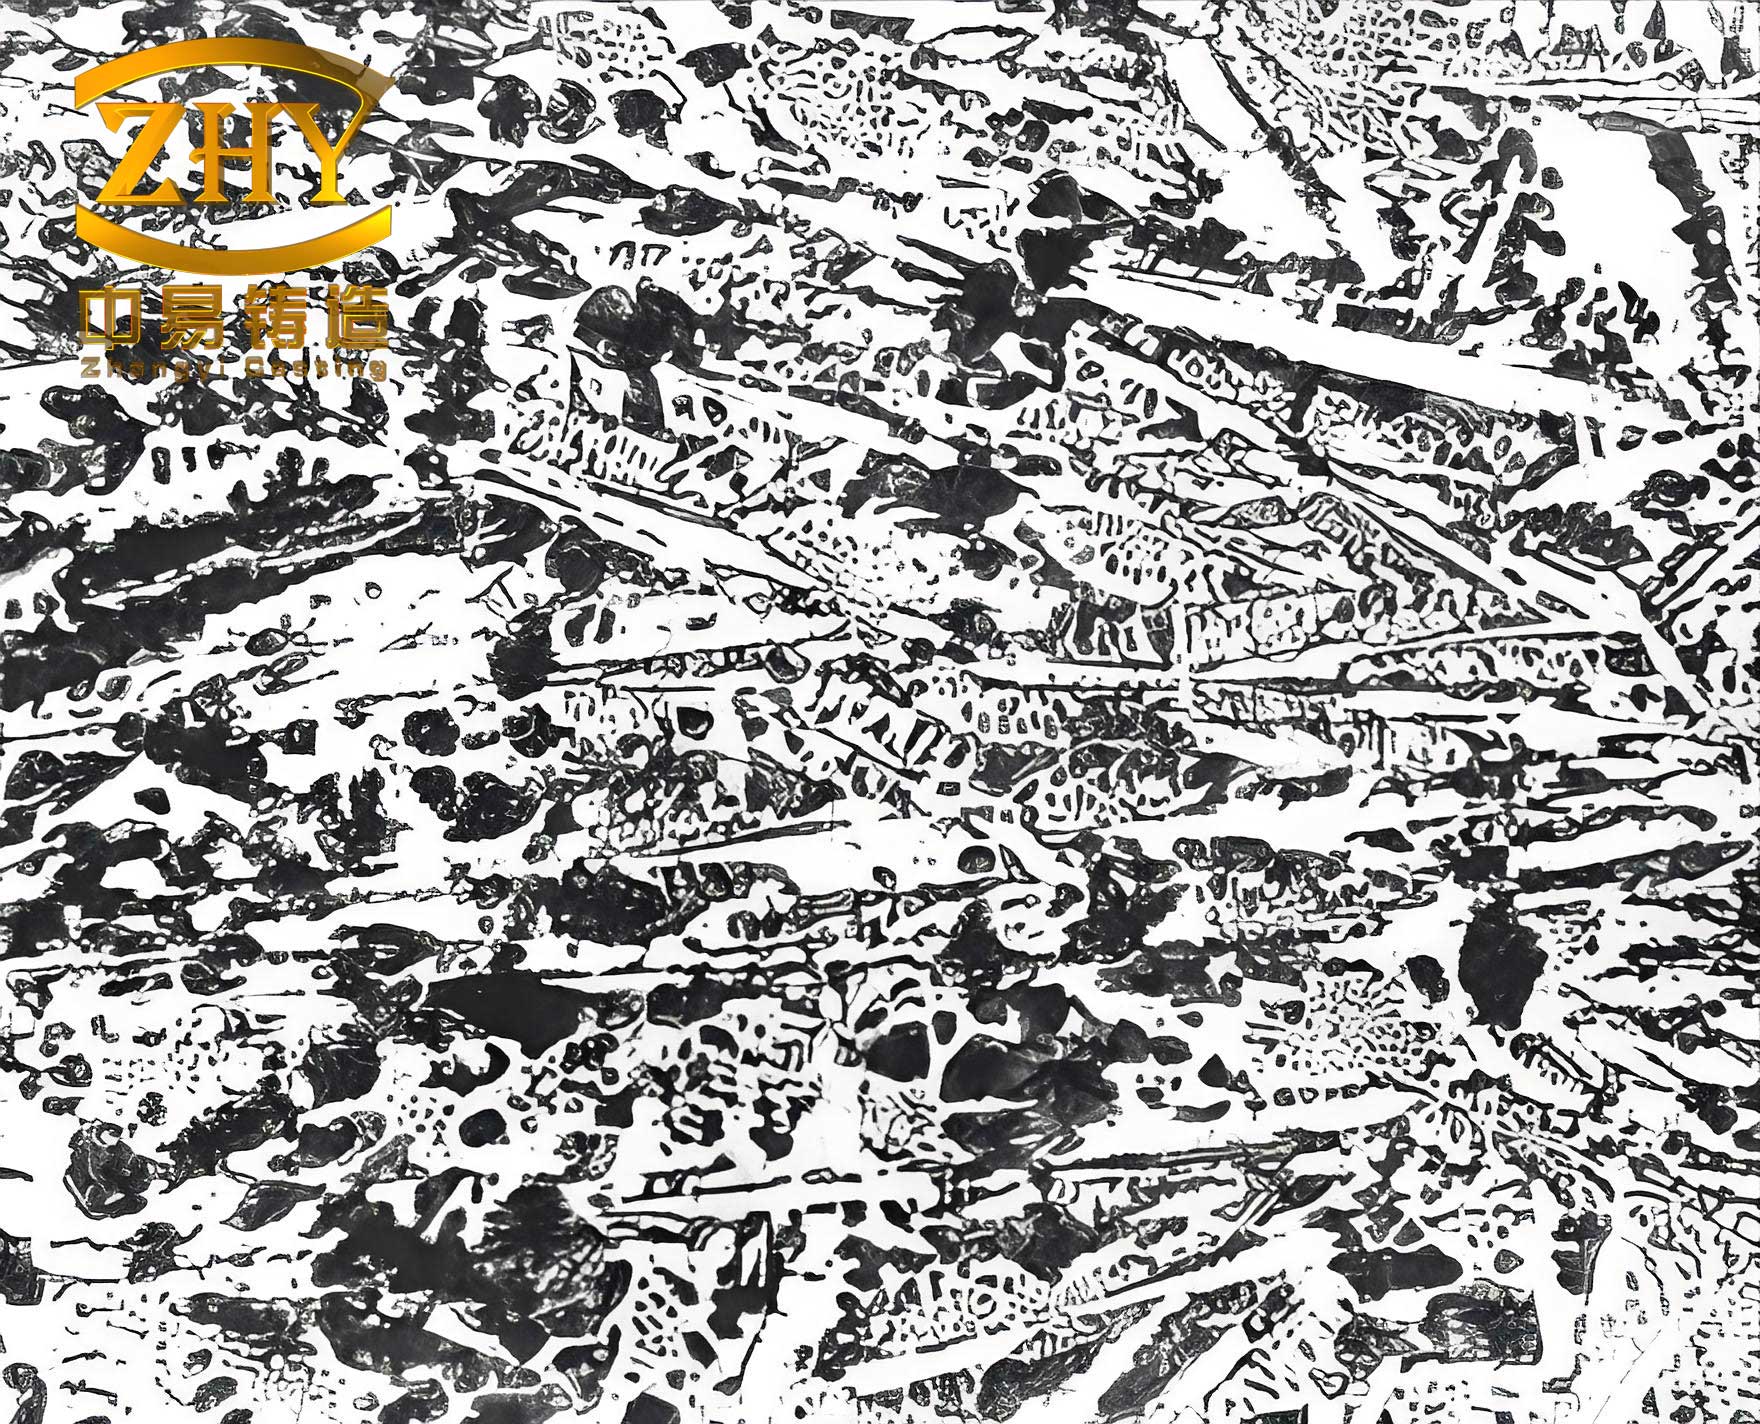
Metallographic examination revealed that the manganese-based inoculation significantly refined the eutectic carbide network in the as-cast white cast iron. Compared to a non-inoculated structure, the carbides appeared more fragmented and less interconnected. This modification enhances the continuity of the metallic matrix, which is a prerequisite for improved toughness, as it allows for greater load transfer and potential for plastic deformation within the matrix before fracture initiates at the carbides.
2.2 Forgeability and Microstructural Evolution During Deformation
The medium-manganese white cast iron exhibited excellent hot workability. Under the specified heating regime, the material could be forged without surface cracking or internal failure. The most profound microstructural change induced by forging was the physical breakdown of the continuous carbide network. The applied compressive strain fragmented the brittle carbides, aligning them along the direction of metal flow. This process drastically reduces the mean free path for crack propagation and transforms the microstructure from one dominated by a continuous brittle skeleton to one consisting of discrete carbide particles or short rods within a metallic matrix. The degree of this refinement increases with the applied deformation ratio.
2.3 Microstructure After Thermomechanical Treatment
The microstructure following the combined forging and heat treatment (Schedules 1-4) was markedly different from the traditionally heat-treated cast material (Schedule 5). In the thermomechanically processed white cast iron, the carbides were uniformly distributed as fine, isolated particles. The matrix itself, depending on the specific heat treatment schedule, could consist of tempered martensite, lower bainite, or a mixture of transformation products, providing a strong and tough support for the hard carbides. In contrast, the normalized cast sample (Schedule 5) still retained traces of the original carbide network, albeit somewhat spheroidized, resulting in inferior mechanical properties.
3. Mechanical Properties and Fractography
The mechanical properties, including hardness, impact toughness, and flexural strength, were evaluated for the material under different processing conditions. A summary of the key results is presented in Table 5.
| Processing Condition | Hardness (HRC) | Impact Toughness (J/cm²) | Flexural Strength (MPa) | Notes |
|---|---|---|---|---|
| As-Cast + Normalized (Ref.) | 52 – 55 | 4.5 – 5.5 | ~650 | Brittle, networked carbides |
| Forged + Direct Quench & Tempered (Schedule 1) | 58 – 60 | 9.0 – 11.0 | ~1200 | Good combination of hardness and toughness |
| Forged, Reheated (850°C), Q&T (Schedule 2) | 56 – 58 | 12.0 – 14.0 | ~1350 | Optimized toughness |
| Forged, Reheated (1000°C), Q&T (Schedule 4) | 48 – 50 | 8.0 – 9.5 | ~1100 | Lower hardness, moderate toughness |
The data clearly demonstrates the dramatic improvement achievable through thermomechanical processing. For instance, Schedule 2 (forging + reheating to 850°C, quenching, and tempering at 280°C) resulted in a white cast iron with an impact toughness over 200% higher than the reference cast-and-normalized material, while maintaining a high hardness level suitable for wear applications. The flexural strength was also more than doubled.
3.1 Fracture Mechanism Analysis
Macroscopic examination of fracture surfaces showed a distinct difference. The fracture surface of the as-cast and normalized white cast iron was coarse and crystalline, indicative of a purely brittle cleavage fracture. In contrast, the fracture surface of the forged and heat-treated white cast iron was much finer and had a greyish, fibrous appearance, suggesting a more ductile fracture mode.
Scanning Electron Microscopy (SEM) fractography provided conclusive evidence. The fracture surface of the thermomechanically treated white cast iron revealed a high density of micro-dimples (ductile tear ridges) surrounding the carbide particles. This is a classic signature of microvoid coalescence, a fracture mechanism involving nucleation, growth, and coalescence of voids, which requires substantial localized plastic deformation in the matrix. The presence of these dimples confirms that the matrix in the processed white cast iron is capable of significant plastic flow, thereby absorbing considerable energy before fracture. The critical event is now the decohesion at the carbide/matrix interface or fracture of the carbide particles themselves, rather than unchecked propagation along a pre-existing brittle network.
The transition in fracture mode can be conceptually related to the Griffith criterion for brittle fracture. The original continuous carbide network acts as a large, sharp flaw of length ‘2c’. The fracture stress $\sigma_f$ is given by:
$$\sigma_f \approx \frac{K_{IC}}{\sqrt{\pi c}}$$
where $K_{IC}$ is the fracture toughness of the carbide phase, which is very low. The large effective flaw size ‘c’ of the network leads to a very low $\sigma_f$. Forging reduces the effective flaw size to the dimension of individual carbide particles or the spacing between them, dramatically increasing the stress required for crack propagation.
3.2 Strengthening Mechanisms
The enhancement in strength, particularly yield and flexural strength, arises from multiple synergistic mechanisms activated by the thermomechanical process:
- Grain Refinement (Hall-Petch Strengthening): The forging process and subsequent phase transformation refine the austenite grain size, leading to a stronger matrix. The contribution to yield strength $\Delta \sigma_{HP}$ is:
$$\Delta \sigma_{HP} = k_y \cdot d^{-1/2}$$
where $k_y$ is a material constant and $d$ is the average grain diameter. - Dislocation Strengthening: The hot deformation introduces a high density of dislocations, which are partially retained or rearranged during subsequent cooling and heat treatment, contributing to strength.
- Precipitation/Dispersion Strengthening: The finely fragmented and uniformly distributed carbide particles act as potent obstacles to dislocation motion. The strengthening increment $\Delta \sigma_{part}$ for bypassing non-shearable particles (Orowan mechanism) is proportional to:
$$\Delta \sigma_{part} \propto \frac{Gb}{\lambda}$$
where $G$ is the shear modulus, $b$ is the Burgers vector, and $\lambda$ is the inter-particle spacing. Forging decreases $\lambda$, thereby increasing strength. - Transformation Strengthening: The quenching process produces a strong martensitic or bainitic matrix.
The overall strength $\sigma_y$ can be approximated by a linear superposition of these contributions:
$$\sigma_y = \sigma_0 + \Delta \sigma_{HP} + \Delta \sigma_{disl} + \Delta \sigma_{part} + \Delta \sigma_{trans}$$
where $\sigma_0$ is the lattice friction stress.
4. Discussion: The Role of Integrated Processing
The superior properties of the final product are not the result of a single step but the integration of three critical stages: inoculation, forging, and heat treatment. Each stage plays a specific and indispensable role in the strengthening and toughening of white cast iron.
Inoculation serves as the crucial first step by modifying the morphology of the eutectic carbides during solidification. While it may not completely eliminate the network in the as-cast state, it makes it more susceptible to fragmentation during subsequent forging by promoting a finer, less robust carbide skeleton. It prepares the initial microstructure for successful thermomechanical processing.
Forging (Thermomechanical Processing) is the transformative stage. It physically destroys the continuity of the carbide network, which is the root cause of brittleness. It simultaneously refines the microstructure, aligns the carbide fragments, and work-hardens the matrix. This stage fundamentally changes the nature of the material from a brittle composite with a continuous ceramic network to a ductile-phase composite where hard particles are dispersed in a continuous metallic matrix. The forgeability of this specific medium-manganese white cast iron is a key enabler.
Post-Forging Heat Treatment allows for precise control over the final matrix microstructure and the state of the carbides. Processes like quenching and tempering develop a high-strength, tough matrix (e.g., tempered martensite). The tempering step relieves internal stresses introduced during forging and quenching, further enhancing toughness and dimensional stability. The choice of reheating temperature (e.g., 850°C vs. 1000°C) affects carbide dissolution and re-precipitation, austenite grain size, and hardenability, allowing for property tailoring.
The combination of Schedule 2 (forging + 850°C reheat, quench, and temper) proved particularly effective. The 850°C austenitizing temperature is likely high enough to achieve a homogeneous austenitic structure with sufficient carbon in solution for good hardenability, but low enough to prevent excessive austenite grain growth and excessive carbide dissolution, which could lead to coarser carbides upon quenching. This balance yields an optimal combination of a fine-grained, strong matrix and a fine dispersion of hard carbides.
5. Conclusions
Based on the comprehensive investigation into the processing, microstructure, and properties of medium-manganese white cast iron, the following conclusions can be drawn:
- Manganese-based melt inoculation is an effective method for modifying the as-cast carbide morphology in white cast iron, resulting in a finer and less continuous eutectic network. This modification improves the continuity of the metallic matrix and provides a more favorable starting microstructure for subsequent deformation processing.
- Contrary to traditional belief, the investigated medium-manganese white cast iron exhibits excellent hot forgeability under appropriate heating conditions. The material can withstand significant plastic deformation (≥50% reduction in a single pass) without failure, enabling industrial-scale thermomechanical processing.
- The application of hot forging is profoundly effective in breaking the continuous carbide network, which is the primary source of brittleness in white cast iron. The degree of microstructural refinement, including carbide fragmentation and matrix grain refinement, increases with the applied deformation ratio.
- Thermomechanical treatment, integrating controlled forging with optimized post-forging heat treatment (e.g., reheating to 850°C, quenching, and tempering at 280°C), is the most effective methodology discovered for the simultaneous strengthening and toughening of white cast iron. This process can more than double the impact toughness and flexural strength compared to conventionally processed cast material, while retaining high hardness suitable for wear-resistant applications.
- The dramatic improvement in properties is attributed to a fundamental change in the microstructure and fracture mechanism. The processed white cast iron transitions from a brittle structure with a continuous carbide network to a ductile-phase composite with fine, isolated carbides in a strong, tough matrix. Fracture occurs via a microvoid coalescence mechanism, requiring substantial energy absorption, as opposed to cleavage along brittle carbides.
This work demonstrates that through an integrated approach of inoculation, forging, and heat treatment, the property limitations of white cast iron can be substantially overcome. This paves the way for expanding its applications into more demanding service conditions where a combination of high wear resistance and improved toughness is required, potentially enabling substitution for more expensive or less wear-resistant materials in various engineering components.