
In the context of demanding rapid prototyping for critical industrial components, my team was recently tasked with delivering three sample shell castings for a large explosion-proof electric motor housing. The delivery window was an aggressive twenty days, a timeline that rendered conventional pattern-making and tooling routes impractical. We strategically decided to leverage additive manufacturing, specifically binder jetting 3D printing for sand molds and cores, to meet this challenge. This article details our first-person experience and methodology in producing these complex shell castings.
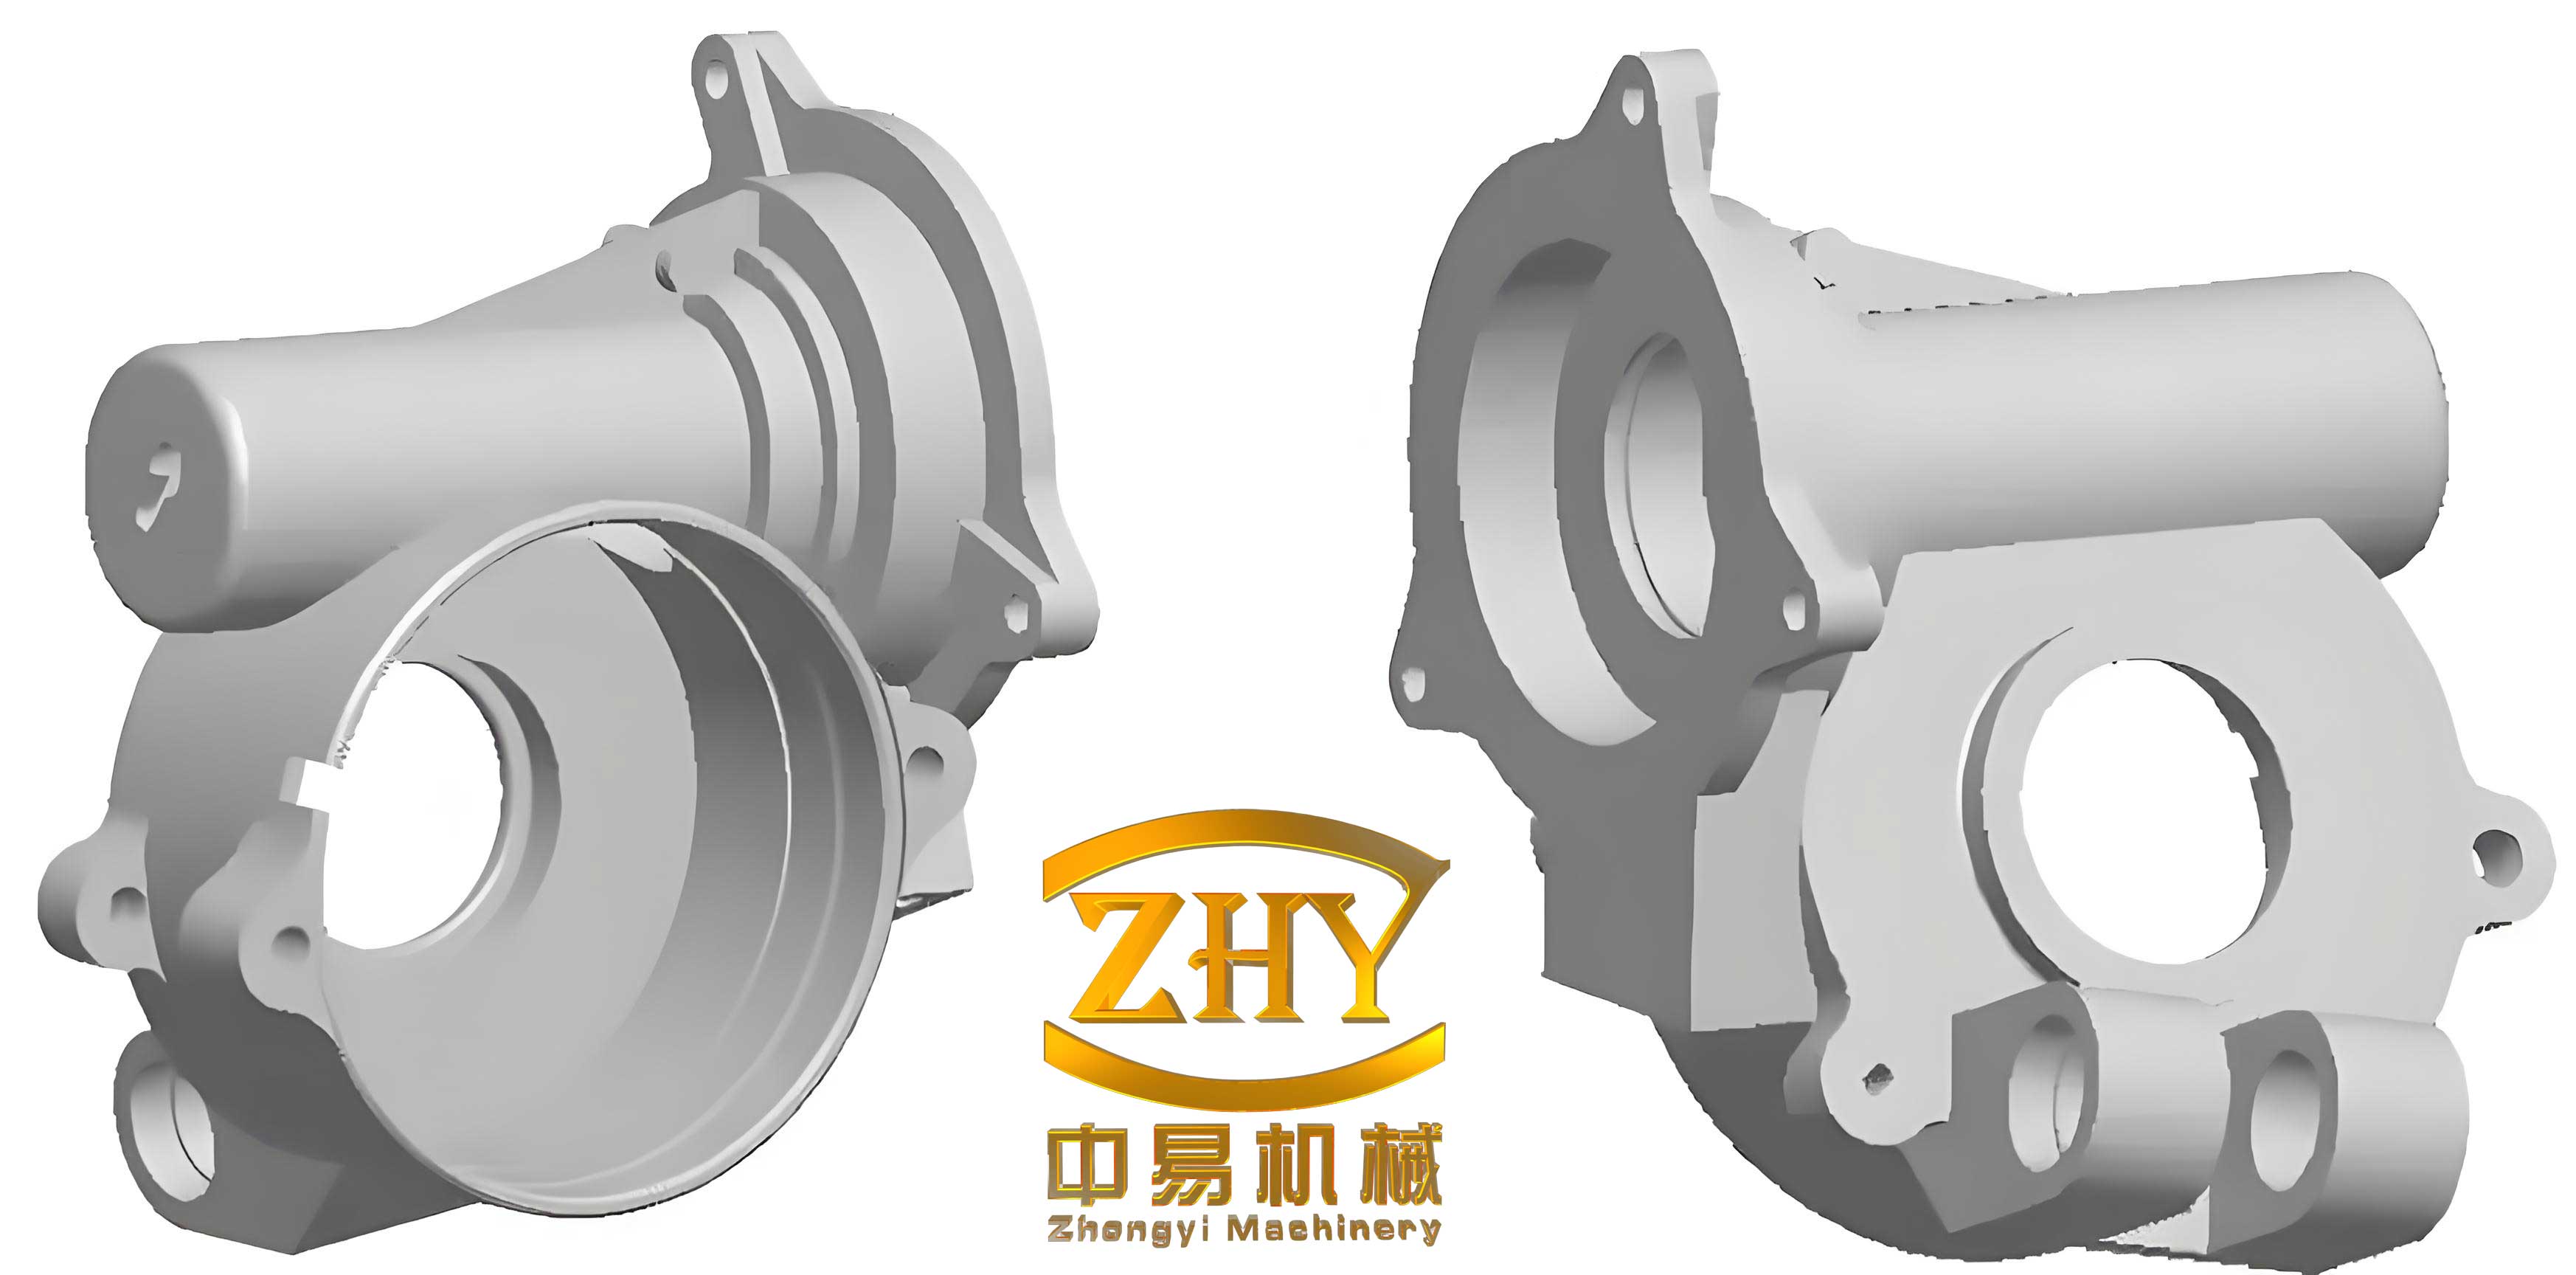
The component in question is a substantial shell casting, designated with the material grade HT250 (a gray iron). The primary dimensions of the shell casting are 1,412 mm in length, 836 mm in width, and 796 mm in height, with a main wall thickness of 25 mm. The design features numerous cooling fins radiating from the main body, which taper from a root thickness of 11 mm down to a delicate 5 mm at their tips, with heights varying between 80 mm and 120 mm. These fins are dual-purpose, serving both as functional heat-dissipation structures and critical aesthetic surfaces. This combination presented a significant founding challenge: ensuring complete fill of these thin sections required an elevated pouring temperature, while simultaneously meeting stringent dimensional accuracy requirements of CT Grade 9 per GB/T 6414-1999. The internal geometry included five intricate airway passages where any core burn-in or penetration would be nearly impossible to clean, mandating flawless core surface quality.
Our production was based on a domestic 2215 model 3D printer with a maximum build envelope of 2,200 mm × 1,500 mm × 700 mm. This constraint directly informed our parting strategy for the shell casting molds.
Casting Process Design for the Shell Casting
The axi-symmetric nature of the main shell casting body suggested a vertical orientation for pouring, aligning the part’s central axis with the direction of gravity. This positioning offered the most straightforward gating and feeding approach for a part of this geometry.
We opted for a semi-pressurized gating system. The key ratios for the cross-sectional areas were designed as follows:
$$ \sum F_{sprue} : \sum F_{runner} : \sum F_{ingate} = 1 : 1.5 : 0.8 $$
The sprue was introduced at the top flange of the shell casting. The runner was arranged in a spiral pattern on the upper plane of the mold, and ingates were taken from the bottom outer side of this runner into the mold cavity. This top-gating design facilitated rapid mold filling, which was crucial for the thin fins. Given the relatively uniform wall thickness of the main body (23-28 mm), extensive feeding was not the primary concern. However, we placed small liquid-supply risers exclusively on the thickest sections of the top flange. The total venting area was set to be 1.5 times the choke area to ensure smooth expulsion of air and gases. A ceramic filter was placed at the sprue well to trap slag. Crucially, all gating and risering were located on machined surfaces of the final shell casting, allowing for clean removal by machining with minimal secondary finishing. This design yielded an excellent casting yield of over 90% for these substantial shell castings.
3D-Printed Sand Mold Design and Assembly
The size of the shell casting necessitated a multi-part core assembly strategy to fit within the printer’s build volume. To preserve the critical surface finish and avoid parting lines on the external fins, we designed the entire outer mold segment containing the fin impressions as single, large cores. The internal cavity of the shell casting, measuring 744 mm in one dimension, exceeded the printer’s Z-height. Furthermore, printing large, curved surfaces along the vertical build direction can lead to a stair-stepping effect. Therefore, we split the mold along the axial (vertical) direction of the shell casting.
We utilized 100/140 mesh silica sand with domestic bonding agents. The printing parameters were meticulously set to achieve a balance between speed, resolution, and sand compaction, as summarized below:
| Parameter | Setting |
|---|---|
| Layer Thickness | 0.32 mm |
| Print Resolution | 0.10 mm |
| Recoater Blade Angle | 0.2° |
| Print Head Speed | 280 m/s |
| Sand Spreader Vibration | 3800 rpm |
| Build Chamber Temperature | 23 ± 5 °C |
Post-printing, the cores were thoroughly cleaned using compressed air at 0.5 MPa. A water-based alumina coating with a Baume gravity of 50 ± 2 °Bé was applied via flow coating to all mold cavity surfaces to prevent metal penetration, especially in the delicate airway cores. The coated molds were then dried at 80°C for a minimum of 4 hours.
Assembly was performed on a rigid, flat steel plate. The sequence began with stacking and securing the internal cavity cores. The large outer shell cores (with fin impressions) were then positioned around them. Finally, the top closing cores (containing the gating system) were placed. The assembly was diagonally clamped, and the surrounding volume was backed up with resin-bonded sand to resist metallostatic pressure during the pour of the shell castings.
Melting and Pouring for the Gray Iron Shell Castings
The chemical composition target for the HT250 shell castings was carefully chosen to balance fluidity for thin-section filling with the required mechanical properties. The charge makeup and final chemistry are shown in the table below.
| Aspect | Detail |
|---|---|
| Charge Composition | 5-15% Pig Iron + 50-70% Steel Scrap + 30-35% Returns |
| Target Chemistry | C: 3.2-3.3%, Si: 1.9-2.1%, Mn: 0.55-0.75%, P: <0.10%, S: 0.065-0.105% |
| Inoculation | 0.15% addition of 75% FeSi |
| Pouring Temperature | 1410 ± 10 °C (measured in pouring basin) |
| Pouring Time | 45 seconds |
The relatively high carbon equivalent, calculated approximately using the formula for gray iron, promoted excellent fluidity:
$$ CE \approx \%C + 0.3(\%Si + \%P) $$
For our target composition, this yields:
$$ CE \approx 3.25 + 0.3(2.0 + 0.08) = 3.25 + 0.624 = 3.874 $$
This high CE was instrumental in successfully filling the thin fins of the shell castings. The inoculation treatment with FeSi was essential for promoting a uniform Type A graphite distribution and ensuring the desired strength in the final shell castings. The pouring parameters were controlled to ensure a smooth, non-turbulent fill.
Results and Validation of the 3D-Printed Shell Castings
The molds were poured within the same day of assembly to prevent moisture pick-up. After a 24-hour cooling period, the shell castings were shaken out. The benefits of the integrated gating/risering design on machined surfaces became immediately apparent: removal of this hardware was straightforward, and the resulting shell castings required virtually no grinding or finish work on the external surfaces. Total cleaning time was less than one hour per shell casting.
Visual inspection of the first shell casting revealed excellent surface finish with complete fill of all complex features, including the challenging thin fins. Dimensional checks confirmed the overall accuracy met the CT 9 grade requirement. Critically, the internal airway passages were clean and free from any adherence of sand, validating the efficacy of the core coating process for these shell castings.
Technical Advantages and Quantitative Analysis
The success of this project highlights several key advantages of using 3D printing for complex shell castings, which can be summarized quantitatively:
1. Lead Time and Cost Elimination: The total cycle time from digital model to finished shell casting was under 20 days. This bypassed weeks or months typically required for pattern manufacturing. The cost savings from eliminating hard tooling for a low-volume prototype run are substantial and can be modeled as:
$$ Savings_{tooling} = C_{pattern} + C_{coreboxes} + T_{lead\_time} * C_{delay} $$
Where \( C_{pattern} \) and \( C_{coreboxes} \) are the capital costs of pattern equipment, \( T_{lead\_time} \) is the extended project time, and \( C_{delay} \) is the cost of delay per unit time.
2. Enhanced Design Freedom and Yield: The ability to print complex cores allowed us to design the gating system optimally within the 3D space above the shell casting, contributing directly to the high yield. The yield \( Y \) is defined as:
$$ Y = \frac{W_{casting}}{W_{total\_poured}} \times 100\% $$
Our achieved yield of >90% for these shell castings is exceptionally high for a complex, one-off production.
3. Dimensional Integrity: The accuracy of the shell castings stems from the digital process chain and rigid sand cores. Dimensional deviation \( \delta \) can be related to printer resolution \( R_p \) and process parameters \( k \):
$$ \delta \propto f(R_p, k) $$
With our parameters (0.10 mm resolution, 0.32 mm layer), the as-printed cores provided a foundation that easily met the CT9 tolerance band for the large shell castings.
4. Metallurgical Consistency: The controlled, rapid filling from the top-gated system minimized temperature gradients during solidification of the shell castings. The solidification time \( t_s \) for a section of thickness \( d \) can be approximated by Chvorinov’s rule:
$$ t_s = k \left( \frac{V}{A} \right)^n = k \cdot (d)^n $$
where \( V \) is volume, \( A \) is surface area, and \( k \) and \( n \) are constants. For plate-like sections of the shell castings (main wall and fins), the modulus \( V/A \approx d/2 \). Our uniform wall design and pouring practice helped ensure consistent solidification conditions, promoting uniform microstructure throughout the shell castings, which is critical for their performance in service.
In conclusion, the adoption of binder jetting 3D printing technology for sand mold production proved to be a decisive and successful strategy for the rapid manufacture of high-quality, large explosion-proof motor shell castings. The process enabled unprecedented flexibility in gating design, eliminated traditional tooling, ensured exceptional dimensional accuracy, and facilitated the casting of complex thin-wall features. This project serves as a compelling demonstration of how additive manufacturing is transforming the prototyping and low-volume production paradigm for critical, heavy-section shell castings, offering a viable pathway that combines speed, quality, and cost-effectiveness.