
In the field of heavy industry, the production of high-integrity shell castings, such as turbine shells for gas turbines, represents a significant technological challenge. These components are critical in energy generation and aerospace applications, where performance and reliability are paramount. As a casting engineer involved in this project, I will elaborate on the comprehensive approach we developed to manufacture complex shell castings, focusing on a specific turbine shell. The process integrates advanced casting techniques, material science, and rigorous quality control to overcome inherent difficulties like dimensional accuracy, surface defects, and internal integrity. Throughout this discussion, the term “shell castings” will be emphasized to highlight the broader applicability of these methods.
The turbine shell casting in question serves as a key part of the combustion chamber in gas turbines, directing airflow, supporting rotational components, and maintaining structural integrity. Its complex geometry features multiple thin-walled sections and narrow passages, making it prone to defects during casting. The material is a ferritic heat-resistant steel, 15Cr1Mo1V, with specific chemical requirements to withstand high temperatures and stresses. Our goal was to localize production, reducing reliance on expensive imports, by devising a robust casting process. This involved addressing several critical aspects: dimensional control, surface quality, internal soundness, and deformation prevention. The following sections detail our solutions, supported by tables and formulas to summarize key parameters.
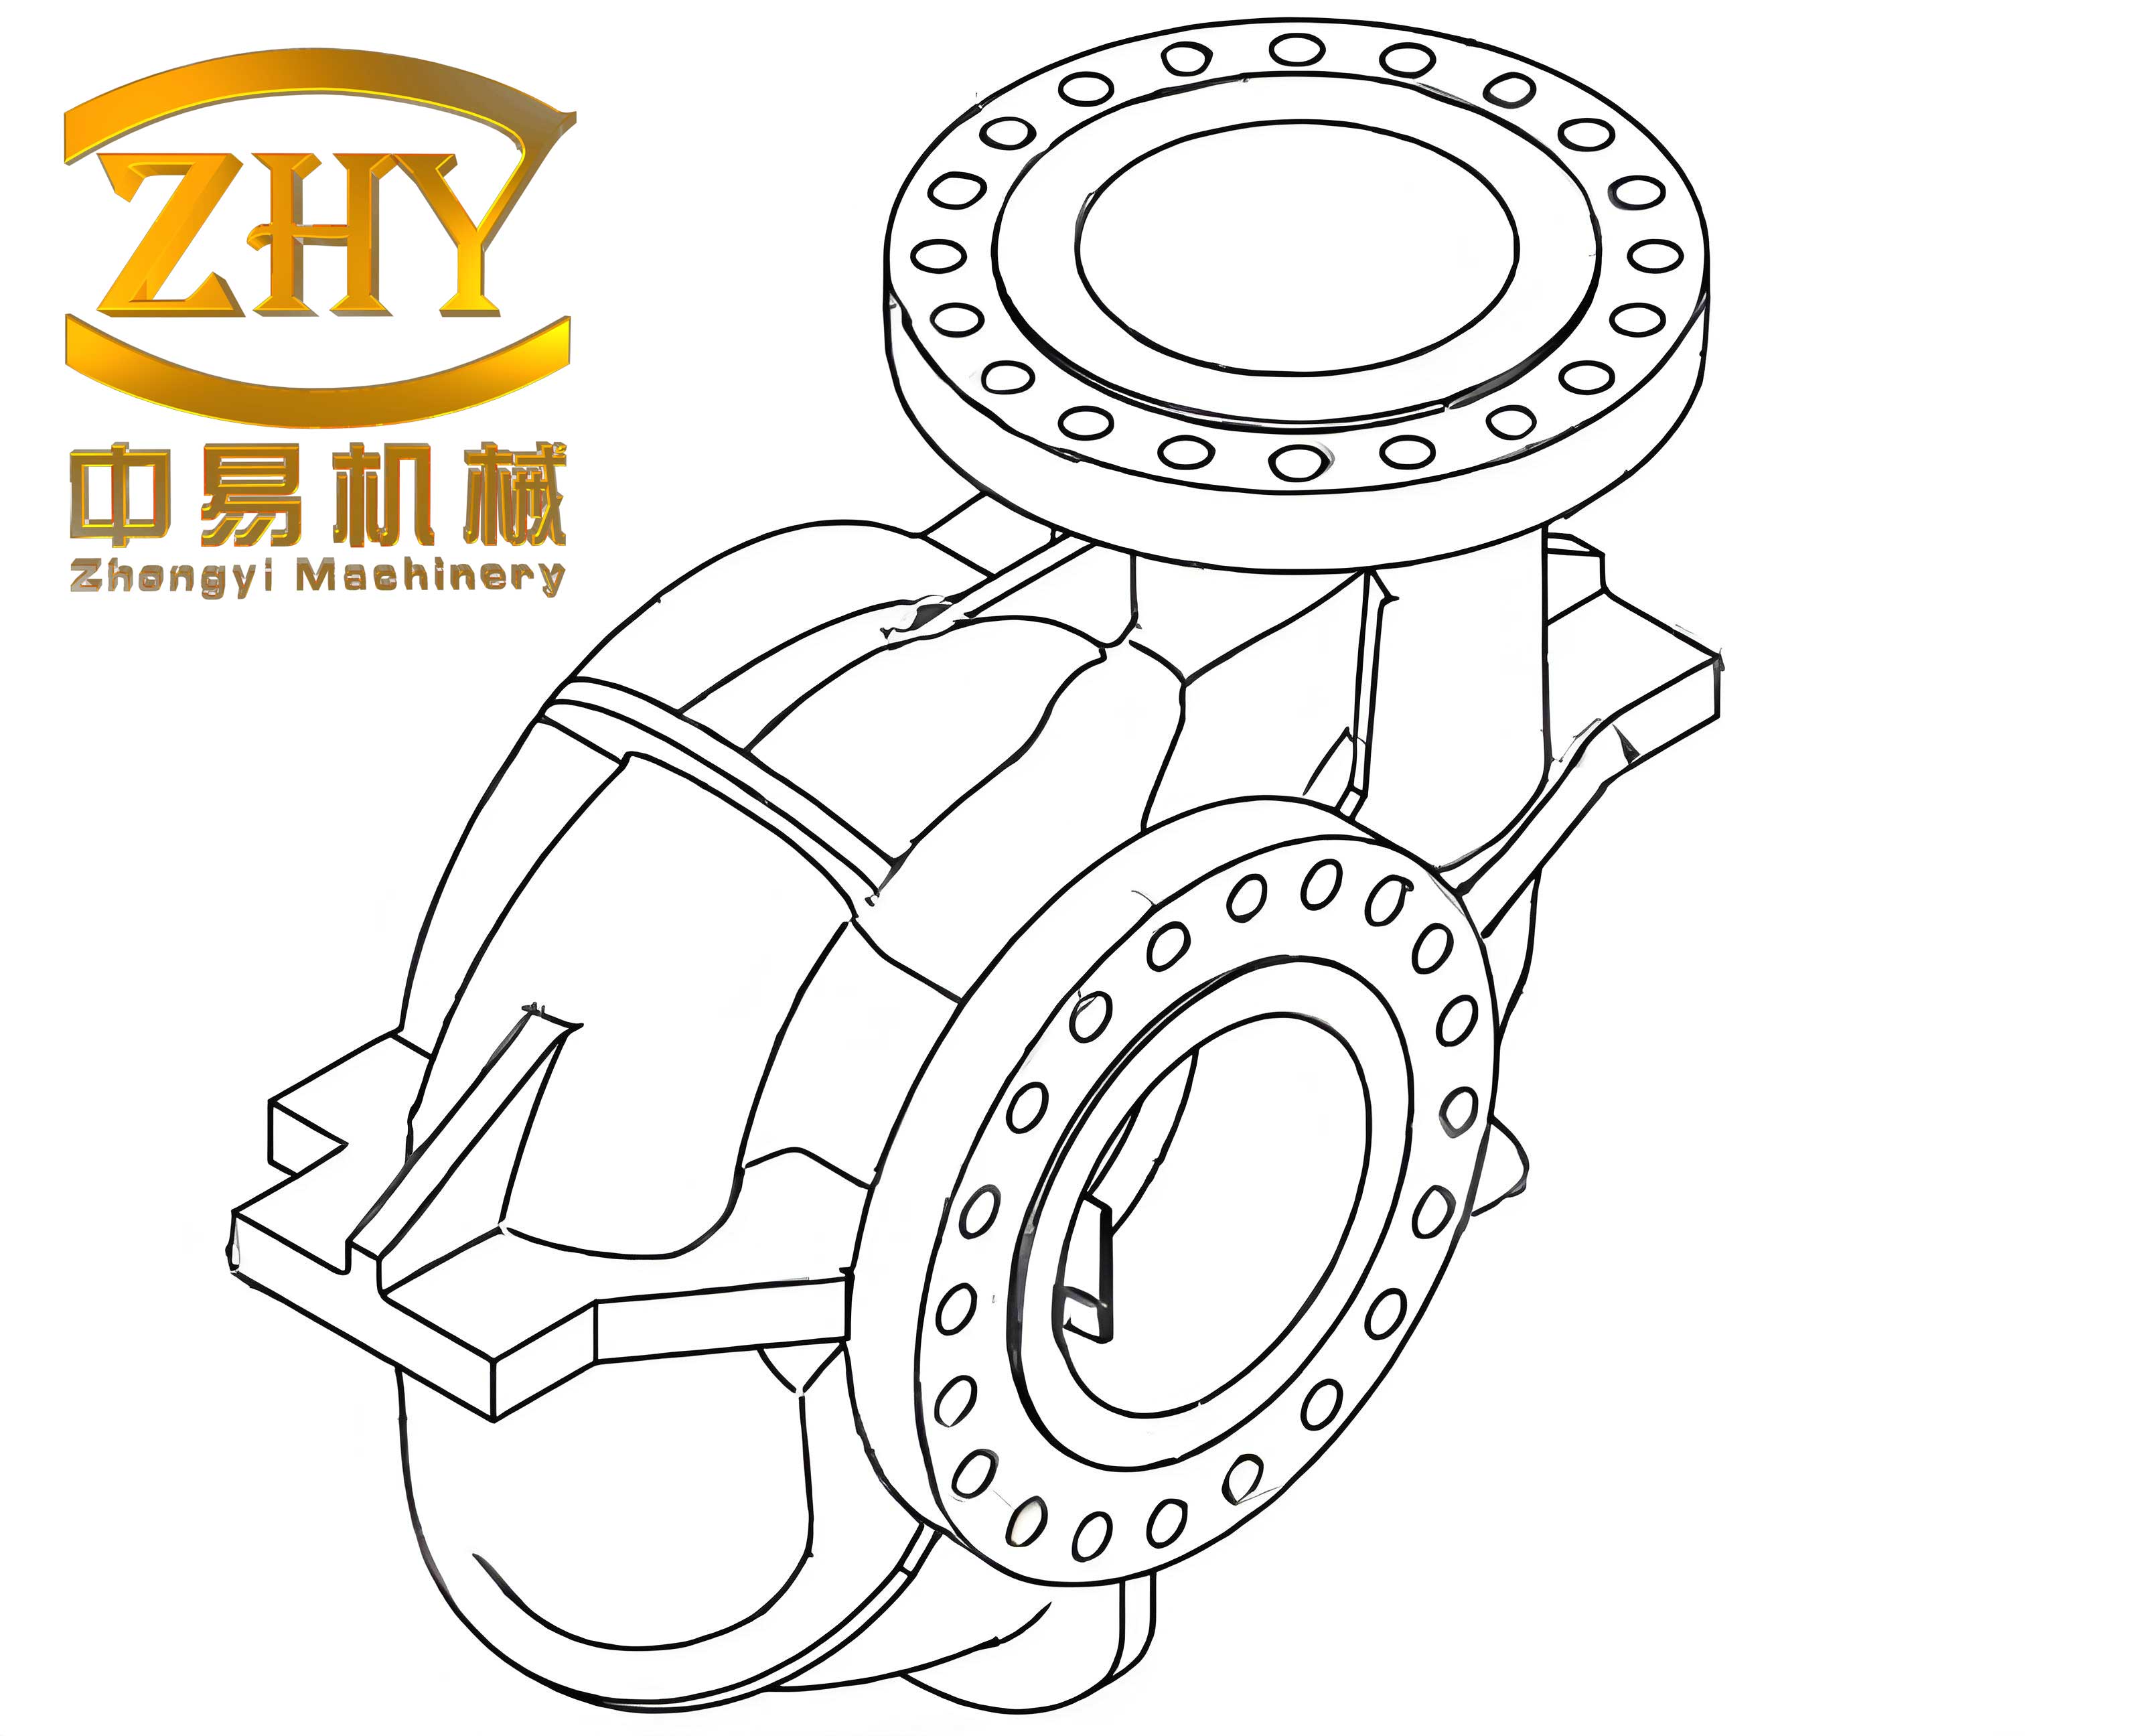
One of the primary challenges in producing such shell castings is the strict dimensional tolerance. The turbine shell has intricate airways with walls only 20 mm thick, spaced 65 mm apart, and connected only at the base, leading to high susceptibility to distortion. To achieve the required precision, we designed the casting with a controlled shrinkage allowance. The radial contraction was set between 1.5% and 1.9%, calculated based on the material’s solidification behavior. This can be expressed using the formula for linear shrinkage: $$ \Delta L = L_0 \cdot \alpha $$ where $\Delta L$ is the dimensional change, $L_0$ is the original length, and $\alpha$ is the shrinkage coefficient, ranging from 0.015 to 0.019 for this alloy. Additionally, we incorporated anti-deformation ties (拉筋) between the airway walls, with a height of 300 mm and spacing of 250 mm, to maintain shape during processing. These ties were removed only after final heat treatment, ensuring stability throughout manufacturing.
Surface defects in shell castings, such as sand sticking, cold shuts, or oxidation, are particularly problematic due to the difficulty of accessing narrow internal passages for repair. To mitigate this, we optimized the molding sand composition. For sections with wall thickness below 50 mm, we used high-purity silica sand (SiO₂ content >99.26%). For thicker regions and the core forming the airways, we employed chromite sand as a facing material, which offers better chilling effects and surface finish. The use of chromite sand enhances heat extraction, reducing the risk of surface imperfections. The selection criteria are summarized in Table 1.
| Wall Thickness | Sand Type | Purpose |
|---|---|---|
| < 50 mm | High-purity silica sand | General molding for thin sections |
| ≥ 50 mm | Chromite sand (face) with silica back sand | Improved cooling and surface quality |
| Airway cores | Chromite sand | Chilling effect to prevent shrinkage and ensure clean surfaces |
Internal defects like shrinkage porosity and cracks are common in shell castings due to complex geometry and alloy composition. The 15Cr1Mo1V steel contains vanadium, which increases crack sensitivity. To address this, we designed a gating and risering system that promotes directional solidification. The gating system is bottom-pour type, with a calculated ratio of cross-sectional areas: $$ \sum A_{\text{nozzle}} : \sum A_{\text{sprue}} : \sum A_{\text{runner}} : \sum A_{\text{ingate}} = 1 : 1.5 : 4.6 : 4.1 $$ This ratio minimizes turbulence and slag inclusion. The pouring temperature was set at 1580 °C ± 5 °C, higher than the liquidus temperature of 1450 °C, to improve fluidity for thin walls. The rise speed of the molten metal was controlled between 12 and 14 mm/s, derived from the equation: $$ v = \frac{Q}{A} $$ where $v$ is the rise speed, $Q$ is the volumetric flow rate, and $A$ is the cross-sectional area of the cavity. This ensures smooth filling and reduces defect formation.
Riser design is crucial for feeding shell castings during solidification. We used a combination of open and blind risers to compensate for shrinkage in hotspots like flanges and wall junctions. The riser volume was determined based on Chvorinov’s rule, which relates solidification time to volume-to-surface area ratio: $$ t = k \left( \frac{V}{A} \right)^2 $$ where $t$ is solidification time, $k$ is a mold constant, $V$ is volume, and $A$ is surface area. By optimizing riser placement and size, we ensured adequate feeding. Post-pouring, exothermic covering compounds were applied to risers to maintain thermal efficiency. Numerical simulation using MAGMA software validated our design, showing minimal shrinkage porosity in critical areas, as illustrated by liquid fraction analysis.
Core assembly for shell castings requires precision to maintain internal passage dimensions. We adopted a multi-core structure, with cores bonded using alkaline phenolic resin sand. To manage gas evolution, which can cause blowholes, we embedded vent ropes (Φ12 mm) within cores, placed within 50 mm of the surface. The cores were fixed by welding internal reinforcement frames, then patched with resin-bonded sand. After coating with alcohol-based alumina paint (0.6–0.8 mm thick) and drying, the assembly ensured accurate airway geometry. This method is essential for producing high-quality shell castings with complex internal features.
Heat treatment of shell castings is vital to achieve desired microstructures and mechanical properties. For 15Cr1Mo1V steel, we implemented a three-stage process: full annealing, normalizing, and tempering. The schedule aims to homogenize the structure and reduce residual stresses, preventing deformation. The kinetics of phase transformation can be described by the Avrami equation: $$ f = 1 – \exp(-k t^n) $$ where $f$ is the transformed fraction, $k$ is a rate constant, $t$ is time, and $n$ is an exponent. During normalizing, we used fog cooling to achieve a cooling rate that limits pro-eutectoid ferrite to below 5%, resulting in a bainitic matrix. Table 2 outlines the heat treatment parameters.
| Stage | Temperature (°C) | Time (h) | Cooling Method |
|---|---|---|---|
| Full Annealing | 920–940 | 4–6 | Furnace cool to 300 °C |
| Normalizing | 960–980 | 2–3 | Fog cool to 550 °C, then air cool |
| Tempering | 720–740 | 4–6 | Air cool |
Deformation control is a recurring theme in shell castings production. Beyond anti-deformation ties, we designed a dedicated support plate (料盘) for heat treatment. This plate, cast from the same material, features a grid structure with 200 mm thick walls and镂空 sections to minimize thermal gradients. The plate helps maintain the casting’s shape during heating and cooling cycles. The effectiveness of such supports can be analyzed using thermal stress models, such as: $$ \sigma = E \alpha \Delta T $$ where $\sigma$ is stress, $E$ is Young’s modulus, $\alpha$ is thermal expansion coefficient, and $\Delta T$ is temperature difference. By reducing $\Delta T$ through controlled heating rates (max 100 °C/h) and cooling rates, we minimized distortion risks.
Pouring practice for shell castings involves careful parameter selection. We used argon shielding to prevent oxidation during pouring—argon was flushed into the mold cavity before pouring, and a protective argon ring surrounded the ladle nozzle. The initial velocity of metal entry was kept below 0.5 m/s to avoid splash, and near the end of pouring, a half-flow technique was employed to ensure risers fill smoothly. These measures are critical for defect-free shell castings. The overall pouring time can be estimated by: $$ T = \frac{V_{\text{casting}}}{Q} $$ where $V_{\text{casting}}$ is the casting volume and $Q$ is the flow rate, adjusted for system characteristics.
Shakeout and cleaning of shell castings require timing to avoid cracking. We allowed the casting to cool to below 100 °C in the mold before shakeout, which took approximately 15 days due to the mass and geometry. This slow cooling reduces thermal shock and preserves dimensional accuracy. After shakeout, shot blasting was performed to remove surface scale, followed by non-destructive testing. Ultrasonic testing (UT) per JB/T 9630.2–1999 Grade 2 and magnetic particle testing (MT) per JB/T 9630.1–1999 Grade 1 were conducted to verify internal and surface quality, respectively. These standards ensure that shell castings meet rigorous industrial requirements.
Our production validation confirmed the efficacy of this process. The finished turbine shell casting exhibited dimensions within CT8级 tolerance per ГОСТ P 53464–2009, with smooth airway surfaces (Ra < 12.5 μm) and no major defects. The microstructure comprised granular bainite with less than 5% pro-eutectoid ferrite, meeting mechanical property specifications. This success underscores the importance of integrated process design for complex shell castings. Future work may explore additive manufacturing for cores or advanced simulation tools to further optimize riser and gating designs.
In conclusion, the manufacturing of turbine shell castings demands a holistic approach that addresses dimensional stability, surface integrity, internal soundness, and deformation control. Through tailored casting parameters, innovative core assembly, and precise heat treatment, we achieved a reliable production process. The use of chromite sand, controlled pouring rates, and numerical simulation played key roles. This methodology can be extended to other types of shell castings in demanding applications, highlighting the versatility of these techniques. Continuous improvement in materials and processes will further enhance the quality and efficiency of shell castings production.