
In the realm of modern manufacturing, the production of high-integrity aluminum alloy components presents significant challenges, particularly for complex, thin-walled geometries. My extensive work focuses on one such demanding component: an irregularly shaped aluminum alloy shell casting. Traditionally, these shell castings were manufactured using conventional high-pressure die-casting (HPDC) techniques. While efficient, this method often resulted in components with inherent defects like gas porosity and entrapped air, severely compromising their mechanical properties, especially ductility and pressure tightness. The part’s structural complexity—featuring multiple external bosses, internal ribs, and sharp internal corners—exacerbated these production difficulties. This article details my comprehensive investigation and successful implementation of Indirect Squeeze Casting (ISC) as a superior alternative to HPDC for manufacturing these critical shell castings, leading to a dramatic enhancement in their metallurgical quality and performance metrics.
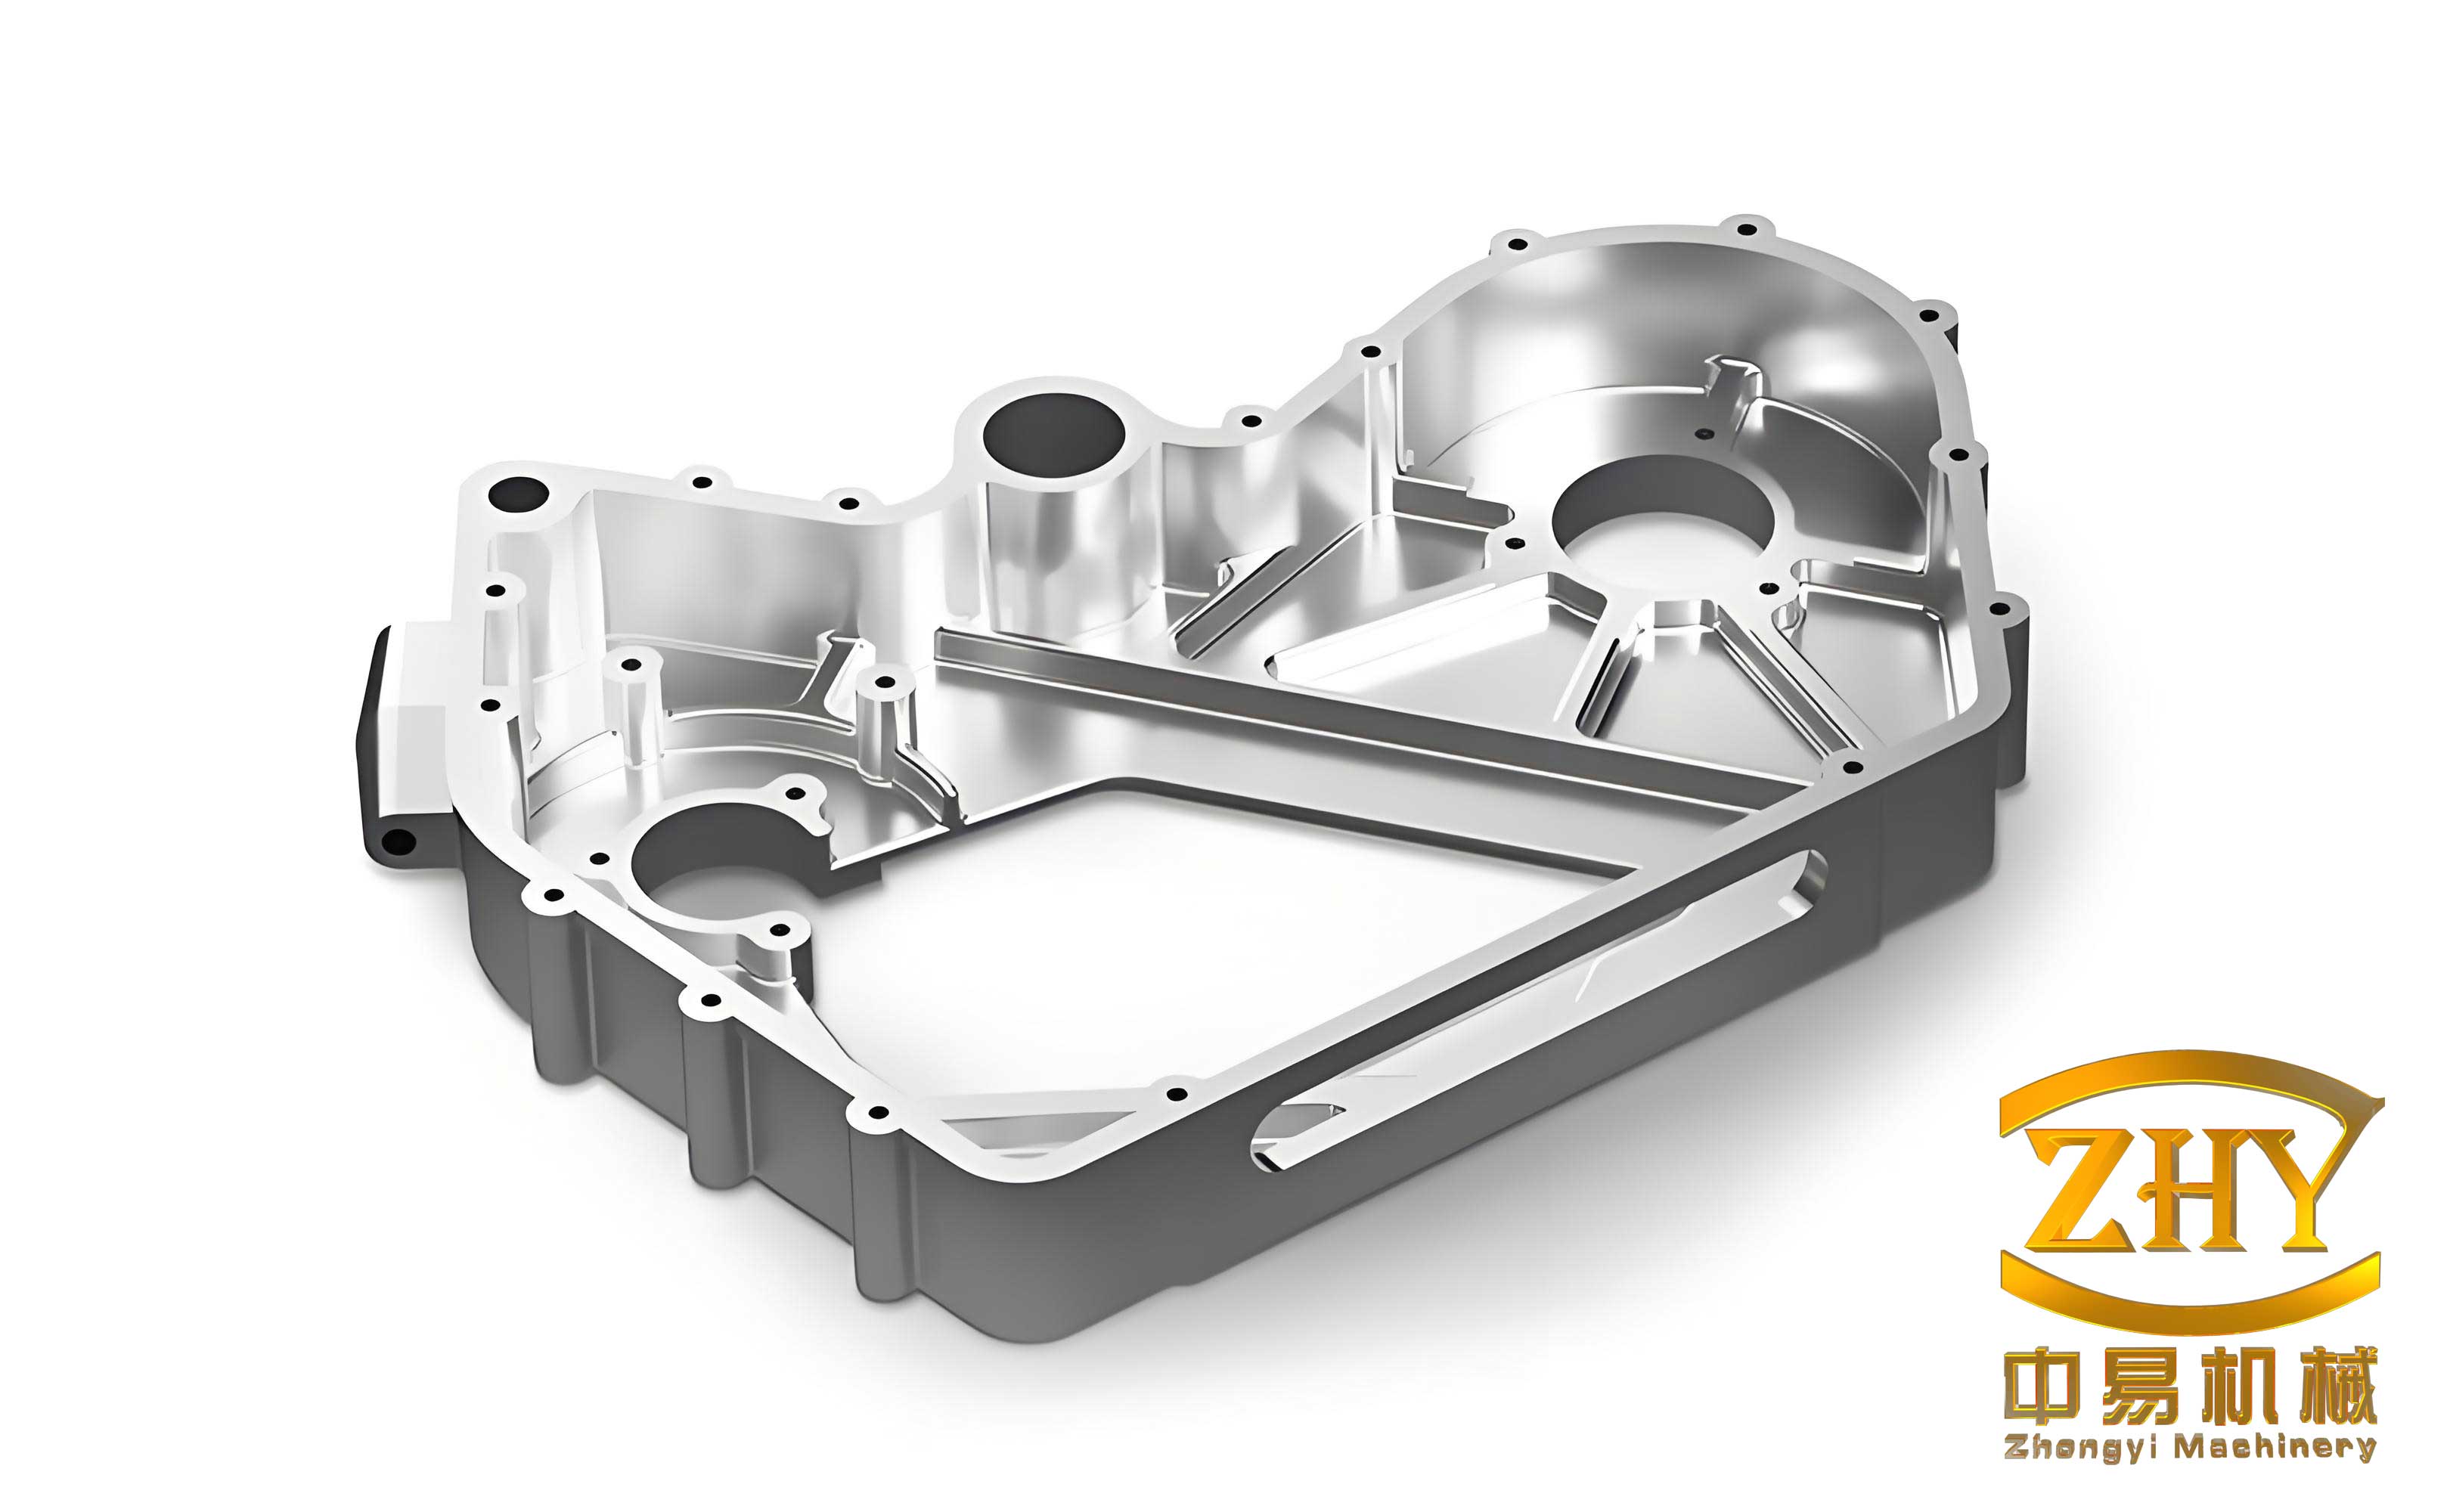
The specific aluminum alloy shell casting under investigation is characterized by a tubular structure with a highly irregular contour. Its design includes several thin ribs and protruding bosses on the surface, alongside intricate internal geometry with numerous sharp angles and transitions. The performance requirements for these shell castings were stringent: a minimum tensile strength of 245 MPa, a yield strength of 145 MPa, and a critical need to pass a 1.5 MPa pneumatic pressure leak test. However, components produced via the traditional HPDC process consistently exhibited elongation rates below 1%, indicating extreme brittleness, and suffered from leakage failures due to subsurface porosity. The typical defect profile is summarized in Table 1.
| Defect Type | Primary Cause in HPDC | Impact on Shell Casting |
|---|---|---|
| Gas Porosity/Entrapped Air | Turbulent melt flow during high-speed injection; air entrapment in the cavity. | Leads to leakage paths, reduces effective load-bearing area, catastrophic for pressure integrity. |
| Shrinkage Porosity | Inadequate feeding pressure during solidification; premature gate freezing. | Creates internal voids, lowers mechanical strength (especially yield and tensile). |
| Cold Shuts | Melt fronts meeting without complete fusion due to low temperature or slow filling. | Creates weak, discontinuous planes in the casting structure. |
| Low Elongation (<1%) | Combination of fine gas pores and oxide films acting as stress concentrators. | Results in brittle failure, inability to absorb impact or deformation energy. |
The fundamental limitation of HPDC lies in its filling dynamics. The process relies on extremely high injection velocities (0.5 – 1.1 m/s) to fill the mold before the metal solidifies. This turbulent flow is described by a high Reynolds number:
$$Re = \frac{\rho v L}{\mu}$$
where \( \rho \) is the melt density, \( v \) is the injection velocity, \( L \) is a characteristic length, and \( \mu \) is the dynamic viscosity. In HPDC, \( Re \) often exceeds the critical threshold for turbulent flow, leading to vortex formation and air entrainment. This entrapped air, compressed into small bubbles during the intensification phase, becomes permanently lodged within the shell castings. Furthermore, the rapid solidification inherent to HPDC, while beneficial for fine microstructure, hinders effective metallostatic feeding to compensate for shrinkage, resulting in shrinkage porosity.
To overcome these intrinsic flaws, I spearheaded a complete process overhaul, replacing HPDC with Indirect Squeeze Casting. The core principle of ISC is the combination of laminar, non-turbulent mold filling with the application of a high, sustained hydrostatic pressure throughout the solidification phase. This methodology fundamentally alters the defect formation mechanics. The process sequence I developed and optimized is as follows:
- Molten Metal Transfer & Die Preparation: The aluminum alloy (typically a Al-Si-Mg series like A356 or equivalent) is melted and degassed. The die, pre-heated to a controlled temperature, is coated with a lubricant/release agent.
- Slow, Laminar Filling of the Shot Sleeve: The molten metal is poured into a vertical shot sleeve (or “pre-chamber”) attached to the die. This filling step is gravity-driven and quiescent.
- Plunger-Actuated Laminar Cavity Fill: A hydraulically actuated plunger advances at a controlled, slow speed (typically 0.03 – 0.10 m/s), pushing the melt through the gate and into the mold cavity in a laminar, non-turbulent manner.
- Application of Intensification Pressure: Once the cavity is completely filled, the plunger continues its advance, applying a high, sustained pressure (50-150 MPa) on the solidifying metal. This pressure is maintained until complete solidification.
- Ejection and Cycle Repeat: After solidification, the die opens, and the finished shell casting is ejected.
The success of this ISC process for our complex shell castings hinged on two pillars of innovation: radical die redesign and meticulous parameter optimization.
Die Design and Tooling Innovation for ISC Shell Castings
The existing HPDC die was fundamentally incompatible with the ISC process logic. My team executed a complete redesign. The most critical change was reorienting the parting plane. The original horizontal parting (left-right die opening) was rotated 90 degrees to create a vertical parting (top-bottom opening). This was essential for integrating the vertical shot sleeve and ensuring symmetrical, axial pressure application on the solidifying casting.
Key modifications included:
- Shot Sleeve Integration: The original right-side ingate was permanently sealed. A dedicated cavity was machined directly below the main mold cavity, within the bottom die block, to house the custom-designed shot sleeve. This positioned the metal source axially below the casting.
- Plunger and Sleeve Fabrication: The shot sleeve and plunger were machined from premium hot-work tool steel (H13 grade) and heat-treated to high hardness (45-48 HRC) for wear and thermal fatigue resistance. The clearance between the plunger and sleeve was precisely controlled to 0.10 – 0.15 mm per side. This tight tolerance minimizes metal leakage (“flash”) past the plunger while allowing for thermal expansion, which is crucial for maintaining pressure integrity. The relationship for required clearance (\(\delta\)) can be approximated by considering thermal expansion:
$$\delta_{min} \ge \alpha \cdot D \cdot \Delta T$$
where \( \alpha \) is the coefficient of thermal expansion for H13, \( D \) is the sleeve diameter, and \( \Delta T \) is the operational temperature rise. - Gating and Venting: The gate area was significantly enlarged compared to HPDC to reduce flow velocity and facilitate feeding. Strategic vents were placed at the end of fill locations to allow air to escape passively during the slow fill stage.
| Component | Material | Key Hardness | Critical Dimension/Tolerance | Function |
|---|---|---|---|---|
| Main Die Cavity | H13 Steel | 42-46 HRC | Mirror-finish on casting surfaces | Forms final shape of shell casting |
| Shot Sleeve | H13 Steel | 45-48 HRC | Inner Dia. tolerance: +/- 0.02mm | Holds molten metal; withstands plunger pressure |
| Plunger | H13 Steel | 48-50 HRC | Clearance: 0.10-0.15mm/side | Applies pressure to melt column |
| Ejector Pins | H11 Steel | 50-52 HRC | Precision ground surface | Removes solidified shell casting from die |
Parameter Optimization and Theoretical Foundation
The transition to ISC necessitated a complete re-evaluation and optimization of all process parameters. Our production trials were conducted on a 5000 kN vertical hydraulic press equipped with precise closed-loop control for plunger position and pressure. The optimized parameter window, established through a Design of Experiments (DOE) approach, is detailed in Table 3. Each parameter’s role is governed by fundamental principles of fluid dynamics and solidification science.
| Process Parameter | HPDC Baseline | ISC Optimized Range | Rationale & Governing Principle |
|---|---|---|---|
| Filling Velocity (Plunger) | 0.5 – 1.1 m/s | 0.03 – 0.05 m/s | Ensures laminar flow (Re < 2000), preventing air entrainment. Critical for defect-free shell castings. |
| Filling Time | ~0.01 – 0.05 s | ~0.2 s | Slower fill allows for sequential, directional solidification front advancement, improving feedability. |
| Intensification Pressure | 30 – 70 MPa (brief) | 80 – 100 MPa (sustained) | High pressure acts on the mushy zone, suppressing gas pore nucleation and forcing liquid into shrinkage voids. Pressure must exceed the sum of metallostatic and capillary pressures: $$P_{applied} > \rho g h + \frac{2\gamma_{sl}}{r_{crit}}$$ |
| Die Temperature | 150 – 200 °C | 200 – 250 °C | Higher temperature reduces thermal shock, promotes directional solidification from casting towards the shot sleeve (feeder), and minimizes cold shuts. |
| Shot Sleeve Temperature | N/A (Cold Chamber) | 250 – 300 °C | Prevents formation of an overly thick solidified skin (“shell”) in the sleeve, which would impede pressure transmission to the casting cavity. |
| Pouring Temperature | ~680 °C | 700 – 720 °C | Higher superheat delays freezing in the gates and thin sections, ensuring they remain open as feeding channels during pressurization. |
The optimization of filling velocity was paramount. By reducing the velocity by an order of magnitude, the Reynolds number falls well into the laminar regime. This laminar flow front progressively fills the cavity, pushing air ahead of it towards the vents, effectively eliminating turbulence-induced porosity in the final shell castings.
The intensification pressure mechanism is the heart of the ISC advantage. During solidification, shrinkage occurs as the metal transitions from liquid to solid. In HPDC, the gate freezes quickly, isolating the casting from the pressure source. In ISC, the large gate area and the direct, pressurized liquid metal column in the shot sleeve remain liquid much longer. The applied pressure \(P\) is transmitted through this liquid column to the solidifying mushy zone. This pressure drastically increases the feeding efficiency. It can be modeled as enhancing the effective feeding distance, which in traditional casting is limited by the viscosity of flow through the dendritic network. The pressure compensates for the pressure drop \( \Delta P \) required for interdendritic flow:
$$ \Delta P = \frac{\mu L_f v_f}{K} $$
where \( \mu \) is the viscosity of the interdendritic liquid, \( L_f \) is the feeding distance, \( v_f \) is the feeding velocity, and \( K \) is the permeability of the mushy zone. The applied ISC pressure provides the driving force to overcome this \( \Delta P \), allowing feeding to occur over much longer distances, thereby eliminating shrinkage porosity throughout the shell casting.
Furthermore, the high pressure suppresses the nucleation and growth of hydrogen gas pores. The critical radius \( r_{crit} \) for a pore to nucleate or grow under an external pressure \( P_{ext} \) is given by:
$$ r_{crit} = \frac{2 \gamma_{lg}}{P_{H_2} – P_{ext}} $$
where \( \gamma_{lg} \) is the liquid-gas surface tension and \( P_{H_2} \) is the partial pressure of hydrogen in the melt. By applying a high \( P_{ext} \) (the intensification pressure), \( r_{crit} \) becomes very large, meaning hydrogen remains in solution or forms pores only on very few, potent substrates, leading to a drastic reduction in porosity.
Microstructural and Mechanical Property Enhancement
The impact of the ISC process on the metallurgy of the aluminum shell castings is profound and measurable. The combination of slower cooling (compared to HPDC) and high pressure results in a superior microstructure.
- Grain Structure: The microstructure shows a fine, equiaxed dendritic structure. The pressure during solidification reduces air gap formation at the metal-die interface, improving heat transfer and potentially leading to a slightly finer grain size than in gravity casting, though not as fine as in HPDC.
- Porosity: This is the most dramatic improvement. Radiographic inspection and density measurements show porosity levels reduced to less than 0.1%, compared to 1-3% typical in HPDC parts. Polished and etched cross-sections reveal a dense, virtually pore-free matrix.
- Secondary Phase Morphology: For Al-Si-Mg alloys, the eutectic silicon morphology is modified from a coarse, acicular plate-like structure to a finer, more fibrous form due to the influence of pressure on solidification kinetics. This improves ductility.
The mechanical property data, presented in Table 4, unequivocally demonstrates the superiority of ISC-produced shell castings. All test specimens were taken from the actual castings and subjected to a T6 heat treatment (solutionizing, quenching, and artificial aging).
| Mechanical Property | HPDC Shell Casting | ISC Shell Casting (This Work) | Percentage Improvement |
|---|---|---|---|
| Ultimate Tensile Strength (UTS) | 245 – 260 MPa | 290 – 310 MPa | ~18% – 20% |
| Yield Strength (0.2% Offset) | 145 – 155 MPa | 180 – 190 MPa | ~24% – 27% |
| Elongation at Break (%) |
0.5% – 1.0% | 8.0% – 10.0% | > 800% |
| Hardness (Brinell HB) | 80 – 90 HB | 95 – 110 HB | ~19% – 22% |
| Pressure Tightness | ~70% Pass Rate at 1.5 MPa | > 97% Pass Rate at 1.5 MPa | Massive improvement in reliability |
The order-of-magnitude increase in elongation is the most significant achievement. This dramatic boost in ductility is a direct consequence of the near-elimination of stress-concentrating pores and oxide films. The relationship between porosity fraction (\(f\)) and ductility can be empirically described by models such as:
$$ \epsilon_f \approx \epsilon_0 (1 – k f^{2/3}) $$
where \( \epsilon_f \) is the elongation with porosity, \( \epsilon_0 \) is the elongation of the pore-free matrix, and \( k \) is a constant. By reducing \( f \) to a minimal value, \( \epsilon_f \) approaches \( \epsilon_0 \), unlocking the inherent ductility of the heat-treated aluminum alloy. This makes the shell castings far more robust and resistant to failure under unexpected loads or impacts.
The yield strength improvement can be attributed to better feeding (less micro-porosity acting as early failure sites) and potentially a more homogeneous distribution of strengthening precipitates (like Mg₂Si in Al-Si-Mg systems) due to the influence of pressure on solid-state diffusion during aging. The increased hardness correlates well with the higher density and strength.
Conclusion and Industrial Impact
The systematic replacement of High-Pressure Die Casting with Indirect Squeeze Casting for the manufacture of complex aluminum alloy shell castings has proven to be a transformative process optimization. The project successfully addressed the core deficiencies of HPDC—entrapped gas and shrinkage porosity—by fundamentally re-engineering both the tooling design and the process physics. The key to success was the synergistic control of ultra-slow, laminar filling to prevent air entrainment, coupled with the application of a high, sustained hydrostatic pressure to suppress pore formation and actively feed solidification shrinkage.
The results speak for themselves: shell castings produced via this optimized ISC process exhibit exceptional metallurgical integrity, characterized by density exceeding 99.9% of theoretical and a completely transformed mechanical property profile. The leap in elongation from less than 1% to 8-10% signifies a transition from a brittle component to a tough, reliable one. This is complemented by significant gains in tensile strength, yield strength, and hardness. Consequently, the pressure tightness qualification rate soared to over 97%, ensuring functional reliability.
This case study establishes a robust technical framework for employing Indirect Squeeze Casting as a premium manufacturing solution for high-performance, complex, thin-walled aluminum shell castings where structural integrity, leak-tightness, and dynamic load-bearing capacity are non-negotiable requirements. The process, while potentially having a slightly longer cycle time than HPDC, delivers unmatched quality, reducing scrap, post-machining rejection rates, and warranty failures, thereby offering a superior lifecycle cost for critical applications.