
As a researcher deeply involved in the field of advanced manufacturing and casting technology, I have witnessed the increasing demands for high-performance components in hydroelectric power generation. Among these, guide vanes for water turbines stand out due to their critical role in directing flow, regulating output, and ensuring safe shutdown. These components operate under harsh conditions, including silt abrasion, water impact, and cavitation, necessitating superior mechanical properties such as wear resistance, corrosion resistance, and high hardness. However, the complex geometry of guide vanes—comprising a blade body (瓣体) connected to long and short shafts—poses significant challenges in casting, often leading to internal defects like shrinkage cavities and porosity. In this article, I will delve into a detailed exploration of these casting defects, utilizing numerical simulation as a core tool for analysis and optimization. My focus will be on how temperature field management and innovative design adjustments can mitigate these issues, drawing from extensive computational and practical insights. Throughout this discussion, I will emphasize the term “casting defects” to highlight their prevalence and impact, while incorporating tables and formulas to summarize key points systematically.
The guide vane structure typically consists of three main parts: a short shaft, a blade body, and a long shaft, with the blade body being thinner than the shafts. This disparity in thickness creates thermal imbalances during solidification, especially in vertical casting processes, which are preferred for their simplicity and reduced stress deformation. In my experience, the junction between the blade body and the long shaft is particularly prone to axial shrinkage porosity, a common type of casting defect that can compromise the integrity of the entire component. For instance, in production settings, extensive axial shrinkage zones have been observed, sometimes rendering castings irreparable. To address this, I employ numerical simulation techniques to model the solidification process, allowing for a predictive analysis of temperature distributions and defect formation. This approach not only aligns with practical findings but also enables proactive工艺 adjustments.
In the initial casting process, the guide vane had a total length of 3.79 meters, a blade width of 1.17 meters, and a net weight of approximately 4 tons. Using modulus calculations, the casting modulus was determined to be around 7.8 cm. Based on empirical formulas for riser design, where the riser modulus \( M_{riser} \) is set as \( (1.2 \text{ to } 1.4) \) times the casting modulus \( M_{casting} \), a value of \( M_{riser} = 1.4 \times M_{casting} \approx 11 \, \text{cm} \) was adopted. The riser, positioned on the long shaft, was designed as a truncated cone with dimensions: upper radius of 400 mm, lower radius of 320 mm, height of 700 mm, and a sand skirt of 100 mm at the base. Additionally, chill plates were placed at the short shaft to accelerate cooling and prevent shrinkage at its junction with the blade body. The gating system was simplified to a horizontal runner directly connected to the casting, with a diameter of 100 mm. Despite these measures, numerical simulations revealed persistent casting defects, prompting a deeper investigation into the temperature field dynamics.
Through software like MAGMAsoft, I simulated the solidification process by dividing the casting into millions of elements and setting initial parameters such as a pouring temperature of 1580°C and a termination temperature of 800°C. The temperature field results at various solidification stages—1%, 35%, 75%, and 100%—illustrated uneven thermal distributions. For example, at 35% solidification, the blade body’s center remained hotter (around 1510°C) than its periphery, while the short shaft cooled rapidly due to chills. By full solidification, while a general temperature gradient from short shaft to long shaft was observed, it was insufficient for optimal riser feeding, leading to residual hot spots at the long shaft-blade junction. This thermal behavior directly correlates with the formation of casting defects, as areas with slower cooling and inadequate feeding are susceptible to shrinkage porosity.
To predict these casting defects quantitatively, I applied the Niyama criterion, a widely used判据 based on dendrite feeding channels during solidification. The criterion is expressed as:
$$ \frac{G}{\sqrt{R}} < C_{Niyama} $$
where \( G \) is the local temperature gradient (°C/cm), \( R \) is the cooling rate (°C/min), and \( C_{Niyama} \) is a critical constant, typically ranging from 0.8 to 1.1 °C1/2·min1/2/cm for different casting sizes. In this case, a value of 1.0 °C1/2·min1/2/cm was used. Regions where this inequality holds are likely to exhibit shrinkage porosity. The simulation output confirmed extensive discontinuous porosity along the long shaft’s axis and minor defects in the blade body, matching实际 observations of casting defects in production. This validation underscores the reliability of numerical tools in identifying and analyzing casting defects.
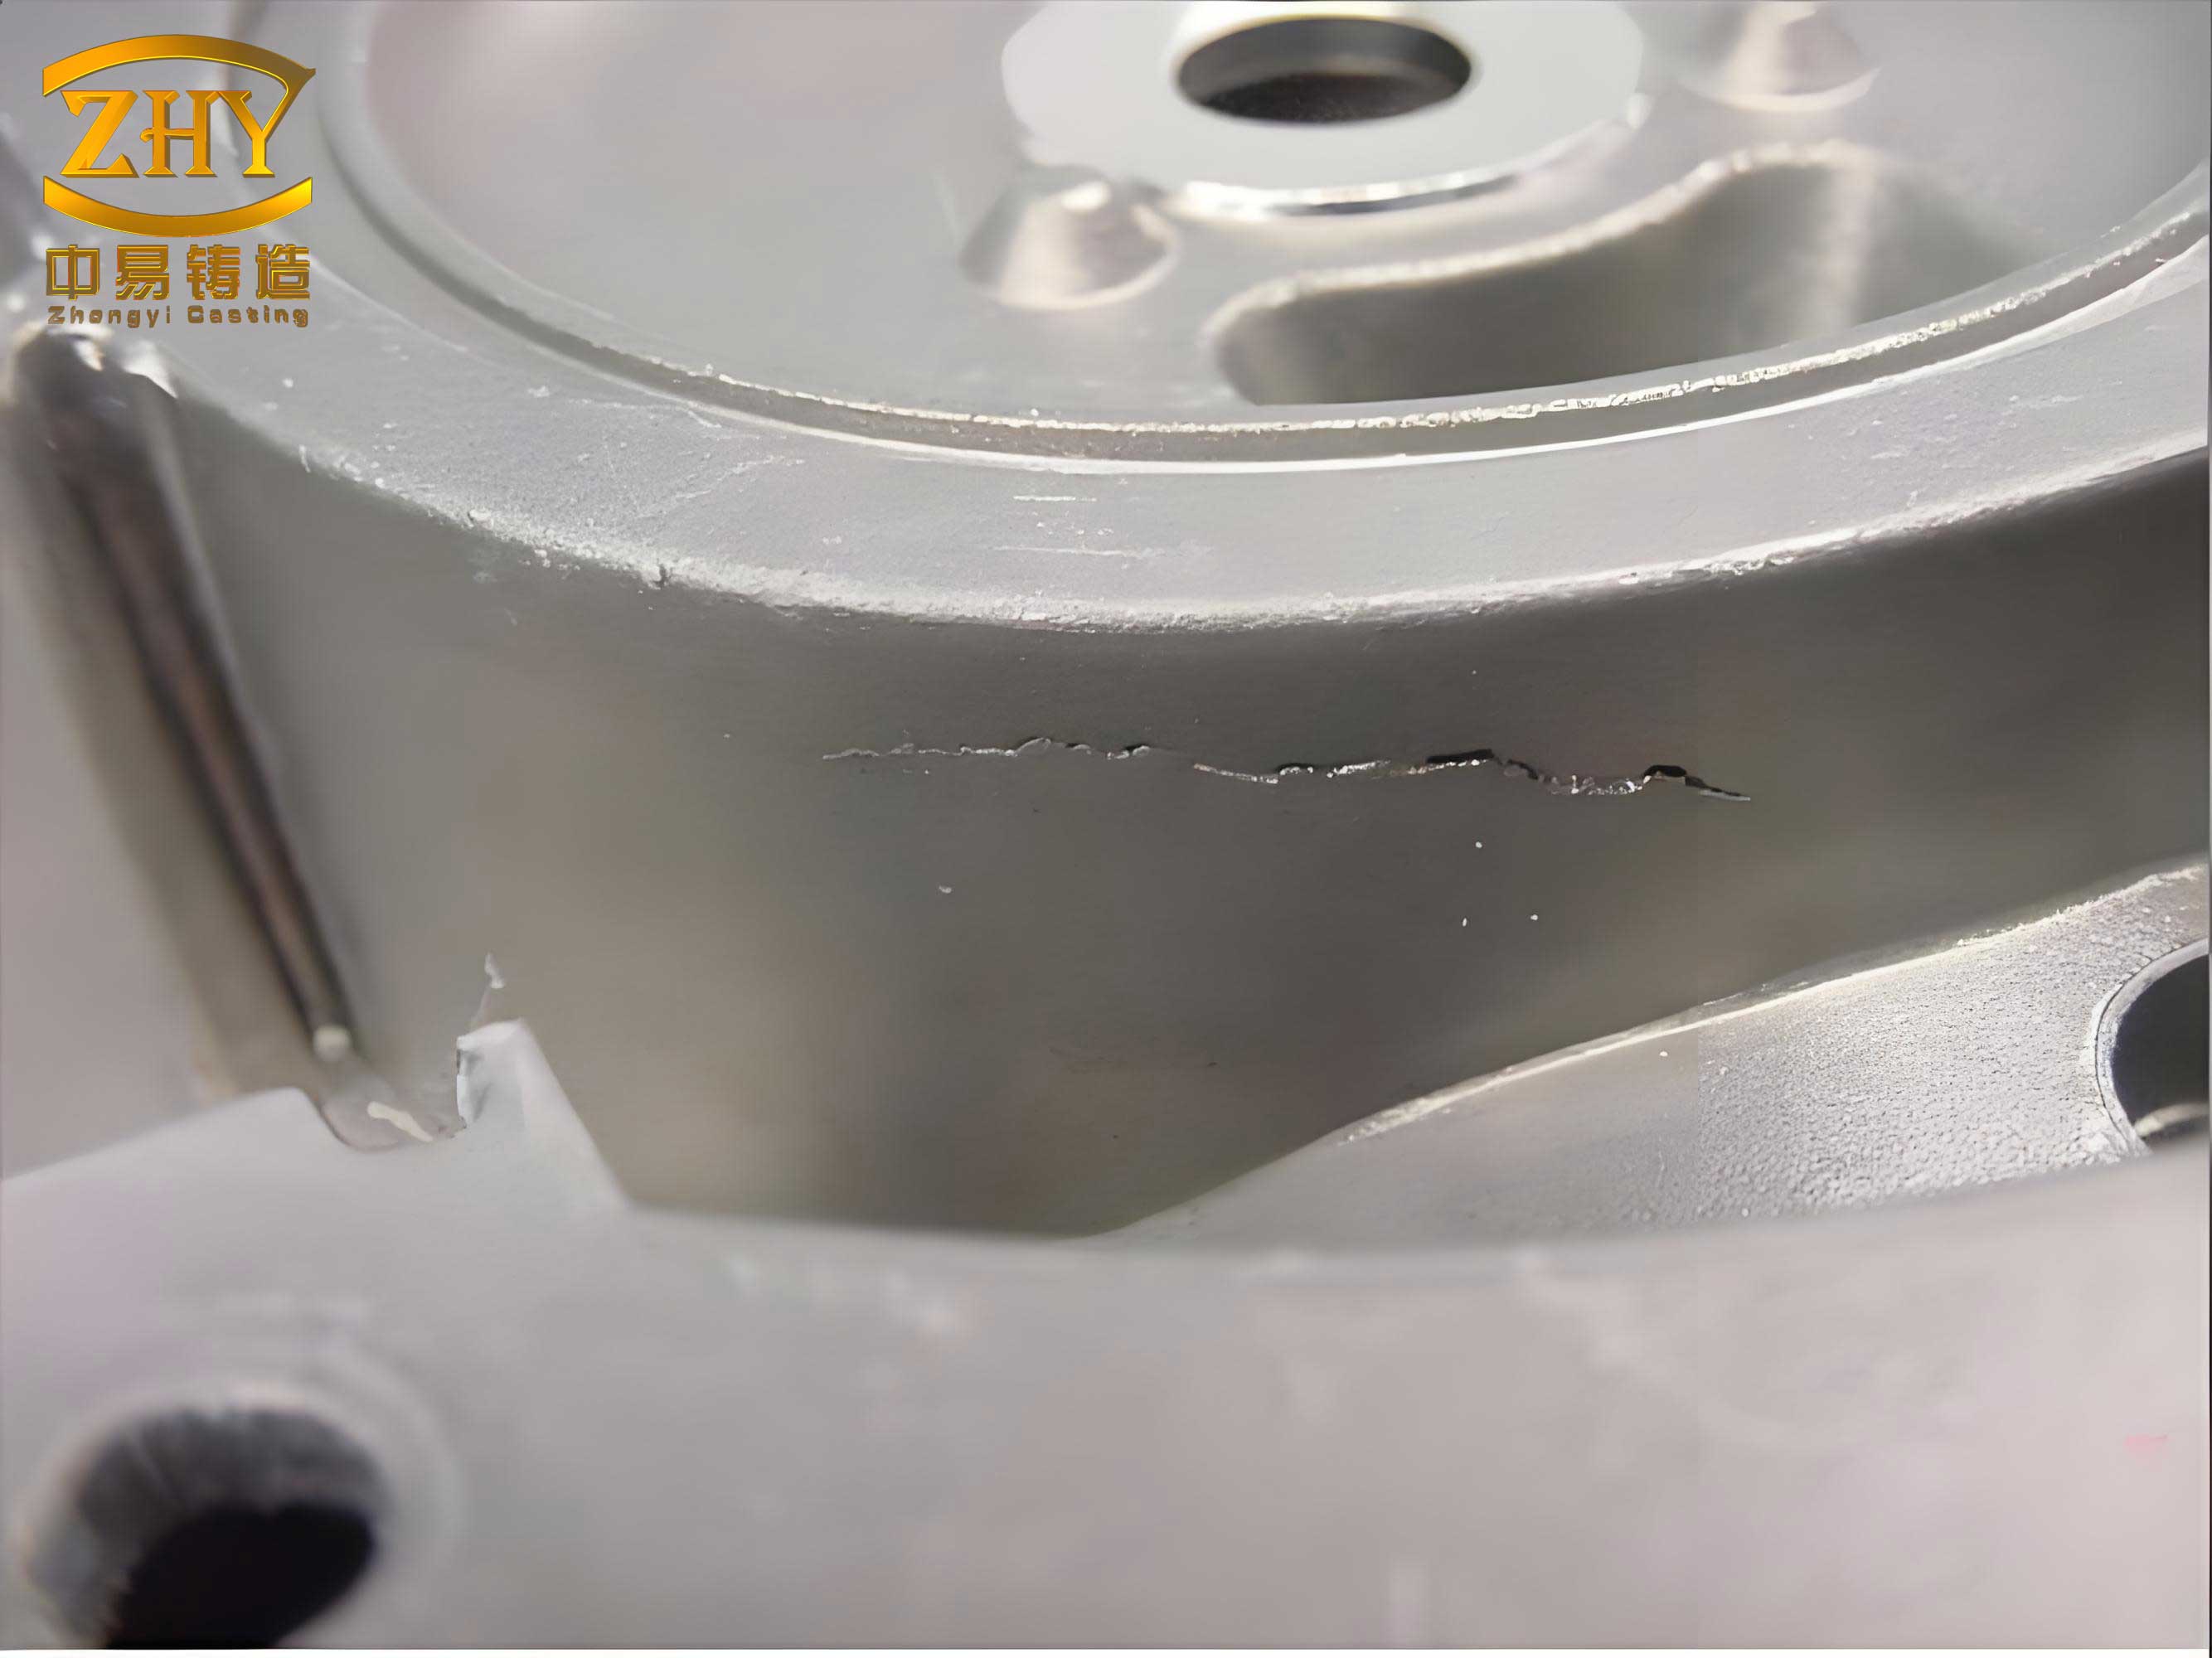
The root cause of these casting defects lies in the lack of a sufficient temperature gradient for directional solidification toward the riser. In the original design, the long shaft and blade body had relatively uniform temperatures, hindering effective feeding from the riser to the blade. To rectify this, I introduced an annular noumenon allowance (ring-shaped body padding) on the long shaft. This design, based on the rolling circle method, incrementally increases the cross-sectional modulus toward the riser, fostering a steeper thermal gradient. The design formulas are:
$$ D_1 = (1.04 \text{ to } 1.1) \times D $$
$$ D_2 = (1.04 \text{ to } 1.1) \times D_1 $$
where \( D \), \( D_1 \), and \( D_2 \) represent diameters of successive circles, with a factor of 1.04 chosen for this application. This adjustment raised the casting modulus to 8.9 cm, necessitating a larger riser with a modulus of approximately 13.3 cm (using \( M_{riser} = 1.5 \times M_{casting} \)). The optimized riser dimensions were: upper radius 410 mm, lower radius 330 mm, height 800 mm, and a 100 mm sand skirt. The gating and chill designs remained unchanged.
Re-simulating the optimized process revealed a transformed temperature field. At full solidification, a clear ascending gradient from short shaft to long shaft was established, with the riser junction maintaining the highest temperature (around 1380°C). This promotes sequential solidification, ensuring that the riser effectively feeds both the long shaft and blade body. Defect prediction using the Niyama criterion showed no shrinkage cavities or porosity in the casting本体, confirming the elimination of casting defects. Practical trials produced guide vanes free from such defects, validating the simulation results. The table below summarizes the key parameters and outcomes before and after optimization:
| Aspect | Original Process | Optimized Process |
|---|---|---|
| Casting Modulus (cm) | 7.8 | 8.9 |
| Riser Modulus (cm) | 11.0 | 13.3 |
| Temperature Gradient | Insufficient for feeding | Steady increase to riser |
| Shrinkage Porosity | Present in long shaft and blade | Absent in casting body |
| Key Modification | None | Annular noumenon allowance |
Further analysis involves the mathematical modeling of heat transfer during solidification. The governing equation for transient heat conduction in the casting can be expressed as:
$$ \rho c_p \frac{\partial T}{\partial t} = \nabla \cdot (k \nabla T) + Q $$
where \( \rho \) is density, \( c_p \) is specific heat, \( T \) is temperature, \( t \) is time, \( k \) is thermal conductivity, and \( Q \) represents latent heat release during phase change. In numerical simulations, this equation is discretized using finite element methods to compute temperature evolution. By integrating the Niyama criterion, we can derive a defect susceptibility index \( S \) for casting defects:
$$ S = \int_{V} \left( \frac{G}{\sqrt{R}} – C_{Niyama} \right) dV $$
where \( V \) is the volume of the casting. Regions with \( S < 0 \) indicate a high risk of shrinkage porosity. For the guide vane, the original design yielded positive \( S \) values in critical zones, signaling casting defects, while the optimized design showed \( S > 0 \) throughout, corroborating defect-free outcomes.
The economic and operational implications of mitigating casting defects are profound. In hydro turbine applications, guide vanes with internal defects can lead to premature failure, costly repairs, and downtime. By employing numerical simulation, we not only predict casting defects but also optimize designs proactively, reducing scrap rates and enhancing component longevity. For instance, the annular allowance design adds minimal material but significantly improves feeding efficiency, as quantified by the feeding distance \( L_f \), which can be estimated as:
$$ L_f = 4.5 \times \sqrt{M_{casting}} $$
where \( M_{casting} \) is in centimeters. In the optimized case, \( L_f \) increased from approximately 12.6 cm to 13.4 cm, extending the riser’s effective range. This principle can be generalized to other large-axis castings, offering a novel approach to tackling casting defects in similar geometries.
In conclusion, my investigation demonstrates that casting defects in turbine guide vanes, particularly shrinkage cavities and porosity, stem from inadequate temperature gradients during solidification. Through numerical simulation, I identified these casting defects and devised an optimized工艺 incorporating an annular noumenon allowance. This adjustment established a directional temperature field, enabling sequential solidification and effective riser feeding. The result was a complete elimination of casting defects in both simulated and actual castings, validating the synergy between computational tools and practical manufacturing. This methodology not only addresses immediate quality concerns but also provides a framework for advancing casting techniques in the energy sector, where reliability and performance are paramount. Future work could explore adaptive simulation algorithms or material-specific models to further refine defect prediction and control, continually pushing the boundaries of casting excellence.
To encapsulate the technical details, I present below a comparative formula table highlighting the key equations used in analyzing and optimizing casting defects:
| Equation Name | Formula | Application in Casting Defects |
|---|---|---|
| Modulus Calculation | \( M = \frac{V}{A} \) | Determines feeding requirements; critical for riser design to prevent casting defects. |
| Riser Modulus Rule | \( M_{riser} = (1.2 \text{ to } 1.5) \times M_{casting} \) | Ensures adequate feeding capacity, reducing risks of casting defects like shrinkage. |
| Niyama Criterion | \( \frac{G}{\sqrt{R}} < C_{Niyama} \) | Predicts shrinkage porosity; a core tool for identifying potential casting defects. |
| Heat Transfer Equation | \( \rho c_p \frac{\partial T}{\partial t} = \nabla \cdot (k \nabla T) + Q \) | Models temperature field dynamics, essential for simulating solidification and casting defects. |
| Feeding Distance | \( L_f = 4.5 \times \sqrt{M_{casting}} \) | Estimates riser effectiveness in mitigating casting defects over long sections. |
Through this comprehensive approach, I have shown how numerical simulation serves as a powerful ally in the battle against casting defects, transforming challenges into opportunities for innovation and quality enhancement in casting processes.