
In the realm of advanced manufacturing for aerospace applications, precision investment casting stands as a pivotal technology, enabling the production of complex, high-integrity components with exceptional dimensional accuracy and superior metallurgical properties. This process, often referred to as lost-wax casting, involves creating a ceramic shell around a sacrificial wax pattern, which is subsequently melted out to form a mold cavity for metal pouring. The quality of the final casting is profoundly influenced by numerous factors, among which the design of the gating system is paramount. The gating system governs the flow of molten metal into the mold, affecting filling behavior, temperature distribution, solidification patterns, and ultimately, the incidence of defects such as shrinkage porosity, inclusions, and hot tears. In this comprehensive study, I delve into the intricacies of gating system design for a specific aerospace component—a guider inner ring—through the lens of precision investment casting. The objective is to empirically evaluate and compare two distinct gating system configurations, analyzing their impact on the internal quality of castings made from a high-performance nickel-based alloy. The findings underscore a fundamental principle: for components with relatively simple geometries, a simplistic gating approach can often yield superior results by promoting laminar flow and mitigating thermal gradients, thereby enhancing defect-free yield rates.
Precision investment casting has evolved significantly, driven by demands from sectors like aerospace, where components must withstand extreme thermal and mechanical stresses. The process typically involves several sequential steps: pattern creation, assembly, shell building, dewaxing, firing, melting and pouring, knockout, and post-processing. Each step requires meticulous control to ensure final quality. However, the design phase, particularly for the gating and feeding system, is where many casting defects are either prevented or inadvertently introduced. The gating system must fulfill multiple functions: facilitate rapid and complete mold filling with minimal turbulence, enable effective feeding to compensate for solidification shrinkage, and allow for the escape of gases and exclusion of non-metallic inclusions. In aerospace applications, where components like turbine blades, nozzles, and guide vanes are commonplace, even minor internal flaws can lead to catastrophic failures. Therefore, optimizing gating design through both empirical experimentation and theoretical modeling is a continuous pursuit in foundry engineering.
The component under investigation here is an inner ring for an aircraft engine guider. This part, while conceptually simple in its annular form with specific recesses, presents challenges in achieving consistent internal soundness. Historically, casting such components as monolithic pieces has been problematic, leading to the adoption of a segmentation strategy—casting simpler subsections and assembling them mechanically. This study focuses on the inner ring subsection, aiming to establish a reliable precision investment casting process for its production. The alloy selected is K424, a nickel-based casting alloy renowned for its high temperature strength, good plasticity, and favorable castability, attributed to its elevated aluminum and titanium content. Its nominal chemical composition is detailed in Table 1.
| Element | Min | Max | Typical |
|---|---|---|---|
| C | 0.14 | 0.20 | 0.17 |
| Cr | 8.5 | 10.5 | 9.5 |
| Ni | Balance | Balance | Balance |
| Co | 12.0 | 15.0 | 13.5 |
| W | 1.0 | 1.5 | 1.25 |
| Mo | 2.7 | 3.4 | 3.05 |
| Al | 5.0 | 5.7 | 5.35 |
| Ti | 4.2 | 4.7 | 4.45 |
| Nb | 0.5 | 1.0 | 0.75 |
| V | 0.5 | 1.0 | 0.75 |
| B | 0.015 | – | 0.015 |
| Zr | 0.02 | – | 0.02 |
| Ce | 0.02 | – | 0.02 |
| Fe | – | ≤2.0 | 1.0 |
| Mn | – | ≤0.40 | 0.20 |
| Si | – | ≤0.40 | 0.20 |
| P | – | ≤0.040 | 0.020 |
| S | – | ≤0.015 | 0.008 |
| Pb | – | ≤0.001 | 0.0005 |
| Bi | – | ≤0.0005 | 0.0003 |
To fabricate the wax patterns for this study, I employed rapid prototyping technology, specifically Selective Laser Sintering (SLS) of a fusible polymer. This approach aligns perfectly with the iterative nature of process development in precision investment casting, as it eliminates the need for expensive hard tooling during the prototyping phase. The digital model of the inner ring was created using CAD software, exported as an STL file, and then built layer-by-layer via SLS. The resulting patterns exhibited satisfactory surface finish (approximately Ra 6.3 µm after post-processing) and dimensional accuracy, which are critical for ensuring the fidelity of the final ceramic shell and casting. The overall process flow for precision investment casting in this context is summarized in Figure 1, though detailed graphical representations are omitted per instruction. The patterns were then assembled with designed gating systems to form clusters, which underwent standard shell building procedures involving successive dips in ceramic slurries and stucco applications, followed by drying, dewaxing, and high-temperature firing to achieve adequate mold strength and permeability.
The core of this investigation lies in the design and comparison of two gating system layouts, designated Scheme A and Scheme B. Both schemes were conceived based on fundamental principles of gating design but with differing philosophies. Scheme A was designed with an emphasis on robust feeding and compensation for solidification shrinkage, incorporating multiple ingates and a more complex runner layout to ensure metal delivery to various sections of the ring. Scheme B, in contrast, adopted a minimalist philosophy, featuring a simpler runner and ingate arrangement intended to promote smooth, directional metal flow with minimal flow divergence or convergence within the mold cavity. The schematic layouts of these systems are described textually: Scheme A involved a central downsprue feeding into a horizontal runner that bifurcated, with each branch leading to multiple ingates positioned along the inner ring’s circumference, aiming for uniform filling. Scheme B utilized a single, straightforward runner channel with strategically placed ingates to encourage a more linear, sequential filling pattern. Crucially, all other process parameters were held constant: the master alloy was melted in a vacuum induction furnace (ZG0.025 type), superheated to a consistent temperature, and poured into preheated ceramic shells. The casting parameters are tabulated in Table 2.
| Parameter | Value | Unit |
|---|---|---|
| Alloy Melting Temperature | 1500 ± 10 | °C |
| Mold Shell Preheat Temperature | 900 ± 20 | °C |
| Pouring Temperature | 1480 ± 5 | °C |
| Vacuum Level During Pouring | ≤ 0.1 | mbar |
| Cooling Time in Vacuum | 30 | minutes |
After solidification and cooling, the castings were extracted from the shells via mechanical knockout. They subsequently underwent standard post-processing steps: cut-off from the gating system, grinding to remove residual gates and surface imperfections, and a tailored heat treatment cycle to optimize the microstructure and mechanical properties. The critical evaluation of internal quality was performed using non-destructive testing (NDT) methods, primarily fluorescent penetrant inspection (FPI) to detect surface-breaking defects like shrinkage porosity and cracks. For a subset of castings, radiographic inspection was also conducted to assess sub-surface integrity. The results from these inspections form the basis of the comparative analysis.
The experimental outcomes revealed a clear distinction between the two gating schemes. Castings produced using Scheme A consistently exhibited indications of shrinkage porosity, predominantly localized in the annular recessed regions of the inner ring. FPI showed diffuse or clustered signals in these areas, suggestive of micro-shrinkage or spongy porosity. In contrast, castings from Scheme B showed significantly cleaner FPI results, with the vast majority passing inspection without any notable defect indications in critical zones. This stark difference in internal quality, despite identical material and process conditions, points directly to the influence of gating-induced flow dynamics and thermal management. To quantify these observations, I compiled defect statistics from multiple casting trials for each scheme, as shown in Table 3.
| Gating Scheme | Number of Castings Trialed | Castings with Defects in Recess Zone | Defect Rate (%) | Primary Defect Type |
|---|---|---|---|---|
| Scheme A | 15 | 12 | 80.0 | Shrinkage Porosity |
| Scheme B | 15 | 2 | 13.3 | Minor Inclusions |
To understand the underlying physics, I analyze the molten metal flow behavior using principles of fluid dynamics and heat transfer. The flow of liquid metal during filling in precision investment casting can be approximated as a transient, incompressible, viscous flow with free surface and heat exchange. Key governing equations include the continuity equation and the Navier-Stokes equations for momentum conservation. For an incompressible fluid, the continuity equation is:
$$ \nabla \cdot \mathbf{u} = 0 $$
where $\mathbf{u}$ is the velocity vector field. The momentum equation is:
$$ \rho \left( \frac{\partial \mathbf{u}}{\partial t} + (\mathbf{u} \cdot \nabla) \mathbf{u} \right) = -\nabla p + \mu \nabla^2 \mathbf{u} + \rho \mathbf{g} $$
Here, $\rho$ is density, $p$ is pressure, $\mu$ is dynamic viscosity, and $\mathbf{g}$ is gravitational acceleration. During filling, the energy equation governing temperature distribution is also critical:
$$ \rho C_p \left( \frac{\partial T}{\partial t} + (\mathbf{u} \cdot \nabla) T \right) = k \nabla^2 T + \dot{q} $$
where $C_p$ is specific heat capacity, $T$ is temperature, $k$ is thermal conductivity, and $\dot{q}$ represents any internal heat source (e.g., latent heat release during solidification, which begins soon after filling). In Scheme A, the design leads to multiple metal streams converging in the confined recessed region. This convergence creates a zone of flow impingement and recirculation, increasing local turbulence. The Reynolds number ($Re$) can be used to characterize flow regime:
$$ Re = \frac{\rho u L}{\mu} $$
where $u$ is characteristic velocity and $L$ is characteristic length. Higher $Re$ indicates greater tendency for turbulence. In the convergence zone, effective $L$ decreases and local $u$ may increase due to flow restriction, potentially pushing $Re$ into a transitional or turbulent range. Turbulent flow enhances mixing but also increases energy dissipation as heat, contributing to localized superheating. Moreover, the complex runner layout may cause uneven flow distribution, leading to some ingates feeding metal earlier or later than others, creating thermal gradients.
Conversely, Scheme B’s simpler design promotes more laminar, sequential filling. The flow is largely unidirectional, minimizing flow convergence and recirculation. This maintains a lower $Re$ and reduces turbulent kinetic energy generation. Consequently, the temperature field during filling is more uniform, and the solidification front progresses more orderly from the point of fill initiation towards the last areas to fill. This orderly progression is crucial for establishing directional solidification, which is key to feeding shrinkage effectively. The thermal behavior can be further analyzed by considering the thermal modulus, a geometric factor influencing solidification time. For a section of the casting, the solidification time $t_s$ is roughly proportional to the square of the volume-to-surface-area ratio (Chvorinov’s rule):
$$ t_s = B \left( \frac{V}{A} \right)^n $$
where $B$ is a mold constant, $V$ is volume, $A$ is surface area, and $n$ is an exponent typically close to 2. In the recessed zone, $V/A$ is relatively small, making it susceptible to early solidification. In Scheme A, the added heat from turbulent dissipation increases the local metal temperature, effectively increasing the local $V/A$ ratio by delaying the start of solidification, but this also creates a “hot spot” that solidifies last, isolated from feeding paths, leading to shrinkage porosity. Scheme B avoids this by not introducing excessive heat in that zone.
To quantify the thermal aspects, I consider a simplified heat transfer model for the metal in the recess zone. The rate of temperature change due to convection and conduction can be modeled. Assuming a lumped parameter approach for a small control volume, the energy balance during filling and initial cooling can be expressed as:
$$ \frac{dT}{dt} = \frac{h A_s}{\rho V C_p} (T_m – T) + \frac{\dot{q}_{turb}}{\rho C_p} $$
where $h$ is heat transfer coefficient, $A_s$ is surface area of the volume, $T_m$ is mold temperature, and $\dot{q}_{turb}$ represents turbulent heating per unit volume, which is significant in Scheme A but negligible in Scheme B. Integrating this equation shows that for Scheme A, the temperature decay is slower due to the $\dot{q}_{turb}$ term, extending the local solidification time and creating conditions ripe for shrinkage formation.
The superiority of the simpler gating system in this case study aligns with a growing understanding in precision investment casting: complexity in gating is not always beneficial. For components with simple geometries—defined here as those without drastic changes in section thickness, isolated heavy sections, or intricate internal passages—a gating system that prioritizes smooth, laminar flow often outperforms a more complex system designed primarily for intensive feeding. Complex gating can introduce unintended turbulence, flow separation, and uneven thermal profiles, which counteract their intended benefits. This principle is particularly relevant in precision investment casting of nickel-based superalloys like K424, which have a narrow solidification range and are prone to formation of microporosity if solidification is not carefully controlled.
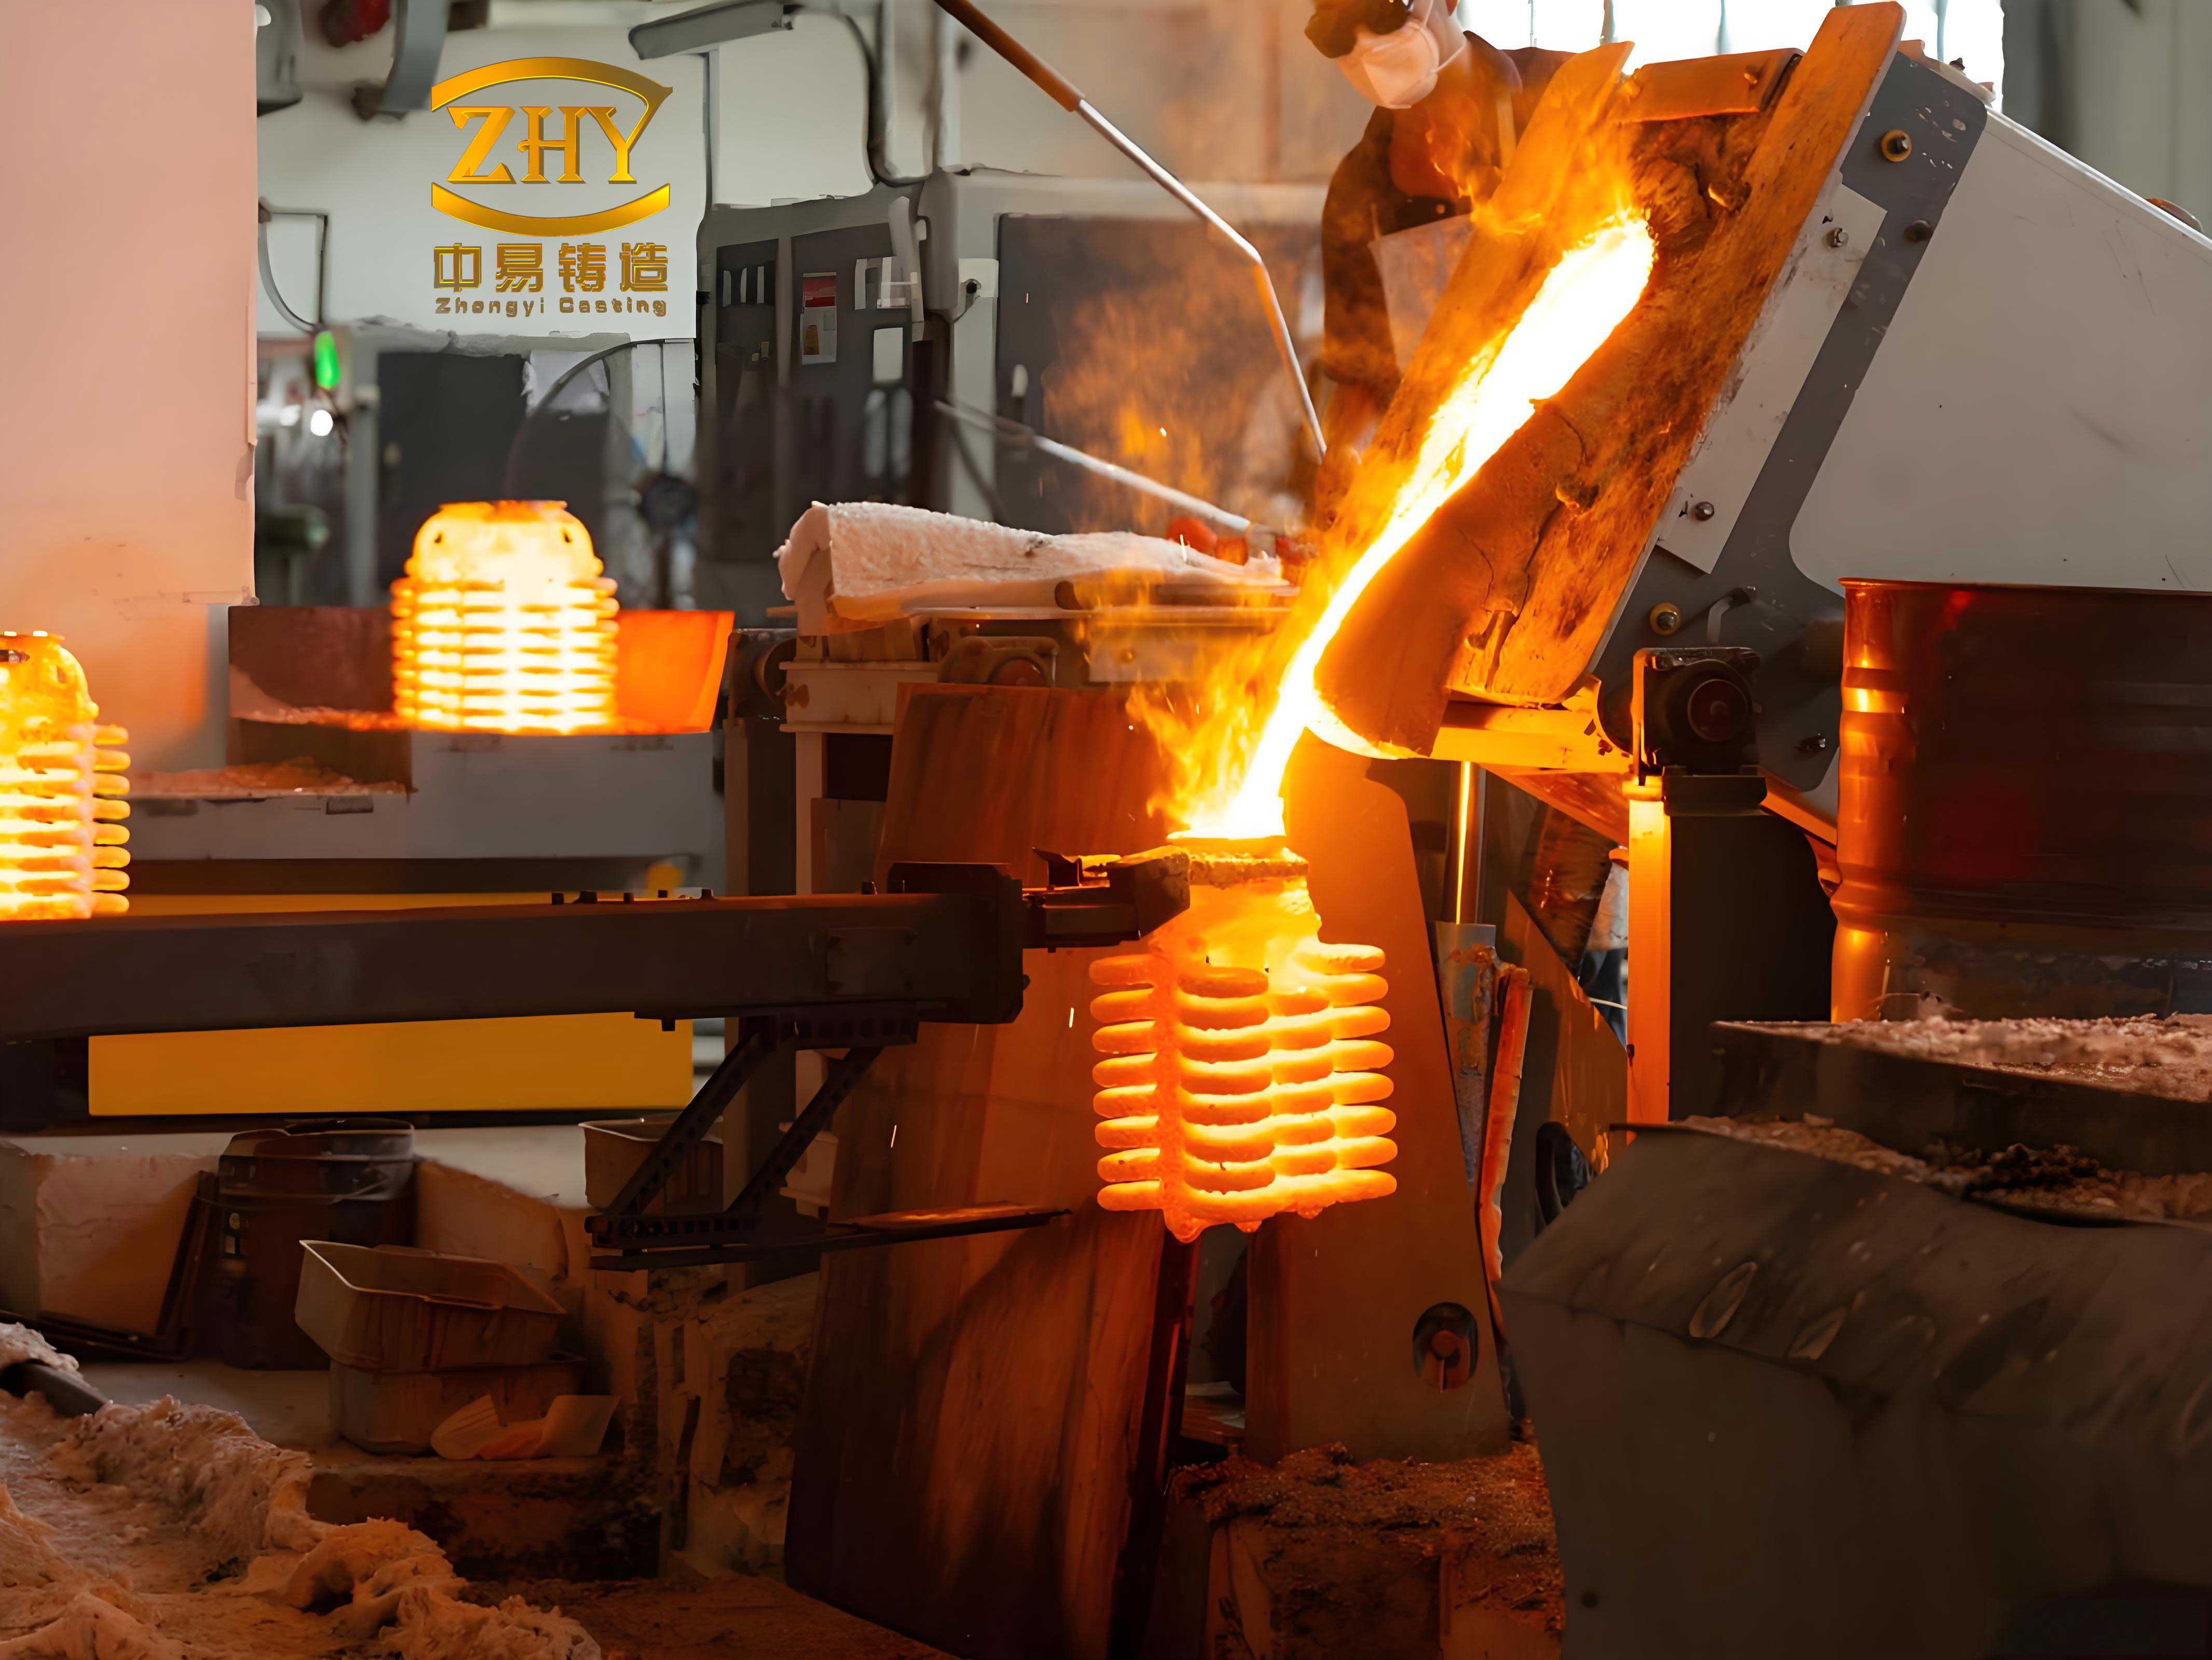
The image above provides a visual reference for the precision investment casting process, illustrating the intricate ceramic shells and the level of detail achievable. This technology is indispensable for aerospace components where performance and reliability are non-negotiable. In the context of this study, the ceramic shell integrity, influenced by the pattern quality from rapid prototyping, provided a consistent mold environment, allowing the gating design to be the sole variable under investigation.
Expanding the discussion, I can formalize a decision matrix for gating system selection in precision investment casting based on component geometry complexity. This matrix, presented in Table 4, incorporates factors such as flow stability, feeding requirement, and defect risk.
| Component Geometry Complexity | Recommended Gating Philosophy | Key Design Focus | Expected Defect Risks if Mismatched |
|---|---|---|---|
| Simple (Uniform sections, no isolated masses) | Simplistic, Laminar-Flow Promoting | Minimize turbulence, directional filling | Shrinkage in unintended hot spots, oxide inclusions |
| Moderate (Moderate thickness variations, some cores) | Balanced | Controlled filling with targeted feeders | Misruns, localized shrinkage |
| Complex (Extreme section changes, internal cavities) | Complex, Multi-feeder Systems | Ensured feed metal accessibility, temperature control | Gross shrinkage, hot tears, core blows |
For the inner ring, classified as simple, Scheme B embodies the recommended philosophy. The mathematical justification for favoring laminar flow can be further solidified by considering the momentum dissipation. Turbulent flows have higher effective viscosity due to eddy formation, which increases shear stress and pressure drop. The pressure head required to fill the mold, $H_{req}$, can be estimated using an extended Bernoulli equation with head loss terms:
$$ H_{req} = \frac{p_2 – p_1}{\rho g} + (z_2 – z_1) + \frac{u_2^2 – u_1^2}{2g} + h_{L} $$
where subscripts 1 and 2 denote two points in the flow path, $z$ is elevation, and $h_L$ is head loss due to friction and minor losses (bends, contractions, expansions). For turbulent flow, $h_L$ is larger, potentially requiring a higher pouring head or leading to incomplete filling if not accounted for. However, in vacuum precision investment casting, gravity pouring is common, and the head is fixed. Thus, excessive $h_L$ can result in sluggish filling, allowing premature solidification in thin sections. While not an issue in this study due to sufficient head, it illustrates another downside of unnecessary complexity.
Furthermore, the defect formation can be modeled probabilistically. Let $P_{defect}$ be the probability of shrinkage porosity in a critical zone. It can be related to local solidification time $t_s$ and temperature gradient $G$ at the end of filling. A semi-empirical relationship might be:
$$ P_{defect} = \alpha \exp\left(-\beta G \sqrt{t_s}\right) + \gamma $$
where $\alpha, \beta, \gamma$ are material-dependent constants. In Scheme A, $G$ is lower and $t_s$ is longer in the recess due to turbulent heating, increasing $P_{defect}$. Scheme B maintains higher $G$ and shorter $t_s$ there, reducing $P_{defect}$.
In conclusion, this detailed investigation into gating system design for a guider inner ring via precision investment casting has demonstrated that a simplistic gating approach can significantly enhance internal quality for components with simple geometry. The comparative trials showed an 80% defect rate with a complex, feeding-oriented design (Scheme A) versus a 13.3% defect rate with a simple, flow-oriented design (Scheme B). The underlying fluid dynamics and heat transfer analysis, supported by fundamental equations, reveal that turbulent flow convergence and localized superheating are the primary culprits for shrinkage porosity in the complex scheme. Therefore, the paradigm for gating design in precision investment casting should be tailored to component complexity: simplicity and flow control take precedence for geometrically simple parts. This insight not only advances the specific application but also contributes to the broader body of knowledge in precision investment casting, guiding engineers toward more reliable and efficient manufacturing routes for critical aerospace components. Future work could involve computational fluid dynamics (CFD) simulations to quantitatively predict flow patterns and temperature fields for new designs, further optimizing the precision investment casting process.