
The development of wear-resistant materials is critical for industries such as cement production, power generation, and mining, where components are subjected to severe abrasive and corrosive environments. Among the various candidate materials, high-chromium white cast iron stands out due to its exceptional combination of hardness, toughness, and corrosion resistance, particularly when the chromium content exceeds 24%. This family of alloys derives its properties from a hard microstructure comprising chromium carbides embedded within a metallic matrix. However, the as-cast structure often contains a significant amount of metastable austenite, which is relatively soft and unstable. Therefore, heat treatment is an essential and definitive step to unlock the full potential of high-chromium white cast iron, transforming the matrix to a harder martensitic structure and optimizing the carbide distribution.
This study presents a comprehensive investigation into the heat treatment of white cast iron with chromium contents ranging from 10% to 28%. The primary objective is to establish a systematic understanding of how austenitizing temperature, cooling method, and tempering temperature interact with the alloy composition to determine the final hardness, toughness, and wear resistance. By identifying the optimal heat treatment parameters for each chromium level, this work aims to provide a foundational guide for industrial practice, enabling the reliable production of high-performance wear parts.
1. Experimental Methodology
The research was conducted using a series of seven different high-chromium white cast iron compositions. The alloys were prepared in a 150 kg medium-frequency induction furnace. Raw materials included carbon steel scrap, high- and low-carbon ferrochromium, and ferromolybdenum. The melt was superheated to between 1550°C and 1650°C before pouring into sand molds at a temperature range of 1420°C to 1480°C. Final deoxidation was performed with aluminum, and a rare-earth alloy was used for modification to refine the as-cast structure.
The chemical compositions of the seven white cast iron variants, determined via spectroscopic analysis, are detailed in Table 1. The carbon content was maintained between 2.4% and 2.8%, while chromium was systematically varied from approximately 10% to 28%. Molybdenum was added in the range of 0.4% to 0.7% to enhance hardenability and tempering resistance.
| Designation | C | Si | Mn | Cr | Mo | S | P |
|---|---|---|---|---|---|---|---|
| 10Cr | 2.46 | 0.69 | 0.41 | 10.57 | 0.40 | 0.045 | 0.057 |
| 13Cr | 2.43 | 0.70 | 0.52 | 12.90 | 0.54 | 0.031 | 0.069 |
| 15Cr | 2.39 | 0.64 | 0.75 | 15.98 | 0.49 | 0.046 | 0.050 |
| 19Cr | 2.52 | 0.62 | 0.56 | 19.35 | 0.62 | 0.035 | 0.047 |
| 24Cr | 2.68 | 0.67 | 0.49 | 24.02 | 0.48 | 0.040 | 0.048 |
| 26Cr | 2.73 | 0.63 | 0.71 | 26.57 | 0.72 | 0.036 | 0.042 |
| 28Cr | 2.79 | 0.59 | 0.68 | 28.04 | 0.50 | 0.041 | 0.039 |
1.1 Heat Treatment Procedures
All heat treatments were carried out in a box-type resistance furnace. A two-stage heating process was employed to minimize thermal stress: a preheat at 650°C for 2.5 hours followed by austenitization at the target temperature.
Austenitization and Quenching: Specimens from each white cast iron composition were austenitized at temperatures of 900°C, 930°C, 960°C, 1000°C, 1050°C, and 1120°C for 2.5 hours. Following austenitization, two quenching media were used: forced air cooling (fan quenching) and oil quenching using N32 grade oil. The resulting as-quenched hardness (HRC) was measured at five points on each specimen and averaged; the results are consolidated in Table 2.
Tempering: Specimens that exhibited peak hardness in the as-quenched condition were selected for tempering studies. These samples were tempered at 200°C, 300°C, 400°C, 500°C, and 600°C for 4 hours. After tempering, hardness was measured again. Furthermore, standard un-notched Charpy impact specimens (10 mm x 10 mm x 55 mm) were machined from the tempered samples and tested. The tempered hardness and impact toughness (aK) data are presented in Table 3.
| Aust. Temp. (°C) | 10Cr | 13Cr | 15Cr | 19Cr | 24Cr | 26Cr | 28Cr | |||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Air | Oil | Air | Oil | Air | Oil | Air | Oil | Air | Oil | Air | Oil | Air | Oil | |
| 900 | 57.1 | 64.1 | 54.9 | 62.7 | 54.8 | 60.3 | 56.0 | – | – | – | – | – | – | – |
| 930 | 61.9 | 63.9 | 57.8 | 65.3 | 54.9 | 63.1 | 57.9 | 57.4 | 57.8 | 59.5 | – | – | – | 59.3 |
| 960 | 57.5 | 59.5 | 62.7 | 63.5 | 63.1 | 64.9 | 59.8 | 62.9 | 60.5 | 63.0 | 60.9 | 60.7 | – | 59.7 |
| 1000 | 53.5 | 51.5 | 55.2 | 60.9 | 62.9 | 63.1 | 62.7 | 65.4 | 62.3 | 64.8 | 61.9 | 64.3 | 62.1 | 62.5 |
| 1050 | 48.0 | 49.5 | 51.6 | 52.4 | 57.1 | 56.0 | 63.7 | 63.1 | 63.4 | 63.5 | 62.7 | 63.7 | 63.0 | 62.9 |
| 1120 | – | – | – | – | – | – | 59.3 | – | 62.3 | 59.3 | 62.7 | 61.2 | 62.9 | 63.7 |
| Sample (Composition & Quench) | 200°C | 300°C | 400°C | 500°C | 600°C | |||||
|---|---|---|---|---|---|---|---|---|---|---|
| HRC | aK (J/cm²) | HRC | aK (J/cm²) | HRC | aK (J/cm²) | HRC | aK (J/cm²) | HRC | aK (J/cm²) | |
| 10Cr, 900°C Oil | 63.7 | 3.2 | 60.5 | 3.4 | 64.1 | 3.5 | 62.5 | 3.8 | 54.1 | 4.0 |
| 13Cr, 960°C Air | 61.2 | 3.7 | 60.3 | 3.8 | 62.4 | 3.9 | 60.1 | 3.6 | 57.5 | 4.2 |
| 13Cr, 930°C Oil | 63.9 | 3.6 | 62.5 | 3.1 | 64.7 | 4.2 | 62.7 | 3.4 | 56.7 | 4.1 |
| 15Cr, 960°C Air | 62.0 | 3.8 | 62.9 | 3.8 | 63.0 | 4.0 | 60.0 | 4.2 | 55.3 | 4.6 |
| 15Cr, 960°C Oil | 63.1 | 4.0 | 62.4 | 3.9 | 64.3 | 3.7 | 62.9 | 3.9 | 55.7 | 4.2 |
| 19Cr, 1050°C Air | 63.1 | 3.7 | 63.4 | 3.7 | 62.9 | 4.3 | 63.5 | 3.7 | 57.3 | 4.5 |
| 19Cr, 1000°C Oil | 63.2 | 3.9 | 62.7 | 3.8 | 63.9 | 3.8 | 64.5 | 3.6 | 59.5 | 4.1 |
| 24Cr, 1000°C Oil | 63.9 | 4.0 | 62.5 | 3.7 | 64.0 | 3.9 | 63.5 | 3.7 | 60.5 | 3.9 |
| 26Cr, 1000°C Oil | 63.5 | 3.7 | 62.9 | 3.5 | 64.6 | 3.9 | 64.1 | 3.8 | 60.5 | 3.9 |
| 26Cr, 1050°C Air | 62.1 | 4.5 | 62.0 | 4.0 | 62.9 | 3.6 | 63.6 | 4.0 | 59.7 | 4.0 |
| 28Cr, 1120°C Oil | 63.0 | 3.7 | 61.5 | 3.9 | 62.1 | 3.9 | 63.9 | 3.9 | 62.1 | 3.9 |
1.2 Microstructural and Property Evaluation
Metallographic samples were prepared from as-cast, as-quenched, and quenched-and-tempered conditions. They were etched with 4-15% nital solution and examined under an optical microscope. The key microstructural features for each state are described in the discussion section.
Abrasive Wear Testing: Dry sand abrasive wear tests were conducted on selected heat-treated samples (10Cr, 13Cr, 15Cr, 28Cr) using an MLD-10 dynamic load abrasion tester. The abrasive was quartz sand with a particle size of 0.212-0.425 mm. The tests ran for 3 hours under an impact energy of 2.5 J.
Corrosive-Abrasive Wear Testing: To evaluate corrosion-wear resistance, samples of the 26% chromium white cast iron in both as-cast and heat-treated conditions were tested in a slurry of quartz sand (0.106-0.150 mm) and dilute sulfuric acid (pH = 4.5). The mass loss was measured at 1-hour intervals using a precision balance. The wear data is summarized in Table 4.
| Material & Condition | Test Type | Mass Loss (g) | Avg. Wear Rate (g/h) |
|---|---|---|---|
| Hour 1 | Hour 2 | Hour 3 | Total | |||
| 10Cr, 900°C Oil + 380°C Temp | Dry Abrasion | 1.0954 | 1.4782 | 0.3185 | 2.8921 | 0.9641 |
| 13Cr, 930°C Oil + 400°C Temp | Dry Abrasion | 1.6789 | 1.0987 | 0.1987 | 2.9763 | 0.9921 |
| 15Cr, 960°C Air + 400°C Temp | Dry Abrasion | 1.1446 | 0.3589 | 0.2185 | 1.7220 | 0.5740 |
| 28Cr, 1120°C Oil + 520°C Temp | Dry Abrasion | 0.3911 | 0.0757 | 0.0616 | 0.5284 | 0.1761 |
| 26Cr, As-Cast | Corrosion-Abrasion | 17.2545 | 13.8975 | 10.9768 | 42.1288 | 14.0429 |
| 26Cr, 930°C Air + 450°C Temp | Corrosion-Abrasion | 28.9436 | 27.4503 | 24.4324 | 80.8263 | 26.9421 |
| 26Cr, 960°C Air + 450°C Temp | Corrosion-Abrasion | 24.9738 | 20.4593 | 26.4982 | 71.9313 | 23.9771 |
| 26Cr, 1050°C Air + 500°C Temp | Corrosion-Abrasion | 15.7653 | 13.0432 | 9.4327 | 38.2412 | 12.7471 |
2. Results and Analysis
2.1 Microstructural Evolution
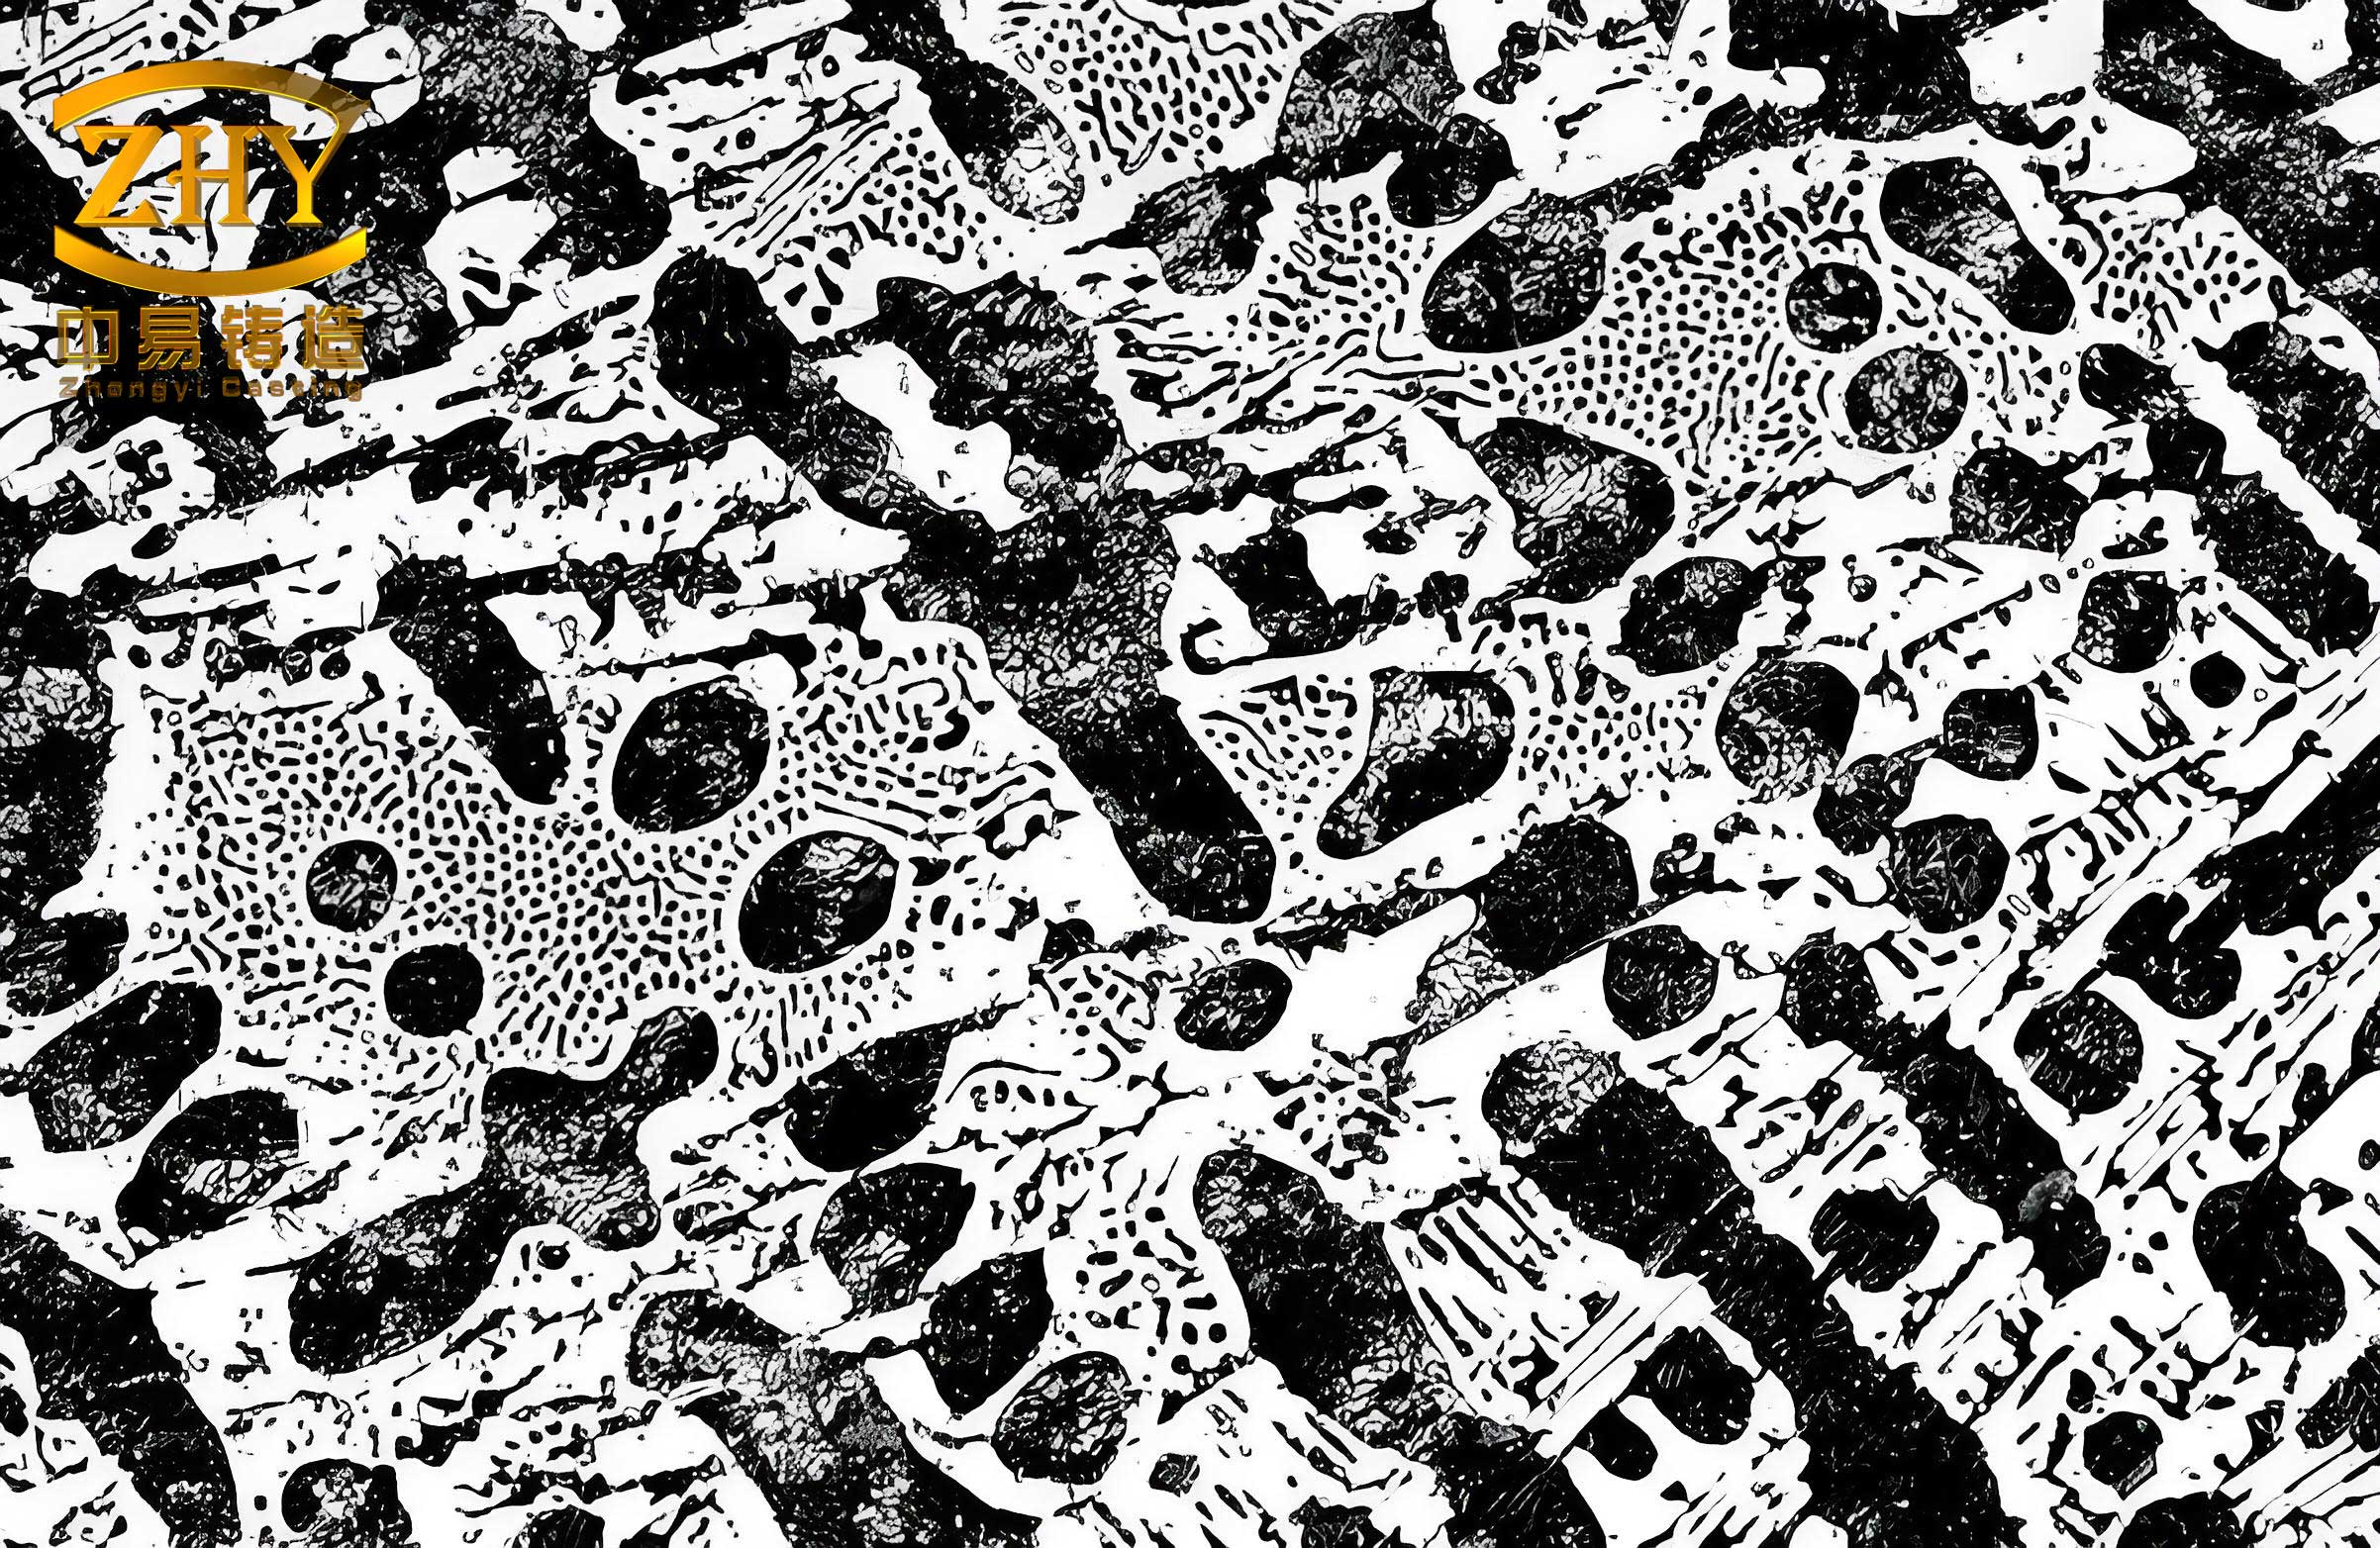
The microstructure of the as-cast high-chromium white cast iron consisted of primary and/or eutectic chromium carbides (M7C3) in a matrix of austenite, with some localized areas of transformed products like troostite. Upon quenching from the austenitizing temperature, the matrix transformed to martensite, but a certain volume fraction of retained austenite was always present. The final microstructure after the complete quench-and-temper cycle comprised the stable eutectic carbides, secondary carbides precipitated from the matrix during tempering, and tempered martensite. A key observation was that increasing the alloy content (Cr, Mo) led to significant grain refinement and a more uniform, finer distribution of carbides in the white cast iron.
2.2 The Influence of Austenitizing Temperature on Hardness
The data in Table 2 reveals a fundamental relationship: for a given white cast iron composition and cooling method, there exists a specific austenitizing temperature that yields peak hardness. This can be expressed as finding the temperature TA_peak that maximizes hardness H for a given composition C and cooling rate q:
$$ T_{A\_peak} = \arg \max_{T_A} \, H(C, T_A, q) $$
For example, for oil quenching, the peak hardness for the 13% Cr white cast iron occurred at 930°C, for the 15% Cr at 960°C, and for the 26% Cr at 1000°C. This trend is visualized in Figure 2, which shows that TA_peak increases with chromium content. The underlying mechanism involves the solubility of carbon and alloying elements in austenite. Below TA_peak, the austenite is undersaturated, leading to excessive secondary carbide precipitation during heating and an austenite matrix lean in carbon and alloys, resulting in lower hardenability and softer martensite. Above TA_peak, carbon and chromium dissolve extensively into the austenite, increasing its stability. This leads to a higher amount of soft retained austenite after quenching, thereby reducing overall hardness. TA_peak represents the optimal balance where the austenite is sufficiently saturated to form hard martensite upon quenching but not so saturated as to become highly stable.
Furthermore, the activation energy for carbon diffusion in austenite increases with the concentration of strong carbide formers like chromium and molybdenum. This can be conceptually related by an Arrhenius-type relationship where the effective diffusion coefficient D is reduced:
$$ D_{eff} \propto \exp\left(-\frac{Q_0 + \alpha \cdot [Cr] + \beta \cdot [Mo]}{RT_A}\right) $$
where Q0 is the base activation energy, α and β are coefficients, [Cr] and [Mo] are concentrations, R is the gas constant, and TA is the austenitizing temperature. The reduced diffusivity at higher alloy levels necessitates a higher temperature (TA_peak) to achieve the same degree of homogenization and carbon/chromium partitioning required for optimal hardening in these white cast irons.
2.3 Effect of Quenching Medium
A consistent finding across all compositions was the superiority of oil quenching over air quenching for achieving higher and more consistent hardness in white cast iron (see Table 2). Air cooling, being slower, allows for more significant precipitation of secondary carbides during the continuous cooling transformation. This depletes the austenite of carbon and alloying elements, lowering its hardenability and resulting in a lower-carbon, softer martensite. In contrast, the faster cooling rate of oil suppresses this precipitation to a more optimal level, preserving a higher carbon content in the austenite which transforms into harder martensite. Additionally, the favorable cooling characteristics of oil in the martensite transformation range (Ms to Mf) help reduce the risk of quench cracking. Oil quenching also proved more robust against seasonal ambient temperature variations, which can adversely affect the consistency of air-quenched hardness in white cast iron components.
2.4 Tempering Behavior and Secondary Hardening
The tempering response of high-chromium white cast iron is complex due to the interplay of several phenomena. The data in Table 3 illustrates this clearly. Tempering at 200-300°C primarily relieves quench stresses with only a slight decrease in hardness, as the martensite retains a high carbon concentration.
In the range of 400-500°C, two competing processes occur simultaneously: (1) the continued decomposition of martensite, which tends to lower hardness, and (2) the decomposition of retained austenite into fresh, hard martensite or bainite upon cooling (often called “secondary quenching”), which tends to increase hardness. The net effect is a hardness peak at a specific tempering temperature Ttemp_peak. This peak temperature is composition-dependent, shifting to higher values with increased alloy content:
$$ T_{temp\_peak} \approx f([Cr], [Mo]) $$
For instance, Ttemp_peak was ~400°C for 10-15% Cr white cast iron, ~450°C for 19-24% Cr, and 500-540°C for 26-28% Cr. This shift is due to the increased thermal stability of both the martensite and the retained austenite imparted by higher chromium and molybdenum levels.
A pronounced secondary hardening effect was observed specifically in the 26% and 28% chromium white cast irons. Samples that were slightly under-hardened after quenching (e.g., exhibiting lower than expected as-quenched hardness) could recover full hardness when tempered at 500°C or 540°C, respectively. This is attributed to a significant volume of highly alloyed retained austenite transforming to martensite during the tempering cycle’s cooling stage. This phenomenon provides a valuable processing window where slightly sub-optimal quenching can be corrected during tempering, while still effectively relieving stresses.
At 600°C, over-tempering occurs. Coarse, spheroidized carbides precipitate, losing their potent dispersion-strengthening effect, and the matrix softens considerably, leading to a significant drop in hardness for all grades of white cast iron.
2.5 Wear and Corrosion-Wear Performance
The dry abrasive wear data in Table 4 demonstrates the dramatic improvement in wear resistance with increasing chromium content and proper heat treatment. The 28% Cr white cast iron, subjected to high-temperature austenitization and tempering, exhibited a wear rate nearly an order of magnitude lower than the 10% Cr material. This is a direct result of its harder, more stable matrix and a higher volume fraction of harder (Cr,Fe)7C3 carbides.
The corrosion-wear tests on the 26% chromium white cast iron yielded particularly insightful results. Contrary to some previous literature, the heat-treated condition (1050°C air cool + 500°C temper) showed superior resistance to the corrosive-abrasive slurry compared to the as-cast material. The wear rate for the heat-treated sample was 12.75 g/h, significantly better than the as-cast rate of 14.04 g/h, and vastly superior to samples treated at lower austenitizing temperatures. The relationship between austenitizing temperature and corrosive-abrasive wear loss W for the 26Cr alloy can be modeled as a decreasing function:
$$ W \propto \exp(-k \cdot T_A) \quad \text{for a fixed tempering condition} $$
where k is a positive constant. This improvement is metallurgically sound. Higher austenitizing temperatures increase the carbon and chromium content in solid solution within the austenite matrix. Upon transformation, this leads to a matrix with a higher overall electrode potential. Consequently, the electrochemical potential difference between the carbide phases and the matrix is reduced, diminishing the driving force for galvanic corrosion in the corrosive environment. Thus, a properly heat-treated high-chromium white cast iron offers not just better abrasion resistance, but also enhanced performance in combined corrosion-wear situations.
3. Conclusions
This systematic study on the heat treatment of high-chromium white cast iron, with chromium contents ranging from 10% to 28%, has led to the establishment of clear, practical guidelines and a deeper understanding of the underlying metallurgical principles.
- A Generalized Heat Treatment Rule: A fundamental rule for this family of white cast irons is that higher chromium contents require higher austenitizing and tempering temperatures. For example, low-chromium (10-13% Cr) white cast iron performs best with a treatment like 900-960°C oil quench + 360-400°C temper, while high-chromium (26-28% Cr) white cast iron requires 1050-1120°C oil/air quench + 500-540°C temper.
- Optimal Austenitizing Temperature (TA_peak): For a given composition and quenchant, a specific austenitizing temperature yields peak hardness. This temperature increases with the chromium content of the white cast iron due to the reduced diffusivity of carbon in alloy-rich austenite, necessitating higher thermal energy for optimal carbide dissolution and matrix homogenization.
- Superiority of Oil Quenching: Oil quenching is consistently more effective than air quenching for high-chromium white cast iron. It provides a faster cooling rate that optimizes secondary carbide suppression, resulting in higher and more reproducible hardness. It also offers better resistance to quench cracking and is less sensitive to ambient conditions.
- Tempering and Secondary Hardening: The tempering peak hardness shifts to higher temperatures with increasing alloy content. A distinctive secondary hardening phenomenon, allowing for hardness recovery, is prominent in very high-chromium (≥26% Cr) white cast irons when tempered at 500-540°C. This provides a useful corrective mechanism for quenching variations.
- Enhanced Corrosion-Wear Resistance: Proper high-temperature heat treatment significantly improves the corrosion-abrasion resistance of high-chromium (e.g., 26% Cr) white cast iron compared to its as-cast state. This is achieved by elevating the matrix’s electrode potential through increased solute content, thereby reducing galvanic corrosion activity with the carbides.
In summary, the performance of high-chromium white cast iron is not inherent but is critically engineered through heat treatment. The guidelines derived from this study enable the tailored optimization of hardness, toughness, and wear-corrosion resistance based on the specific alloy composition, providing a reliable foundation for manufacturing high-performance, durable components for the most demanding industrial applications.