
In my own practice, I have come to view investment casting not as a single operation but as a chain of tightly coupled decisions. Each decision begins with the geometry of the part and ends with the metallurgical condition of the delivered component. When I examine a casting problem, I first ask whether the intended shape can be reproduced by a consumable pattern, whether the shell can survive thermal shock, and whether the alloy can fill the cavity before solidification closes the critical sections. These questions place investment casting close to other precision routes, yet they also distinguish it from evaporative pattern casting, where a foam pattern is vaporized by the incoming metal. In investment casting, the pattern is removed before pouring, so the mold is empty when the liquid metal arrives. That difference shapes nearly every process parameter I select. It also explains why I keep returning to evaporative pattern casting as a useful comparison: both routes rely on a sacrificial pattern, both demand careful dimensional compensation, and both succeed or fail on the basis of filling, feeding, and shell or mold stability. However, investment casting offers a distinct advantage when the part has thin walls, fine surface detail, or internal passages that must be reproduced with high fidelity. For titanium alloy impellers and similar components, that advantage is often decisive.
My aim in this article is to set out a first-person, engineering-oriented account of investment casting technology and equipment. I will describe the process from pattern making through shell building, dewaxing, melting, pouring, cleaning, inspection, and post-processing. I will use tables and formulas to summarize the relationships that matter most in production. I will also discuss the role of rapid prototyping, especially stereolithography, in shortening the path from design to casting. Throughout, I will keep the keyword evaporative pattern casting in view, because comparing investment casting with evaporative pattern casting helps clarify why certain equipment and process choices are made. In some low-volume or large-part applications, evaporative pattern casting can be attractive because it avoids wax injection and shell removal. In high-precision, thin-wall, reactive-alloy applications, investment casting usually remains the stronger option. My own experience with titanium impellers has reinforced that conclusion.
Process Principles and Workflow
Investment casting, often called lost-wax casting, uses a fusible or dissolvable pattern. I typically begin with a wax or plastic pattern that replicates the final part, including machining allowance, shrinkage allowance, and draft where needed. The pattern is assembled onto a runner and gate system. Then I coat the assembly with refractory slurry and stucco repeatedly until a ceramic shell of sufficient thickness and strength forms. After the shell dries, I remove the pattern by heating, melting, burning, or dissolving it. The resulting cavity is fired, preheated, and filled with molten metal. Once solidification is complete, I break the shell, cut off the gates, clean the surface, heat treat if required, and inspect the casting. This sequence is simple to describe but difficult to control. Every step introduces dimensional change, thermal stress, or contamination risk.
When I compare this sequence with evaporative pattern casting, I notice that evaporative pattern casting leaves the pattern in place and relies on the metal front to decompose the foam. That means the mold filling and pattern removal occur simultaneously. In investment casting, pattern removal occurs before pouring. This separation gives me more freedom to verify the cavity, preheat the shell uniformly, and select a pouring atmosphere without worrying about foam decomposition products. It also means that investment casting can use reactive alloys such as titanium with less risk of carbon pickup, although oxygen and nitrogen pickup remain serious concerns. For this reason, I treat shell chemistry, binder selection, and vacuum quality as first-order variables rather than secondary details.
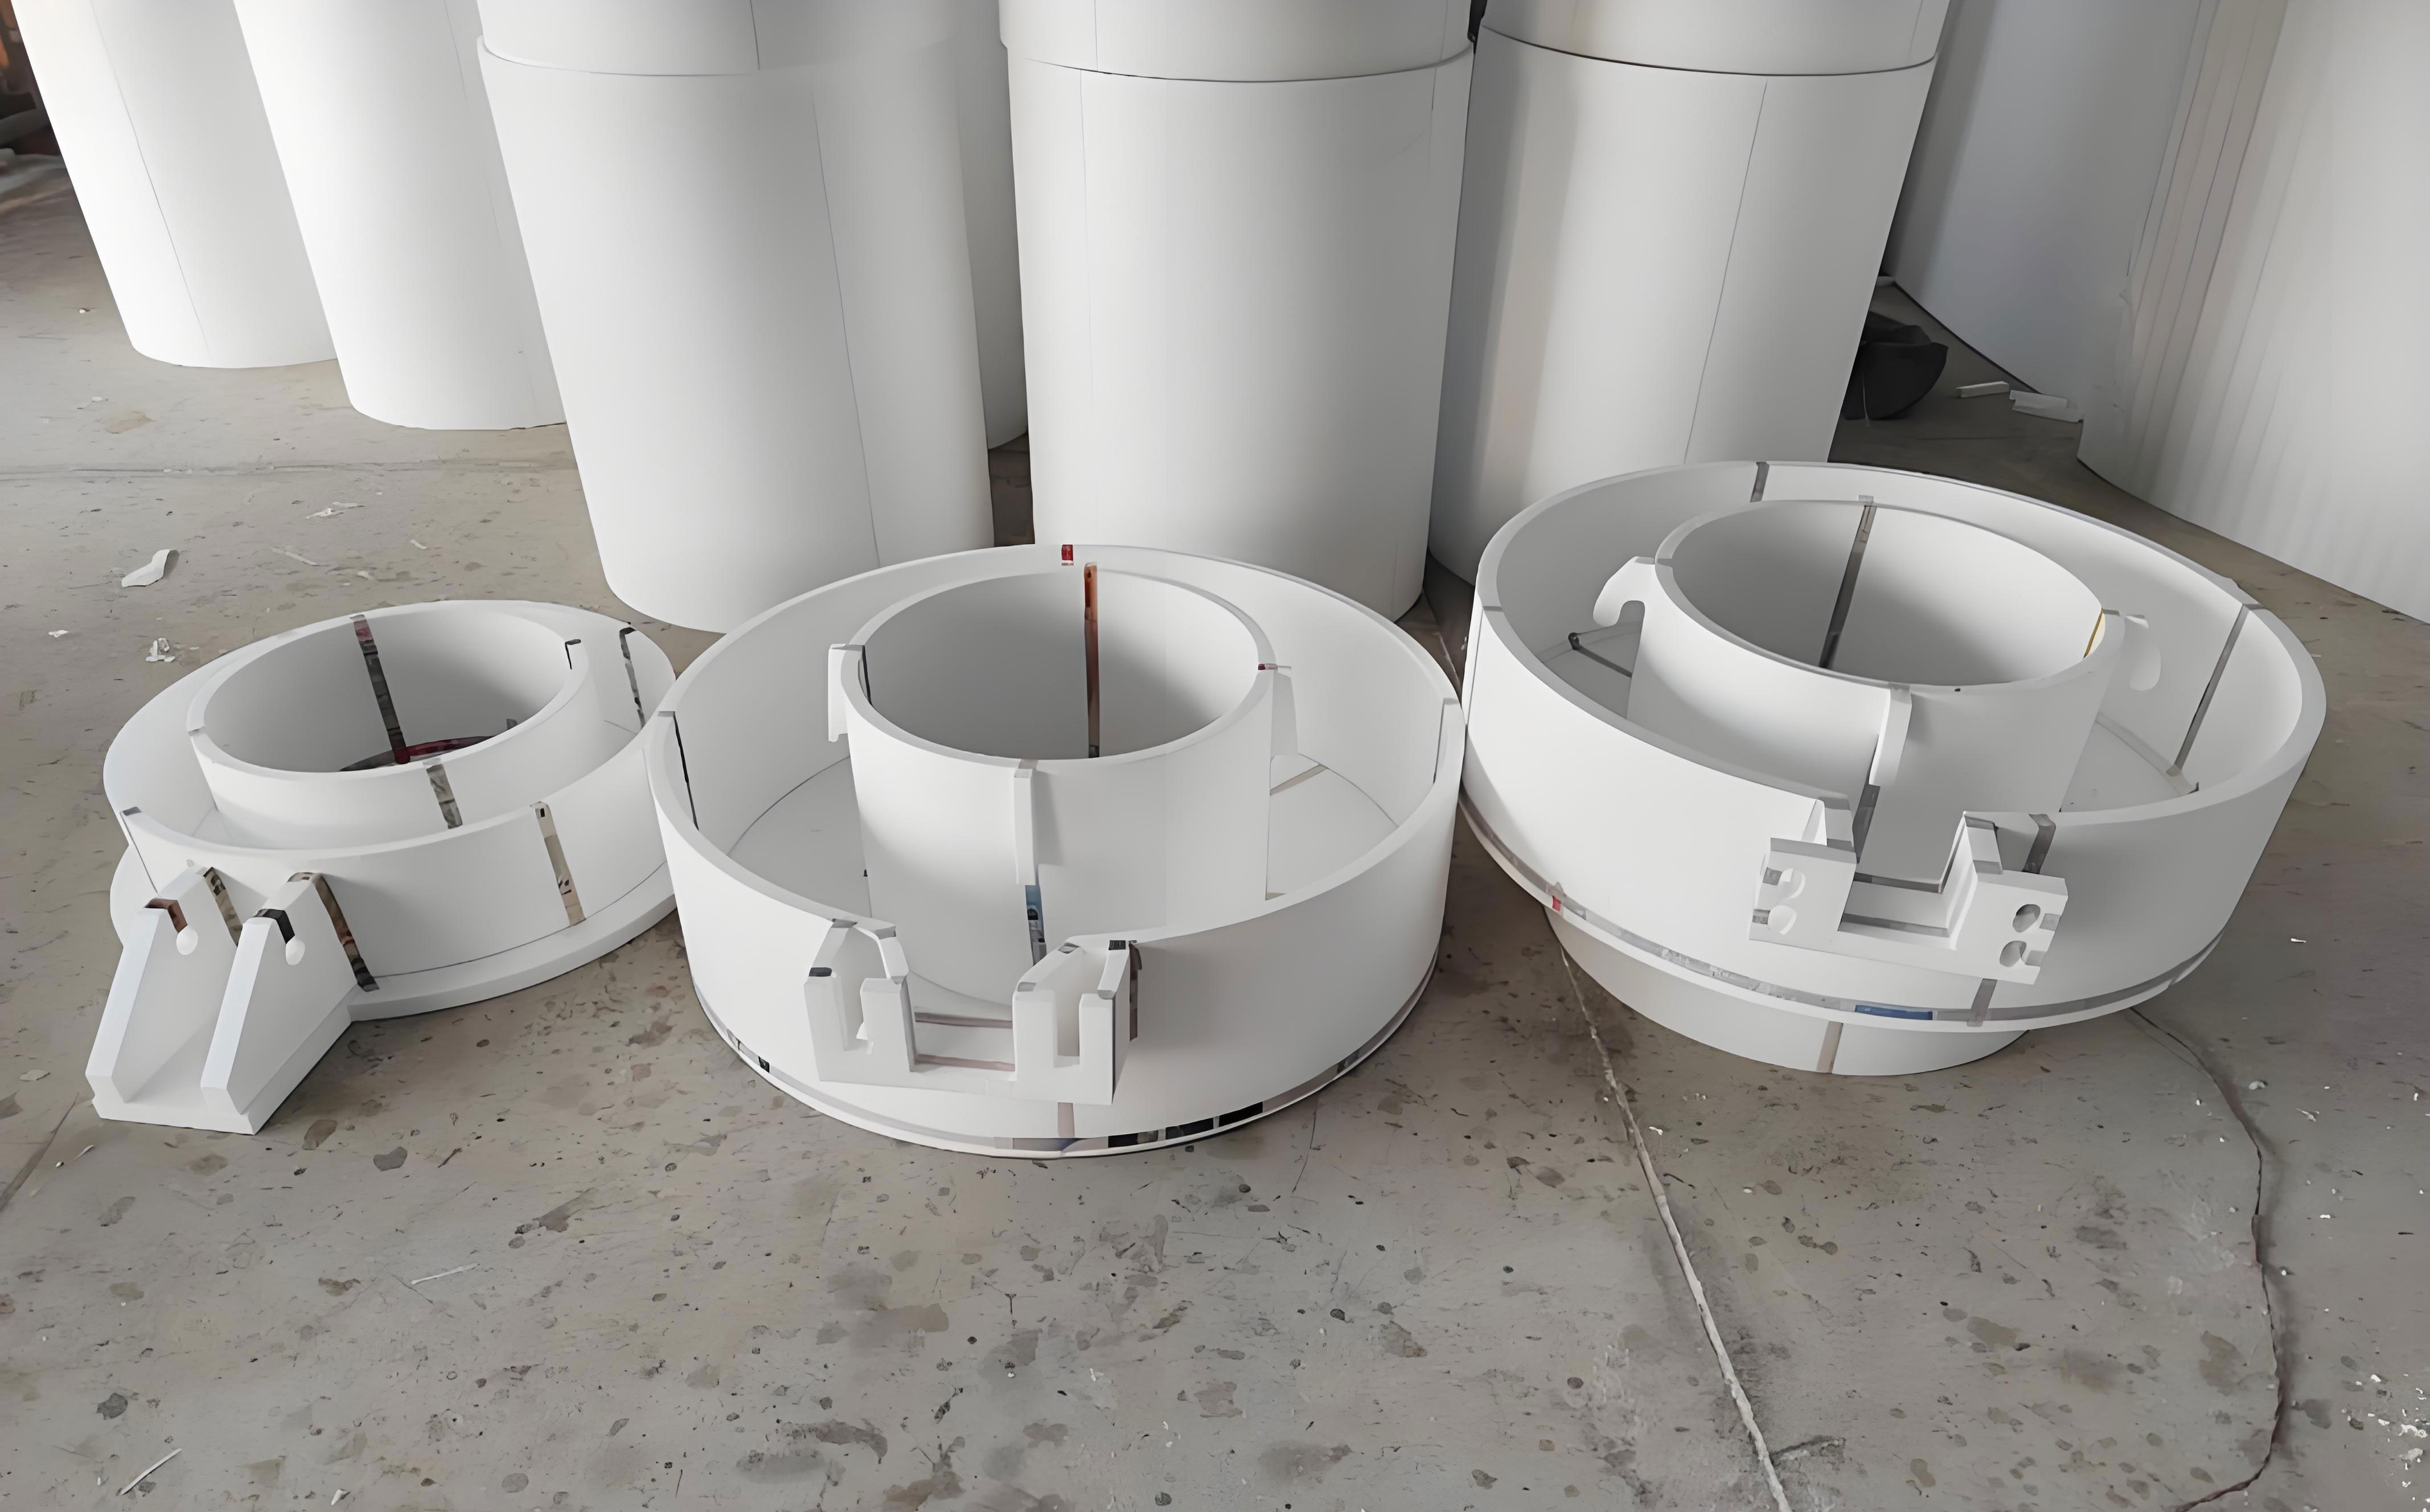
The workflow I use for a typical precision casting can be summarized as follows. I first define the part geometry and tolerances. I then design the wax pattern die or choose an additive manufacturing route. Next, I determine the shrinkage allowances and gate system. After that, I build and test the ceramic shell. Finally, I establish melting, pouring, and inspection parameters. Each stage feeds back into the previous ones. If the trial casting shows shrinkage porosity, I may change the gate location, increase the feed path, adjust the pouring temperature, or modify the centrifugal speed. If the shell cracks, I may change the binder, the stucco grading, the drying schedule, or the firing profile. In my view, the most successful investment casting projects are those in which the engineer treats the process as a system rather than a list of independent operations. This systems view also helps when I evaluate whether evaporative pattern casting might be a better fit for a particular production volume or geometry.
Key Process Parameters and Their Relationships
I have found that investment casting quality depends on a relatively small set of parameters. These include wax injection temperature and pressure, shell thickness, binder concentration, drying time, firing temperature, melt superheat, pouring rate, centrifugal speed, and mold preheat. The interactions among them are not linear, and small changes can shift the defect population from one mode to another. Therefore, I use formulas to estimate starting points, then refine them with trials and simulation. For example, the centrifugal speed in a vertical or horizontal centrifugal casting machine can be estimated from the required gravity coefficient and the casting radius. A common expression is:
$$ n = 29.9 \sqrt{\frac{G}{R}} $$
Here, \(n\) is the rotational speed in revolutions per minute, \(G\) is the gravity coefficient, and \(R\) is the inner surface radius in centimeters. When \(G\) is greater than approximately 10, the centrifugal force is usually sufficient to improve feeding and density in thin-wall castings. I often start with \(G = 10\) to \(15\) and then increase it only if the shell strength and machine capacity allow. Excessive speed can cause segregation, shell cracking, or gate erosion. This balance is similar in principle to the compromises found in evaporative pattern casting, where pouring speed and foam degradation must be matched to avoid defects. In both processes, the metal front must remain stable long enough to fill the mold without entraining gas or oxide films.
Another important relationship is the shrinkage compensation. I treat the final dimension as a product of successive contractions. If the wax pattern shrinks by a factor \(s_w\) and the metal shrinks by a factor \(s_m\), then a first-order estimate of the die dimension is:
$$ L_{die} = \frac{L_{final}}{(1 – s_w)(1 – s_m)} $$
In practice, I use directional shrink factors rather than a single isotropic value. For a titanium impeller, I might apply \(s_w = 1.2\%\) for the wax and \(s_m = 1.0\%\) for the titanium alloy, but I adjust these values according to section thickness, gating restraint, and shell rigidity. If the part has a long, slender blade, the shrinkage in the blade direction may differ from the shrinkage in the hub. This anisotropic behavior is one reason I prefer simulation before cutting a die. It is also a reason I study evaporative pattern casting data, because foam patterns sometimes show different collapse and shrinkage behavior that can inform my understanding of pattern-scale effects.
Shell thickness is another parameter I control closely. The shell must withstand handling, dewaxing, firing, and pouring. A typical shell might have a face coat of 0.1 to 0.3 mm and a backup coat that builds the total thickness to 5 to 10 mm, depending on part size. I estimate the total thickness as:
$$ \delta_{total} = \sum_{i=1}^{N} \delta_i $$
where \(\delta_i\) is the thickness contributed by each slurry and stucco layer. I usually apply five to eight backup layers for small to medium castings and more layers for large castings. Each layer must dry sufficiently before the next is applied. If the drying is incomplete, the shell can delaminate or release gas during pouring. If the shell is too thick, it may resist contraction and cause hot tears. This trade-off is familiar to anyone who has worked with evaporative pattern casting, where the refractory coating must also balance strength, permeability, and collapsibility. In both processes, the mold or shell is not a passive container; it actively influences solidification and stress evolution.
I also monitor the solidification time and cooling rate. For a simple section, the solidification time can be estimated from the volume-to-area ratio:
$$ t_s = C \left( \frac{V}{A} \right)^2 $$
where \(t_s\) is the solidification time, \(V\) is the volume, \(A\) is the surface area, and \(C\) is a constant that depends on the alloy and mold. A larger \(V/A\) ratio means slower cooling and a greater tendency toward shrinkage porosity unless feeding is adequate. The Niyama criterion is useful for predicting shrinkage defects in castings:
$$ N = \frac{G}{\sqrt{\dot{T}}} $$
where \(G\) is the temperature gradient and \(\dot{T}\) is the cooling rate. Low Niyama values indicate a higher risk of shrinkage porosity. I use this criterion in simulation to compare gating designs. When I move from a top gating system to a bottom gating system, the temperature gradient and cooling rate change, and the Niyama distribution shifts. That shift is often enough to eliminate cold shuts and scattered porosity. The same logic applies to evaporative pattern casting, although the foam decomposition front adds an additional gas pressure term. In investment casting, the empty cavity gives me more direct control over the thermal field.
| Parameter | Starting value | Acceptable range | Primary effect |
|---|---|---|---|
| Wax injection temperature | 65 °C | 60–75 °C | Pattern dimensional stability and surface finish |
| Wax injection pressure | 2.5 MPa | 1.5–4.0 MPa | Fill completeness and shrinkage void formation |
| Wax shrink factor | 1.2% | 0.9–1.3% | Pattern-to-die compensation |
| Metal shrink factor | 1.0% | 0.8–1.5% | Casting dimension and hot tear tendency |
| Face coat thickness | 0.2 mm | 0.1–0.3 mm | Surface finish and chemical resistance |
| Backup shell thickness | 7 mm | 5–10 mm | Shell strength and collapsibility |
| Firing temperature | 1050 °C | 950–1150 °C | Binder burnout and shell strength |
| Melt superheat | 50 °C | 30–80 °C | Fluidity and gas pickup |
| Centrifugal speed | 225 rpm | 200–250 rpm | Feeding, filling, and density |
| Vacuum level | 4 MPa | 3–6 MPa | Gas removal and reactive alloy protection |
Titanium Alloy Impeller: Technical Requirements and Casting Difficulties
Titanium alloy impellers are among the most demanding components I have encountered in investment casting. They operate in corrosive fluids, often at high rotational speeds, and they must maintain dynamic balance. A typical impeller may have a maximum outer dimension of 300 mm, a height of 80 mm, and blade thickness as low as 6 mm. The alloy may be commercially pure titanium or a titanium alloy such as Ti-6Al-4V. The casting must be dimensionally accurate, dense, and free from cracks, cold shuts, and porosity. Because titanium has a high melting point and high chemical reactivity, the melt must be protected from oxygen, nitrogen, hydrogen, and carbon. The shell must also resist reaction with the liquid titanium. These requirements make the process window narrow.
In my trials, the first major difficulty was superheat. Compared with many steels and nickel alloys, titanium has a relatively high melting point and low superheat tolerance. If the melt is overheated, it picks up interstitial elements and loses ductility. If it is not overheated enough, it may not fill thin blade sections. The second difficulty was gating. A single in-gate location near the hub can lead to cold shuts at the blade tips and shrinkage porosity in the hub. The third difficulty was shell stability. Titanium reacts with many refractory materials, so I had to select a face coat that would not contaminate the alloy. The fourth difficulty was inspection. Internal defects in titanium are not always visible on the surface, so I relied on X-ray radiography, ultrasonic testing, and destructive sectioning during process development. These challenges are not unique to investment casting; they also appear in evaporative pattern casting when titanium or other reactive alloys are poured. However, the empty cavity of investment casting gives me a better chance to control the atmosphere and preheat the shell before the metal arrives.
For the initial design, I used a top gating system with a central sprue and five radial gates. The sprue diameter was 60 mm, and the gates were inclined at 25 degrees. The intention was to promote directional solidification from the blade tips toward the hub. In trial production, I used vacuum arc skull melting and centrifugal pouring. The melting current was 15 kA, the voltage was 40 V, and the centrifugal speed was 250 rpm. After shell removal and sandblasting, visual inspection revealed significant shrinkage porosity and cold shuts near the blade edges. The defects were concentrated in regions where the metal front had stalled or where the thermal gradient was unfavorable. I concluded that the top gating system did not provide enough feed metal to the thin blade sections and that the centrifugal force alone could not overcome the premature freezing of the titanium front. This result led me to redesign the gating system.
| Defect | Location | Probable cause | Corrective action |
|---|---|---|---|
| Cold shut | Blade tip and thin edges | Low superheat, high heat loss, poor fill | Increase superheat, modify gate location, preheat shell |
| Shrinkage porosity | Hub and gate vicinity | Insufficient feed path, unfavorable gradient | Bottom gating, larger sprue, increased centrifugal force |
| Gas porosity | Upper section | Entrapped gas, shell outgassing | Improve vacuum, firing schedule, venting |
| Shell cracking | Thick sections and corners | Thermal expansion mismatch, weak shell | Adjust binder, stucco grading, firing profile |
| Surface contamination | Face coat interface | Reaction with refractory | Use yttria face coat, zirconia binder |
| Hot tear | Blade root | Restraint during cooling | Reduce shell strength, modify gating, improve preheat |
Process Design and Improvement for the Titanium Impeller
After the first trial, I redesigned the process around a bottom gating system. The new design used a spherical-bottom refractory centrifugal cup. The in-gate was introduced at the bottom center of the casting, and the cross-sectional diameter of the runner and gate remained 60 mm. This change altered the filling sequence. Instead of dropping metal from the top, the metal rose from the bottom, which reduced turbulence and helped push the air out ahead of the front. I also kept the centrifugal parameters and melting parameters close to the original trial so that I could isolate the effect of gating. I then used finite element analysis with a commercial casting simulation package to compare the top-gated and bottom-gated designs. The simulation showed that the bottom-gated design produced a more uniform temperature gradient and a higher Niyama value in the blade and hub regions. The cold shut risk decreased significantly, and the shrinkage porosity was confined to a small area near the sprue that could be removed by machining.
The simulation also allowed me to study the effect of centrifugal radius. I ran several cases with different radial positions and found that the filling behavior improved when the impeller was placed at a larger radius, provided that the shell could withstand the increased pressure. The centrifugal pressure can be approximated by:
$$ P = \frac{1}{2} \rho \omega^2 r^2 $$
where \(P\) is the pressure, \(\rho\) is the density of the melt, \(\omega\) is the angular velocity, and \(r\) is the radial distance. As \(r\) increases, the pressure increases, which improves feeding. However, the same pressure increases the risk of shell cracking and gate erosion. Therefore, I selected a moderate radius and a speed of 200 to 250 rpm. The corresponding gravity coefficient was between 10 and 15, which is consistent with the formula given earlier. This optimization is similar to the balance I seek in evaporative pattern casting, where the foam pattern must decompose at a rate that matches the metal front without generating excessive gas pressure. In both cases, the goal is a stable, progressive fill.
I also modified the shell system for the titanium impeller. The face coat used yttria as the refractory filler and a zirconium acetate binder. The slurry ratio was controlled between 1:1.0 and 1:2.5 by weight. The backup layers used a silica sol binder and mullite stucco. I applied five face and backup layers with a drying time of at least 12 hours per layer, followed by six to eight additional layers with a drying time of at least 8 hours per layer. A wire mesh was inserted at the sixth layer to increase strength. The eighth layer was applied without stucco to produce a smooth outer surface. After coating, I did not dewax in the conventional autoclave. Instead, I placed the shell directly into a high-temperature furnace so that the pattern could burn out and collapse before the shell expanded enough to crack. The firing temperature was 1050 °C, and the holding time was 4 to 6 hours. This schedule was critical for avoiding shell rupture and for ensuring that the face coat remained chemically stable.
| Layer | Slurry or binder | Refractory | Drying time | Notes |
|---|---|---|---|---|
| Face coat | Zirconium acetate | Yttria | ≥ 12 h | Uniform coverage, no runoff |
| Layer 2 | Silica sol | Mullite | ≥ 12 h | Fine stucco |
| Layer 3 | Silica sol | Mullite | ≥ 12 h | Intermediate stucco |
| Layer 4 | Silica sol | Mullite | ≥ 12 h | Intermediate stucco |
| Layer 5 | Silica sol | Mullite | ≥ 12 h | Coarse stucco |
| Layer 6 | Silica sol | Mullite | ≥ 8 h | Wire mesh inserted |
| Layer 7 | Silica sol | Mullite | ≥ 8 h | Coarse stucco |
| Layer 8 | Silica sol | None | ≥ 8 h | Seal coat, no stucco |
Melting, Pouring, and Centrifugal Casting
For titanium alloys, I use vacuum arc skull melting with a water-cooled copper crucible. The skull is a thin layer of solidified titanium that protects the crucible from the melt and prevents contamination. The electrode is consumed, and the molten pool is formed inside the skull. The process is well suited to reactive alloys because the melt contacts mainly titanium or titanium alloy rather than copper. I have also evaluated vacuum induction melting with ceramic crucibles, but for titanium the risk of crucible reaction is high. For the impeller trial, I used a vacuum arc skull furnace with centrifugal pouring. The melting current was in the range of \(1.2 \times 10^4\) A to \(1.8 \times 10^4\) A, the electrode melting rate was about 15 kg/min, and the vacuum level was at least 4 MPa. The mold was preheated to reduce thermal shock and improve fill.
Pouring is the moment when all prior decisions are tested. I try to keep the pour rate steady and the superheat controlled. If the pour is too slow, the metal may freeze before the cavity is full. If the pour is too fast, the flow may become turbulent and entrain gas or oxide films. In centrifugal casting, the rotation adds a radial pressure that helps feed thin sections. The centrifugal force also causes the melt to press against the mold wall, which can improve heat transfer and density. However, the same force can cause the shell to crack if the shell is weak or if the rotation is started too abruptly. I usually ramp the speed gradually and wait for the mold to reach the set speed before pouring. This procedure is similar to the controlled acceleration used in evaporative pattern casting when the foam pattern must be decomposed without collapse defects. In both processes, the goal is to keep the metal front stable and progressive.
After pouring, I allow the casting to cool in the shell. The cooling rate must be controlled to avoid hot tears and to promote a fine microstructure. For titanium alloys, rapid cooling can produce a martensitic structure in some alloys, while slow cooling can produce coarse alpha plates. I usually specify a stress-relief heat treatment after shell removal. If the casting is intended for high-cycle fatigue, I may also apply hot isostatic pressing to close internal porosity. Hot isostatic pressing is especially useful for titanium castings because it can heal shrinkage defects that would otherwise reduce fatigue life. I have found that a combination of optimized gating, centrifugal casting, and hot isostatic pressing can produce impellers that meet stringent radiographic and mechanical requirements. This multi-step approach is one reason investment casting remains competitive with evaporative pattern casting for high-integrity titanium components.
| Parameter | Value | Unit | Purpose |
|---|---|---|---|
| Melting current | \(1.2 \times 10^4\) to \(1.8 \times 10^4\) | A | Melt rate and superheat control |
| Voltage | 35–45 | V | Arc stability |
| Electrode melting rate | 15 | kg/min | Production rate |
| Vacuum level | ≥ 4 | MPa | Prevent oxidation and gas pickup |
| Centrifugal speed | 200–250 | rpm | Feed and fill enhancement |
| Gravity coefficient | 10–15 | – | Density and feeding |
| Mold preheat | 800–1000 | °C | Reduce thermal shock and improve fluidity |
| Pouring time | 3–8 | s | Controlled fill |
Stereolithography and Rapid Pattern Development
Stereolithography, often abbreviated as SLA, has changed the way I approach pattern development for complex investment castings. In the traditional route, I would machine a wax injection die, inject wax patterns, assemble them, and then build the shell. For a complex closed impeller, that route may require two or more dies, precise wax welding, and extensive dimensional checks. The die cost and lead time are high, especially for low-volume production. With SLA, I can print the pattern directly from a computer-aided design model. The printed pattern is then coated with refractory slurry, fired, and poured. This eliminates the need for a wax injection die in the prototype stage and reduces the number of assembly steps. It also allows me to test multiple gate designs quickly.
However, SLA patterns are not a direct substitute for wax. Photopolymer resins have different thermal expansion and burnout behavior. If the pattern is solid, it may expand rapidly during firing and crack the shell. To mitigate this, I design the pattern with a hollow interior. The hollow core allows the pattern to collapse inward during heating instead of expanding outward against the shell. I also add vents at blade exits and thick sections so that decomposition gases can escape. After firing, I purge the shell with compressed air to remove residual ash. The face coat must be compatible with the resin and the alloy. For titanium, I use yttria face coats and zirconia acetate binders because they are stable at high temperature and resist reaction with the melt. The backup layers use silica sol and mullite. This approach is similar in spirit to evaporative pattern casting, where the pattern is also consumed during the casting process. The difference is that in investment casting, the pattern is removed before pouring, so the gas products do not interact with the liquid metal. That separation is a major advantage for reactive alloys.
I have also used SLA patterns to evaluate the filling behavior of thin blades. The printed pattern can reproduce features as small as 0.1 mm, which is sufficient for most impeller blade profiles. The surface finish of the printed pattern depends on the layer thickness and post-curing. With a layer thickness of 0.05 mm and proper orientation, I can achieve a surface roughness that is acceptable for many castings. If a smoother surface is required, I can polish the pattern or apply a thin coating. The dimensional accuracy of the printed pattern is also important. I compensate for resin shrinkage and firing shrinkage in the computer-aided design model. The total shrinkage can be estimated as:
$$ L_{final} = L_{CAD} (1 – s_{resin})(1 – s_{firing})(1 – s_{metal}) $$
where \(s_{resin}\) is the resin shrinkage, \(s_{firing}\) is the firing shrinkage, and \(s_{metal}\) is the metal shrinkage. I usually measure these factors experimentally for each resin and shell system. This data-driven approach reduces trial-and-error and improves first-pass yield. It also helps me compare the economics of investment casting with evaporative pattern casting. For large, simple parts, evaporative pattern casting may require less tooling and fewer steps. For small, complex, high-precision parts, investment casting with SLA patterns is often more capable.
| Route | Tooling cost | Lead time | Dimensional accuracy | Best application |
|---|---|---|---|---|
| Wax injection die | High | Long | Excellent | High-volume production |
| SLA printed pattern | Low to medium | Short | Very good | Prototypes and low-volume production |
| Machined wax | Medium | Medium | Good | Simple geometries |
| Evaporative pattern casting | Low to medium | Short to medium | Moderate to good | Large, simple, low-to-medium volume |
Equipment Types and Functions
Investment casting equipment can be grouped into pattern making, shell building, dewaxing, melting, pouring, cleaning, and inspection. Each group has a specific function, and the selection of equipment determines the achievable quality and productivity. In my experience, the most important equipment decisions are the melting furnace, the shell building system, the dewaxing autoclave or furnace, and the inspection tools. A mismatch between equipment and process requirements can lead to chronic defects that are difficult to solve by parameter changes alone.
Pattern making equipment includes wax injection presses, wax extruders, and additive manufacturing machines. Wax injection presses must maintain precise temperature and pressure. If the temperature is too low, the wax may not fill thin sections. If the temperature is too high, the wax may shrink excessively or flash. Additive manufacturing machines, such as SLA printers, are used for rapid pattern production. They are especially valuable for complex internal geometries that cannot be easily molded in wax. Shell building equipment includes slurry mixers, robotic arms, fluidized beds, and drying rooms. The slurry mixer must maintain uniform viscosity and prevent sedimentation. The robotic arm controls the dipping and stuccoing sequence. The drying room must control temperature, humidity, and airflow. If the humidity is too high, the shell may not dry; if the humidity is too low, the shell may crack. Dewaxing equipment includes autoclaves, flash fire furnaces, and high-temperature furnaces. Autoclaves use steam pressure to melt and remove wax. Flash fire furnaces burn out the pattern. High-temperature furnaces fire the shell and remove residual carbon.
Melting equipment for investment casting includes induction furnaces, vacuum arc furnaces, and vacuum induction furnaces. For titanium alloys, vacuum arc skull melting is often preferred because it minimizes crucible contamination. For superalloys, vacuum induction melting with ceramic crucibles is common. Pouring equipment includes tilt pourers, bottom pourers, and centrifugal casting machines. Centrifugal casting machines are used for thin-wall and rotationally symmetric parts. They can improve fill and density, but they also require careful shell support and speed control. Cleaning equipment includes knockout stations, cut-off machines, sandblasting cabinets, and ultrasonic cleaners. Inspection equipment includes coordinate measuring machines, X-ray systems, ultrasonic testing systems, and metallographic microscopes. The choice of inspection equipment depends on the criticality of the casting. For titanium impellers, I use X-ray radiography for internal defects and coordinate measuring machines for dimensional verification.
When I compare investment casting equipment with the equipment used in evaporative pattern casting, I see both overlap and difference. Both processes require sand handling, coating, pouring, and cleaning. However, evaporative pattern casting does not require wax injection, shell building, or dewaxing. Instead, it requires foam molding, pattern coating, and sand compaction. This makes evaporative pattern casting attractive for large parts and simple geometries. Investment casting requires more steps and more precise control, but it can produce finer details and thinner walls. The equipment list for investment casting is longer, and the capital cost is higher. Therefore, I recommend investment casting when the part geometry or alloy requires it. For parts that can tolerate the surface finish and tolerance of evaporative pattern casting, that process may be more economical.
| Category | Investment casting equipment | Evaporative pattern casting equipment | Primary function |
|---|---|---|---|
| Pattern making | Wax injection press, SLA printer | Foam molding machine, CNC foam cutter | Create sacrificial pattern |
| Mold or shell building | Slurry mixer, robot arm, fluidized bed, drying room | Coating booth, sand mixer, compaction table | Form refractory mold |
| Pattern removal | Autoclave, flash fire furnace, high-temperature furnace | None (pattern vaporized during pour) | Create cavity |
| Melting | Induction furnace, vacuum arc furnace, vacuum induction furnace | Induction furnace, cupola, electric arc furnace | Melt alloy |
| Pouring | Tilt pourer, bottom pourer, centrifugal machine | Ladle, pouring basin, tilt pourer | Fill mold |
| Cleaning | Knockout, cut-off, sandblast, ultrasonic cleaner | Shakeout, cut-off, sandblast | Remove mold and gates |
| Inspection | X-ray, CMM, ultrasonic, metallography | X-ray, CMM, ultrasonic, visual | Verify quality |
Auxiliary Equipment and Quality Control
Auxiliary equipment often receives less attention than the main furnace or robot, but it can determine whether a process is stable. In my experience, the dewaxing system is one of the most critical auxiliary systems. If the dewaxing temperature varies by more than \(\pm 1^\circ C\), the pattern may deform or the shell may crack. I use a programmable autoclave with uniform steam distribution and a controlled pressure ramp. For flash fire furnaces, I control the heating rate so that the pattern burns out gradually. If the heating rate is too fast, the shell may explode from internal pressure. If it is too slow, carbon residue may remain in the shell and react with the alloy. After dewaxing, I inspect the shell for cracks and check the cavity dimensions with a borescope or coordinate measuring system.
Other auxiliary equipment includes slurry viscometers, humidity sensors, thermocouples, vacuum gauges, and flow meters. These instruments provide the data I need to control the process. For example, slurry viscosity affects coating thickness and shell strength. I measure viscosity daily and adjust the binder content as needed. Humidity affects drying rate and shell cracking. I maintain the drying room at a controlled temperature and relative humidity. Vacuum level affects gas removal and reactive alloy protection. I calibrate vacuum gauges regularly and monitor the pumping curve. These small details may seem routine, but they are essential for repeatability. In evaporative pattern casting, similar attention must be paid to sand compaction, coating permeability, and foam density. In both processes, the auxiliary systems create the environment in which the main process can succeed.
Quality control in investment casting is a combination of in-process checks and final inspections. In-process checks include wax pattern dimensions, shell thickness, shell weight, dewaxing completeness, melt temperature, pour time, and vacuum level. Final inspections include visual examination, dimensional measurement, radiographic testing, penetrant testing, ultrasonic testing, and mechanical testing. For critical parts, I use statistical process control to track key parameters. When a parameter drifts, I investigate the cause and correct it before defects appear. This proactive approach is more effective than inspecting defects after they occur. It also helps me compare the capability of investment casting with evaporative pattern casting. If the required tolerance or surface finish is beyond the capability of evaporative pattern casting, investment casting is the appropriate choice, even if it requires more equipment and control.
| Stage | Checkpoint | Method | Target |
|---|---|---|---|
| Pattern | Dimensions and surface | CMM, visual | Within tolerance, no flash or sink |
| Shell | Thickness and integrity | Micrometer, visual | 5–10 mm, no cracks |
| Dewaxing | Residual wax and carbon | Weight loss, visual | Complete removal |
| Firing | Temperature and time | Thermocouple, controller | 1050 °C, 4–6 h |
| Melting | Superheat and composition | Pyrometer, spectrometer | Within alloy specification |
| Pouring | Speed and vacuum | Flow meter, vacuum gauge | Stable fill, no gas pickup |
| Cleaning | Surface and gates | Visual, sandblast | No residual shell, clean gates |
| Final | Internal and external defects | X-ray, ultrasonic, penetrant | Meet acceptance criteria |
Simulation and Data-Driven Optimization
Simulation has become an indispensable part of my investment casting workflow. I use finite element analysis to predict filling, solidification, stress, and distortion. The simulation helps me compare gating designs, optimize mold preheat, and select centrifugal speed. It also helps me understand why a defect occurs. For example, if the simulation shows a low Niyama value in a blade root, I can add a chill, change the gate location, or increase the local feed path. If the simulation shows a high stress concentration during cooling, I can adjust the shell thickness or the firing schedule. The goal is to reduce trial-and-error and shorten the development cycle.
I also use data-driven methods to optimize process parameters. I collect data from production runs, including wax temperature, injection pressure, shell thickness, drying time, firing temperature, melt superheat, pouring time, centrifugal speed, and inspection results. I then use regression analysis or machine learning to identify the parameters that most strongly influence defect rates. For example, I might find that cold shuts are most sensitive to melt superheat and gate location, while shrinkage porosity is most sensitive to centrifugal speed and sprue diameter. This information allows me to prioritize process improvements. It also helps me compare investment casting with evaporative pattern casting. If the data show that a part can be produced with a simpler process and acceptable quality, I may recommend evaporative pattern casting. If the data show that the required quality can only be achieved with investment casting, I focus on optimizing the investment casting parameters.
One of the most useful simulation outputs is the temperature field at the moment of filling. If the temperature field is non-uniform, the metal may freeze in thin sections before the cavity is full. I use the following criterion to estimate the risk of cold shut:
$$ R_{cs} = \frac{T_{melt} – T_{liquidus}}{T_{liquidus} – T_{mold}} $$
where \(R_{cs}\) is a dimensionless risk index. A higher value indicates a greater risk of cold shut because the available superheat is low relative to the heat loss to the mold. I aim to keep this index within a range that experience has shown to be safe for the alloy and section thickness. For titanium, the range is narrow, so I often preheat the shell and increase the centrifugal speed. The same type of thermal analysis can be applied to evaporative pattern casting, but the foam decomposition front adds a heat sink and gas source that must be modeled separately. In investment casting, the empty cavity simplifies the thermal boundary condition.
| Output | Interpretation | Action |
|---|---|---|
| Fill time | Time to complete cavity filling | Adjust pour rate or gate size |
| Temperature field | Hot and cold zones | Modify gating or preheat |
| Niyama criterion | Shrinkage porosity risk | Add feed path or chill |
| Cooling rate | Microstructure and stress | Adjust shell or alloy composition |
| Stress field | Hot tear and distortion risk | Modify shell thickness or cooling |
| Velocity field | Turbulence and gas entrapment | Change gate geometry or pour rate |
| Solid fraction | Feeding path closure | Increase sprue or centrifugal speed |
Comparison with Evaporative Pattern Casting
I often evaluate evaporative pattern casting as an alternative to investment casting when I am selecting a process for a new part. The two processes share the concept of a sacrificial pattern, but they differ in how the pattern is removed and how the mold is formed. In evaporative pattern casting, a foam pattern is coated with a refractory wash and embedded in unbonded sand. When the metal is poured, the foam vaporizes and the metal takes its place. The pattern remains in the mold until the metal front reaches it. This means that the mold filling and pattern removal are coupled. The decomposition products must escape through the coating and sand, and the metal must not be cooled too quickly by the endothermic decomposition. In investment casting, the pattern is removed before pouring. The cavity is empty and can be preheated. The shell is strong and can be made from materials that resist the alloy. This gives investment casting an advantage for thin walls, fine surface detail, and reactive alloys.
However, evaporative pattern casting has advantages in other areas. It requires less tooling for large parts, because the foam pattern can be cut or molded without a wax injection die. It can produce large castings with relatively low capital cost. It also avoids the shell building and dewaxing steps, which reduces lead time and energy consumption. For parts with simple geometry, moderate tolerance, and low-to-medium production volume, evaporative pattern casting can be very economical. I have seen evaporative pattern casting used successfully for pump bodies, manifolds, and large brackets. In those cases, the surface finish and dimensional tolerance were adequate, and the lower tooling cost was a major benefit.
When I compare the two processes for a titanium impeller, investment casting is usually the better choice. Titanium reacts with many materials, and the decomposition products of a foam pattern could contaminate the melt. The thin blades require a strong, preheated shell and a controlled atmosphere. The internal passages require a pattern that can be removed completely without leaving residue. Investment casting meets these requirements. Evaporative pattern casting would struggle with the thin walls and the reactive alloy, although it might be suitable for a larger, thicker, less critical titanium component. In my view, the decision should be based on a systematic comparison of geometry, alloy, tolerance, surface finish, production volume, and cost. I use a weighted scoring matrix for this purpose.
| Criterion | Weight | Investment casting score | Evaporative pattern casting score | Weighted investment | Weighted evaporative |
|---|---|---|---|---|---|
| Dimensional accuracy | 0.20 | 9 | 6 | 1.80 | 1.20 |
| Surface finish | 0.15 | 9 | 6 | 1.35 | 0.90 |
| Thin-wall capability | 0.15 | 9 | 5 | 1.35 | 0.75 |
| Reactive alloy compatibility | 0.15 | 9 | 5 | 1.35 | 0.75 |
| Tooling cost | 0.10 | 5 | 9 | 0.50 | 0.90 |
| Lead time | 0.10 | 6 | 8 | 0.60 | 0.80 |
| Large-part capability | 0.05 | 5 | 9 | 0.25 | 0.45 |
| Production volume flexibility | 0.10 | 7 | 8 | 0.70 | 0.80 |
| Total | 1.00 | – | – | 7.90 | 6.55 |
Economic and Environmental Considerations
In my experience, the economic analysis of investment casting must consider the entire life cycle, not just the piece price. The tooling cost for wax injection dies can be high, but the cost per part decreases with volume. For low volumes, SLA patterns or machined wax patterns can reduce tooling cost. The shell building process consumes refractory materials, water, and energy. The dewaxing and firing steps consume energy and generate emissions. The melting and pouring steps consume significant energy, especially for titanium alloys that require vacuum and high superheat. The cleaning and inspection steps add labor and equipment cost. To compete with evaporative pattern casting, investment casting must deliver a higher-quality part that reduces downstream machining, scrap, or failure risk. If the part can be made by evaporative pattern casting without sacrificing performance, the lower cost and shorter lead time of evaporative pattern casting are compelling.
I also consider environmental impact. Investment casting uses water-based slurries and refractory materials. The waste shell is typically landfilled, although some materials can be recycled. The wax pattern can be recovered in an autoclave and reused, which reduces waste. The binder and stucco systems are being developed to reduce volatile organic compounds and dust. Additive manufacturing reduces material waste compared with machining, but the photopolymer resin must be handled and disposed of properly. In evaporative pattern casting, the foam pattern is vaporized, which can produce emissions that must be captured and treated. The sand can be reused after thermal reclamation. Both processes have environmental challenges, and both are improving. I believe that the most sustainable choice is the one that minimizes total material and energy use while meeting the performance requirements. For a titanium impeller, investment casting may have a higher initial energy cost, but it can reduce scrap and extend service life. For a large, simple part, evaporative pattern casting may have a lower total environmental footprint.
| Factor | Investment casting | Evaporative pattern casting |
|---|---|---|
| Tooling cost | High for wax dies, lower for SLA | Low to medium |
| Piece cost at high volume | Low to medium | Low |
| Piece cost at low volume | Medium to high | Low to medium |
| Energy consumption | High | Medium to high |
| Material waste | Moderate, shell waste | Moderate, foam and sand waste |
| Recyclability | Wax reusable, shell limited | Sand reusable, foam consumed |
| Surface finish | Excellent | Good |
| Dimensional tolerance | Excellent | Moderate |
Future Developments and My Perspective
Looking ahead, I expect investment casting to become more digital, more automated, and more sustainable. Digital design and simulation will continue to reduce trial-and-error. Additive manufacturing will continue to expand the range of patterns that can be produced. Automated shell building will improve consistency and reduce labor. Advanced melting and pouring systems will improve alloy cleanliness and process control. In situ sensors will provide real-time data on temperature, pressure, and flow, enabling closed-loop control. Machine learning will help operators predict defects and optimize parameters. These developments will strengthen the position of investment casting in aerospace, medical, automotive, and energy applications.
At the same time, I expect evaporative pattern casting to improve as well. Foam materials, coatings, and sand systems are evolving. Simulation models for foam decomposition are becoming more accurate. Automated foam cutting and molding are reducing labor. For large and simple parts, evaporative pattern casting will remain a cost-effective alternative. For complex and critical parts, investment casting will remain the preferred route. In my own work, I plan to continue using both processes where they make sense. I will keep comparing them on the basis of technical requirements, cost, lead time, and environmental impact. I will also continue to refine the process parameters and equipment for titanium alloy impellers, because those components demand the best that investment casting can offer.
In conclusion, investment casting is a powerful manufacturing process that combines a sacrificial pattern with a refractory shell to produce complex, high-integrity metal components. The process requires careful control of pattern dimensions, shell properties, melting, pouring, and solidification. Titanium alloy impellers represent a challenging application, but with bottom gating, optimized centrifugal casting, yttria face coats, controlled firing, and simulation, I can achieve sound castings. SLA patterns provide a flexible route for prototypes and low-volume production. Equipment selection must match the part requirements and production volume. Auxiliary equipment and quality control are essential for repeatability. When I evaluate alternatives, I always consider evaporative pattern casting as a potential lower-cost option for simpler geometries. However, for thin walls, fine details, and reactive alloys, investment casting remains my method of choice. The future of the field will depend on continued innovation in materials, automation, simulation, and sustainability, and I intend to remain engaged with all of these developments.
My final recommendation to other engineers is to treat investment casting as a system. Start with the alloy and the geometry. Define the critical tolerances and defect acceptance criteria. Select the pattern route and shell system. Model the filling and solidification. Design the gating and feeding. Choose the melting and pouring equipment. Establish the inspection plan. Then iterate based on data. Do not assume that a single parameter change will solve every problem. Do not ignore the auxiliary systems. And do not overlook evaporative pattern casting as a possible alternative when the part requirements permit it. By combining rigorous analysis with practical trials, I have been able to improve yield, reduce defects, and deliver castings that meet demanding specifications. That is the approach I will continue to use in future projects.