
In my research and practical experience within the foundry and mining sectors, I have consistently focused on enhancing the performance of wear-resistant materials. Among these, high-chromium white cast iron stands out due to its exceptional combination of hardness and toughness, making it indispensable in applications subjected to severe abrasion. The key to unlocking its full potential lies not just in its chemical composition, but profoundly in the subsequent heat treatment processes. This article details my systematic investigation into optimizing the “quenching and tempering” process for high-chromium white cast iron, aiming to establish a quantitative and qualitative understanding of how specific thermal cycles dictate its final microstructure, and consequently, its mechanical properties.
The superior wear resistance of this alloy originates from its unique microstructure. Unlike ordinary white cast iron, which contains a continuous network of brittle M3C-type carbides, high-chromium white cast iron forms hard, discontinuous (Cr,Fe)7C3 carbides embedded within a metallic matrix. While these carbides provide the primary abrasion resistance, their effectiveness is wholly dependent on the supporting matrix. A soft matrix allows these hard phases to be plucked out easily, leading to catastrophic wear. Therefore, the matrix must be hardened to securely anchor the carbides. Through heat treatment, we can transform the as-cast matrix, typically austenitic or pearlitic, into much harder martensite. The challenge, and the core of my work, is to identify the precise thermal parameters that maximize hardness without excessively compromising toughness.
The experimental material for this study was prepared using a charge consisting of scrap carbon steel, high-carbon chromium steel, ferromanganese, ferromolybdenum, nickel, recycled graphite electrodes, and a rare-earth alloy for inoculation. The melt was processed in an induction furnace and cast into standard Y-block molds to produce samples for heat treatment and testing. The targeted chemical composition was within the range typical for high-chromium white cast iron: 2.8-3.2% C, 18-22% Cr, 0.5-1.5% Mo, 0.5-1.0% Ni, and 0.5-1.0% Mn.
The central experimental variable was the heat treatment cycle. I employed a “quench and temper” process. The quenching temperature ($T_q$) is critical as it determines the carbon and alloy content of the austenite prior to cooling. Four different quenching temperatures were selected: 950°C, 1000°C, 1050°C, and 1100°C. Samples were held at these temperatures for 120 minutes to achieve complete austenitization and partial dissolution of secondary carbides, followed by forced air cooling (air quenching). Subsequently, each batch of quenched samples was subjected to tempering at five different temperatures ($T_t$): 200°C, 400°C, 500°C, 600°C, and 700°C. The schematic of the heat treatment cycle is conceptually represented below, where $\tau$ represents time.
$$ \text{Temperature} \uparrow T_q \xrightarrow{\text{Hold: } \tau=120 \text{ min}} \text{Air Cool} \rightarrow \text{Room Temp} \rightarrow \text{Reheat to } T_t \xrightarrow{\text{Hold}} \text{Furnace Cool} $$
The as-cast and heat-treated samples were then subjected to comprehensive analysis. Rockwell hardness (HRC) was measured on ground surfaces. Impact toughness was assessed using unnotched Charpy specimens. Most importantly, microstructural evolution was studied using optical and scanning electron microscopy on properly etched samples (using Villela’s reagent). The volume fraction of carbides, the matrix constituents (martensite, retained austenite, secondary carbides), and their morphology were carefully characterized.
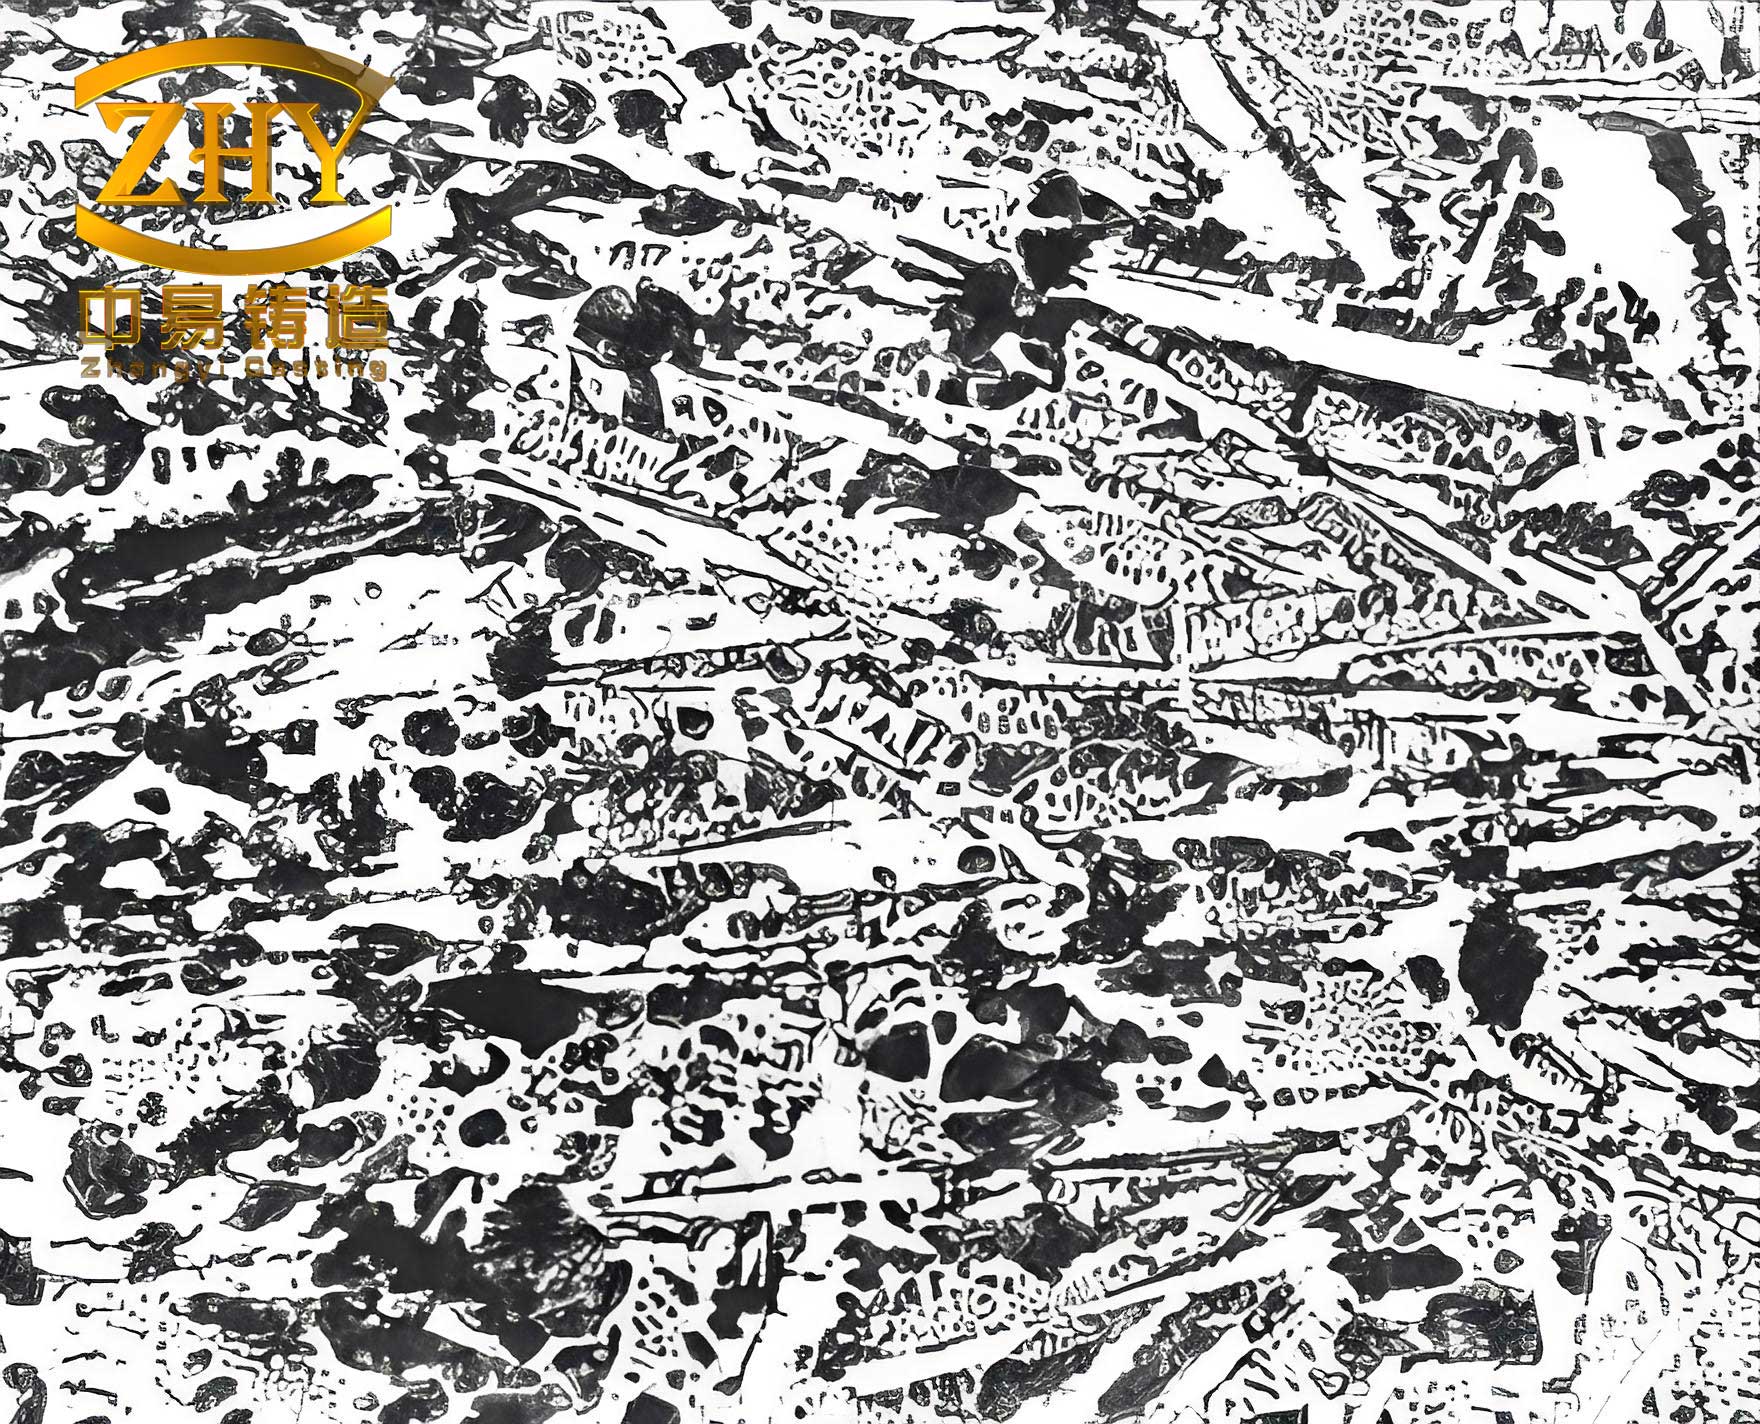
The initial microstructure of the as-cast high-chromium white cast iron consisted of primary (Cr,Fe)7C3 carbides in a matrix dominated by austenite, with some pearlitic transformation products. After optimal heat treatment, the microstructure transformed dramatically. The matrix became primarily martensitic, with fine secondary carbides precipitated within the laths. The primary carbides remained unchanged, but were now firmly embedded in a hard, supportive matrix.
Analysis of Quenching Temperature Effects
My experiments clearly demonstrated that the quenching temperature is a decisive parameter for final hardness. The relationship is not linear but exhibits a distinct peak. The data from my tests are summarized in Table 1.
| Quenching Temperature, $T_q$ (°C) | 950 | 1000 | 1050 | 1100 |
|---|---|---|---|---|
| As-Quenched Hardness (HRC) | 58.2 | 61.5 | 64.8 | 62.0 |
The hardness increase from 950°C to 1050°C can be explained by the thermodynamics of carbide dissolution. At lower $T_q$, the austenite is under-saturated. During heating and holding, secondary carbides precipitate extensively, depleting the austenite of carbon and chromium. Upon air cooling, this lean austenite transforms into a relatively soft, low-carbon martensite. As expressed in the following conceptual relation, the carbon content in austenite ($C_{\gamma}$) is a function of temperature and time:
$$ C_{\gamma}(T_q, \tau) = C_0 – \Delta C_{ppt}(T_q, \tau) $$
where $C_0$ is the nominal carbon content and $\Delta C_{ppt}$ is the carbon lost to secondary precipitation.
At an optimal $T_q$ (around 1050°C in my study), the dissolution and precipitation reach a favorable equilibrium. A sufficient amount of carbon and chromium remains in solution to stabilize the austenite against pearlitic transformation during cooling, yet not so much as to excessively suppress the Martensite Start ($M_s$) temperature. The result is a full transformation to a high-carbon, alloy-rich martensite with high hardness. The $M_s$ temperature can be approximated by an equation considering alloying effects:
$$ M_s(°C) \approx 539 – 423C_{\gamma} – 30.4Cr_{\gamma} – 17.7Ni_{\gamma} – 12.1Mo_{\gamma} – 7.5Mn_{\gamma} $$
At excessively high $T_q$ (1100°C), excessive dissolution occurs. The austenite becomes highly enriched and very stable, causing a significant depression of the $M_s$ temperature. Upon air cooling, a substantial amount of retained austenite ($\gamma_R$) remains at room temperature, softening the overall structure. The volume fraction of martensite ($V_m$) and retained austenite ($V_{\gamma R}$) follows:
$$ V_m + V_{\gamma R} = 1 $$
where $V_{\gamma R}$ increases markedly with increasing $T_q$ beyond the optimum.
Analysis of Tempering Temperature Effects
Tempering is essential to relieve quenching stresses and improve toughness. My investigation into tempering revealed complex interactions between the tempering temperature and the prior quenching condition. The hardness data after tempering are presented in Table 2.
| Tempering Temp, $T_t$ (°C) | As-Quenched Ref. | 200 | 400 | 500 | 600 | 700 |
|---|---|---|---|---|---|---|
| Quenched at 950°C | 58.2 | 57.8 | 57.5 | 56.0 | 48.5 | 35.2 |
| Quenched at 1000°C | 61.5 | 61.0 | 60.8 | 59.5 | 52.1 | 38.0 |
| Quenched at 1050°C | 64.8 | 64.5 | 64.3 | 64.0 | 63.5 | 45.7 |
| Quenched at 1100°C | 62.0 | 62.5 | 63.0 | 64.2 | 58.0 | 41.3 |
A key observation is the remarkable tempering resistance of this high-chromium white cast iron. For samples quenched at or below 1000°C, hardness remains nearly constant up to 400°C. This is due to a balancing act: the softening from martensite decomposition (transition from $\alpha’$-martensite to tempered martensite with $\epsilon$-carbide) is counteracted by the precipitation of fine, secondary alloy carbides from both the martensite and any retained austenite, which provides secondary hardening.
The behavior at 500-600°C is particularly interesting and depends on the initial quench. For low-$T_q$ samples, significant softening occurs by 600°C as tempering progresses to the formation of softer cementite and recrystallization. However, for samples quenched at 1050°C and 1100°C, which contain higher amounts of retained austenite ($\gamma_R$), a distinct secondary hardening peak appears around 500-550°C. During tempering in this range, the enriched $\gamma_R$ becomes unstable and decomheres, transforming into fresh martensite (during subsequent cooling) and precipitating more carbides. This phenomenon can be modeled as a time-temperature-transformation process for the retained austenite.
The impact toughness, a critical measure of the material’s resistance to fracture under shock loading, showed a clear dependency on both quenching and tempering temperatures, as shown in Table 3.
| Tempering Temp, $T_t$ (°C) | As-Quenched | 200 | 400 | 500 | 600 | 700 |
|---|---|---|---|---|---|---|
| Quenched at 950°C | 6.5 | 8.0 | 9.2 | 8.5 | 10.1 | 12.5 |
| Quenched at 1000°C | 7.0 | 8.8 | 10.5 | 9.8 | 11.5 | 14.0 |
| Quenched at 1050°C | 8.5 | 10.5 | 12.8 | 11.5 | 13.0 | 15.8 |
| Quenched at 1100°C | 7.8 | 9.5 | 11.0 | 10.0 | 12.2 | 14.5 |
Toughness generally improves with increasing tempering temperature due to stress relief and increased ductility of the matrix. A peak in toughness is often observed at intermediate tempering temperatures (400-600°C), after which over-tempering and grain coarsening may cause a slight decline. The samples quenched at 1050°C consistently showed the best combination of hardness and toughness after tempering, as the optimal matrix structure provided a good balance of strength and ductility.
Based on my extensive experimental data and microstructural analysis, I can draw the following conclusions for the heat treatment of high-chromium white cast iron. The final mechanical properties are extremely sensitive to the quenching temperature. There exists an optimal quenching window (around 1050°C for the specific composition and cooling rate in my study) that maximizes hardness by promoting a fully martensitic matrix with high carbon and alloy content, while minimizing detrimental retained austenite.
This grade of white cast iron possesses exceptional tempering resistance. Hardness remains stable for tempering temperatures up to at least 400°C. For components requiring the ultimate in wear resistance where some toughness can be sacrificed, a low-temperature temper (200-250°C) is suitable. However, for most industrial applications demanding a better toughness-hardness balance, a higher tempering temperature is beneficial. Specifically, tempering at 500-550°C can induce a valuable secondary hardening effect in samples that contained initial retained austenite, further enhancing wear resistance.
Therefore, the optimal heat treatment process I recommend for achieving an outstanding combination of high wear resistance and adequate toughness in high-chromium white cast iron is: Austenitizing at 1050°C for 120 minutes, followed by air quenching, and then tempering at 500°C for a minimum of 2 hours, followed by furnace cooling. This regimen ensures the formation of a hard, supportive martensitic matrix finely strengthened by secondary carbides, with minimal retained austenite and relieved internal stresses, making this white cast iron truly fit for the most demanding abrasive environments.