
In my experience with heavy marine components, the propeller is never just a bronze shape. It is a hydrodynamic device, a fatigue-loaded structure, and a cast product whose final pitch, camber, skew, and balance are all born inside the mould. For that reason, I treat every propeller drawing as a foundry problem first and a machining problem second. The central question is always how to translate a complex pitch surface into a practical sand mould casting process without losing dimensional control, internal soundness, or alloy quality. Over many campaigns, I have found that the most reliable route is to classify the propeller by its pitch distribution and blade-section type, then select a sand mould casting method that matches that class. This article summarizes the regularities I use in production, with particular attention to large-skew propellers and high-manganese aluminum bronze.
The casting process for a marine propeller depends on two dominant variables: the pitch distribution along the radius and the geometric family of the blade section. Once these are understood, the pattern equipment, scraper boards, pitch triangles, compensation plates, false blades, and gating system can be chosen with confidence. In my own practice, I reduce the problem to five broad classes: constant pitch, local linear radial variable pitch, full linear radial variable pitch, axial variable pitch, and axial-radial variable pitch. Each class has a characteristic sand mould casting response. The same logic applies when the blade is highly skewed, although skew introduces additional risks of distortion, unbalanced contraction, and oxide entrapment at the tip.
1. Foundry regularity from design data
When I review a propeller design, I do not begin with the casting drawing. I begin with the pitch diagram and the blade-section schedule. The pitch diagram tells me whether the blade surface can be scraped with a simple board, whether it needs a hinged scraper, or whether it must be built from a base pitch surface plus compensation sand plates. The blade-section schedule tells me whether the aerofoil-like camber can be formed directly, whether the tip must be filled, or whether a false blade is required to support the moulding sand. This is the foundation of every successful sand mould casting sequence.
The governing geometric relation for pitch is simple but powerful. At any radius \(r\), the pitch angle is determined by the local pitch \(P(r)\) and the circumference at that radius:
$$
\theta(r) = \tan^{-1}\left(\frac{P(r)}{2\pi r}\right)
$$
For a reference or base pitch \(P_0\), the base pitch angle is:
$$
\theta_0(r) = \tan^{-1}\left(\frac{P_0}{2\pi r}\right)
$$
Therefore the pitch correction angle that a scraper, triangle, or compensation plate must produce is:
$$
\phi(r) = \theta(r) – \theta_0(r)
$$
I treat \(\phi(r)\) as a signed quantity. A positive value means that the local pitch surface must be raised or rotated in one direction relative to the base surface. A negative value means the opposite. This signed convention is essential in sand mould casting because it allows the same compensation-plate formulas to be used for normal blades and for large-skew blades, provided the plate length is extended beyond the usual chord limits.
When the design is produced by a series chart, I compare the series parameters with the actual drawing. Many published series look similar in tabular form, but their blade sections and pitch distributions behave very differently in the mould. For example, a constant-pitch propeller is easy to identify, but once a linear radial pitch variation is added to each section, the resulting blade surface may become a nonlinear radial variable-pitch surface. In that case, the moulding method must follow the nonlinear surface, not the nominal series name. I have seen avoidable scrap created by assuming that a linear series always remains linear after individual section corrections.
2. Common propeller series and their casting characteristics
The table below summarizes the practical characteristics I track when selecting a sand mould casting method. The series names are given generically, and the important columns are blade number, thickness fraction, disc ratio, pitch ratio range, hub ratio, section type, pitch distribution, and skew or rake.
| Series family | Blade number | Thickness fraction | Disc ratio | Pitch ratio range | Hub ratio | Blade section | Pitch distribution | Skew or rake |
|---|---|---|---|---|---|---|---|---|
| General cargo series | 3 to 5 | 0.045 to 0.060 | 0.45 to 0.70 | 0.6 to 1.2 | 0.16 to 0.20 | Root aerofoil, tip arched | Constant pitch | Small skew |
| High-speed patrol series | 3 to 4 | 0.030 to 0.045 | 0.60 to 0.90 | 0.8 to 1.4 | 0.14 to 0.18 | Root aerofoil, tip arched | Near constant pitch | Small rake |
| Tug and trawler series | 4 | 0.050 to 0.070 | 0.55 to 0.80 | 0.5 to 1.0 | 0.18 to 0.22 | Root aerofoil, tip arched | Constant pitch or local radial variation | Moderate skew |
| Container and ferry series | 5 to 6 | 0.040 to 0.055 | 0.70 to 1.05 | 0.7 to 1.3 | 0.16 to 0.20 | Root aerofoil, tip arched | Linear radial variable pitch | Moderate to large skew |
| Axial variable-pitch series | 4 to 7 | 0.035 to 0.060 | 0.50 to 1.00 | 0.5 to 1.5 | 0.15 to 0.22 | Root aerofoil, tip arched | Axial pitch change | Small to moderate skew |
| Combined axial-radial series | 4 to 7 | 0.035 to 0.060 | 0.55 to 1.10 | 0.5 to 1.6 | 0.15 to 0.22 | Root aerofoil, tip arched | Axial plus nonlinear radial variation | Large skew possible |
| Large-skew series | 5 to 7 | 0.030 to 0.055 | 0.65 to 1.15 | 0.7 to 1.4 | 0.15 to 0.20 | Root aerofoil, tip arched or modified | Nonlinear axial-radial variation | Large skew, often with forward rake |
In my classification, the most difficult group is not necessarily the largest propeller. It is the combined axial-radial variable-pitch group with large skew. That group demands the most careful sand mould casting design because the blade surface changes in two directions at once, and the tip may lie well outside the central plane of the blade. A small error in the compensation plate can create a visible pitch error after machining, and a small error in gating can create oxide inclusions precisely where the blade is thinnest.
3. Five classes of propeller pitch and their sand mould casting schemes
I use the following five-class system when writing process instructions. It is short enough for the shop floor and detailed enough for the pattern shop. Each class has a preferred sand mould casting scheme, and each scheme includes a fallback when the blade section is too complex to form directly.
| Class | Pitch character | Typical series or type | Sand mould casting scheme | Notes |
|---|---|---|---|---|
| I | Constant pitch | General cargo, patrol, some workboat propellers | Pitch-surface scraper plus external pitch triangular plate plus false blade | The standard constant-pitch surface is usually an arched section. If an aerofoil section must be produced, a blade-section template can add the camber. For small diameters, I often fill the raised part of the aerofoil to simplify moulding. |
| II | Local linear radial variable pitch | Certain tug and fishing series | Articulated scraper plus internal and external pitch triangular plates plus false blade | The hinge point is placed at the pitch-change station. If the aerofoil section is required, a blade-section template is used. |
| III | Full linear radial variable pitch | Some ferry and cargo series | Articulated scraper plus internal and external pitch triangular plates plus false blade; pitch-gauge coordinate moulding as an alternative | The hinge point is usually outside the external triangular plate. The transition between pitch zones must be blended to avoid a ridge. |
| IV | Axial variable pitch | Axial-flow series and related families | Base pitch-surface scraper plus external pitch triangular plate plus compensation sand plate plus false blade | The compensation plate creates the axial pitch change. Pitch-gauge coordinate moulding may also be used. |
| V | Axial-radial variable pitch, including nonlinear radial variation and large skew | Large-skew propellers, combined axial-radial series | Base pitch-surface scraper plus external pitch triangular plate plus compensation sand plate plus false blade; pitch-gauge coordinate moulding as a parallel check | This is the most demanding class. For large-skew blades, the tip section may lie outside the normal central plane, so the compensation plate must be extended and the auxiliary gating must be arranged carefully. |
For class V, I do not rely on a single method. I use two independent checks whenever the geometry is critical: the external pitch triangular plate plus compensation sand plate method, and pitch-gauge coordinate moulding. The first controls the overall surface; the second verifies the position of the section at selected radii. When both agree, the sand mould casting has a much higher chance of meeting the pitch tolerance without repeated trial-and-error machining.
4. Large-skew propellers: definition and foundry significance
A large-skew propeller is not simply a propeller with a swept tip. Skew is the angular displacement of the tip relative to the root, measured between the radiation line through the root section and the hub centreline and the radiation line through the tip section and the hub centreline. In my classification, the full-skew value for a given blade number is:
$$
S_{100} = \frac{360^\circ}{Z}
$$
where \(Z\) is the number of blades. For a five-blade propeller, \(S_{100} = 72^\circ\). I treat a propeller as a large-skew propeller when its skew reaches or exceeds that full-skew value, or when the design intent clearly places it in the large-skew family. The hydrodynamic benefit is well known: large skew can delay cavitation and reduce unsteady forces. The foundry penalty is equally well known: the blade becomes a long, curved, thin-walled cantilever inside the mould, and the tip may project far from the central plane.
In sand mould casting, large skew creates three practical problems. First, the blade is more likely to distort during cooling because the mass distribution is asymmetric and the constraint from the mould is uneven. Second, the tip is thin and may be difficult to fill without cold shuts or oxide inclusions. Third, the compensation plate geometry is less intuitive because the section is offset from the usual midline. I address these problems by combining a conservative compensation strategy with auxiliary gating and a moulding layout that supports the tip without locking it.
5. Case study of a large-skew propeller
The following case illustrates the approach I use in production. The propeller had a moderate diameter, five blades, a forward rake angle, and a variable pitch ratio whose average value was moderate. The disc ratio and hub ratio were typical of a high-performance marine propeller. The material was a high-manganese aluminum bronze. The theoretical weight, rough casting weight, and poured weight were all tracked separately because the gating and feeding system added a significant amount of metal.
The pitch distribution was a nonlinear axial-radial variable pitch. Because the diameter was not large, I decided to fill the raised portions of the aerofoil section in the mould so that the shape could be formed more easily. This is a common compromise in sand mould casting: if the section is small and the camber is not critical over the whole surface, filling the raised part simplifies the pattern and reduces the risk of sand collapse. The camber can then be restored by machining where it matters. Although a large-skew blade is prone to distortion, the moderate diameter allowed me to use the average pitch-change rate as the basis for a reverse deformation allowance. Because the average pitch ratio was not extreme and the blade did not overhang the hub excessively, I applied conventional machining allowances and then verified them with pitch-gauge checks.
To protect the pitch surface, I used two methods in parallel. First, I used the external pitch triangular plate plus compensation sand plate method. Second, I used pitch-gauge coordinate moulding as an independent verification. This dual approach is, in my experience, the most reliable way to keep a large-skew sand mould casting within tolerance. The triangular plate controls the global pitch relationship, while the compensation plate controls the local deviation. The pitch gauge then confirms the result at specific radii and angular positions.
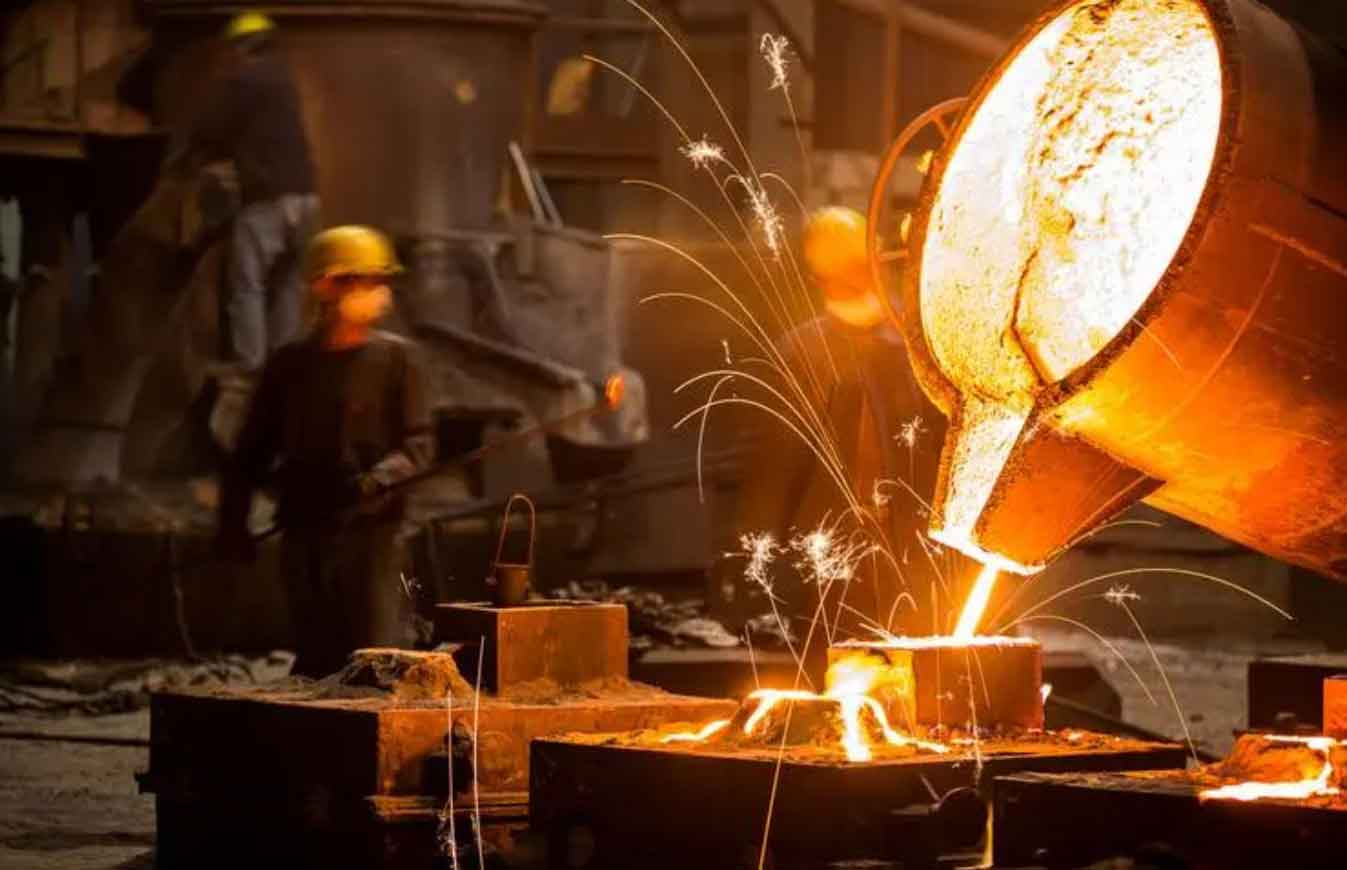
Because high-manganese aluminum bronze is highly prone to oxidation and gas absorption during melting, and because the metal inevitably picks up secondary oxide inclusions while flowing through the gating system, I paid special attention to slag trapping and slag removal. The gating system was designed so that it first acts as a closed, restrictive passage and then opens progressively toward the mould cavity. This helps maintain a full runner and reduces the chance of entrained oxide skins reaching the blade. I also increased mould drying and purged the cavity with argon before pouring to minimize secondary oxidation.
6. Two practical problems in large-skew sand mould casting
The first problem is secondary oxide inclusion at the forward-skewed tip. In a large-skew blade, the tip is often the last region to fill and the most difficult to feed. If the metal arrives cold or with entrained oxide, the defect appears exactly where the section is thin and where fatigue performance is most sensitive. To counter this, I add auxiliary ingates from the hub region along the parting plane. These auxiliary ingates are led through the cover half to the lowest point of the trailing edge at the tip of each blade. In a five-blade propeller, I generally use one auxiliary ingate per blade, although the exact number depends on the blade spacing and the gating layout. The purpose is to let clean metal fill the tip region first and drive oxide inclusions back toward the risers or overflow.
The second problem is contraction distortion. The auxiliary ingate is helpful for filling, but it can also act as a restraint. If it is too rigid, the contraction of the blade can pull against it and change the pitch or camber. Therefore, the auxiliary ingate must be designed with a weak, collapsible section. In my practice, I reduce the cross-section near the blade connection and use a slightly tapered neck so that it can yield during solidification and cooling. The gate must feed the tip, but it must not become a structural tie rod. This balance is one of the most important details in large-skew sand mould casting.
The same principle applies to the false blade and the external plates. They should support the sand and define the surface, but they should not lock the casting. I prefer a layout in which the blade can contract slightly along its length while the pitch surface remains supported. If the moulding assembly is too rigid, the casting may look acceptable in the green state but reveal a pitch error after cooling or after stress relief.
7. Compensation plate calculation for normal and large-skew blades
The compensation sand plate is the heart of variable-pitch sand mould casting. It converts the difference between the base pitch surface and the required local pitch surface into a physical wedge or plate that is placed on the mould surface. For a normal blade section, I use the following working definitions. Let \(L_g\) be the length from the guide end of the compensation plate to the installation reference, and let \(L_t\) be the length from the installation reference to the trailing end. Let \(\phi\) be the signed pitch correction angle at the section under consideration.
The guide-end height of the compensation plate is:
$$
h_g = L_g \tan \phi
$$
The trailing-end height is:
$$
h_t = L_t \tan \phi
$$
The total plate length is:
$$
L_c = L_g + L_t
$$
The distance from the guide end to the installation reference point is:
$$
x_0 = L_g + \Delta x
$$
where \(\Delta x\) is the local offset required by the pattern layout. When \(\phi > 0\), the plate rises in one direction; when \(\phi < 0\), the plate rises in the opposite direction. The sign convention must be carried through all calculations. In my shop instructions, I specify the sign explicitly rather than relying on a verbal description of “up” or “down.” This avoids the classic error in which a compensation plate is installed backward on one blade and forward on another.
For a large-skew blade, the same formulas apply, but the definition of \(L_g\) and \(L_t\) must be extended beyond the normal chord. The plate installation is still referenced to the midline of the base pitch surface, but the guide-end and trailing-end lengths are measured to the actual extremes of the skewed section. The section may lie outside the central plane, so the plate is longer than it would be for a normal blade. If this extension is ignored, the compensation plate will not cover the full section, and the tip will be under-compensated. I have found that the formulas can be unified for normal and large-skew blades once this extension is understood.
| Symbol | Meaning | Typical unit |
|---|---|---|
| \(r\) | Local radius of the blade section | mm or m |
| \(P(r)\) | Required local pitch at radius \(r\) | mm or m |
| \(P_0\) | Base or reference pitch | mm or m |
| \(\theta(r)\) | Local pitch angle | degrees or radians |
| \(\theta_0(r)\) | Base pitch angle | degrees or radians |
| \(\phi(r)\) | Signed pitch correction angle | degrees or radians |
| \(L_g\) | Length from guide end to installation reference | mm |
| \(L_t\) | Length from installation reference to trailing end | mm |
| \(h_g\) | Compensation plate height at guide end | mm |
| \(h_t\) | Compensation plate height at trailing end | mm |
| \(L_c\) | Total compensation plate length | mm |
| \(Z\) | Number of blades | dimensionless |
| \(S\) | Skew angle at the tip | degrees |
| \(S_{100}\) | Full-skew reference angle | degrees |
In practice, I calculate the compensation plate at several radii rather than only at the root and tip. A typical schedule might include the root, 0.3R, 0.5R, 0.7R, 0.9R, and the tip. At each station, I tabulate \(P(r)\), \(\theta(r)\), \(\theta_0(r)\), \(\phi(r)\), \(L_g\), \(L_t\), \(h_g\), and \(h_t\). The pattern shop then uses these values to make the plate. The foundry uses the same table to set the plate and verify its position. This shared table is one of the simplest ways to prevent communication errors in variable-pitch sand mould casting.
| Station | Local pitch \(P(r)\) | Base pitch \(P_0\) | Local pitch angle \(\theta(r)\) | Base pitch angle \(\theta_0(r)\) | Correction \(\phi(r)\) | Plate height \(h_g\) | Plate height \(h_t\) |
|---|---|---|---|---|---|---|---|
| Root | \(P_R\) | \(P_0\) | \(\theta_R\) | \(\theta_0\) | \(\phi_R\) | \(L_g \tan\phi_R\) | \(L_t \tan\phi_R\) |
| 0.3R | \(P_{0.3}\) | \(P_0\) | \(\theta_{0.3}\) | \(\theta_0\) | \(\phi_{0.3}\) | \(L_g \tan\phi_{0.3}\) | \(L_t \tan\phi_{0.3}\) |
| 0.5R | \(P_{0.5}\) | \(P_0\) | \(\theta_{0.5}\) | \(\theta_0\) | \(\phi_{0.5}\) | \(L_g \tan\phi_{0.5}\) | \(L_t \tan\phi_{0.5}\) |
| 0.7R | \(P_{0.7}\) | \(P_0\) | \(\theta_{0.7}\) | \(\theta_0\) | \(\phi_{0.7}\) | \(L_g \tan\phi_{0.7}\) | \(L_t \tan\phi_{0.7}\) |
| 0.9R | \(P_{0.9}\) | \(P_0\) | \(\theta_{0.9}\) | \(\theta_0\) | \(\phi_{0.9}\) | \(L_g \tan\phi_{0.9}\) | \(L_t \tan\phi_{0.9}\) |
| Tip | \(P_T\) | \(P_0\) | \(\theta_T\) | \(\theta_0\) | \(\phi_T\) | \(L_g \tan\phi_T\) | \(L_t \tan\phi_T\) |
When \(\phi > 0\), the guide end and trailing end rise in the same algebraic sense as the required pitch change. When \(\phi < 0\), the plate is reversed. For large-skew sections, the same table is used, but \(L_g\) and \(L_t\) are measured to the extended section boundaries. This is the point at which many foundries either succeed or fail: they apply the correct formula to the wrong section length. In my experience, the extension is not a minor correction for large-skew propellers; it is essential for pitch accuracy.
8. High-manganese aluminum bronze: composition and property control
The alloy used for high-performance marine propellers is a high-manganese aluminum bronze. It sits at the top of the propeller-material hierarchy. As ship tonnage, speed, and propulsion power increase, its use becomes more widespread. The mechanical properties of this alloy are closely related to its chemical composition, especially the aluminum content, while manganese, iron, and nickel also influence performance. In my control charts, I collapse part of this influence into an aluminum equivalent so that the melt can be adjusted before pouring.
A practical aluminum equivalent can be written as:
$$
\mathrm{Al}_{eq} = \mathrm{Al} + a\mathrm{Mn} + b\mathrm{Fe} + c\mathrm{Ni}
$$
where \(a\), \(b\), and \(c\) are coefficients chosen from historical heats and mechanical test results. In my own practice, I use an engineering approximation in which manganese, iron, and nickel each contribute to the effective aluminum level. The exact coefficients are less important than maintaining a consistent internal standard and correlating that standard with tensile tests. The mechanical properties correlate approximately linearly with the aluminum equivalent over the narrow production window.
| Element | Typical specification range, wt% | Recommended narrow control range, wt% | Foundry role |
|---|---|---|---|
| Al | 11.0 to 13.0 | 11.4 to 12.4 | Strengthening, hard-phase formation, castability |
| Mn | 7.0 to 9.0 | 7.4 to 8.6 | Solid-solution strengthening, deoxidation assistance |
| Fe | 2.5 to 3.5 | 2.8 to 3.4 | Grain refinement, control of brittle phases |
| Ni | 1.5 to 2.5 | 1.8 to 2.4 | Toughness, corrosion resistance, phase stability |
| Cu | Balance | Balance | Matrix |
The specification range for this alloy is narrow, but the production window is even narrower. In my experience, a composition within the broad specification can still fail to meet mechanical requirements if the aluminum equivalent is not controlled. The melt must be held within a tight range, and the furnace operator must know the target aluminum equivalent before tapping. I recommend treating the following as a working control band:
$$
\mathrm{Al}_{eq,\min} \le \mathrm{Al}_{eq} \le \mathrm{Al}_{eq,\max}
$$
The exact values depend on the specification and the heat history, but the principle is always the same: control the equivalent, not just the individual elements. When the aluminum equivalent is too low, strength and hardness may be insufficient. When it is too high, ductility and toughness may drop, and the risk of brittle phase formation increases. This is especially important in large-skew sand mould casting, where thin tip sections must remain tough despite rapid cooling.
| Property | Typical requirement | Foundry implication |
|---|---|---|
| Tensile strength | At least 630 MPa | Requires accurate Al equivalent and sound feeding |
| Yield strength | At least 280 MPa | Sensitive to phase balance and cooling rate |
| Elongation | At least 16% | Falls rapidly if Al equivalent is too high |
| Hardness | Approximately 160 to 220 HB | Used as a quick check of melt consistency |
| Corrosion resistance | Marine service | Controlled by Ni and Fe balance, not by Al alone |
I also pay attention to melting practice. High-manganese aluminum bronze is easily oxidized and absorbs gas. The melt should be protected, the charge should be clean, and the pouring temperature should be controlled within a narrow range. Superheat that is too high increases gas absorption and oxidation; superheat that is too low produces cold shuts in thin blade tips. In large-skew sand mould casting, the tip is the critical region, so I prefer a pouring temperature that fills the tip without overheating the bulk of the melt.
9. Gating and filtration for clean sand mould casting
Because secondary oxide inclusions are a major risk in this alloy, the gating system must do more than deliver metal. It must trap slag, stabilize flow, and avoid re-entrainment. I use a gating system that is initially closed and then progressively opens toward the cavity. A practical area ratio is:
$$
F_s : F_r : F_g = 1 : 2 : 4
$$
where \(F_s\) is the sprue cross-section, \(F_r\) is the runner cross-section, and \(F_g\) is the total gate cross-section. This progressive opening reduces jetting and helps the runner remain full. In some moulds, I use a slightly different ratio depending on the number of blades and the pouring time, but the principle remains: avoid a sudden expansion that creates turbulence, and avoid a restrictive gate that produces a high-velocity jet into the blade.
I also use a refractory filter in the runner system. The filter pore size is chosen to capture oxide skins without excessively slowing the fill. In my practice, a filter with approximately 1.5 to 2.5 mm apertures works well for medium and large propeller castings. The filter must be placed where it can be replaced easily and where it does not create a cold spot. If the filter is too small, it can block and cause a misrun. If it is too large, it may not trap the fine oxide particles that cause polishing defects on the blade surface.
| Gating feature | Recommended practice | Reason |
|---|---|---|
| Sprue | Tapered, with a well at the base | Prevents air entrainment and reduces turbulence |
| Runner | Full, slightly enlarged after the sprue | Maintains metal pressure and helps slag float |
| Gate | Progressive opening, total area about four times the sprue | Reduces jet velocity into the blade |
| Filter | Refractory mesh, 1.5 to 2.5 mm aperture | Traps secondary oxides and slag |
| Auxiliary ingate | One per blade at the tip trailing edge, collapsible neck | Fills thin tip and drives oxides to risers |
| Riser | Located at the hub and heavy sections | Feeds shrinkage and provides an oxide exit |
10. Mould drying, gas purging, and sand control
Moisture and gas are enemies of sound sand mould casting, especially in high-manganese aluminum bronze. I dry the mould thoroughly before closing. The drying schedule depends on the mould size and the binder system, but the goal is to remove free moisture and reduce the risk of steam reaction at the metal front. After closing, I purge the cavity with argon before pouring. This reduces the oxygen content in the cavity and lowers the probability of secondary oxide formation on the advancing metal surface. Argon purging is not a substitute for good gating, but it is a useful additional control.
The sand itself must be strong enough to resist erosion but permeable enough to vent gas. For large propellers, I use a facing sand with good refractory properties and a backing sand that provides strength. The sand must be compacted evenly around the blade edges. Soft spots can cause sand wash, and hard spots can cause gas defects or hot tears because they restrain contraction. In large-skew sand mould casting, the sand around the tip must be especially uniform. A hard patch on one side of the tip can pull the blade out of position during cooling.
I also pay attention to the coating. A good refractory coating can improve surface finish and reduce metal penetration. However, the coating must not be so thick that it fills the fine details of the pitch surface. In my experience, a thin, uniform coating is better than a thick patchy coating. The coating should be dried completely before the mould is closed.
11. Pattern equipment and moulding assembly
The pattern equipment for variable-pitch sand mould casting is a system, not a single pattern. It includes the base pitch surface, the external pitch triangular plate, the compensation sand plate, the false blade, and the pitch gauge. The base pitch surface establishes the reference geometry. The external triangular plate controls the pitch relationship between sections. The compensation plate adds the local correction. The false blade supports the sand at the blade edge and helps form the tip. The pitch gauge provides an independent check.
I prefer to make the external triangular plate and the compensation plate as separate items because they serve different functions. If they are combined into one complex piece, it becomes difficult to adjust one without disturbing the other. Separate plates also allow the pattern shop to verify each element independently. In large-skew work, this modular approach is particularly valuable because the compensation plate may need to be extended or reworked after the first casting.
The false blade should be designed so that it can be removed without damaging the mould. It should support the sand at the blade edge, but it should not create a sharp notch that acts as a stress riser in the casting. In some cases, I use a slightly tapered false blade so that the mould sand is supported but the casting edge is not excessively thick. The goal is to produce a clean blade edge with enough material for machining.
| Tooling element | Function | Key control |
|---|---|---|
| Base pitch surface | Defines the reference pitch | Accurate radius and angular setting |
| External pitch triangular plate | Controls global pitch | Correct length and angle at each station |
| Compensation sand plate | Adds local pitch correction | Signed thickness and extended length for skew |
| False blade | Supports sand at blade edge | Clean release and no sharp notch |
| Pitch gauge | Verifies section position | Calibrated against the design pitch diagram |
| Auxiliary ingate pattern | Forms tip feed channel | Collapsible neck and correct location |
12. Shrinkage, distortion, and reverse deformation
Shrinkage is never uniform in a propeller. The hub is thick and cools slowly, while the blade edges are thin and cool quickly. In a large-skew propeller, the blade also has an asymmetric mass distribution, so the contraction is not symmetric about the blade midline. I compensate for this by adding reverse deformation to the pattern. The amount depends on the alloy, the blade size, the skew, and the mould stiffness. For moderate diameters, I use the average pitch-change rate as a guide and then adjust after the first casting. For large diameters, I prefer to make a preliminary casting or a partial trial to measure the distortion before committing to the final pattern.
The reverse deformation is not a single number. It varies from root to tip and from leading edge to trailing edge. In my process sheets, I specify the reverse deformation at the same stations used for the compensation plate calculation. This allows the pattern shop to blend the correction smoothly. If the reverse deformation is applied only at the tip, it can create a kink in the blade surface. A smooth blend is essential for hydrodynamic performance and for avoiding stress concentrations.
I also consider the effect of the moulding sand on restraint. A very hard mould can prevent contraction and cause hot tears. A very soft mould can allow the blade to sag. The ideal mould is firm enough to hold the shape but compliant enough to yield slightly during cooling. In large-skew sand mould casting, I often use a slightly softer sand around the tip and a stronger sand around the hub. This differential compaction helps the blade contract without losing its pitch.
13. Inspection and dimensional verification
Inspection of a propeller casting begins before the metal is poured. The mould assembly should be checked against the pitch diagram, the compensation plate table, and the reverse deformation schedule. After pouring and cooling, the casting is checked for surface defects, sand inclusions, gas porosity, and shrinkage. Dimensional verification focuses on pitch, camber, skew, blade thickness, and balance. I use a pitch gauge or a coordinate measuring method to verify the blade surface at selected radii. The same stations used in the compensation plate calculation are used for inspection, which makes it easy to compare the design intent with the actual casting.
If a pitch error is found, I first determine whether it is a global error or a local error. A global error usually comes from the external triangular plate, the base pitch surface, or the mould assembly. A local error usually comes from the compensation plate, the reverse deformation, or a distorted section. By separating global and local errors, I can correct the tooling without remaking everything. This diagnostic approach has saved considerable time in large-skew sand mould casting.
| Inspection item | Method | Typical cause of deviation | Corrective action |
|---|---|---|---|
| Pitch at root | Pitch gauge or template | Base pitch surface error | Recheck base plate and assembly |
| Pitch at mid-radius | Pitch gauge or coordinate check | Compensation plate height error | Adjust plate thickness or length |
| Pitch at tip | Pitch gauge or coordinate check | Extended length not used for skew | Extend compensation plate and recheck |
| Camber | Blade-section template | Filled aerofoil or sand collapse | Restore section in pattern or machining |
| Skew | Angular measurement | Mould shift or uneven contraction | Correct false blade and sand compaction |
| Blade thickness | Ultrasonic or mechanical gauge | Pattern wear or coating buildup | Repair pattern, control coating |
| Balance | Static or dynamic balancing | Uneven blade weight | Adjust machining allowance and gating |
14. Defect prevention in sand mould casting of propellers
The defects I see most often in propeller sand mould casting are oxide inclusions, gas porosity, shrinkage porosity, sand wash, cold shuts at the tip, and pitch distortion. Each has a different cause, but they often interact. For example, a cold shut at the tip may be caused by low pouring temperature, but it can also be caused by a restrictive auxiliary ingate or a filter that blocks too early. A pitch distortion may be caused by a rigid auxiliary ingate, but it can also be caused by uneven sand compaction or a poorly supported false blade.
| Defect | Likely cause | Prevention |
|---|---|---|
| Oxide inclusion | Turbulent flow, dirty charge, poor slag trapping | Progressive gating, filter, argon purge, clean melt |
| Gas porosity | Wet mould, high gas content, low permeability | Dry mould, control superheat, improve venting |
| Shrinkage porosity | Insufficient feeding at hub or thick section | Proper riser design, chills where needed |
| Sand wash | Weak sand, high gate velocity, poor compaction | Stronger facing sand, reduce gate velocity, uniform ramming |
| Cold shut at tip | Low temperature, slow fill, narrow auxiliary gate | Optimize pouring temperature, enlarge or reposition auxiliary ingate |
| Pitch distortion | Rigid gating, uneven contraction, poor reverse deformation | Collapsible ingate, balanced sand, correct reverse deformation |
| Blade edge crack | Sharp false blade, hot tear, excessive restraint | Round false blade edges, softer sand at tip, control cooling |
In my experience, the most effective defect-prevention strategy is to treat the mould as a thermal and mechanical system, not just a shape. The gating must deliver clean metal, the sand must allow controlled contraction, and the tooling must define the pitch surface without locking the blade. When these three requirements are met, the sand mould casting process becomes repeatable, even for large-skew propellers.
15. Summary of my working rules
The following rules summarize the approach I use for marine propeller sand mould casting:
First, classify the propeller by pitch distribution and blade-section type before selecting the moulding method. Constant pitch, linear radial variable pitch, axial variable pitch, and combined axial-radial variable pitch each require a different sand mould casting scheme.
Second, for variable-pitch blades, always compute the signed pitch correction angle \(\phi(r)\) and use it consistently in the compensation plate formulas. The guide-end and trailing-end heights are \(h_g = L_g \tan\phi\) and \(h_t = L_t \tan\phi\). For large-skew blades, extend \(L_g\) and \(L_t\) to the actual section extremes.
Third, define large skew by the full-skew reference \(S_{100} = 360^\circ / Z\). For a five-blade propeller, \(S_{100} = 72^\circ\). Large-skew blades require extended compensation plates, auxiliary tip gating, and a compliant moulding layout.
Fourth, control the high-manganese aluminum bronze within a narrow production window. Use an aluminum equivalent to account for the combined effects of aluminum, manganese, iron, and nickel. Keep the melt clean and the pouring temperature within a narrow range.
Fifth, use a gating system that is initially closed and then progressively opens. A ratio close to \(F_s : F_r : F_g = 1 : 2 : 4\), with a refractory filter, helps trap oxides and reduces turbulence. Purge the cavity with argon before pouring and dry the mould thoroughly.
Sixth, design the auxiliary ingate to feed the tip without restraining contraction. A collapsible neck is essential. This is especially important in large-skew sand mould casting, where the tip is thin and the blade is long.
Seventh, verify the mould with two independent methods whenever possible. The external pitch triangular plate plus compensation sand plate method controls the surface, while pitch-gauge coordinate moulding verifies the result. When both agree, the casting has a much higher probability of meeting pitch and balance requirements.
Eighth, use reverse deformation at the same stations used for the compensation plate calculation. Apply it smoothly from root to tip. A sudden change creates a kink; a missing change creates a pitch error.
Ninth, inspect the casting at the same stations used in the design and tooling calculations. If an error appears, determine whether it is global or local before altering the tooling. This saves time and prevents over-correction.
Finally, remember that a marine propeller is a safety-critical component. The sand mould casting process must be controlled from pattern design through pouring, cooling, and inspection. When the pitch surface, gating system, alloy composition, and moulding assembly are all treated as one integrated system, high-quality propellers can be produced reliably, including large-skew designs in high-manganese aluminum bronze.