
In my extensive experience within the manufacturing and foundry industry, I have witnessed a transformative shift in the production of complex components, particularly in the realm of machine tool casting. The integration of advanced digital technologies, such as 3D printing and numerical simulation, has revolutionized how we design, prototype, and produce castings for machine tools. This article delves deep into the application of these technologies, emphasizing the keyword ‘machine tool casting’ throughout, to provide a comprehensive overview of modern practices. The focus is on enhancing precision, reducing lead times, and improving cost-efficiency, which are critical for maintaining competitiveness in today’s industrial landscape. Machine tool casting, as a specialized field, demands high accuracy and reliability, and the adoption of innovative methods like selective laser sintering (SLS) and ProCAST simulation has become indispensable.
The foundational concept behind modern machine tool casting lies in the synergy between digital design and physical fabrication. Traditionally, casting processes involved extensive trial-and-error, leading to prolonged development cycles and increased costs. However, with the advent of computational tools, we can now simulate the entire casting process virtually, predicting defects and optimizing parameters before any metal is poured. This not only ensures the integrity of machine tool casting components but also aligns with sustainable manufacturing by minimizing material waste. In this narrative, I will explore how ProCAST numerical simulation and SLS-based 3D printing are leveraged to streamline the production of high-quality castings, using a case study of a large aluminum alloy chuck for precision machine tools as a pivotal example. The emphasis on machine tool casting here underscores its significance in achieving dimensional stability and mechanical performance required for demanding applications.
To begin, let us consider the role of numerical simulation in machine tool casting. ProCAST, a finite element analysis software, is extensively used to model the filling, solidification, and cooling stages of casting processes. By inputting material properties, boundary conditions, and geometric data, we can predict potential issues such as shrinkage porosity, hot tears, and misruns. For instance, in the production of a commercial vehicle front beam sample, which is a critical machine tool casting component, ProCAST was employed to analyze the reliability of the casting process design. The simulation accounts for thermal gradients and fluid flow, which are governed by fundamental equations of heat transfer and fluid dynamics. The heat conduction equation is central to this analysis:
$$ \frac{\partial T}{\partial t} = \alpha \nabla^2 T $$
where \( T \) is temperature, \( t \) is time, and \( \alpha \) is thermal diffusivity. This equation helps in modeling the cooling behavior of the casting, ensuring uniform solidification to avoid defects. In machine tool casting, such precision is paramount because any internal flaw can compromise the component’s strength and durability. The use of ProCAST allows for iterative design adjustments, virtually testing different gating and risering systems until an optimal configuration is achieved. This proactive approach significantly enhances the first-pass yield rate, reducing the need for physical prototypes and rework. Below is a table summarizing key parameters analyzed in ProCAST for a typical machine tool casting simulation:
| Parameter | Description | Typical Value Range | Impact on Machine Tool Casting |
|---|---|---|---|
| Pouring Temperature | Initial temperature of molten metal | 680°C – 750°C for aluminum | Affects fluidity and defect formation |
| Cooling Rate | Rate of temperature drop during solidification | 0.5°C/s – 10°C/s | Influences microstructure and mechanical properties |
| Mold Material | Thermal properties of the mold | Sand, ceramic, or metal | Determines heat extraction efficiency |
| Gating Design | Layout of channels for metal flow | Varied based on geometry | Controls filling pattern and turbulence |
| Riser Size | Volume of feeders for shrinkage compensation | 10% – 20% of casting volume | Prevents porosity in thick sections |
Transitioning from simulation to physical modeling, selective laser sintering (SLS) technology plays a crucial role in rapid prototyping for machine tool casting. SLS uses a laser to fuse powdered materials, such as polystyrene, into intricate patterns that serve as expendable models in investment casting. This method eliminates the need for traditional mold development, which is often time-consuming and expensive. For the front beam sample, polystyrene patterns were printed via SLS, enabling quick iteration and validation of the design before committing to metal casting. The SLS process involves layer-by-layer fabrication, governed by parameters like laser power, scan speed, and layer thickness. The energy density \( E_d \) applied during sintering can be expressed as:
$$ E_d = \frac{P}{v \cdot h \cdot t} $$
where \( P \) is laser power, \( v \) is scan speed, \( h \) is hatch spacing, and \( t \) is layer thickness. Optimizing this equation ensures proper fusion without distortion, which is vital for achieving high-dimensional accuracy in machine tool casting patterns. The integration of SLS with investment casting, often referred to as rapid investment casting, allows for the production of complex geometries that are difficult to machine. This synergy is particularly beneficial for machine tool casting components that require fine details and tight tolerances. The following table compares traditional pattern making with SLS-based approach for machine tool casting applications:
| Aspect | Traditional Pattern Making | SLS-Based Pattern Making | Advantages for Machine Tool Casting |
|---|---|---|---|
| Lead Time | Weeks to months | Days to weeks | Faster time-to-market |
| Cost | High due to tooling | Lower as no molds needed | Reduced upfront investment |
| Design Flexibility | Limited by mold complexity | High, allows freeform geometries | Enables innovative machine tool casting designs |
| Accuracy | Depends on craftsmanship | Consistent, within ±0.1 mm | Improves precision of final castings |
| Material Waste | Significant from machining | Minimal, unused powder recycled | Aligns with sustainable manufacturing |
The combination of ProCAST simulation and SLS printing culminates in a streamlined workflow for producing high-integrity machine tool casting samples. In the case of the commercial vehicle front beam, after virtual validation, the SLS patterns were used in a ceramic shell investment casting process. The molten metal, typically aluminum or steel, was poured into the mold, resulting in a casting that met all dimensional and performance specifications. This integrated approach not only boosts the first-pass success rate but also slashes production cycles by up to 50%, as evidenced in various industry applications. Machine tool casting, when augmented with these digital tools, becomes more agile and responsive to design changes, which is essential in sectors like automotive and aerospace where innovation is rapid.
Now, let us delve into a specific case study that highlights the advancements in machine tool casting: the manufacturing of a large aluminum alloy chuck for precision machine tools. This component, weighing 800 kg with dimensions of φ2200 mm × 200 mm, exemplifies the challenges and solutions in modern foundry practices. The material chosen was ZL401 aluminum alloy, known for its excellent castability and self-quenching properties. In machine tool casting, selecting the right alloy is critical; ZL401 undergoes natural aging after casting, forming an α-phase supersaturated solid solution that enhances strength and hardness without requiring heat treatment. The chemical composition and mechanical properties of ZL401 are pivotal for machine tool casting applications, as summarized below:
| Element/Property | Composition (wt.%) or Value | Role in Machine Tool Casting |
|---|---|---|
| Silicon (Si) | 10.0 – 12.0 | Improves fluidity and reduces shrinkage |
| Magnesium (Mg) | 0.2 – 0.5 | Enhances strength via precipitation hardening |
| Zinc (Zn) | 5.0 – 7.0 | Contributes to natural aging response |
| Tensile Strength | 250 – 300 MPa | Ensures durability under operational loads |
| Hardness | 80 – 100 HB | Provides wear resistance for machine tool casting |
| Density | 2.7 g/cm³ | Lightweight compared to iron, reducing inertia |
The casting process for this aluminum chuck was meticulously designed to achieve sound metallurgy and dimensional accuracy. A three-part mold was used, with the working face oriented downward and covered with 60 mm thick aluminum chill plates to promote directional solidification. Gravity pouring with a bottom gating system ensured smooth filling, minimizing turbulence and oxide inclusion. The gating design was optimized using ProCAST simulations to verify thermal gradients and solidification patterns. The risers, arranged in inner and outer circles, compensated for shrinkage, a common concern in large-scale machine tool casting. The total casting weight, including feeders, was 1258 kg, which after machining yielded an 800 kg finished part with a machining allowance of 10 mm on all critical surfaces. This process underscores the importance of integrating simulation and traditional foundry expertise for successful machine tool casting.
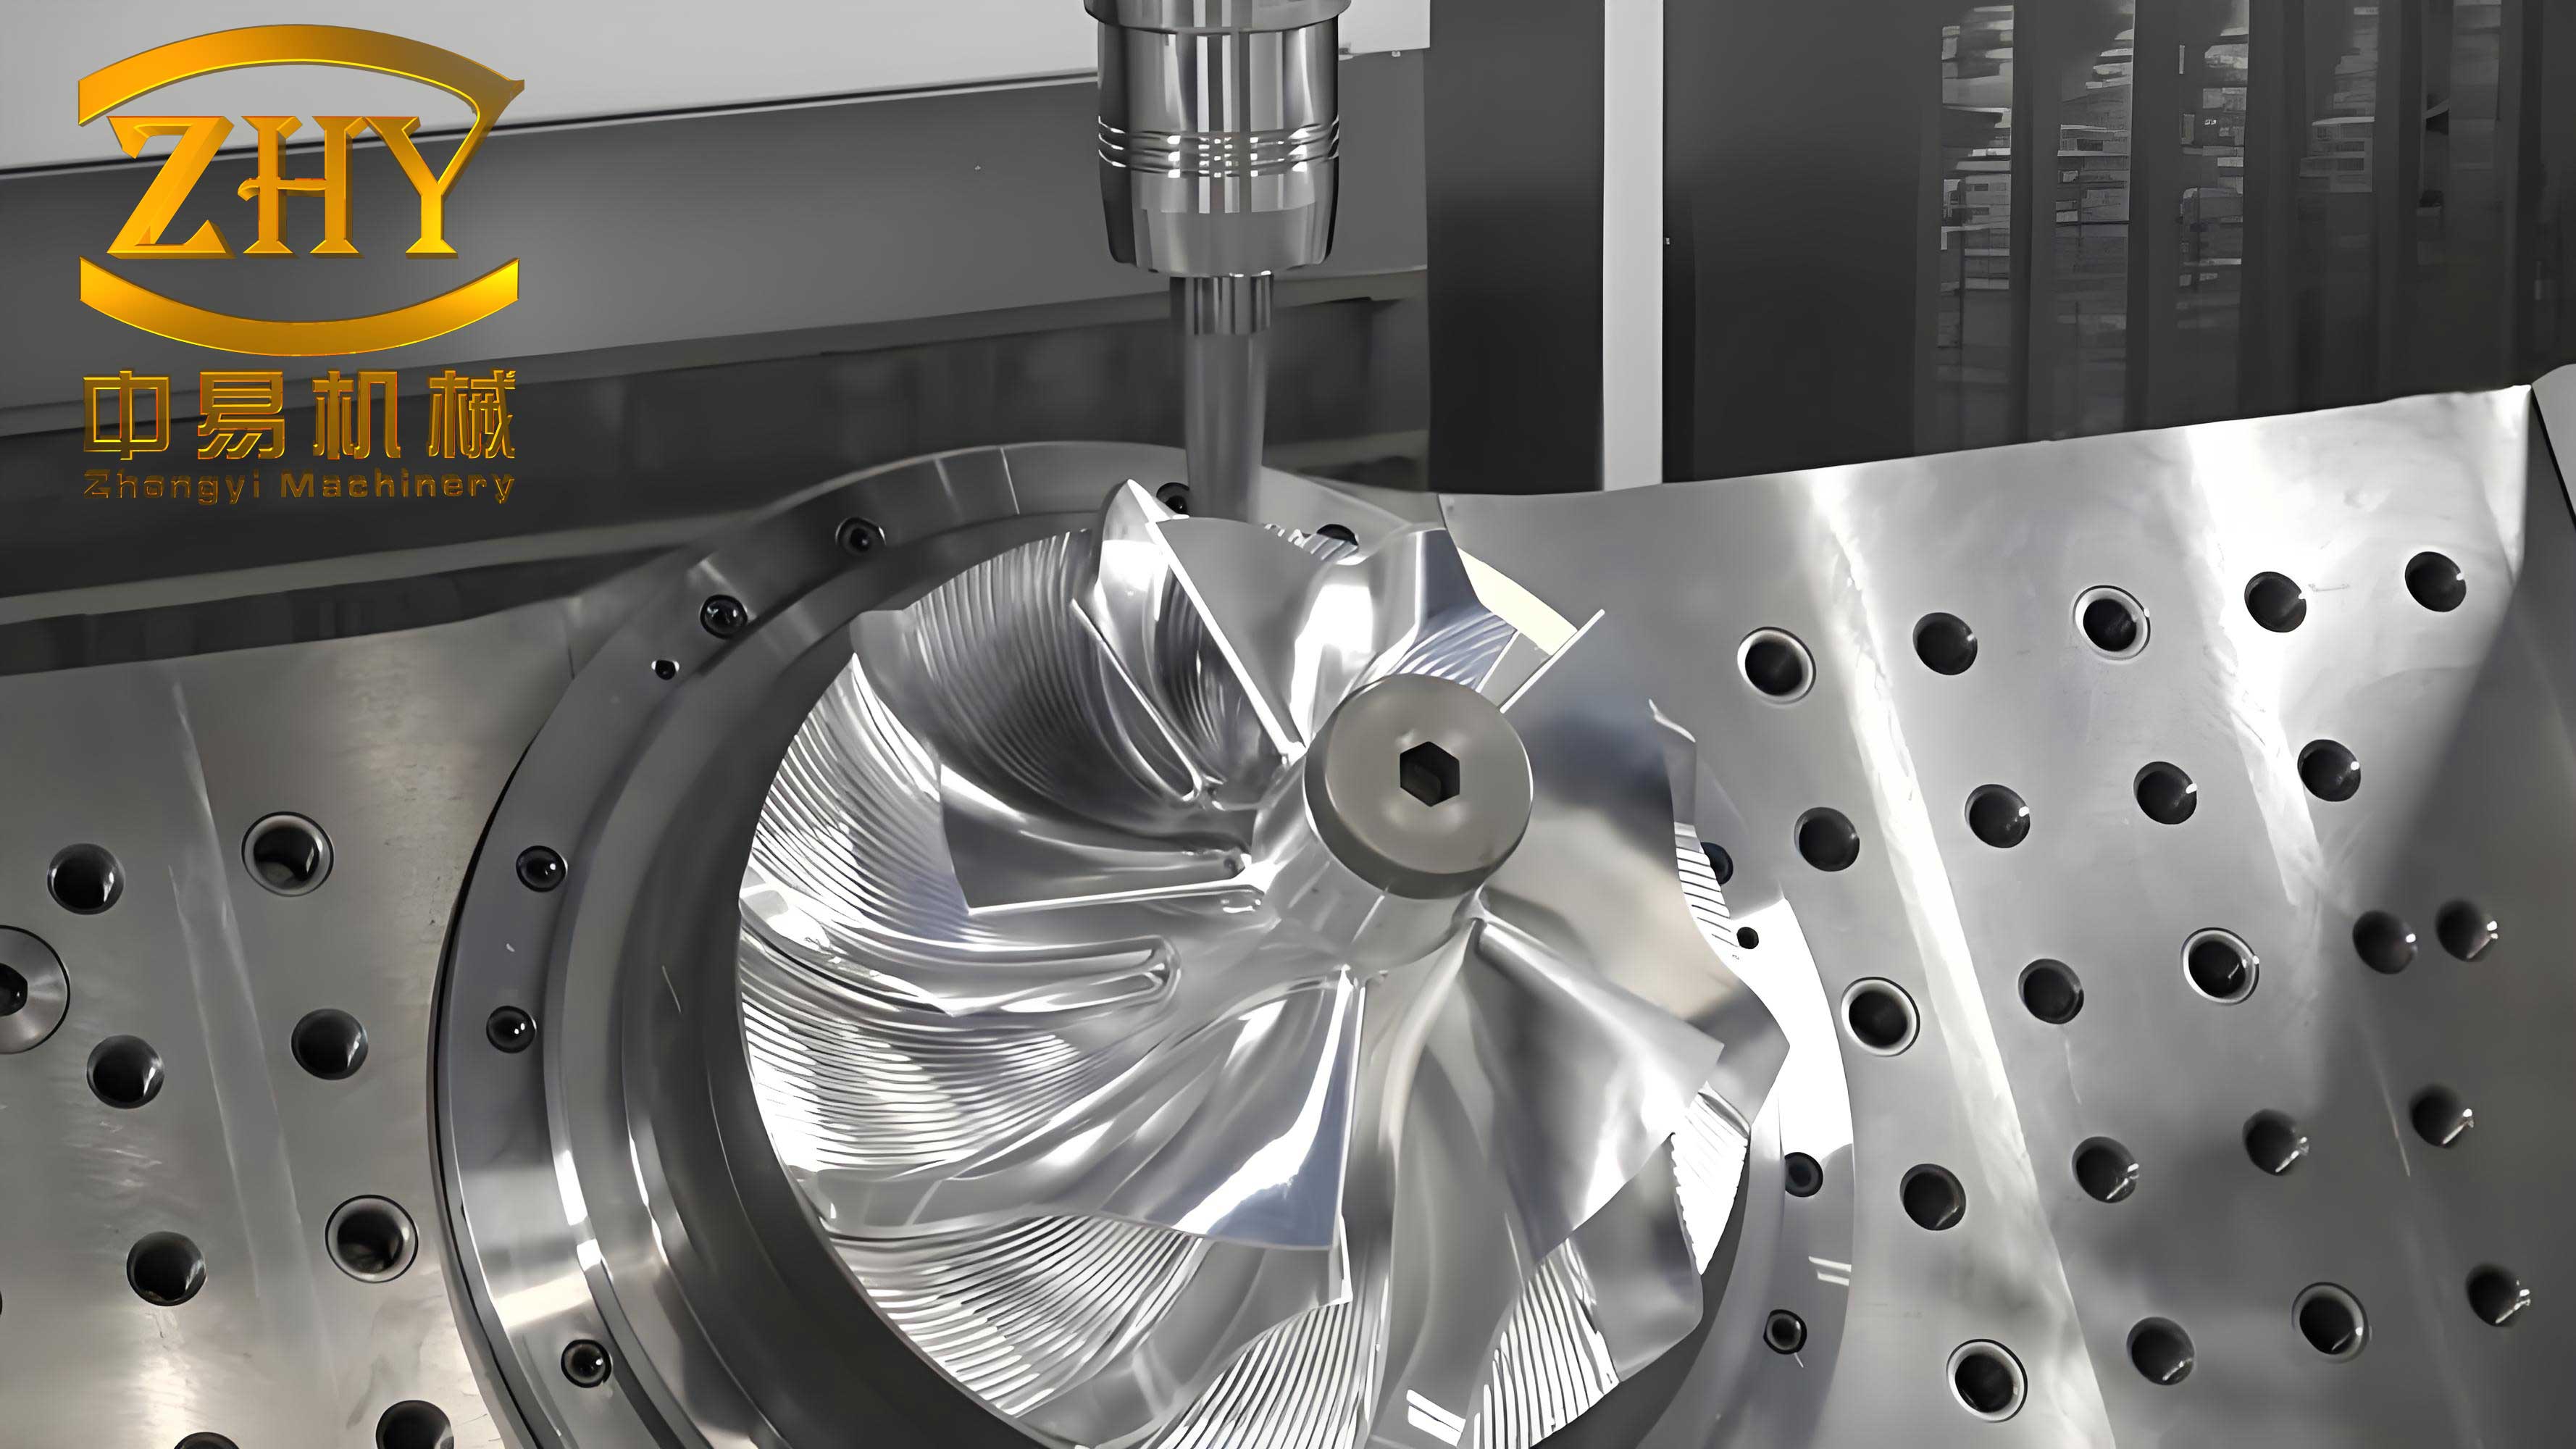
To visualize the complexity and scale of such a machine tool casting component, consider the following image that illustrates a typical large chuck during production. The intricate details and size highlight the challenges addressed by advanced manufacturing techniques.
The benefits of using aluminum alloy for machine tool casting are profound, especially in applications requiring reduced rotational inertia. For instance, this aluminum chuck weighs only 800 kg, whereas an equivalent cast iron version would weigh approximately 2311 kg. The reduction in mass directly translates to lower motor power requirements and enhanced precision in machine tools, as the inertia force \( F_i \) is given by:
$$ F_i = m \cdot a $$
where \( m \) is mass and \( a \) is angular acceleration. By minimizing \( m \), we reduce the energy needed for acceleration and deceleration, improving dynamic response. This is a key consideration in high-speed machining, where machine tool casting components must balance strength with lightweight design. Moreover, ZL401’s natural aging capability eliminates the need for costly heat treatment cycles, further streamlining production. The wear resistance of this alloy also ensures longevity in demanding environments, making it ideal for machine tool casting applications that involve continuous operation.
Expanding on the technical aspects, the solidification behavior of ZL401 in machine tool casting can be modeled using the Chvorinov’s rule, which estimates solidification time \( t_s \):
$$ t_s = C \left( \frac{V}{A} \right)^n $$
where \( V \) is volume, \( A \) is surface area, \( C \) is a mold constant, and \( n \) is an exponent typically around 2. For the chuck casting, with a high volume-to-area ratio, proper riser design was crucial to avoid shrinkage defects. ProCAST simulations helped in determining the optimal riser size and placement, ensuring that the last solidifying regions were fed adequately. This analytical approach is fundamental to achieving defect-free machine tool casting, as internal porosity can severely compromise mechanical integrity. Additionally, the fluid flow during mold filling is governed by the Navier-Stokes equations, which in their simplified form for incompressible flow, are:
$$ \rho \left( \frac{\partial \mathbf{u}}{\partial t} + \mathbf{u} \cdot \nabla \mathbf{u} \right) = -\nabla p + \mu \nabla^2 \mathbf{u} + \mathbf{f} $$
where \( \rho \) is density, \( \mathbf{u} \) is velocity vector, \( p \) is pressure, \( \mu \) is dynamic viscosity, and \( \mathbf{f} \) represents body forces. Simulating these equations in ProCAST allows us to visualize metal flow patterns, identify potential cold shuts or air entrapment, and adjust gating designs accordingly. For machine tool casting, where components often have thin walls and complex features, such detailed analysis is indispensable.
The integration of 3D printing and simulation technologies also opens new avenues for customization in machine tool casting. With SLS, we can produce patterns for one-off or low-volume productions without the economic burden of hard tooling. This is particularly advantageous for prototyping new machine tool designs or manufacturing replacement parts for legacy equipment. Furthermore, the digital thread connecting CAD models, simulation results, and printed patterns ensures consistency and traceability, which are critical in quality assurance for machine tool casting. The table below outlines the workflow for producing a machine tool casting component using these integrated technologies:
| Step | Activity | Technologies Used | Outcome for Machine Tool Casting |
|---|---|---|---|
| 1. Design | CAD modeling of component | CAD software (e.g., SolidWorks) | Digital blueprint for machine tool casting |
| 2. Simulation | Virtual analysis of casting process | ProCAST or similar FEA tools | Optimized process parameters, defect prediction |
| 3. Pattern Making | Fabrication of expendable patterns | SLS 3D printing with polystyrene | High-accuracy patterns without molds |
| 4. Mold Preparation | Investment shell building | Ceramic slurry and stucco application | Refractory mold for metal pouring |
| 5. Casting | Melting and pouring of metal | Induction furnace, gravity pouring | Raw casting with minimal defects |
| 6. Post-Processing | Heat treatment, machining, inspection | CNC machining, NDT methods | Finished machine tool casting component |
Looking ahead, the future of machine tool casting is poised for further innovation with the adoption of additive manufacturing for direct metal printing and the use of artificial intelligence to enhance simulation accuracy. For example, machine learning algorithms can analyze historical casting data to predict defects with higher precision, reducing reliance on empirical rules. Additionally, the development of new aluminum and composite alloys will expand the possibilities for lightweight, high-strength machine tool casting components. The ongoing research in areas like digital twins, where a virtual replica of the casting process is maintained in real-time, promises to bring unprecedented levels of control and optimization to foundries. In all these advancements, the core objective remains to produce reliable and precise machine tool casting parts that meet the evolving demands of modern manufacturing.
In conclusion, the marriage of ProCAST numerical simulation and SLS-based 3D printing has fundamentally transformed the landscape of machine tool casting. By enabling virtual validation and rapid prototyping, these technologies reduce time-to-market, cut costs, and improve product quality. The case study of the large aluminum chuck illustrates how strategic material selection and process optimization can yield significant performance benefits, such as reduced inertia and enhanced precision. As we continue to push the boundaries of digital manufacturing, machine tool casting will undoubtedly remain at the forefront, driving innovation in industries ranging from automotive to aerospace. The key takeaway is that embracing these integrated approaches not only solves immediate production challenges but also paves the way for more agile and sustainable foundry operations. Through continuous improvement and adoption of cutting-edge tools, the future of machine tool casting looks brighter than ever, promising components that are stronger, lighter, and more cost-effective.