
In my extensive experience within the precision investment casting industry, producing high-integrity shell castings for demanding applications has always been a fascinating and intricate challenge. Shell castings, by their very nature, often involve complex geometries with varying wall thicknesses, internal passages, and stringent quality requirements, particularly in sectors like aerospace and defense. The journey from a conceptual design to a finished, reliable shell casting is a symphony of meticulous planning, precise execution, and continuous process optimization. This article delves deep into the comprehensive methodology I employ for manufacturing such components, focusing on the unique challenges of thin-walled, structurally intricate shell castings. I will systematically explore structural analysis, gating system design, the pivotal shell-building process, thermal treatments, and final finishing, enriching the discussion with empirical data tables and fundamental engineering formulas.
The foundational step in any successful shell casting project is a thorough structural and manufacturability analysis. The component in focus here is a quintessential example of a challenging shell casting: a rectangular housing with dramatic variations in wall thickness, from substantial corner sections to expansive, delicate panels. Such disparities immediately flag potential issues like distortion, shrinkage porosity in thick zones, and filling challenges in thin sections. For shell castings, the aspect ratio of internal features is critical; deep, narrow cavities complicate the investment process, affecting coating flow, sand stucco penetration, and subsequent core removal. While casting such features can alleviate some shell-building stresses and reduce shrinkage, the final decision must balance casting feasibility with post-casting machining capabilities and dimensional tolerances. In this case, the decision was made not to cast the deep corner holes, prioritizing machining accuracy over certain casting advantages. This analysis underscores a core principle: every shell casting requires a tailored approach where design, casting process, and secondary operations are considered as an interconnected system.
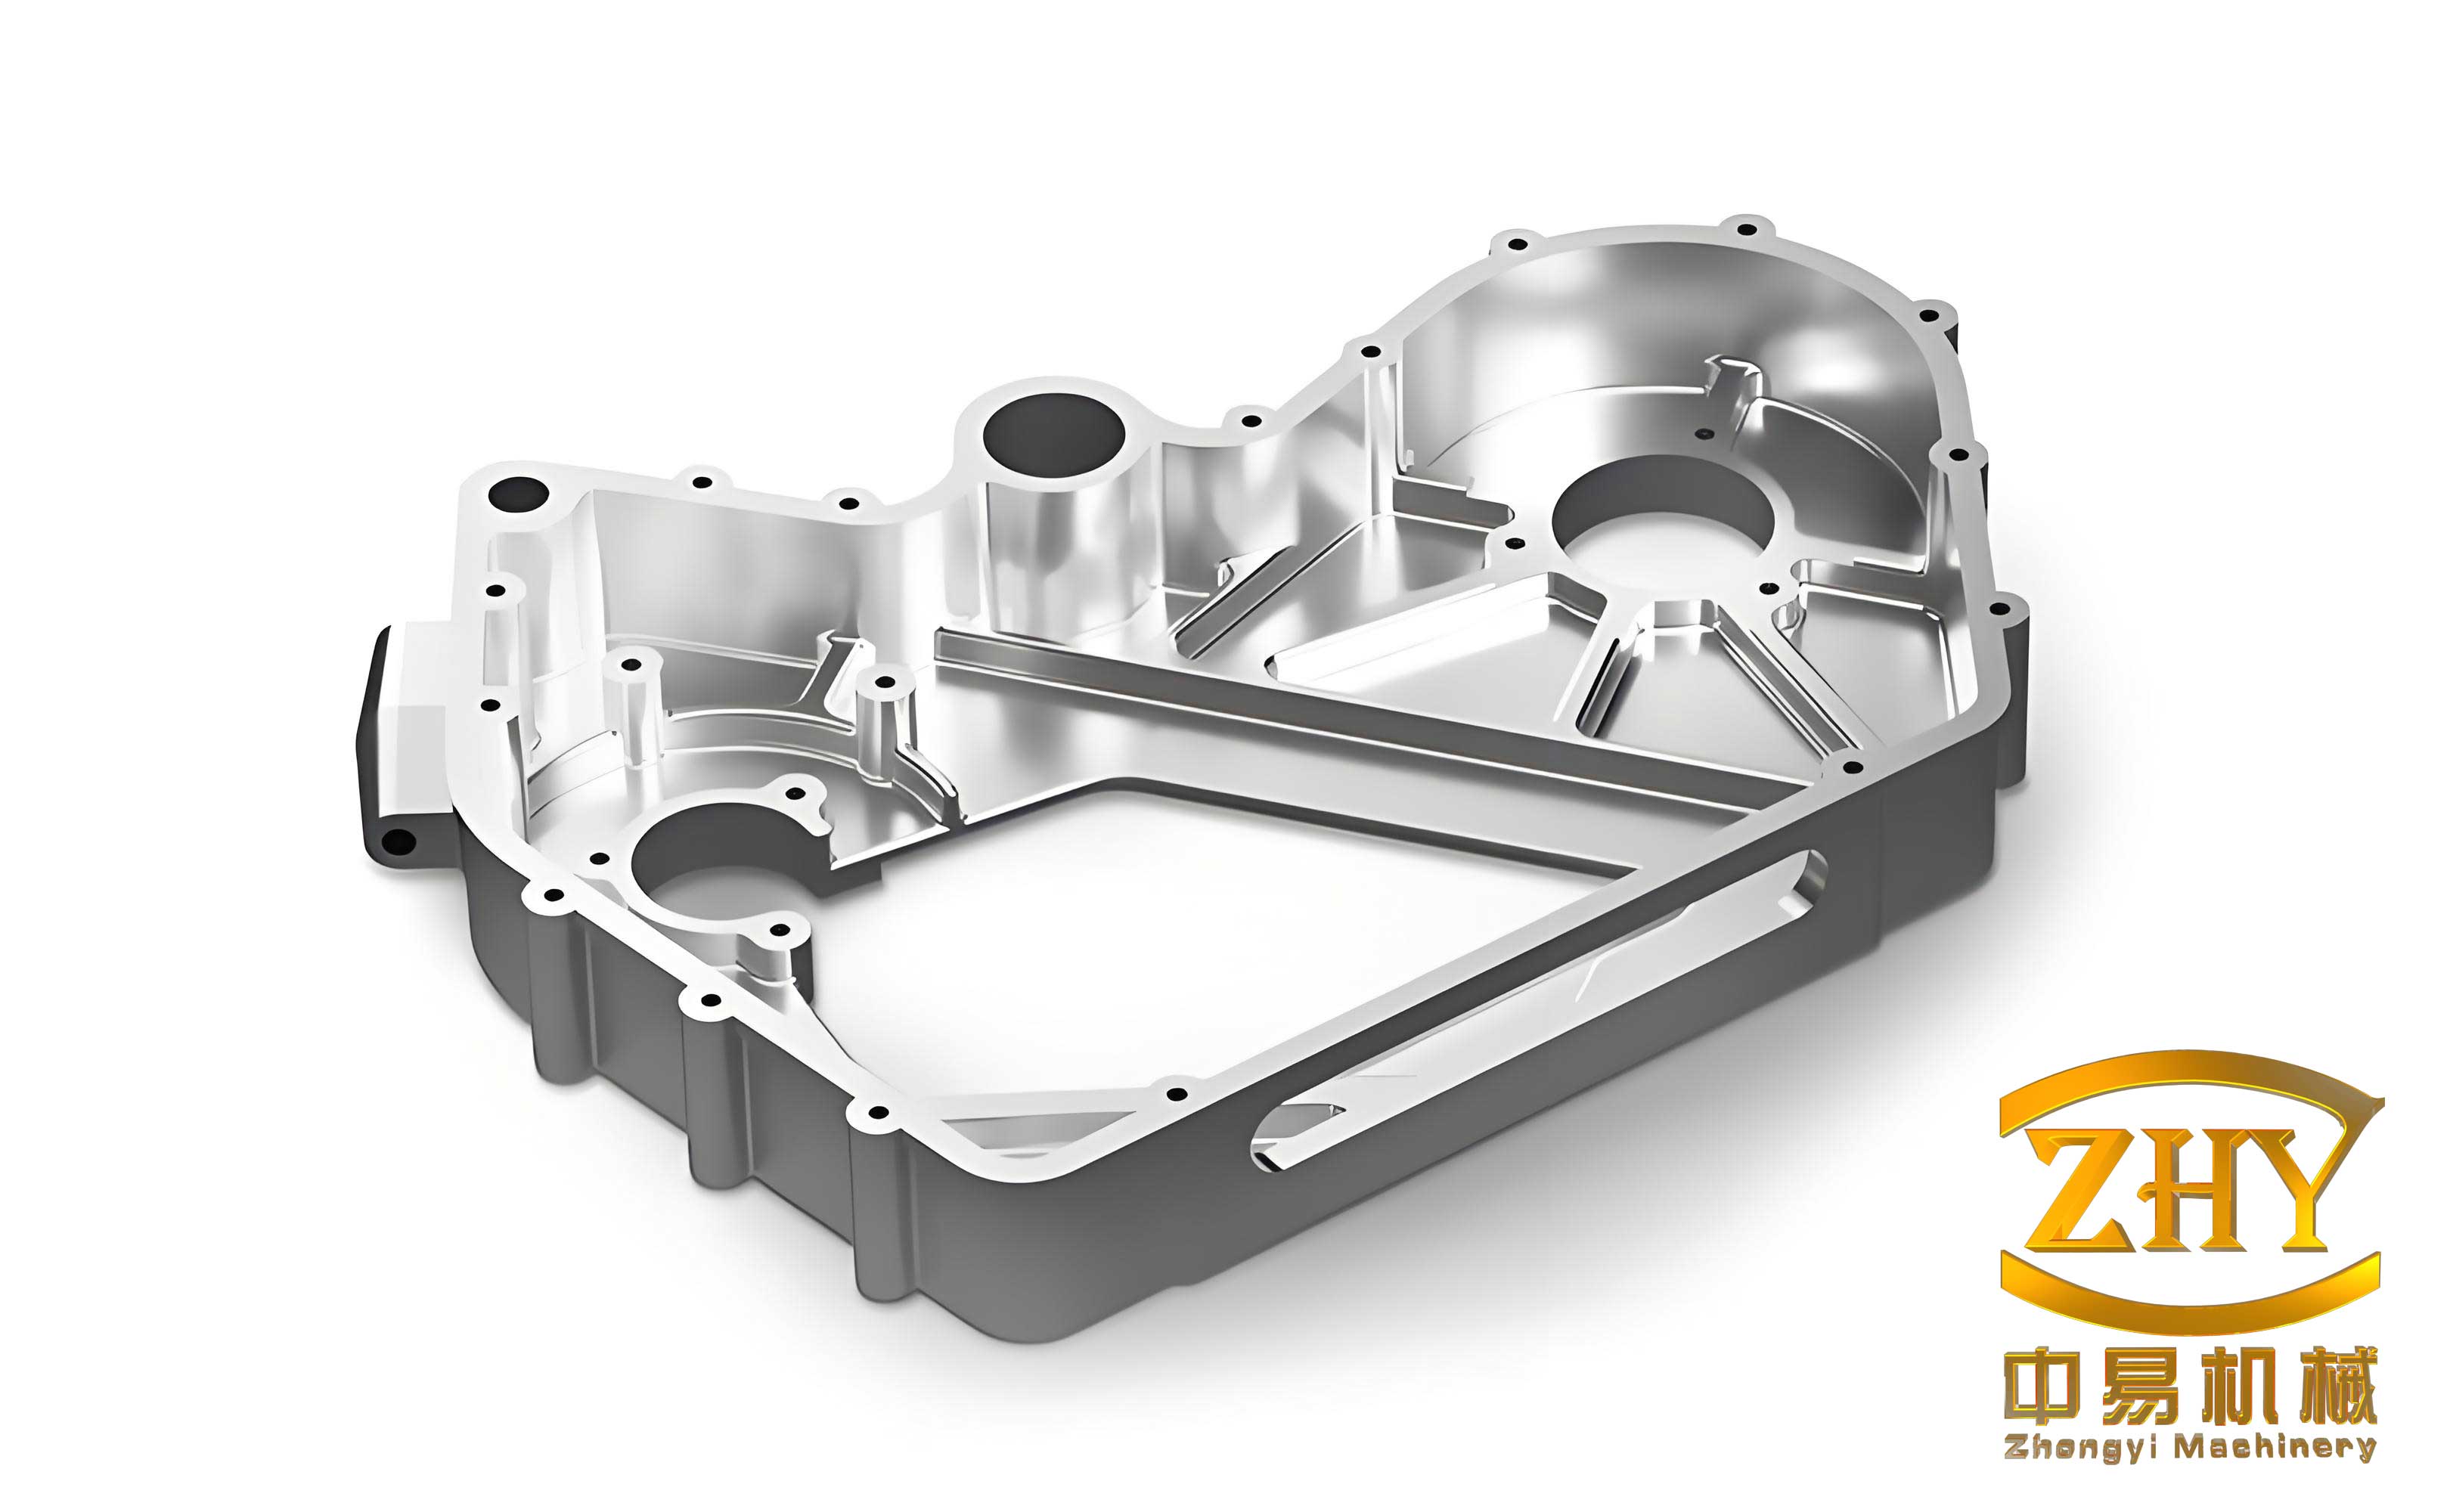
The heart of the process lies in the gating and rigging design, which directly impacts soundness, surface finish, and yield. For these specific shell castings, several schemes were prototyped and evaluated. A vertical assembly with a square central sprue offered good shell-building characteristics for the recessed faces but left unacceptable gate marks on non-machined surfaces. A top-pouring, suspended scheme promoted filling but introduced risks of mold erosion, oxide entrapment, and fragile pattern assembly connections. An inclined mounting strategy improved coating access but led to unacceptable distortion and isolated shrinkage in the un-gated thick corners. The optimal solution, derived from iterative testing, was a vertical assembly with extended, shaped gates connecting to the component’s machined faces. This configuration, with patterns staggered in the cluster to facilitate coating, ensured directional solidification toward the feeder, excellent surface finish on critical外观 surfaces, and minimal distortion. The key takeaway for producing reliable shell castings is that the gating system must serve multiple masters: thermal control, filling dynamics, and shell-building practicality.
| Scheme Description | Advantages | Disadvantages | Suitability for Shell Castings |
|---|---|---|---|
| Vertical with Central Sprue | Good shell coating access, simple cluster. | Gate marks on finished surfaces, potential for distortion. | Low. Compromises cosmetic requirements. |
| Top-Pouring Suspended | Excellent fill capability, good venting. | Risk of oxide/sand inclusions, fragile gates, extra machining. | Moderate. Requires excellent process control. |
| Inclined Mounting | Improved coating for deep recesses. | Unbalanced shrinkage, severe distortion. | Low. Unacceptable for dimensionally critical parts. |
| Vertical with Extended Shaped Gates | Directional solidification, excellent finish on key surfaces, minimal distortion. | Requires precise gate design and cutting. | High. Balances metallurgical and cosmetic needs. |
The creation of the ceramic shell itself is the most critical phase in determining the surface quality and dimensional fidelity of the final shell castings. For thin-walled, large-flat-area components, the primary risks are shell delamination, mold cracking, and insufficient strength leading to metal penetration or distortion. I utilize a sodium silicate-based binder system, where control is paramount. The slurry parameters are tightly governed. The viscosity $\eta$ of the prime slurry is crucial for achieving a uniform coating without draining or pooling, especially on vertical surfaces. It can be related to the binder properties and powder loading by empirical relationships such as:
$$ \eta \propto \left( \frac{\phi}{\phi_m – \phi} \right)^n $$
where $\phi$ is the volume fraction of refractory flour, $\phi_m$ is the maximum packing fraction, and $n$ is a constant. In practice, for the first coat on these delicate shell castings, I maintain a viscosity between 50-60 seconds (as measured by a Zahn cup), corresponding to a specific gravity of 1.27-1.29 for the binder and a powder-to-liquid ratio of 1:1.5 to 1:1.7.
The hardening reaction between sodium silicate (Na$_2$O·mSiO$_2$) and ammonium chloride (NH$_4$Cl) is fundamental:
$$ \text{Na}_2\text{O}·m\text{SiO}_2 + 2\text{NH}_4\text{Cl} \rightarrow 2\text{NaCl} + 2\text{NH}_3↑ + m\text{SiO}_2·\text{H}_2\text{O} $$
The precipitated silica gel forms the bond. To ensure complete and uniform reaction, especially in deep recesses of the shell casting pattern, the hardening bath concentration is kept above 25% NH$_4$Cl, with immersion times adjusted for coat number. The first two coats are critically hand-brushed into corners to eliminate air entrapment—a common nucleation site for shell delamination. Between dipping and stuccoing, the cluster is constantly rotated to prevent gravitational slurry run-off, which creates weak, laminated zones. The drying kinetics between coats are equally vital; insufficient ambient drying before hardening can trap solvent and weaken the layer, while excessive drying can cause cracking. A balance is struck through controlled humidity and time.
| Process Stage | Key Parameter | Target Value/Range | Rationale |
|---|---|---|---|
| Slurry Preparation (Prime Coat) | Binder Modulus (M) | 3.1 – 3.2 | Optimal gelation speed and strength. |
| Binder Specific Gravity | 1.27 – 1.29 | Controls silica content and reactivity. | |
| Powder-to-Liquid Ratio | 1 : 1.5 – 1.7 | Determines slurry viscosity and coating thickness. | |
| Hardening | NH₄Cl Solution Concentration | > 25% | Ensures complete silica gel formation. |
| Prime Coat Hardening Time | 25-30 minutes | Complete reaction without over-saturation. | |
| Drying | Intercoat Drying Time (Ambient) | 60-90 minutes | Allows alcohol evaporation, prevents cracks. |
| Dewaxing | Autoclave Medium & Temperature | High-Pressure Steam > 95°C | Rapid wax removal, minimal shell expansion. |
Following dewaxing and thorough washing to remove residual salts and loose grains, the green shells for our shell castings must undergo a controlled firing process. This serves to burn out any residual pattern material, volatilize chemical residues, and sinter the ceramic matrix to develop adequate high-temperature strength. The thermal cycle must be designed to avoid thermal shock. A gradual ramp-up to 300°C is employed to drive off free and chemically bound water. The critical sintering range for a typical fused silica-based shell is between 850°C and 950°C. The holding time at peak temperature, typically 1.5 to 2.5 hours at 880°C, is calculated based on the shell’s thickness and density to ensure through-thickness sintering. The relationship between sintering strength and time/temperature can be approximated by models for viscous sintering:
$$ \frac{\Delta L}{L_0} \propto \left( \frac{\gamma t}{\eta r} \right)^{1/n} $$
where $\Delta L/L_0$ is the linear shrinkage, $\gamma$ is the surface energy, $t$ is time, $\eta$ is the viscosity of the glassy phase, $r$ is the particle radius, and $n$ is a constant. For shell castings with large flat areas, it is imperative to fire shells in a manner that prevents mechanical loading or restraint, which can induce permanent warpage. They are placed on fine sand or special setters to allow free thermal expansion and contraction.
The metallurgical phase for carbon steel shell castings, such as ZG230-450, focuses on achieving clean, sound metal with optimal fluidity. Deoxidation practice is critical to prevent gas porosity and oxide films, which are catastrophic in thin sections. A combination of aluminum and ferro-silicon is commonly used. The final pouring temperature is a compromise: high enough to fill thin walls but low enough to minimize metal-mold reaction and grain growth. For these steel shell castings, I have established that the ideal pouring temperature range is 1520°C to 1550°C. The fluidity length $L_f$ of the molten steel, a key factor for filling thin sections, is influenced by temperature and composition according to relationships like:
$$ L_f = k (T_{pour} – T_{liquidus}) $$
where $k$ is a constant dependent on alloy properties and mold characteristics. Preheating the fired shells to approximately 800°C before pouring is essential to prevent premature freezing in the thin sections of the shell castings. The filling process must be rapid and turbulent-free to avoid air entrapment. The well-established Bernoulli’s principle governs the flow velocity $v$ from the pouring cup:
$$ v = \sqrt{2gh} $$
where $g$ is gravity and $h$ is the metallostatic head. This highlights the importance of maintaining adequate head pressure throughout the pour to ensure complete filling of the intricate shell castings.
Once solidified and cooled, the shell castings enter the post-casting processing stage. The ceramic shell is removed via mechanical vibration—a delicate operation for thin-walled parts to avoid damage. The gates, designed for easy removal, are separated using abrasive cut-off wheels. The final surface preparation involves shot blasting with fine steel media (e.g., 0.5 mm diameter) for a controlled duration (e.g., 20 minutes) to remove the refractory glaze and reveal the base metal without peening over delicate features. For the steel shell castings discussed, a stress-relief anneal is performed, typically heating to 600-650°C, holding, and furnace cooling, to relieve residual stresses from uneven cooling and ensure dimensional stability during machining. The inspection criteria for these high-integrity shell castings are severe, often requiring radiographic or penetrant testing to verify the absence of shrinkage, hot tears, or inclusions in critical areas.
In conclusion, the precision investment casting of complex shell castings is an exercise in systems engineering. Success hinges on the synergistic optimization of every step: from the initial DFM analysis that guides feature design, through the rigging strategy that controls solidification, to the chemically and thermally precise shell-building process that forms the negative mold. The subsequent melting, pouring, and finishing steps must all be executed with the unique geometry of the shell casting in mind. Through rigorous control of parameters—quantified in tables and understood through fundamental physical and chemical principles—it is possible to consistently produce high-quality, thin-walled shell castings that meet the most demanding mechanical and cosmetic specifications. The experience garnered from producing such components continuously refines the empirical models and instinct that guide the process, ensuring that each new project in the realm of shell castings builds upon a foundation of proven practice and scientific understanding.
Furthermore, the economics of shell castings production can be modeled. The total cost $C_{total}$ per shell casting is a sum of material, labor, and overhead costs, which scale with complexity:
$$ C_{total} = C_{material} + C_{labor} \cdot T_{process} + C_{overhead} $$
Where $T_{process}$ is the total handling time. Process optimization, such as increasing cluster yield or reducing shell coat count without compromising quality, directly improves $C_{total}$. For instance, the number of ceramic coats $N$ required for a shell casting is determined by a mechanical strength criterion related to the metallostatic pressure $P_m$ during pouring:
$$ P_m = \rho g h $$
The shell must withstand this pressure, requiring a thickness $t_s$ that scales with $N$. An empirical rule might be $t_s \approx k \cdot N$, where $k$ is the average coat thickness. Optimizing $N$ is thus a key lever for efficiency in producing shell castings.
The field continues to evolve with advancements in binder systems (like colloidal silica versus sodium silicate), refractory materials, and simulation software for solidification and stress analysis. These tools allow for even more precise prediction and control, pushing the boundaries of what is possible with intricate shell castings. The ultimate goal remains constant: to transform a complex design intent into a robust, net-shape or near-net-shape metal component reliably and economically, a challenge that the investment casting process for shell castings is uniquely positioned to meet.