
As a researcher in the field of advanced manufacturing, I have dedicated significant effort to optimizing the production of critical components for renewable energy systems. Among these, hollow driving shell castings for wind turbines represent a pinnacle of engineering challenge due to their stringent performance requirements and complex geometry. Wind energy, as a clean and renewable source, has gained global prominence, driving demand for durable and efficient components. These shell castings, typically made from ductile iron, serve as key parts in gearboxes, bases, and bearing housings, operating at heights exceeding 100 meters and enduring temperatures as low as -40°C for over 20 years. In this article, I will elaborate on the comprehensive quality control measures and production processes developed for these shell castings, drawing from my experiences and research to provide an in-depth analysis that spans design, metallurgy, and validation.
The primary challenge in producing these shell castings lies in meeting the high standards for mechanical properties, microstructural integrity, and defect minimization. The castings must adhere to specifications such as EN-GJS-400-18U-LT, which mandates a minimum Charpy V-notch impact energy of 7 J per sample and an average of 10 J at -20°C, alongside full non-destructive testing via ultrasonic and magnetic particle methods per EN12680.3 and DIN EN1369 Level 2. To address this, I have focused on a holistic approach that integrates casting design, material chemistry, and processing parameters. This article will delve into each aspect, utilizing tables and formulas to summarize key data and theoretical foundations, thereby offering a robust framework for practitioners in the industry.
Analysis of Casting Process Difficulties
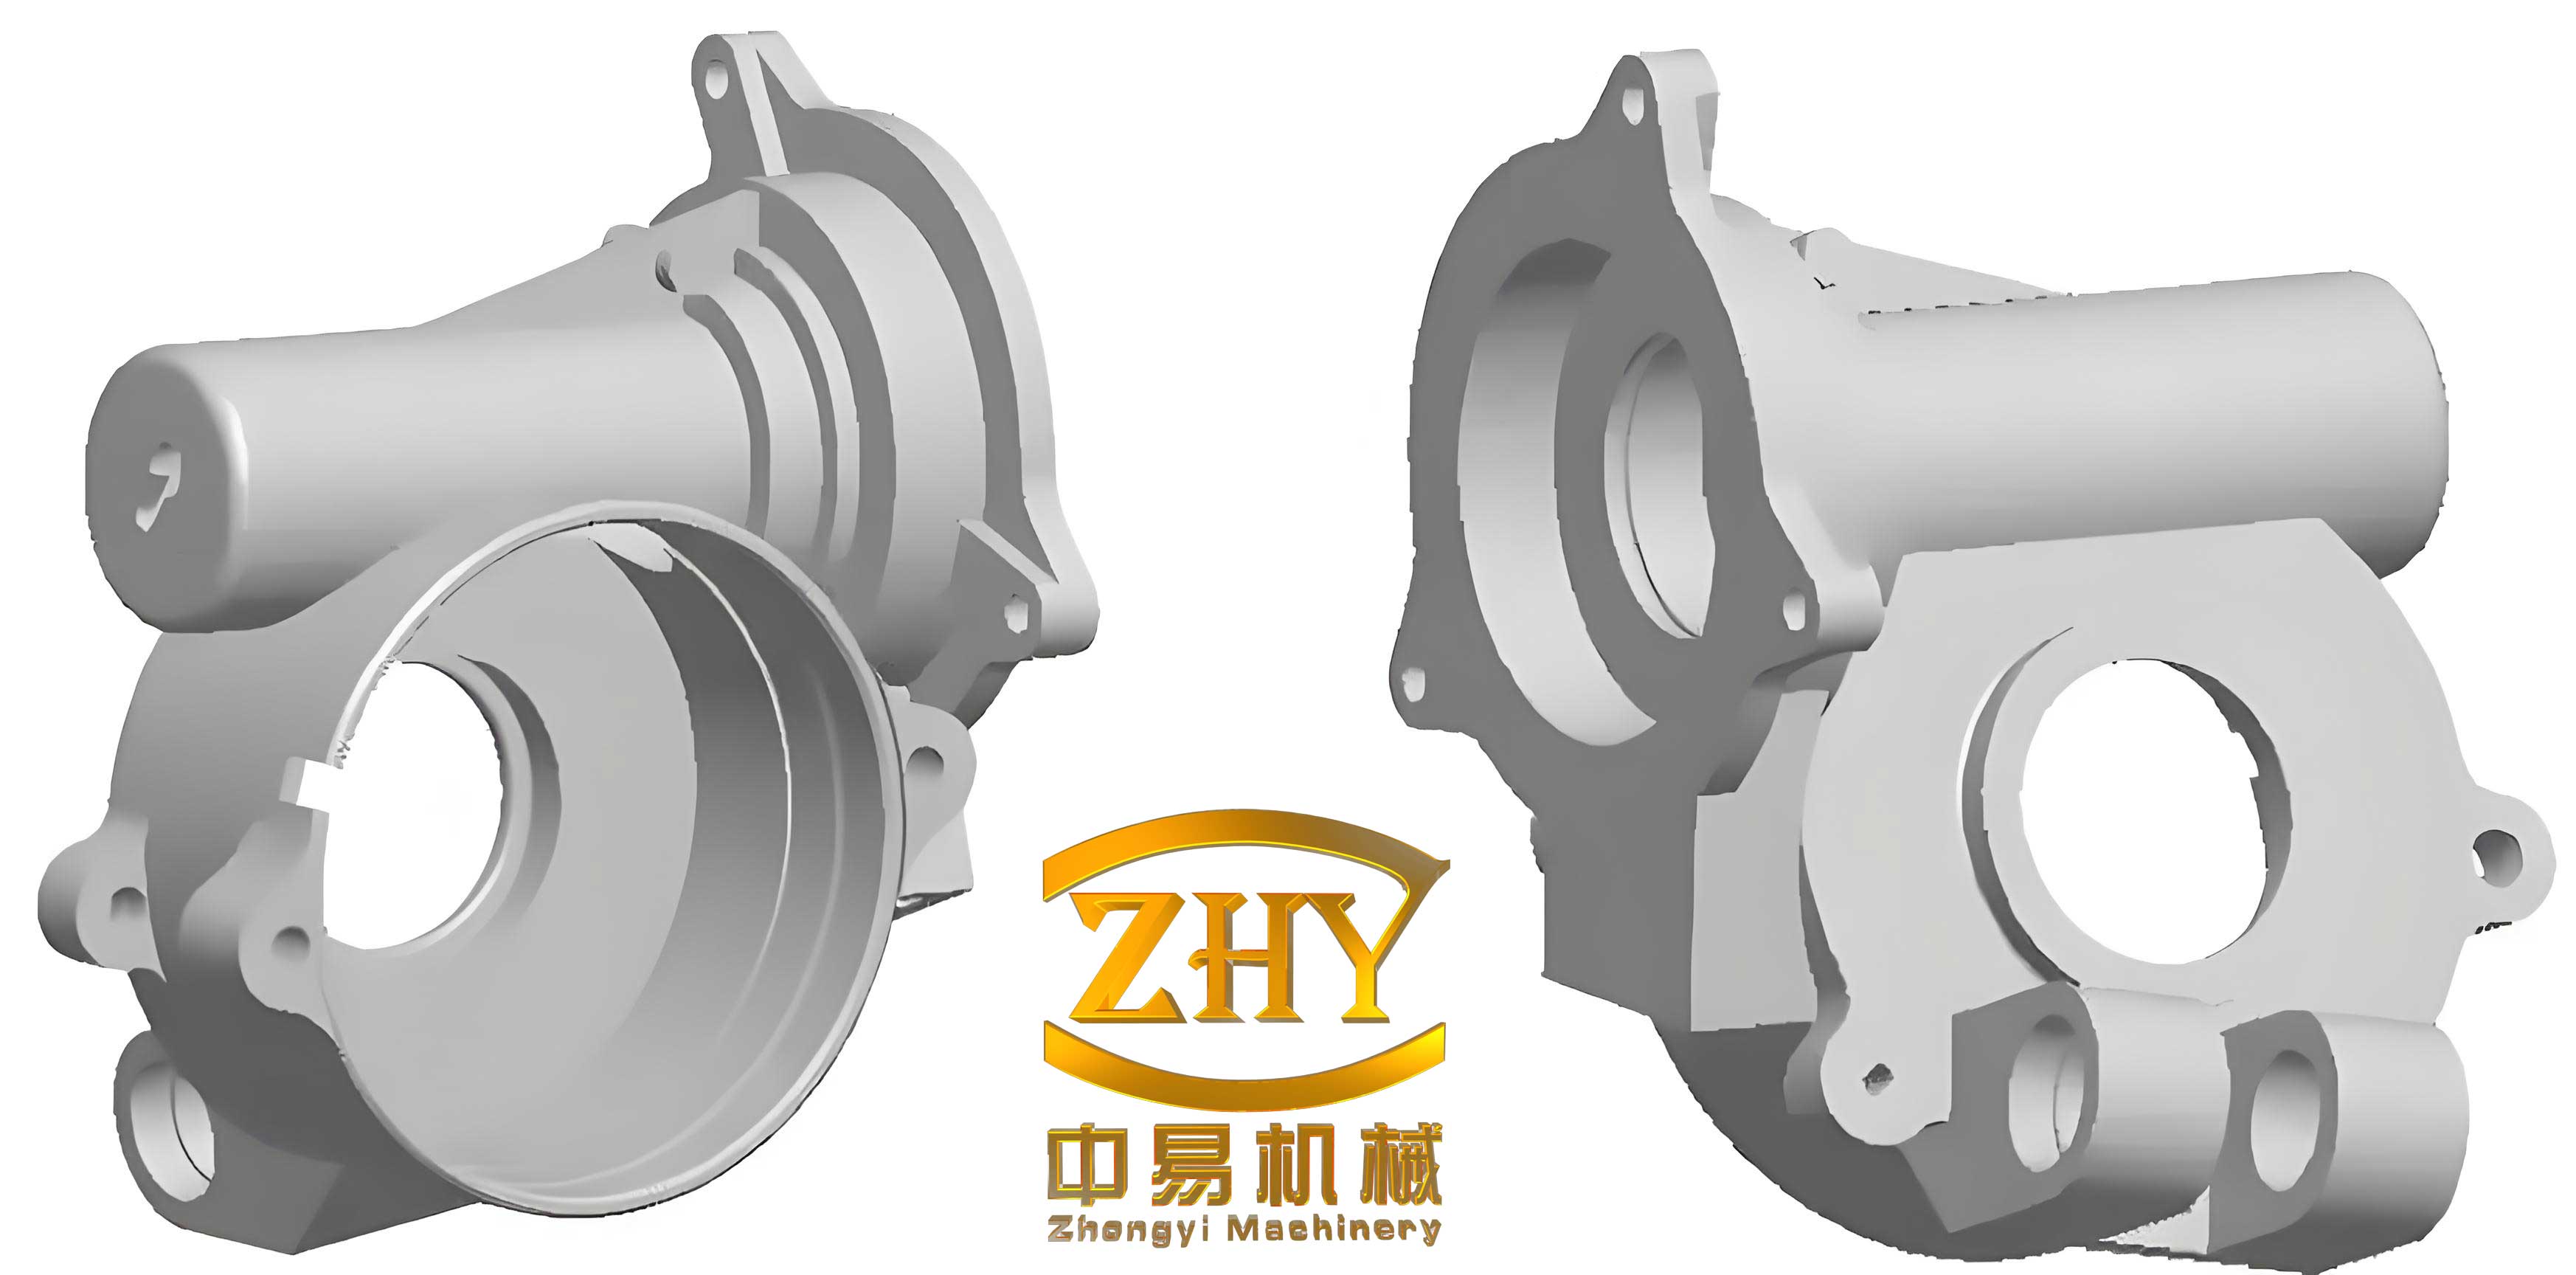
From my perspective, the difficulties in producing these shell castings stem from their structural and performance demands. The component features a truncated conical shape with an outer contour of approximately ϕ1,678 mm × ϕ800 mm × 743 mm and a mass of 1,514 kg. Key dimensions include a wall thickness of 40 mm, reinforcement ribs of 30 mm, and maximum thickness zones of 70 mm. Such geometry necessitates precise control over solidification and cooling to avoid defects like shrinkage porosity, cold shuts, and microstructural inhomogeneities. The requirement for low-temperature toughness further complicates matters, as ductile iron must maintain high ductility and impact resistance under sub-zero conditions. I have analyzed these challenges through the lens of material science, where the balance between graphite nodularity, matrix structure, and impurity levels becomes critical. For instance, the impact energy requirement can be modeled using fracture mechanics principles, where the transition temperature $T_c$ is influenced by composition and processing:
$$T_c = T_0 + k \cdot \Delta C + m \cdot \Delta S$$
Here, $T_0$ represents a base transition temperature, $k$ and $m$ are material constants, $\Delta C$ denotes deviations in carbon equivalent, and $\Delta S$ signifies sulfur content variations. This formula underscores the need for tight compositional control, which I will expand upon in later sections.
Casting Process Design
In my work, the casting process design for shell castings revolves around achieving dimensional accuracy, surface finish, and internal soundness. I employ a systematic approach that encompasses parting line selection, core design, gating system layout, and cooling strategies, all tailored to the unique geometry of the hollow driving shell.
Parting Line Design
I typically choose parting lines that minimize machining allowances and facilitate mold assembly. For these shell castings, the parting plane is positioned to allow for uniform machining allowances of 12-14 mm on various surfaces. I utilize furan resin cold-setting sand for both molds and cores, with surface finishing to reduce roughness. The use of zircon-based coatings, applied at 0.4-0.6 mm thickness, prevents defects like sand adhesion and burn-on, ensuring high-quality surface integrity for the shell castings.
Core Design
The internal structure of the shell castings requires multiple cores to form cavities and reinforcing ribs. Based on my designs, three core types are employed: a central core for the hollow interior, a peripheral core for the outer shape, and smaller cores for lug holes. The arrangement ensures stability during pouring and minimizes core shifts. I summarize the core specifications in Table 1, highlighting their roles in achieving the desired geometry for shell castings.
| Core Type | Dimensions (mm) | Mass (kg) | Function |
|---|---|---|---|
| Central Core | ϕ734 × 530 | 236 | Forms internal hollow cavity |
| Peripheral Core | ϕ1420 × ϕ516 × 552 | 1109 | Defines outer contour and ribs |
| Lug Hole Cores (6 units) | 100 × 70 × 70 | 0.5 each | Creates mounting holes |
Gating System Design
My approach to gating emphasizes low turbulence and steady filling, crucial for avoiding oxide inclusions and cold defects. I implement a semi-closed bottom-gating system with a ceramic sprue of ϕ70 mm, radial ingates at the flange, and multiple vents and risers. The gating ratio, adjusted for optimal flow, is set at $\Sigma F_{\text{sprue}} : \Sigma F_{\text{runner}} : \Sigma F_{\text{ingate}} = 1 : 1.8 : 1.6$, where $F$ denotes cross-sectional area. This design promotes laminar flow, reducing the Reynolds number $Re$ below critical thresholds:
$$Re = \frac{\rho v D}{\mu}$$
Here, $\rho$ is molten iron density, $v$ is flow velocity, $D$ is characteristic diameter, and $\mu$ is dynamic viscosity. By controlling $v$ through gating geometry, I minimize turbulence, enhancing the quality of shell castings.
Cooling System Design
To address uneven cooling in thick sections of shell castings, I combine chill plates and intensified cooling methods. Chills, with thicknesses equal to the wall thickness (e.g., 50 mm for 50 mm sections), are strategically placed to accelerate solidification. The cooling rate $R$ can be estimated using Fourier’s law of heat conduction:
$$R = \frac{k \Delta T}{\rho c_p L^2}$$
where $k$ is thermal conductivity, $\Delta T$ is temperature gradient, $\rho$ is density, $c_p$ is specific heat, and $L$ is characteristic length. By optimizing chill placement, I reduce solidification time $t_s$, which correlates with defect formation:
$$t_s = \frac{V}{A} \cdot \frac{\Delta H}{R}$$
Here, $V$ is volume, $A$ is surface area, and $\Delta H$ is latent heat. Table 2 outlines the chill specifications used in my production trials for shell castings.
| Chill Type | Thickness (mm) | Spacing (mm) | Quantity | Location |
|---|---|---|---|---|
| Type 1 | 50 | 20 | 20 | Outer wall sections |
| Type 2 | 50 | 20 | 12 | Rib intersections |
| Type 3 | 50 | 20 | 12 | Flange regions |
Melting and Pouring Process Control
From my experience, the metallurgical control of ductile iron for shell castings is paramount to achieving the required low-temperature toughness and mechanical properties. I focus on composition optimization, melting practices, and inoculation techniques, all aimed at enhancing graphite nodularity and matrix homogeneity.
Chemical Composition Control
I meticulously regulate alloying elements to balance strength, ductility, and impact resistance. Based on my research, the composition ranges for shell castings are designed as follows, with each element playing a specific role:
- Carbon (C): 3.65–3.80% – Promotes graphite formation and fluidity, but excess can cause floating.
- Silicon (Si): 1.90–2.40% – Strengthens ferrite but reduces toughness if too high; I limit it to below 2.5% for low-temperature applications.
- Manganese (Mn): <0.20% – Minimized to avoid carbide formation and segregation.
- Phosphorus (P) and Sulfur (S): <0.02% and <0.012%, respectively – Controlled to reduce brittle phases.
- Rare Earth (RE): 0.010–0.020% and Magnesium (Mg): 0.035–0.060% – Ensure graphite spheroidization without excessive residues.
The carbon equivalent $CE$ is a critical parameter, calculated as:
$$CE = \%C + \frac{\%Si + \%P}{3}$$
For shell castings, I target a $CE$ of 4.2–4.4 to optimize castability and mechanical properties. The effect of silicon on impact energy $E$ can be modeled empirically:
$$E = E_0 – \alpha \cdot (\%Si – \%Si_{\text{opt}})^2$$
where $E_0$ is maximum impact energy, $\alpha$ is a constant, and $\%Si_{\text{opt}}$ is the optimal silicon content (around 2.0%). Table 3 summarizes my target composition for producing high-quality shell castings.
| Element | Target Range | Influence on Properties |
|---|---|---|
| C | 3.65–3.80 | Enhances fluidity and graphite precipitation |
| Si | 1.90–2.40 | Increases strength, but reduces toughness if high |
| Mn | <0.20 | Reduces impact resistance if elevated |
| P | <0.02 | Prevents phosphide eutectic formation |
| S | <0.012 | Minimizes slag formation and improves nodularity |
| RE | 0.010–0.020 | Aids in graphite spheroidization |
| Mg | 0.035–0.060 | Primary spheroidizing agent |
Melting, Spheroidization, Inoculation, and Pouring
In my practice, I use a duplex melting process involving a cupola and medium-frequency induction furnace to achieve consistent superheat and composition. Charge materials include 50–70% pig iron, 20–40% returns, and 10–20% scrap steel, all selected for purity. Spheroidization is performed via the sandwich method with 1.0–1.2% magnesium-ferrosilicon alloy, while inoculation employs two-stage treatment: 0.3% FeSi75 during pouring and 0.2–0.3% fine-grained Ba-Si inoculant before casting. The kinetics of nodular graphite formation can be described by the Avrami equation:
$$X(t) = 1 – \exp(-k t^n)$$
where $X(t)$ is the fraction transformed, $k$ is a rate constant dependent on inoculation, and $n$ is an exponent related to nucleation sites. Pouring temperature is maintained at $1320 \pm 10^\circ\text{C}$ to balance fluidity and shrinkage, with the solidification time $t_f$ estimated as:
$$t_f = \frac{\Delta T_m}{\dot{T}}$$
Here, $\Delta T_m$ is the melting range and $\dot{T}$ is the cooling rate. By optimizing these parameters, I ensure that the shell castings exhibit fine graphite nodules and a ferritic matrix, essential for low-temperature performance.
Production Validation and Results
Through my production trials, I have validated the effectiveness of these quality control measures. Multiple shell castings were manufactured and subjected to rigorous testing, all meeting the specified standards. The attached test bars, with dimensions of 70 mm × 70 mm × 180 mm, demonstrated excellent mechanical properties and microstructure.
Microstructural analysis revealed graphite nodularity above 95%, nodule size of 5–8 μm, ferrite content exceeding 95%, pearlite below 5%, and carbides under 1%, aligning with EN1563 requirements. The mechanical properties, summarized in Table 4, confirm the suitability of these shell castings for wind turbine applications.
| Property | Standard Requirement | Measured Value | Remarks |
|---|---|---|---|
| Tensile Strength (MPa) | ≥370 | 404 | Exceeds standard |
| Yield Strength (MPa) | ≥230 | 262 | High strength-ductility balance |
| Elongation (%) | ≥15.0 | 24.0 | Excellent ductility |
| Hardness (HB) | 120–175 | 144 | Within acceptable range |
| Charpy Impact Energy (-20°C) | Single ≥7 J, Avg. ≥10 J | 15, 14, 13 J (Avg. 14 J) | Superior low-temperature toughness |
The success of these shell castings can be attributed to the integrated approach encompassing design precision, compositional control, and advanced processing. I have further analyzed the data using statistical models, such as regression analysis for property prediction:
$$Y = \beta_0 + \beta_1 X_1 + \beta_2 X_2 + \epsilon$$
where $Y$ represents impact energy, $X_1$ and $X_2$ are factors like silicon content and cooling rate, $\beta$ coefficients indicate influence magnitudes, and $\epsilon$ is error. This model helps refine process windows for future productions of shell castings.
Conclusion
In summary, my work on hollow driving shell castings for wind power highlights the critical importance of a systematic quality control strategy. By addressing design complexities through optimized parting lines, cores, gating, and cooling systems, and by enforcing stringent metallurgical controls via composition targeting and advanced inoculation, I have achieved shell castings that meet the demanding standards of the wind energy sector. The validation through mechanical and non-destructive testing confirms the robustness of these measures. As renewable energy demands grow, such methodologies will be essential for scaling up production while maintaining reliability. I believe that continued research into material science and process simulation will further enhance the performance of shell castings, contributing to sustainable energy solutions globally.