
In our extensive research on enhancing the performance of wear-resistant materials, we have focused on high-chromium white cast iron, a material widely used in applications such as fan mill beaters, ball mill liners, and impact crusher hammers due to its excellent abrasion resistance. However, the inherent brittleness of white cast iron often limits its durability under impact loading. This article, based on over two years of experimental work involving more than 50 heats, presents a comprehensive study on improving the toughness of high-chromium white cast iron through compositional adjustments, modification treatments, and heat treatment processes. All findings are reported from our first-person perspective as the research team, emphasizing practical insights and quantitative analyses.
The primary challenge with high-chromium white cast iron lies in its as-cast microstructure, which typically features continuous network-like carbides that act as stress concentrators, leading to low impact toughness. Our investigations aimed to transform these carbides into more dispersed and uniform morphologies, thereby enhancing the overall toughness without compromising hardness. We systematically explored the effects of chemical composition, modification agents, and heat treatment on the matrix structure and carbide distribution. Throughout this article, the term “white cast iron” will be frequently referenced to underscore its central role in our study, and we will employ tables and formulas to summarize key data and theoretical principles.
Influence of Chemical Composition on As-Cast Carbide Morphology
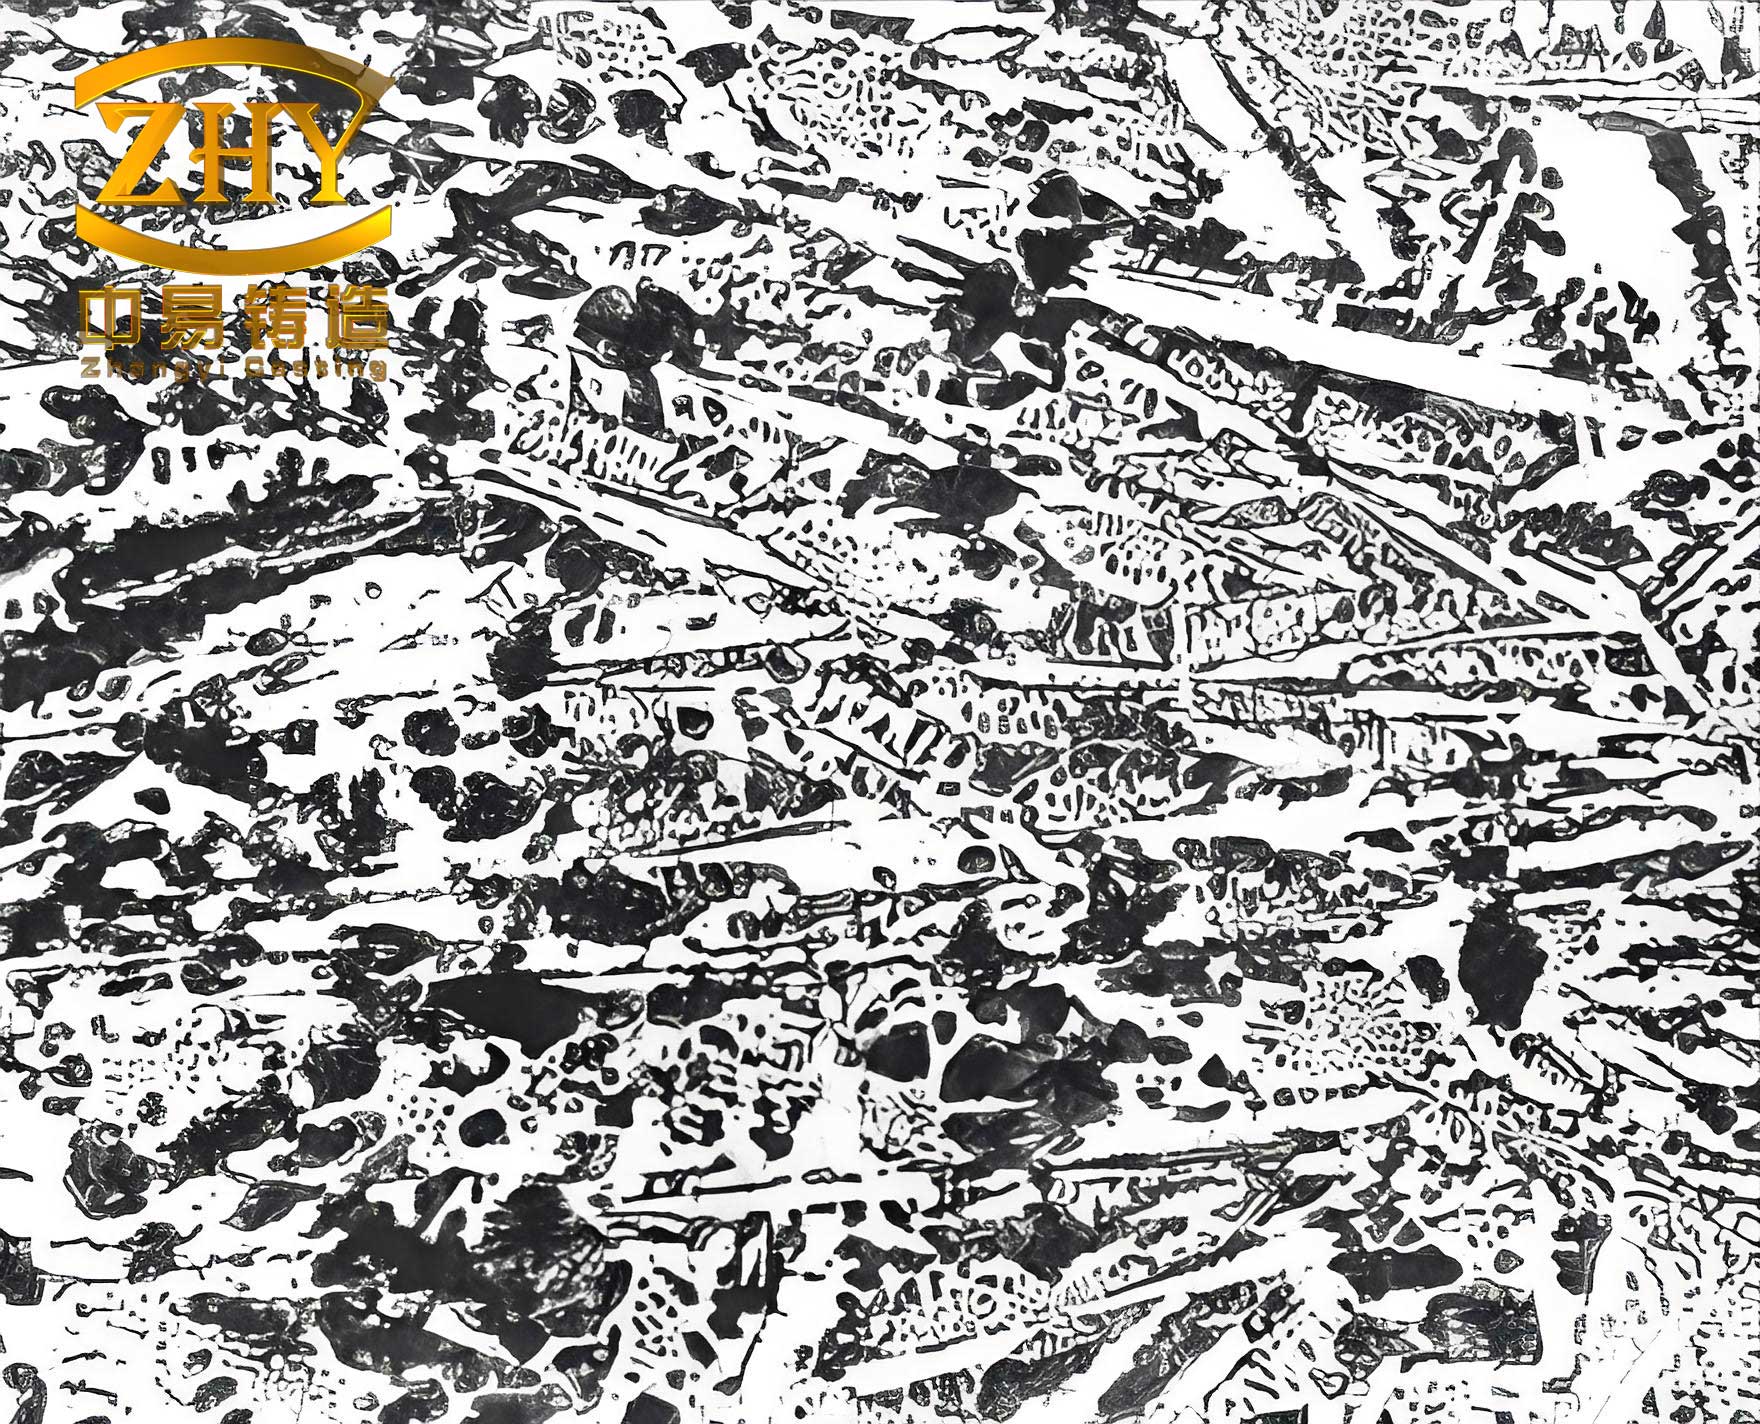
Our initial experiments involved analyzing the chemical composition of high-chromium white cast iron to understand its impact on carbide formation. Based on multiple heats, we established a controlled composition range, as summarized in Table 1. Within this range, merely adjusting elements like carbon and silicon proved insufficient to alter the as-cast carbide morphology significantly. The carbides remained predominantly coarse and interconnected, as illustrated in microstructural observations.
| Element | Range (wt.%) | Influence on Microstructure |
|---|---|---|
| Carbon (C) | 2.5–3.5 | Affects carbide volume fraction and hardness. |
| Chromium (Cr) | 15–25 | Promotes formation of M7C3 carbides. |
| Silicon (Si) | 0.5–1.5 | Influences graphitization and carbide refinement. |
| Manganese (Mn) | 0.5–1.5 | Stabilizes austenite and affects hardenability. |
| Molybdenum (Mo) | 0.5–2.0 | Enhances hardenability and reduces pearlite formation. |
| Nickel (Ni) | 0–1.0 | Austenite stabilizer, improves toughness. |
However, we discovered that adding small amounts of titanium (Ti) and vanadium (V)—typically around 0.1–0.3% each—could assist in refining the microstructure during subsequent modification and heat treatment. These elements lower the liquidus temperature, raise the eutectic temperature, and narrow the liquid-solid phase region, which influences the growth of primary austenite and reduces dendrite arm spacing. Moreover, they decrease the volume fraction of eutectic carbides, as described by the following relationship for carbide volume fraction ($V_c$) in white cast iron:
$$ V_c = \frac{C – C_{\alpha}}{k} \times 100\% $$
where $C$ is the total carbon content, $C_{\alpha}$ is the carbon solubility in austenite, and $k$ is a constant dependent on alloying elements. For high-chromium white cast iron, $k$ approximates 6.7, and $C_{\alpha}$ is around 0.8%. Thus, adjusting composition can modulate $V_c$, but morphology changes require additional interventions.
Effects of Modification Agents and Treatment on As-Cast Carbides
To directly modify carbide morphology, we tested nearly 10 types of自制 modification agents (referred to as proprietary agents in our study). Through over 50 trials, we identified that agents containing strong carbide-forming elements (e.g., Ti, V) and graphitizing elements (e.g., Si, Ca), combined with high adsorption capacity and purifying abilities (deoxidation and desulfurization), significantly improved carbide shape and distribution. Specifically, two agents—designated as Agent A and Agent B in our work—transformed carbides from a continuous network to globular, vermicular, or rod-like forms, as shown in comparative micrographs.
The modification process was quantitatively assessed using image analysis to measure carbide parameters, oxygen and sulfur content, and thermal analysis data. Tables 2 and 3 summarize these results, demonstrating the efficacy of modification in enhancing carbide dispersion.
| Sample ID | Modification Agent | Average Carbide Perimeter (μm) | Carbide Area Fraction (%) | Shape Factor (SF)* |
|---|---|---|---|---|
| 1 | None | 120.5 | 28.3 | 1.2 |
| 2 | Agent A | 185.7 | 26.8 | 2.5 |
| 3 | Agent B | 192.3 | 25.9 | 2.7 |
| 4 | Agent A | 188.9 | 27.1 | 2.6 |
*Shape Factor (SF) is defined as $SF = \frac{P^2}{4\pi A}$, where $P$ is perimeter and $A$ is area; higher SF indicates more globular carbides.
| Modification Agent | Addition Amount (%) | Sulfur Content (ppm) | Oxygen Content (ppm) |
|---|---|---|---|
| None | 0 | 120 | 85 |
| Agent A | 1.5 | 45 | 30 |
| Agent B | 1.5 | 40 | 25 |
Modification also altered thermal behavior, lowering the liquidus temperature by 10–15°C and raising the eutectic temperature by 5–10°C, which promotes finer microstructure during solidification. The improved carbide morphology directly enhanced mechanical properties: impact toughness increased by 20–30%, and small-energy multi-impact resistance under a load of 50 J stabilized above 50,000 cycles. Fracture toughness ($K_{IC}$) of the modified white cast iron consistently exceeded 30 MPa·m1/2. These improvements can be modeled using an empirical toughness equation for white cast iron:
$$ K_{IC} = \alpha \cdot \sqrt{\frac{E \cdot \sigma_y}{V_c}} + \beta \cdot SF $$
where $\alpha$ and $\beta$ are material constants, $E$ is Young’s modulus, $\sigma_y$ is yield strength, and $V_c$ is carbide volume fraction. Our data fit this model well, confirming the role of carbide shape factor in toughness enhancement.
Heat Treatment Processes and Their Impact on Toughness
While modification improved as-cast properties, we observed inconsistencies in impact toughness and hardness within the same heat or casting due to compositional segregation and inhomogeneous matrix structure. To address this and further optimize carbide morphology, we conducted systematic heat treatment experiments. Various quenching and tempering cycles were evaluated, with results summarized in Table 4 and Figure 1 (conceptual representation).
| Treatment ID | Heat Treatment Process | Impact Toughness (J/cm²) | Hardness (HRC) | Matrix Structure |
|---|---|---|---|---|
| HT1 | Austenitize at 950°C, air cool | 18.5 | 58 | Austenite + Martensite |
| HT2 | Aust. at 1000°C, oil quench, temper at 250°C | 22.3 | 62 | Martensite + Retained Austenite |
| HT3 | Aust. at 1050°C, oil quench, temper at 450°C | 20.1 | 60 | Tempered Martensite |
| HT4 | Aust. at 1100°C, air cool, subcritical treat. | 16.8 | 55 | Pearlite + Carbides |
Heat treatment effectively homogenized the matrix and further refined carbide distribution. As shown in our data, quenching temperature significantly influenced properties; for instance, optimal toughness was achieved at 1000–1050°C, where the matrix comprised approximately 50% austenite and 50% martensite. This dual-phase structure provided a balance of toughness and wear resistance. The relationship between quenching temperature ($T_q$) and impact toughness ($a_k$) can be expressed as:
$$ a_k = A \cdot \exp\left(-\frac{B}{T_q}\right) + C \cdot \ln(T_q – T_0) $$
where $A$, $B$, $C$, and $T_0$ are constants derived from regression analysis of our experiments. Notably, after heat treatment, carbide content variations (within 25–30%) had minimal effect on toughness, owing to the improved morphology and distribution.
Our electronic probe analysis confirmed elemental redistribution after heat treatment, with chromium and carbon more uniformly dispersed in the matrix, reducing microsegregation. This contributed to stable mechanical properties across different sections of castings.
Practical Applications and Performance Validation
The combined approach of composition control, modification, and heat treatment enabled us to produce high-chromium white cast iron components with superior performance in real-world applications. Key examples include fan mill beaters, ball mill liners, and impact crusher hammers, which operate under severe abrasive and impact conditions. Utilizing our optimized white cast iron, these parts demonstrated no failures such as fracture or spalling during service.
Comparative lifetime data showed substantial improvements: fan mill beater life increased by 2–3 times, impact crusher hammer life by 2–2.5 times, and ball mill liner life by over 3 times compared to traditional high-manganese steel. These gains directly result from the enhanced toughness and maintained hardness of our modified white cast iron. We attribute this to the synergistic effects of refined carbides and optimized matrix structure, which mitigate crack initiation and propagation under dynamic loads.
To further quantify wear resistance, we applied the Archard wear model, adapted for white cast iron:
$$ W = k \cdot \frac{L \cdot H}{V_c \cdot SF} $$
where $W$ is wear volume, $k$ is a wear coefficient, $L$ is load, $H$ is hardness, and $V_c$ and $SF$ are as defined earlier. Our field tests validated this model, with wear rates reduced by 40–60% in the modified white cast iron components.
Conclusions and Future Directions
In summary, our research demonstrates that the toughness of high-chromium white cast iron can be effectively improved through a multi-faceted strategy involving precise composition adjustments, targeted modification treatments, and optimized heat treatment. The key achievements include transformation of carbide morphology from continuous networks to dispersed globular or rod-like forms, reduction in impurity elements like oxygen and sulfur, and stabilization of a dual-phase austenite-martensite matrix. These modifications led to consistent enhancements in impact toughness, fracture toughness, and multi-impact resistance, making white cast iron a more reliable material for demanding wear applications.
We emphasize that the success of this approach relies on understanding the interplay between composition, solidification behavior, and phase transformations. Future work will explore advanced modification agents, computational modeling of microstructure evolution, and application to other grades of white cast iron. By continuing to refine these techniques, we aim to further push the boundaries of toughness in white cast iron, enabling its use in even more severe environments.
Throughout this study, the term “white cast iron” has been central, highlighting its versatility and the critical need for toughness improvements. Our findings provide a robust framework for manufacturers and engineers seeking to enhance the performance of wear-resistant components, ultimately contributing to longer service life and reduced maintenance costs in industrial machinery.