
In my investigation into the field of wear-resistant materials, I have focused on high-chromium white cast iron, a material renowned for its excellent abrasion resistance. The economic impetus to substitute molybdenum with manganese in this alloy is significant, as molybdenum is costly and its supply can be volatile. However, this substitution introduces a critical challenge: manganese markedly increases the volume of retained austenite post-heat treatment, which in turn compromises the hardness and, consequently, the wear performance of the white cast iron. This study was initiated to develop a optimized heat treatment protocol specifically designed to minimize retained austenite in a high-chromium white cast iron with elevated manganese content, thereby achieving a hardness comparable to its molybdenum-containing counterpart while utilizing a potentially lower processing temperature.
The core objective was to systematically identify the optimal parameters for a two-stage heat treatment process: first, a pearlitic conditioning treatment, followed by high-temperature austenitization and quenching. I employed an orthogonal experimental design to efficiently explore the effects of multiple variables. The response metrics were the amount of retained austenite, measured using X-ray diffraction analysis, and the macro-hardness. Success in this endeavor would validate a more cost-effective pathway for producing high-performance manganese-modified high-chromium white cast iron, expanding its application scope where deep hardenability is required.
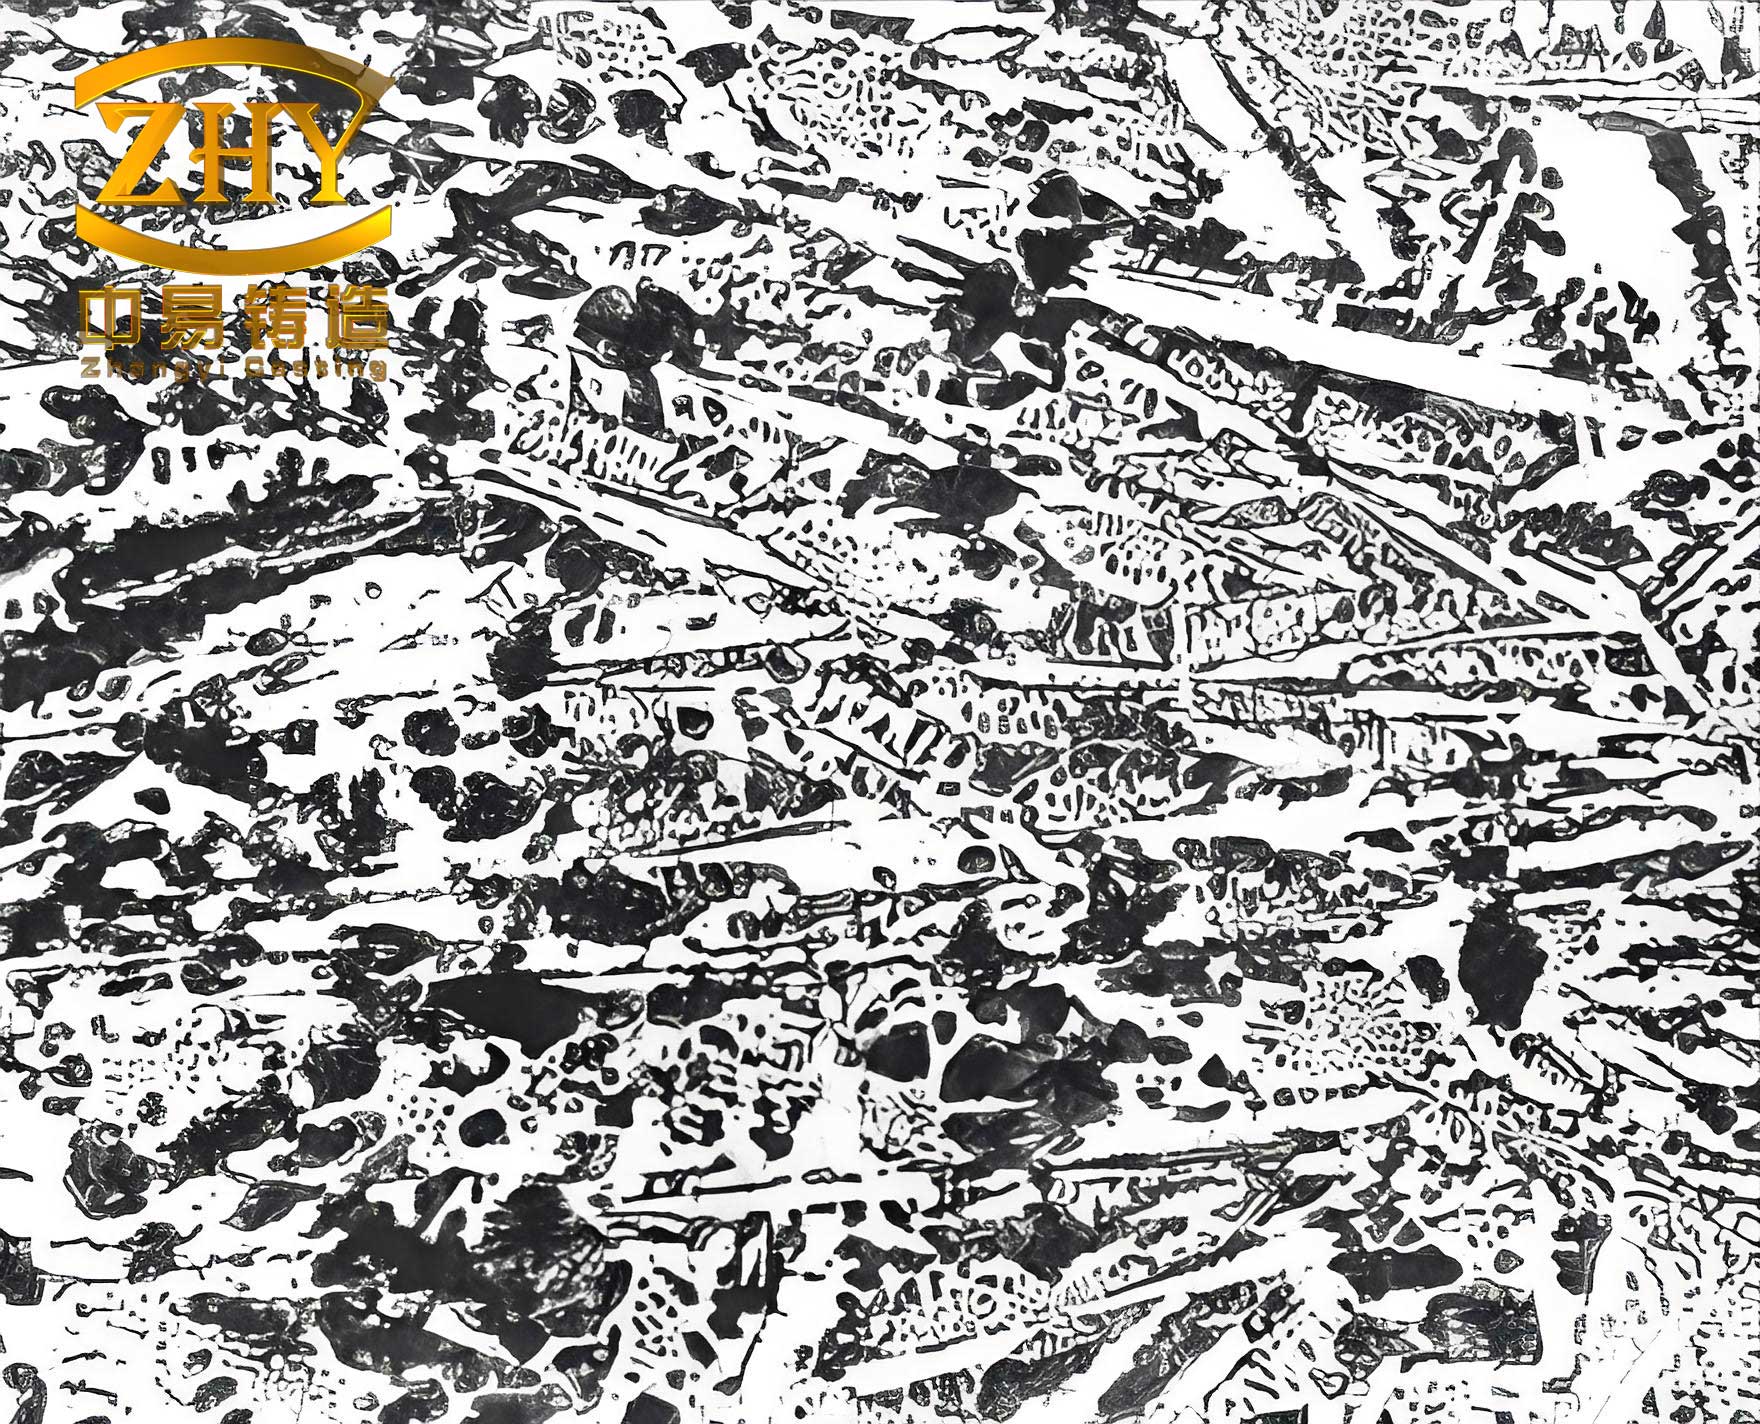
The material used for this research was a high-chromium white cast iron with a nominal composition designed to facilitate manganese substitution. The base chemistry was crucial, and I will refer to the alloy simply as the experimental high-chromium white cast iron throughout this article. The melting and casting were performed under controlled conditions to ensure a consistent carbide network and matrix structure characteristic of white cast iron. The as-cast microstructure typically consists of primary carbides (M7C3) embedded in a metastable austenitic or pearlitic matrix, depending on the cooling rate and composition.
The heat treatment strategy was predicated on the thermodynamic and kinetic principles governing phase transformations in white cast iron. The first stage, the pearlitic conditioning, aims to partially decompose the as-cast austenite into a pearlitic structure. This step creates a more favorable starting condition for the subsequent austenitization, potentially reducing the chemical and microstructural stability of the austenite phase. The second stage involves heating to an austenitizing temperature, holding for a sufficient time to achieve carbon and alloy element redistribution, followed by rapid quenching to transform the austenite into martensite. The challenge is that the high manganese content strongly suppresses the martensite start (Ms) temperature, leading to substantial retained austenite. The process can be conceptually modeled. The driving force for the austenite-to-martensite transformation is related to the undercooling below the Ms temperature. The Ms temperature itself is a function of composition:
$$ M_s (^{\circ}C) = 539 – 423C – 30.4Mn – 17.7Ni – 12.1Cr – 7.5Mo + 10Co – 7.5Si $$
where the element symbols represent their weight percentages. In our high-manganese white cast iron, the Mn term becomes significantly negative. The volume fraction of retained austenite (Vγ) after quenching can be empirically related to the Ms temperature and the quench rate, but a more practical approach for this study was to measure it directly via XRD using the integrated intensity of diffraction peaks from the martensite and austenite phases:
$$ V_{\gamma} = \frac{1}{1 + G \cdot \frac{I_{\alpha}}{I_{\gamma}}} $$
where Iα and Iγ are the integrated intensities of selected martensite and austenite peaks, respectively, and G is a calibration constant dependent on the specific diffraction planes and material.
To optimize the multi-variable heat treatment process, I designed an L9(34) orthogonal array. The four key factors investigated were: (A) Pearlitic conditioning temperature, (B) Pearlitic conditioning time, (C) Austenitizing temperature, and (D) Austenitizing time. Each factor was tested at three levels. The response variables were the retained austenite content (measured by XRD) and the Rockwell C hardness (HRC). The experimental matrix and the raw results are summarized in Table 1.
| Experiment No. | A: Pearlitic Temp. (°C) | B: Pearlitic Time (hr) | C: Austenitizing Temp. (°C) | D: Austenitizing Time (hr) | Retained Austenite (%) | Hardness (HRC) |
|---|---|---|---|---|---|---|
| 1 | 650 | 2 | 950 | 1 | 28.5 | 58.2 |
| 2 | 650 | 4 | 980 | 2 | 22.1 | 61.5 |
| 3 | 650 | 6 | 1010 | 3 | 18.7 | 63.8 |
| 4 | 700 | 2 | 980 | 3 | 15.3 | 65.0 |
| 5 | 700 | 4 | 1010 | 1 | 12.8 | 66.4 |
| 6 | 700 | 6 | 950 | 2 | 20.5 | 62.0 |
| 7 | 750 | 2 | 1010 | 2 | 10.5 | 67.8 |
| 8 | 750 | 4 | 950 | 3 | 25.0 | 59.5 |
| 9 | 750 | 6 | 980 | 1 | 17.2 | 64.1 |
The analysis of the orthogonal experiment involved calculating the mean response for each factor at each level (K1, K2, K3) and the range (R) to determine the significance and optimal level of each factor. The calculations for retained austenite content are shown in Table 2. The goal was to minimize retained austenite.
| Factor | Level 1 Mean (K1) | Level 2 Mean (K2) | Level 3 Mean (K3) | Range (R) | Optimal Level |
|---|---|---|---|---|---|
| A: Pearlitic Temp. | 23.10 | 16.20 | 17.57 | 6.90 | Level 2 (700°C) |
| B: Pearlitic Time | 18.10 | 19.97 | 18.80 | 1.87 | Level 1 (2 hr) |
| C: Austenitizing Temp. | 24.67 | 18.20 | 14.00 | 10.67 | Level 3 (1010°C) |
| D: Austenitizing Time | 19.50 | 17.70 | 19.67 | 1.97 | Level 2 (2 hr) |
From Table 2, the order of significance for minimizing retained austenite is: Austenitizing Temperature (C) > Pearlitic Conditioning Temperature (A) > Austenitizing Time (D) > Pearlitic Conditioning Time (B). The preliminary optimal combination for low retained austenite is A2, B1, C3, D2: Pearlitic conditioning at 700°C for 2 hours, followed by austenitization at 1010°C for 2 hours, then quenching. A similar analysis was performed for hardness (maximizing HRC), which yielded a consistent optimal factor level combination. Therefore, this set of parameters was identified as the best for this specific high-chromium white cast iron.
I then conducted a verification heat treatment run using these optimized parameters. The resulting microstructure was examined. The X-ray diffraction analysis confirmed a dramatic reduction in retained austenite. The calculated volume fraction was approximately 12%, a significant achievement for a high-manganese white cast iron. The hardness measured was 67.5 HRC, which is indeed comparable to the typical hardness range (66-68 HRC) reported for premium high-chromium-molybdenum white cast iron subjected to conventional high-temperature (e.g., 1050°C) heat treatment. This confirms that the developed two-stage process effectively mitigates the austenite-stabilizing effect of manganese.
The metallurgical rationale behind this success is multifaceted. The pearlitic conditioning at 700°C promotes the decomposition of austenite into ferrite and carbide. This reduces the overall carbon content in the matrix that will be re-austenitized. During the subsequent heating to 1010°C, the austenite that forms starts from a mixture of ferrite and carbides, leading to a potentially different and less homogeneous carbon distribution compared to direct austenitization from as-cast austenite. A lower average carbon content in the austenite at the quenching temperature raises the Ms temperature. We can approximate this effect. The carbon content in austenite (Cγ) at the austenitizing temperature is in equilibrium with the carbides. For high-chromium white cast iron, the solubility of carbon in austenite increases with temperature. At a lower austenitizing temperature (like our optimized 1010°C versus a typical 1050°C), the equilibrium carbon content in austenite is slightly lower. Combining this with the pre-conditioning that likely started with a lower-carbon matrix, the effective Cγ is reduced. Plugging a lower carbon value into the Ms formula increases Ms, facilitating more complete martensitic transformation upon quenching. The transformation kinetics can be described by the Koistinen-Marburger relationship for the volume fraction of martensite (fm) as a function of undercooling below Ms:
$$ f_m = 1 – \exp[-\alpha (M_s – T)] $$
where T is the temperature during quenching, and α is a material constant. A higher Ms leads to a larger value of (Ms – T) at room temperature, thus increasing fm and decreasing retained austenite. Furthermore, the conditioning treatment may also refine the austenite grain structure or alter the carbide morphology, providing more nucleation sites for martensite.
The implications for the broader category of white cast iron are substantial. This work demonstrates that strategic heat treatment design can overcome composition-driven limitations. For foundries and manufacturers, adopting such a process for manganese-alloyed high-chromium white cast iron could yield considerable cost savings without sacrificing key mechanical properties. It also suggests that lower austenitizing temperatures might be feasible for certain grades of white cast iron, reducing energy consumption and distortion.
To further generalize the findings, I propose a model correlating the process parameters to the final retained austenite content for this family of alloys. While empirical, it can serve as a guide. Let Vγ be the retained austenite fraction, Tp and tp the pearlitic conditioning temperature and time, and Ta and ta the austenitizing temperature and time. A multi-linear regression analysis on the data from Table 1 yields an approximate relationship (with normalized factors):
$$ V_{\gamma} (\%) \approx 35.2 – 0.08(T_p – 700) – 0.5(t_p – 4) – 0.12(T_a – 980) + 0.3(t_a – 2) $$
This equation highlights the strong negative coefficient for austenitizing temperature (Ta), meaning increasing Ta decreases Vγ, consistent with our analysis. The positive coefficient for austenitizing time (ta) suggests that excessive holding might allow carbon to fully homogenize, stabilizing austenite. The model underscores the non-linear, interactive effects that the orthogonal design helped to disentangle.
In conclusion, my research successfully identified an optimized two-stage heat treatment process for a high-manganese, high-chromium white cast iron. The combination of pearlitic conditioning at 700°C for 2 hours and austenitization at 1010°C for 2 hours, followed by quenching, resulted in a microstructure with only about 12% retained austenite and a hardness exceeding 67 HRC. This performance matches that of more expensive molybdenum-containing grades, validating the feasibility of a cost-effective manganese substitution strategy for high-chromium white cast iron. The study underscores the critical role of tailored thermal processing in unlocking the potential of alloyed white cast iron, providing a valuable framework for further development in this important class of wear-resistant materials.