
In the development of large diesel engines, bearing covers serve as critical components for fixing and supporting the crankshaft, enduring cyclic alternating loads during operation. Therefore, their quality requirements are extremely high. Recently, our company embarked on the development of a large bearing cover for a diesel engine, characterized by its substantial dimensions and thick sections. Initial casting process designs, based on past experience, led to defects such as shrinkage porosity and slag inclusion. This prompted a dedicated technical攻关, focusing on optimizing the casting process for ductile cast iron. This article details our approach, analysis, and solutions, emphasizing the use of advanced techniques to enhance the integrity and yield of ductile cast iron castings.
The material of choice for this component is ductile cast iron, specifically grade QT400-15, which offers a combination of high strength and good ductility. Ductile cast iron is renowned for its graphite nodular structure, imparting superior mechanical properties compared to gray iron. However, casting large sections in ductile cast iron presents unique challenges, primarily due to the risk of shrinkage porosity and slag inclusion during solidification. Our goal was to design a robust process that mitigates these defects while improving economic efficiency.
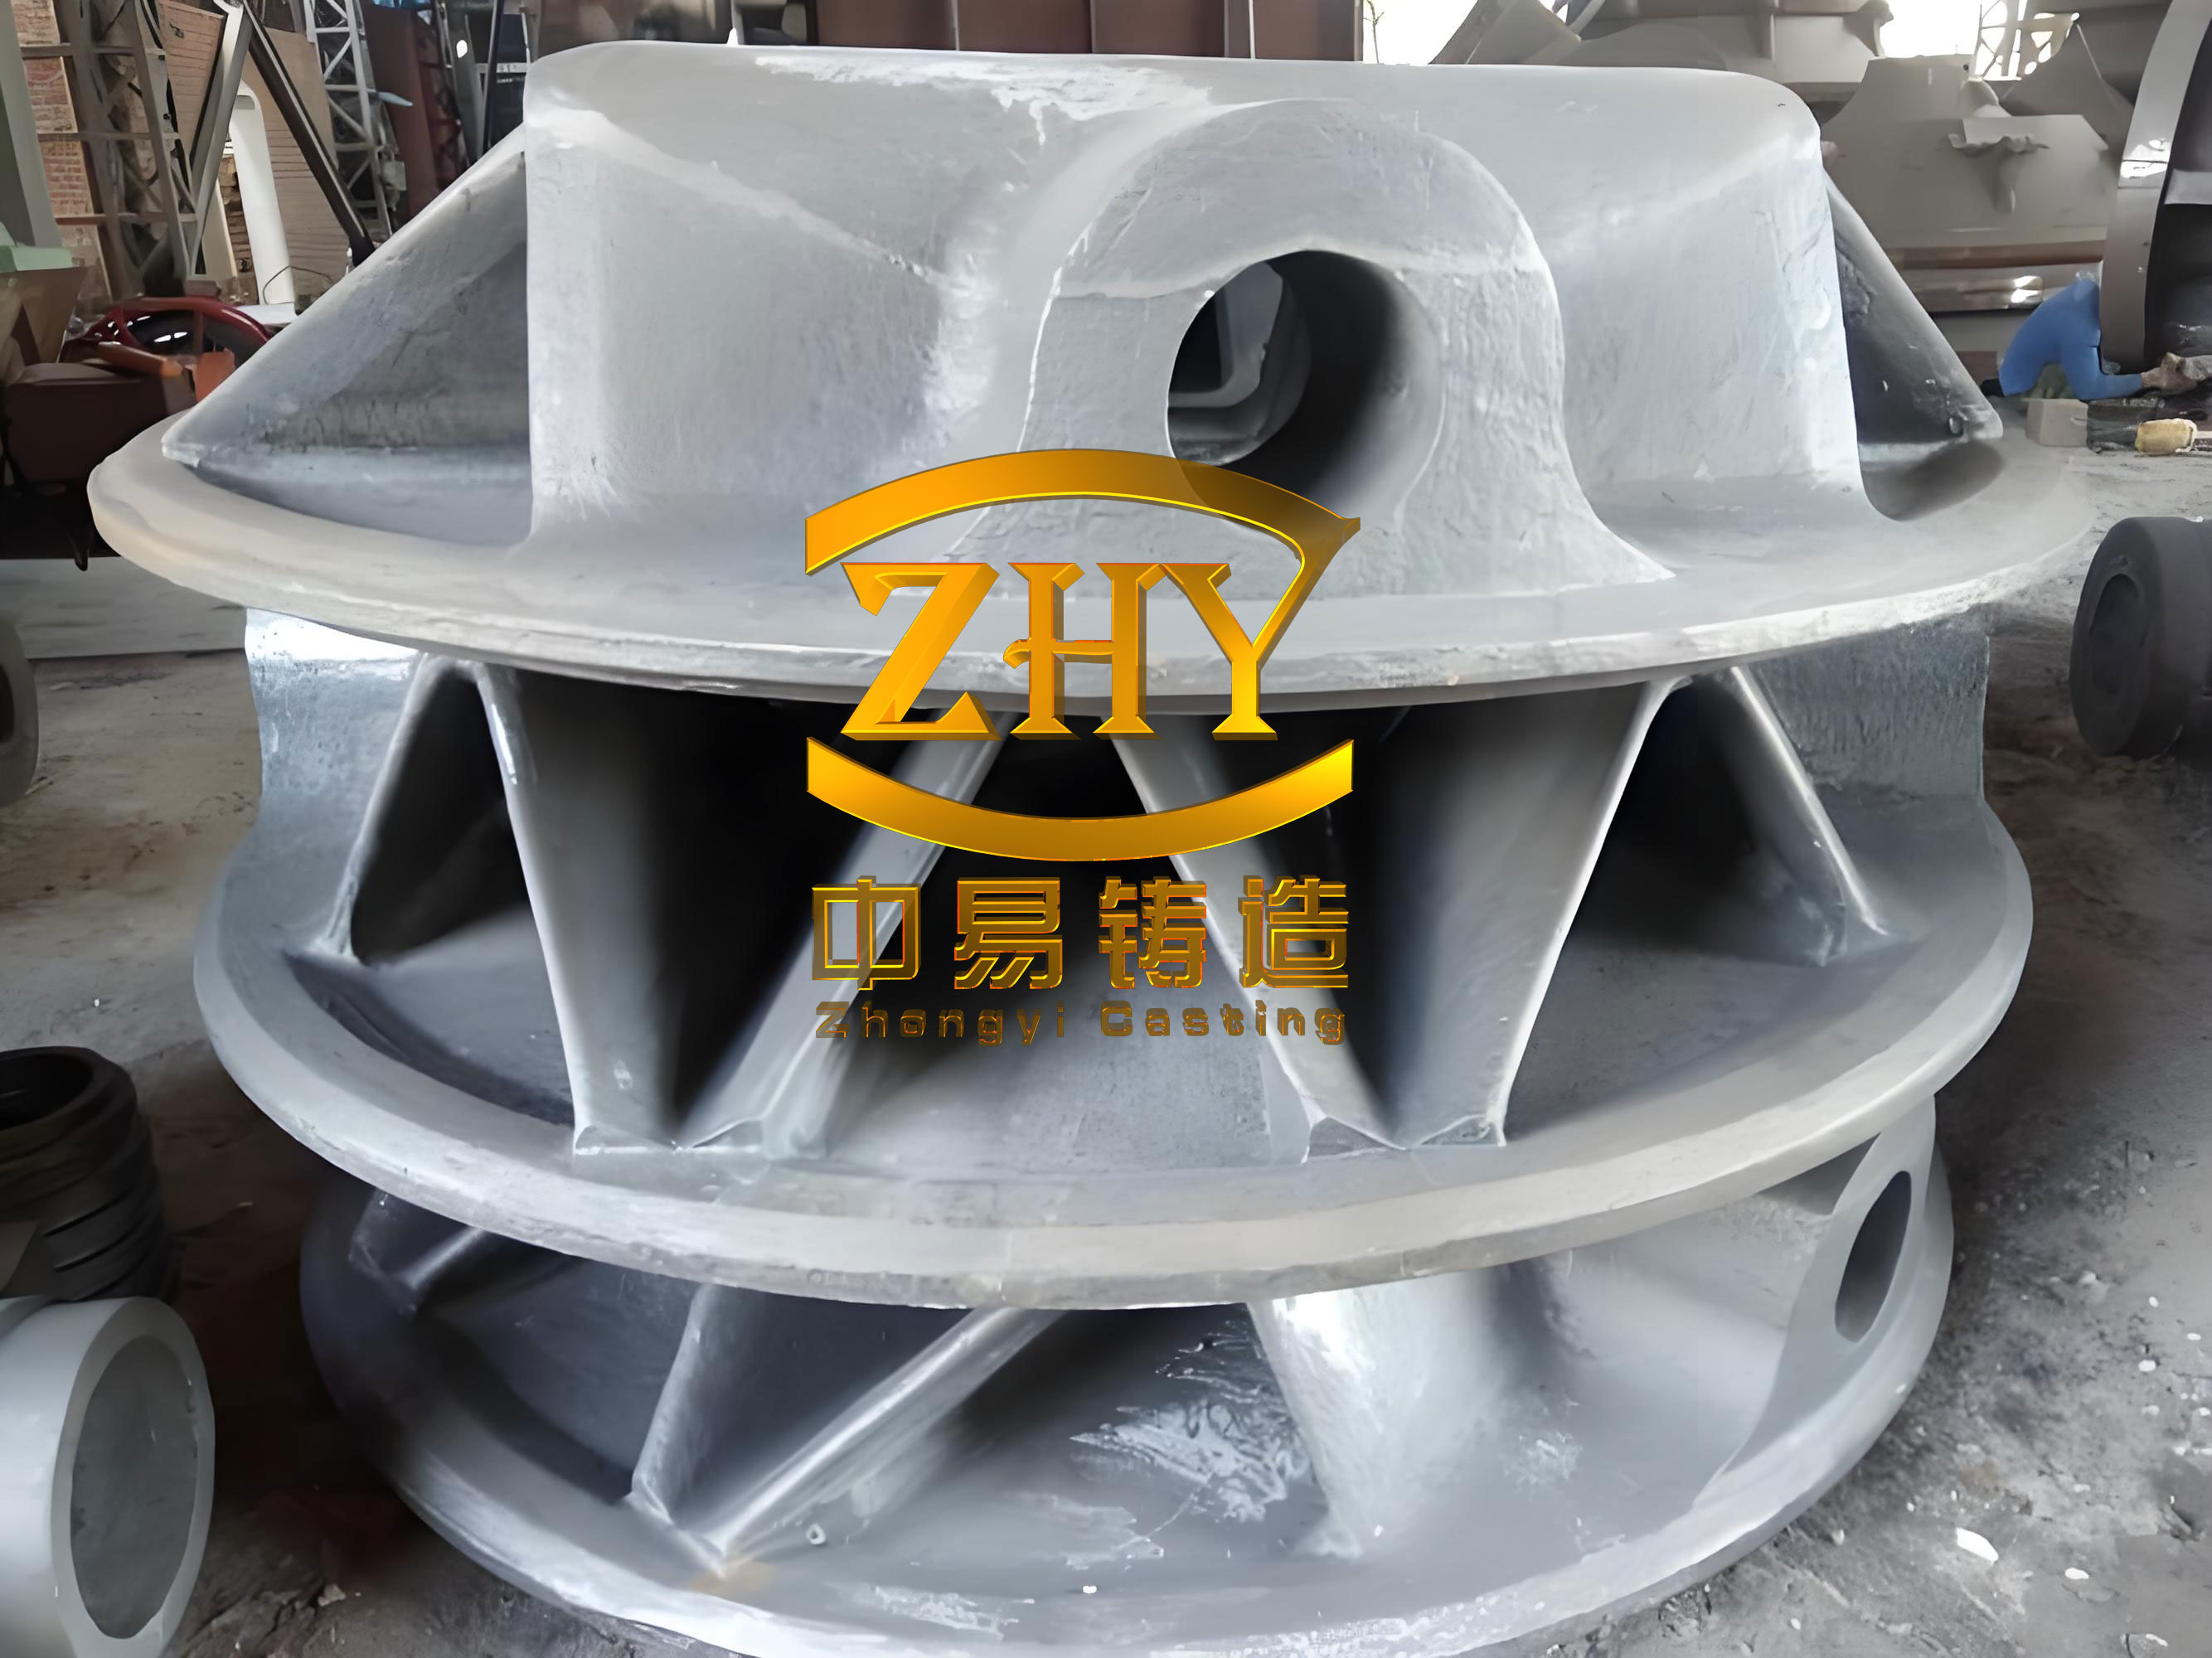
The original bearing cover had an outline dimension of 700 mm × 450 mm × 150 mm, with a rough casting weight of approximately 190 kg. The maximum thickness was 150 mm. Critical technical requirements included the absence of any defects within a 10 mm radius around the main bolt holes, which were to be machined post-casting. The initial process design employed traditional methods: insulation risers were placed above thick sections, with chills positioned underneath to promote directional solidification. Two ceramic foam filters were incorporated into the gating system to trap inclusions. While this setup reduced some risks, it failed to eliminate shrinkage porosity completely and resulted in a low casting yield of 56%. The inherent issue was the large thermal mass created by not casting the bolt holes, which acted as a significant heat source.
Upon inspection, defects were identified both on the surface and internally. Surface defects exhibited characteristics of slag inclusion, while internal dissection revealed dispersed porous structures near the bolt hole regions, indicative of shrinkage porosity. Energy-dispersive X-ray spectroscopy (EDS) analysis of the surface inclusions showed high concentrations of oxygen, silicon, calcium, and other elements, typical of slag formation. The root causes were twofold: firstly, the filtration system was inefficient due to the short distance between the sprue and the filters, and the vertical orientation of the filters limited their effectiveness during the initial pouring stage. Secondly, the decision not to cast the bolt holes created a massive thermal junction, exceeding the effective feeding range of the risers, despite the use of chills.
To address these issues, we formulated a comprehensive improved process design. The modifications centered on three areas: the gating and filtration system, the component geometry, and the cooling methodology. A fundamental understanding of ductile cast iron solidification behavior guided these changes. The solidification of ductile cast iron involves graphite expansion during the eutectic reaction, which can compensate for shrinkage if properly harnessed. The solidification time for a casting section can be estimated using Chvorinov’s rule:
$$ t = k \left( \frac{V}{A} \right)^n $$
where \( t \) is the solidification time, \( V \) is the volume of the section, \( A \) is its surface area, \( k \) is a mold constant, and \( n \) is an exponent typically close to 2. For thick sections, \( V/A \) is large, leading to longer solidification times and increased shrinkage risk. Our strategy was to reduce the effective \( V/A \) ratio at critical locations.
The first improvement was to the filtration system. We relocated the sprue to increase the length of the runner before the filters. More importantly, we changed the orientation of the ceramic foam filters from vertical to horizontal. This ensures that molten metal flows upward through the filter, enhancing the filtration mechanism through better cake formation and mechanical entrapment. The pressure drop across a filter can be described by the Darcy-Forchheimer equation for flow through porous media:
$$ \frac{\Delta P}{L} = \frac{\mu}{K} v + \beta \rho v^2 $$
where \( \Delta P \) is the pressure drop, \( L \) is the filter thickness, \( \mu \) is the dynamic viscosity, \( K \) is the permeability, \( v \) is the superficial velocity, \( \beta \) is the inertial coefficient, and \( \rho \) is the density. Horizontal placement promotes a more uniform flow distribution, improving inclusion capture efficiency early in the pour.
The second major change was to cast the bolt holes instead of machining them from solid. This drastically reduces the volume of the thermal junction. To support the sand cores forming these holes, steel core reinforcements were embedded to prevent breakage or deformation. The reduction in thermal mass is significant. Consider the volume of a cylindrical bolt hole region. If the hole diameter is \( d \) and the depth is \( h \), the removed volume is \( V_{hole} = \pi (d/2)^2 h \). This volume no longer contributes to the heat of fusion that must be dissipated, thereby shortening the local solidification time.
The third improvement involved optimizing the cooling system. We replaced the risers over the thick sections with conformal chills that closely match the contour of the thermal junctions. Chills extract heat rapidly, increasing the cooling rate \( R \) and temperature gradient \( G \). The Niyama criterion, often used to predict shrinkage porosity in castings, is given by:
$$ N_y = \frac{G}{\sqrt{R}} $$
A higher \( G \) and \( R \) lead to a larger \( N_y \) value, indicating a lower propensity for shrinkage. By applying chills directly to the hot spots, we aimed to increase both parameters. Additionally, we adjusted the chemical composition of the ductile cast iron within the specification of QT400-15 to favor a higher graphitization potential, enhancing the internal feeding pressure from graphite expansion. The equilibrium solidification theory for ductile cast iron suggests that proper use of chills can control the solidification sequence, allowing the graphite expansion to compensate for shrinkage effectively.
| Parameter | Original Process | Improved Process |
|---|---|---|
| Bolt Hole Formation | Machined from solid | Casted with sand cores |
| Filter Orientation | Vertical | Horizontal |
| Cooling for Thick Sections | Riser + Chill | Conformal Chill only |
| Runner Length before Filter | Short | Extended |
| Estimated Thermal Junction Volume | Large (Full section) | Reduced (Cored section) |
| Casting Yield | 56% | 82% |
To validate the improved design, we employed MAGMA simulation software. The filling simulation showed a stable mold filling pattern with reduced turbulence. The solidification and shrinkage analysis indicated a significant decrease in the risk of shrinkage porosity, with critical areas now showing a Niyama value above the threshold for soundness. The simulation results confirmed that the porosity-prone zones were shifted away from the critical bolt hole regions, with a minimum distance exceeding 76 mm.
Physical verification was conducted on prototype castings. Visual inspection revealed no surface slag inclusions. Destructive testing involving sectioning of the castings confirmed that any residual shrinkage porosity was located at a safe distance from the bolt holes, well beyond the 10 mm requirement. A small batch of 20 castings was produced using the new process, and all were found to be free from the aforementioned defects. The casting yield improved dramatically from 56% to 82%, representing a substantial cost saving.
The success of this project underscores several key principles in the casting of large ductile iron components. Firstly, the design of the gating and filtration system is paramount for cleanliness. A horizontal filter placement with adequate runner length significantly enhances slag removal efficiency. Secondly, for thick-section ductile cast iron parts, reducing the thermal mass through strategic use of cores is more effective than relying solely on risers for feeding. This aligns with the concept of “thermal modulation” to control solidification. Thirdly, the application of conformal chills provides a targeted and efficient method to increase cooling rates and temperature gradients, working in synergy with the inherent graphite expansion of ductile cast iron.
| Element | Composition (wt.%) | Role in Solidification |
|---|---|---|
| Carbon (C) | 3.6 – 3.9 | Graphite formation, fluidity |
| Silicon (Si) | 2.4 – 2.8 | Graphitizer, strengthens ferrite |
| Manganese (Mn) | < 0.3 | Minimized to prevent segregation |
| Phosphorus (P) | < 0.05 | Minimized to avoid brittleness |
| Sulfur (S) | < 0.02 | Minimized before nodularization |
| Magnesium (Mg) | 0.03 – 0.05 | Nodularizing agent |
| Cerium (Ce) / Lanthanum (La) | Trace | Nodularizing aids |
The graphite expansion pressure during eutectic solidification of ductile cast iron can be modeled as an internal pressure source. If \( V_g \) is the volume increase due to graphite precipitation and \( \beta \) is the compressibility of the mushy zone, the pressure generated \( P_{graphite} \) can be related to the volumetric change. Effective use of chills helps to create a rigid mold wall early, containing this pressure to counteract shrinkage. The combined effect of chilling and graphite expansion can be conceptualized through a modified feeding criterion:
$$ F = \frac{P_{graphite} + P_{metallostatic}}{P_{shrinkage}} $$
where \( F > 1 \) indicates sound casting. Our process optimizations aimed to maximize \( P_{graphite} \) through composition control and ensure it is effectively utilized by solidifying the skin rapidly with chills.
In conclusion, the development of a reliable casting process for large ductile iron bearing covers requires a holistic approach. By integrating filtration system redesign, component geometry optimization via coring, and targeted cooling with conformal chills, we successfully eliminated shrinkage porosity and slag inclusion defects. The material behavior of ductile cast iron was leveraged to its advantage. This case study demonstrates that for heavy-section ductile cast iron castings, a shift from traditional riser-based feeding to a controlled solidification approach with chills and optimized geometry yields superior quality and higher productivity. Future work may involve further refining the chill design using simulation tools and exploring advanced filter materials to achieve even cleaner ductile cast iron melts.
The principles established here are applicable to a wide range of thick-section ductile cast iron components. The key is to manage the solidification dynamics by controlling heat extraction and minimizing isolated thermal masses. Ductile cast iron, with its unique solidification characteristics, responds well to such engineered cooling strategies. Continuous improvement in the casting of ductile cast iron parts remains a vital endeavor for enhancing the performance and reliability of critical machinery components.