
In my years of foundry practice, I have devoted significant effort to understanding and mitigating sand casting defects in light green sand mold iron castings. The workshop where I work produces small machine tool components such as tailstock bodies, bearing supports, carriage boxes, and gearboxes using green sand molding with clay-bonded silica sand. The green sand process offers many advantages: low material cost, sharp mold contours, minimal pattern draft, low tooling wear, rapid mold production, no drying required, short production cycles, easy shakeout, and good sand reclamation with low ash content. However, the inherent limitations of green sand—relatively low strength, high moisture content, and high gas evolution—make the castings prone to several typical sand casting defects: blowholes (gas porosity), sand inclusions, scabs, and metal penetration (burn-on). Over time, I have systematically analyzed each defect category and implemented effective countermeasures. This article summarizes my practical experience, supported by quantitative data, tables, and mathematical relationships, to help other foundry engineers reduce rejection rates and improve casting quality.
1. Classification and Root Causes of Sand Casting Defects
From production statistics, the overall rejection rate for small green sand castings in my facility once exceeded 10%, causing substantial economic loss. Among the defective castings, the major sand casting defects were:
- Blowholes (gas porosity)
- Sand inclusions
- Scabs (expansion defects)
- Metal penetration (burn-on)
Each defect type originates from specific combinations of sand properties, molding practice, metal composition, and pouring conditions. The following table summarizes the primary causes identified in my investigation:
| Defect Type | Primary Causes | Contributing Factors |
|---|---|---|
| Blowholes (Gas Porosity) | Moisture in green sand; high volatile content; poor mold venting; excessive mold hardness; high gas content in molten metal; improper gating system | Water content >4.5%; coal dust >0.5%; permeability below 55; pouring temperature too low; damp charge materials |
| Sand Inclusions | Low sand strength; friable mold edges; inadequate ramming; careless core setting or mold closing; excessive fines or ash | Green compressive strength <0.08 MPa; toughness insufficient; mold surface damaged during assembly |
| Scabs (Expansion Defects) | Thermal expansion of sand surface layer; low hot-wet tensile strength; non-uniform ramming; absence of mold reinforcement | Low thermal conductivity of sand; calcium bentonite not activated; lack of nails or chaplets; high thermal gradient |
| Metal Penetration (Burn-on) | Coarse sand grains; low sand refractoriness; high pouring temperature; open mold pores; lack of anti-penetration additives | AFS grain fineness <50; clay content too low; no coal dust or lustrous carbon additive; no mold coating |
2. Detailed Mechanism of Each Sand Casting Defect
2.1 Blowholes (Gas Porosity)
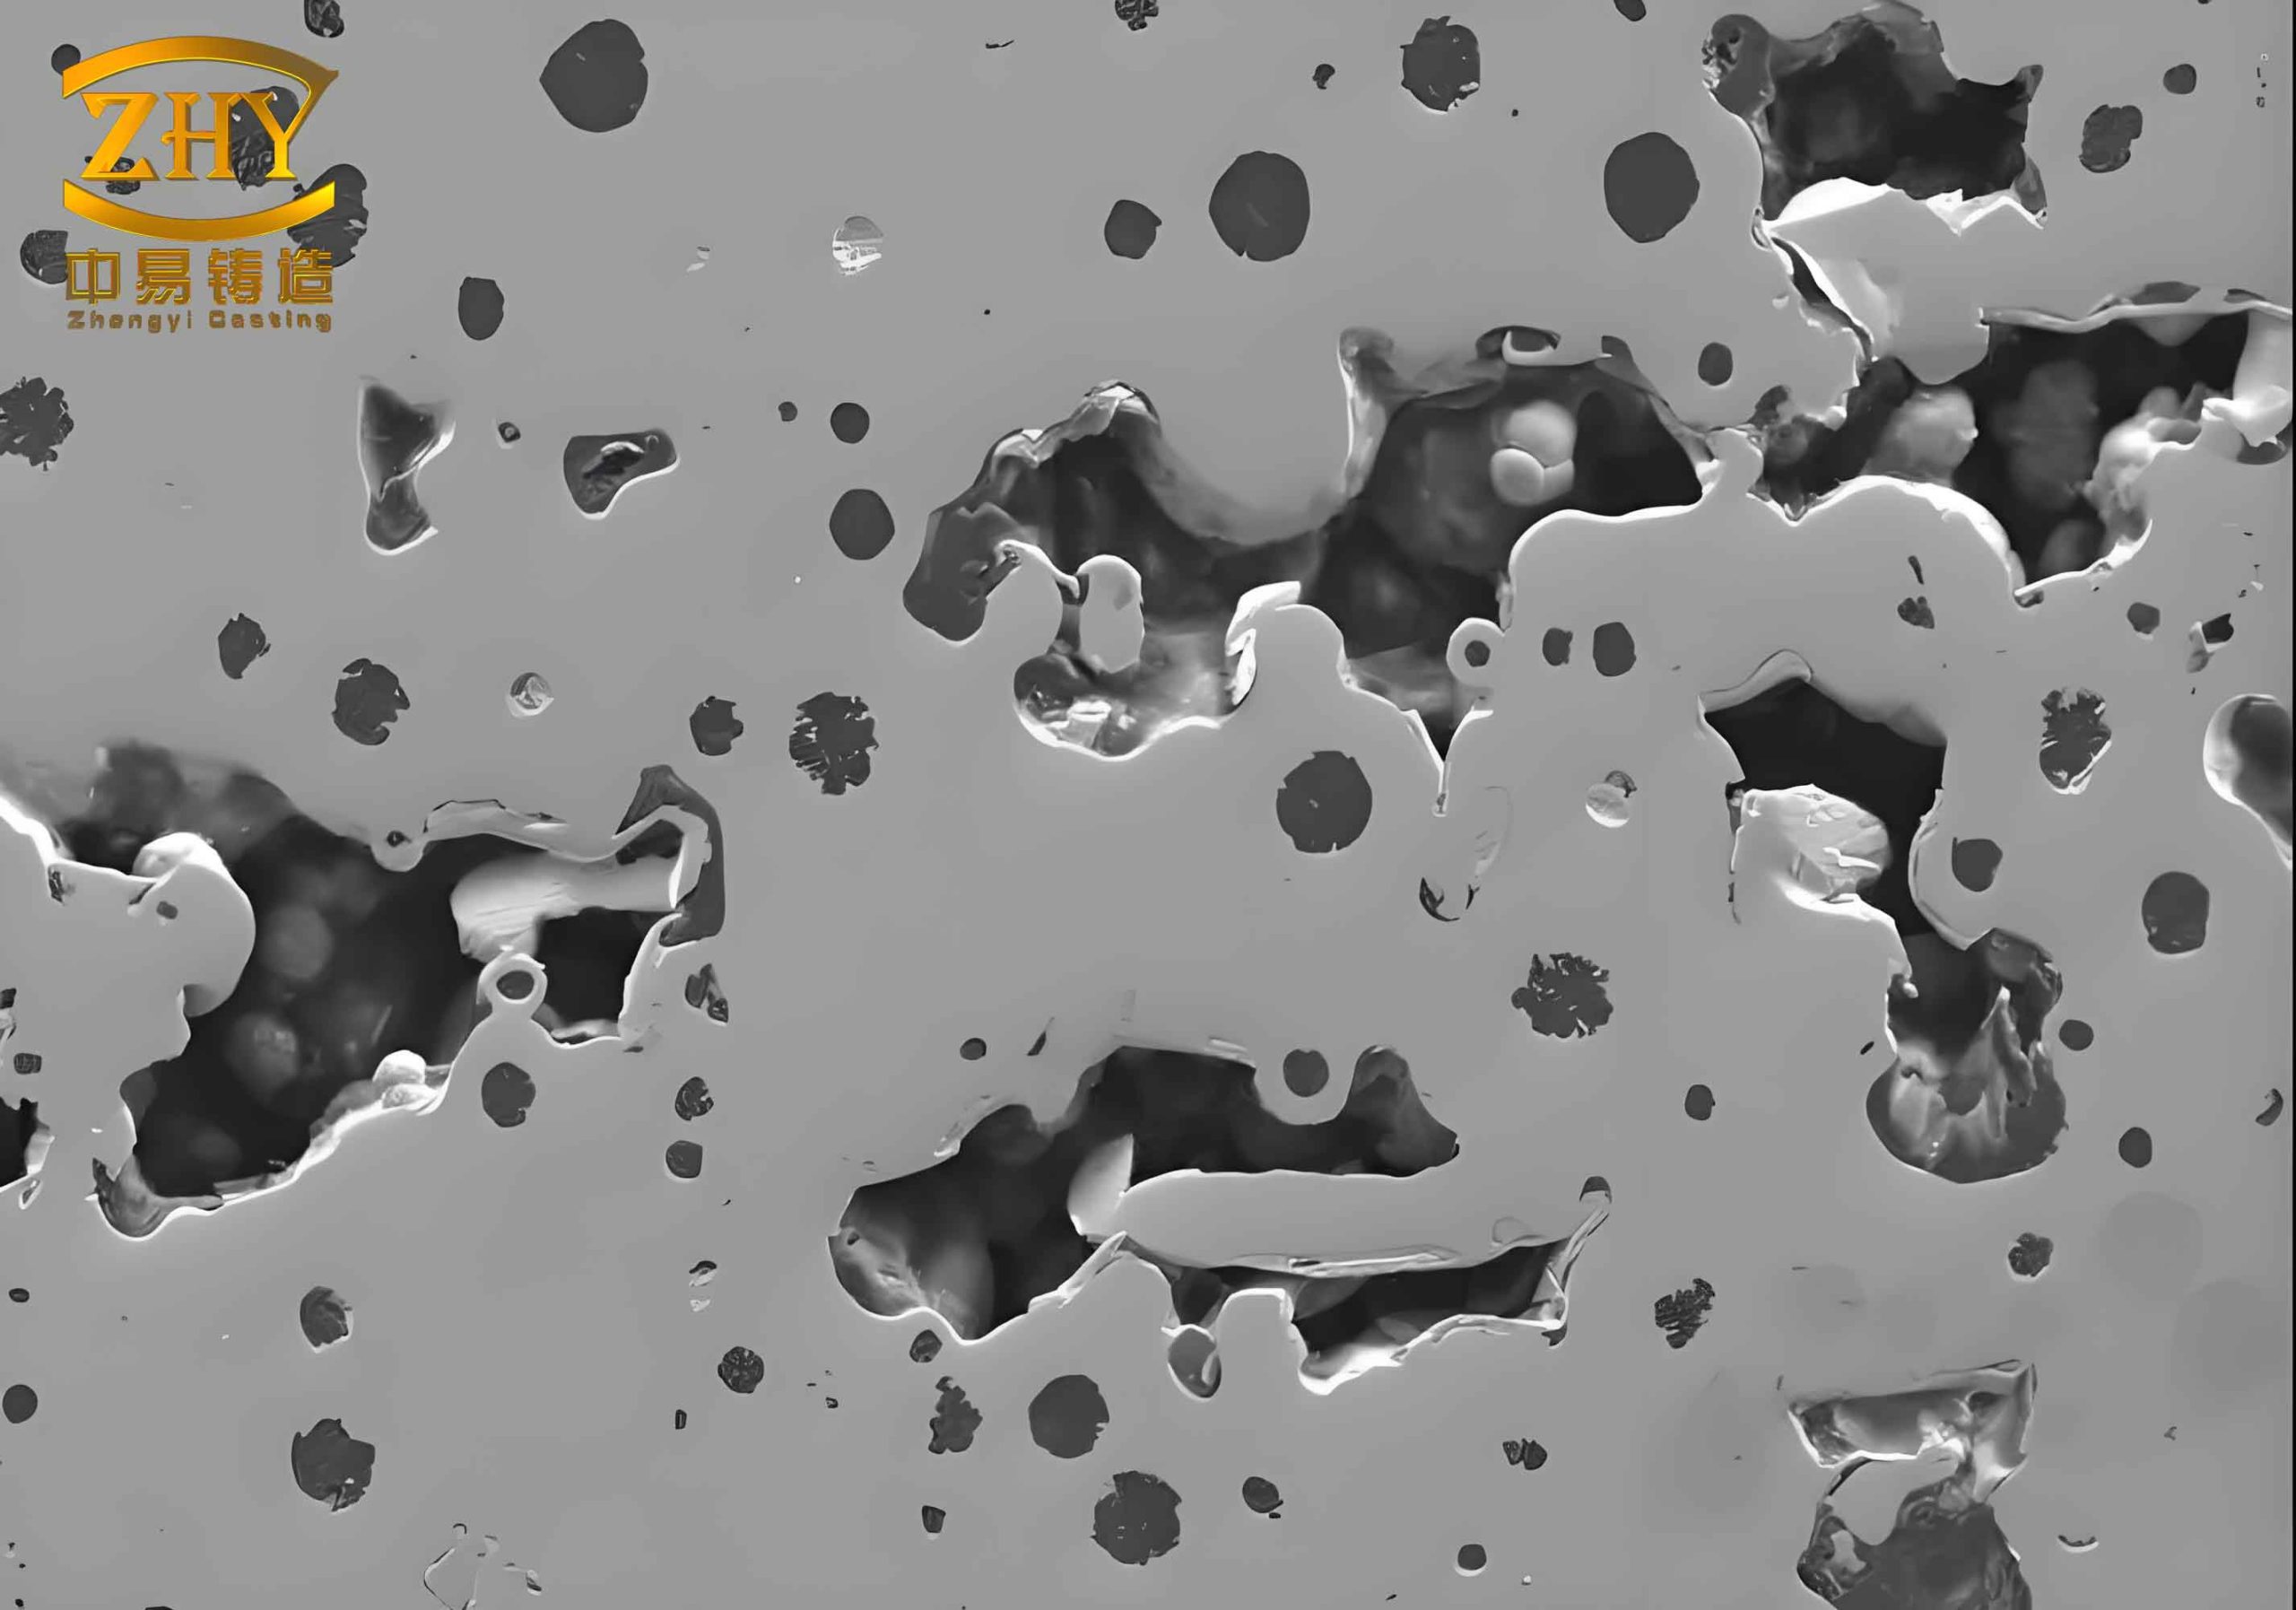
Blowholes are the most frequent sand casting defects in green sand molding. In my observation, they account for about 40% of all rejections. The root cause is the evolution of gas from moisture, coal dust, and other volatiles in the sand when contacted by molten iron. The gas expands rapidly and, if not vented, becomes trapped in the solidifying metal. Three types of gas sources exist:
- Mold gas: Water vapor from the sand; decomposition of coal dust (hydrocarbons, CO, CO₂); gas from core binders.
- Metal gas: Dissolved hydrogen or oxygen in the melt; reduction of oxides; gas released during solidification.
- Entrained gas: Air trapped in the mold cavity due to turbulent filling or poor gating design.
The volume of gas generated from sand moisture can be estimated by:
$$ V_{\text{gas}} = \frac{m_{\text{water}} \cdot R \cdot T}{M_{\text{water}} \cdot P} $$
where \( m_{\text{water}} \) is the mass of water in the sand layer adjacent to the casting, \( R \) is the universal gas constant, \( T \) the temperature (in Kelvin), \( M_{\text{water}} \) the molar mass of water, and \( P \) the pressure. For a typical small casting with a surface area of 0.1 m² and a sand layer thickness of 5 mm containing 3.5% moisture, the gas volume at 1000°C can exceed 0.5 liters—enough to cause multiple blowholes if not vented.
In practice, I have found that controlling sand moisture to 3.0–4.0% (as per the table below) is the most critical parameter. Permeability must be kept between 55 and 80 to allow gas escape. Mold hardness should not exceed 80–85 units to avoid sealing the pore network. Additionally, venting holes (pricks) are made on the cope surface, and risers are placed at high points to collect gas.
2.2 Sand Inclusions
Sand inclusions are another common sand casting defect, caused by loose sand grains or small lumps that break off from the mold or core surface and become embedded in the casting. In my shop, this defect was often traced to poor mold handling—excessive ramming on one side leading to non-uniform density, or careless core setting that abrades the mold cavity. The required sand properties to resist erosion and spalling include adequate green compressive strength and good toughness (deformation before fracture). The following empirical relationship links the critical sand strength to the metallostatic pressure:
$$ \sigma_{\text{crit}} = \frac{\rho_{\text{metal}} \cdot g \cdot h_{\text{head}}}{k} $$
where \( \rho_{\text{metal}} \) is the density of liquid iron (~7000 kg/m³), \( g \) is gravity (9.81 m/s²), \( h_{\text{head}} \) is the metal head height (typically 0.2–0.5 m for small castings), and \( k \) is a safety factor (~0.5 for green sand). For a 0.3 m head, the required green compressive strength is about 0.09 MPa. In our practice, we maintain a green compressive strength of 0.08–0.12 MPa.
I also found that a high content of fines (ash) reduces sand toughness and increases friability. Therefore, the reclaimed sand must be screened, and the total fines should be kept below 12%.
2.3 Scabs (Expansion Defects)
Scabs are typical sand casting defects for green sand molds, especially when casting flat surfaces. The mechanism involves rapid heating of the sand surface layer, which expands and buckles away from the backing sand. The gap thus formed fills with metal, creating a scab. The expansion strain of the sand layer can be approximated by:
$$ \varepsilon = \alpha \cdot \Delta T $$
where \( \alpha \) is the linear thermal expansion coefficient of silica sand (~18 × 10⁻⁶ /°C) and \( \Delta T \) is the temperature rise (e.g., from 20°C to 800°C, so 780°C). This gives an expansion of about 1.4%, which, if restrained, can generate compressive stresses high enough to cause buckling.
To prevent scabs, I have applied the following countermeasures:
- Use sodium-activated bentonite (Na-bentonite) instead of calcium bentonite to improve hot-wet tensile strength. The activation reaction is:
$$ \text{Ca-Bentonite} + \text{Na}_2\text{CO}_3 \rightarrow \text{Na-Bentonite} + \text{CaCO}_3 $$
Na-bentonite has a higher swelling capacity and better high-temperature bond.
- Reduce thermal gradient by using sand with higher thermal conductivity (e.g., adding fine graphite or iron oxide).
- Insert steel nails or chaplets in the cope surface, flush with the mold cavity, to anchor the sand layer.
- Ensure uniform ramming and avoid excessive hardness in localized areas.
2.4 Metal Penetration (Burn-on)
Metal penetration occurs when molten iron infiltrates the interstices between sand grains, forming a mechanically interlocked layer that is difficult to remove. The critical condition for penetration is given by the capillary pressure equation:
$$ \Delta P = \frac{2 \gamma \cos \theta}{r} $$
where \( \gamma \) is the surface tension of liquid iron (~1.8 N/m), \( \theta \) is the contact angle (for clean silica, ~110°, so cosθ negative, meaning non-wetting), and \( r \) is the effective pore radius. Penetration occurs if the metallostatic pressure exceeds the capillary pressure. For a given head, smaller pores (finer sand) increase capillary resistance. However, if the sand is too fine, permeability drops and gas defects increase. Hence, a balance must be struck.
In my practice, I use a base sand with AFS grain fineness number (GFN) of 55–70. The addition of 0.2–0.4% coal dust (with >30% volatiles) creates a reducing atmosphere and deposits a lustrous carbon film on sand grains, which reduces iron wetting and fills pores. The carbon film can be represented by the decomposition:
$$ \text{C}_x\text{H}_y \rightarrow x\text{C} + y/2 \text{H}_2 $$
Further, applying a thin zircon or graphite coating on the mold surface is very effective. We introduced a spray coating of alcohol-based graphite that reduced burn-on defects by 60%.
3. Preventive Measures and Process Optimization
Based on the above analysis, I established a comprehensive set of control parameters for sand preparation, molding, melting, and pouring. The following table lists the key parameters and their target ranges:
| Process Step | Parameter | Target Value / Range | Purpose |
|---|---|---|---|
| Sand Preparation | Base sand grain size distribution | 50/100, 70/140, 100/200 (AFS GFN 55–70) | Balance permeability and surface finish |
| Clay content (Na-bentonite) | 0.6%–0.9% (of total sand weight) | Adequate green strength and hot-wet tensile strength | |
| Coal dust content | 0.2%–0.4% (ratio clay:coal ≈ 1:2.5–3.0) | Reduce metal penetration and produce lustrous carbon | |
| Moisture content | 3.0%–4.0% | Control gas evolution; maintain workability | |
| Molding | Mold hardness (B-scale) | 75–85 | Adequate strength without blocking permeability |
| Permeability (AFS standard) | 55–80 | Allow gas escape | |
| Venting: risers, pricks | Riser at high points; pricks 10–15 per 100 cm² | Prevent gas entrapment | |
| Melting & Pouring | Pouring temperature | 1330–1380°C | Low temperature reduces gas absorption and penetration |
| Charge materials | Clean, dry, rust-free; preheated if needed | Reduce hydrogen pickup |
3.1 Sand Mixing Procedure
The sequence and duration of sand mixing are critical for uniform distribution of binder and additives. I adopted the following procedure in a batch muller:
- Add 90–95% reclaimed sand + 5–10% new sand.
- Add water (about 60% of total required) and mull for 5–10 seconds.
- Add coal dust and bentonite (premixed) and continue mulling for 90–120 seconds.
- Add the remaining water to adjust final moisture and mull for another 5–10 seconds.
- Discharge sand; total mulling time: 2–3 minutes.
- Aerate and temper for 2–3 hours before use to ensure moisture equilibration.
The green sand properties are checked every hour. The following primary relationships govern the sand behavior:
Green compressive strength (MPa) as a function of bentonite content \( B \) (%) and moisture \( M \) (%):
$$ \sigma_{\text{green}} \approx 0.02 + 0.12B – 0.015M \quad (\text{R}^2 \approx 0.85) $$
Permeability as a function of fines content \( F \) (%) and moisture:
$$ P \approx 120 – 10F – 15M \quad (\text{for AFS GFN 60}) $$
These equations help me adjust the mix quickly when deviations occur.
3.2 Molding and Core Setting
I use ZA148 jolt-squeeze molding machines. The jolt cycle is set to achieve uniform mold hardness across the parting surface. After stripping, the mold is inspected, and any loose sand is blown away with compressed air. Cores are made from oil-sand or shell sand, cured before use. Core prints are designed with adequate clearance to avoid crushing the mold. During closing, the cope is lowered gently, and alignment pins ensure centering.
3.3 Gating System Design
The gating system is designed to promote smooth, non-turbulent filling. For small castings (mass 5–50 kg), I use the following empirical gating ratios based on choke area:
$$ A_{\text{sprue}} : A_{\text{runner}} : A_{\text{gate}} = 1 : 1.2 : 1.5 $$
The choke area \( A_c \) is calculated from the desired pouring time \( t \) (seconds):
$$ A_c = \frac{m_{\text{casting}}}{\rho_{\text{metal}} \cdot C_d \cdot \sqrt{2g h_{\text{effective}}} \cdot t} $$
where \( C_d \) is the discharge coefficient (0.75–0.85) and \( h_{\text{effective}} \) is the effective metal head. For a 10 kg casting poured in 8 seconds with a 0.3 m head, the choke area is about 1.2 cm². Multiple ingates are used to distribute metal evenly and avoid erosion of the mold.
3.4 Melting and Pouring
I melt gray iron (grade HT200) in a cupola or electric induction furnace. The charge consists of clean pig iron, steel scrap, and returns. All materials are preheated to remove moisture and oil. After melting, the iron is deslagged and held at 1400–1420°C for a few minutes to allow degassing. Then the temperature is lowered to the pouring range (1330–1380°C) by adding cool returns. Lower pouring temperature reduces the tendency for gas absorption and metal penetration, but must remain high enough to ensure filling of thin sections. The pouring ladle is dried and preheated. The pouring stream is kept short and continuous to minimize oxidation and air entrapment.
4. Results and Quantitative Improvements
After implementing these measures over six months, I recorded a significant reduction in all major sand casting defects. The data from 200 consecutive production lots (each lot ~100 castings) are summarized below:
| Defect Type | Before Implementation (%) | After Implementation (%) | Reduction (%) |
|---|---|---|---|
| Blowholes | 4.2 | 1.8 | 57% |
| Sand inclusions | 3.0 | 0.9 | 70% |
| Scabs | 2.5 | 0.6 | 76% |
| Metal penetration | 1.8 | 0.5 | 72% |
| Total rejection rate | 11.5% | 3.8% | 67% |
The best monthly rejection rate reached 3.0%, which is economically viable for small machine tool castings. The key success factors were:
- Strict control of sand moisture within 3.0–4.0%.
- Use of Na-activated bentonite with proper coal dust ratio.
- Optimized ramming and venting.
- Reduced pouring temperature (1330–1380°C).
- Improved cleaning and handling of molds.
5. Conclusion
Green sand molding remains a cost-effective method for producing small iron castings, but the prevalence of sand casting defects such as blowholes, sand inclusions, scabs, and metal penetration can degrade quality and increase costs. Through systematic analysis of defect mechanisms and rigorous process control—covering raw materials, sand mixing, molding practice, gating design, melting, and pouring—I have successfully reduced the rejection rate from over 10% to below 4%. The use of quantitative relationships, such as permeability models, strength equations, and capillary pressure analysis, provided a scientific basis for decision-making. The tables and formulas presented in this article serve as practical guides for foundry engineers seeking to minimize sand casting defects in green sand production. Continuous monitoring and adjustment of key parameters are essential to maintain high-quality output.
By sharing my experience and data, I hope to assist other foundry professionals in tackling the persistent challenge of sand casting defects and achieving both higher yields and better customer satisfaction.