
In foundry engineering, the production of high-quality ductile iron castings demands a comprehensive understanding of melting metallurgy, nodularizing treatment, mold filling, and solidification control. Among all discontinuities that can be detected in ductile iron castings, slag inclusions are particularly dangerous because they not only spoil the machined surface but also reduce load-carrying cross-sections and create stress concentration sites. In my experience, slag-related defects are among the most common causes of rejection in heavy-section ductile iron castings. The defect is often described as black slag or black spot because it appears as dark, irregular patches on fracture surfaces, machined faces, or the natural casting surface. In many industrial cases, the failure was so severe that a substantial portion of a production batch had to be scrapped. I have personally observed scrap rates caused by slag inclusions in ductile iron castings exceeding 10%, which is completely unacceptable for a modern foundry.
The origin of slag inclusions in ductile iron castings is closely related to the chemical reactivity of liquid cast iron after nodularizing treatment. The spheroidizing agent usually contains magnesium, and the inoculant may contain rare-earth elements. These elements have a high affinity for oxygen and sulfur. As a result, molten ductile iron can form oxides and sulfides very easily at the surface. When the metal is transferred from the ladle to the pouring cup and then through the gating system, fresh metal surfaces are continuously exposed to air. If the flow is turbulent, the oxidized surface film is broken and folded into the interior of the liquid metal. These entrained films and particles then remain in the casting after solidification. Therefore, the gating system has a decisive influence on the soundness of ductile iron castings.
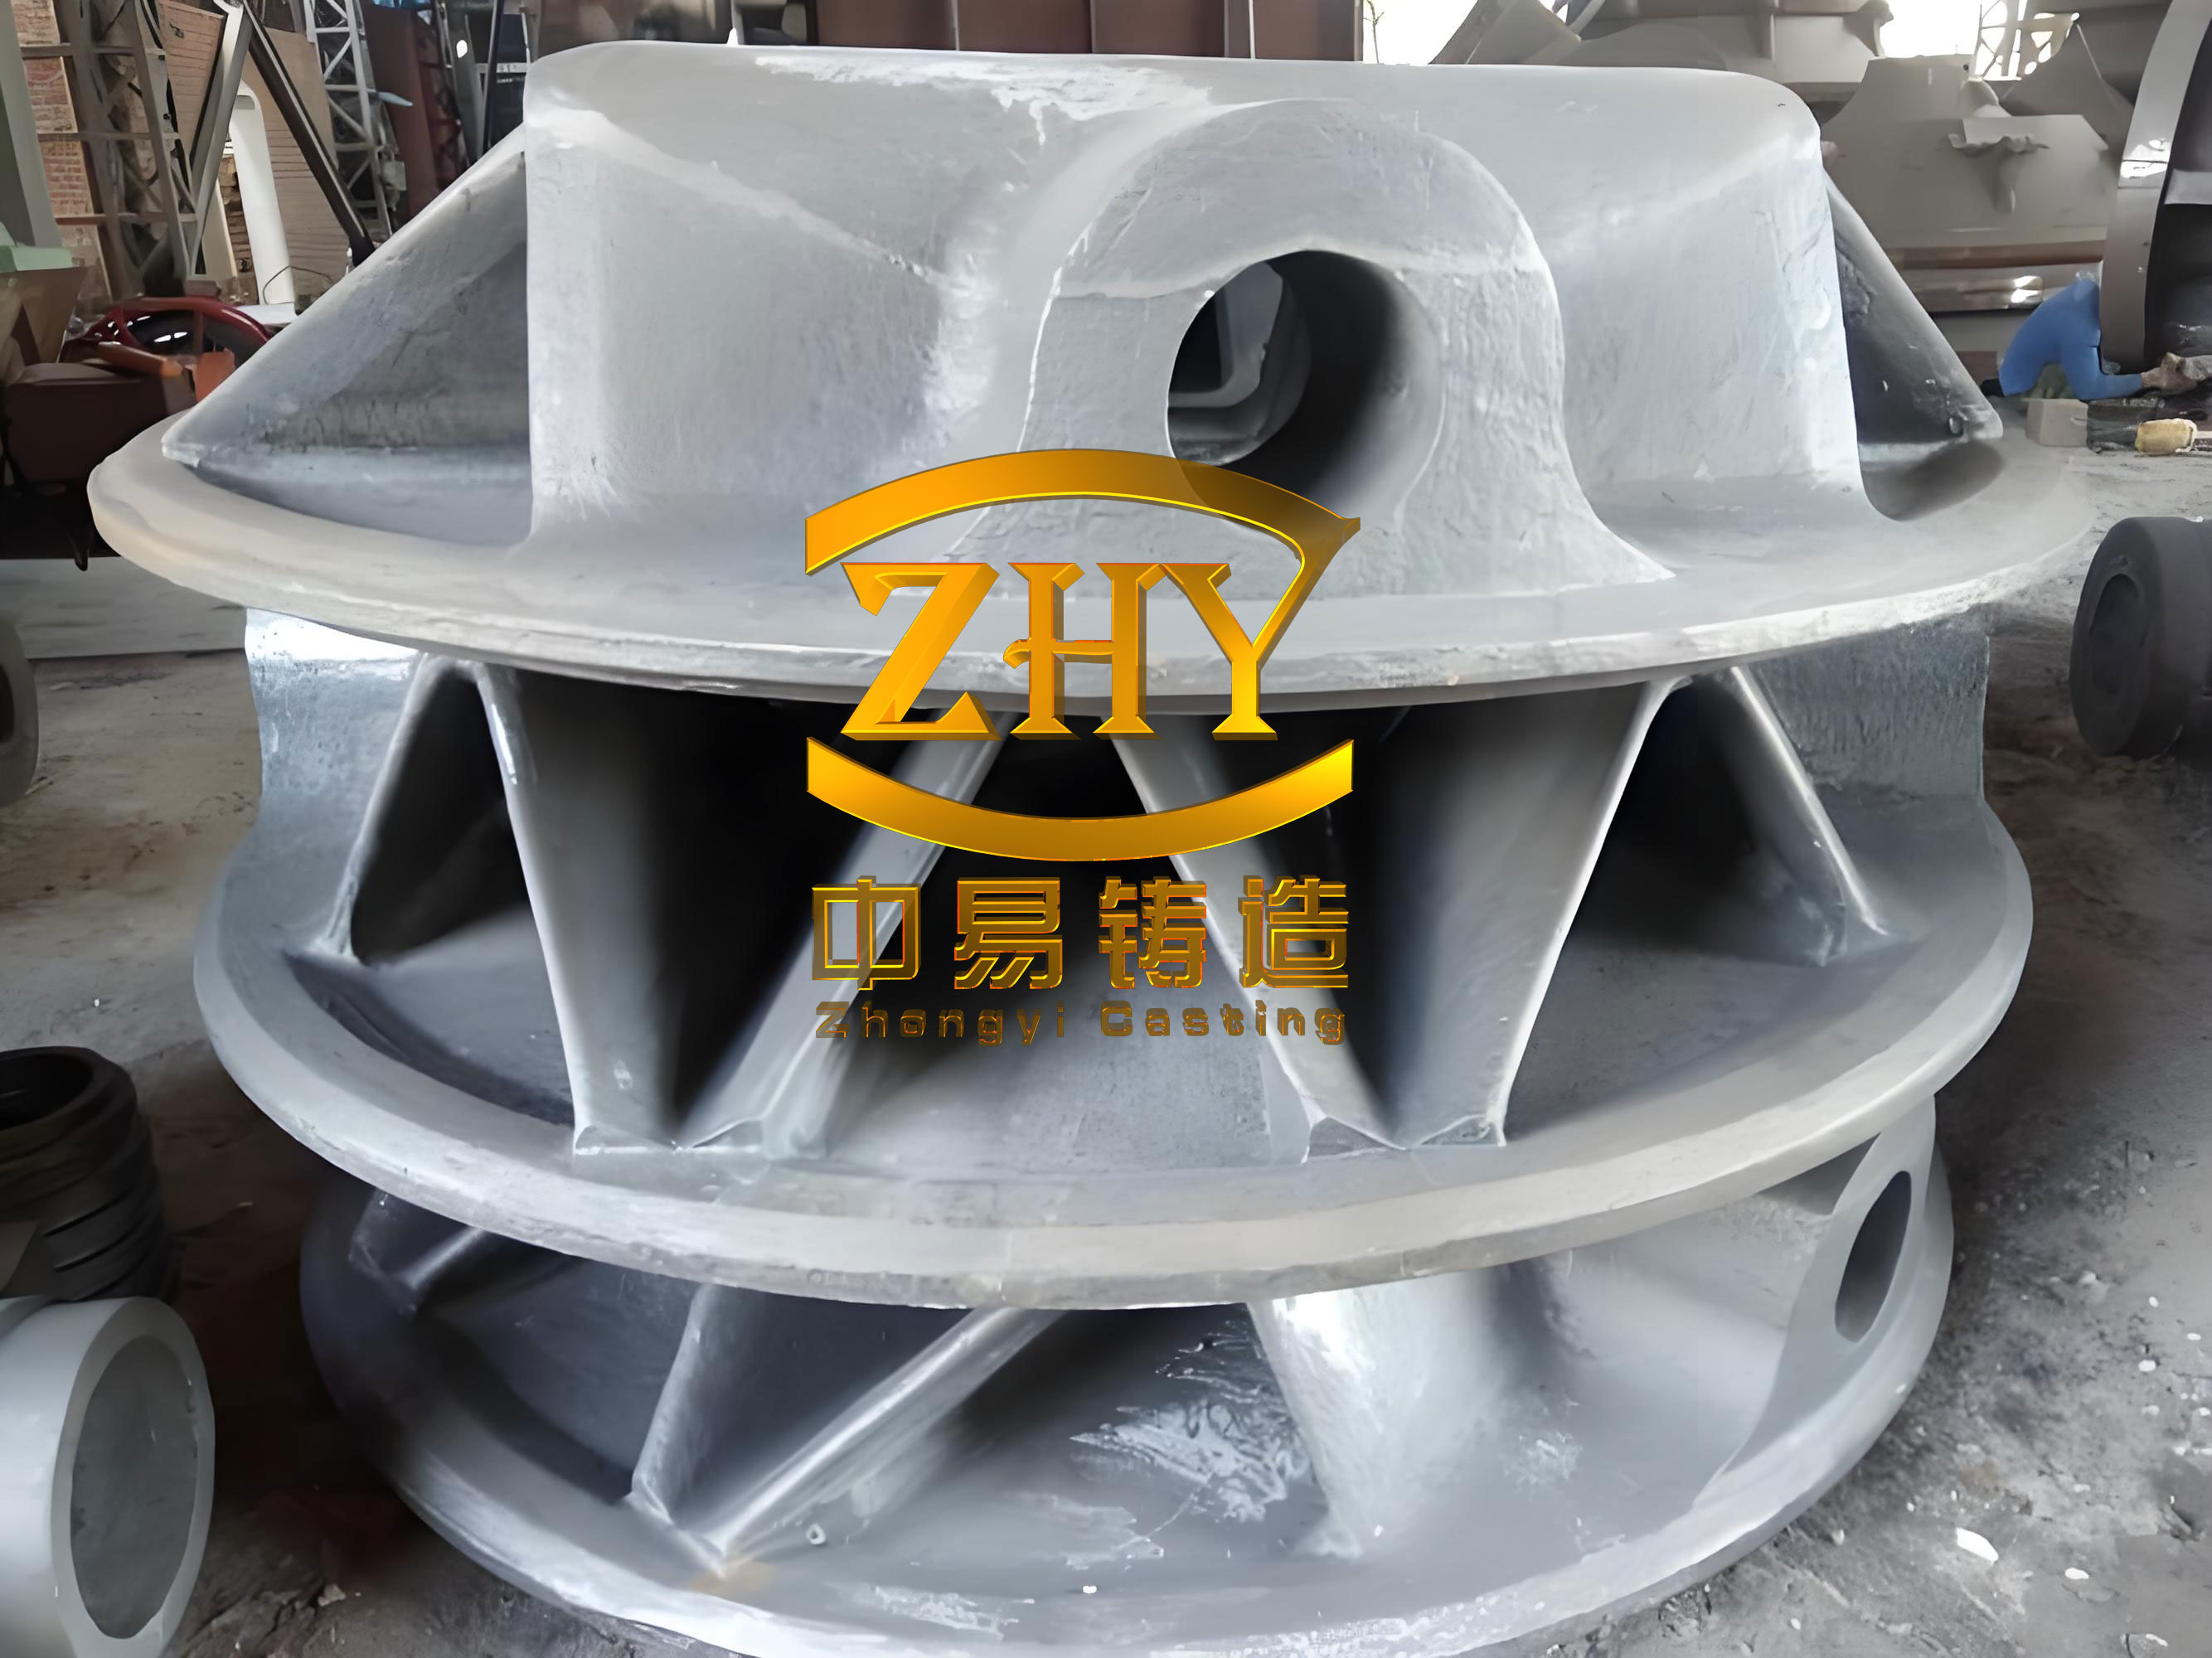
One particularly challenging case that I analyzed involved a diffusion-body casting made from QT400-18 ductile iron. The component was a large annular housing intended for an industrial gas-turbine-like application. The gross weight of the finished casting was 1480 kg, while the pouring weight, including the gating system and feeding aids, was 2000 kg. The pouring temperature was maintained between 1315 °C and 1330 °C, and the pouring time was targeted at 30 seconds, with an allowable tolerance of plus or minus 5 seconds. The main production problem was severe slag inclusion. The defects were concentrated at the top surface of the casting and on the internal cylindrical wall. In some production periods, the slag-related reject rate reached as high as 12%, causing serious disturbance to delivery schedules and manufacturing cost.
To determine the nature of the defect, I selected samples from the upper regions of rejected castings and prepared them for metallographic examination. The sections showed obvious clusters of non-metallic inclusions with a dendritic morphology. The inclusion clusters were relatively large, with the maximum measured length varying from approximately 600 μm up to more than 1000 μm. These inclusions were not isolated particles; they formed continuous network-like films. Because they appeared in the upper zones of the casting, it was evident that the inclusions had a lower density than the surrounding liquid iron and had floated upward during the period between mold filling and complete solidification.
The first step in the investigation was to classify the slag. In practical foundry terminology, the slag that exists in the ladle before pouring is often called primary slag. It comes from the nodularizing reaction, desulfurization products, and oxidized materials skimmed from the bath surface. If this slag is not removed completely, it can enter the mold during pouring and create large superficial defects. The second category is secondary slag, which is generated during pouring and mold filling. This type of slag is usually more dangerous because it is formed inside the gating system or the mold cavity itself, and it is more difficult to remove by simple skimming. In this diffusion-body casting, the metallographic evidence clearly suggested that the dominant problem was secondary oxidation slag rather than primary ladle slag. The inclusions were fine, dendritic, and widely distributed in the upper part of the casting, which is a typical result of reoxidation and entrainment during turbulent filling.
The chemical composition and structure of slag in ductile iron castings is complex. The main components are oxides such as MgO, SiO₂, Al₂O₃, FeO, and MnO, together with sulfides including MgS and CaS. Magnesium is particularly active. During nodularizing treatment, it reacts with oxygen and sulfur to form a dross layer. Even after the dross is skimmed, a thin film of oxidation products can form on the free surface of the melt. When this film is submerged by a turbulent stream, it becomes a solid inclusion. The table below summarizes the major possible phases and their role in the formation of slag defects in ductile iron castings.
| Phase | Approximate density (g/cm³) | Origin | Effect in ductile iron castings |
|---|---|---|---|
| MgO | 3.6 | Nodularizing reaction and reoxidation | High-melting-point particles; forms fragile surface films |
| SiO₂ | 2.6 | Sand erosion, oxidation of silicon | Viscous oxide phase; may combine with other oxides |
| Al₂O₃ | 3.9 | Oxidation of aluminum in the melt | Hard refractory inclusions; extremely harmful |
| FeO | 5.7 | Oxidation of iron | Increases wettability; favors further oxidation |
| MnO | 5.4 | Oxidation of manganese | Sometimes present in complex silicates |
| MgS | 2.8 | Reaction between magnesium and sulfur | Dark sulfide inclusions; often segregated at grain boundaries |
| CaS | 2.6 | Desulfurization products | Small globular inclusions; less harmful than oxides |
| Complex silicates | 3.0–4.0 | Combination of several oxide phases | Dendritic or film-like inclusions; typical of secondary slag |
The formation of these inclusions can be described by simple thermodynamic reactions. For example, magnesium oxidation and magnesium sulfide formation can be written as:
$$[Mg] + [O] \rightarrow MgO(s)$$
$$[Mg] + [S] \rightarrow MgS(s)$$
Similarly, aluminum in the melt can react with oxygen to form alumina:
$$2[Al] + 3[O] \rightarrow Al_2O_3(s)$$
These reactions occur mainly at the metal surface. In a quiet flow, the oxide film remains on top of the liquid and can be trapped in the gating system or directed into a sprue cavity where it floats to the riser. In a turbulent flow, however, the surface film is repeatedly folded into the bulk liquid. The depth of the folded film depends on the flow velocity and the amount of surface turbulence. For the diffusion-body casting, the original gating design clearly allowed this folding process to take place.
Another important factor in the formation of slag defects is the buoyancy of the inclusions. For a spherical inclusion of diameter \(d_p\), the terminal rising velocity in liquid iron can be estimated from Stokes’ law:
$$v_{\mathrm{rise}} = \frac{g \, d_p^2 \, (\rho_{\mathrm{Fe}} – \rho_{\mathrm{slag}})}{18 \, \mu}$$
where \(g\) is the gravitational acceleration, \(\rho_{\mathrm{Fe}}\) is the density of liquid iron, \(\rho_{\mathrm{slag}}\) is the density of the slag particle, and \(\mu\) is the dynamic viscosity of the liquid iron. Because the density of slag is generally much lower than that of liquid iron, isolated particles may rise and separate from the metal. However, in a strongly turbulent flow, the upward movement is counteracted by eddies. Large film-like inclusions are also difficult to separate. Therefore, reducing turbulence is essential for the production of clean ductile iron castings.
I then examined the original gating system in detail. The original process used a closed, pressurizing gating system with mid-height injection. The total cross-sectional area ratio was:
$$F_{\mathrm{sprue}} : F_{\mathrm{runner}} : F_{\mathrm{inner\_gate}} = 1 : 2.07 : 0.83$$
In this closed arrangement, the sprue was larger than the inner gates, and the flow rate was controlled by the total inner gate area. The sprue was a ceramic tube with a diameter of 70 mm, giving a cross-sectional area of 38.465 cm². The runner consisted of two trapezoidal channels with a combined area of 80.00 cm². There were eight flat inner gates, each measuring 38/42 mm by 10 mm, with a total area of 32.00 cm². The dimensions are summarized in the following table.
| Component | Quantity | Description | Total cross-sectional area (cm²) | Area ratio |
|---|---|---|---|---|
| Sprue | 1 | Ceramic tube, OD/ID, nominal diameter 70 mm | 38.47 | 1.00 |
| Runner | 2 | Trapezoidal runner, 40/60 × 80 mm | 80.00 | 2.08 |
| Inner gate | 8 | Flat gate, 38/42 × 10 mm | 32.00 | 0.83 |
Using the pouring data, I calculated the average volumetric flow rate. The mass poured into the mold was 2000 kg, and the density of liquid ductile iron was approximately 7000 kg/m³. Thus, the average flow rate can be obtained as:
$$Q = \frac{W}{\rho \, t_{\mathrm{pour}}}$$
Substituting the production values,
$$Q = \frac{2000}{7000 \times 30} \approx 9.52 \times 10^{-3} \, \mathrm{m^3/s}$$
This is equivalent to about 9520 cm³/s. With the original inner gate area of 32.00 cm², the average velocity at the inner gate was:
$$v_{\mathrm{old}} = \frac{Q}{A_{\mathrm{old}}} = \frac{9520}{32.00} \approx 298 \, \mathrm{cm/s}$$
This velocity is approximately 3.0 m/s, which was far above the reasonable maximum gate velocity of about 1.5 m/s for ductile iron castings. Even if some allowance is made for the difference between average and instantaneous flow rates, the original design was undoubtedly producing turbulent, violent filling. The liquid iron left the narrow inner gates with high kinetic energy, splashed into the mold cavity, and formed vortices. The mid-height injection position added an extra fall distance, which increased the speed still further. This explains why the internal wall and top surfaces were particularly affected by slags. The high-speed stream carried oxidized films into the upper regions, where they accumulated and became embedded in the solidifying shell of ductile iron castings.
The original gating system had another disadvantage. Because it was a closed system, the inner gates were the smallest cross-section. The metal was accelerated at the gate exits. The high velocity produced a severe contraction and atomization of the stream. Small droplets with oxide skins were generated. These droplets were not able to recombine into the main stream in the mold cavity. Instead, they froze as globular or dendritic inclusions. The metallographic observation of elongated, dendritic slag clusters was fully consistent with this kind of turbulent reoxidation mechanism.
To solve the problem, I decided to convert the gating system from a closed design to an open design. In an open gating system, the choke is placed in the sprue. All downstream areas are larger than the sprue. This reduces the flow velocity gradually and keeps the runner full, while avoiding excessive velocity at the gates. The new gating ratio was chosen as:
$$F_{\mathrm{sprue}} : F_{\mathrm{runner}} : F_{\mathrm{inner\_gate}} = 1 : 2.17 : 2.7$$
The sprue diameter was reduced from 70 mm to 60 mm. This gave a new sprue area of:
$$A_{\mathrm{sprue}} = \frac{\pi d^2}{4} = \frac{\pi \times 6^2}{4} \approx 28.27 \, \mathrm{cm^2}$$
The runner was redesigned as two trapezoidal channels with a combined cross-sectional area of 60.75 cm². The inner gates were enlarged from eight narrow gates to six wide flat gates, each having a cross-section of 80/90 mm by 15 mm. The total inner gate area was 76.5 cm². The key parameters of the modified gating system are shown below.
| Component | Quantity | Description | Total cross-sectional area (cm²) | Area ratio |
|---|---|---|---|---|
| Sprue | 1 | Ceramic tube, nominal diameter 60 mm | 28.27 | 1.00 |
| Runner | 2 | Trapezoidal runner, 35/100 × 90 mm | 60.75 | 2.15 |
| Inner gate | 6 | Flat gate, 80/90 × 15 mm | 76.50 | 2.71 |
With the enlarged inner gate area, the average velocity at the inner gates was reduced significantly. Under the actual pouring conditions used for this component, the calculated gate velocity was approximately 1.08 m/s. This value was close to the recommended limit for ductile iron castings, but it was low enough to prevent serious surface turbulence. The metal stream emerging from each inner gate was compact and continuous. There was no visible splashing, spraying, or vena contracta entrainment. As a result, the formation of secondary slag in the mold cavity became much less likely.
In addition to the design of the gating system, filtration was introduced to remove non-metallic inclusions before the liquid iron entered the mold cavity. I selected ceramic foam filters with dimensions of 120 mm × 120 mm × 20 mm. Ceramic foam filters are widely used in ductile iron castings because they mechanically trap particles and films while also reducing the local flow velocity. Each filter was capable of passing up to 400 kg of ductile iron under the given pouring conditions. The theoretical number of filters required for a pouring weight of 2000 kg was:
$$N_{\mathrm{required}} = \frac{W_{\mathrm{pour}}}{W_{\mathrm{filter}}} = \frac{2000}{400} = 5$$
To provide a safety factor and to match the two runner branches in the gating layout, I installed six filter pads. The filters were placed at the transition between the upper and lower runner sections. This location allowed the metal to be cleaned just before it was distributed to the inner gates. The liquid iron passed through the ceramic foam, which stopped large oxide films, sulfide particles, and eroded sand grains. The filters also smoothed the flow front and reduced local velocity fluctuations. This was particularly valuable for the quality of the ductile iron castings, because it prevented the thin oxide skins from being carried into the main cavity.
The comparison between the old and new designs can be summarized as follows.
| Parameter | Original design | Modified design |
|---|---|---|
| Gating system type | Closed, pressure system | Open, unpressurized system |
| Choke location | Inner gates | Sprue |
| Sprue diameter | 70 mm | 60 mm |
| Total inner gate area | 32 cm² | 76.5 cm² |
| Calculated gate velocity | > 1.5 m/s, possibly about 3 m/s | ≈ 1.08 m/s |
| Filter | None | 6 ceramic foam filters, 120 × 120 × 20 mm |
| Slag-related scrap rate | Up to 12% | Almost zero |
| Surface condition | Dark inclusions on top and inner wall | Clean surface, no visible slag clusters |
| Metallographic cleanliness | Dendritic inclusions, 600–1000 μm | No significant inclusions in critical zones |
After the modified system was introduced, the first castings were inspected with the same methods used previously. The improvement was immediately visible. The top surface and the inner cylindrical wall were clean. Metallographic samples taken from the same locations that had previously shown massive dendritic inclusions no longer contained any significant non-metallic defects. I continued to monitor the production process for more than 100 subsequent pieces. No casting was rejected because of severe slag inclusions. This was a major improvement because the earlier reject rate had occasionally reached 12%.
The solution also had a positive effect on the mechanical reliability of the ductile iron castings. Slag inclusions in the old components had acted as internal notches. When tensile specimens or component sections were loaded, the inclusions opened early and reduced the effective load-bearing area. In some cases, the inclusions were connected to the exterior surface, causing leakage. After the gating redesign and filtration, the microstructure became much sounder. The material was able to develop the full strength and elongation expected of QT400-18 ductile iron. The product passed the customer’s final inspection and was accepted for serial production.
This case shows that the elimination of slag defects in ductile iron castings is not always achieved by changing the melting practice or the nodularizing agent. Sometimes the problem lies in the way the metal is introduced into the mold. In the diffusion-body casting described here, the fundamental cause of the slag was excessive velocity in the original closed gating system. The high gate velocity produced turbulence and reoxidation. The turbulent liquid iron folded oxide films into the metal stream, and those films floated to the top surfaces where they solidified as dendritic inclusions.
The main technical actions that solved the problem were as follows. First, the gating system was changed to an open, unpressurized system with the sprue as the choke. This reduced the velocity at the inner gates to about 1.08 m/s. Second, the number and geometry of inner gates were changed from eight narrow gates to six wide gates. This lower the exit momentum and minimized the risk of spray and vortex formation. Third, ceramic foam filters were installed in the runner to remove primary oxide and sulfide particles before they entered the cavity. These three changes combined to provide stable, clean filling of the mold.
It is also important to note that the modification did not complicate the production process. The new ceramic sprue was simple to use. The ceramic foam filters were easy to locate in the existing mold assembly because the runner junction was designed with a suitable seat. The pouring temperature and pouring time remained within the established ranges. The foundry workers did not need special additional skills. This is another reason why the improvement was sustainable in mass production of ductile iron castings.
I believe this case can be used as a reference for similar heavy-section ductile iron castings. The same analytical approach can be applied to other components: characterize the slag, distinguish primary from secondary inclusions, calculate the gate velocity, check the gating ratio, and introduce filters if necessary. The most important lesson is that the filling behavior of ductile iron must be controlled from the design stage. If the gating system produces turbulent flow, the quality of the liquid metal is destroyed during the last few seconds before solidification. No amount of good metal treatment can compensate for a poor gating design.
In conclusion, the occurrence of slag inclusions in the diffusion-body ductile iron casting was a process-related problem. By converting the gating system from closed to open, by increasing the total inner gate area, and by installing ceramic foam filters, the gate velocity was reduced from a dangerously high value to a safe level. The result was a dramatic reduction in the scrap rate and a substantial improvement in the cleanliness and mechanical reliability of the final product. This experience reinforces the fundamental engineering principle that mold filling control is one of the most powerful tools available for producing sound ductile iron castings.