
Ductile iron castings are widely used in modern industry because they combine the castability of gray iron with mechanical properties that are comparable to steel in many applications. However, ductile iron castings are also known for their sensitivity to solidification-related defects, especially shrinkage cavities and dispersed microporosity. In my work, I analyzed a shell-shaped casting made of QT500-7 ductile iron. The component is used in mechanical instrumentation equipment, and it has to meet strict dimensional and pressure-tightness requirements. Since the casting geometry contains several local heavy sections and abrupt wall transitions, the design of the feeding system is critical. I therefore developed two casting processes for these ductile iron castings and evaluated them by numerical simulation before production. The main purpose was to select a robust process that would produce sound castings and to compare the simulation predictions with actual production results.
1. Component Characteristics and Material Requirements
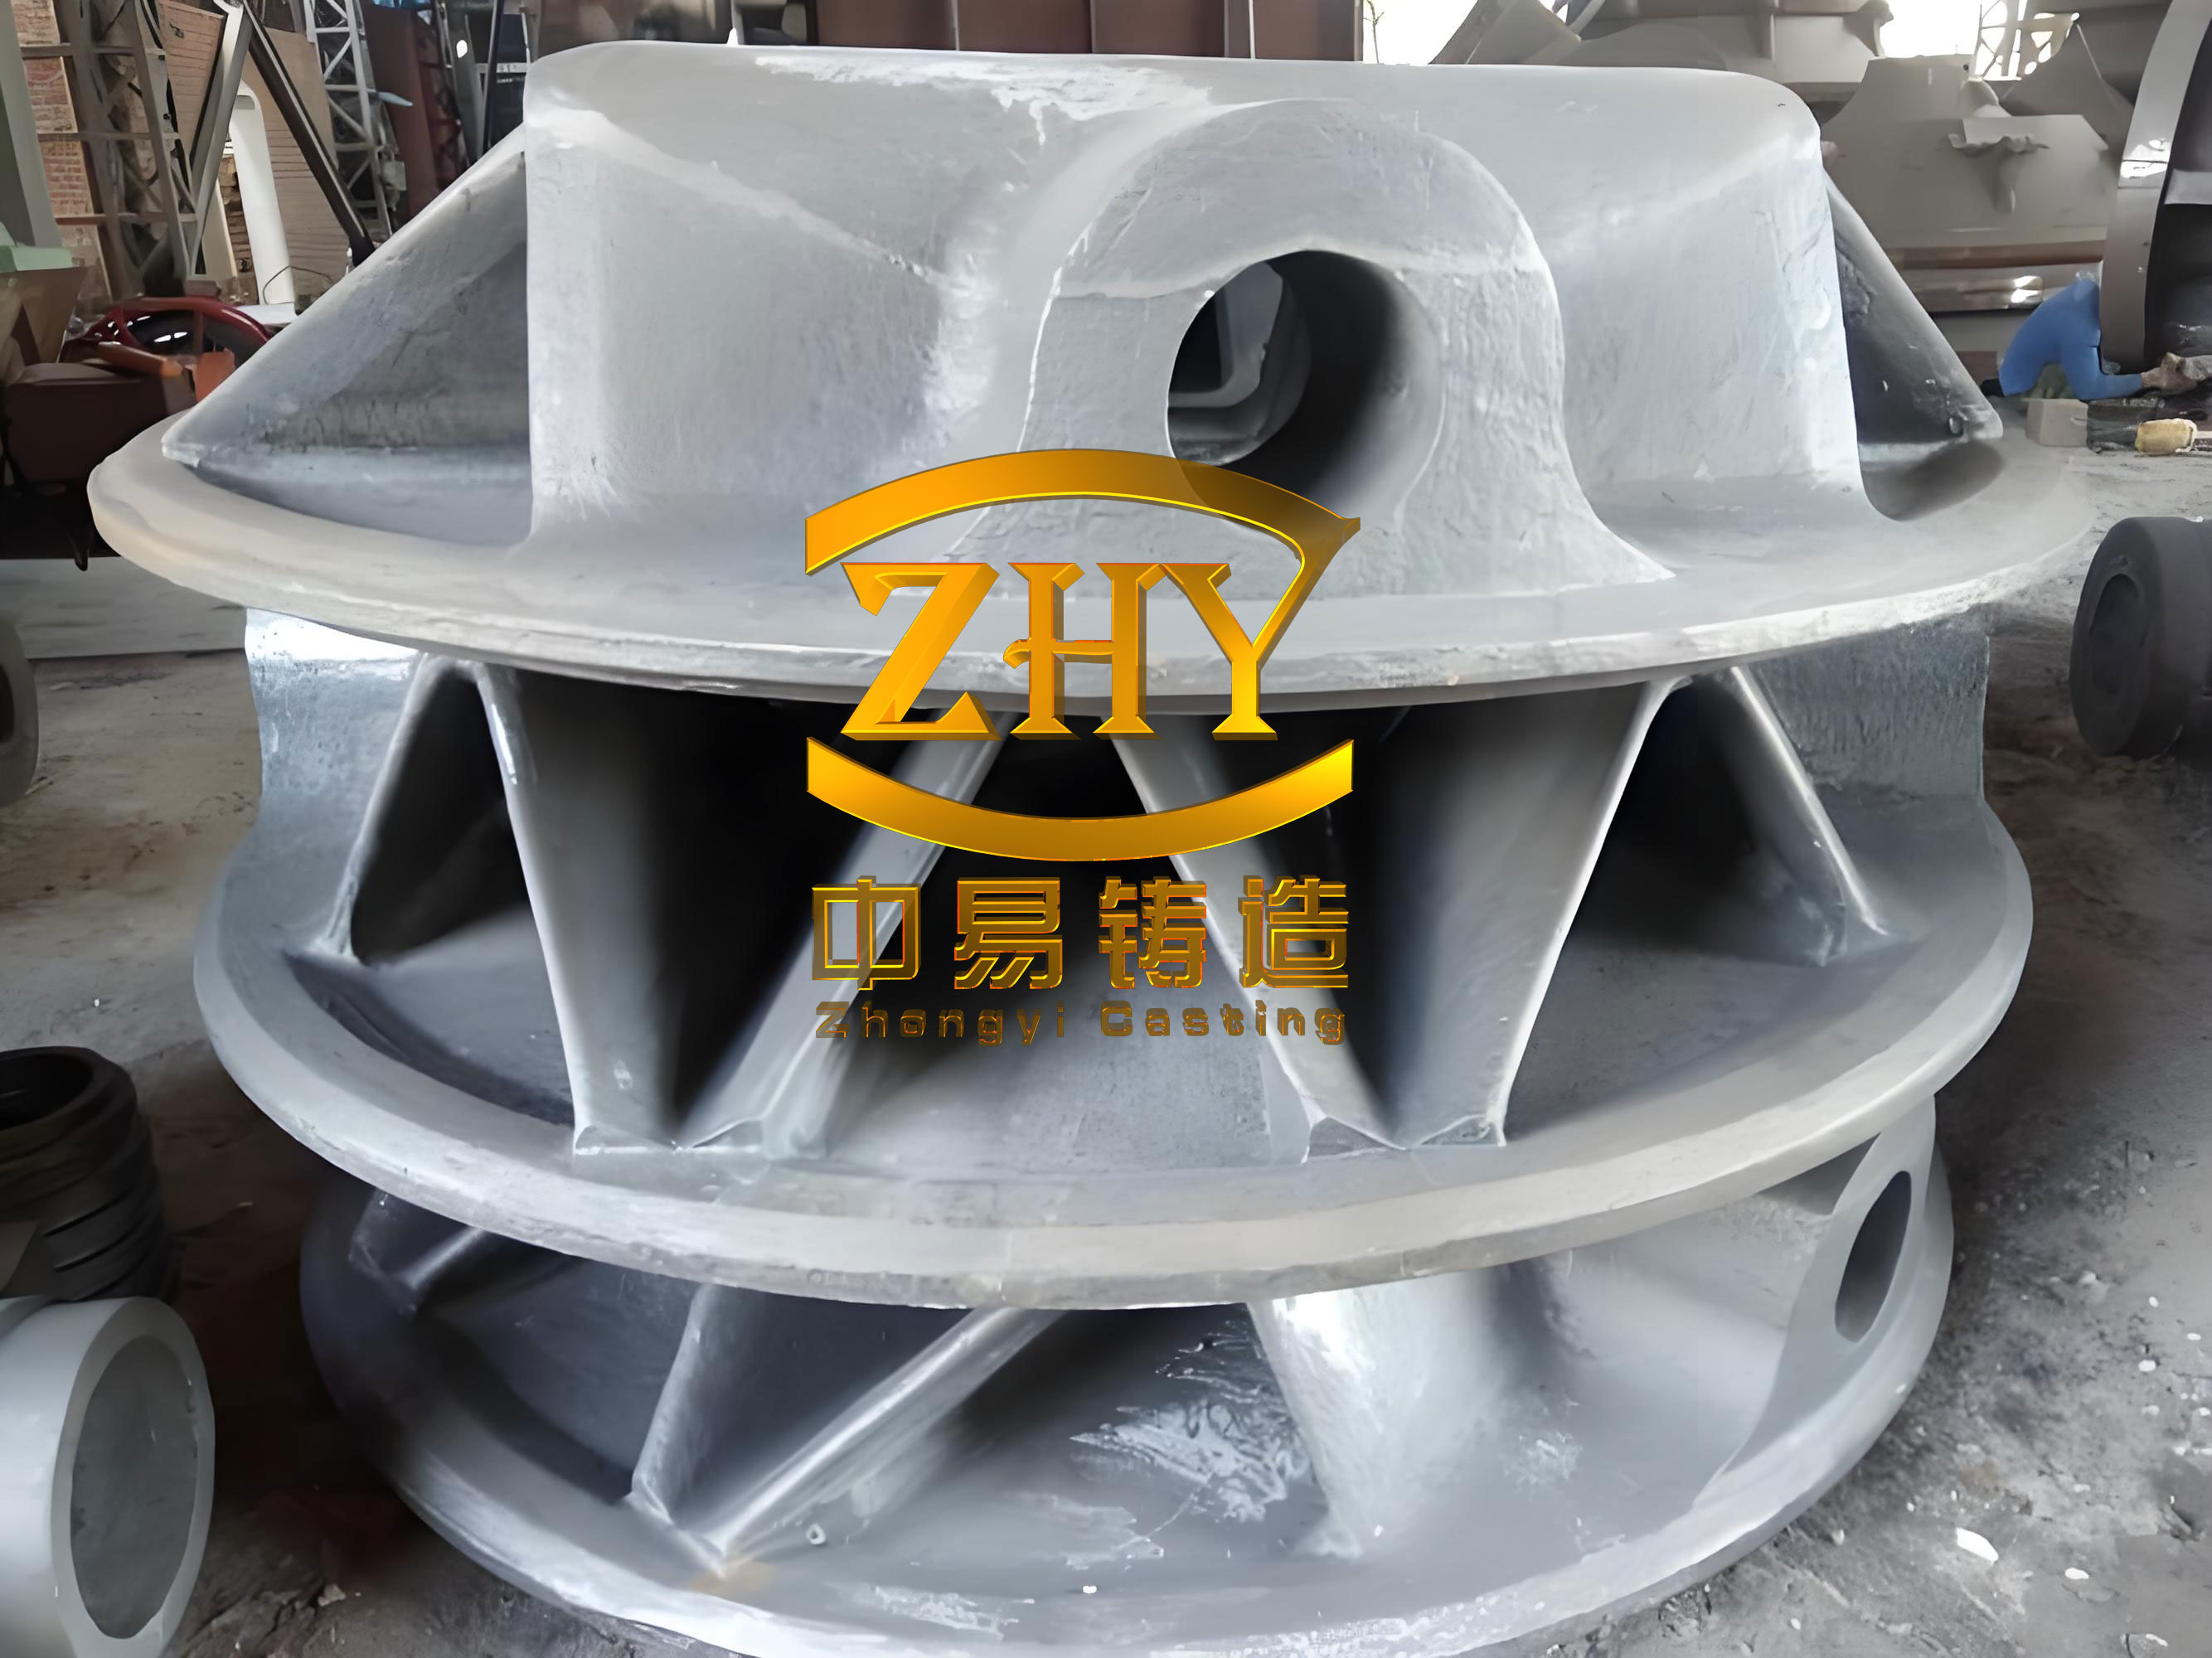
The shell casting studied in this project has a complex shape. It consists of a lower flange-like section and a central cylindrical bore. The lower section is relatively thin but contains local bosses and corners where the thermal center is large. The cylindrical bore creates a natural mold core and causes the surrounding metal to solidify slowly. The wall-thickness distribution is not uniform, and this makes ductile iron castings particularly prone to the formation of isolated liquid regions during the final stage of solidification. Those isolated liquid regions cannot be fed by the riser because the surrounding dendrites have already formed a coherent solid network. As a result, shrinkage porosity appears after machining.
The material specified for this component was QT500-7 ductile iron. This grade is required to have a minimum tensile strength of 500 MPa, a minimum yield strength of 320 MPa, and a minimum elongation of 7%. Its matrix is generally ferritic with some pearlite, and the graphite is present as spheroids. The required mechanical properties and the need for pressure tightness made it necessary to pay close attention to the solidification feeding of the casting. Table 1 summarizes the material data and casting conditions used in the process analysis.
| Item | Value or Description |
|---|---|
| Material grade | QT500-7 ductile iron |
| Minimum tensile strength | 500 MPa |
| Minimum yield strength | 320 MPa |
| Minimum elongation | 7% |
| Brinell hardness | 170–230 HB |
| Graphite form | Nodular / spheroidal graphite |
| Matrix | Ferritic-pearlitic |
| Mold material | Resin-bonded sand |
| Pouring temperature | 1350 °C |
| Casting process | Sand casting with cold iron chills |
For ductile iron castings, the solidification behavior is not the same as that of ordinary gray iron. In gray iron, flake graphite precipitates continuously during eutectic solidification and compensates for solidification shrinkage. In ductile iron castings, graphite grows as nodules, and the liquid feeding behavior is different. The solidification interval is often wider, and the pasty region is larger. If the mold is rigid and the graphite expansion is effectively used, the tendency to shrinkage can be reduced. However, if the feeding path is blocked too early or if the mold wall expands under metallostatic pressure, shrinkage porosity can still form. Therefore, riser design, chilling strategy, and gating system layout must be evaluated together.
2. Two Casting Process Alternatives
Two different feeding methods were designed for the same shell casting. Both processes used chills at the lower end face and around the central cylindrical bore. The chills had the same size, position, and form in both cases. The difference between the two alternatives was mainly the riser type and the gating arrangement.
Scheme A used a blind riser combined with an ingate. The riser neck width was 10 mm. In this arrangement, liquid metal enters through the riser and then flows into the casting cavity. This type of feeding system can be effective because the flowing liquid metal keeps the riser neck hot for a longer time. However, the flow of liquid metal through the riser can also create a flow-induced hot spot in the casting region beneath the riser. If the riser is placed directly over the largest casting hot spot, it may increase the size of that hot spot instead of simply feeding it. This problem was observed in the simulation.
Scheme B used a simpler gating system, with one sprue and one riser. The riser was an open pressure-edge riser, also called a slot riser or pressure-edge feeder. It was made conformal to the circular upper face of the casting, and the pressure-edge slot thickness was 8 mm. By using this design, the liquid metal did not pass through the riser in a way that created an artificial hot spot. Instead, the riser was placed directly above the hot spot, and the continuous slot provided a direct feeding path. This design proved to be more effective in the simulation and later in production.
| Feature | Scheme A | Scheme B |
|---|---|---|
| Riser type | Blind riser | Open pressure-edge riser |
| Riser feeding element | Ingate combined with riser neck | Conformal pressure-edge slot |
| Riser neck / slot width | 10 mm | 8 mm |
| Riser location | At the maximum hot spot | At the hot spot, on the upper circular face |
| Gating system | More complex, with metal passing through the riser | Single sprue and single riser |
| Cold iron chills | Identical | Identical |
| Primary feeding path | Riser neck to casting | Continuous slot to casting |
3. Numerical Simulation Model
I created three-dimensional models of the casting, gating system, risers, chills, and sand mold for both schemes. The simulation was based on transient heat transfer and solidification calculations. The main equation solved during the solidification analysis was the Fourier heat conduction equation with a latent-heat source term:
$$ \rho c_p \frac{\partial T}{\partial t} = \nabla \cdot \left( k \nabla T \right) + \dot{Q} $$
In this equation, \( \rho \) is density, \( c_p \) is specific heat, \( k \) is thermal conductivity, \( T \) is temperature, and \( t \) is time. The term \( \dot{Q} \) represents the heat released by phase transformation. For ductile iron castings, the phase change occurs over a temperature interval, so the latent heat release is related to the rate of solid fraction change:
$$ \dot{Q} = \rho L \frac{\partial f_s}{\partial t} $$
In this expression, \( L \) is the latent heat and \( f_s \) is the solid fraction. In a simplified linear solidification model, the solid fraction can be expressed as:
$$ f_s(T) = \frac{T_l – T}{T_l – T_s}, \quad T_s \le T \le T_l $$
where \( T_l \) is the liquidus temperature and \( T_s \) is the solidus temperature. The liquid fraction is then:
$$ f_l = 1 – f_s $$
The simulation model also allowed me to compute the thermal gradient \( G \) and the cooling rate \( \dot T \). These quantities are important for predicting shrinkage porosity in ductile iron castings. The thermal gradient magnitude is defined as:
$$ G = \left| \nabla T \right| = \sqrt{ \left( \frac{\partial T}{\partial x} \right)^2 + \left( \frac{\partial T}{\partial y} \right)^2 + \left( \frac{\partial T}{\partial z} \right)^2 } $$
and the cooling rate is:
$$ \dot T = \frac{\partial T}{\partial t} $$
From these values, the Niyama criterion can be calculated:
$$ N_y = \frac{G}{\sqrt{\dot T}} $$
Low Niyama values indicate regions where the thermal gradient is small relative to the cooling rate. In many castings, these regions are susceptible to microshrinkage because the liquid cannot be fed through the fine mushy zone. For ductile iron castings, the Niyama criterion must be used carefully because graphite expansion can modify the feeding behavior, but it is still useful as a relative indicator.
The numerical model also respected the feeding rule based on modulus. The modulus \( M \) of a casting or riser is defined as the ratio of volume to cooling surface area:
$$ M = \frac{V}{A} $$
The solidification time is related to the modulus by Chvorinov’s rule:
$$ t_s = K M^2 $$
where \( K \) depends on mold material, casting material, and pouring conditions. For the riser to remain liquid after the casting has solidified, its modulus must be sufficiently large:
$$ M_r \approx 1.2 M_c $$
In this relationship, \( M_r \) is the modulus of the riser and \( M_c \) is the modulus of the casting region being fed. The riser neck or feeding slot must also remain open long enough to allow liquid metal to flow into the casting. This means the neck modulus must be selected carefully:
$$ M_n \approx 1.0 \sim 1.1 M_c $$
These modulus calculations provided a useful starting point for the riser dimensions. The simulation then verified whether the chosen dimensions were adequate for the actual casting geometry and gating layout.
4. Simulation Results for Scheme A
The first simulation was carried out for Scheme A, in which a blind riser was placed directly over the largest hot spot. The residual liquid distribution at a late stage of solidification showed clear evidence of feeding problems. Some regions in the lower part of the casting remained liquid after the surrounding metal had already solidified. These regions were isolated liquid islands. They could not be fed by the blind riser because the liquid feeding path had already been interrupted by solid grains.
The interpretation of this result is important. The ingate that passed through the riser kept the riser neck warm, and this had a positive effect on feeding. However, the same flowing metal also increased the size of the hot spot below the riser. In other words, the riser was placed exactly at the thermal center of the casting, but the gating system made that thermal center even larger. Because the riser was not large enough to compensate for this enlarged hot spot, the resulting solidification pattern was unfavorable.
From a design point of view, this is a common problem in ductile iron castings. A riser must be close to a hot spot to feed it effectively, but it should not significantly increase the size of that hot spot. The best solution is to place the riser near the hot spot rather than directly over it, especially when the gating system is directed through the riser. If the hot spot is too large, additional cooling such as chills should be used to reduce the local modulus.
| Evaluation item | Observation |
|---|---|
| Residual liquid at late solidification | Isolated liquid islands present in the lower casting section |
| Feeding path | Interrupted by solidified dendrites before the riser could fully feed the casting |
| Riser effectiveness | Partially effective only; the riser neck stayed open but the casting hot spot was enlarged |
| Effect of gating system | The ingate through the riser increased the local thermal center |
| Predicted defect risk | High risk of dispersed shrinkage porosity in the isolated liquid regions |
| Possible correction | Move the riser beside the hot spot or provide a larger riser plus stronger chilling |
These simulation results showed that the residual liquid distribution was not simply a matter of riser size. The interaction between the gating system and the riser influenced the solidification sequence. In ductile iron castings, the formation of an isolated liquid island is particularly dangerous because the pasty zone is wide. Once the solid fraction reaches a critical value, the remaining liquid cannot flow through the narrow interdendritic channels. The result is a pressure drop and the formation of shrinkage porosity:
$$ \Delta P = \int_{0}^{L_f} \frac{\mu}{K_p} v_l \, dx $$
Here, \( \mu \) is the dynamic viscosity of the liquid metal, \( K_p \) is the permeability of the mushy zone, \( v_l \) is the liquid velocity, and \( L_f \) is the length of the feeding path. When the permeability becomes very low, even a small feeding distance causes a large pressure drop. This is why the isolated liquid islands in Scheme A were considered unacceptable.
5. Simulation Results for Scheme B
Scheme B was designed with a simpler gating layout and a different riser concept. The riser was a conformal pressure-edge riser placed on the upper circular face of the shell casting. The feeding slot was continuous, with a thickness of 8 mm. I expected this design to produce better feeding because the liquid metal did not have to pass through an ingate before reaching the casting. The simulation confirmed this expectation.
In the residual liquid distribution for Scheme B, no isolated liquid islands appeared during the final stage of solidification. The liquid remaining in the casting remained connected to the riser through the pressure-edge slot. The feeding path was open long enough to compensate for solidification shrinkage. This is exactly what is needed for sound ductile iron castings.
Several factors contributed to the improved behavior. First, the open pressure-edge riser eliminated the flow-induced hot spot that had been present in Scheme A. Second, the riser was placed directly on the hot spot, so the temperature gradient in the casting was directed toward the riser. Third, the use of cold iron chills at the lower section and around the central cylindrical bore reduced the solidification time of those heavy regions, helping to establish a favorable directional solidification pattern.
The lower section of the casing had a rectangular cross-section with a relatively high length-to-width ratio. In such a section, a long thin cooling path can freeze early and cut off the supply of liquid metal to the hottest part. The chills were therefore essential. Without chilling, the feed path from the riser to the lower hot spots would be too long, and even a well-designed pressure-edge riser might not produce sound ductile iron castings. The chills increased the local thermal gradient and moved the solidification front in a way that promoted feeding from the riser.
| Evaluation item | Observation |
|---|---|
| Residual liquid at late solidification | No isolated liquid islands observed |
| Feeding path | Continuous and connected to the riser until the final stage |
| Riser effectiveness | High; pressure-edge slot remained open and fed the solidification shrinkage |
| Effect of gating system | No harmful flow-induced hot spot |
| Effect of cold iron chills | Improved directional solidification in the rectangular lower section |
| Predicted defect risk | Low; sound casting expected |
I also compared the solidification time of the riser, the casting, and the feeding slot in Scheme B. The modulus relationship can be expressed in the form:
$$ t_{s,r} \ge t_{s,c} \ge t_{s,n} $$
where \( t_{s,r} \) is the solidification time of the riser, \( t_{s,c} \) is the solidification time of the casting, and \( t_{s,n} \) is the solidification time of the feeding slot. In a correct design, the riser should solidify last, the casting should solidify earlier, and the feeding slot should solidify at a time that allows liquid metal to flow until the casting is fully solidified. Scheme B satisfied this sequence much better than Scheme A.
6. Comparison of the Two Schemes
When I compared the two simulation results, the difference was clear. Scheme A produced a residual-liquid distribution with isolated pools and a high risk of microporosity. Scheme B produced a smooth solidification sequence with no isolated pools and a much lower risk of shrinkage defects. This comparison is summarized in Table 5.
| Design Aspect | Scheme A | Scheme B |
|---|---|---|
| Riser type | Blind riser | Open pressure-edge riser |
| Feeding path | Blocked in late solidification | Remained open |
| Isolated liquid islands | Present | Absent |
| Flow-induced hot spot | Yes | No |
| Predicted shrinkage | Likely | Unlikely |
| Process complexity | More complex gating | Simpler gating |
| Suitability for production | Not suitable | Suitable |
This comparison shows that numerical simulation is not only useful for verifying a final design; it is also useful for rejecting a poor design before expensive tooling is made. For ductile iron castings, the cost of a defect discovered after machining is very high because the machining cost has already been added. Simulation allows the process engineer to see the solidification sequence and predict whether the feeding system is correct.
7. Production Verification
Based on the simulation results, I selected Scheme B as the final production process. The castings were produced by manual resin-sand molding. The molten iron was spheroidized before pouring, and the pouring temperature was controlled at approximately 1350 °C. The castings were then allowed to cool, were knocked out, and were subjected to normal fettling and heat treatment before machining.
The machined castings did not show any obvious shrinkage cavities, surface porosity, or other solidification-related defects. The dimensional accuracy met the requirements of the drawing. This result was consistent with the simulation prediction. The absence of defects was particularly important because the shell casting is used in a mechanical instrumentation application where internal porosity cannot be tolerated.
The production run therefore confirmed that the simulations were reliable for this ductile iron shell casting. The same simulation methodology can be applied to other ductile iron castings with similar geometry and feeding conditions. In particular, the ability to visualize the residual liquid distribution helps identify dangerous isolated liquid regions that are difficult to detect by simple modulus calculations.
8. Lessons for the Design of Ductile Iron Castings
From this study, I drew several practical conclusions that are useful for the future design of ductile iron castings.
First, riser placement must be considered together with the gating system. A blind riser combined with an ingate should not be placed directly over the largest hot spot if the ingate creates a flow-induced hot spot in the casting below the riser. The riser should be located near the hot spot so that it can feed the region without making the thermal center larger. This is a key point for producing sound ductile iron castings.
Second, the pressure-edge riser is a powerful tool for ductile iron castings. Because it uses a continuous slot, it can be made conformal to the casting contour. This keeps the feeding path short and direct. In Scheme B, the pressure-edge slot remained open until the casting was sufficiently solidified, and no liquid islands appeared in the residual liquid maps.
Third, chills are often necessary for ductile iron castings with long rectangular sections. The lower section of this shell casting had a large length-to-width ratio. Without chills, this section would have solidified in a way that isolated the liquid in the heavy zones. The chills increased the thermal gradient and promoted directional solidification toward the riser. The use of chills is therefore not optional in such cases; it must be part of the process design.
Fourth, numerical simulation can help optimize ductile iron castings before production. The simulation did not replace engineering judgment, but it provided important information about the solidification sequence and residual liquid distribution. By comparing two alternatives, I was able to select the better process with confidence. The actual production results then confirmed the simulation predictions.
9. Conclusion and Recommendations
The shell casting made of QT500-7 ductile iron was successfully produced using a conformal pressure-edge riser and cold iron chills. The same component was originally considered with a blind riser and ingate, but simulation showed that this arrangement would leave isolated liquid regions in the casting. The production trial using the pressure-edge riser produced sound ductile iron castings with no visible shrinkage defects.
I recommend that future work on similar ductile iron castings include a systematic simulation study before finalizing the feeding system. The following points should always be checked:
1. The residual liquid distribution at the final stage of solidification should not contain isolated liquid islands.
2. The riser should solidify later than the casting region it feeds.
3. The feeding slot or riser neck should be sized so that it remains open during the critical feeding period.
4. Chills should be used to control the solidification of long thin sections and heavy bosses.
5. The gating system should not create a flow-induced hot spot that increases the modulus of the casting region.
Numerical simulation is a practical tool for evaluating these conditions before mold making. The results obtained in this project show that simulation can accurately predict the behavior of ductile iron castings and can lead to robust, economical casting designs. By applying the same procedure to other components, it is possible to reduce the risk of shrinkage defects, reduce trial castings, and improve the overall quality of ductile iron castings.