
I was assigned to develop a robust casting process for a main reduction shell cover used in heavy truck axle assemblies. This component, a ductile iron casting grade QT400-15, presented an interesting feeding challenge because the design combined a relatively thin main wall with local thick sections. The casting envelope was 554 mm × 350 mm × 138 mm, the nominal wall thickness was only 7 mm, and the local thick sections were up to 37 mm. The total weight was 20 kg. The customer specification permitted no shrinkage cavities, no surface shrinkage depressions, and no internal shrinkage porosity. That requirement is common for critical ductile iron castings, but achieving it is difficult when thin and thick sections coexist in one mold.
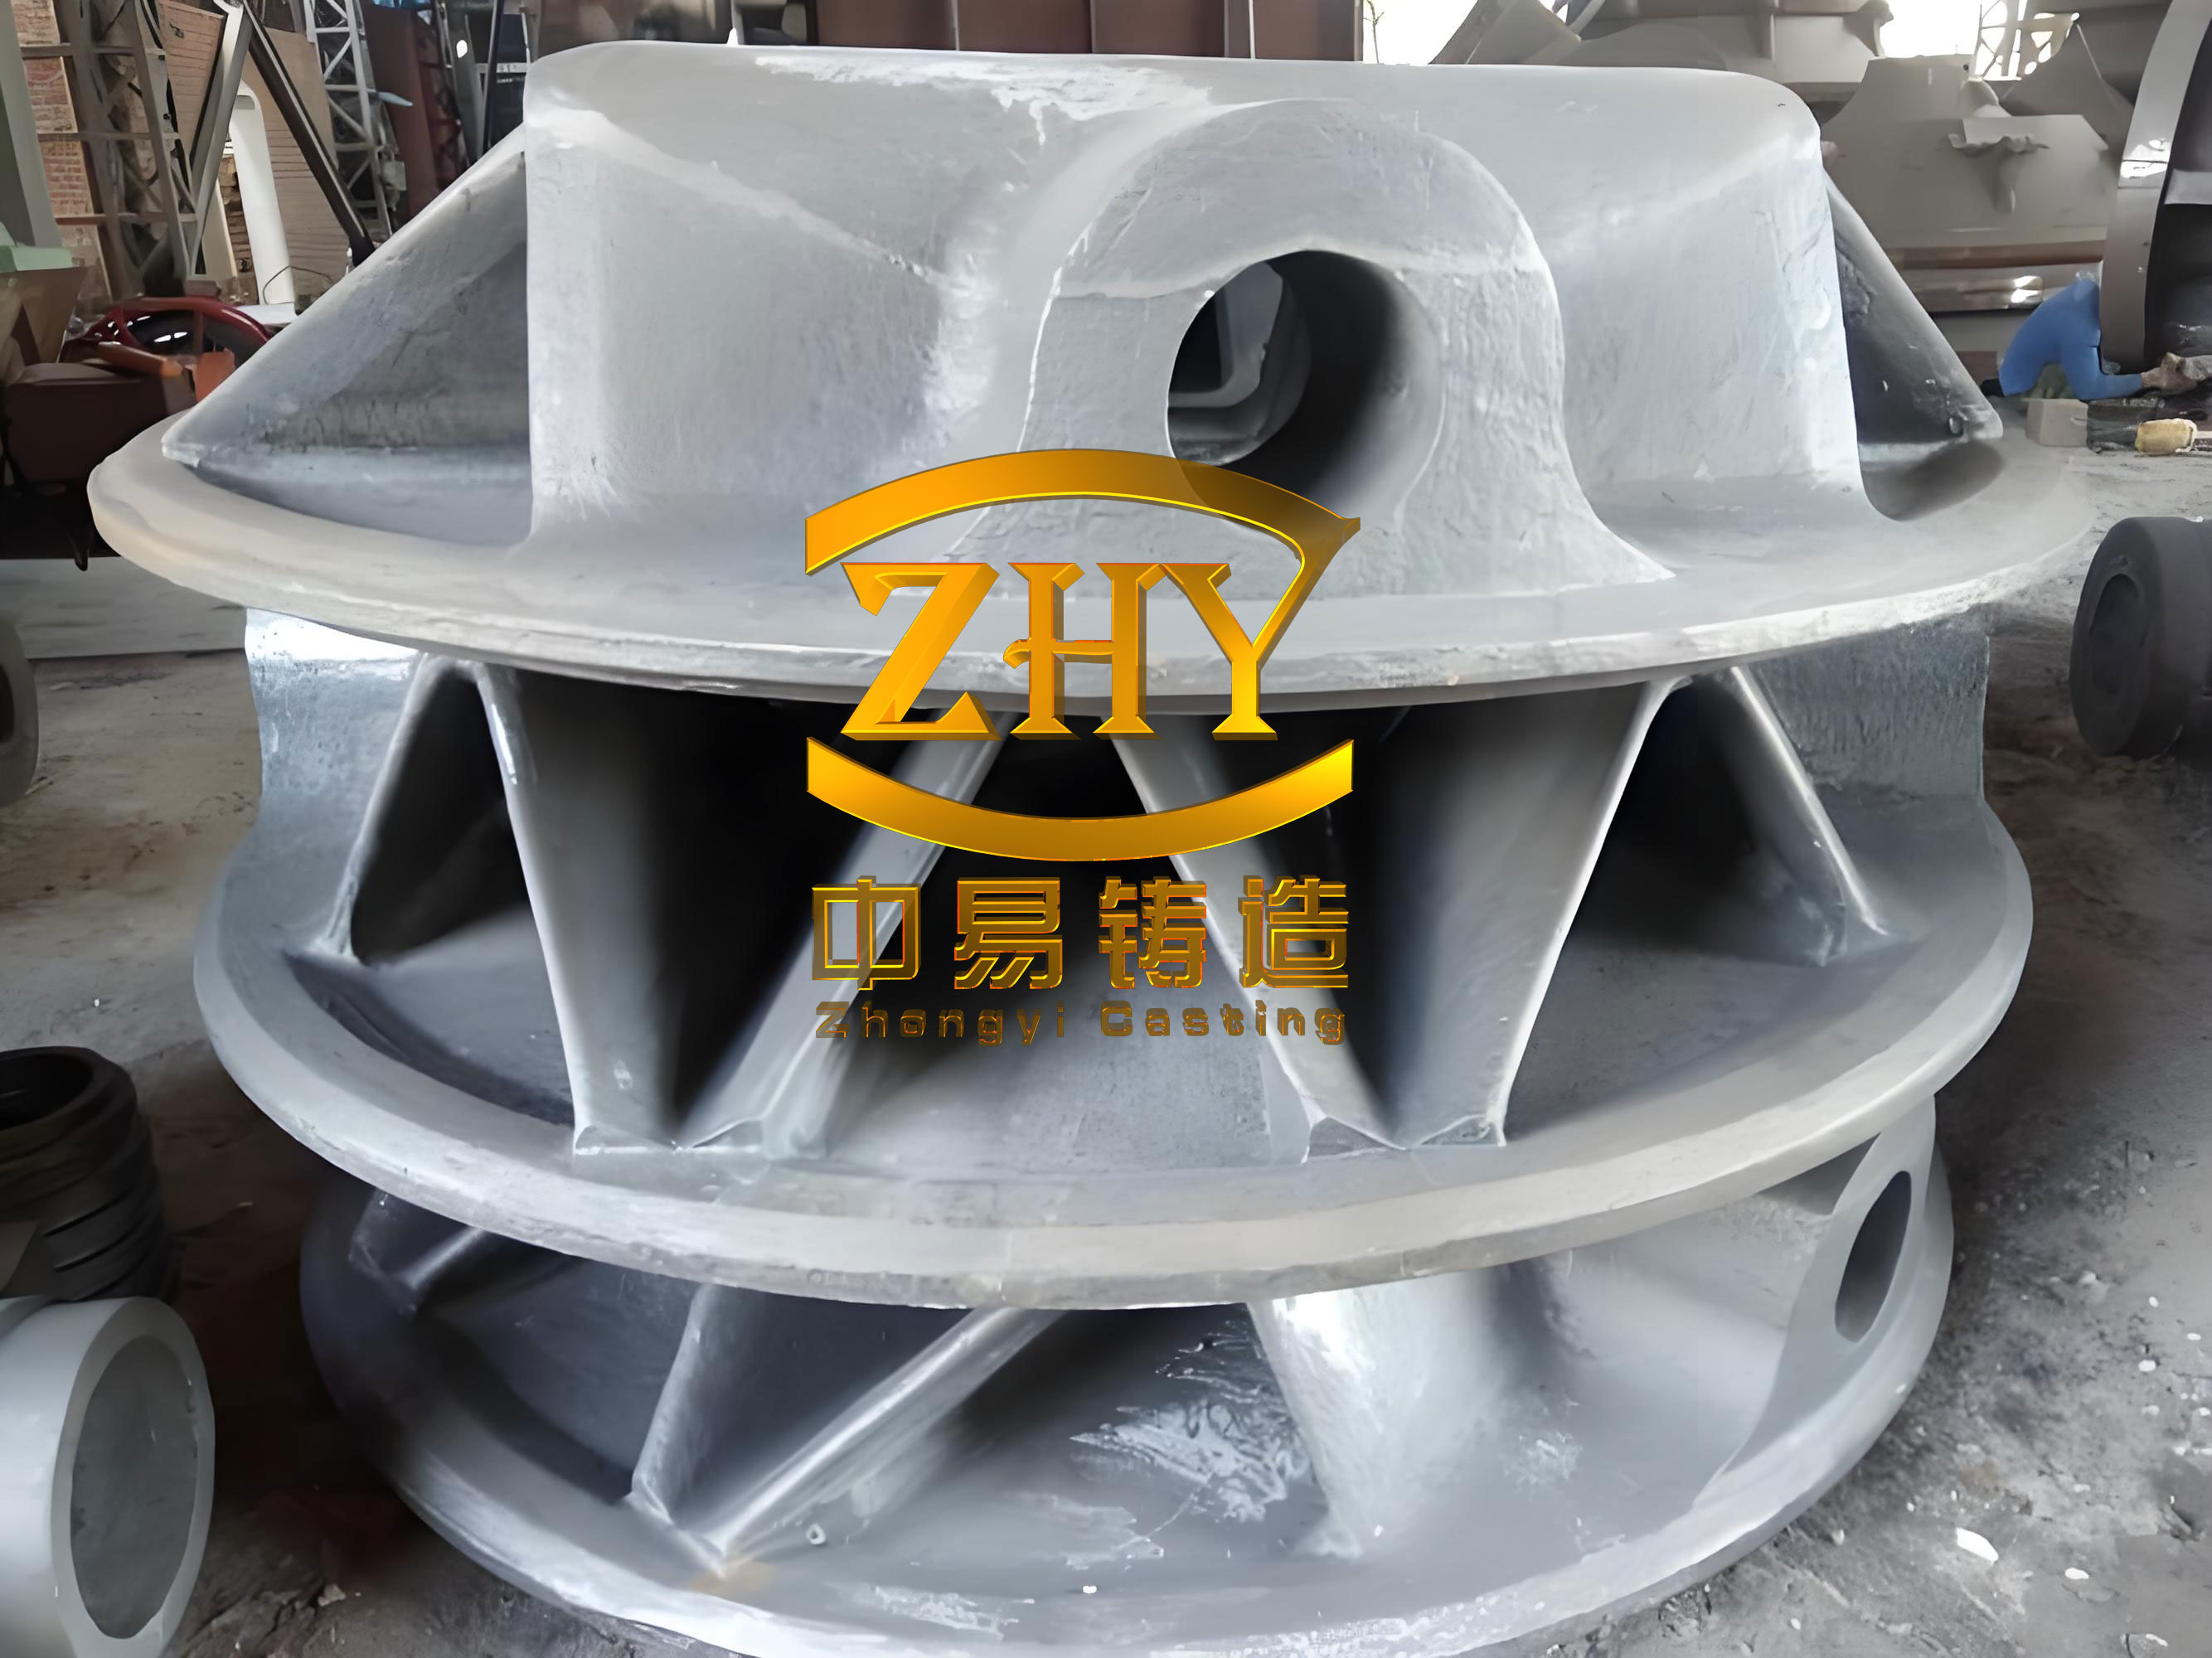
The production environment was a horizontal flaskless green-sand molding line. Cores were made in the hot-box process. Melting was done in a medium-frequency induction furnace. The mold box available for this project measured 700 mm × 600 mm × 250 mm/250 mm, and the layout used one casting per mold. Because the line is automatic, the riser design, gating system, and mold filling behavior had to be stable enough for mass production. I therefore spent considerable time analyzing the thermal centers, calculating the solidification modulus, and testing different riser arrangements before finalizing the process.
Ductile iron castings are notorious for shrinkage defects even though the precipitation of graphite during eutectic solidification is accompanied by volume expansion. The graphitization expansion can partly compensate for liquid contraction, but it also depends on the rigidity of the mold, the carbon equivalent, the pouring temperature, the inoculation practice, and the geometry of the casting. In green-sand molds, mold wall movement can occur if the graphitization pressure is high and the mold is not sufficiently rigid. This mold wall movement can increase the feeding demand instead of reducing it. I therefore treated shrinkage prevention in ductile iron castings as a system-level problem that included riser sizing, gating design, melting practice, and process control.
The first decision concerned the parting line and the pouring position. The horizontal molding line made it convenient to set the parting at the middle of the flange of the cover. This allowed easy pattern withdrawal and easy correction of dimensional variations caused by mold shift or parting-line mismatch. For the same main reduction shell cover, I considered two pouring positions: the flat disc side upward, and the flat disc side downward.
When the disc side is upward, the casting is mainly in the drag and the gating system is essentially top-gated. The ferrostatic pressure is high, and the heavy section near the ingates receives hot metal at the beginning of filling. This favors gravity feeding and tends to reduce shrinkage defects in ductile iron castings. The main disadvantage is that the metal falls into the mold cavity and can erode the sand, creating sand inclusions and surface defects. The surface quality therefore becomes more difficult to control.
When the disc side is downward, the gating system is bottom-fed. The liquid iron fills the cavity quietly, so the surface quality is better and the risk of sand erosion is low. The disadvantage is that the upper part of the casting is higher in the cope and is filled later with cooler metal. The thermal centers in that upper region are difficult to feed. The shrinkage tendency is correspondingly greater. In my first trials, I evaluated both positions. The surface quality requirement was critical, and the upper thermal center could be compensated with properly designed risers. Therefore I chose the disc-down position and accepted the challenge of feeding the upper hot spot.
The following table compares the two pouring positions I evaluated.
| Aspect | Disc side upward | Disc side downward |
|---|---|---|
| Gating type | Top-gated, essentially gravity filling | Bottom-gated, quiet filling |
| Ferrostatic pressure | Relatively high | Moderate at upper sections |
| Feeding of heavy sections | Good, especially for lower hot spots | Poor for upper isolated hot spots |
| Surface defects from sand erosion | Higher risk | Lower risk |
| Shrinkage tendency | Lower in most cases | Higher at the top of the casting |
| Final selection for this product | Not selected | Selected after riser modifications |
After the pouring position was fixed, I performed a systematic hot-spot analysis. In foundry engineering, a structural hot spot is a geometrical region where the volume of metal is large compared with the cooling surface area. Such a region stores more heat, releases more heat during solidification, and therefore solidifies later than the surrounding areas. A process hot spot is created by the casting method itself, for example by the ingate, a riser contact, a core print, or a vent that adds extra metal to the original geometry. Both types of hot spots matter in ductile iron castings because the feeding demand at the last solidifying zone determines whether shrinkage defects will appear.
I used the classical solidification modulus concept. The modulus of a hot spot is defined as the ratio of volume to cooling surface area:
$$M = \frac{V}{A}$$
According to Chvorinov’s rule, the solidification time of a simple casting section is proportional to the square of the modulus:
$$t_s = B M^2$$
Here, B is a constant that depends on the molding material, the metal properties, and the interface heat-transfer conditions. For the same mold and metal, the section with the largest modulus has the longest solidification time. For a large flat plate of thickness a, the cooling occurs mainly through the two faces, so the modulus can be approximated as:
$$M = \frac{a}{2}$$
For the main wall of this casting, with a thickness of 7 mm, the modulus is approximately:
$$M_{7} = \frac{7}{2} = 3.5\ \text{mm}$$
For the local thick section of 37 mm, the modulus is approximately:
$$M_{37} = \frac{37}{2} = 18.5\ \text{mm}$$
The theoretical ratio of solidification times is therefore:
$$\frac{t_{s,37}}{t_{s,7}} = \left(\frac{M_{37}}{M_{7}}\right)^2 = \left(\frac{18.5}{3.5}\right)^2 \approx 28$$
This means the thickest part of these ductile iron castings would remain liquid about 28 times longer than the thin walls if it behaved as an isolated plate. In reality, the thin sections feed the thick sections, but the substantial difference in modulus explains why the local 37 mm thick areas are critical. If any of those areas are not properly fed, shrinkage cavities will form.
I identified two major structural hot spots in the main reduction shell cover. The first hot spot was at the lower disc boss, which is close to the ingate. The second and more severe hot spot was at the upper heavy section around the Ø125 mm cored hole. The upper hot spot was especially dangerous because it was filled late, it was located high in the cope, and it was isolated from the main mass of liquid metal after the ingates froze.
I also considered that an ingate itself creates a process hot spot. In the disc-down position, the ingate is placed against the lower boss. The ingate adds a large mass of metal directly beside the structural hot spot. If I simply poured through that ingate without feeding, the combination of the structural hot spot and the process hot spot would be larger than the original geometry. This would increase the local shrinkage tendency. I therefore needed not only to feed the original hot spot but also to avoid making it worse through poor gate placement.
The next table summarizes the hot-spot assessment.
| Hot spot | Location | Characteristics | Feeding action | Observed risk |
|---|---|---|---|---|
| Position 1 | Lower disc boss, near ingate | Moderate modulus; ingate creates a process hot spot | Hot riser placed at the ingate | Initially produced shrinkage porosity without a riser |
| Position 2 | Upper section around Ø125 mm cored hole | Isolated thermal center, filled late with cooler metal | Cold riser plus exothermic block | Initially produced surface sink and internal shrinkage |
For the first hot spot at the lower disc boss, I used a hot riser. A hot riser is a riser that is connected directly to the gating system and therefore receives fresh, hot liquid iron during filling. This keeps the riser hot for a longer time and improves feeding efficiency. I calculated that the hot-spot modulus at the lower boss required a riser with enough volume and enough modulus to outlast the solidification of the boss. Based on the geometry and multiple trials, I selected a cylindrical hot riser with a diameter of 55 mm and a height of 85 mm.
$$M_{\text{riser, position 1}} = 55\ \text{mm diameter}, \quad H = 85\ \text{mm}$$
The riser was placed directly at the ingate so that the process hot spot caused by the ingate would not create a separate shrinkage zone. The heavy liquid iron entering through the ingate passed near the riser base and kept it hot. This approach eliminated the lower-boss shrinkage defect. I confirmed by sectioning sample castings that no internal shrinkage porosity remained at that location.
The upper hot spot at position 2 was more challenging. I first attempted to use equalized solidification theory. That theory suggests that, in ductile iron castings, the expansion caused by graphite precipitation may compensate for shrinkage if the chemical composition is controlled correctly. Therefore, I made a trial without any riser at position 2. The result was immediate and clear: all castings showed surface shrinkage depressions and severe internal shrinkage porosity at the upper heavy section. The graphitization expansion alone was not sufficient to eliminate the feeding demand in this isolated thermal center.
I then tried a conventional cold riser near position 2. A cold riser, in this context, is a riser that is not directly fed by the gating system. It relies on the liquid metal that enters the riser during mold filling and on the thermal balance after filling. The cold riser is often colder than the hottest part of the casting because the casting is filled before the riser receives enough hot metal. If the riser freezes before the hot spot, it cannot feed the shrink-age.
For this reason, I chose a large cold riser with a diameter of 80 mm and a height of 110 mm. I intentionally selected the riser modulus to be about two times the modulus of the hot spot:
$$M_{\text{riser}} \approx 2 M_{\text{hot spot}}$$
I also offset the riser neck, moving it a little away from the exact thermal center, in order to avoid adding more metal to the hot spot and increasing its modulus. This is an important detail in ductile iron castings because a riser neck that is too large may create a process hot spot larger than the original one.
When I ran the process with this ordinary cold riser, the defect frequency was reduced but not eliminated. About 20% of the castings still showed shrinkage porosity at position 2. The failure showed that the cold riser body was solidifying too early, or the riser neck was freezing before the thermal center was completely solid. The upper hot spot was still the last to receive feed metal. Simply making the riser larger was not attractive because the available space in that area was limited and a larger riser could interfere with the cored Ø125 mm hole and the mold assembly.
I therefore looked for a way to extend the effective solidification time of the cold riser without increasing its physical size. The solution was to place an exothermic block inside the cold riser cavity. The exothermic block releases heat through an exothermic chemical reaction after the mold is filled. This heat raises the temperature of the riser metal and slows its solidification. In effect, the exothermic block increases the thermal modulus of the riser.
I placed a Ø80 mm cold riser inside the upper circular area near the Ø125 mm hole. The riser neck was formed by the sand core, and the geometry created what foundry engineers call a sharp-sand effect. The sharp sand wedge at the riser neck has a reduced heat-absorbing mass behind it. It becomes heat-saturated quickly, so it dissipates heat more slowly than a plain wall. This slow cooling helps keep the riser neck in the liquid state for a longer time. As long as the riser neck remains open, the liquid metal in the riser can continue to feed the solidifying thermal center. By combining the sharp-sand neck and the exothermic block, I achieved local directional solidification at position 2. The hot spot remained connected to the liquid riser supply until the end of solidification.
The following table shows the observed improvement at the upper hot spot after each process change.
| Trial condition | Riser arrangement | Result at position 2 |
|---|---|---|
| Trial A | No riser | Surface sink and internal shrinkage in all castings |
| Trial B | Ordinary cold riser Ø80 mm × 110 mm, neck offset | Shrinkage defect in about 20% of castings |
| Trial C | Cold riser Ø80 mm × 110 mm with exothermic block and sharp-sand neck | No shrinkage defect; stable in mass production |
The final riser arrangement solved the most severe shrinkage problem in these ductile iron castings. It also reduced the dependence on manual skill because the exothermic block was placed in a defined position before mold closing and the rest of the process was automatic.
With the feeding strategy established, I turned my attention to the gating system. The available mold box was 700 mm × 600 mm × 250 mm/250 mm. I used one casting per mold. The gating system was a semi-closed, semi-open system. This means that the sprue is the restrictive element, but the runner and ingates are gradually opened to reduce the metal velocity and to avoid pressure surges. I designed the ingates so that the cross-sectional areas followed the ratio:
$$\Sigma S_{\mathrm{sprue}} : \Sigma S_{\mathrm{runner}} : \Sigma S_{\mathrm{ingate}} = 1 : 1.15 : 1.3$$
This ratio is typical for ductile iron castings produced on automatic green-sand molding lines. It provides a stable filling rate and reduces the risk of aspiration, sand erosion, and dross formation.
I also used two ingates rather than one. Two ingates distribute the incoming liquid iron over a wider area and reduce local heating of the mold. This is beneficial because concentrated ingate heat can create process hot spots that increase shrinkage. The two ingates were positioned so that one of them served the lower hot-spot area, and both together reduced the temperature gradient across the casting.
A foam ceramic filter was placed in the gating system. The filter size was 60 mm × 60 mm × 15 mm, with a pore density of 10 PPI (pores per inch). The filter removed inclusions and controlled the initial metal flow. In ductile iron castings, the filter also helps to reduce turbulence and prevent the re-oxidation of magnesium, which can otherwise form dross and oxide films.
The following table summarizes the gating and mold parameters used in mass production.
| Parameter | Value |
|---|---|
| Molding process | Horizontal flaskless green-sand line |
| Mold box size | 700 mm × 600 mm × 250 mm / 250 mm |
| Cavities per mold | 1 |
| Core making | Hot-box process |
| Gating ratio | 1 : 1.15 : 1.3 |
| Filter | 60 mm × 60 mm × 15 mm, 10 PPI foam ceramic |
| Number of ingates | 2 |
| Riser at lower hot spot | Hot riser Ø55 mm × 85 mm |
| Riser at upper hot spot | Cold riser Ø80 mm × 110 mm with exothermic block |
Melting and metallurgical control were equally important. I realized that a geometrically perfect riser system could not succeed if the liquid iron chemistry and inoculation were not optimized. Shrinkage defects in ductile iron castings are strongly affected by the carbon equivalent, residual magnesium, sulfur content, and inoculation quality.
The charge consisted of 35% returns and 65% clean steel scrap. Graphite was added in the furnace as a recarburizer to adjust the carbon content. This high-steel charge is common for ductile iron production because it gives low residual elements and better control of matrix structure. However, it also tends to produce more shrinkage if the inoculation is not sufficient. I therefore added 0.6% to 0.8% silicon carbide in the later stage of the furnace melt. The silicon carbide promotes graphite nucleation and reduces undercooling. It also helps to create a more homogeneous liquid iron and to minimize chill.
Spheroidization was performed in the ladle using a magnesium treatment process. I was careful to control the spheroidizer addition because excess residual magnesium increases the shrinkage tendency in ductile iron castings. The target for residual magnesium was 0.03% to 0.05%. Rare-earth residual was controlled below 0.03%. Sulfur was controlled below 0.02% to obtain efficient magnesium recovery and good nodularity.
Inoculation was carried out in two steps. The first inoculation was added into the ladle during spheroidization. The second was a stream inoculation during pouring. The total amount of inoculant was 1% of the liquid iron weight. This dual inoculation practice improves the nodule count and increases the number of graphite nuclei. A high nodule count is important for reducing shrinkage because the graphite precipitates in a more dispersed way and the eutectic solidification is less pasty.
The carbon equivalent was targeted at:
$$CE = 4.55\% \pm 0.05\%$$
I calculated the carbon equivalent using the common cast-iron formula:
$$CE = C + \frac{1}{3}(Si + P)$$
The chemical composition after spheroidization was controlled according to the following table.
| Element | Mass fraction, % |
|---|---|
| C | 3.65 – 3.80 |
| Si | 2.55 – 2.80 |
| Mn | < 0.30 |
| P | < 0.06 |
| S | < 0.02 |
| RE | < 0.03 |
| Mg | 0.03 – 0.05 |
The carbon equivalent in these ductile iron castings was kept close to the eutectic composition. This reduces the liquid-to-solid contraction and increases the graphitization expansion. A near-eutectic liquid iron also has better fluidity, which helps to fill thin sections and improve feeding.
Pouring temperature is another critical variable. I found the optimum pouring temperature range for this product to be 1380 °C to 1400 °C. If the pouring temperature is too high, the liquid iron holds more heat, the total contraction increases, and the shrinkage tendencies become more severe. If the pouring temperature is too low, the metal may lose fluidity before filling thin sections, and the upper hot spot may be so cold that even the exothermic riser cannot feed it properly. The controlled pouring temperature range helped maintain a uniform thermal field in the mold and improved the reliability of the riser system.
The table below summarizes the melting and pouring parameters I used.
| Parameter | Control value |
|---|---|
| Charge materials | 35% returns + 65% steel scrap |
| Silicon carbide addition | 0.6% – 0.8% in late furnace melt |
| Spheroidizer addition | Controlled to obtain residual Mg 0.03% – 0.05% |
| Total inoculant | 1.0% of liquid iron weight |
| Carbon equivalent target | 4.55% ± 0.05% |
| Pouring temperature | 1380 °C – 1400 °C |
I also used the Niyama criterion as a diagnostic tool during the development trials. The Niyama criterion is based on the thermal gradient and cooling rate at the end of solidification:
$$N_y = \frac{G}{\sqrt{\dot{T}}}$$
Here, G is the local temperature gradient and \(\dot{T}\) is the cooling rate. A low Niyama value at the centerline or at the thermal center indicates a higher risk of micro-porosity. In ductile iron castings, the critical value is not universal, but the criterion helped me to understand why the upper hot spot was failing. The ordinary cold riser gave a low Niyama value at the hot spot. After the exothermic block was added, the thermal gradient near the hot spot improved dramatically because the riser stayed liquid and maintained a temperature difference between the feeding path and the solidifying section.
Another important consideration was the mold rigidity. For ductile iron castings, graphitization expansion creates internal pressure during solidification. If the mold wall moves outward, this expansion energy is absorbed by the mold and cannot be used for feeding. Green-sand molds are less rigid than chemically bonded sand molds. I therefore controlled the mold compaction and sand properties to achieve good mold hardness. This is often forgotten in shrinkage analysis, but it is one of the reasons why the same casting can be sound in a furan sand mold and defective in a green-sand mold. In this project, the horizontal molding line produced molds with adequate hardness, and I made sure that the venting and ramming were uniform around the risers and the upper hot spot.
During the first production runs, I inspected the castings by macro-etching and sectioning at the critical hot spots. The lower boss section showed sound metal after the hot riser was installed. The upper hot-spot section remained sound only when both the exothermic block and the sharp-sand riser neck were present. When either condition was missing, the defect returned. This confirmed that the combination of geometry and thermal control was responsible for the success.
The final process was stable over many production batches. The shrinkage defects disappeared entirely from the casting quality records. The process also became more tolerant to normal variations in pouring temperature, sand temperature, and inoculation because the riser system had a safety margin. This is exactly what is needed for mass production of ductile iron castings on an automatic molding line.
In summary, I learned several important lessons from this development. First, the choice of pouring position has a decisive effect on both appearance and feeding. For this main reduction shell cover, the disc-down position was chosen because it provided the required surface quality, but it forced me to solve a difficult upper hot spot. Second, the ingate itself can become a process hot spot, so it must be considered together with the structural hot spot. Placing a hot riser at the ingate eliminated the lower-boss shrinkage. Third, an isolated upper hot spot may not be saved by an ordinary cold riser if the riser freezes too early. The use of an exothermic block combined with a sharp-sand riser neck created local directional solidification and solved the last remaining defect.
Finally, metallurgical control is inseparable from geometrical design. The combination of near-eutectic carbon equivalent, controlled residual magnesium, strong inoculation, silicon carbide addition, and a pouring temperature range of 1380 °C to 1400 °C made the ductile iron castings more tolerant to solidification shrinkage. Every one of these elements contributes to the soundness of ductile iron castings. Riser calculations and gating formulas are necessary, but they are not sufficient. The result of this project was a reliable and repeatable process for producing high-quality ductile iron castings with no shrinkage defects.
For foundry engineers working on similar ductile iron castings, I recommend the following approach. Start with a careful hot-spot analysis using the modulus concept. Remember that process hot spots created by ingates and riser necks can be as dangerous as structural hot spots. Design the riser not only for the size of the hot spot but also for its continuity with the liquid supply. If a cold riser is unavoidable, do not hesitate to use an exothermic block or an insulating sleeve. Pay attention to the sharp-sand effect at the riser neck, because a small geometrical detail can make a large difference in feeding behavior. And above all, control the liquid iron composition and pouring temperature within tight limits.
The successful production of this main reduction shell cover demonstrates that sound ductile iron castings can be produced on a high-pressure green-sand molding line if the casting engineer treats the process as a complete system. Shrinkage defects are not inevitable. They are the result of an imbalance between volume contraction, heat transfer, mold rigidity, and feeding capacity. When those factors are brought into balance, the result is stable production, low scrap, and reliable ductile iron castings.