
Rare earth magnesium alloys, particularly the WE43A composition, have become essential structural materials in aerospace, automotive, and defence industries because of their high specific strength, high specific stiffness, and excellent elevated-temperature properties. In my study, the focus is placed on the characterization of casting defects and their influence on the mechanical performance and corrosion resistance of WE43A rare earth magnesium alloy. I systematically investigated three major categories of casting defect: porosity, inclusions, and segregation. Through controlled foundry experiments, X-ray non-destructive inspection, and fracture surface analysis, I prepared samples with five porosity grades, five inclusion grades, and eight segregation grades. The present article summarizes the defect morphologies, quantitative defect area statistics, tensile properties, fatigue behaviour, fatigue life prediction models, and corrosion resistance of specimens containing different levels of casting defect.
1. Introduction and Background
Casting defect formation is one of the most important factors controlling the reliability of rare-earth magnesium alloy components. WE43A alloy, with a nominal composition of Y, Nd, Zr, and Gd, offers excellent mechanical properties after proper heat treatment. However, during the casting process, the high chemical activity of magnesium favours oxidation, gas entrapment, and micro-segregation. These phenomena can lead to various casting defects such as porosity, oxide inclusions, and compositional segregation. Even a small amount of casting defect can locally reduce the load-bearing cross-section, introduce stress concentration, and accelerate fatigue crack initiation. Therefore, understanding the exact role of each casting defect type on the final performance of WE43A alloy is of great theoretical and practical importance.
In my work, I investigated whether different casting defect levels can be quantitatively linked to changes in tensile strength, ductility, fatigue life, fatigue limit, and corrosion current density. The results show that the severity of casting defect is not only reflected by the defect area fraction on the fracture surface but also by the failure mechanism observed in the scanning electron microscope. For example, porosity is a volume defect that directly reduces the effective area, while inclusions act as brittle particles that can debond from the matrix, and segregation creates brittle intermetallic networks along grain boundaries. These casting defects have different influences, and their ranking is important for the quality control of rare-earth magnesium alloy castings.
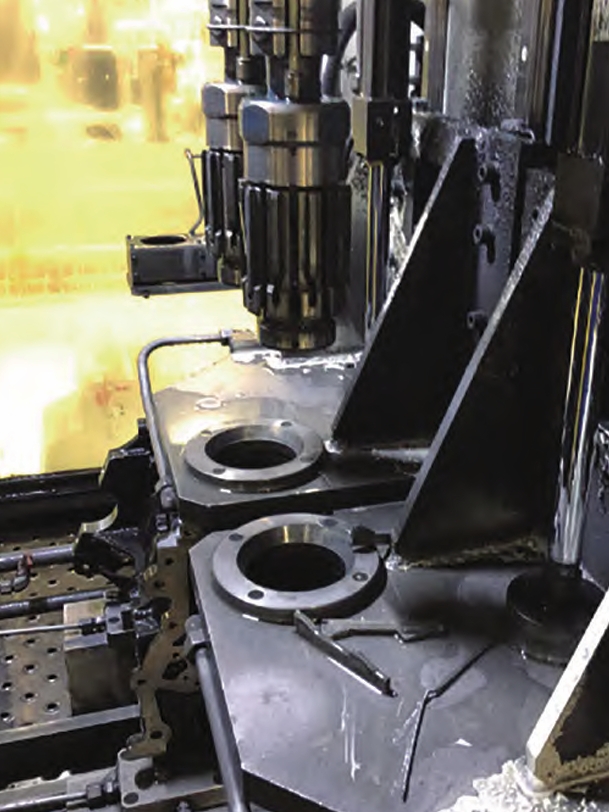
The image above illustrates a typical magnesium alloy component used in an engine cylinder block. Such cast components are often required to withstand cyclic loads and corrosive environments. Therefore, the presence of casting defect in these components must be carefully evaluated. My study is designed to provide a quantitative basis for defect acceptance criteria and fatigue life assessment of WE43A rare earth magnesium alloy castings.
2. Material and Experimental Methods
The material used in this study is WE43A rare earth magnesium alloy. The chemical composition is given in Table 1. The alloy was molten at approximately 750 °C and cast into moulds. Different casting parameters, including degassing conditions, inclusion content, rare-earth element concentration, and cooling rates, were adjusted to obtain samples with different casting defect grades. The defect grades were verified by X-ray non-destructive inspection according to the relevant magnesium alloy casting specification.
| Y | Nd | Zr | Gd | Mg |
|---|---|---|---|---|
| 3.7–4.3 | 2.0–2.5 | 0.40–1.0 | 0.4–0.6 | Balance |
For microstructure observation, specimens were ground with silicon carbide papers from 400 to 2000 grit, polished with 1.5 µm diamond paste, and then etched with 10 % citric acid for about 15 seconds. Metallographic observation was performed using an optical microscope, and fracture surfaces were examined using scanning electron microscopy. An energy-dispersive spectrometer was used for local composition analysis. X-ray diffraction was used for phase identification. The defect areas on fracture surfaces were measured by ImageJ software, and the surface defect fraction was calculated by dividing the total defect area by the fracture area.
Tensile tests were conducted on cylindrical specimens with a diameter of 5.00 mm and a gauge length of 25 mm, using a universal testing machine. The tensile strain rate was set to 0.00025 s⁻¹. Four-point bending fatigue tests were conducted on plate specimens with a thickness of 7.4 mm, width of 21.0 mm, and length of 82.2 mm. The loading rollers had a diameter of 10 mm. The mean stress was 100 MPa, the loading frequency was 20 Hz, and the stress amplitude started at 50 MPa. The fatigue limit was determined by a step-loading method, with each load level maintained for 500,000 cycles. Electrochemical corrosion tests were performed in a 3.5 wt.% NaCl solution using a CHI600C electrochemical workstation. A saturated calomel electrode was used as the reference electrode, platinum as the counter electrode, and the specimen as the working electrode. Potentiodynamic polarization curves were recorded in the potential range from -1.9 V to -1.1 V at a scan rate of 1 mV/s.
3. Effect of Porosity Casting Defect on Mechanical Properties
3.1 Porosity Morphology and Quantitative Area Statistics
In this study, porosity is one of the most severe casting defects in rare-earth magnesium alloys. The macroscopic appearance of porosity on the fracture surface was uneven and irregular. Unlike inclusions, porosity appears as voids or cavities, and it is usually located at grain boundaries. The microscopic morphology of porosity was characterized by black, irregular strip-like holes and ellipsoidal cavities. These cavities existed mainly along the grain boundaries, which is typical for solidification shrinkage porosity. The irregular distribution of porosity indicates insufficient liquid feeding during solidification.
| Porosity grade | Defect area mean (µm²) | Surface porosity fraction (%) |
|---|---|---|
| S1 | 1,220,112.39 | 0.83 |
| S2 | 3,131,143.22 | 2.13 |
| S3 | 8,364,366.74 | 5.69 |
| S4 | 31,208,128.55 | 21.23 |
| S5 | 44,879,111.65 | 30.53 |
As the porosity casting defect grade increased from S1 to S5, the surface porosity fraction increased monotonically. This quantitative relationship confirms that the fracture surface defect area can be used as a reliable indicator for the casting defect severity. In my analysis, the equivalent diameter of porosity was also calculated from the measured area using the following relation:
$$A = \frac{\pi d^2}{4}$$
Thus, the equivalent diameter is obtained as:
$$d = \sqrt{\frac{4A}{\pi}}$$
For the porosity grades S1 to S5, the calculated equivalent diameters are given in Table 3.
| Porosity grade | Equivalent diameter (mm) |
|---|---|
| S1 | 0.512 |
| S2 | 0.685 |
| S3 | 0.987 |
| S4 | 1.253 |
| S5 | 1.571 |
3.2 Effect of Porosity on Tensile Properties
Table 4 presents the tensile properties of WE43A specimens with different porosity casting defect grades. It is evident that porosity has a strong influence on ultimate tensile strength and elongation. When the porosity grade was S1, the tensile strength dropped only slightly from 280 MPa to 261 MPa. However, when the porosity grade exceeded S1, both strength and ductility decreased significantly. At S5, the tensile strength decreased by about 70 %. The engineering stress-strain response indicates that porosity reduces the effective load-bearing cross-section and promotes local stress concentration, leading to earlier fracture.
| Grade | Tensile strength (MPa) | Yield strength (MPa) | Elongation (%) | Reduction of area (%) | Elastic modulus (GPa) |
|---|---|---|---|---|---|
| W | 280 | 180 | 4.50 | 4.50 | 45.00 |
| S1 | 261 | 182 | 4.26 | 4.21 | 44.52 |
| S2 | 201 | 148 | 2.48 | 2.52 | 44.78 |
| S3 | 194 | 138 | 2.51 | 2.31 | 45.44 |
| S4 | 161 | 135 | 2.44 | 2.03 | 44.31 |
| S5 | 82 | 68 | 2.63 | 2.79 | 45.69 |
The maximum reduction proportions caused by porosity are summarized in Table 5. The elastic modulus remained almost unchanged with increasing porosity casting defect, indicating that the intrinsic atomic bonding stiffness was not affected. In contrast, the strength and ductility decreased substantially because porosity increases the effective crack length and reduces the energy required for crack propagation.
| Property | Maximum reduction (%) |
|---|---|
| Tensile strength | 70.71 |
| Yield strength | 62.22 |
| Elongation | 44.89 |
| Reduction of area | 54.89 |
| Elastic modulus | 1.53 |
Fractographic observation of tensile specimens containing porosity casting defect revealed brittle fracture characteristics. The fracture surfaces exhibited cleavage planes and decohesion steps, which are typical for magnesium alloys with a hexagonal close-packed structure. The limited number of active slip systems at room temperature restricts plastic deformation, and porosity acts as an internal stress raiser, thus further increasing brittleness.
3.3 Effect of Porosity on Fatigue Properties
Fatigue tests were performed using the four-point bending method. Table 6 summarizes the fatigue life and fatigue limit as functions of porosity casting defect grade. The fatigue life of the defect-free specimen was 2,506,109 cycles, and the fatigue limit was 42 MPa. When porosity grade S1 was present, the fatigue life dropped by about 36 %. The decline rate was initially rapid and then gradually slowed down as the porosity casting defect grade increased.
| Porosity grade | Fatigue life (cycles) | lg (fatigue life) | Fatigue limit (MPa) |
|---|---|---|---|
| W | 2,506,109 | 6.399 | 42.0 |
| S1 | 363,915 | 5.561 | 35.0 |
| S2 | 138,627 | 4.994 | 30.3 |
| S3 | 68,076 | 4.833 | 29.2 |
| S4 | 44,463 | 4.648 | 27.0 |
| S5 | 39,445 | 4.596 | 26.0 |
The fatigue life decreased monotonically with the porosity casting defect level. The maximum reduction in lg(fatigue life) was about 28 %, while the maximum reduction in fatigue limit was about 38 %. The fatigue fracture surface showed that the crack initiated from the porosity casting defect near the surface. The crack propagation region was relatively flat, while the final fracture region was characterized by cleavage facets. This confirms that porosity casting defect acts as a pre-existing crack and significantly reduces the crack initiation period.
3.4 Fatigue Life Prediction Based on Paris Equation
In my research, I used linear elastic fracture mechanics to correlate the fatigue life with the initial crack size, which is related to the porosity casting defect. The Paris equation can be written as:
$$\frac{da}{dN} = c \left(\Delta K\right)^n$$
where c and n are material constants, and the stress intensity factor range is:
$$\Delta K = Y \Delta\sigma \sqrt{\pi a}$$
By integrating the Paris equation from the initial crack size \(a_0\) to the critical crack size \(a_c\), the fatigue life can be expressed as:
$$N_c = \int_{a_0}^{a_c} \frac{da}{c \left(Y \Delta\sigma \sqrt{\pi a}\right)^n}$$
After integration, the fatigue life is given by:
$$N_c = \frac{1}{\left(n-2\right)cY^n\Delta\sigma^n\pi^{n/2}} \left(\frac{1}{a_0^{(n-2)/2}} – \frac{1}{a_c^{(n-2)/2}}\right)$$
For a fixed material and loading condition, the above equation can be simplified to:
$$N_c = B\left(\frac{1}{a_0^{(n-2)/2}} – D\right)$$
In this expression, \(B\) combines all the constant parameters, and \(D\) is related to the critical crack size. For WE43A magnesium alloy, the fatigue crack growth exponent \(n\) was taken as 3. By fitting the experimental data, the relationship between the equivalent diameter \(d\) and fatigue life was obtained as:
$$N_c = 516588.3\left(\frac{1}{d^{0.5}} – 0.8073\right)$$
The coefficient of determination \(R^2\) for this fitting was 0.8468, indicating good agreement. The fatigue limit can also be estimated from the S-N curve expression:
$$S = S_L \left[H + A_2 \left(N + C_2\right)^{-B_2}\right]$$
where \(H=1\), \(A_2=25.7\), \(B_2=0.32\), and \(C_2=47.3\). Substituting the fatigue life relation into the S-N equation yields:
$$S_L = \frac{150}{1 + 25.7 \times \left(A_3 a_0^{-0.5} – C_3\right)^{-0.32}}$$
The fitting result for fatigue limit versus equivalent diameter is shown by the equation:
$$S_L = \frac{150}{1 + 25.7 \times \left(582.5 d^{-0.5} – 285\right)^{-0.32}}$$
The coefficient of determination \(R^2\) for this prediction was 0.9134. This model provides a practical method to evaluate the fatigue performance of rare-earth magnesium alloy castings with known porosity casting defect grades, avoiding expensive and time-consuming fatigue tests for every possible defect condition.
4. Effect of Inclusion Casting Defect on Mechanical Properties
4.1 Inclusion Morphology and Quantitative Area Statistics
Inclusions are another common type of casting defect in rare-earth magnesium alloys. In my study, the microscopic inclusions were mainly black, spherical or ellipsoidal particles distributed in the magnesium matrix. The macroscopic inclusions appeared as black irregular areas on the fracture surface. Energy-dispersive X-ray spectroscopy showed that the main component of the macro-inclusions was magnesium oxide, which formed because of the high chemical affinity of magnesium with oxygen during melting and pouring.
| Inclusion grade | Defect area mean (µm²) | Surface inclusion fraction (%) |
|---|---|---|
| J1 | 118,078.55 | 0.08 |
| J2 | 350,346.47 | 0.24 |
| J3 | 1,411,829.58 | 0.96 |
| J4 | 8,669,714.67 | 5.60 |
| J5 | 10,255,631.33 | 6.97 |
The surface inclusion fraction increased from 0.08 % to about 6 % with increasing inclusion casting defect grade. Although the area fraction is smaller than that of porosity, inclusions are still important because they are brittle and poorly bonded to the matrix. During tensile deformation, inclusions can crack or debond, creating voids that reduce ductility and fatigue resistance.
4.2 Effect of Inclusion on Tensile Properties
The tensile properties of specimens with different inclusion casting defect grades are given in Table 8. Compared with porosity, inclusions had a weaker influence on tensile strength. The ultimate tensile strength only decreased by about 9 %, and the yield strength by about 8 %. However, the elongation decreased markedly, with a maximum reduction of about 60 %. This indicates that inclusions are more detrimental to ductility than to strength.
| Grade | Tensile strength (MPa) | Yield strength (MPa) | Elongation (%) | Reduction of area (%) | Elastic modulus (GPa) |
|---|---|---|---|---|---|
| W | 236 | 182 | 3.59 | 3.79 | 47 |
| J1 | 221 | 176 | 2.62 | 1.99 | 44 |
| J2 | 214 | 167 | 2.75 | 2.73 | 42 |
| J3 | 222 | 172 | 1.46 | 2.23 | 44 |
| J4 | 215 | 169 | 1.41 | 2.32 | 43 |
| J5 | 224 | 172 | 1.59 | 1.83 | 44 |
Fracture surfaces of tensile specimens containing inclusion casting defect showed typical transgranular fracture. Cracks were often observed near inclusions, and some inclusions were pulled out, leaving shallow dimples or cavities. The weak interface between the oxide inclusion and the magnesium matrix is responsible for the earlier crack initiation. The overall fracture mode remained brittle, but the crack path was more tortuous compared with porosity-induced fracture.
4.3 Effect of Inclusion on Fatigue Properties
Table 9 presents the fatigue life and fatigue limit for different inclusion casting defect grades. In the absence of inclusions, the fatigue life was 4,972,069 cycles. With increasing inclusion grade, the fatigue life decreased steadily. At grade J5, the fatigue life was 54,441 cycles, and the fatigue limit decreased from 42 MPa to 28 MPa.
| Inclusion grade | Fatigue life (cycles) | lg (fatigue life) | Fatigue limit (MPa) |
|---|---|---|---|
| W | 4,972,069 | 6.399 | 42.0 |
| J1 | 290,569 | 5.463 | 34.0 |
| J2 | 138,481 | 5.141 | 30.3 |
| J3 | 147,547 | 5.168 | 31.5 |
| J4 | 77,665 | 4.890 | 28.8 |
| J5 | 54,441 | 4.735 | 28.0 |
It is interesting to note that although the tensile strength was only slightly affected by inclusions, the fatigue life decreased substantially. This is because fatigue loading is very sensitive to local stress concentrations. Each inclusion casting defect acts as a potential fatigue crack initiation site under cyclic loading. Once a crack nucleates at an inclusion, it propagates under repeated stress until final fracture. Fatigue fracture observations confirmed the presence of inclusions at the crack origin, followed by a stable crack growth region with fatigue striations and a final rapid fracture region with cleavage facets.
5. Effect of Segregation Casting Defect on Mechanical and Corrosion Properties
5.1 Segregation Morphology and Quantitative Area Statistics
Segregation is a casting defect characterized by non-uniform distribution of alloying elements. In my study, the segregation structure in WE43A rare earth magnesium alloy was mainly composed of a continuous network of Mg₄₁Nd₅ phase and smaller granular Mg₂₄Y₅ phase. The segregated eutectic phases were predominantly located at grain boundaries. Energy-dispersive spectroscopy mapping confirmed that Nd was enriched in the continuous network, while Y appeared as fine particles within the α-Mg matrix.
| Segregation grade | Defect area mean (µm²) | Surface segregation fraction (%) |
|---|---|---|
| PX1 | 1,014,301.32 | 0.69 |
| PX2 | 5,277,336.88 | 3.59 |
| PX3 | 8,320,209.74 | 5.66 |
| PX4 | 11,054,447.03 | 7.52 |
| PX5 | 15,920,111.53 | 10.83 |
| PX6 | 26,548,296.84 | 18.06 |
| PX7 | 35,838,646.61 | 24.38 |
| PX8 | 38,425,867.97 | 26.14 |
The surface segregation fraction increased from about 0.69 % to more than 26 % as the segregation casting defect grade increased. The presence of brittle eutectic networks along grain boundaries weakens the grain boundary cohesion and provides a preferential path for crack propagation.
5.2 Effect of Segregation on Tensile Properties
Table 11 shows the tensile properties of specimens with different segregation casting defect grades. The yield strength remained almost unchanged for most segregation grades, while the ultimate tensile strength decreased significantly at high segregation levels. The elongation and reduction of area dropped dramatically, with maximum reductions of about 81 % and 89 %, respectively. At grade PX8, the material fractured before yielding, and the tensile strength was equal to the yield strength at 139 MPa.
| Grade | Tensile strength (MPa) | Yield strength (MPa) | Elongation (%) | Reduction of area (%) | Elastic modulus (GPa) |
|---|---|---|---|---|---|
| W | 268 | 184 | 3.91 | 4.08 | 45 |
| PX1 | 246 | 181 | 2.92 | 3.53 | 45 |
| PX2 | 248 | 178 | 2.80 | 3.91 | 45 |
| PX3 | 237 | 179 | 1.80 | 2.97 | 46 |
| PX4 | 245 | 176 | 1.98 | 3.65 | 46 |
| PX5 | 206 | 189 | 1.36 | 1.67 | 47 |
| PX6 | 190 | 181 | 1.27 | 1.33 | 46 |
| PX7 | 189 | 179 | 1.14 | 1.32 | 46 |
| PX8 | 139 | 139 | 0.75 | 0.45 | 43 |
The tensile fracture surfaces of segregated specimens exhibited both transgranular and intergranular fracture features. Secondary cracks were observed near the segregated phase region. Because the Mg₄₁Nd₅ network is hard and brittle, it cannot accommodate plastic deformation. When the applied stress reaches a critical value, cracks initiate at the brittle phase and propagate along the grain boundaries, leading to a significant loss of ductility.
5.3 Effect of Segregation on Fatigue Properties
The fatigue properties of specimens with different segregation casting defect grades are listed in Table 12. The defect-free specimen had a fatigue life of 4,606,827 cycles and a fatigue limit of 42 MPa. At the lowest segregation grade PX1, the fatigue life decreased to 246,017 cycles, which is already more than one order of magnitude lower than the defect-free condition. The fatigue life continued to decrease with increasing segregation grade, reaching 29,337 cycles at PX8. The fatigue limit decreased by about 39 % at the highest segregation grade.
| Segregation grade | Fatigue life (cycles) | lg (fatigue life) | Fatigue limit (MPa) |
|---|---|---|---|
| W | 4,606,827 | 6.66 | 42.0 |
| PX1 | 246,017 | 5.39 | 33.7 |
| PX2 | 162,165 | 5.21 | 38.7 |
| PX3 | 117,128 | 5.07 | 30.9 |
| PX4 | 105,808 | 5.02 | 30.6 |
| PX5 | 97,957 | 4.99 | 30.3 |
| PX6 | 64,254 | 4.81 | 28.7 |
| PX7 | 53,028 | 4.72 | 27.9 |
| PX8 | 29,337 | 4.47 | 25.6 |
Fatigue fracture surface analysis showed that the fatigue crack initiated in the segregated region. The crack propagation region exhibited cleavage river patterns, and the final fracture region contained many secondary cracks associated with the brittle segregation network. The casting defect not only reduces the crack initiation life but also accelerates the crack growth rate by providing a low-energy intergranular fracture path.
5.4 Effect of Segregation on Corrosion Resistance
In addition to mechanical properties, I investigated the influence of segregation casting defect on the corrosion behaviour of WE43A alloy. Specimens with different segregation grades were immersed in a 3.5 wt.% NaCl solution for 12 hours. As the segregation casting defect grade increased, the localized corrosion area became larger and deeper. The corrosion morphology changed from slight pitting at PX1 to a thick and cracked corrosion product layer at PX8.
Potentiodynamic polarization tests were performed to obtain the corrosion potential and corrosion current density. The results are summarized in Table 13.
| Segregation grade | Corrosion potential (V vs SCE) | Corrosion current density (A/cm²) |
|---|---|---|
| PX1 | -1.573 | 2.090 × 10⁻⁵ |
| PX2 | -1.560 | 4.200 × 10⁻⁵ |
| PX3 | -1.545 | 8.500 × 10⁻⁵ |
| PX4 | -1.520 | 1.600 × 10⁻⁴ |
| PX5 | -1.498 | 3.200 × 10⁻⁴ |
| PX6 | -1.476 | 6.500 × 10⁻⁴ |
| PX7 | -1.451 | 9.800 × 10⁻⁴ |
| PX8 | -1.432 | 2.467 × 10⁻³ |
With increasing segregation casting defect grade, the corrosion potential shifted to more positive values, from -1.573 V to -1.432 V. This shift can be attributed to the increasing amount of Mg₂₄Y₅ and Mg₄₁Nd₅ phases, which have higher corrosion potentials than the α-Mg matrix. However, the corrosion current density increased significantly from \(2.090 \times 10^{-5}\) to \(2.467 \times 10^{-3}\) A/cm², spanning more than two orders of magnitude. Therefore, the corrosion rate increased dramatically, even though the corrosion potential became slightly nobler.
The corrosion mechanism of WE43A alloy in NaCl solution involves anodic dissolution of magnesium and cathodic oxygen reduction:
$$\text{Mg} \rightarrow \text{Mg}^{2+} + 2e^-$$
$$O_2 + 2H_2O + 4e^- \rightarrow 4OH^-$$
The dissolved Mg²⁺ ions react with OH⁻ to form Mg(OH)₂, which can then decompose into MgO:
$$\text{Mg(OH)}_2 \rightarrow \text{MgO} + H_2O$$
Energy-dispersive spectroscopy analysis of the corrosion products showed that the main products were MgO and MgCl₂. The presence of chloride ions destroys the partially protective surface film and accelerates localized corrosion. The segregation casting defect increases the galvanic coupling between the matrix and the secondary phases, resulting in a higher corrosion current density.
6. Comparative Discussion of Casting Defect Types
Based on my experimental results, it is useful to compare the influence of porosity, inclusion, and segregation casting defects on the tensile and fatigue properties of WE43A magnesium alloy. Table 14 summarizes the maximum reductions caused by each type of casting defect.
| Property | Porosity reduction (%) | Inclusion reduction (%) | Segregation reduction (%) |
|---|---|---|---|
| Tensile strength | 70 | 9 | 48 |
| Yield strength | 62 | 8 | 24 |
| Elongation | 41 | 60 | 81 |
| Reduction of area | 55 | 51 | 89 |
| Fatigue life (lg) | 28 | 26 | 33 |
| Fatigue limit | 38 | 33 | 39 |
It is evident that porosity casting defect has the strongest negative effect on tensile strength and yield strength because it directly removes load-bearing material and creates severe stress concentration. Inclusion casting defect is less harmful to strength but still strongly affects ductility and fatigue resistance. Segregation casting defect has the greatest influence on ductility and fatigue life because the continuous brittle network at grain boundaries destroys the coherence of the matrix.
7. Conclusions
In this work, I systematically characterized the casting defects in WE43A rare earth magnesium alloy and analysed their effects on tensile properties, fatigue properties, and corrosion resistance. The main conclusions are as follows:
First, porosity casting defect appears as irregular black strip-like and ellipsoidal cavities distributed along grain boundaries. The surface porosity fraction increases from about 0.8 % to 30 % as the porosity grade increases. The tensile strength and yield strength can be reduced by up to 70 % and 62 %, respectively. The fatigue life and fatigue limit are also significantly reduced, with maximum reductions of about 28 % and 38 %, respectively. A fatigue life prediction model based on the Paris crack growth equation was established, which can be used to estimate the fatigue life and fatigue limit of components containing porosity casting defect from the equivalent defect diameter.
Second, inclusion casting defect in WE43A alloy is mainly magnesium oxide with irregular black morphology. The surface inclusion fraction increases from 0.08 % to about 6 %. Inclusions have a limited effect on tensile strength, with a maximum reduction of about 9 %, but they significantly reduce the elongation and reduction of area by up to 60 % and 51 %, respectively. The fatigue life and fatigue limit decrease by about 26 % and 33 %, respectively.
Third, segregation casting defect is characterized by the formation of a continuous Mg₄₁Nd₅ network and fine Mg₂₄Y₅ particles at grain boundaries. The surface segregation fraction increases from 0.69 % to over 26 %. Segregation has a severe effect on ductility, with the elongation and reduction of area reduced by about 81 % and 89 %, respectively. The tensile strength decreases by up to 48 %, while the fatigue life and fatigue limit decrease by about 33 % and 39 %, respectively. The corrosion current density increases significantly with increasing segregation grade, indicating that segregation casting defect substantially reduces the corrosion resistance of WE43A alloy in chloride-containing environments.
Overall, the results of my research demonstrate that casting defect quantification is essential for the reliable design and quality control of rare earth magnesium alloy components. The combination of fracture surface analysis, image analysis, mechanical testing, and fracture mechanics modelling provides a powerful framework for evaluating the severity of casting defects and predicting their influence on component performance.