
In my extensive experience as a casting process engineer specializing in steel components, I have consistently faced the intricate challenge of producing high-quality, thin-walled steel castings for critical applications such as pump glands. The demand for lightweight yet durable parts in industries like fluid handling drives the need for innovative foundry techniques. This article details a comprehensive process research and development journey for a specific pump gland steel casting, focusing on overcoming filling defects and ensuring internal soundness. Throughout this discussion, the term ‘steel casting’ will be emphasized, as it is the core of our manufacturing focus. The development leverages modern tools like CAE simulation and 3D printed sand molds to achieve precision and reliability.
The subject component is a pump gland, a vital part responsible for sealing and fixation within pump assemblies. Its failure can lead to operational downtime, making casting integrity paramount. This particular steel casting, with a weight of approximately 15.5 kg, is made from material ZG230-450, a cast steel grade. The fundamental parameters of this steel casting are summarized in the table below.
| Parameter | Value | Unit |
|---|---|---|
| Name | Gland | – |
| Material | ZG230-450 | – |
| Weight | 15.5 | kg |
| Length | 270 | mm |
| Width | 270 | mm |
| Height | 105 | mm |
| Max Wall Thickness | 40 | mm |
| Min Wall Thickness | 6 | mm |
The chemical composition and mechanical property requirements for this steel casting grade are critical for its performance. These are outlined in the following tables to establish the material foundation for our process design.
| Element | Requirement | Control Standard |
|---|---|---|
| C | ≤0.30 | 0.18~0.24 |
| Si | ≤0.50 | 0.30~0.45 |
| Mn | ≤0.90 | 0.60~0.90 |
| P | ≤0.04 | ≤0.03 |
| S | ≤0.04 | ≤0.03 |
| Cu | ≤0.30 | ≤0.15 |
| Cr | ≤0.35 | ≤0.20 |
| Mo | ≤0.20 | ≤0.15 |
| Ni | ≤0.30 | ≤0.25 |
| V | ≤0.05 | ≤0.05 |
| Property | Minimum Value | Unit |
|---|---|---|
| Tensile Strength | 450 | MPa |
| Yield Strength | 230 | MPa |
| Elongation | 22 | % |
| Reduction of Area | 32 | % |
The primary structural challenge of this steel casting lies in its numerous cooling ribs or fins. These ribs have a mere 6 mm thickness, heights around 25 mm, and lengths varying from 35 mm to 170 mm. In traditional sand casting practices for carbon steel castings within the 200-400 mm size range, the recommended minimum wall thickness is typically no less than 9 mm. This steel casting, with its 6 mm sections, pushes far beyond conventional limits, making complete filling and avoidance of cold shuts a paramount concern. Furthermore, the small mass of the individual steel casting (around 12.5 kg after accounting for yield) poses a secondary challenge when using standard 1.5-ton ladles for pouring. Controlling pour temperature, time, and flow dynamics for such a small volume from a large ladle is inherently difficult, adversely affecting the filling of thin sections.
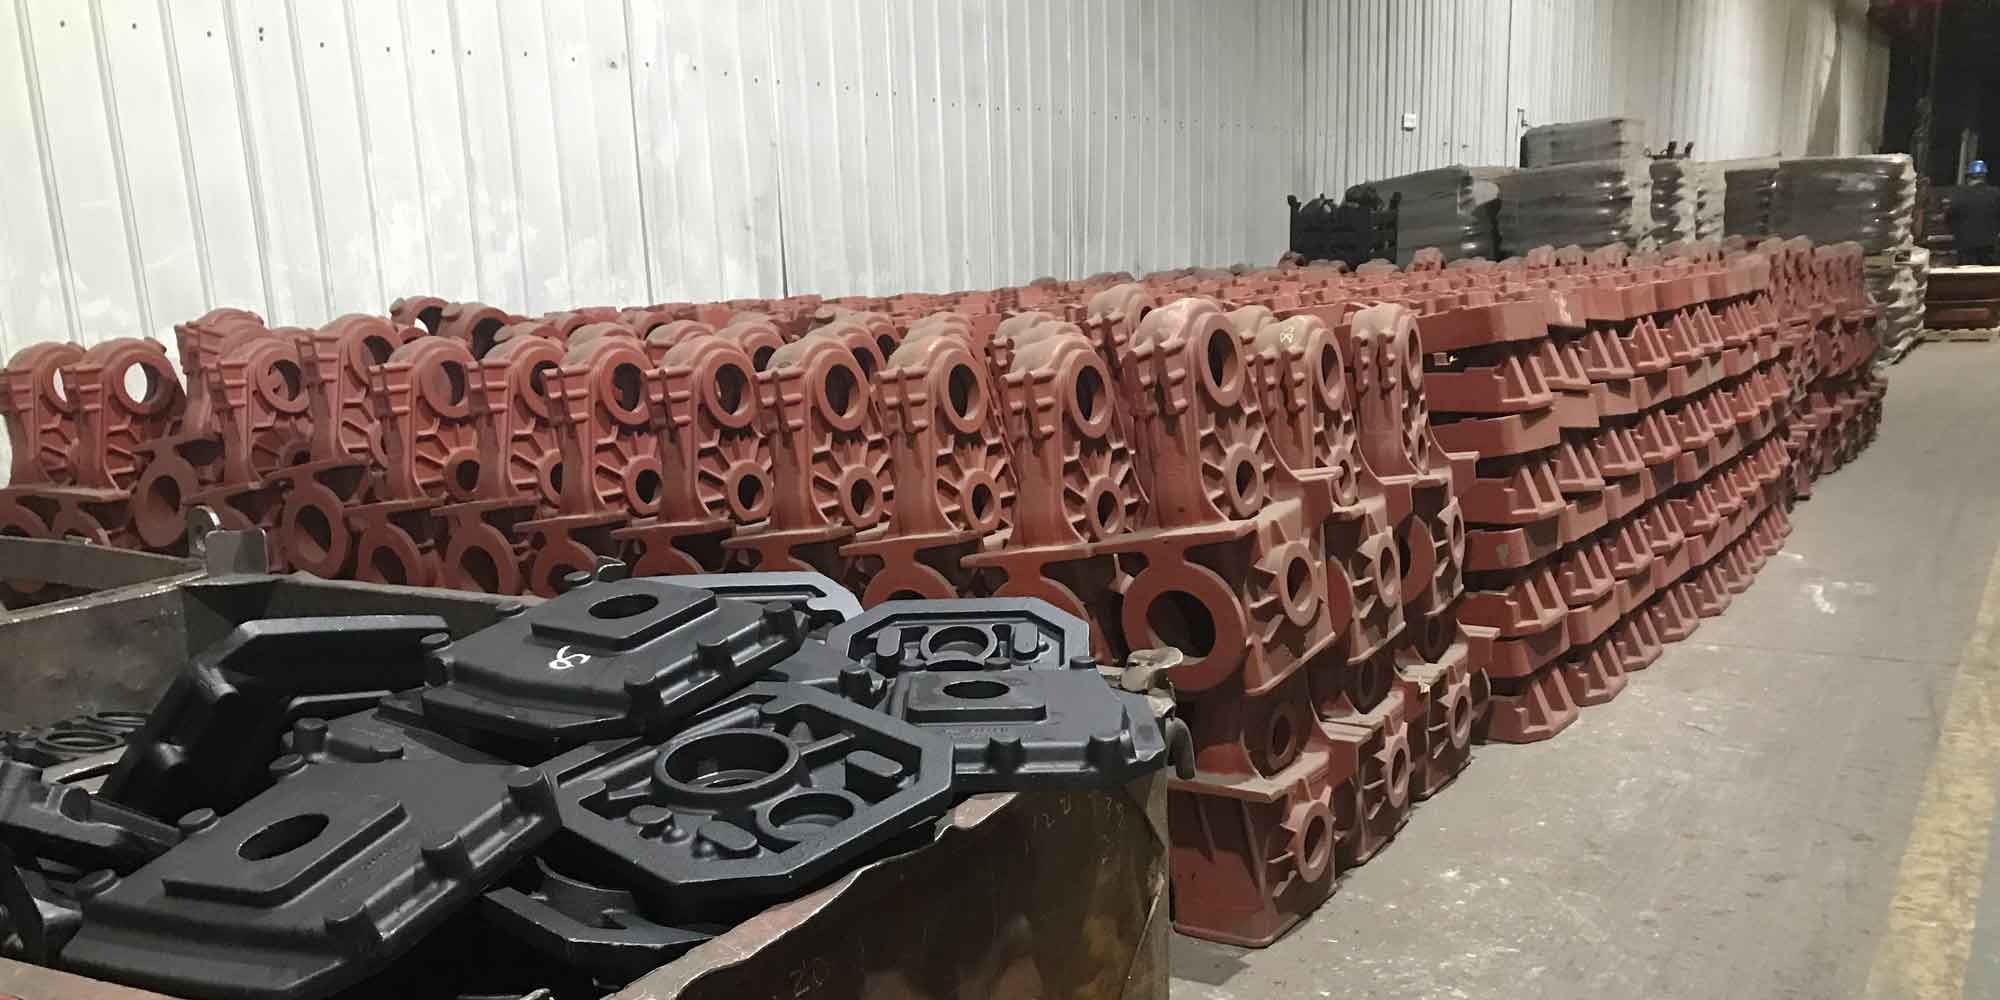
My approach to the casting process design began with a fundamental decision: the pouring position. Recognizing the limitations of conventional tooling and the advantages of additive manufacturing for molds, I opted for a vertical pouring orientation with multiple patterns arranged in a single mold. This strategy for producing these steel castings offers several key benefits for thin-walled steel casting production. Firstly, vertical placement results in a smaller rising metal meniscus cross-section, minimizing thermal gradients across horizontal planes and reducing the risk of cold shuts and gas entrapment. Secondly, it facilitates the effective placement of feeding risers at the top of the steel casting, promoting directional solidification for soundness. Thirdly, using multiple patterns per mold box increases the total poured weight per box, making temperature control during pouring from the large ladle more manageable and improving production efficiency. The schematic representation of this strategy is conceptually vital, and the successful application of such techniques in a modern steel casting facility can be visualized.
The design of the feeding system (risers and chills) is the cornerstone for achieving internal soundness in any steel casting. For cast steel, a fundamental rule is that the riser must solidify after the casting section it feeds. This is often evaluated using the modulus concept, where modulus M is defined as the volume-to-cooling surface area ratio: $$M = \frac{V}{A}$$. To ensure effective feeding, the riser modulus $M_{riser}$ must be greater than the casting modulus $M_{casting}$ in the fed region. Our design criterion mandates $M_{riser} \geq 1.2 \times M_{casting}$. Additionally, the riser must contain sufficient liquid metal to compensate for the liquid shrinkage, solidification shrinkage, and possible mold wall movement of the feeding area. A simplified requirement is that the riser’s available feed metal volume should be greater than one-third of the weight of the fed casting section combined with the riser’s own weight. Through careful analysis of the steel casting’s hot spots and using CAE software for initial validation, a single top riser was selected. Its size was determined based on the modulus calculation of the heaviest section. Strategic use of chills and feeding pads (or “piping”) was incorporated to control solidification patterns and eliminate shrinkage porosity. The design principle can be summarized by ensuring a positive pressure gradient towards the riser throughout solidification, which is governed by the pressure balance equation in the mushy zone: $$P_{riser} + \rho g h > P_{casting} + \frac{2\sigma}{r} + \Delta P_{flow}$$, where $P$ is pressure, $\rho$ is density, $g$ is gravity, $h$ is height, $\sigma$ is surface tension, $r$ is the pore radius, and $\Delta P_{flow}$ is the pressure drop due to interdendritic flow.
The gating system was designed as a bottom-poured, open type with a central sprue. This choice offers a balance between top and bottom pouring advantages for this steel casting. It ensures a relatively uniform temperature distribution between the upper and lower parts of the mold cavity while maintaining a tranquil filling process, minimizing turbulence, slag entrainment, and mold erosion. The cross-sectional areas of the gating channels follow the open system ratio to control flow velocity. For a typical steel casting pour, we aim for a critical velocity to avoid mold penetration, which can be approximated by: $$v_{crit} = \sqrt{\frac{2 \gamma \cos\theta}{\rho r}}$$, where $\gamma$ is the surface tension, $\theta$ is the contact angle, and $r$ is the pore radius in the mold. The fill time $t_f$ is also crucial and is related to the flow rate $Q$ and cavity volume $V_c$: $$t_f \approx \frac{V_c}{Q}$$. For our multi-cavity mold, the total gating system was sized to achieve a fill time of approximately 20 seconds, ensuring the thin ribs are filled before the metal temperature drops excessively.
Computer-Aided Engineering (CAE) simulation played an indispensable role in the iterative optimization of this steel casting process. By virtually simulating the coupled phenomena of fluid flow, heat transfer, and solidification, we could predict and rectify potential defects before committing to physical production. The key simulation parameters for this steel casting are tabulated below.
| Parameter | Value | Unit |
|---|---|---|
| Material | ZG230-450 | – |
| Total Poured Weight per Mold | 273 | kg |
| Pour Temperature | 1590 ± 5 | °C |
| Target Fill Time | 20 | s |
The simulation proceeded in two main phases: filling and solidification. The filling analysis confirmed that the gating design produced a smooth, progressive front without excessive velocity that could lead to splash or air entrainment. The solidification analysis, using criteria like the Niyama criterion for predicting microporosity, guided the refinement of riser size, chill placement, and pad geometry. The Niyama criterion $G/\sqrt{\dot{T}}$ (where $G$ is thermal gradient and $\dot{T}$ is cooling rate) is a key metric; areas with values below a critical threshold indicate a high risk of shrinkage porosity. After several iterations, the simulation results showed a clear directional solidification pattern, with the riser being the last region to solidify and no predicted shrinkage defects in the main body of the steel casting. The thermal analysis also helped verify that the modulus relationship $M_{riser} > 1.2M_{casting}$ held true for all fed sections.
The adoption of 3D printing technology for sand mold production was a game-changer for this complex steel casting. This technology liberates the process designer from constraints related to pattern draft, core box complexity, and parting line location. For this steel casting, I designed the entire mold assembly to consist of only two primary sand pieces. This was achieved by intelligently integrating cores and molds into single printed units. Crucially, all the challenging thin ribs were consolidated into one half of the mold, eliminating any parting lines across these fragile features. This design decision had profound benefits for the final steel casting quality. It prevented the formation of fins or flash on the ribs, which are difficult to remove and can act as stress raisers. It also ensured exceptional dimensional accuracy and minimal casting allowance, reducing both cleaning effort and machining costs. The ability to create complex internal geometries directly in the sand mold is a significant advantage of 3D printing for prototype and low-volume production of intricate steel castings.
The melting and pouring practices are the final critical links in the chain of producing a sound steel casting. For this project, the steel was melted in a medium-frequency induction furnace. To achieve the required cleanliness and gas content levels, an argon stirring degassing treatment was employed during the holding period. Deoxidation was carried out using aluminum pellets added during tapping to control free oxygen and promote a fine grain structure. Temperature control was meticulous. The ladle was preheated to above 800°C to minimize thermal shock and heat loss. The tap temperature was controlled between 1650°C and 1670°C. After skimming, the temperature was allowed to stabilize, and the steel casting was poured at a target temperature of 1590°C ± 5°C. This precise temperature is vital for the thin-section steel casting; too low a temperature risks incomplete filling, while too high a temperature can increase gas solubility, shrinkage volume, and mold-metal reaction. The pouring rate was controlled to match the simulated fill time, ensuring a calm, continuous rise of metal in the mold cavity.
The production validation confirmed the success of the developed process for this steel casting. Upon shakeout and riser removal, the castings exhibited excellent visual quality. The thin ribs were fully formed, with sharp edges and no evidence of cold shuts, misruns, or surface laps. The absence of parting lines on the ribs resulted in a clean as-cast surface, significantly reducing the need for grinding and finishing. Dimensional inspections showed tight conformity to the drawing specifications, a direct benefit of the precision afforded by 3D printed molds. Non-destructive testing (NDT), including magnetic particle or penetrant testing as specified, revealed no surface defects like cracks or hot tears. Most importantly, radiographic inspection confirmed the internal soundness of the steel casting, with no detectable shrinkage cavities or porosity in the critical sections, validating the CAE predictions and riser/chill design. Chemical analysis and mechanical testing of separately cast coupons confirmed that the steel casting material met all requirements specified in Tables 1 and 2. The yield strength, tensile strength, elongation, and reduction of area all fell within or exceeded the specified ranges, proving that the thermal history imposed by our process did not adversely affect the metallurgical properties of the steel casting.
In conclusion, this comprehensive process development project for a thin-walled pump gland steel casting demonstrates a successful methodology for tackling demanding casting applications. By systematically addressing the dual challenges of extreme thin-section filling and internal soundness, we established a robust production route. The synergistic combination of fundamental casting principles—such as modulus-based feeding design and controlled gating—with advanced technologies like CAE simulation and 3D sand printing was instrumental. The CAE software allowed for virtual optimization, saving time and material, while 3D printing provided the manufacturing flexibility to implement an optimal mold design unattainable with traditional patterns. This approach ensured first-pass success, producing steel castings that met all dimensional, aesthetic, and stringent quality requirements. The lessons learned, particularly regarding the vertical multi-cavity approach for thin-walled steel castings and the integration of chills and pads for controlled solidification, are widely applicable to other complex steel casting projects. The future of steel casting lies in such integrated digital-physical processes, enabling the reliable production of lighter, stronger, and more intricate components for advanced engineering applications. The continuous iteration between design, simulation, and additive manufacturing paves the way for further innovation in the field of precision steel casting.