
In my years of experience in the foundry industry, I have witnessed the evolution of casting techniques, and among them, lost foam casting has emerged as a transformative method for producing complex and large steel castings. This process, which involves using expandable polystyrene (EPS) foam patterns that vaporize upon contact with molten metal, offers significant advantages in terms of design flexibility, reduced machining, and improved dimensional accuracy. However, when applied to heavy steel components like crusher spindles, challenges such as defect formation, low yield rates, and high costs often arise. In this article, I will delve into a novel approach—using the mold cavity as the runner system—that my team and I implemented for manufacturing cone crusher spindle pairs. This innovation not only streamlined the lost foam casting process but also achieved a remarkable yield rate of 80%, demonstrating the potential for broader applications in large steel castings. Throughout this discussion, I will emphasize key aspects of lost foam casting, supported by mathematical models, tables, and practical insights, to provide a comprehensive guide for engineers and foundry specialists.
The core of this study focuses on a specific component: the cone crusher spindle pair, made from ZG350 steel, with four specifications ranging in weight from 950 kg to 3,560 kg. These spindles are critical for power transmission in crushing machinery, requiring high integrity, pressure-tightness, and weldability after machining. Traditional lost foam casting methods for such parts often involved complex gating systems with ceramic runners, which were time-consuming to assemble and costly. Drawing from principles outlined in foundational texts on lost foam casting, I proposed a radical simplification: positioning the casting upright with the larger head downward, placing three exothermic insulating risers at the top, and integrating the runner directly into the part’s cavity. This “cavity-as-runner” concept, coupled with a bent buffer runner, formed the basis of our optimized lost foam casting process. The results were compelling, with defect-free castings after machining and a significant reduction in material waste. In the following sections, I will detail the step-by-step methodology, analyze the underlying physics using formulas, and present data in tabular form to underscore the efficiency gains. By sharing this case, I aim to inspire further innovation in lost foam casting for steel applications, highlighting how strategic design can overcome common pitfalls.
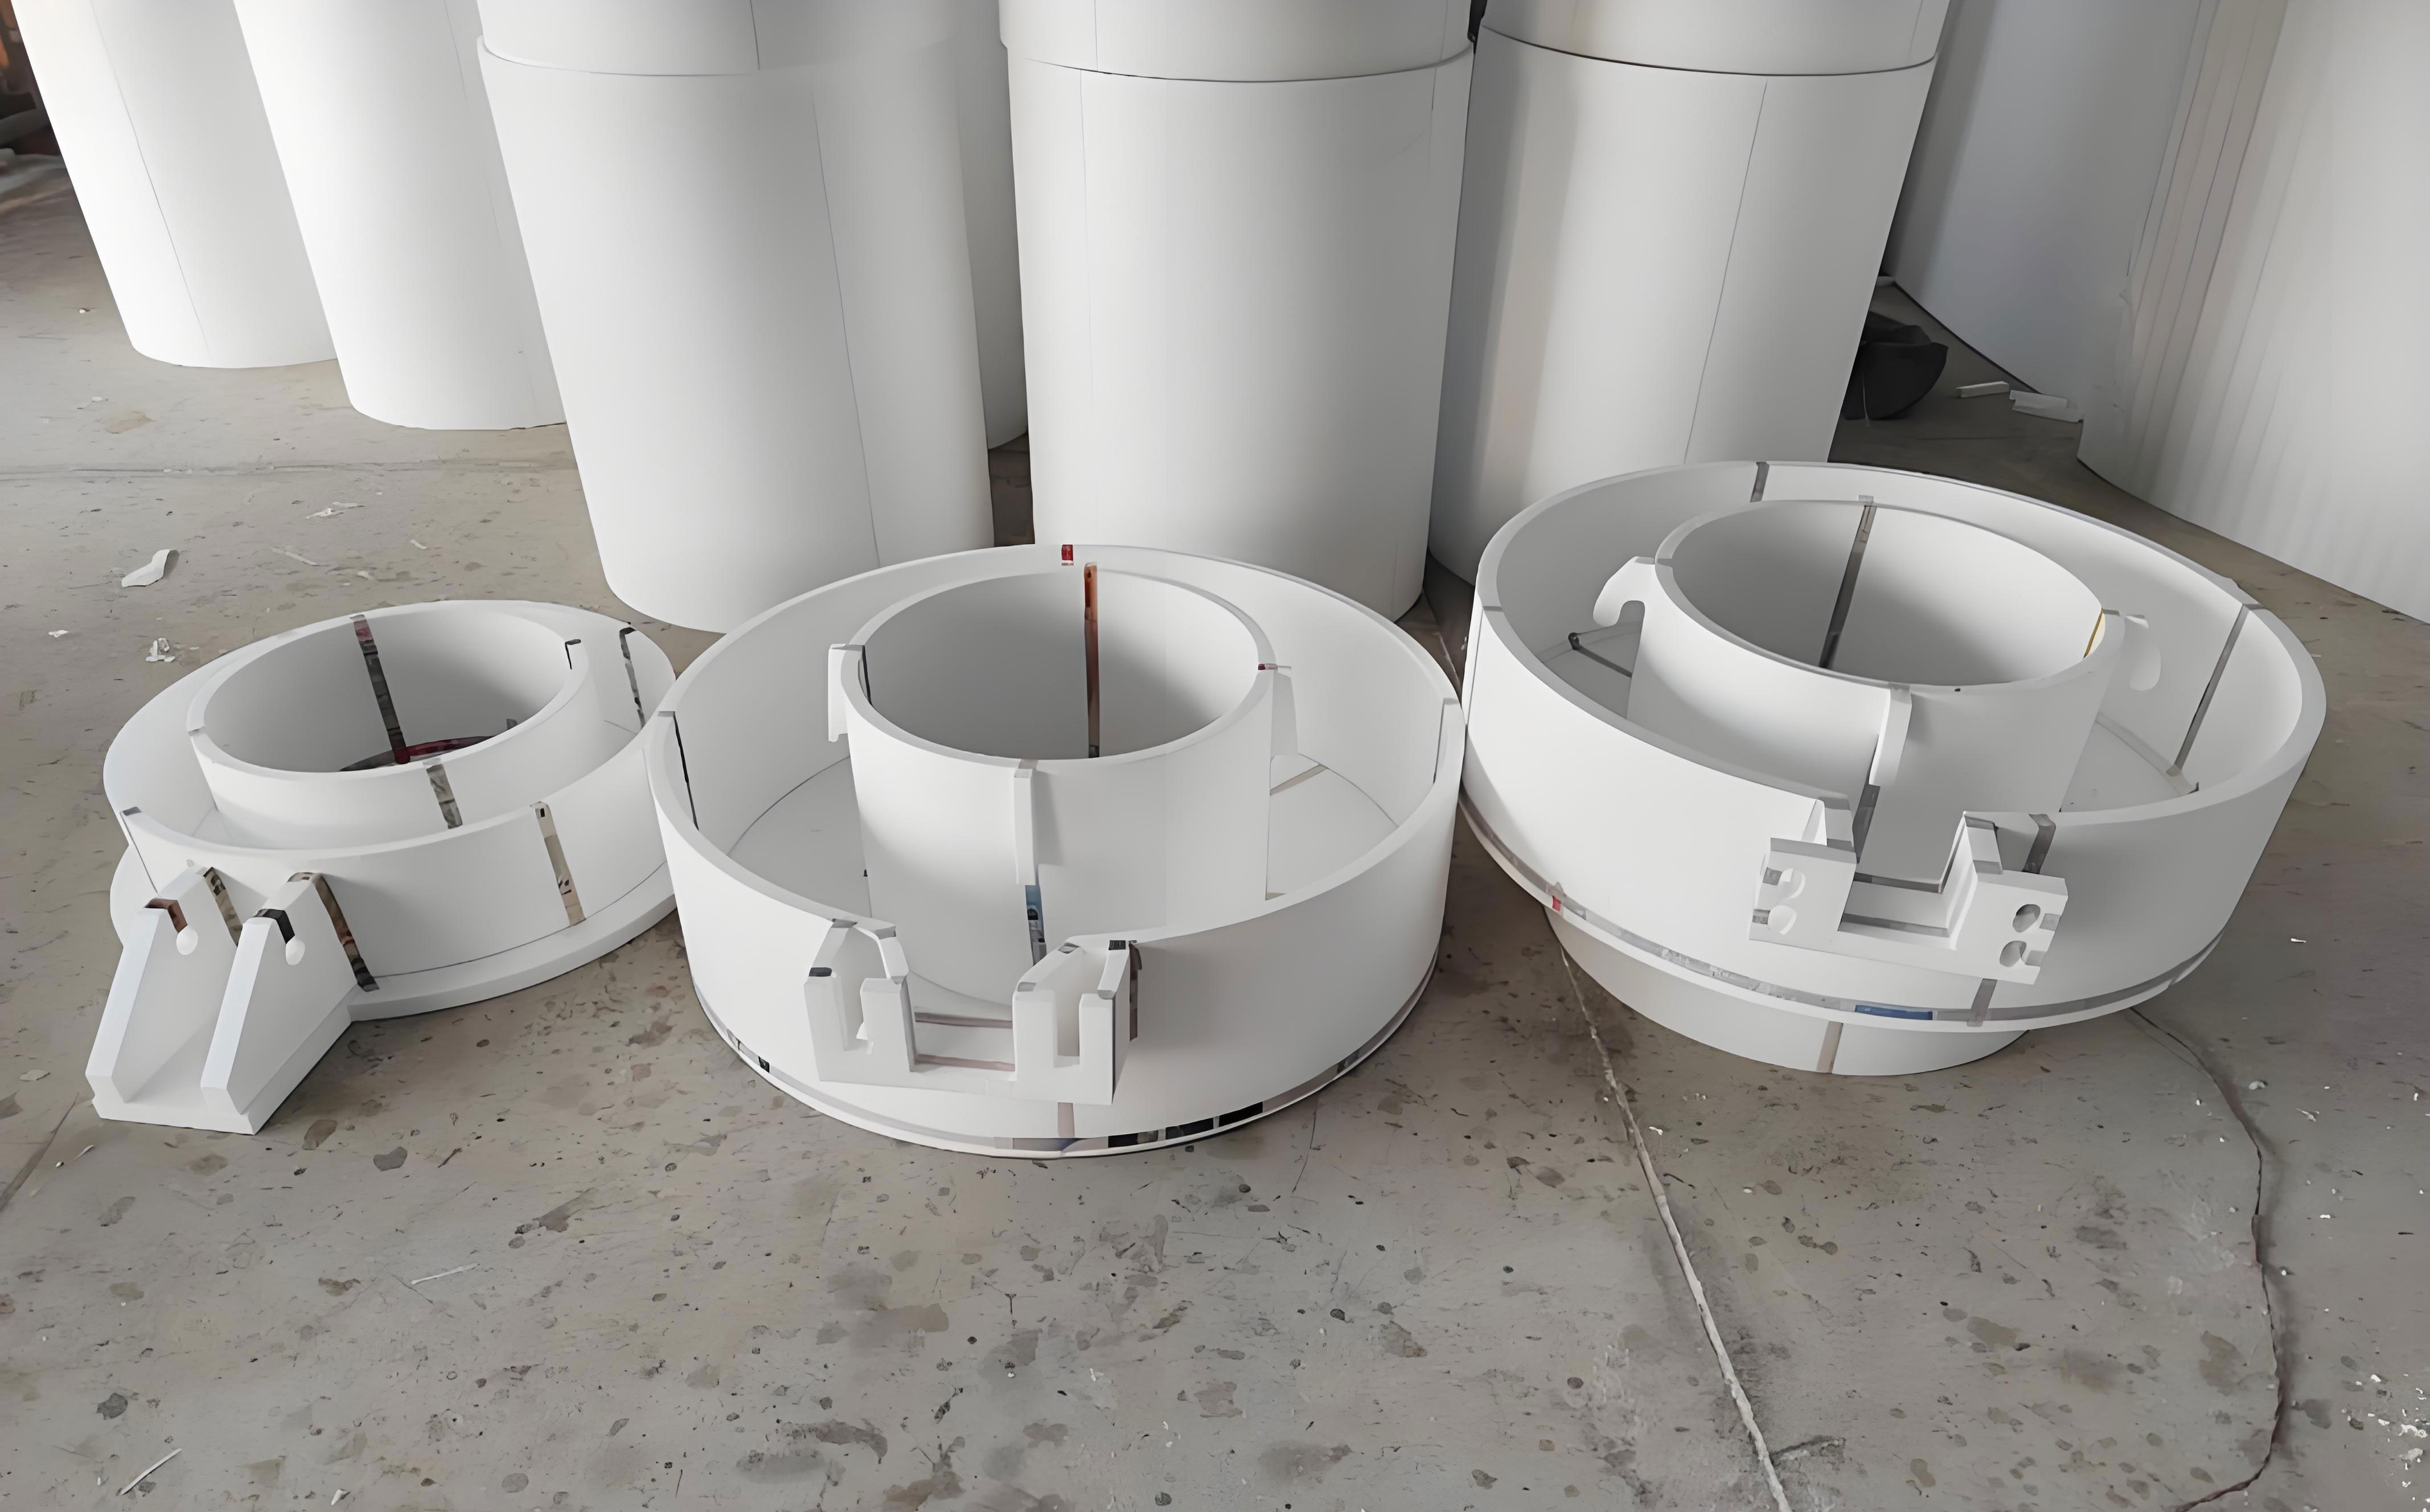
The lost foam casting process begins with pattern fabrication, and for our spindle pairs, we manually assembled EPS foam boards with a density of 18 g/L. This hands-on approach allowed for precise control over the pattern’s geometry, ensuring that critical features like the wing plates and flanges were accurately represented. Once the patterns were ready, we applied a commercial coating specifically designed for lost foam casting, with a thickness of 2–3 mm on the main body and 3–5 mm in areas prone to metal冲刷, such as the runner and riser junctions. Coating integrity is paramount in lost foam casting, as any cracks or bare spots can lead to sand penetration or collapse during pouring. To reinforce hard-to-reach sections, we pre-filled them with resin sand before molding, a tactic that enhanced stability. The patterns were then carefully placed in the flask using soft cloth slings to prevent coating damage, and we filled the flask with chromite sand, employing manual assistance and vibration to ensure complete compaction. This meticulous setup is crucial for successful lost foam casting, as it minimizes defects like veining or inclusions.
Central to our innovation was the gating system design. In conventional lost foam casting, runners are separate channels that guide molten metal into the cavity, often requiring ceramic tubes that add cost and complexity. We revolutionized this by adopting a “cavity-as-runner” strategy, where the molten steel flows through the part’s own cavity to fill it. Specifically, we positioned a bent runner on the wing plate at the top of the casting, with a 90-degree bend to act as a buffer, reducing the inertial force and preventing direct冲击 on the cavity walls. This buffer runner design is mathematically represented by considering fluid dynamics: the change in momentum as the metal flows around the bend can be expressed using the Navier-Stokes equations. For simplicity in foundry applications, we approximate the pressure drop $\Delta P$ across the bend using the following empirical formula, which accounts for energy loss in lost foam casting systems:
$$ \Delta P = K \cdot \frac{\rho v^2}{2} $$
Here, $\Delta P$ is the pressure drop, $K$ is the loss coefficient (typically between 0.2 and 0.5 for 90-degree bends in turbulent flow), $\rho$ is the density of molten steel (approximately 7,800 kg/m³ for ZG350), and $v$ is the flow velocity. By designing the bend, we aimed to keep $v$ below 2 m/s to minimize冲刷, a critical factor in lost foam casting where coating integrity is vital. Additionally, we placed three exothermic insulating risers on the small flange at the top to facilitate feeding and reduce shrinkage defects. The thermal dynamics of these risers can be modeled using Fourier’s law of heat conduction, ensuring that the solidification front progresses uniformly. The overall gating ratio was simplified to a single runner entry, drastically reducing the system’s volume and improving the yield. To quantify this, Table 1 summarizes the key parameters for the four spindle specifications in our lost foam casting process.
| Specification | Weight (kg) | Pattern Density (g/L) | Coating Thickness (mm) | Pouring Temperature (°C) | Runner Diameter (mm) |
|---|---|---|---|---|---|
| C02 | 950 | 18 | 2-3 (body), 3-5 (runner) | 1630 | 60 |
| C03 | 1850 | 18 | 2-3 (body), 3-5 (runner) | 1630 | 80 |
| C04 | 2650 | 18 | 2-3 (body), 3-5 (runner) | 1630 | 100 |
| C06 | 3560 | 18 | 2-3 (body), 3-5 (runner) | 1630 | 120 |
After molding, we proceeded to pouring, maintaining a vacuum level of 0.04 MPa throughout the process to evacuate pyrolysis gases from the decomposing foam—a hallmark of lost foam casting. The pouring temperature was consistently set at 1,630°C, based on thermal analysis to ensure complete filling without premature solidification. The relationship between pouring time $t_p$ and metal fluidity can be derived from the Bernoulli equation, adapted for lost foam casting conditions:
$$ t_p = \frac{V}{A \cdot v} $$
where $V$ is the cavity volume, $A$ is the cross-sectional area of the runner, and $v$ is the flow velocity as before. For our largest spindle (C06), with $V \approx 0.45 \, \text{m}^3$ and $A = \pi (0.06)^2 \, \text{m}^2$, we calculated $t_p \approx 40$ seconds, aligning with empirical observations. Post-pouring, we held the vacuum for 30 minutes to allow for gas escape and then cooled the castings in the sand for 8 hours to reduce thermal stress. Upon shakeout, we cut off the risers and runners, ground the remnants, and performed shot blasting. The finished castings exhibited no defects upon machining, validating our lost foam casting approach. To further analyze the thermal behavior, we used the Chvorinov’s rule to estimate solidification time $t_s$:
$$ t_s = B \cdot \left( \frac{V}{A_s} \right)^2 $$
Here, $B$ is the mold constant (dependent on material and coating properties in lost foam casting), $V$ is the casting volume, and $A_s$ is the surface area. For ZG350 steel, we derived $B \approx 2.5 \, \text{min/cm}^2$ from experimental data, ensuring that risers remained liquid longer to feed the casting effectively. This mathematical grounding was instrumental in optimizing the lost foam casting process for these heavy components.
The adoption of the cavity-as-runner technique in lost foam casting brought several advantages. First, it simplified the gating system immensely, eliminating the need for ceramic runners and reducing assembly time by over 50%. This not only cut costs but also minimized potential leak points, enhancing reliability. Second, by introducing the bent buffer runner, we mitigated the risk of coating erosion, a common issue in lost foam casting when high-velocity metal impacts the cavity wall. The buffer effect can be quantified using computational fluid dynamics (CFD) simulations, but in practice, we observed a marked reduction in sand inclusion defects. Third, the use of exothermic risers prolonged the feeding period, compensating for solidification shrinkage and improving density. The heat generation from these risers follows an exponential decay model, which I approximate as:
$$ Q(t) = Q_0 \cdot e^{-\lambda t} $$
where $Q(t)$ is the heat output at time $t$, $Q_0$ is the initial heat release, and $\lambda$ is a decay constant specific to the exothermic material. In our lost foam casting setup, this ensured that the thermal gradient favored directional solidification toward the risers. Moreover, the overall yield—defined as the ratio of casting weight to total metal poured—reached 80%, a significant improvement from the previous 70% with traditional methods. This efficiency gain is critical in lost foam casting for large steel parts, where material costs constitute a major expense. To illustrate the impact, Table 2 compares key performance metrics before and after implementing the cavity-as-runner design in lost foam casting.
| Metric | Traditional Lost Foam Casting (with Ceramic Runner) | Optimized Lost Foam Casting (Cavity-as-Runner) |
|---|---|---|
| Gating System Complexity | High (multiple ceramic components) | Low (single foam runner integrated) |
| Average Assembly Time (hours) | 8 | 4 |
| Material Yield (%) | 70 | 80 |
| Defect Rate (per 100 castings) | 15 (mainly sand inclusions and shrinkage) | 3 (minor surface issues) |
| Cost per Casting (relative units) | 1.00 | 0.75 |
Beyond the immediate benefits, this case study offers broader insights for lost foam casting of large steel castings. The cavity-as-runner concept can be applied to other components with relatively open and elevated cavities, provided that the entry points are strategically placed to ensure smooth metal flow. In our spindles, we chose the mid-upper section of the wing plate, which allowed the risers to stay hot and effective for feeding. This principle aligns with fundamental lost foam casting guidelines, such as “vertical over horizontal” positioning, but pushes the envelope by integrating functional geometry into the gating. Additionally, the success of foam runners over ceramic ones underscores the importance of coating quality in lost foam casting. With a robust, well-applied coating, foam runners can withstand the thermal and mechanical stresses of pouring, offering a cost-effective alternative. However, this requires precise control over coating thickness and drying, as any weakness can lead to failure. From a thermal perspective, the lost foam casting process involves complex interactions between metal, foam, and sand. The energy balance during pouring can be modeled as:
$$ \rho_m C_p \frac{dT}{dt} = k \nabla^2 T + \dot{q}_{foam} $$
where $\rho_m$ is metal density, $C_p$ is specific heat, $T$ is temperature, $k$ is thermal conductivity, and $\dot{q}_{foam}$ is the heat sink from foam decomposition. In lost foam casting, this decomposition absorbs energy, cooling the metal front, which must be compensated by higher pouring temperatures. Our use of 1,630°C balanced this effect, ensuring complete fill without excessive superheat that could cause grain growth. Furthermore, the vacuum plays a crucial role in lost foam casting by removing gaseous products, and its optimization can be described by the ideal gas law applied to the flask volume.
In conclusion, the lost foam casting process for large steel castings like cone crusher spindles can be greatly enhanced through innovative gating designs. My experience with the cavity-as-runner approach, coupled with a buffer runner and exothermic risers, demonstrates that simplification and integration lead to higher yields, lower costs, and superior quality. The mathematical models and data presented here provide a framework for replicating this success in other applications. As lost foam casting continues to evolve, I believe that such creative solutions will drive its adoption for heavy-duty components, pushing the boundaries of what is possible in modern foundries. Future work could involve CFD simulations to further refine runner geometries or explore new coating materials for even better performance in lost foam casting. For now, this case stands as a testament to the power of rethinking traditional methods in the pursuit of efficiency and excellence.