
In the manufacturing of wind turbine components, the use of ductile cast iron has become prevalent due to its superior mechanical properties, including high strength, fatigue resistance, and good damping capacity. However, shrinkage defects, particularly shrinkage porosity, pose significant challenges in producing large and complex ductile cast iron castings, such as hubs, main frames, and bearing housings. These defects can severely compromise the structural integrity and performance of the components, especially under harsh operational conditions involving wind loads, impacts, and low temperatures. As an engineer specializing in casting technology, I have extensively studied the root causes of shrinkage in ductile cast iron and implemented effective preventive measures. This article delves into a comprehensive analysis of shrinkage formation mechanisms, factors influencing defect occurrence, and practical strategies to mitigate them, with an emphasis on empirical data, tables, and mathematical models to enhance understanding and application.
Ductile cast iron, also known as nodular cast iron, undergoes a “mushy” solidification process characterized by a prolonged eutectic reaction and a high number of eutectic cells. This unique solidification behavior is the fundamental reason for shrinkage tendency. During solidification, graphite nodules precipitate, leading to expansion pressures that can counteract shrinkage, but improper process control often results in dispersed microshrinkage or macroshrinkage. The defect typically manifests as fine, scattered pores within the casting, reducing tensile strength by approximately 60% and fatigue strength by 40–50%. Therefore, addressing shrinkage in ductile cast iron is critical for ensuring the reliability and longevity of wind turbine systems.
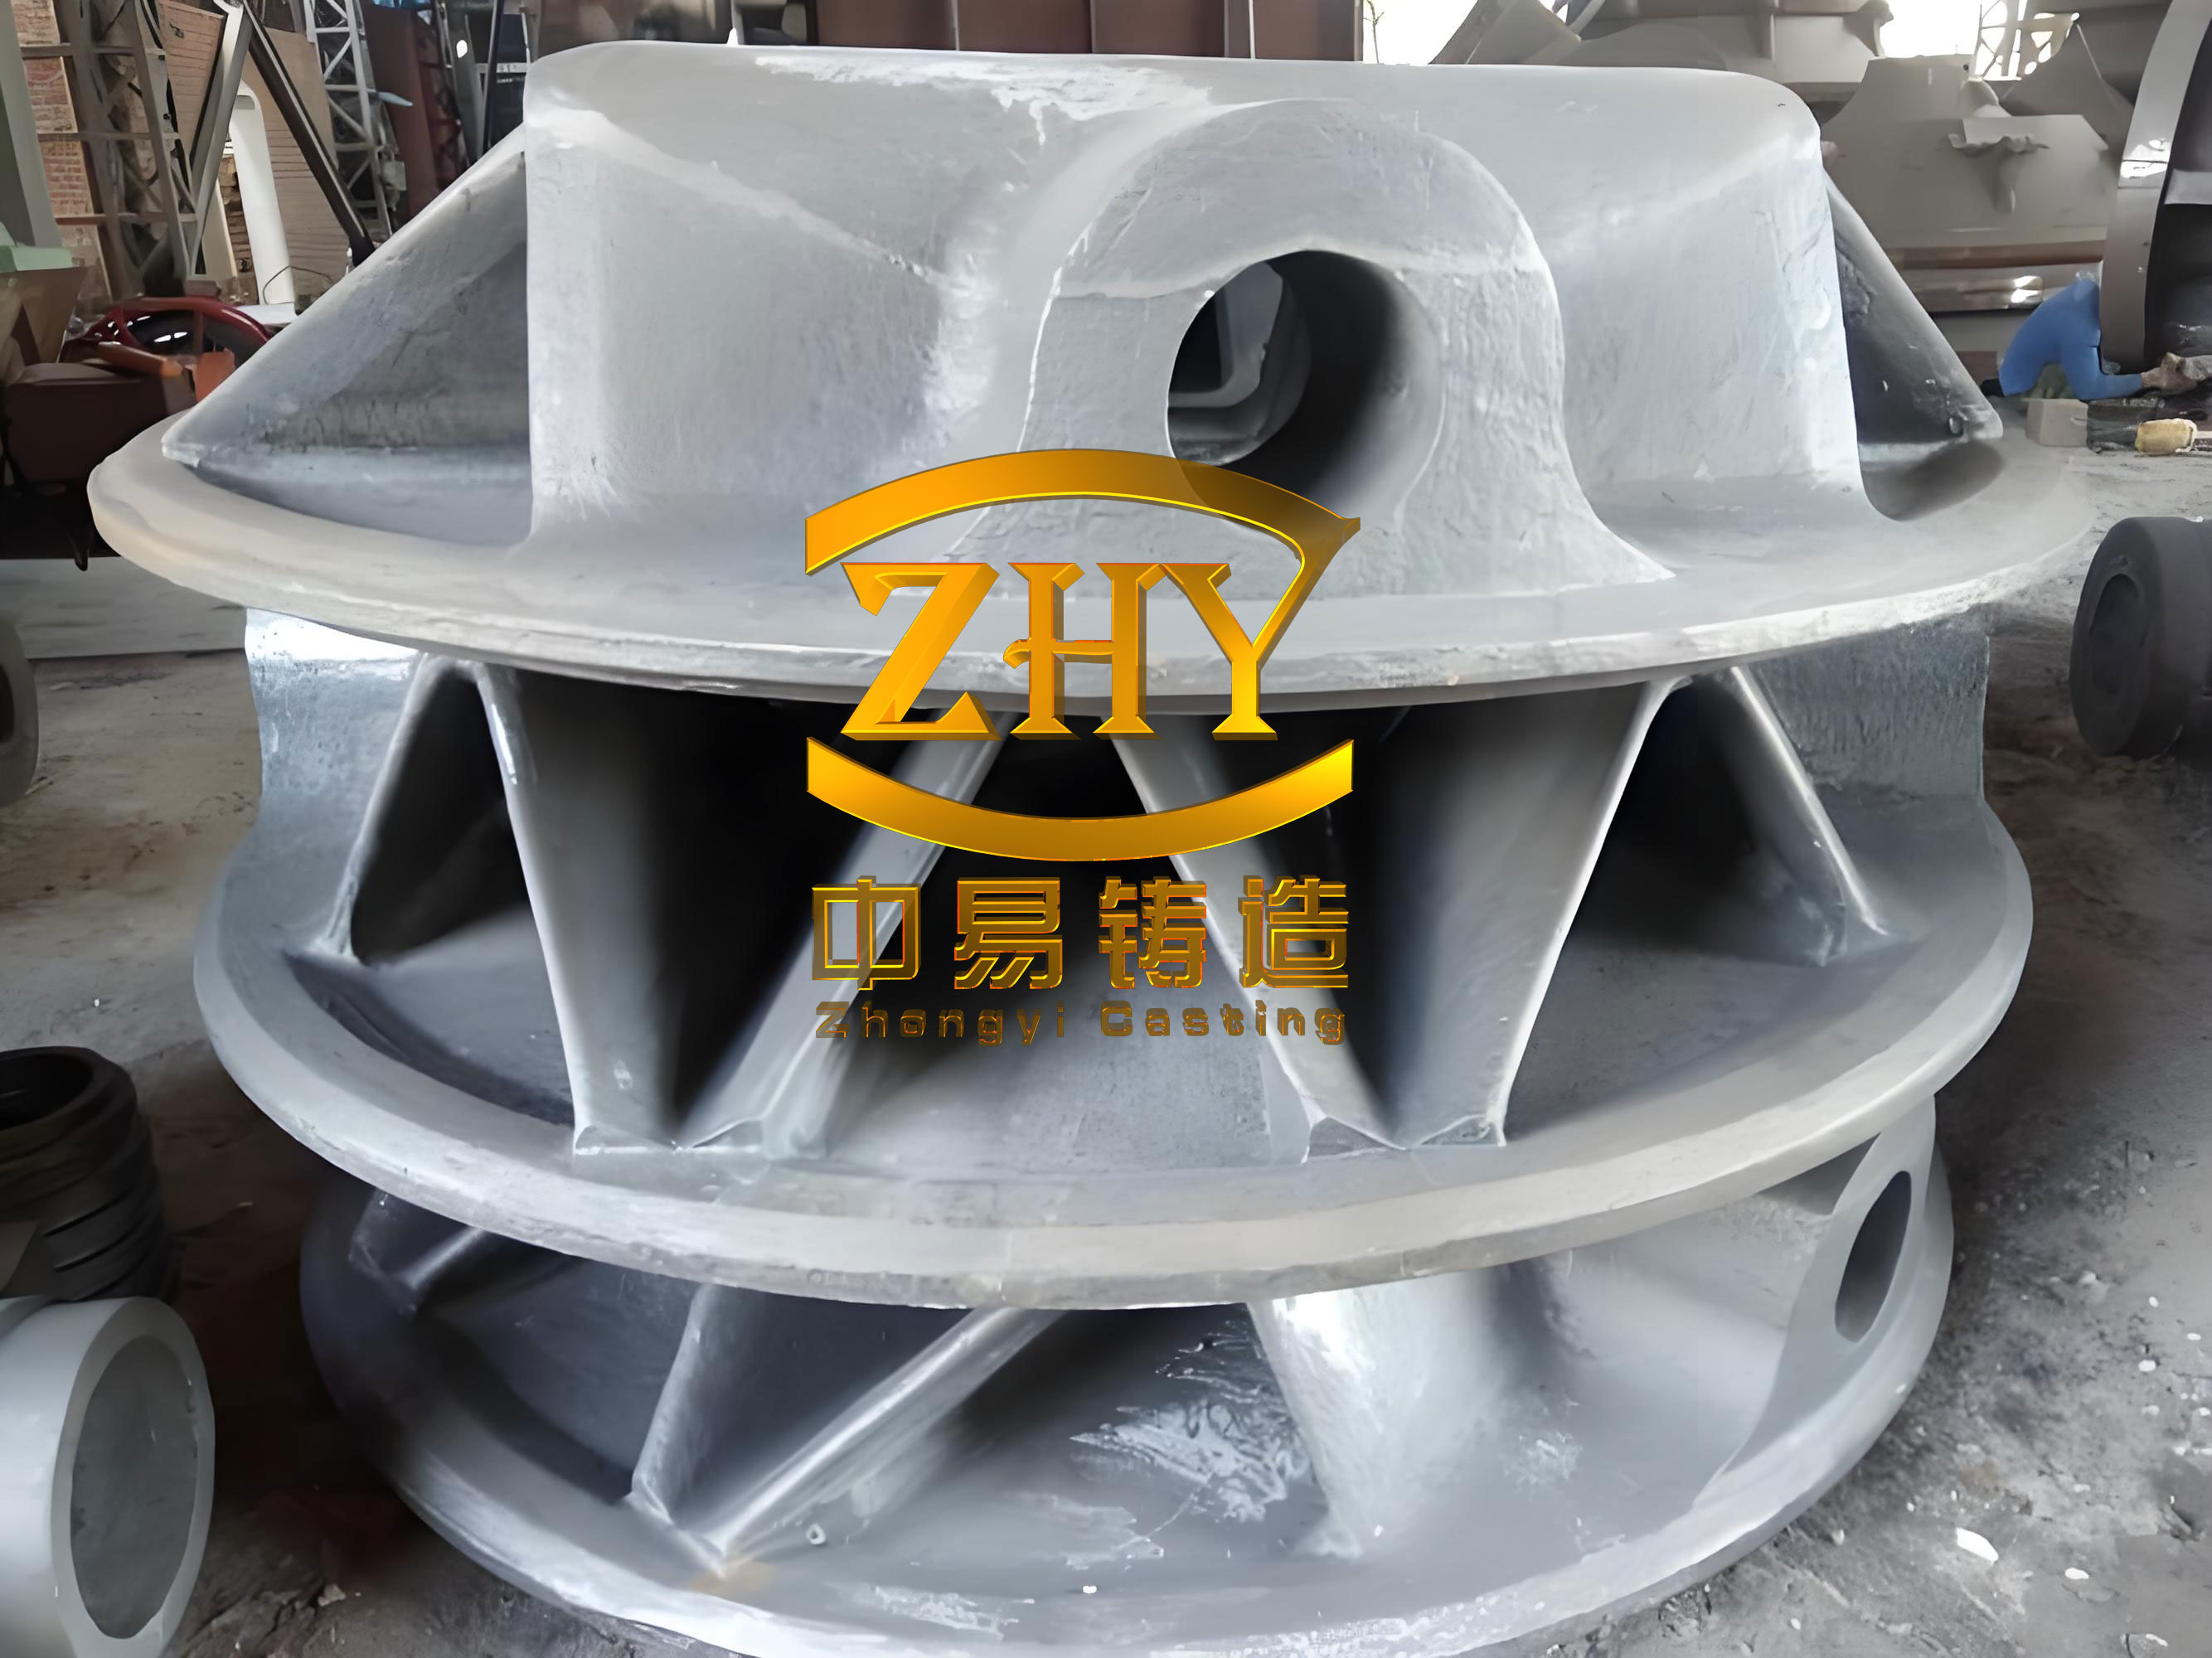
The formation of shrinkage in ductile cast iron is influenced by multiple interrelated factors. From my experience, these can be categorized into five primary aspects: casting design, sand mold quality, gating system design, melting composition, and pouring temperature. Each factor contributes to the overall solidification dynamics and feeding efficiency. To quantify these effects, I often employ mathematical models and simulation tools. For instance, the volumetric shrinkage during solidification can be expressed as: $$ V_s = \beta \cdot V_0 \cdot (T_l – T_s) $$ where \( V_s \) is the shrinkage volume, \( \beta \) is the linear shrinkage coefficient (typically ranging from 0.8% to 1.2% for ductile cast iron), \( V_0 \) is the initial liquid volume, \( T_l \) is the liquidus temperature, and \( T_s \) is the solidus temperature. This formula highlights the importance of temperature control in minimizing shrinkage. Furthermore, the feeding demand in a casting section can be estimated using: $$ F_d = \frac{A \cdot L \cdot \rho \cdot C_p \cdot \Delta T}{H_f} $$ where \( F_d \) is the feeding demand, \( A \) is the cross-sectional area, \( L \) is the length, \( \rho \) is the density, \( C_p \) is the specific heat, \( \Delta T \) is the temperature drop, and \( H_f \) is the latent heat of fusion. Such calculations aid in designing adequate feeding systems for ductile cast iron components.
Casting design plays a pivotal role in shrinkage formation. Wind turbine ductile cast iron parts are often large, with weights exceeding 30 tons and wall thicknesses varying from 60 mm to 120 mm. Thick sections and abrupt changes in wall thickness create thermal centers that solidify last, leading to shrinkage. For example, in a hub casting, the junction between the flange and the body acts as a hotspot. The solidification time for a section can be approximated by Chvorinov’s rule: $$ t = k \cdot \left( \frac{V}{A} \right)^2 $$ where \( t \) is the solidification time, \( k \) is a mold constant, \( V \) is the volume, and \( A \) is the surface area. Thicker sections have a higher \( V/A \) ratio, prolonging solidification and increasing shrinkage risk. To illustrate, Table 1 summarizes common design-related issues in ductile cast iron wind turbine components.
| Factor | Description | Impact on Shrinkage |
|---|---|---|
| Wall Thickness Variation | Sudden transitions from thin to thick sections | Creates isolated hot spots that lack feeding |
| Large Mass Sections | Areas with thickness >100 mm | Extended solidification time increases liquid shrinkage |
| Complex Geometry | Presence of cores and internal cavities | Restricts molten metal flow and feeding paths |
| Inadequate Draft Angles | Sharp corners and edges | Promotes turbulence and air entrapment |
Sand mold quality is another critical factor. In ductile cast iron production, furan resin sand is commonly used due to its high strength and dimensional stability. However, if the sand has low refractoriness or insufficient compaction, mold wall movement can occur under metallostatic pressure and graphite expansion forces, enlarging the cavity and causing shrinkage. The mold deformation can be modeled as: $$ \delta = \frac{P \cdot h}{E_m} $$ where \( \delta \) is the deformation, \( P \) is the pressure (from liquid metal and expansion), \( h \) is the mold wall thickness, and \( E_m \) is the modulus of elasticity of the mold material. High moisture content in the sand reduces the dry layer thickness, increasing deformation susceptibility. Additionally, sand permeability affects gas evolution; low permeability can trap gases, forming pores that exacerbate shrinkage. Empirical data suggests that maintaining sand compactness above 85% and moisture below 0.3% significantly reduces shrinkage in ductile cast iron castings.
The gating system design directly influences feeding efficiency. A poorly designed system hinders directional solidification, leading to shrinkage. Key principles include placing ingates in thin sections to promote progressive solidification toward risers, using adequate riser size and placement, and employing chills in thick areas. The riser efficiency for ductile cast iron can be calculated using: $$ \eta_r = \frac{V_f}{V_r} \times 100\% $$ where \( \eta_r \) is the riser efficiency, \( V_f \) is the volume of feeding metal, and \( V_r \) is the riser volume. For ductile cast iron, riser efficiency is typically lower than for steel due to graphite expansion, often ranging from 10% to 20%. Simulation software like ProCAST is invaluable for optimizing gating designs. Table 2 outlines recommended gating parameters for large ductile cast iron components.
| Parameter | Recommended Value | Rationale |
|---|---|---|
| Ingate Location | At thin sections or near risers | Ensures proper feeding sequence |
| Riser Size Ratio | Riser volume: 15–25% of casting volume | Compensates for liquid and solidification shrinkage |
| Chill Usage | Placed at hotspots and thickness transitions | Accelerates cooling to eliminate thermal centers |
| Pouring Time | 30–60 seconds per ton of metal | Balances turbulence control and temperature loss |
Melting composition is a cornerstone in controlling shrinkage in ductile cast iron. The chemical elements significantly affect fluidity, graphite nucleation, and solidification behavior. Carbon equivalent (CE) is a key parameter, defined as: $$ CE = \%C + \frac{\%Si + \%P}{3} $$ For ductile cast iron, a CE between 4.3 and 4.5 is often optimal to enhance fluidity and reduce shrinkage. However, excessive carbon can lead to carbide formation and increased shrinkage. Silicon promotes graphite formation but must be controlled to maintain low-temperature impact toughness. Magnesium and rare earth elements are nodularizing agents but can hinder graphiteization if over-added. Phosphorus and sulfur are impurities that widen the solidification range and reduce feeding capacity. The ideal composition for wind turbine ductile cast iron, such as QT400-18AL-1, is detailed in Table 3.
| Element | Target Range | Effect on Shrinkage |
|---|---|---|
| Carbon (C) | 3.75–3.95 | Improves fluidity and graphite count; beyond 4.0 increases risk |
| Silicon (Si) | 1.8–2.3 | Promotes ferrite formation; high Si reduces ductility |
| Manganese (Mn) | 0.1–0.3 | Minimal effect; kept low to avoid segregations |
| Phosphorus (P) | ≤0.04 | Reduces feeding capability; forms low-melting phosphides |
| Sulfur (S) | ≤0.015 | Inhibits graphiteization; increases shrinkage tendency |
| Magnesium (Mg) | 0.035–0.06 | Essential for nodularization; excess leads to carbides |
| Rare Earth (RE) | 0.005–0.015 | Aids nodularization; overuse can cause shrinkage |
Inoculation treatment is crucial for achieving a high graphite nodule count and reducing shrinkage in ductile cast iron. Effective inoculation increases the number of graphite spheres, which enhances the feeding channels during solidification. The nodule count per unit area (\( N_n \)) can be related to shrinkage susceptibility by: $$ S_i \propto \frac{1}{N_n} $$ where \( S_i \) is the shrinkage index. A higher \( N_n \) (typically >150 nodules/mm²) indicates better shrinkage resistance. In practice, a combination of pre-inoculation and post-inoculation is employed. For instance, adding ferrosilicon (75% Si) at 0.3–0.5% during tapping and 0.1–0.2% during pouring significantly improves microstructure. The kinetics of inoculation can be described using: $$ \frac{dN}{dt} = k \cdot (C – C_e) $$ where \( N \) is the nodule count, \( t \) is time, \( k \) is a rate constant, \( C \) is the inoculant concentration, and \( C_e \) is the equilibrium concentration.
Pouring temperature is a vital parameter that affects shrinkage formation in ductile cast iron. Low pouring temperatures reduce fluidity and riser feeding efficiency, while high temperatures increase liquid contraction and mold wall movement. The optimal pouring temperature range for large ductile cast iron castings is 1340°C to 1360°C. The temperature drop during pouring can be estimated by: $$ \Delta T_p = \frac{h \cdot A_s \cdot (T_m – T_a) \cdot t_p}{\rho \cdot V \cdot C_p} $$ where \( \Delta T_p \) is the temperature drop, \( h \) is the heat transfer coefficient, \( A_s \) is the surface area, \( T_m \) is the metal temperature, \( T_a \) is the ambient temperature, \( t_p \) is the pouring time, \( \rho \) is density, \( V \) is volume, and \( C_p \) is specific heat. Maintaining a consistent pouring rate and using hot topping for risers are effective practices. Additionally, the solidification shrinkage volume (\( V_{ss} \)) can be calculated as: $$ V_{ss} = \alpha \cdot V_0 \cdot \Delta T_s $$ where \( \alpha \) is the solidification shrinkage coefficient (approximately 4–6% for ductile cast iron), and \( \Delta T_s \) is the temperature drop during solidification.
To prevent shrinkage defects in ductile cast iron, a holistic approach encompassing chemical composition control, casting process optimization, and melting practice refinement is essential. Based on my experience, the following measures have proven effective in industrial production of wind turbine components.
Chemical composition control requires stringent monitoring and adjustment. Using spectroscopy for real-time analysis ensures that elements remain within specified ranges. The carbon equivalent should be optimized using the formula: $$ CE_{opt} = 4.3 + 0.03 \cdot (T_{pour} – 1350) $$ where \( T_{pour} \) is the pouring temperature in °C. This adjustment accounts for temperature effects on fluidity. Additionally, residual magnesium levels should be kept at the lower end of the range to minimize carbide formation. The nodularizing treatment often involves a Mg-FeSi alloy with 5–7% Mg, added at 1.2–1.5% of the iron weight. The reaction efficiency (\( \eta_{Mg} \)) is given by: $$ \eta_{Mg} = \frac{Mg_{residual}}{Mg_{added}} \times 100\% $$ with an ideal \( \eta_{Mg} \) of 40–60% for ductile cast iron.
Casting process control involves advanced simulation and rigorous mold preparation. ProCAST simulations help visualize solidification patterns and identify potential shrinkage zones. The criterion for shrinkage prediction often uses the Niyama criterion: $$ G / \sqrt{\dot{T}} > C $$ where \( G \) is the temperature gradient, \( \dot{T} \) is the cooling rate, and \( C \) is a constant (typically 1–2 for ductile cast iron). Values below this threshold indicate shrinkage risk. In mold making, furan sand with a binder ratio of 1–1.5% and proper compaction to a hardness of 85–90 on the B-scale is recommended. Chills made of cast iron or copper are placed strategically, with their volume calculated as: $$ V_{chill} = 0.5 \cdot V_{hotspot} $$ where \( V_{hotspot} \) is the volume of the thermal center. Riser design follows modulus method: \( M_r = 1.2 \cdot M_c \), where \( M_r \) is the riser modulus and \( M_c \) is the casting modulus, defined as volume divided by cooling surface area.
Melting process control emphasizes temperature management and inoculation. Medium-frequency induction furnaces are preferred for their precise temperature control and stirring action. The melting temperature should be maintained at 1450±10°C to ensure proper dissolution of alloys and gas removal. The hydrogen and oxygen content should be kept below 2 ppm and 50 ppm, respectively, as gases contribute to microshrinkage. The degassing efficiency can be expressed as: $$ \eta_{deg} = \frac{C_i – C_f}{C_i} \times 100\% $$ where \( C_i \) and \( C_f \) are initial and final gas concentrations. Inoculation is performed using FeSi75 with 0.3–0.5% addition during tapping and 0.1–0.2% during pouring via stream inoculation. The fade time of inoculation effect is approximately 10–15 minutes, necessitating quick pouring after treatment.
To summarize the interplay of factors, I often refer to a holistic model for shrinkage prediction in ductile cast iron: $$ S = k_1 \cdot \frac{1}{CE} + k_2 \cdot \Delta T_{pour} + k_3 \cdot \frac{1}{G} + k_4 \cdot P_{impurity} $$ where \( S \) is the shrinkage severity, \( k_1 \), \( k_2 \), \( k_3 \), \( k_4 \) are constants, \( CE \) is carbon equivalent, \( \Delta T_{pour} \) is the deviation from optimal pouring temperature, \( G \) is the temperature gradient, and \( P_{impurity} \) is the impurity level (P + S). This empirical formula underscores the need for balanced control across all parameters.
Implementing these measures has significantly reduced shrinkage defects in ductile cast iron wind turbine castings. For example, in a production batch of hub castings, the rejection rate due to shrinkage dropped from 15% to below 3% after optimizing composition and gating design. Mechanical properties consistently meet standards such as EN 12680 for ultrasonic testing and EN 1369 for magnetic particle inspection. The microstructure of ductile cast iron after improvement shows over 90% nodularity and ferrite content above 90%, with carbides below 1%, as specified in Table 4.
| Parameter | Minimum Requirement | Typical Achieved Value |
|---|---|---|
| Nodularity | ≥90% | 92–95% |
| Ferrite Content | ≥90% | 92–98% |
| Carbide Content | ≤1% | 0.2–0.8% |
| Graphite Size | Grade 5 or finer | Grade 5–6 |
| Phosphide Content | ≤1% | 0.3–0.6% |
In conclusion, shrinkage defects in ductile cast iron for wind turbines are manageable through a systematic approach that addresses design, process, and metallurgical factors. The unique solidification behavior of ductile cast iron necessitates careful control of chemical composition, especially carbon, silicon, and magnesium, alongside optimized gating and risering systems. Simulation tools and mathematical models provide valuable insights for predicting and preventing shrinkage. As wind turbine components continue to grow in size and complexity, ongoing research and adaptation of these strategies will be essential. By leveraging advanced technologies and empirical data, manufacturers can enhance the quality and performance of ductile cast iron castings, ensuring their reliability in demanding environmental conditions. The journey toward defect-free ductile cast iron is iterative, but with diligent application of these principles, significant improvements are attainable.
Looking ahead, emerging techniques such as additive manufacturing for mold cores and real-time monitoring with IoT sensors promise further advancements in shrinkage control for ductile cast iron. However, the fundamentals of sound casting practice remain rooted in understanding the material’s behavior and applying rigorous controls. Through continuous learning and innovation, the industry can overcome the challenges posed by shrinkage, paving the way for more efficient and durable wind energy systems.