
In the manufacturing of injection molding machines, the front plate of the shooting table is a critical component that ensures efficient injection, stable operation, and provides the required clamping force. This part directly influences the quality of molded products. The casting of this component, made from ductile cast iron, presents significant challenges due to its complex geometry, high precision requirements for oil cylinder holes, and the need to withstand high hydraulic pressures. In this article, I will detail the casting process design for a high-hydraulic-pressure ductile cast iron front plate, focusing on the gating system, cooling system, chemical composition selection, and melt treatment controls. The goal is to achieve a defect-free casting with superior mechanical properties and microstructure.
The front plate casting has a weight of approximately 1,700 kg, with a pouring weight of 1,850 kg. Its dimensions are 1,330 mm × 620 mm × 850 mm, featuring a maximum wall thickness of 360 mm and a minimum of 40 mm. The material specification is QT450-10A, a grade of ductile cast iron that requires high tensile strength, yield strength, and elongation. Additionally, the oil cylinder holes must be free from shrinkage porosity and cavities, with a machined surface roughness of Ra 0.4–0.8 μm and the ability to endure hydraulic pressures up to 20 MPa. These stringent demands necessitate a meticulous casting process design.
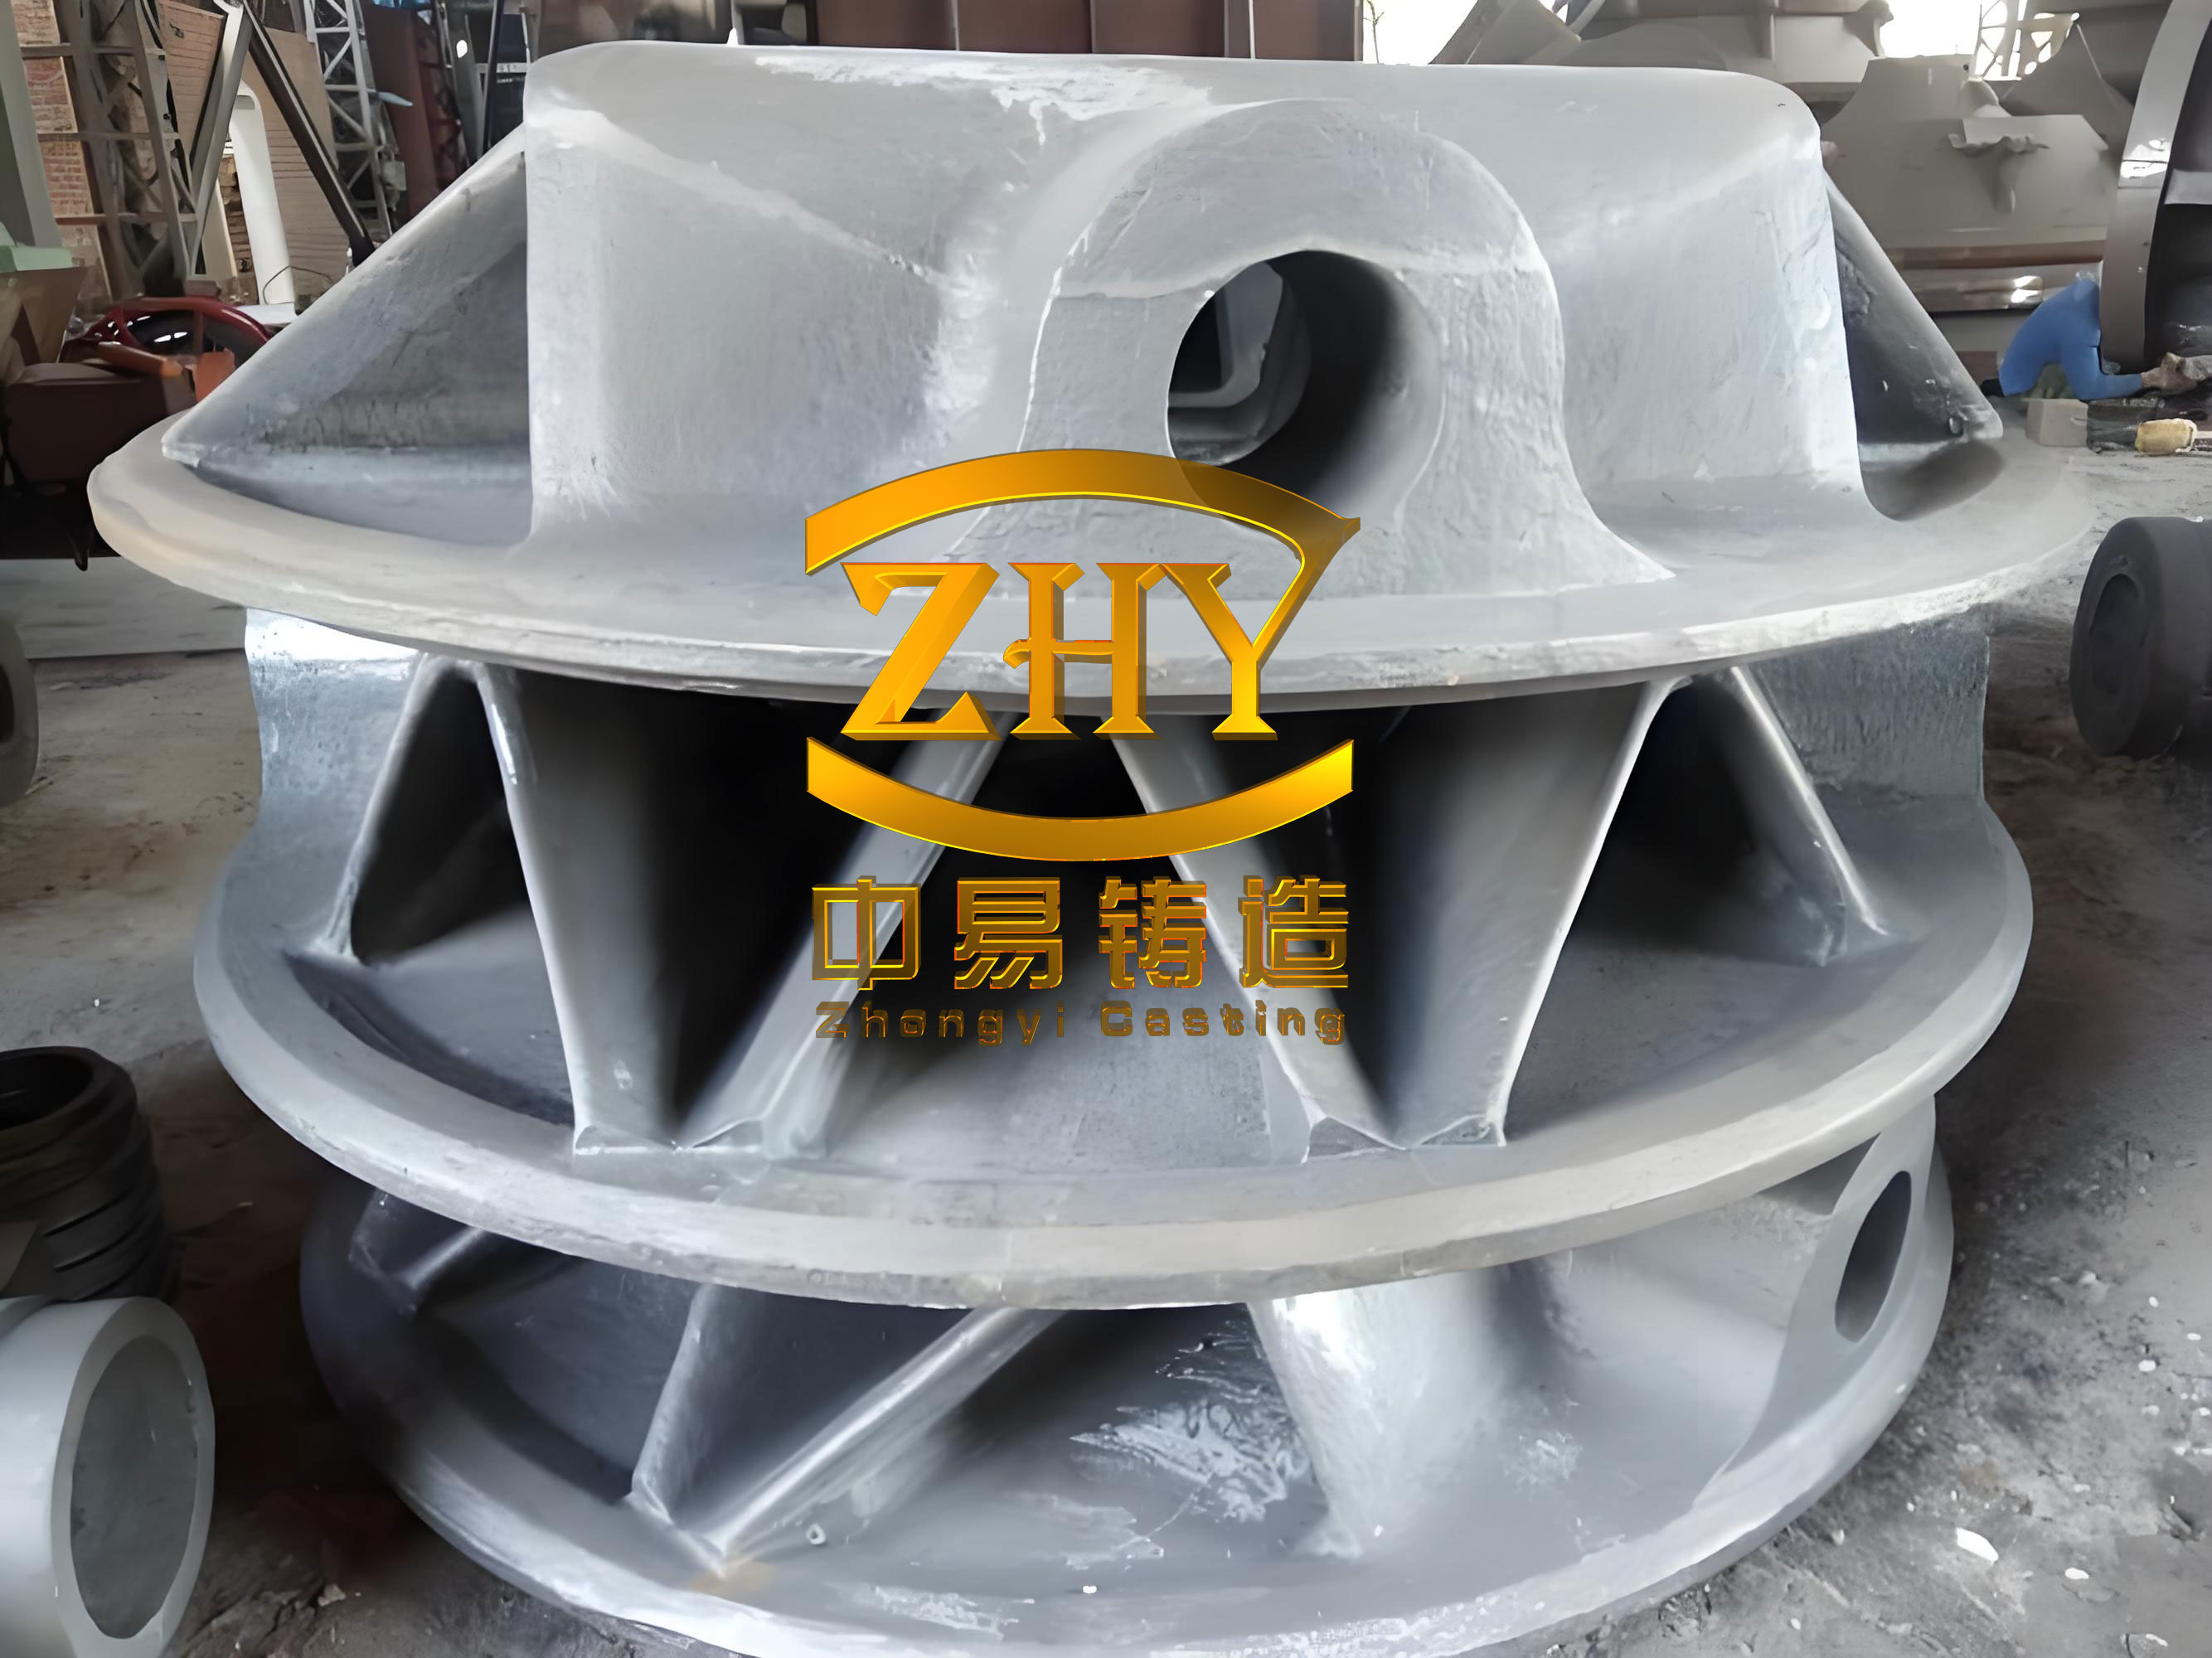
The casting process for ductile cast iron components like the shooting table front plate involves several key aspects. First, the gating and risering system must ensure smooth filling, minimal turbulence, and effective feeding during solidification. Second, a cooling system using chills and specialized sand cores is essential to control solidification patterns and eliminate defects in critical areas. Third, the chemical composition of the ductile cast iron must be optimized to achieve the desired microstructure and mechanical properties. Finally, rigorous control over spheroidization, inoculation, and pouring processes is crucial. Throughout this discussion, I will emphasize the importance of ductile cast iron in meeting these challenges, and I will present formulas and tables to summarize key parameters.
Gating and Riser System Design
For the gating system design, the primary consideration is to allow high-temperature iron to enter the mold cavity quickly and disperse evenly, maximizing slag trapping and venting while reducing the likelihood of shrinkage defects. Based on the structural characteristics of the shooting table front plate, a semi-open, bottom-gating system was adopted. The ingates are located on one side of the casting, following the principle of “large flow rate, low velocity, and stable, clean filling.” This approach ensures uniform temperature distribution in the cavity, smooth filling, rapid mold filling, and minimizes shrinkage formation, all while saving production costs.
The sprue and ingates are made entirely of ceramic tubes to reduce erosion defects. The choke section is set at the sprue, and a filter is designed in the runner. The cross-sectional area ratio of the gating system is ΣFsprue : ΣFrunner : ΣFingate = 1 : 1.25 : 1.10. The pouring time is controlled within 120–150 seconds. According to the large orifice outflow theory, the choke area of the sprue is calculated using the formula:
$$ F_{\text{sprue}} = \frac{G}{0.31 \times \mu \times t \times \sqrt{H_p}} $$
where:
- \( G \) is the pouring weight of iron (1,850 kg),
- \( \mu \) is the flow coefficient (0.35),
- \( t \) is the pouring time (taken as 140 s),
- \( H_p \) is the average pressure head (10.02 mm).
Substituting the values:
$$ F_{\text{sprue}} = \frac{1850}{0.31 \times 0.35 \times 140 \times \sqrt{10.02}} \approx 38.48 \, \text{cm}^2 $$
This corresponds to one ceramic tube with an inner diameter of 70 mm for the sprue. Based on the area ratio, the runner cross-section is 30/40 high 70, and there are six ingates with inner diameters of 30 mm each.
Considering the structural features and experience with risers for ductile cast iron, two safety risers are placed above the two oil cylinder holes. These risers provide a small amount of liquid metal supplementation during cooling and solidification shrinkage, allow venting of gases generated during pouring to reduce air entrapment in the oil cylinder areas, and utilize graphitization expansion to achieve a denser casting body, further enhancing the quality of the oil cylinder holes.
The overall gating and riser system is designed for convenient molding and effective slag removal. Due to the complex surface structure of the front plate and the high technical requirements for the oil cylinder holes, a three-part molding box is used to facilitate shaping and improve efficiency.
| Component | Cross-Sectional Area (cm²) | Dimensions | Quantity |
|---|---|---|---|
| Sprue | 38.48 | Φ70 mm ID ceramic tube | 1 |
| Runner | 48.10 (calculated from ratio) | 30/40 high 70 | 1 |
| Ingates | 42.33 (total for 6 ingates) | Φ30 mm ID ceramic tubes | 6 |
| Risers | N/A | Safety risers above oil holes | 2 |
Cooling System Design
Chills are employed to accelerate cooling at hot spots, reduce the thermal modulus at fillets, and prevent shrinkage porosity and cavities. Analysis of the product structure indicates that hot spots are likely to form at four bosses. Since these bosses have relatively small areas, four chills with dimensions of 100 mm × 100 mm × 80 mm are selected to increase the cooling rate at these locations.
To meet the requirements for surface roughness and hydraulic pressure resistance in the oil cylinder holes, these areas must be free from shrinkage defects. While chills can mitigate defects, they often only relocate defects to non-critical areas rather than eliminating them entirely. Therefore, a combination of chills and feeding paths is necessary to achieve directional solidification and move defects to the risers. Additionally, careful control of pouring temperature and inoculation is required to avoid chill-related issues like white iron formation.
For the oil cylinder holes, a cooling method using a sand core combined with a cast iron core frame is adopted. This design includes a cast iron core frame enveloped by an outer layer of molding sand, which consists of a mixture of 30% chromite sand and 70% ordinary silica sand. The coating thickness is 20–30 mm, and after core formation, the strength of the outer sand layer is controlled between 0.9–1.1 MPa. This approach ensures uniform cooling, minimizes sand drop, and results in a dense microstructure on the hydraulic working surfaces without defects like slag inclusions, gas pores, or white iron.
Simulation analysis comparing a conventional sand core with the sand core plus cast iron frame shows that the latter significantly reduces hot spots and shrinkage defects. The thermal modulus and defect distribution are improved, ensuring the performance of the oil cylinder holes in ductile cast iron castings.
| Element | Type/Material | Dimensions/Composition | Purpose |
|---|---|---|---|
| Chills | Cast iron | 100 mm × 100 mm × 80 mm | Accelerate cooling at bosses |
| Sand Core for Oil Holes | Chromite-silica sand mix on cast iron frame | 30% chromite sand, 70% silica sand, 20–30 mm thickness | Uniform cooling, defect prevention |
| Core Strength | N/A | 0.9–1.1 MPa | Ensure integrity during pouring |
Chemical Composition Selection and Melt Treatment Control
The chemical composition of ductile cast iron is critical for achieving the desired properties. For the QT450-10A grade used in this front plate, the following elements are carefully controlled:
- Carbon (C) and Carbon Equivalent (CE): High carbon content promotes graphite precipitation, enabling self-feeding through graphite expansion to prevent shrinkage. A high CE improves fluidity. Carbon is controlled at 3.45–3.65%, and CE at 4.30–4.45%. The carbon equivalent is calculated as:
$$ \text{CE} = \%\text{C} + \frac{\%\text{Si} + \%\text{P}}{3} $$
For typical values, this ensures good castability and graphite formation in ductile cast iron.
- Silicon (Si): Silicon is a graphitizing element that reduces carbides, pearlite, and phosphide eutectics while increasing ferrite content. It also solid-solution strengthens ferrite, enhancing strength and hardness. Silicon is kept at 2.3–2.6% to balance ductility and strength.
- Manganese (Mn): Manganese stabilizes carbides and promotes pearlite formation. However, excessive Mn can lead to segregation and degraded mechanical properties. For this ductile cast iron component, Mn is limited to below 0.4% (0.25–0.40%) to maintain tensile strength without compromising elongation.
- Phosphorus (P) and Sulfur (S): These are harmful impurities. Phosphorus must be strictly below 0.02% to avoid excessive phosphide eutectics that reduce plasticity and toughness. Sulfur, an anti-graphitizing element, consumes spheroidizing agents and is controlled below 0.015%.
- Residual Magnesium (Mg) and Rare Earth (RE): After spheroidization, residual Mg should be 0.03–0.05%, and RE 0.01–0.03%, to ensure effective nodularization of graphite in ductile cast iron.
| Element | Target Range (wt.%) | Role in Ductile Cast Iron |
|---|---|---|
| Carbon (C) | 3.45–3.65 | Promotes graphite formation, self-feeding |
| Silicon (Si) | 2.3–2.6 | Graphitizer, strengthens ferrite |
| Manganese (Mn) | < 0.4 (0.25–0.40) | Enhances strength, but limited to avoid segregation |
| Phosphorus (P) | < 0.02 | Minimize harmful phosphides |
| Sulfur (S) | < 0.015 | Reduce anti-graphitizing effects |
| Residual Mg | 0.03–0.05 | Ensure graphite spheroidization |
| Residual RE | 0.01–0.03 | Aid nodularization and microstructure control |
| Iron (Fe) | Balance | Base metal |
For spheroidization and inoculation, the spheroidizer addition is set at 1.10–1.20% to achieve the target residual Mg and RE levels. The spheroidization process involves pouring a large flow of iron into the treatment ladle to improve recovery of Mg and RE and enhance desulfurization. After treatment, slag is thoroughly skimmed, and the iron is covered with pearlite to prevent re-sulfurization.
To improve the nodularity and graphite stability in the ductile cast iron, a multiple inoculation process is employed. This includes late inoculation during pouring, with an inoculant addition of about 0.10%. The inoculation enhances graphite nucleation, refines graphite size, and improves the overall properties of the ductile cast iron casting.
Pouring is controlled with low-temperature, rapid pouring to minimize residual stresses and avoid misruns. The pouring temperature is maintained between 1,290–1,320°C, and pouring is completed within 20 minutes after spheroidization to ensure good nodularization in the ductile cast iron.
Implementation Results
Three trial castings of the front plate were produced. The castings were inspected using penetrant testing (PT) according to EN 1371 standard, achieving quality grade I. The oil cylinder holes were free from casting defects. Attached test blocks were evaluated for mechanical properties and microstructure.
The mechanical properties met the customer’s standards: tensile strength ≥ 390 MPa, yield strength ≥ 260 MPa, elongation ≥ 8%, and hardness within 160–210 HB. The microstructure showed a nodularity ≥ 85% and graphite size of 4–7, as required for high-quality ductile cast iron.
| Property | Standard Requirement | Measured Value |
|---|---|---|
| Tensile Strength | ≥ 390 MPa | 480 MPa |
| Yield Strength | ≥ 260 MPa | 340 MPa |
| Elongation | ≥ 8% | 11% |
| Hardness (HB) | 160–210 | 162 |
| Nodularity | ≥ 85% | 90% |
| Graphite Size | 4–7 | 6 |
The successful production demonstrates that the designed casting process is effective for manufacturing high-integrity ductile cast iron components like the shooting table front plate. The combination of proper gating, cooling, and melt treatment ensures defect-free castings with excellent performance under high hydraulic pressures.
Conclusions
Based on the design and trial production, the following conclusions can be drawn for the casting process of the high-hydraulic-pressure ductile cast iron front plate:
- The optimal chemical composition for QT450-10A ductile cast iron includes carbon at 3.45–3.65%, silicon at 2.3–2.6%, manganese below 0.4%, phosphorus below 0.02%, sulfur below 0.015%, residual magnesium at 0.03–0.05%, and residual rare earth at 0.01–0.03%. This composition ensures good graphite nodularization and mechanical properties.
- The gating system using a bottom-gated, multi-ingate design with ceramic tubes ensures smooth filling and reduces shrinkage defects. Risers and chills are combined to provide liquid feeding and enhance cooling at critical areas, improving density and material performance in ductile cast iron castings.
- The cooling method employing a sand core with a cast iron frame for the oil cylinder holes significantly improves performance, meeting the requirements for surface roughness (Ra 0.4–0.8 μm) and hydraulic pressure resistance (20 MPa). This approach minimizes defects and ensures a dense microstructure.
- Multiple inoculation, including late inoculation during pouring, enhances nodularity, refines graphite, and improves the overall properties of ductile cast iron. Controlled pouring at 1,290–1,320°C within 20 minutes after spheroidization is essential for quality consistency.
This process design highlights the versatility and reliability of ductile cast iron for demanding applications. Future work could focus on optimizing simulation models for defect prediction and exploring advanced inoculants to further enhance the properties of ductile cast iron components. The integration of these elements ensures that ductile cast iron remains a preferred material for high-performance castings in industries such as injection molding machinery.