
In my extensive experience within the foundry industry, the lost foam casting process has proven to be a transformative technology for producing complex, high-quality castings with significant advantages in dimensional accuracy, surface finish, and cost-effectiveness. The heart of this process lies in the foam pattern, and consequently, the mold used to create that pattern. The design of this mold is not merely a mechanical exercise; it is a critical engineering endeavor that directly dictates pattern quality, production efficiency, and the final integrity of the cast component. A poorly designed mold can introduce defects, increase labor, and escalate costs, while an optimized design streamlines the entire lost foam casting process. This article, drawn from practical application and refinement, delves into the essential design principles and key technologies for molds used in the lost foam casting process, employing analytical summaries, formulas, and tables to consolidate this knowledge.
The fundamental principle of the lost foam casting process begins with pattern formation. Expanded polystyrene (EPS) beads, pre-foamed to a specific density, are filled into a mold cavity. Live steam is then injected, which softens the bead surfaces and causes the residual blowing agent inside each bead to vaporize and expand. This secondary expansion forces the beads to fuse together at their boundaries, forming a cohesive, solid foam replica of the mold cavity. Finally, cooling water is circulated to set the pattern’s shape before demolding. This cycle of filling, heating, and cooling is the core of pattern production in the lost foam casting process. The efficiency and consistency of this cycle are wholly dependent on mold design.
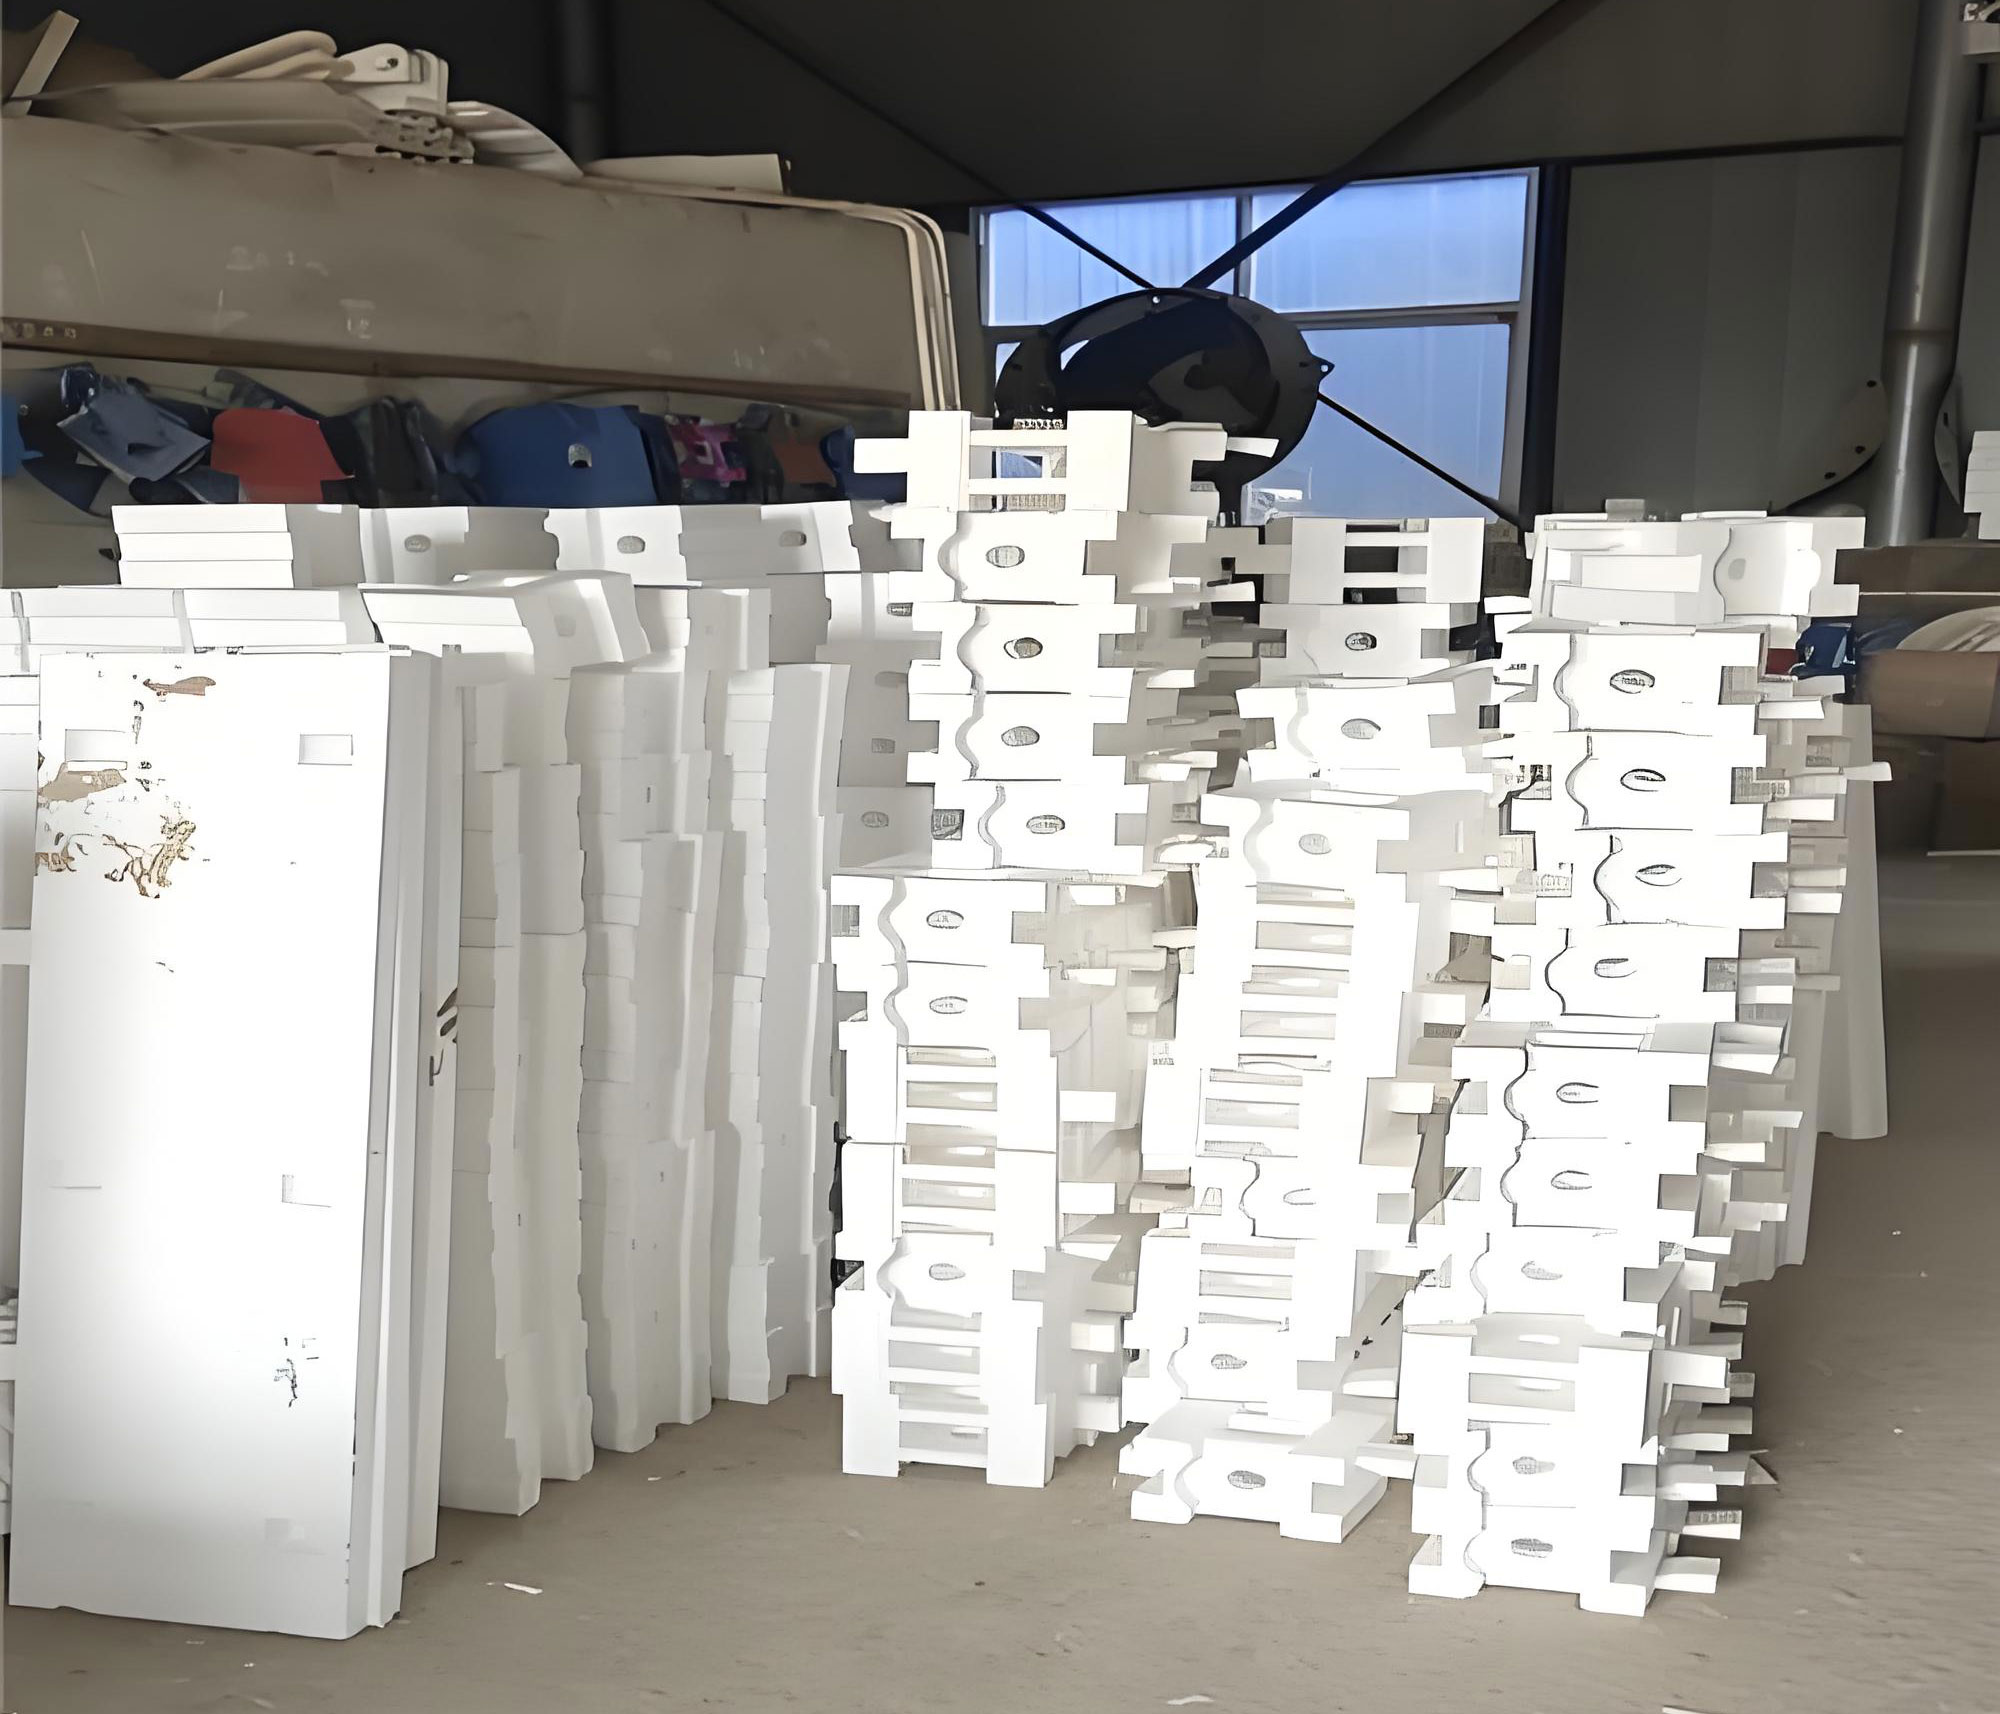
Optimizing the mold for the lost foam casting process requires a systematic approach across multiple design domains. The first critical decision is parting line selection. For simple geometries, a straight parting line along the largest contour is optimal for mold simplicity and easy demolding. For complex parts like engine blocks or transmission housings—common applications in the lost foam casting process—stepped or multi-part splits may be necessary. A key consideration is ensuring precise alignment between mold halves. We typically employ a pin-and-bush system or integrated raised bosses on one half and corresponding recesses on the other. This not only prevents pattern mismatch but also facilitates automated gluing operations when bonding pattern sections, a common step in the lost foam casting process for complex castings.
A fundamental calculation in mold design for the lost foam casting process is the total shrinkage allowance. This must compensate for two distinct contractions: the shrinkage of the foam pattern itself after demolding and aging, and the solidification shrinkage of the molten metal. For a common material like HT200 gray iron, the metal shrinkage ($S_m$) is approximately 0.8% to 1.0%. The pattern shrinkage ($S_p$) depends on bead type and process conditions; for EPS, it typically ranges from 0.3% to 0.5%. The total mold shrinkage allowance ($S_{total}$) is therefore the sum:
$$ S_{total} = S_p + S_m $$
Based on production data, we often apply a unified allowance. For instance, with $S_p \approx 0.5\%$ and $S_m \approx 0.8\%$, a total allowance of 1.3% is frequently used for molds in the lost foam casting process for iron castings. This is applied uniformly to all relevant pattern dimensions.
Machining allowances and draft angles are added to the final mold cavity. A standard machining allowance of 3 mm is common, though it can be increased in areas prone to dimensional variation. Draft angles are crucial for demolding the fragile foam pattern without distortion. While a minimum angle of 1° is standard, areas with deep draws or thin sections may require more. For thin-walled patterns common in the lost foam casting process, internal ribs or gussets are often designed into the mold to prevent pattern warping or collapse during handling and coating. This structural reinforcement is vital for maintaining pattern fidelity.
The evolution from manual to automated features represents a significant advancement in mold design for the lost foam casting process. Traditionally, complex undercuts or internal features were handled by manual inserts or loose pieces. While low-cost, this approach is labor-intensive, prone to misplacement causing dimensional errors, and often results in flash that requires manual trimming. Modern practice favors integrated core-pulling mechanisms. For a transmission housing mold, replacing nine manual inserts with automated hydraulic or pneumatic core-pullers increased production rate by 38% and eliminated related quality variations. The choice of mechanism depends on the core’s size, travel distance, and required force. A common design uses angled leader pins and slides. The force required to withdraw a core ($F_{pull}$) can be estimated by considering the friction and the surface area of the core in contact with the fused foam:
$$ F_{pull} \approx \mu \cdot P_{contact} \cdot A_{surface} $$
where $\mu$ is the coefficient of friction between foam and mold material, $P_{contact}$ is the contact pressure from the expanded beads, and $A_{surface}$ is the core’s surface area. Automated systems must be designed to provide a force margin above this calculated value for reliable operation in the high-cycle lost foam casting process.
Pattern filling uniformity is paramount. The design of fill gates (or shot holes) directly impacts density distribution. The number, location, and size of gates are determined by the cavity volume and geometry. For a long, tubular part like a housing, two opposed gates allow for balanced filling. We use automated shot nozzles with an internal diameter of 16 mm. The fill time ($t_{fill}$) can be modeled in relation to the pressure differential ($\Delta P$), bead fluidity, and gate area ($A_{gate}$):
$$ t_{fill} \propto \frac{V_{cavity}}{A_{gate} \cdot v_{bead}(\Delta P)} $$
where $v_{bead}$ is the bead velocity, a function of the pressure push. Implementing pressurized filling reduced our cycle time by approximately 8 seconds, demonstrating how gate design optimizes the lost foam casting process efficiency.
Mold wall thickness is a critical thermal management parameter in the lost foam casting process. It represents a compromise between structural strength, heat transfer rate, and cycle time. Standard wall thickness ranges from 15 mm to 20 mm. Excessively thick walls act as a thermal mass, slowing both heating and cooling phases and reducing productivity. Excessively thin walls may lack durability. The heat transfer during the steam heating phase can be approximated by Fourier’s law for conduction through the mold wall:
$$ Q = \frac{k \cdot A \cdot (T_{steam} – T_{mold})}{d} $$
Here, $Q$ is the heat flux, $k$ is the thermal conductivity of the mold material (typically aluminum), $A$ is the surface area, $T_{steam}$ is the steam temperature, $T_{mold}$ is the initial mold temperature, and $d$ is the wall thickness. Therefore, reducing $d$ in specific areas increases $Q$, accelerating bead fusion. In practice, we selectively reduce wall thickness to 12.5 mm in locally massive pattern sections to prevent under-fusion or post-expansion defects, a common issue in the lost foam casting process.
Venting is arguably one of the most delicate aspects of mold design for the lost foam casting process. Vent plugs (or vents) must allow air and steam to escape while preventing bead ingress. Their diameter, quantity, and distribution are carefully planned. A dense array of vents is required in deep recesses, corners, and thick sections to prevent air traps that cause voids. We specify vents with pin-point orifices (0.5 mm diameter) and maintain a center-to-center spacing generally below 20 mm, reducing to 15 mm in problematic areas. The total vent area ($A_{vent}$) should be sufficient to allow rapid gas egress without creating a pressure build-up that could deform the softening beads. An empirical relationship ties vent area to projected cavity area and material flow characteristics.
| Design Parameter | Typical Value/Range | Function & Consideration |
|---|---|---|
| Parting Line Type | Straight, Stepped, Multi-part | Determines mold complexity and demolding ease. |
| Total Shrinkage Allowance (for HT200) | 1.3% (0.5% pattern + 0.8% metal) | Compensates for foam aging and metal solidification shrinkage. |
| Machining Allowance | 3 mm (standard) | Provides material for final machining of the casting. |
| Draft Angle | 1° (minimum), higher for deep features | Facilitates pattern removal without damage. |
| Mold Wall Thickness | 15-20 mm (standard), locally adjustable | Balances structural integrity and thermal transfer. |
| Vent Plug Diameter | 0.5 mm (orifice), 4-10 mm (housing) | Allows gas escape while blocking bead entry. |
| Vent Spacing | < 20 mm (general), < 15 mm (thick sections) | Ensures uniform deaeration of the cavity. |
| Fill Gate Diameter | 16 mm (example) | Governs bead injection speed and filling pattern. |
Cooling system design is essential for stabilizing the pattern and achieving a fast cycle time in the lost foam casting process. Water channels are machined close to the cavity surface to maximize heat extraction. The cooling phase must be rapid and uniform to “set” the fused bead structure. Initially, gravity drainage was used, but we found that implementing a vacuum-assisted drainage system significantly improved operational cleanliness and consistency. By applying a vacuum of -0.7 MPa for about 18 seconds after water injection, we ensure complete water removal without splash-back upon mold opening. The required cooling time ($t_{cool}$) can be related to the thermal diffusivity ($\alpha$) of the foam and the thickness of the pattern section ($L$):
$$ t_{cool} \propto \frac{L^2}{\alpha} $$
This square relationship highlights why controlling pattern wall thickness and ensuring efficient mold cooling are so critical in the lost foam casting process.
The layout of the mold, including its platen mounting and the design of the steam/air chambers (often called the “steam chest” or “plenum”), is crucial. The chamber behind the mold cavity must have sufficient volume to ensure even steam distribution and effective vacuum during cooling, but it should not be excessively large as it adds to the thermal mass. A significant improvement was made by relocating ejector cylinders from inside the mold frame to an external position. This change reduced the chamber height from 100 mm to 75 mm, decreasing the volume of air and steam that needed to be heated and cooled, thereby boosting thermal efficiency and reducing cycle time in the lost foam casting process.
| Feature | Manual Design (Traditional) | Automated Design (Modern) | Impact on Lost Foam Casting Process |
|---|---|---|---|
| Core/Undercut Handling | Loose inserts, hand-loaded/unloaded | Integrated hydraulic/pneumatic core-pullers | ↑ Productivity (e.g., +38%), ↓ Labor, ↑ Consistency |
| Pattern Demolding | Manual removal, risk of distortion | Robotic arms or vacuum suction cup extractors | ↑ Pattern quality, enables one-operator multi-machine cells |
| Cooling Water Removal | Gravity drainage, potential splash | Vacuum-assisted drainage system | ↑ Shop cleanliness, ↑ Cooling consistency, ↓ Cycle time |
| Pattern Section Bonding | Manual glue application | Automated gluing robots following定位 points | ↑ Gluing precision, ↑ Throughput, ↓ Adhesive waste |
Finally, auxiliary mechanisms contribute significantly to a robust lost foam casting process. For instance, incorporating vacuum suction cups on an extractor arm to gently lift the pattern from the mold eliminates handling damage and fingerprints. This simple, low-cost automation improves quality control and facilitates higher levels of automation, moving the lost foam casting process closer to full lights-out production for high-volume components.
In conclusion, the design of molds for the lost foam casting process is a multidisciplinary challenge integrating mechanical design, thermal engineering, and material science. Success hinges on a holistic view that considers parting strategy, precise shrinkage calculation, the strategic use of automation over manual interventions, optimized filling and venting, controlled wall thickness for thermal management, efficient cooling, and intelligent overall layout. The trend is unmistakably toward greater automation in every aspect—core pulling, demolding, and handling—to reduce variability, improve working conditions, and enhance the overall economics of the lost foam casting process. Each design decision, from the macroscopic parting line to the microscopic vent hole, reverberates through the entire production chain, ultimately determining the quality and cost of the final casting. Therefore, a deep, analytical, and practical understanding of these mold design principles is indispensable for anyone seeking to master the lost foam casting process.