
Abstract. The production of a sound shell-shaped ductile iron casting is often difficult because the combination of thin walls, local thick sections, and a central bore creates a complex solidification sequence. In this article, we describe our work on a QT500-7 ductile iron shell casting. We designed two casting process variants: one using blind risers with ingates and the other using an open conformal pressing-edge riser. Both designs were evaluated with three-dimensional numerical simulation of the solidification process. The simulation was used to compare residual liquid distribution, feeding paths, hot-spot development, and the risk of shrinkage porosity. The open pressing-edge riser design proved to be more reliable and was selected for production. The actual castings were sound and met the required quality after machining. Our practical experience confirms that the combination of simulation and a rational ductile iron casting design procedure leads to a robust manufacturing solution.
Keywords. ductile iron casting; casting process; numerical simulation; shell casting; shrinkage porosity
1. Introduction
Ductile iron casting is one of the most versatile manufacturing routes for components that require high strength, good wear resistance, and moderate ductility. In particular, the grade QT500-7 offers a good balance between tensile strength and elongation, which makes it suitable for instrument housings, valve bodies, and shell-type parts used in mechanical equipment. However, ductile iron casting is not a trouble-free process if the solidification conditions are not controlled carefully. Although the precipitation of graphite during eutectic solidification leads to volumetric expansion, this expansion does not always compensate for the earlier liquid contraction and the later solid contraction.
Shrinkage porosity is the most common defect in shell-shaped ductile iron castings. It usually occurs in regions that are geometrically isolated by premature solidification of the surrounding metal. Once the feeding channel is blocked, the remaining liquid cannot reach those hot spots. The consequence is internal micro-porosity, decreased pressure tightness, and rejection after machining. In our experience, this type of defect is especially dangerous because it may be hidden under a sound external surface until the part is machined.
Numerical simulation is now an important part of our process development work. It allows us to see the temperature field and the residual liquid distribution at any time during solidification. For a ductile iron casting, the main value of simulation is not only to predict defects but also to compare alternative riser geometries without the cost of repeated shop trials. In this project, we used a commercial finite-element solver to analyze two process plans for a shell-shaped ductile iron casting. The simulation results were then used to choose the better plan and to guide the actual production.
2. Material and Component Requirements
The shell casting investigated in this work is made of QT500-7 ductile iron. This material has a mixed ferritic-pearlitic matrix after normal casting and heat treatment. It combines a minimum tensile strength of 500 MPa with at least 7% elongation, which makes it useful for mechanical instrument components that may be subjected to vibration or moderate pressure. The ductile iron casting must also be machinable and free from harmful internal discontinuities.
The chemical composition of the alloy used for this ductile iron casting is given in Table 1. Magnesium and rare earth elements are present as residual spheroidizing agents. The carbon equivalent is maintained near the eutectic composition so that the graphite can nucleate as spheroids rather than flakes.
| Element | Mass fraction (wt.%) |
|---|---|
| C | 3.5–3.9 |
| Si | 2.0–2.8 |
| Mn | 0.3–0.6 |
| P | ≤ 0.07 |
| S | ≤ 0.02 |
| Mg residual | 0.03–0.06 |
| RE residual | 0.02–0.04 |
The required mechanical properties of the material are summarized in Table 2. These values were used as acceptance criteria after production and machining.
| Property | Minimum value |
|---|---|
| Tensile strength Rm | 500 MPa |
| Yield strength Rp0.2 | 320 MPa |
| Elongation A | 7% |
| Hardness | 170–230 HBW |
3. Geometry and Solidification Characteristics of the Shell
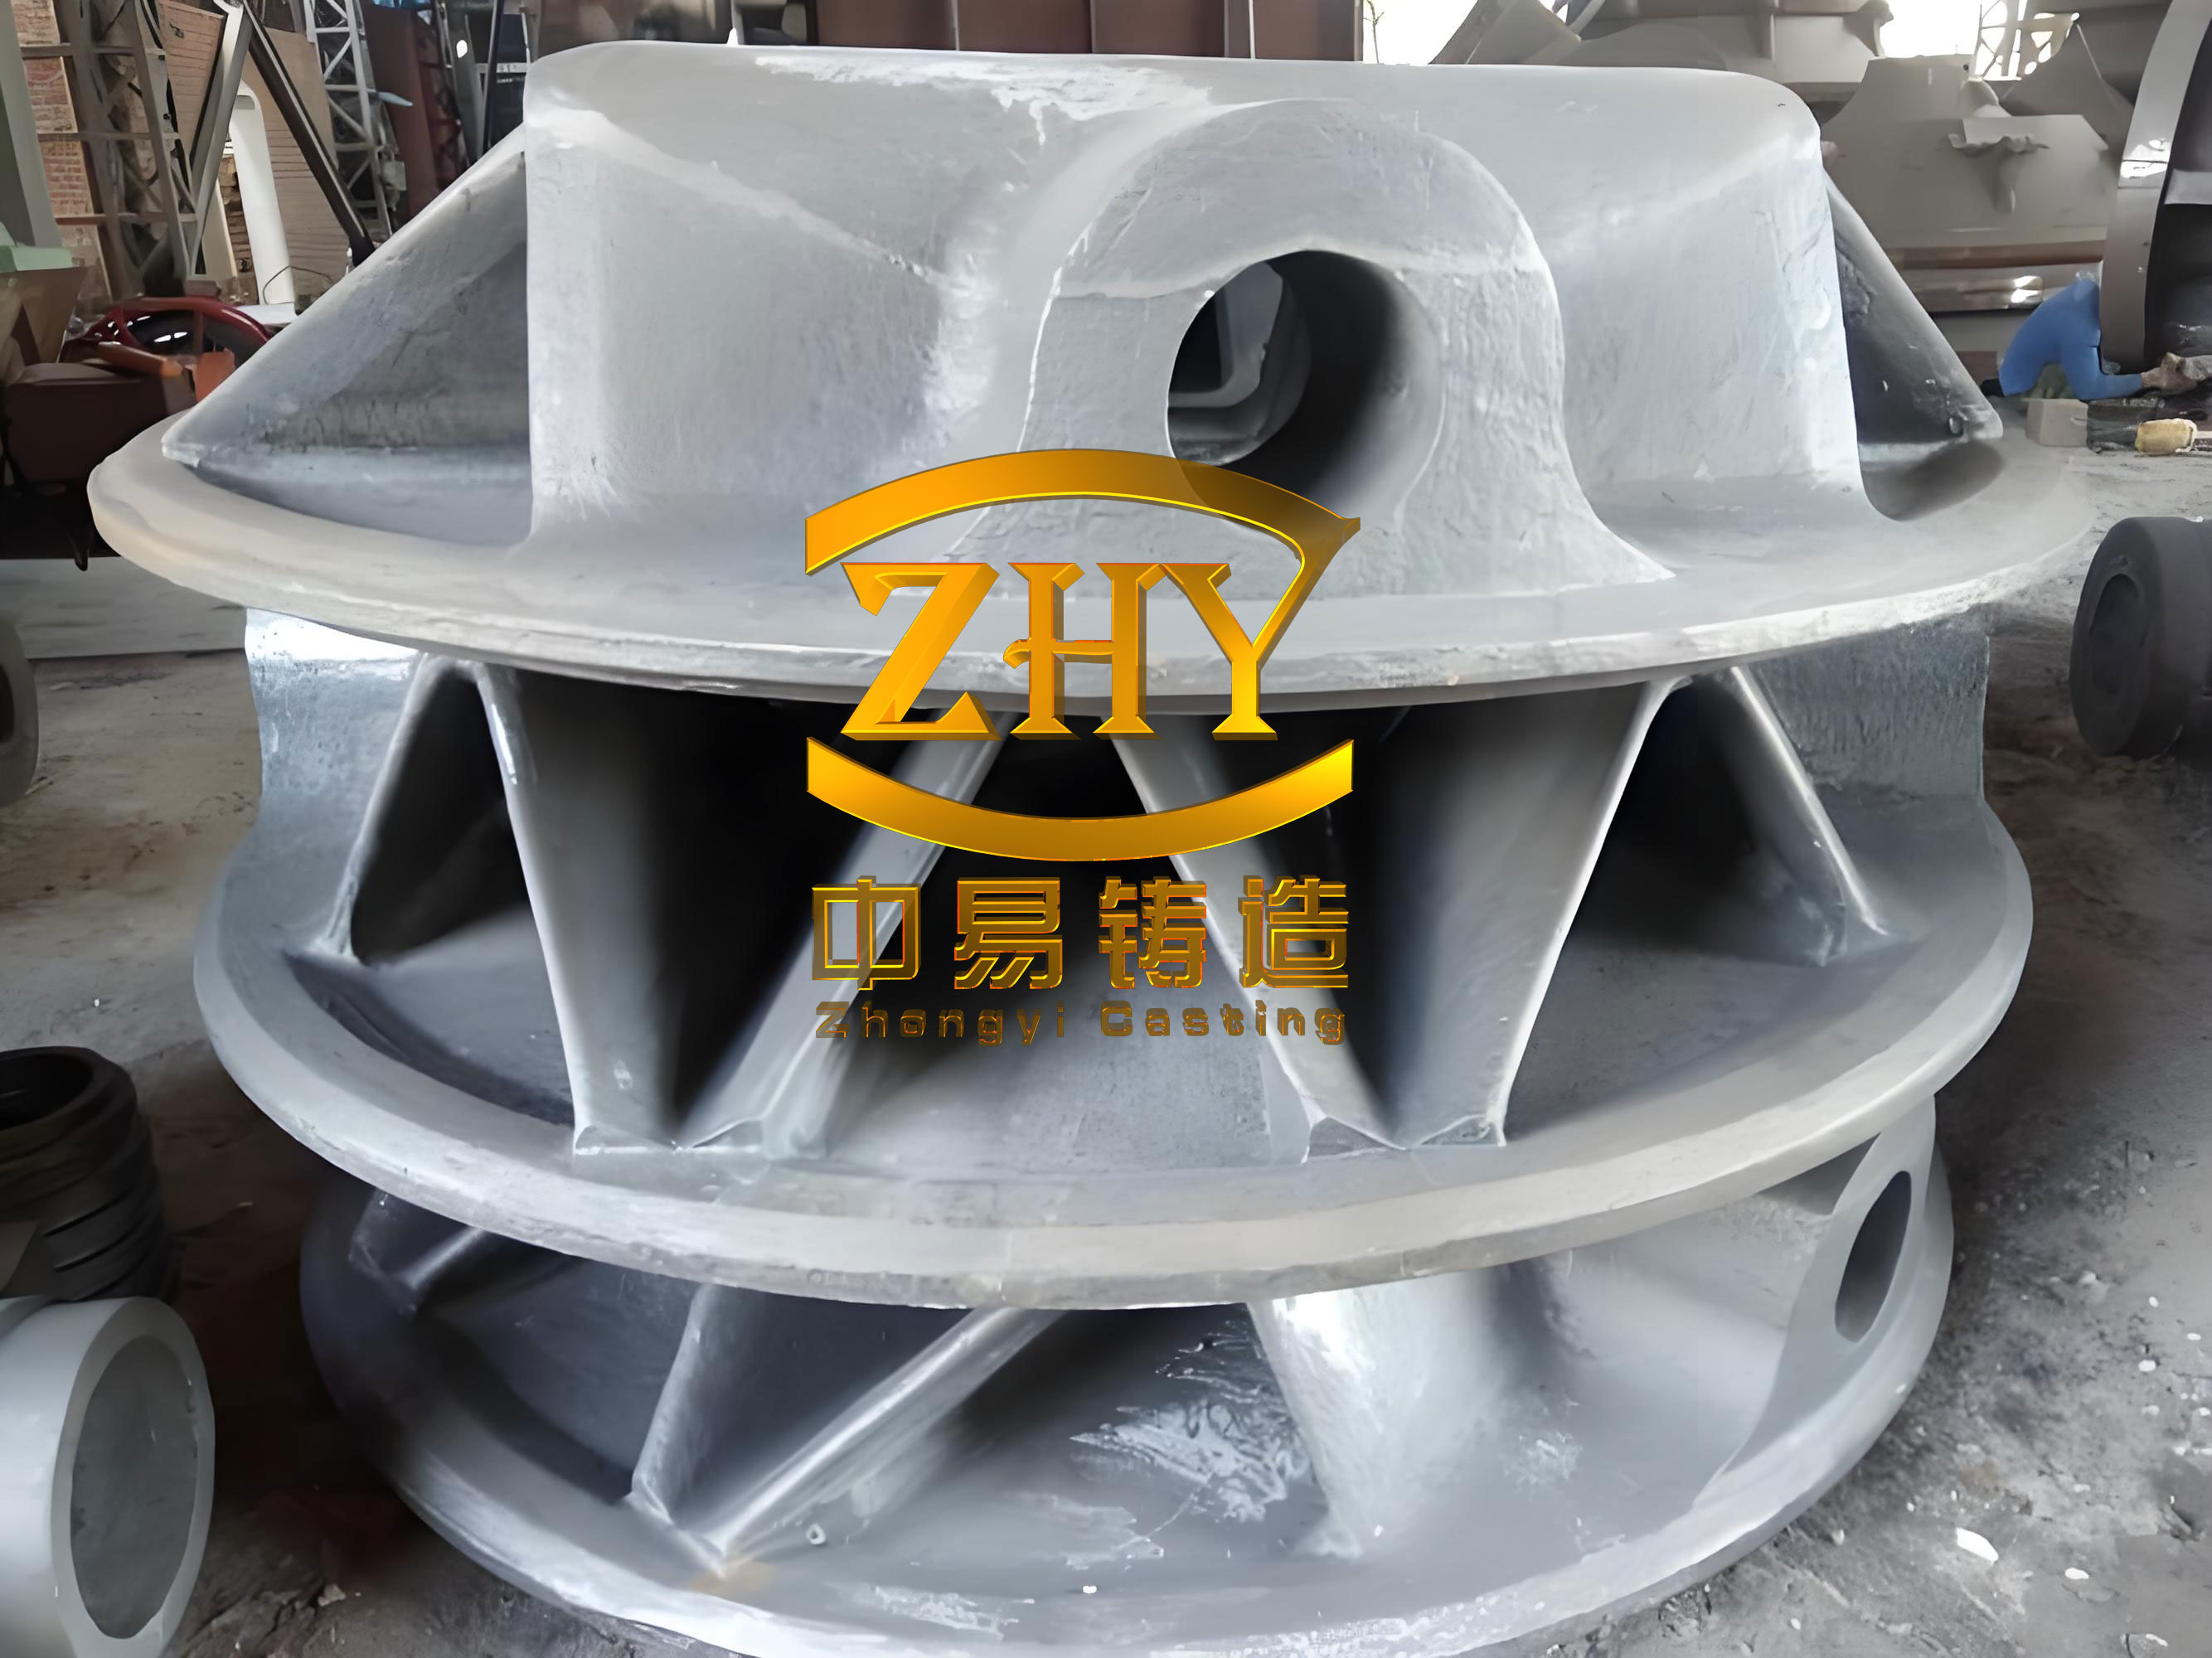
The shell component is a body with an outer contour and a central cylindrical bore. It has a relatively flat lower face, an upper annular face, and several local bosses or flanges that connect the outer wall to the central hub. The wall thickness is not uniform. Some parts of the lower face are comparatively thick, while the upper rim and side walls are thinner. The central bore creates a ring-like section around the core, which can act as a hot spot if the local cooling rate is not sufficient.
A representative ductile iron casting of this shell family is shown below.
To analyze the solidification behavior, we first consider the local thermal modulus \(M\), which is defined as the ratio of the local volume to the cooling surface area:
$$
M = \frac{V}{A_{\mathrm{cool}}}
$$
The solidification time of a simple casting or section is proportional to the square of the modulus according to Chvorinov’s rule:
$$
t_s = B M^2
$$
where \(B\) is a constant that depends on the mold material, the pouring temperature, and the thermophysical properties of the metal. The modulus concept is useful for a ductile iron casting because it allows us to identify the regions that solidify last and therefore require feeding from a riser. If the modulus of a local section is larger than that of the surrounding sections, that section will behave as a thermal hot spot.
For this shell-shaped ductile iron casting, the most critical regions are the lower thick face, the transition between the outer wall and the central hub, and the zone near the central bore. The upper rim is less critical because it can be connected to a riser more easily. The challenge is to create a thermal gradient that drives the last liquid toward the riser rather than allowing isolated liquid islands to form.
4. Design of the Two Casting Processes
We evaluated two different process plans for the same ductile iron casting. Both plans were designed for resin sand molding. Both plans used chills in the lower part of the casting and around the central cylindrical bore. The chills were identical in size, position, and shape. The main difference between the two plans was the riser system and the way in which the liquid metal entered the casting cavity.
4.1 Plan A: Blind riser with ingates
In the first plan, the casting was fed by two blind risers. The risers were connected to the casting through short ingates. The width of the riser neck was approximately 10 mm. The blind risers were placed directly above the largest hot spot of the ductile iron casting. This is a common arrangement because it seems to place the molten metal reserve exactly where it is needed. However, the ingate location introduces an important side effect. Because the liquid metal flows through the ingate and into the mold cavity, the ingate area receives a large amount of heat during filling. This creates a flow hot spot, which can enlarge the original geometric hot spot at the same location.
4.2 Plan B: Open conformal pressing-edge riser
In the second plan, we simplified the gating system to a single sprue and a single riser. The riser was designed as an open riser with a conformal pressing-edge connection along the upper circular face of the casting. The pressing-edge thickness was set to 8 mm. The term pressing-edge means that the riser is connected to the casting by a narrow horizontal slot or lip. In this design, the riser follows the outer contour of the shell so that the feeding distance is short and the feeding contact is continuous. This arrangement was intended to avoid the flow hot-spot problem associated with the ingate under the riser.
Table 3 summarizes the main features of the two process plans.
| Feature | Plan A | Plan B |
|---|---|---|
| Riser type | Blind riser with ingate | Open conformal pressing-edge riser |
| Number of risers | Two | One |
| Feeding connection | 10 mm wide riser neck | 8 mm thick pressing edge |
| Riser position | Directly over the largest hot spot | Along the upper circular contour of the casting |
| Chill placement | Lower face and central bore | Lower face and central bore |
| Expected advantage | Large feeding reserve close to the hot spot | No flow hot spot, continuous feeding path |
| Expected risk | Flow hot spot may enlarge the local thermal modulus | Thin pressing edge may freeze too early if not optimized |
5. Finite Element Model and Simulation Setup
We created three-dimensional finite element models for both process plans. The model included the casting, the riser system, the gating system, the chills, and the resin sand mold. The mesh was refined in the regions of the riser connection and around the hot spots because those regions determine the feeding behavior of the ductile iron casting.
The transient thermal field was solved using the Fourier heat conduction equation with a latent heat source term:
$$
\rho c_p \frac{\partial T}{\partial t}
=
\nabla \cdot \left( k \nabla T \right)
+
\rho L \frac{\partial f_s}{\partial t}
$$
where \(T\) is temperature, \(t\) is time, \(\rho\) is density, \(c_p\) is specific heat, \(k\) is thermal conductivity, \(L\) is latent heat of solidification, and \(f_s\) is the solid fraction. The solid fraction was described with a simple lever rule or linear model between liquidus and solidus temperatures:
$$
f_s(T)
=
\begin{cases}
0, & T \ge T_L \\
\dfrac{T_L – T}{T_L – T_S}, & T_S < T < T_L \\
1, & T \le T_S
\end{cases}
$$
The residual liquid fraction is then defined as:
$$
f_L = 1 – f_s
$$
In the post-processing stage, we also calculated the Niyama criterion to assess the local micro-porosity risk. The Niyama criterion is based on the local temperature gradient \(G\) and the local cooling rate \(\dot T\):
$$
N_y = \frac{G}{\sqrt{\dot T}}
$$
A low value of \(N_y\) indicates a high likelihood of dispersed shrinkage porosity. This criterion is often used for steel and is also helpful for ductile iron casting when combined with the residual liquid distribution.
We also used Darcy’s law to describe the movement of liquid through the mushy zone:
$$
u = -\frac{K}{\mu} \nabla P
$$
where \(u\) is the interdendritic flow velocity, \(K\) is the permeability of the mushy zone, \(\mu\) is the dynamic viscosity, and \(P\) is the pressure. If the pressure drop becomes too large, the liquid cannot feed the deepest parts of the mushy zone and a shrinkage pore is formed.
The main simulation parameters used for the ductile iron casting model are given in Table 4.
| Parameter | Value or description |
|---|---|
| Casting material | QT500-7 ductile iron |
| Mold material | Resin sand |
| Chill material | Cast iron chill |
| Pouring temperature | 1350 °C |
| Initial mold temperature | 20 °C |
| Liquidus temperature | 1180 °C |
| Solidus temperature | 1090 °C |
| Latent heat | 210 kJ/kg |
| Heat transfer coefficient, casting/mold | 400 W/(m²·K) |
| Heat transfer coefficient, casting/chill | 1000 W/(m²·K) |
For a robust comparison, we used the same mesh density, the same material database, and the same numerical convergence criteria for both plans. We focused on the solidification after complete filling. The filling stage strongly influences the initial temperature distribution in the mold and in the metal. Therefore, the ingate geometry and the pouring direction were represented in the model so that the flow hot-spot effect could be reproduced.
6. Simulation Results and Discussion
6.1 Plan A simulation results
The simulation of Plan A showed that the solidification sequence of the ductile iron casting begins in the thin outer walls and moves toward the thicker central sections. At an intermediate stage, the remaining liquid is relatively well connected. However, in the late stage of solidification, the calculation revealed two residual liquid islands. These islands are regions where liquid metal is surrounded by solidified material. They cannot receive additional liquid from the risers because the feeding channel has already been blocked.
This result is important for our understanding of ductile iron casting design. The blind risers in Plan A are located directly above the largest hot spot, but the liquid metal enters the cavity through ingates. During filling, the hot stream continually passes through the riser neck and the ingate. This stream heats the mold and the already thick section around the riser. As a result, the effective local thermal modulus at the hot spot becomes larger than the geometric modulus calculated from the casting geometry alone. The blind riser must therefore feed not only the original hot spot but also an enlarged hot spot. The available feeding capacity is no longer sufficient, and residual liquid islands form near the end of solidification.
The Niyama values in the regions corresponding to the residual liquid islands were low. This indicates a high probability of micro-shrinkage in the ductile iron casting. The exact shape and position of the defective region would be affected by the local solidification time and by the graphite expansion behavior, but in our model the primary cause is clearly the loss of an open feeding path.
We also noticed that the bottom face and the central bore were not sufficiently cooled without an additional thermal effect. The chills helped, but the thermal gradient was not strong enough to pull the last liquid through the entire section. The blind risers provided an early feeding benefit, but they were not capable of feeding the isolated liquid islands at the end of the solidification process.
6.2 Plan B simulation results
The simulation of Plan B showed a more favorable solidification pattern. The open conformal pressing-edge riser was the last region to solidify. The liquid metal was able to flow continuously through the 8 mm pressing edge as the shell solidified. No isolated residual liquid islands appeared in the late stages of solidification.
The pressing-edge design has several advantages for this ductile iron casting. First, the liquid metal enters the casting through a narrow slot along the upper circular face. Because the slot is narrow, it freezes relatively early, but not before the feeding path to the upper sections is no longer needed. More importantly, the riser is open to atmospheric pressure, so the pressure above the liquid metal is able to help push the metal into the mushy zone. This is useful for ductile iron casting, where graphite expansion can create a positive pressure if the feeding channel remains open.
The chills also played an important role in Plan B. The lower face and the central bore sections contain locally thicker metal. Without the chills, these regions would solidify too late and would require a much larger riser. With the chills, the solidification front moved from the bottom and from the central bore toward the upper riser. This directional solidification pattern is exactly what a good ductile iron casting process requires.
In addition, the cross-section near the lower face has a rectangular shape with a relatively high length-to-width ratio. A large flat section of this type is difficult to feed from a single riser if the local cooling is not enhanced. The chill reduces the local solidification time and shifts the hot spot to a location that can be fed more easily. We therefore conclude that the combination of the open pressing-edge riser and the identical chill arrangement is better than the blind riser arrangement in Plan A.
6.3 Comparison of the two simulation results
Table 5 summarizes the main observations from the simulation of the two ductile iron casting process variants.
| Observation | Plan A | Plan B |
|---|---|---|
| Residual liquid distribution | Two isolated liquid islands in late solidification | No isolated liquid islands |
| Feeding path | Blocked before complete solidification | Continuous until the end of solidification |
| Flow hot spot | Yes, created by ingates under the riser | Avoided by the open pressing-edge riser |
| Effect of chill | Present but insufficient to eliminate isolated liquid | Effective in establishing a directional thermal gradient |
| Niyama criterion | Low values in isolated regions | Acceptable values at the same locations |
| Expected shrinkage risk | High | Low |
| Recommended for production | No | Yes |
Based on these results, we selected Plan B as the final process for the production of the shell-shaped ductile iron casting. The simulation clearly showed that simply placing a large blind riser over the hot spot is not always the best solution. The interaction between the gating system and the riser must be considered. In Plan B, the open conformal pressing-edge riser avoided the flow hot spot and created a reliable feeding channel.
7. Production Verification
The selected Plan B was used to produce the actual ductile iron casting. The castings were made by resin sand manual molding. The ductile iron melt was spheroidized using the normal treatment procedure for this grade. The pouring temperature was maintained at 1350 °C. After solidification and cooling, the castings were shaken out, cleaned, heat treated, and finally machined.
The machined castings were inspected visually and dimensionally. No obvious shrinkage porosity, surface shrinkage, or open defects were found. The critical machined surfaces, especially the central bore and the lower face, were sound. The castings met the drawing requirements and passed the acceptance testing. This result agrees with the numerical prediction. The absence of defects in the production run confirms that the simulation model captured the important solidification behavior of the ductile iron casting.
We also observed that the 8 mm pressing-edge thickness was a suitable compromise. It was thin enough to be broken off during knockout or easily cut off during finishing, but thick enough to keep the feeding channel alive during the critical solidification stage. The conformal shape of the riser allowed a uniform feeding contact along the upper contour, which prevented local premature freezing at the connection point.
8. Recommended Design Rules for Similar Ductile Iron Casting
From this project, we can propose several practical rules for the design of a ductile iron casting with shell-like geometry. First, the riser should be positioned near the thermal hot spot but not necessarily directly in contact with the maximum geometric section if the gating system creates a flow hot spot. The word near is important. The riser must be close enough to feed the hot spot, but must not enlarge it by adding extra heat through the ingate.
Second, when a pressing-edge riser is used, the pressing-edge thickness should be selected carefully. If it is too thin, it will freeze before the hot spot has finished solidifying. If it is too thick, it becomes difficult to remove and may create a new hot spot at the junction. For this steel? No, for this ductile iron casting, 8 mm worked well because the upper section is relatively thin. The exact value should be confirmed by simulation for other wall thicknesses.
Third, chills are necessary for shell-shaped ductile iron casting when there are thick flat areas or large bosses. A chill reduces the local modulus and increases the local temperature gradient. This improves the Niyama criterion and helps to avoid micro-shrinkage. The chill should be placed on the surfaces that solidify early in the casting sequence, so that the last liquid is pushed toward the riser.
Fourth, the pouring temperature must not be too high. A high pouring temperature increases the thermal load on the mold and increases the cooling time of the riser neck. In our production, 1350 °C was suitable. The simulation was run with this value, which made the predicted and actual results consistent.
9. Conclusion
In this article, we analyzed two casting process designs for a shell-shaped QT500-7 ductile iron casting. The work was based on finite element simulation of the solidification behavior, followed by production verification. The following conclusions can be drawn:
1. For a ductile iron casting produced with a blind riser and ingate system, the ingate should be placed near the thermal hot spot but not directly inside it. If the ingate is located under the riser, the flowing liquid metal creates a flow hot spot that enlarges the original hot spot. As a result, the riser cannot feed the isolated residual liquid, and shrinkage porosity is likely to form.
2. The open conformal pressing-edge riser design proved to be superior for this shell component. The 8 mm pressing edge provided a continuous feeding path and avoided the flow hot-spot problem. The open riser also allowed atmospheric pressure to assist feeding. The simulation showed no isolated liquid islands in the late stage of solidification.
3. The use of chills on the lower face and around the central bore was an important part of the successful process. The chills increased the thermal gradient and directed the solidification sequence from the bottom and the central bore toward the upper riser. This is a critical design principle for any shell-like ductile iron casting with thick sections that are difficult to feed.
4. The production trial confirmed the simulation result. The ductile iron castings produced with Plan B were sound after machining and satisfied the drawing requirements. This demonstrates that numerical simulation is a valuable tool for the design and optimization of ductile iron casting processes.
In conclusion, a successful ductile iron casting process is not determined by the size of the riser alone. The interaction between the riser, the gating system, the chill arrangement, and the casting geometry is equally important. The combination of thermal modulus analysis, solidification simulation, and practical process knowledge is the most reliable approach for producing high-quality ductile iron casting components.