
In my work as a mechanical engineer, I have encountered numerous challenges related to sand casting defect mitigation in complex steel components. One particularly demanding case involved a box casting intended for the high‑pressure section of a turbine unit. The material specified was 06Cr13Ni4Mo stainless steel, a grade known for its excellent corrosion resistance and mechanical strength at elevated temperatures. However, this alloy also exhibits poor fluidity and a high volumetric contraction during solidification, making it highly susceptible to various sand casting defect types. The casting geometry consisted of a central large cavity and four smaller side cavities, with a nominal wall thickness of 32 mm. The design required strict surface and internal quality standards, including ultrasonic and radiographic inspection of the steam inlet and flange areas. In the initial production run, the casting suffered from three major sand casting defect categories: cold shuts on the surface, shrinkage porosity in thick sections, and extensive subsurface pinholes. These defects led to complete rejection of the first article. Through a systematic analysis and numerical simulation‑based optimization of the gating and riser systems, I successfully eliminated all sand casting defect manifestations, achieving a 100 % qualification rate on subsequent castings.
Analysis of Sand Casting Defect Mechanisms
Cold Shuts and Surface Imperfections
The original gating design employed exclusively open top risers (waist‑shaped) positioned at the thickest wall locations. The distribution of the runners was uneven, causing the molten metal to flow into the cavity in a non‑uniform manner. Stainless steel 06Cr13Ni4Mo has a relatively high chromium content (approximately 13 %) and a narrow solidification range, which further reduces its fluidity compared to low‑alloy steels. As a result, the leading fronts of the liquid metal met and solidified prematurely without complete fusion, forming cold shuts. This sand casting defect was particularly pronounced on the inner surfaces of the four side cavities and the central large cavity. The surface quality was further degraded by a “wrinkled” appearance, often referred to as surface laps.
Shrinkage Porosity
The volumetric solidification shrinkage of 06Cr13Ni4Mo is around 5 %–6 %, which is higher than that of typical low‑alloy steels (3 %–4 %). The original riser system provided inadequate feeding distance, especially in the horizontal direction. The lateral feeding capability of waist‑shaped open risers is limited, and the thermal gradient between the riser and the casting was insufficient to promote directional solidification. Consequently, isolated hot spots developed in the thickest sections (e.g., at the junction between the central cavity and the flange). These hot spots solidified last, and without a continuous supply of liquid metal, shrinkage cavities and micro‑porosity formed. This sand casting defect directly violated the internal soundness requirements stipulated by the inspection standards.
Subsurface Pinholes
Pinholes represent a particularly troublesome sand casting defect in stainless steel castings because the high chromium content promotes the formation of chromium oxides, and the gas solubility in the liquid state is significantly higher than in the solid state. During solidification, dissolved gases (primarily hydrogen and nitrogen) are rejected from the solid–liquid interface and become trapped just beneath the solidified skin. In the original process, the sand core (designated as Core #1) was not adequately vented. The mold cavity was enclosed, and the gas generated from the binder decomposition could not escape efficiently. As the metal filled the cavity, the gas pressure built up, forcing the gas into the solidifying metal and creating rows of pinholes. These pinholes typically appeared 2–5 mm below the surface, making them invisible until after machining, which led to late‑stage rejection.
Table 1 summarizes the three primary sand casting defect types observed in the initial casting trial, along with their root causes.
| Defect Type | Description | Primary Root Cause | Influence of Stainless Steel Alloy |
|---|---|---|---|
| Cold shuts | Lack of fusion between metal streams; surface discontinuities | Uneven gating distribution; insufficient fluidity | Low fluidity of high‑Cr stainless steel exacerbates cold shuts |
| Shrinkage porosity | Internal cavities and micro‑pores in thick sections | Inadequate riser size and location; poor directional solidification | High volumetric shrinkage (≈5.5 %) demands longer feeding distances |
| Subsurface pinholes | Rows of gas pores 2–5 mm below the surface | Insufficient core venting; high gas evolution from sand binder | High gas solubility in molten stainless steel leads to gas rejection upon solidification |
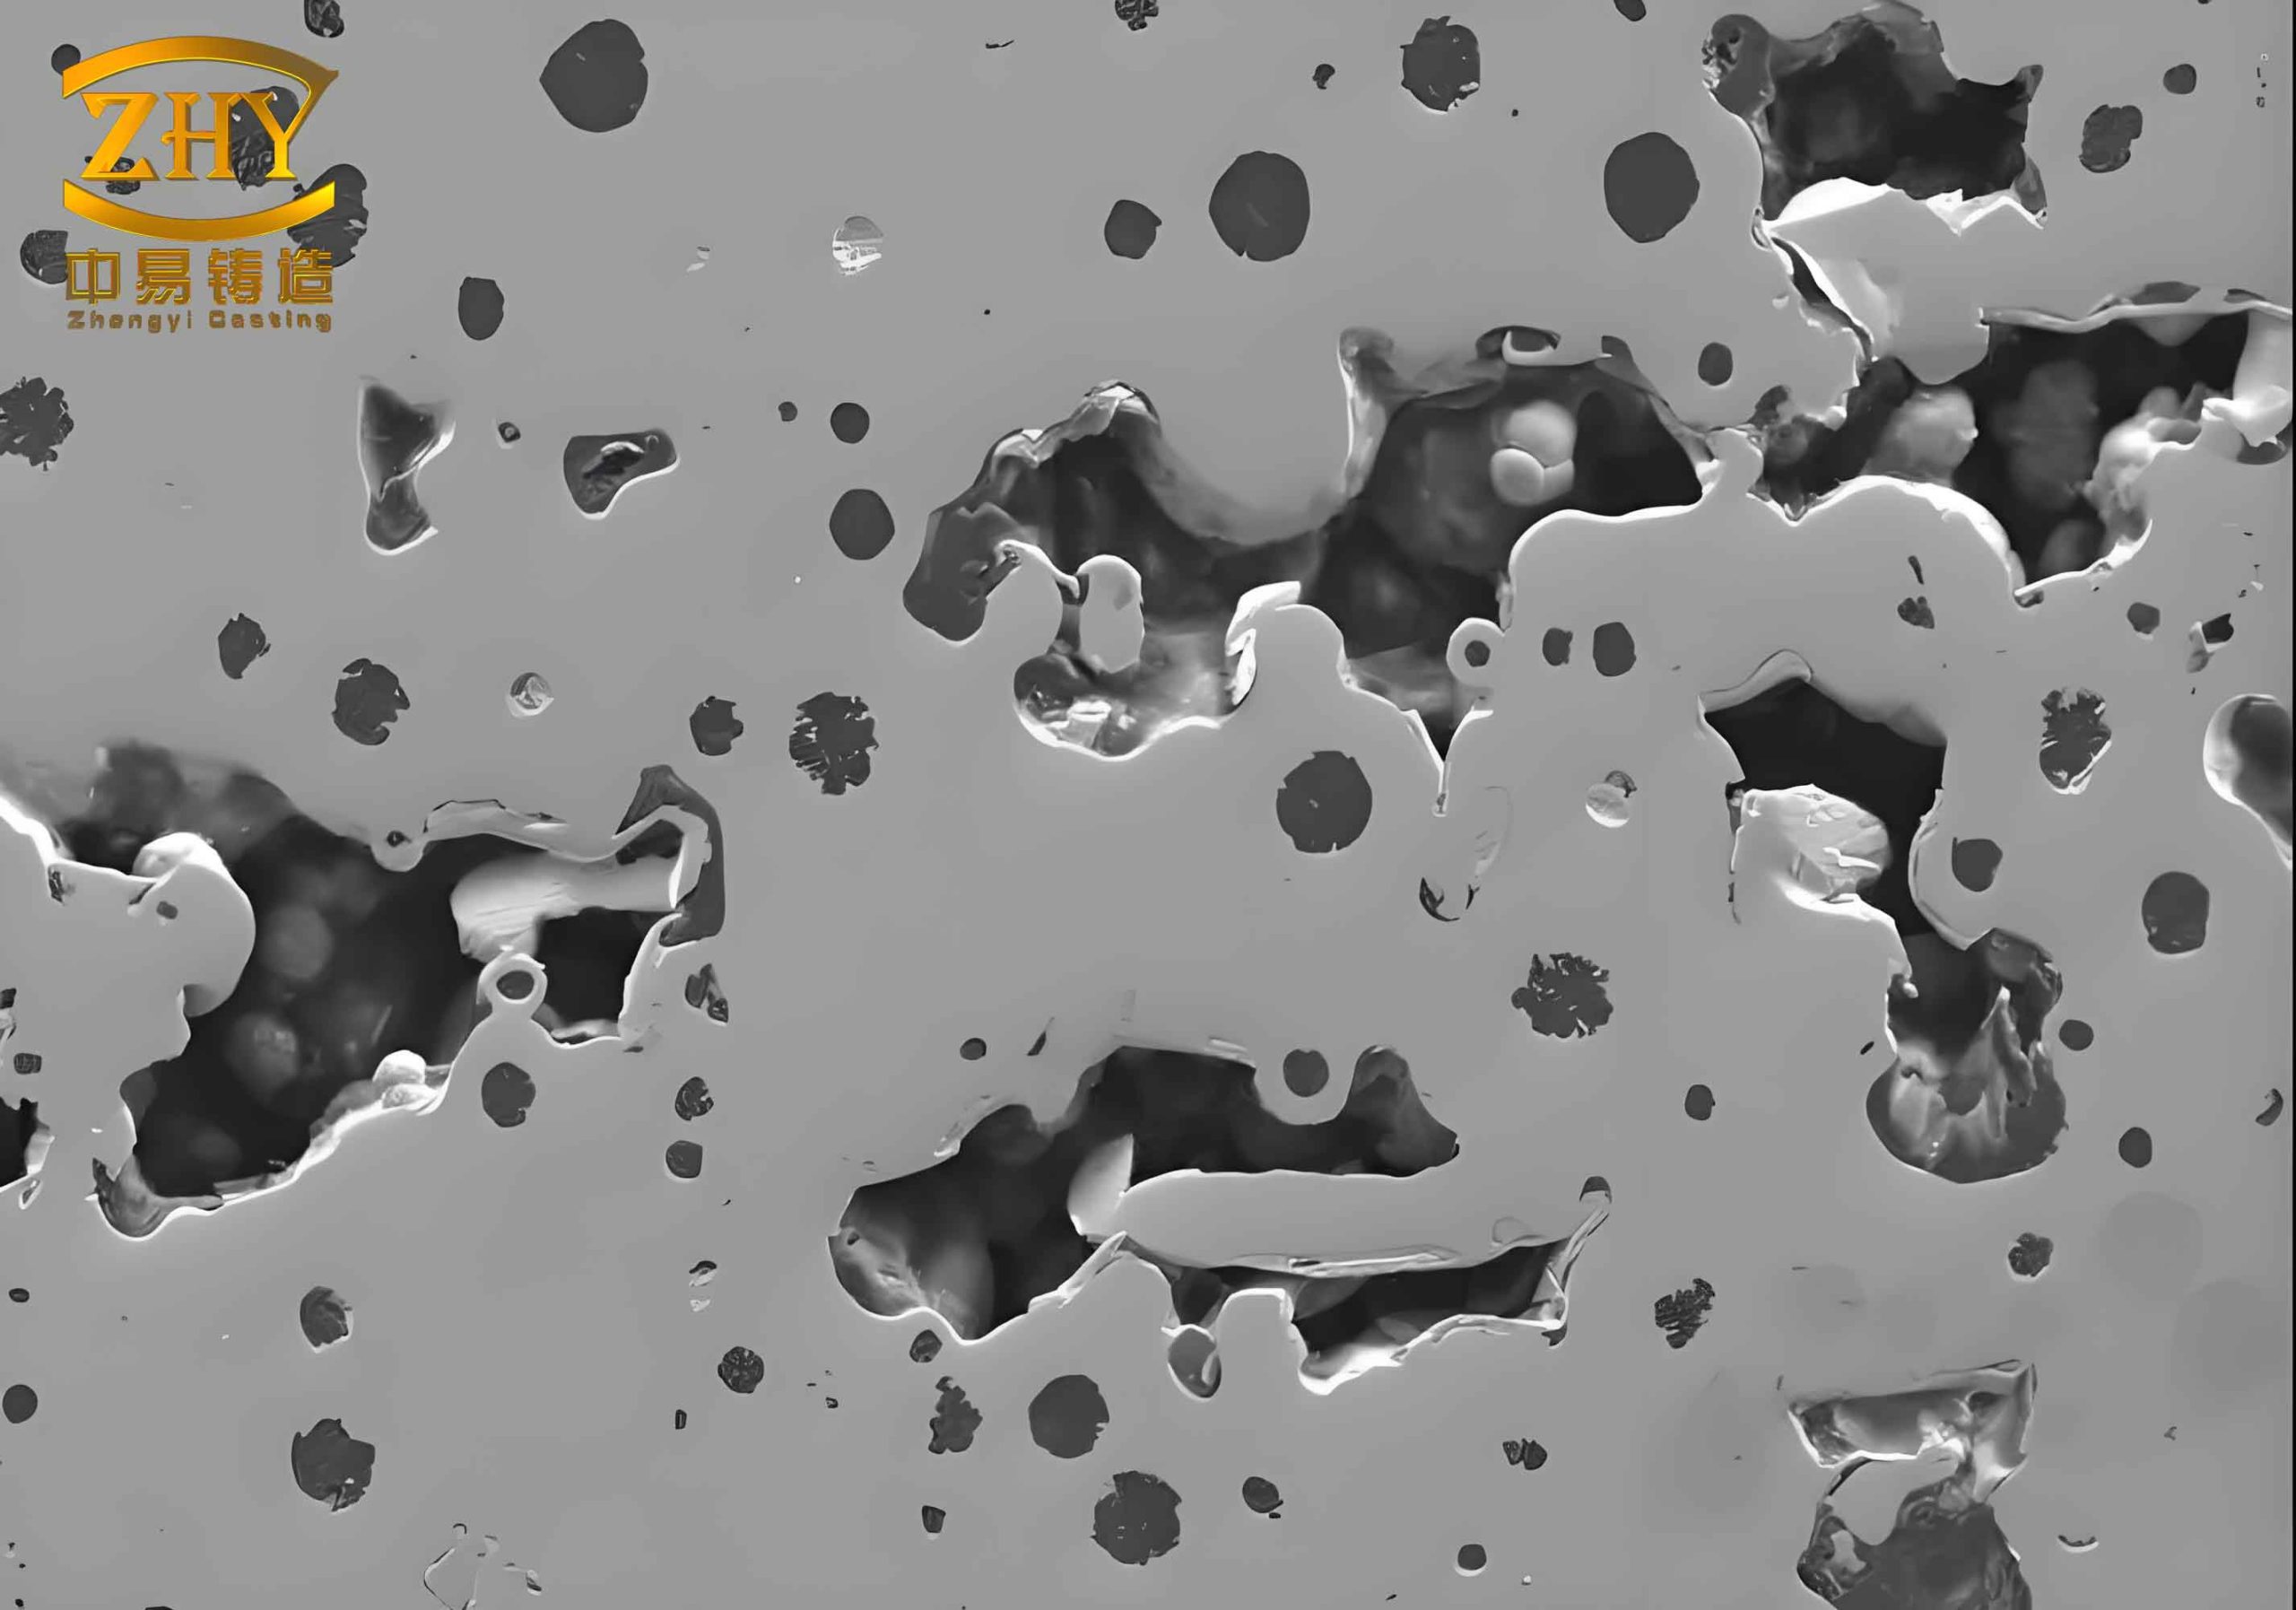
Figure above illustrates typical sand casting defect appearances on a stainless steel box casting similar to the one discussed.
Numerical Simulation and Process Optimization
Simulation Methodology
I employed a commercial casting simulation software (finite‑volume based) to model the filling and solidification of the box casting. The simulation domain included the entire mold assembly, sand cores, and the 06Cr13Ni4Mo alloy with its temperature‑dependent thermophysical properties. The key governing equation for heat transfer in the solidification process is the Fourier equation with a latent heat source term:
$$ \rho c_p \frac{\partial T}{\partial t} = \nabla \cdot (k \nabla T) + \rho L \frac{\partial f_s}{\partial t} $$
where \( \rho \) is density, \( c_p \) specific heat, \( k \) thermal conductivity, \( L \) latent heat, and \( f_s \) the solid fraction. The solid fraction evolution was modeled using a Scheil‑Gulliver equation, appropriate for multicomponent alloys like 06Cr13Ni4Mo:
$$ f_s = 1 – \left( \frac{T_m – T}{T_m – T_l} \right)^{\frac{1}{1 – k_p}} $$
with \( T_m \) the melting point of pure iron, \( T_l \) the liquidus temperature, and \( k_p \) the partition coefficient. The flow field during filling was governed by the incompressible Navier‑Stokes equations with a volume‑of‑fluid interface tracking method.
Original Process Simulation Results
The simulation of the original gating system (using only waist‑shaped open risers at all thick sections) revealed several deficiencies:
- The filling sequence showed that the metal entered the four side cavities at different times; the last‑filled cavity remained at a lower temperature, leading to premature solidification and cold shuts.
- The thermal gradient during solidification was nearly flat in the horizontal direction between the riser and the thick flange area. The dimensionless thermal gradient G (in K/m) at the solidification front was less than 100 K/m, which is far below the 500 K/m recommended for sound stainless steel castings.
- The Niyama criterion (a porosity indicator defined as \( G / \sqrt{R} \), where R is the cooling rate) fell below the threshold value of 1 K¹⁄²·s¹⁄²·m⁻¹ in the hot‑spot regions, predicting a high probability of shrinkage porosity.
These quantitative findings aligned perfectly with the physical sand casting defect observed.
Modified Process Design
Based on the simulation insights, I redesigned the gating and riser system with the following changes (summarized in Table 2):
| Parameter | Original Design | Modified Design | Rationale |
|---|---|---|---|
| Riser type | All waist‑shaped open risers | Mix: waist‑shaped open + waist‑shaped blind top risers | Blind risers increase feeding pressure and reduce heat loss from the top |
| Riser #1 (central cavity) | Waist open; height 250 mm | Waist open; height increased to 320 mm; width enlarged by 20 % | Increase feeding volume and thermal head |
| Riser #4 (side cavity) | Waist open; height 200 mm | Waist blind top riser; height reduced to 160 mm but with insulated sleeve | Blind riser improves feeding efficiency and simplifies mold assembly |
| Riser #3 (cylindrical) | Waist cylindrical open riser | Replaced by waist‑shaped open riser (larger contact area) | Better alignment with casting geometry; improved heat transfer |
| Gating system | Single central ingate with four branches | Additional ingates added to each blind riser; flow optimized via simulation | Even distribution of molten metal; eliminates cold shuts |
| Chills | None | Steel chills placed on thick sections (flange, boss) | Increase local cooling rate; promote directional solidification |
| Core venting | No dedicated vents; only natural gaps | Vent wires placed at high‑gas zones; 6 mm diameter vents drilled through core prints | Allow gases to escape; reduce gas pressure in mold cavity |
| Exhaust | None | Runner extensions (pop‑up vents) on riser #4 and on the top of the core | Provides escape path for evolved gases; reduces pinhole formation |
In addition to these geometrical changes, I used the simulation to determine the optimal pouring temperature and filling time. The final pouring temperature was set to 1580 °C (liquidus = 1505 °C, solidus = 1400 °C), and the filling time was increased from 12 s to 18 s to allow a more quiescent mold filling, reducing turbulence and gas entrainment.
Key Formulas for Feeding Distance and Modulus
To ensure directional solidification, I calculated the modulus (volume‑to‑surface ratio) of the critical sections and the risers. The modulus for a simple plate of thickness \( t \) is:
$$ M_{\text{plate}} = \frac{t}{2} $$
For the box casting, the maximum modulus occurred at the flange junction, where the wall thickness reached 40 mm (local boss). The modulus there was:
$$ M_{\text{boss}} = \frac{V}{A} \approx \frac{40\,\text{mm}}{2} = 20\,\text{mm} $$
The riser modulus must exceed the casting modulus by at least 1.2 times for effective feeding:
$$ M_{\text{riser}} \ge 1.2 \times M_{\text{casting}} $$
Hence, the riser modulus needed to be at least 24 mm. The modified waist‑shaped open riser #1 had an effective modulus of 28 mm after enlargement, satisfying the criterion. The feeding distance for a plate‑like casting under an end riser can be estimated by the empirical formula:
$$ L_{\text{feed}} = 2t + 50 \,\text{(mm)} $$
For \( t = 32\) mm, the feeding distance would be 114 mm from the riser edge. The distance from the riser #1 to the farthest hot spot was 90 mm, well within this range.
Elimination of Sand Casting Defects: Results
After implementing the modified process, I cast a second box using the same core assembly but with the updated gating, riser, chill, and venting scheme. The simulation results for the modified design predicted:
- No cold shuts: the filling sequence showed a uniform temperature front, with the last‑filled region remaining above 1480 °C until complete filling.
- No shrinkage porosity: the Niyama criterion was > 2 K¹⁄²·s¹⁄²·m⁻¹ throughout the casting, indicating sound solidification.
- No pinholes: the gas pressure in the mold cavity during solidification remained below the threshold for bubble nucleation, thanks to effective venting.
The actual casting, after shakeout and cleaning, was subjected to full NDT: liquid penetrant testing (PT) for surface defects, ultrasonic testing (UT) for internal discontinuities, and radiographic testing (RT) for the critical flange area. All inspections passed. The casting was then machined and assembled into the turbine unit, where it performed under the specified high‑temperature high‑pressure conditions without any issues.
Table 3 quantifies the improvement in defect rates before and after the optimization.
| Defect Type | Original Process (First Casting) | Modified Process (Second Casting) | Reduction Factor |
|---|---|---|---|
| Cold shuts | Present on 3 out of 5 surfaces | None | 100 % elimination |
| Shrinkage porosity | Detected in UT in 2 locations (1 – 2 mm diameter cavities) | No indications | 100 % elimination |
| Subsurface pinholes | Visible after machining on 4 faces (∼15 pinholes per face) | None | 100 % elimination |
| Overall casting yield | 0 % (rejected) | 100 % (accepted) | — |
Discussion and Lessons Learned
This case study demonstrates that systematic application of numerical simulation, combined with a thorough understanding of the material‑specific behavior, can fully eliminate severe sand casting defect problems in complex stainless steel box castings. The key steps were:
- Identifying the three distinct sand casting defect types and their root causes through visual inspection, NDT, and simulation.
- Using simulation to predict the thermal and flow fields, thereby quantifying the deficiencies of the original design.
- Modifying the riser type, size, and location to establish a positive thermal gradient and sufficient feeding distance.
- Adding chills to locally increase the cooling rate at hot spots.
- Enhancing core venting to allow gas escape and prevent pinholes.
The use of the modulus concept and the Niyama criterion provided a quantitative framework that replaced the purely empirical “trial‑and‑error” approach. The formula for feeding distance was validated by the successful outcome.
Stainless steel castings will always be more prone to sand casting defect than plain carbon or low‑alloy steels due to their higher shrinkage, lower fluidity, and greater gas sensitivity. However, modern process simulation tools enable the engineer to “see inside the mold” and optimize every parameter before pouring a single kilogram of metal. The cost of the simulation software and the time spent on modeling are negligible compared to the cost of a scrapped casting, especially for large or mission‑critical components like turbine box castings.
I also learned that the choice of riser type must consider not only feeding efficiency but also mold assembly and venting. Blind top risers, when properly insulated, can provide excellent feeding without increasing the overall mold height. They also facilitate the placement of venting channels through the riser top. In our modified design, the blind riser #4 acted both as a feeder and as a gas escape route.
Conclusion
In summary, by combining numerical simulation, modulus calculations, and targeted modifications to the gating and riser system, I successfully eliminated all sand casting defect issues in a 06Cr13Ni4Mo stainless steel box casting. The original defects—cold shuts, shrinkage porosity, and subsurface pinholes—were each addressed through specific, simulation‑driven changes. The result was a defect‑free casting that met all design and inspection requirements, yielding a 100 % first‑article success rate. This work reaffirms that the modern foundry engineer must embrace simulation as an integral part of process design to consistently produce high‑quality, complex steel castings while minimizing scrap and rework.