
In my extensive experience within the precision casting industry, sand hole defects stand out as one of the most prevalent and challenging issues encountered in investment casting production. These defects not only compromise the visual integrity of a component but, more critically, can severely undermine its mechanical properties and service life. When a sand hole is located deep within the internal structure of an investment casting, it may remain undetected through standard visual inspection, posing a significant risk of catastrophic failure in critical applications. Therefore, a thorough understanding of the genesis of these defects and the implementation of robust countermeasures are paramount for any foundry committed to quality and reliability. This article, drawn from years of practical observation and process refinement, will delve into the multifaceted nature of sand hole formation and present a systematic framework for its prevention.
The term “sand hole” specifically refers to cavities or voids on the surface or within the interior of an investment casting that are filled or caused by loose sand grains or refractory particles. These inclusions are fundamentally foreign to the intended metallic matrix. Their presence can be traced to two primary sources: external contamination introduced into the mold cavity, or internal degradation of the ceramic shell itself. The manifestation of a sand hole defect is not uniform; its impact is heavily dependent on location. Surface-breaking sand holes are readily identifiable after shell removal and cleaning. Sub-surface holes, situated close to the casting surface, are typically revealed during machining operations. The most insidious are the deeply embedded sand holes, which remain concealed within the casting body, acting as stress concentrators that drastically reduce the effective load-bearing cross-section and can initiate fatigue cracks.
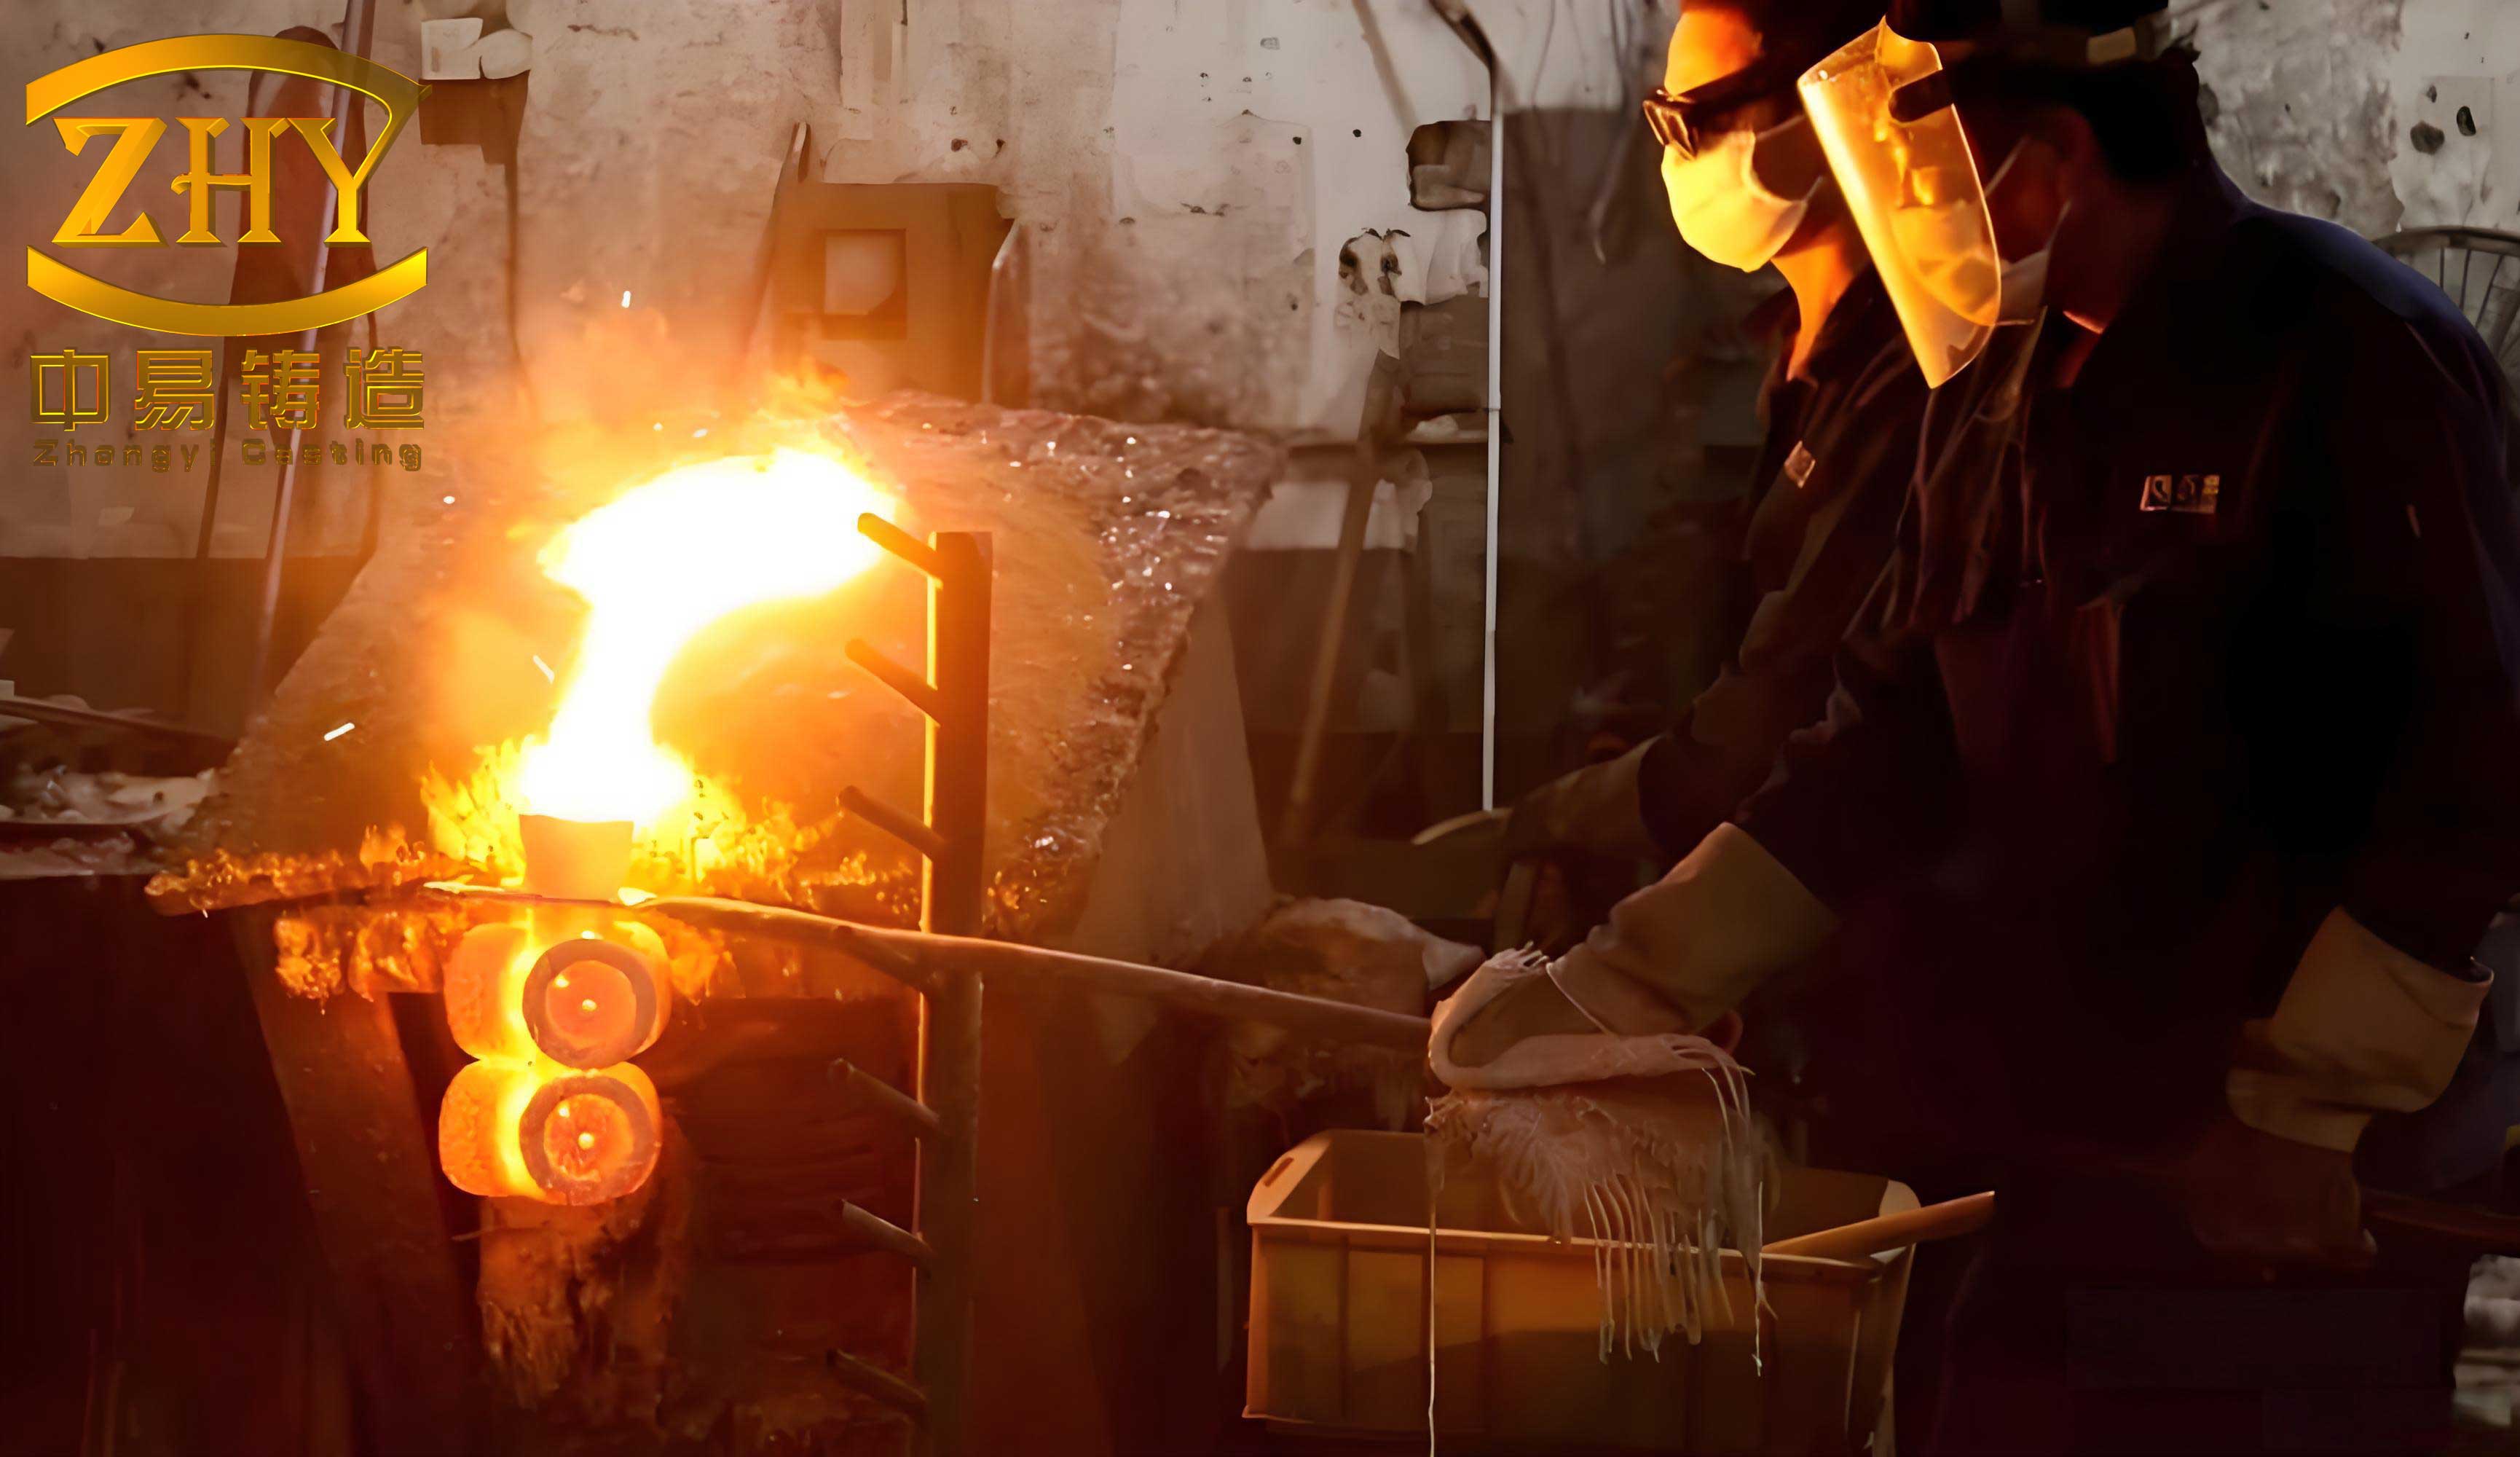
The process of investment casting, renowned for its ability to produce complex, near-net-shape components, involves creating a ceramic shell around a wax pattern. The integrity of this shell is the first and most critical line of defense against defects like sand holes. Any lapse in shell quality or handling directly increases the propensity for such failures. My analysis consistently points to two broad categories of root causes, which I will expand upon with detailed mechanisms and contributing factors.
Root Cause Analysis: External vs. Internal Origins
Identifying the origin of the refractory material found within a sand hole is the first diagnostic step. In practice, I often find that the nature of the inclusion provides a strong clue. If the inclusion consists primarily of loose, unbonded sand, the source is likely external contamination. Conversely, if the inclusion comprises fragments of the bonded ceramic shell facecoat or backup layers, the failure is internal, stemming from shell quality issues.
External Contamination Sources
Contamination originating from outside the mold cavity is often a result of procedural lapses in the investment casting workflow. Based on my observations, the primary vectors include:
- Pattern Assembly and Gating Systems: The wax pattern assembly, which includes the gating system, must be meticulously clean. Any residual sand or refractory dust on the central wax sprue (or core rods) can be transferred into the cavity during dewaxing.
- Dewaxing Process: The autoclave or flash fire dewaxing medium must be kept free of debris. Agitation or boiling of the medium can forcibly carry loose particles into the now-empty cavity through the gating channels.
- Shell Handling and Storage: Between dewaxing and pre-firing, the fragile ceramic shell is vulnerable. Improper handling, storage in dusty environments, or accidental impacts can dislodge sand from the rough exterior shell surface or the pour cup, allowing it to fall into the cavity.
- Pre-firing and Pre-pour Preparation: Failure to thoroughly inspect and clean the cavity—often using suction or compressed air—immediately prior to metal pouring is a common, yet easily avoided, error. Any foreign material present at this stage will be entrained by the molten metal.
The dynamics of metal flow during the investment casting pour then determine the final location of these particles. Heavy, non-wettable particles are often swept to the bottom of the cavity or to remote corners far from the ingate by the advancing metal front, where they become trapped upon solidification. Lighter particles may be caught in turbulent flow zones and encapsulated within the casting wall.
Internal Shell Degradation Sources
This category is technologically more complex and is the focus of most process improvement efforts in investment casting. The ceramic shell is a composite structure, and its failure can take several forms:
- Delamination and Spalling: A lack of cohesive strength between the successive layers of the shell, particularly between the fine facecoat and the coarser backup coats, can lead to separation. This may appear as bulging, peeling, or flaking of the inner surface. During pouring, the high-velocity metal stream can erode and dislodge these weakened sections.
- Shell Friability and Low Strength: An overall weak, crumbly, or “soft” shell is highly susceptible to erosion and mechanical failure. This is often a fundamental issue with the binder chemistry, drying/hardening processes, or material quality.
- Micro-cracks and Fins: Imperfections in the original wax pattern, such as micro-cracks or poor sealing at weld joints for pattern assembly, can translate into thin, fin-like projections of ceramic inside the cavity. These fragile protrusions are easily broken off by the molten metal.
- Gating System Design: A poorly designed gating system that creates excessive turbulence, direct impingement on shell walls, or allows for direct “drop” of material from the pour cup into the cavity can mechanically attack the shell interior.
The root causes of these internal shell failures are deeply embedded in the specifics of the shell-building process, whether it be the waterglass (silicate) process or the more advanced silica sol process. Let’s dissect these with technical rigor.
Fundamental Prevention Strategies: A Three-Pillar Approach
Preventing sand hole defects in investment casting requires a holistic strategy. I advocate for a three-pillar framework: 1) Rigorous exclusion of external contaminants, 2) Meticulous control and optimization of shell manufacturing, and 3) Intelligent design of the product and its feeding system.
Pillar 1: Contamination Control Protocols
This pillar focuses on procedural discipline. Key actions I have implemented successfully include:
– Establishing and auditing cleanroom protocols for pattern assembly and shell handling areas.
– Implementing regular filtration and maintenance schedules for dewaxing equipment and media.
– Mandating a final cavity inspection and clean-out using dedicated, oil-free suction devices immediately before mold pre-heat and pouring.
– Redesigning pour cups to include splash basins or filters that trap falling debris before it enters the sprue.
Pillar 2: Shell Process Optimization – The Heart of Quality
This is the most technical pillar. The goal is to produce a shell that is dense, strong, uniformly dried/hardened, and well-bonded. The process variables differ significantly between the two primary investment casting shell systems.
A. Material Selection: The choice of refractories and binders sets the foundation. The following table summarizes critical specifications for common materials used in both processes.
| Material | Primary Use | Key Chemical/Physical Requirements |
|---|---|---|
| Silica Sol | Binder | SiO2 content ~30%, Na2O ≤ 0.5%, pH 9-10, viscosity ≤ 8×10⁻⁴ m²/s, particle size 9-20 nm. |
| Zircon Flour/Sand | Facecoat | ZrO2 ≥ 65%, (ZrO2+SiO2) ≥ 98.6%, Fe2O3 ≤ 0.1%, pH ~6.0. |
| Mullite Flour/Sand | Backup Coats | Al2O3 44-48%, SiO2 50-54%, low alkali & lime content. |
| Waterglass | Binder | Modulus (M) = 3.0-3.4; Density: Facecoat 1.25-1.28 g/cm³, Backup 1.30-1.32 g/cm³. |
| Quartz Flour/Sand | Face/Backup | SiO2 ≥ 98%, alkali oxides ≤ 1.0%, moisture ≤ 0.3%. |
| Alumina-Chamotte Flour | Backup Coats | Al2O3 > 80%, low impurities, moisture ≤ 0.3%. |
B. Slurry Formulation and Control: The slurry, a suspension of refractory flour in the binder, must be precisely controlled. Key parameters are the binder-to-powder ratio (often expressed as a weight ratio), viscosity, and pH. The viscosity ($\eta$) is a critical control parameter and can be related to the solids loading ($\phi$) by models like the Krieger-Dougherty equation for concentrated suspensions:
$$ \eta = \eta_0 \left(1 – \frac{\phi}{\phi_{max}}\right)^{-[\eta] \phi_{max}} $$
where $\eta_0$ is the binder viscosity, $\phi_{max}$ is the maximum packing fraction, and $[\eta]$ is the intrinsic viscosity. In practice, we control this via routine viscosity measurements (e.g., using a Zahn or Ford cup) and density checks. For a silica sol facecoat slurry, a typical flour-to-binder ratio is 3.6:1 to 4.0:1 by weight, yielding a viscosity of 32-38 seconds (Ford #4 cup). Adequate aging (“reposing”) time after mixing is crucial for complete powder wetting and de-aeration; 24 hours for new slurry is a common standard in investment casting.
C. The Shell-Building Process Parameters: Each dip, sand stucco application, and drying/hardening step must be controlled. The following tables contrast the two main processes. Note that drying in silica sol systems is a physical gelation and moisture removal process, while hardening in waterglass systems is a chemical reaction.
| Shell Layer | Stucco Grit Size (Mesh) | Drying Environment | Minimum Drying Time (hrs) |
|---|---|---|---|
| Facecoat (1st) | 100-120 | 22-26°C, 60-70% RH, Low Airflow | 4-6 |
| Transition (2nd) | 30-60 | 22-26°C, 40-60% RH, Moderate Airflow | >8 |
| Backup (3rd-n) | 16-30 | 22-26°C, 40-60% RH, High Airflow (6-8 m/s) | >12 |
| Seal Coat | N/A | 22-26°C, 40-60% RH | >14 |
The drying time ($t_d$) for a silica sol layer can be approximated by a diffusion-limited model, emphasizing why controlling humidity (RH) is critical:
$$ t_d \propto \frac{\delta^2}{D_{eff}} $$
where $\delta$ is the coating thickness and $D_{eff}$ is the effective moisture diffusivity, which is highly dependent on temperature and ambient RH.
| Shell Layer | Stucco | Hardening (in AlCl3 Solution) | Drain/Dry Time |
|---|---|---|---|
| Facecoat | Fine Quartz Sand | 20-25°C, 10-20 min | 15-40 min (air dry) |
| Backup Coats | Coarser Quartz/Alumina | 20-25°C, 20-25 min | 20-30 min (often forced air) |
The hardening reaction for waterglass with aluminum chloride can be simplified as:
$$ \text{Na}_2\text{O} \cdot n\text{SiO}_2 + \text{AlCl}_3 + \text{H}_2\text{O} \rightarrow \text{SiO}_2 \cdot n\text{H}_2\text{O} (gel) + \text{Al(OH)}_3 + \text{NaCl} $$
Inadequate hardening time, incorrect concentration, or insufficient drying between layers leads to a weak, poorly consolidated shell prone to spalling—a direct precursor to sand holes in the subsequent investment casting operation.
D. Process Monitoring and Control: Beyond parameters, implementing statistical process control (SPC) for slurry properties, recording environmental conditions, and performing regular shell strength tests (e.g., modulus of rupture tests on sample bars) are essential practices for consistent investment casting shell quality.
Pillar 3: Design for Manufacturing (DFM) in Investment Casting
The design of the wax pattern and the gating system significantly influences defect formation. Collaborative work with design engineers has yielded several key principles:
- Pattern Design: Avoid sharp internal corners in the wax pattern. Incorporate generous radii to facilitate smooth coating and reduce stress concentration in the ceramic shell. Ensure wax injection parameters eliminate micro-cracks.
- Gating System Design: The gating system must achieve several goals: minimize turbulence, avoid direct impingement of metal on delicate shell areas, and promote favorable thermal gradients. Computational Fluid Dynamics (CFD) simulation is an invaluable tool for optimizing this in investment casting. The use of filters, flow diffusers, or tangential gating can reduce erosive forces. The initial fill velocity is critical; a common rule of thumb is to keep the gate velocity ($v_g$) below a critical threshold to prevent erosion:
$$ v_g < \sqrt{\frac{\sigma_{shell}}{\rho_{metal} \cdot C_d}} $$
where $\sigma_{shell}$ is the shell’s erosion resistance strength, $\rho_{metal}$ is the metal density, and $C_d$ is a drag coefficient. - Pouring Practice: Adopt a “press-and-pour” or “tilt-pour” technique where possible to reduce metal drop height and initial impact. Start the pour slowly to allow the metal to rise smoothly up the sprue before increasing the flow rate.
Advanced Considerations and Emerging Trends
The pursuit of zero defects in investment casting is ongoing. Several advanced topics warrant discussion:
Shell Drying Kinetics: For silica sol shells, the drying process is rate-limiting. The use of dehumidified air, temperature-controlled drying chambers, and even microwave-assisted drying technologies can dramatically reduce cycle times while improving shell uniformity and strength. The drying rate can be modeled more comprehensively by considering both internal and external mass transfer resistances.
Alternative Binders and Materials: New binder systems, such as hybrid sol-silicate or environmentally friendly colloidal alumina, are being explored. These may offer different gelation behaviors and improved high-temperature properties, further reducing the risk of shell-related defects in investment casting.
Non-Destructive Testing (NDT): For high-integrity investment castings, post-cast NDT like digital radiography (DR) or computed tomography (CT) scanning is becoming standard to detect internal sand holes and other inclusions that escape visual and machining inspection.
Data Analytics and AI: Integrating data from all stages of the investment casting process—wax injection, shell room environment, slurry properties, furnace parameters, and pour data—into a centralized database allows for predictive analytics. Machine learning models can identify subtle correlations between process deviations and the later occurrence of sand hole defects, enabling proactive correction.
Conclusion: A Culture of Prevention in Investment Casting
Mitigating sand hole defects in investment casting is not achieved by a single silver bullet but through the diligent application of a comprehensive, science-based strategy. It requires a deep understanding of materials science (binder chemistry, refractory properties), fluid dynamics (metal flow, slurry rheology), and process engineering (drying kinetics, thermal processing). From my perspective, the most successful investment casting foundries are those that view the ceramic shell not just as a disposable mold, but as a precision-engineered component in its own right. They combine stringent contamination control, statistically managed shell-building processes, and intelligent design principles. Furthermore, fostering a culture of continuous improvement and root-cause problem-solving among all personnel is indispensable. By embracing this holistic approach, the incidence of sand hole defects can be driven down to negligible levels, ensuring that investment casting continues to deliver components of the highest integrity for the most demanding applications across aerospace, medical, and energy sectors. The journey towards flawless investment casting is perpetual, but each step in understanding and controlling these complex interactions yields tangible rewards in quality and reliability.