
In my extensive experience in foundry engineering, the pursuit of efficient and cost-effective manufacturing methods for complex automotive components has always been a central focus. Among these, shell castings for critical assemblies like wheel reducers present significant challenges in terms of quality, material integrity, and production economics. Traditional sand casting methods, while widely used, often fall short in delivering consistent results, especially for ductile iron parts requiring specific microstructures. This article details my firsthand application and optimization of the sand-faced metal mould casting process specifically for automotive wheel reducer shell castings. This technique, which marries the advantages of permanent metal moulds with thin sand linings, has proven transformative for producing high-integrity shell castings in an as-cast condition.
The core challenge with wheel reducer shell castings lies in their geometry—a cylindrical body with a substantial flange and significant variation in wall thickness. Producing these as ductile iron castings, particularly with a ferritic matrix like QT450-10, demands precise control over the solidification kinetics. Rapid cooling, inherent to metal mould processes, can lead to undesirable carbide formation and inhibited graphite nodularization. My approach involved a comprehensive redesign of the process around the sand-faced metal mould principle, with meticulous attention to gating, cooling modulation via variable sand lining thickness, and the unique challenge of integral core formation. The successful implementation not only validated the process but also yielded substantial economic benefits, reducing costs by approximately 20% compared to conventional green sand methods. Throughout this work, the term ‘shell castings’ refers precisely to these critical, pressure-containing housing components.
The fundamental principle of sand-faced metal mould casting can be described by analyzing the heat transfer dynamics. The process involves a metal mould (the ‘iron type’) coated with a thin, thermally insulating layer of resin-bonded sand. The thermal resistance of the system governs the cooling rate of the casting. We can model the heat extraction using a simplified one-dimensional heat flow equation through the composite wall of the solidifying casting, the sand layer, and the metal mould:
$$ q = \frac{T_{cast} – T_{amb}}{\frac{L_{cast}}{k_{cast}} + \frac{L_{sand}}{k_{sand}} + \frac{L_{mould}}{k_{mould}} + \frac{1}{h}} $$
Here, \( q \) is the heat flux, \( T \) represents temperatures, \( L \) denotes thicknesses, and \( k \) signifies thermal conductivities. The subscript ‘cast’ refers to the solidifying shell casting, ‘sand’ to the facing layer, ‘mould’ to the metal mould, and ‘amb’ to the ambient. The convective heat transfer coefficient at the mould’s outer surface is \( h \). The critical parameter for controlling the cooling rate for ferritic ductile iron shell castings is the sand layer thickness \( L_{sand} \), as its thermal conductivity \( k_{sand} \) is significantly lower than that of the metal mould. By strategically varying \( L_{sand} \), we can create differential cooling rates across the casting, ensuring progressive solidification favorable for feeding and microstructure development.
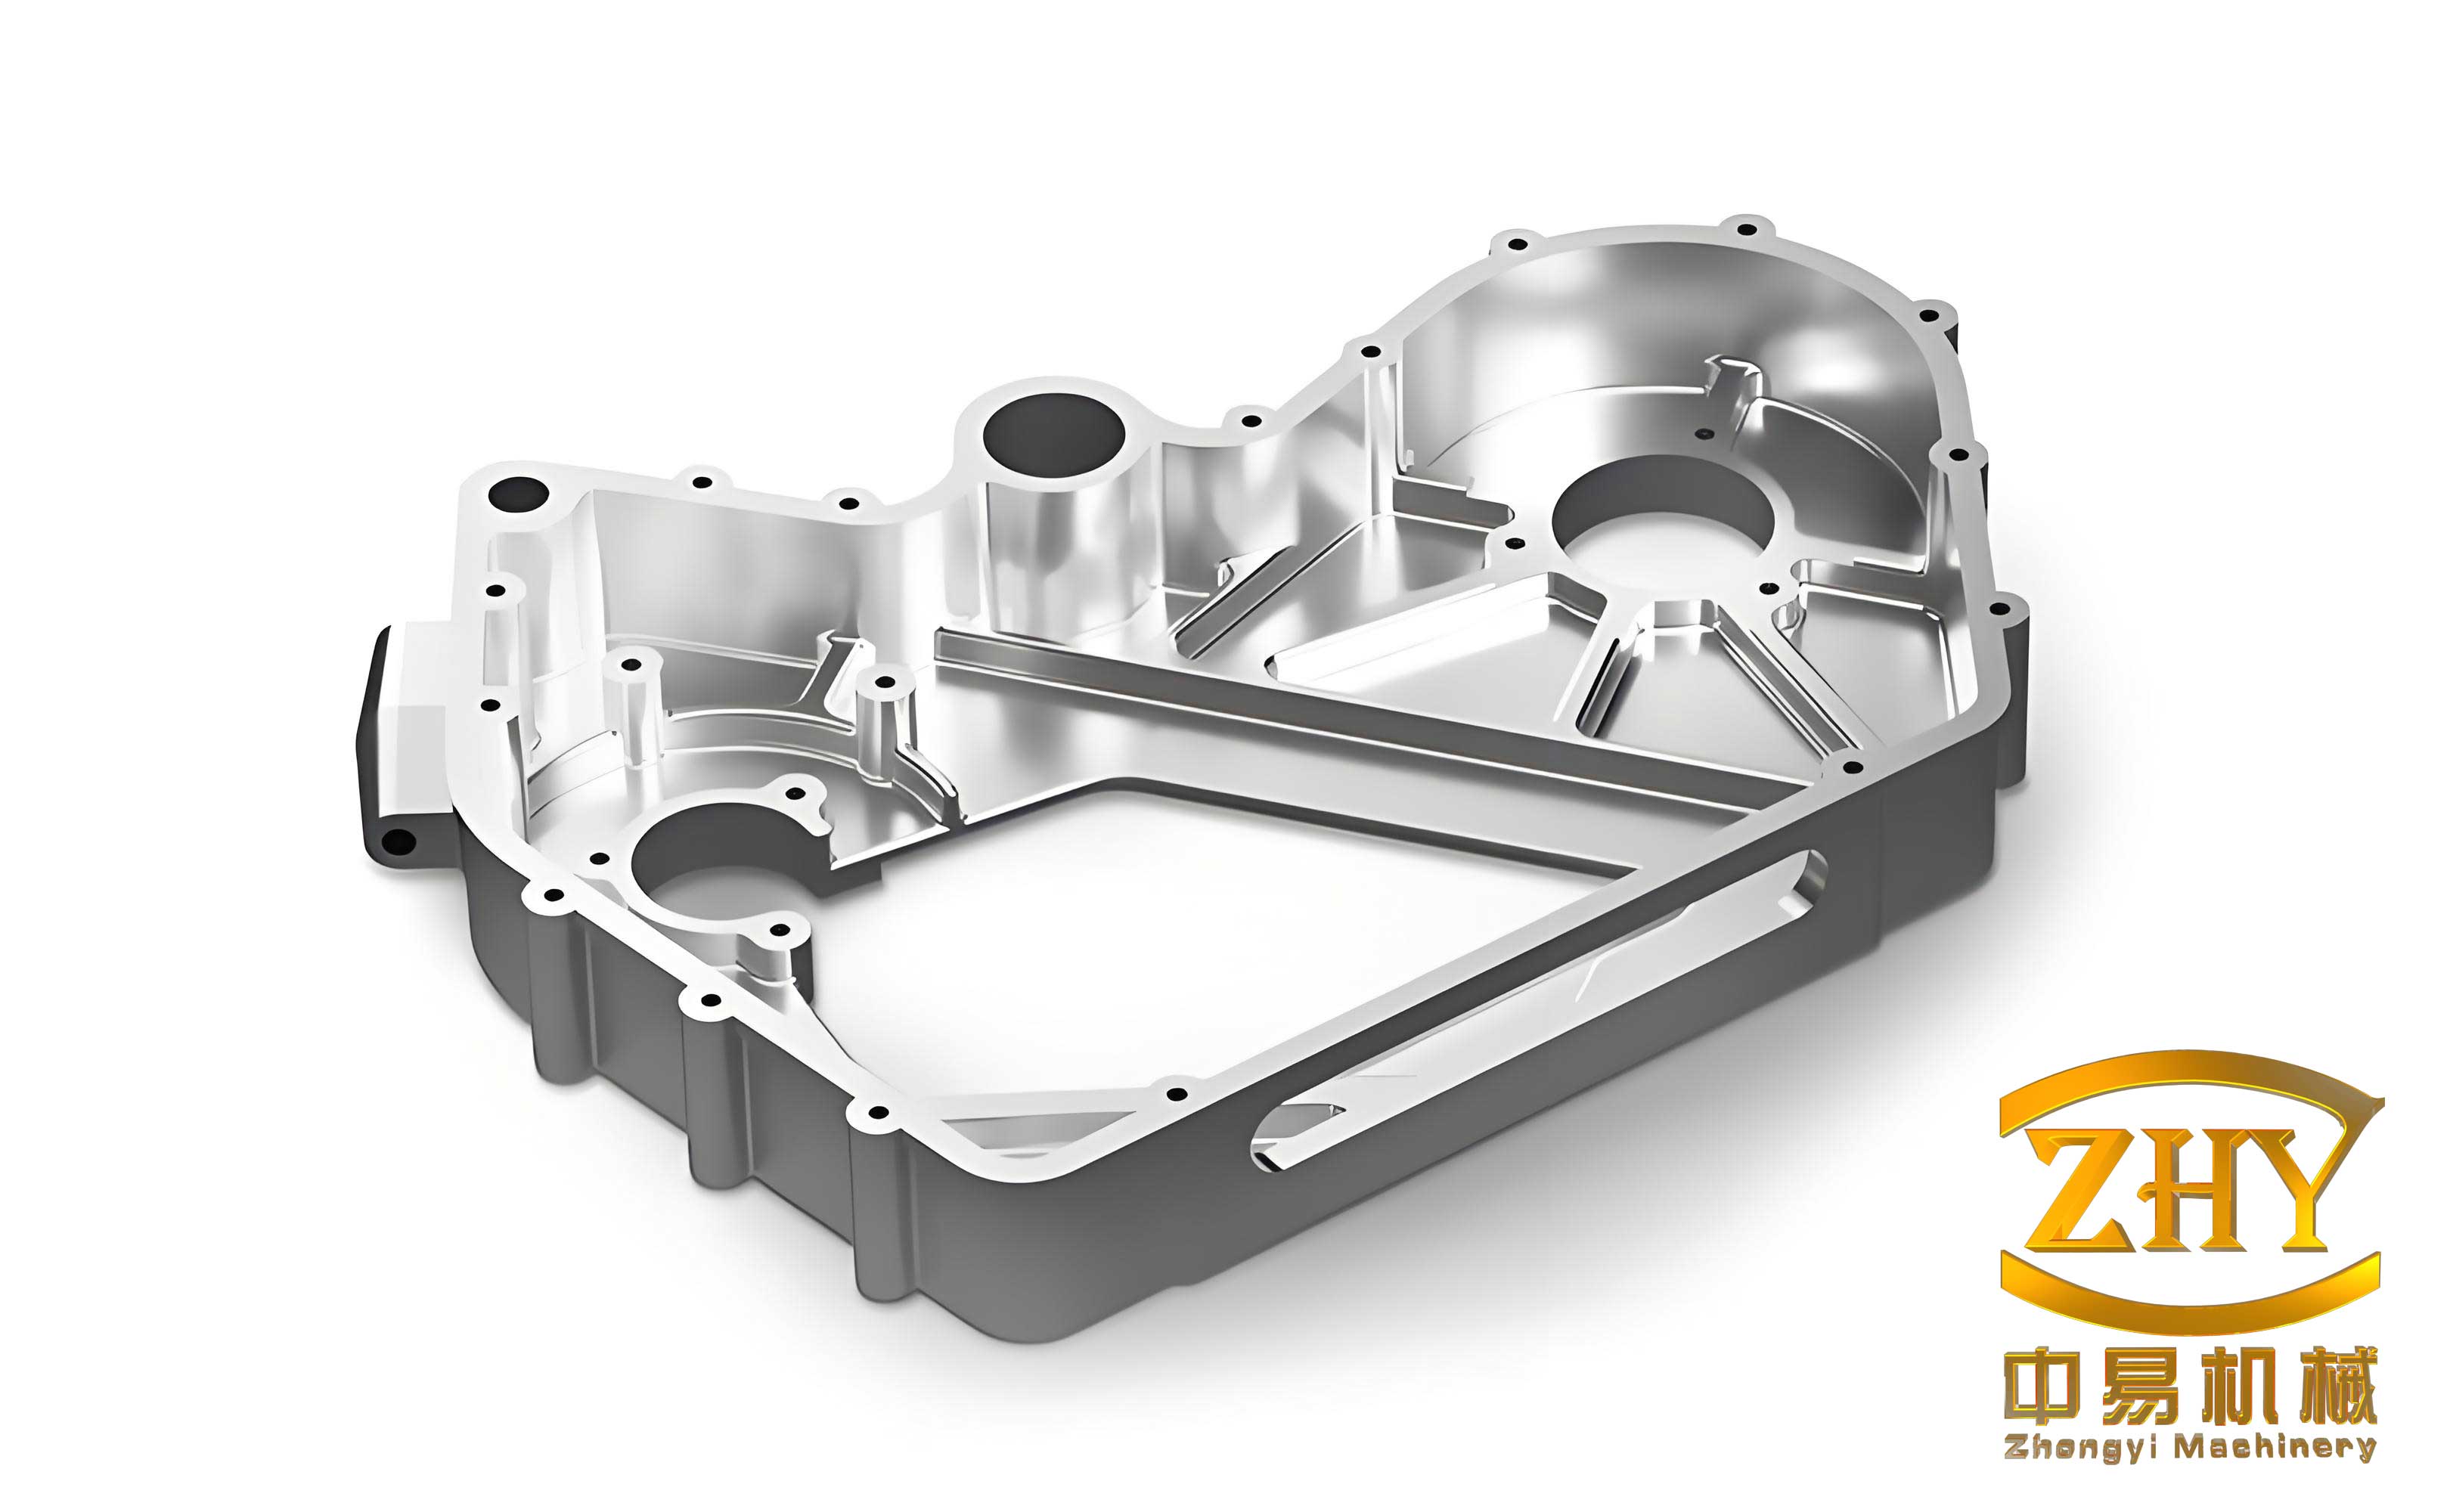
Designing the process for these specific shell castings required addressing several unique aspects. Firstly, to eliminate a separate core-making step and improve accuracy, an integral core (a “self-forming” core) was designed as part of the upper mould half. This presented a significant challenge in ensuring proper venting during the sand shooting process to achieve a dense, uniform sand layer. Secondly, the requirement for a primarily ferritic matrix in the final shell castings necessitated a slower cooling regime than typically used for pearlitic grades. This was primarily managed by adjusting the sand facing thickness. Thirdly, the mechanical extraction of the casting after solidification required special consideration due to the contraction of the casting onto the integral metal core.
The final process design was for a two-cavity mould (producing two shell castings per pour) with a top-pouring, side-gating system. The gating ratio was carefully calibrated to ensure non-turbulent filling and adequate feeding pressure. A key design table summarizing the critical process parameters is presented below:
| Process Parameter | Value or Specification | Rationale for Shell Castings |
|---|---|---|
| Casting Material | Ductile Iron QT450-10 (Ferritic) | Required mechanical properties for automotive wheel reducer housing. |
| Mould Configuration | Horizontal parting, 2 cavities/mould | Optimizes productivity and layout for symmetrical shell castings. |
| Gating System | Top-pouring, side gate on flange | Minimizes slag entrainment, provides thermal gradient for feeding. |
| Gating Ratio (ΣFgate:ΣFrunner:Fsprue) | 1 : 1.2 : 4.5 | Ensures pressurized flow and uses sprue as a feeding riser. |
| Sand Facing Thickness (General) | 7 – 9 mm | Moderates cooling rate to favor ferrite formation in shell castings. |
| Sand Facing Thickness (Feeding Channels) | 12 – 15 mm | Insulates thermal arteries to delay solidification for effective feeding. |
| Sand Facing Thickness (Heavy Sections) | 4 – 5 mm | Accelerates cooling in thick areas to match solidification timing. |
| Mould Temperature at Pouring | 150 – 200 °C | Prevents thermal shock, reduces mistruns, stabilizes cycle time. |
| Metal/Mould Weight Ratio | ~1 : 7 | Provides sufficient thermal mass for consistent cooling of shell castings. |
To virtually validate and refine this design before creating physical tooling, I employed numerical solidification simulation software. The 3D models of the shell castings, gating system, sand layers, and metal mould were constructed and analyzed. The governing energy equation for the transient solidification process, solved by the finite element method in the simulation, is:
$$ \rho c_p \frac{\partial T}{\partial t} = \nabla \cdot (k \nabla T) + \dot{q}_{latent} $$
where \( \rho \) is density, \( c_p \) is specific heat, \( T \) is temperature, \( t \) is time, \( k \) is thermal conductivity, and \( \dot{q}_{latent} \) is the latent heat source term due to phase change. The simulation provided critical insights into temperature fields and feeding patterns. The results confirmed that with the optimized sand thickness profile, the thermal gradients were correctly oriented, with the heavier sections of the shell castings remaining liquid longer to feed the thinner walls. The predicted absence of shrinkage porosity was a key outcome. The progressive solidification from the thin walls towards the thick sections and the feeding sprue can be conceptually verified using Chvorinov’s rule, comparing the modulus (Volume/Surface Area) of different sections:
$$ t_f = K \left( \frac{V}{A} \right)^n $$
Here, \( t_f \) is the local solidification time, \( V \) is volume, \( A \) is the cooling surface area, \( K \) is a constant dependent on mould material and casting properties, and \( n \) is an exponent often close to 2. By designing the process so that the modulus of the feeder (sprue) is greater than that of the thick sections of the shell castings, and the thick sections are greater than the thin walls, directional solidification is promoted.
The transition from simulation to production required precise control over metallurgy and process execution. The chemical composition was tightly controlled to achieve the target as-cast ferritic matrix in the shell castings. A special inoculation and alloying strategy was implemented to counteract the tendency for carbides due to the relatively faster cooling of metal mould processes. The table below details the target composition range and the function of key elements:
| Element | Weight % Range | Role in Shell Castings Production |
|---|---|---|
| Carbon (C) | 3.75 – 3.85 | Promotes graphite formation, provides graphitic expansion to counteract shrinkage. |
| Silicon (Si) | 2.70 – 2.85 | Strong graphitizer, essential for achieving ferritic matrix in as-cast shell castings. |
| Manganese (Mn) | 0.10 – 0.15 | Kept very low to prevent segregation and stabilize ferrite. |
| Sulfur (S) | 0.010 – 0.015 | Low level is critical for efficient Mg treatment and nodule formation. |
| Phosphorus (P) | ≤ 0.030 | Minimized to reduce embrittlement in the final shell castings. |
| Magnesium (Mg) | 0.032 – 0.058 | Nodulizing agent, crucial for achieving spherical graphite in ductile iron shell castings. |
| Cerium (Ce) & other RE | Trace (via inoculant) | Counteracts deleterious trace elements, improves inoculation effectiveness. |
The melting and treatment practice was pivotal. I used a medium-frequency induction furnace, with a tapping temperature of 1500-1530°C. The treatment involved a low-rare-earth ferritic-grade nodulizer added at 1.2% in a sandwich method, followed by a robust inoculation practice using a composite inoculant totaling 1.3%. Multiple inoculation stages (ladle, stream, and in-mould) were employed to ensure a high nodule count and suppress chill in the shell castings. The pouring temperature was maintained between 1380-1420°C to balance fluidity and thermal demand on the mould.
Production results on a dedicated sand-faced metal mould casting line confirmed the simulation predictions and design efficacy. The shell castings were produced consistently with excellent surface finish and dimensional accuracy. Sectioning and machining of critical areas revealed no subsurface shrinkage defects. Mechanical testing confirmed the properties met the QT450-10 specification. The microstructure of the shell castings, examined at various locations, consistently showed a matrix of over 85% ferrite with well-nodularized graphite (Type I, size class 6-7) and no free carbides, fulfilling the requirement for as-cast production. The economic analysis revealed significant gains, primarily from a higher metal yield (near-net-shape, minimal gating), drastic reduction in scrap rate (from sand-related defects), and the elimination of a separate annealing heat treatment cycle normally required for ferritic ductile iron shell castings produced in sand.
The relationship between the process parameters and the final quality of shell castings can be further formalized. The success in achieving sound, as-cast ferritic shell castings hinges on balancing the cooling rate. An empirical relationship linking the sand thickness (\(L_s\)), the critical cooling rate through the eutectic range for carbide avoidance (\(CR_{crit}\)), and the casting section modulus (\(M\)) can be postulated:
$$ CR_{calc} = f(T_{pour}, T_{mould}, k_s, L_s, M) \leq CR_{crit} $$
For the specific alloy and shell castings geometry, the designed sand thickness profile ensured \(CR_{calc}\) remained below \(CR_{crit}\) while still being sufficiently high to achieve a dense, fine microstructure. Furthermore, the feeding efficiency (\(FE\)) can be expressed as a function of the temperature gradient (\(G\)) and the solidification velocity (\(R\)), often referenced in the context of the \(G/R\) ratio for soundness:
$$ FE \propto \frac{G}{\sqrt{R}} $$
The designed gating and sand thickness variation maximized \(G\) in the direction toward the feeder, ensuring high feeding efficiency for these complex shell castings.
In conclusion, the application of sand-faced metal mould casting technology to automotive wheel reducer shell castings represents a significant advancement in manufacturing efficiency and product quality. From my perspective, the key to success was a holistic integration of innovative tooling design (addressing the integral core challenge), physics-based simulation for optimization, and precise metallurgical control tailored to the constraints and advantages of the process. The ability to produce high-integrity, as-cast ferritic ductile iron shell castings with minimal finishing and no heat treatment unlocks substantial value. This case study underscores the potential of this versatile process for a wide range of medium-to-high volume cast components where quality, consistency, and cost are paramount. The repeated success in producing these demanding shell castings validates the robustness of the approach and serves as a model for similar applications in the automotive and heavy machinery sectors.