
In the realm of precision manufacturing for critical components such as sun wheels, which serve as essential parts in large gear pumps, the demand for high dimensional accuracy and superior surface finish is paramount. To meet these stringent requirements, our team has extensively relied on and refined the investment casting process. This article, drawn from our practical experience, delves into the comprehensive methodology we employed to successfully produce a series of sun wheel castings, effectively overcoming significant challenges like shrinkage porosity at thermal junctions. The entire investment casting operation, from pattern creation to final pouring, will be detailed here, incorporating analytical summaries via tables and formulas to encapsulate key process parameters.
The sun wheels in question varied in design, including both straight and helical gear blades, with dimensions ranging from 189mm × 66mm to 272mm × 279mm and weights between 15 kg and 43 kg. The material specification was CF8M, an austenitic stainless steel. The primary obstacle was eliminating severe shrinkage cavities and porosity at the hot spots near the ingate roots, a common issue in thick-section investment casting. Through systematic process design, we achieved defect-free castings. The following sections elaborate on each stage of our investment casting protocol.
1. Wax Pattern Fabrication and Gating System Design
The initial phase in any investment casting process is the creation of an accurate wax pattern. Given the substantial size of the sun wheel, we utilized aluminum dies for injection molding. The wax injection parameters were meticulously controlled to ensure pattern integrity and dimensional stability. The process conditions are summarized below:
| Parameter | Value or Range | Remarks |
|---|---|---|
| Ambient Temperature | 22–24 °C | Maintained for consistent wax behavior |
| Wax Temperature | 56–60 °C | Optimal for fluidity and minimal shrinkage |
| Injection Pressure | 0.8–1.0 MPa | Ensures complete die filling |
| Injection Time | 50 s | Controlled to prevent turbulence |
| Holding Time | 20 min | Critical for compensating wax solidification shrinkage |
After ejection, patterns were cooled in water to minimize distortion, and parting lines and flow marks were meticulously removed. The gating system design is arguably the most critical aspect in preventing shrinkage defects in investment casting. For this sun wheel, we adopted a top-feeding system with a sizable riser to act as a thermal and mass reservoir. The gating assembly was modular for ease of fabrication. The main runner block measured 160 mm × 150 mm × 110 mm, and to ensure stability and adequate feeding, two pouring cups (each Ø130 mm × Ø90 mm × 180 mm) were employed. The design prioritized directional solidification towards the riser. The volume ratio of the gating system to the casting is a key factor, often expressed by the feeding modulus, $M$, defined as the volume-to-surface area ratio:
$$ M = \frac{V}{A} $$
where $V$ is the volume and $A$ is the surface area of the casting section. For effective feeding, the riser’s modulus, $M_r$, must satisfy $M_r > k \cdot M_c$, where $M_c$ is the modulus of the casting’s hot spot and $k$ is a safety factor (typically 1.1 to 1.2). Our design ensured this criterion was met for the thick hub section. The gating system also incorporated handling lugs on the runner block for safer manipulation during subsequent investment casting steps.
2. Shell Building via Silica Sol Process
To achieve the necessary shell strength and surface finish, we employed a silica sol binder system, a cornerstone of modern precision investment casting. The shell was built up with multiple layers, each with specific slurry compositions and stucco applications. The process parameters were optimized to balance permeability, strength, and dimensional accuracy. The slurry formulations for different coats are detailed below:
| Coating Layer | Binder & Refractory | Liquid-to-Powder Ratio (by weight) | Cup Viscosity (s) | Powder & Stucco Details |
|---|---|---|---|---|
| Primary (1st & 2nd) | Silica Sol + Zircon Flour | 1 : 3.6 | 36 ± 2 | Zircon flour, 320 mesh |
| Intermediate (3rd) | Silica Sol + Chamotte Flour | 1 : (1.6–1.8) | 16–19 | Chamotte sand, 30–60 mesh |
| Back-up (4th–7th) | Silica Sol + Chamotte Flour | 1 : (1.3–1.5) | 13–15 | Chamotte sand, 16–30 mesh |
| Seal Coat | Silica Sol + Chamotte Flour | 1 : (1.1–1.2) | 12–13 | – |
The drying conditions for each layer were strictly controlled to prevent cracking or inadequate bonding, which is vital for the integrity of the investment casting mold. The following table outlines the drying schedule:
| Coating Layer | Stucco Material (Mesh Size) | Drying Temperature (°C) | Relative Humidity (%) | Drying Time (h) | Airflow |
|---|---|---|---|---|---|
| Primary (1st) | Zircon Sand, 100 mesh | 24 ± 2 | 50–70 | 8–9 | Still air |
| Primary (2nd) | Mullite Sand, 80 mesh | 24 ± 2 | 50–70 | 12–14 | Gentle breeze |
| Intermediate (3rd) | Chamotte Sand, 30–60 mesh | 24 ± 2 | 40–60 | 15–16 | 3–5 m/s |
| Back-up (4th–7th) | Chamotte Sand, 16–30 mesh | 24 ± 2 | 30–50 | 16–18 | 6–8 m/s |
| Seal Coat | – | 24 ± 2 | 30–50 | 24 | 6–8 m/s |
During shell building, particular attention was paid to clearing loose sand from the intricate blade passages after each coating to ensure they remained open. This is a critical step in investment casting to avoid blockages that could cause gas entrapment or incomplete filling.
3. Dewaxing: A Modified Sequential Approach
Dewaxing is a sensitive step in investment casting, especially for large, complex shells with varying wall thicknesses. Conventional rapid dewaxing can induce thermal stresses, leading to shell cracking or distortion. To mitigate this, we implemented a modified sequential dewaxing technique. The entire shell, except for the exposed riser, was wrapped with three layers of waste newspaper. This insulation ensured that the riser area was heated first during autoclave dewaxing, allowing the wax to melt and drain out through the riser, creating a clear path before the bulk of the shell heated up. This promoted a more controlled, directional wax removal, reducing internal pressure. The dewaxing parameters were:
- Pressure: 0.60–0.75 MPa
- Time: 25–30 minutes
The effectiveness of this method can be partly analyzed by considering the heat transfer. The rate of wax melting is governed by the heat flux, $q$, which can be approximated by Fourier’s law in one dimension during the initial phase:
$$ q = -k \frac{\Delta T}{\Delta x} $$
where $k$ is the thermal conductivity of the shell/wax composite, $\Delta T$ is the temperature difference, and $\Delta x$ is the thickness. By insulating the main body, we effectively increased $\Delta x$ for that region, slowing its heating and allowing the riser pathway to establish first. This procedural innovation is a significant refinement in the investment casting workflow for heavy-section castings.
4. Shell Firing and Pouring Methodology
Proper firing of the ceramic shell is essential to remove residual volatiles, sinter the binder, and achieve adequate high-temperature strength for the investment casting pour. Given the shell’s large volume and the casting’s significant thermal mass, we employed an elevated temperature with an extended soak time to ensure uniform heating through the shell thickness. The firing regime was:
- Firing Temperature: 1080–1100 °C
- Soaking Time: 1.0–1.5 hours
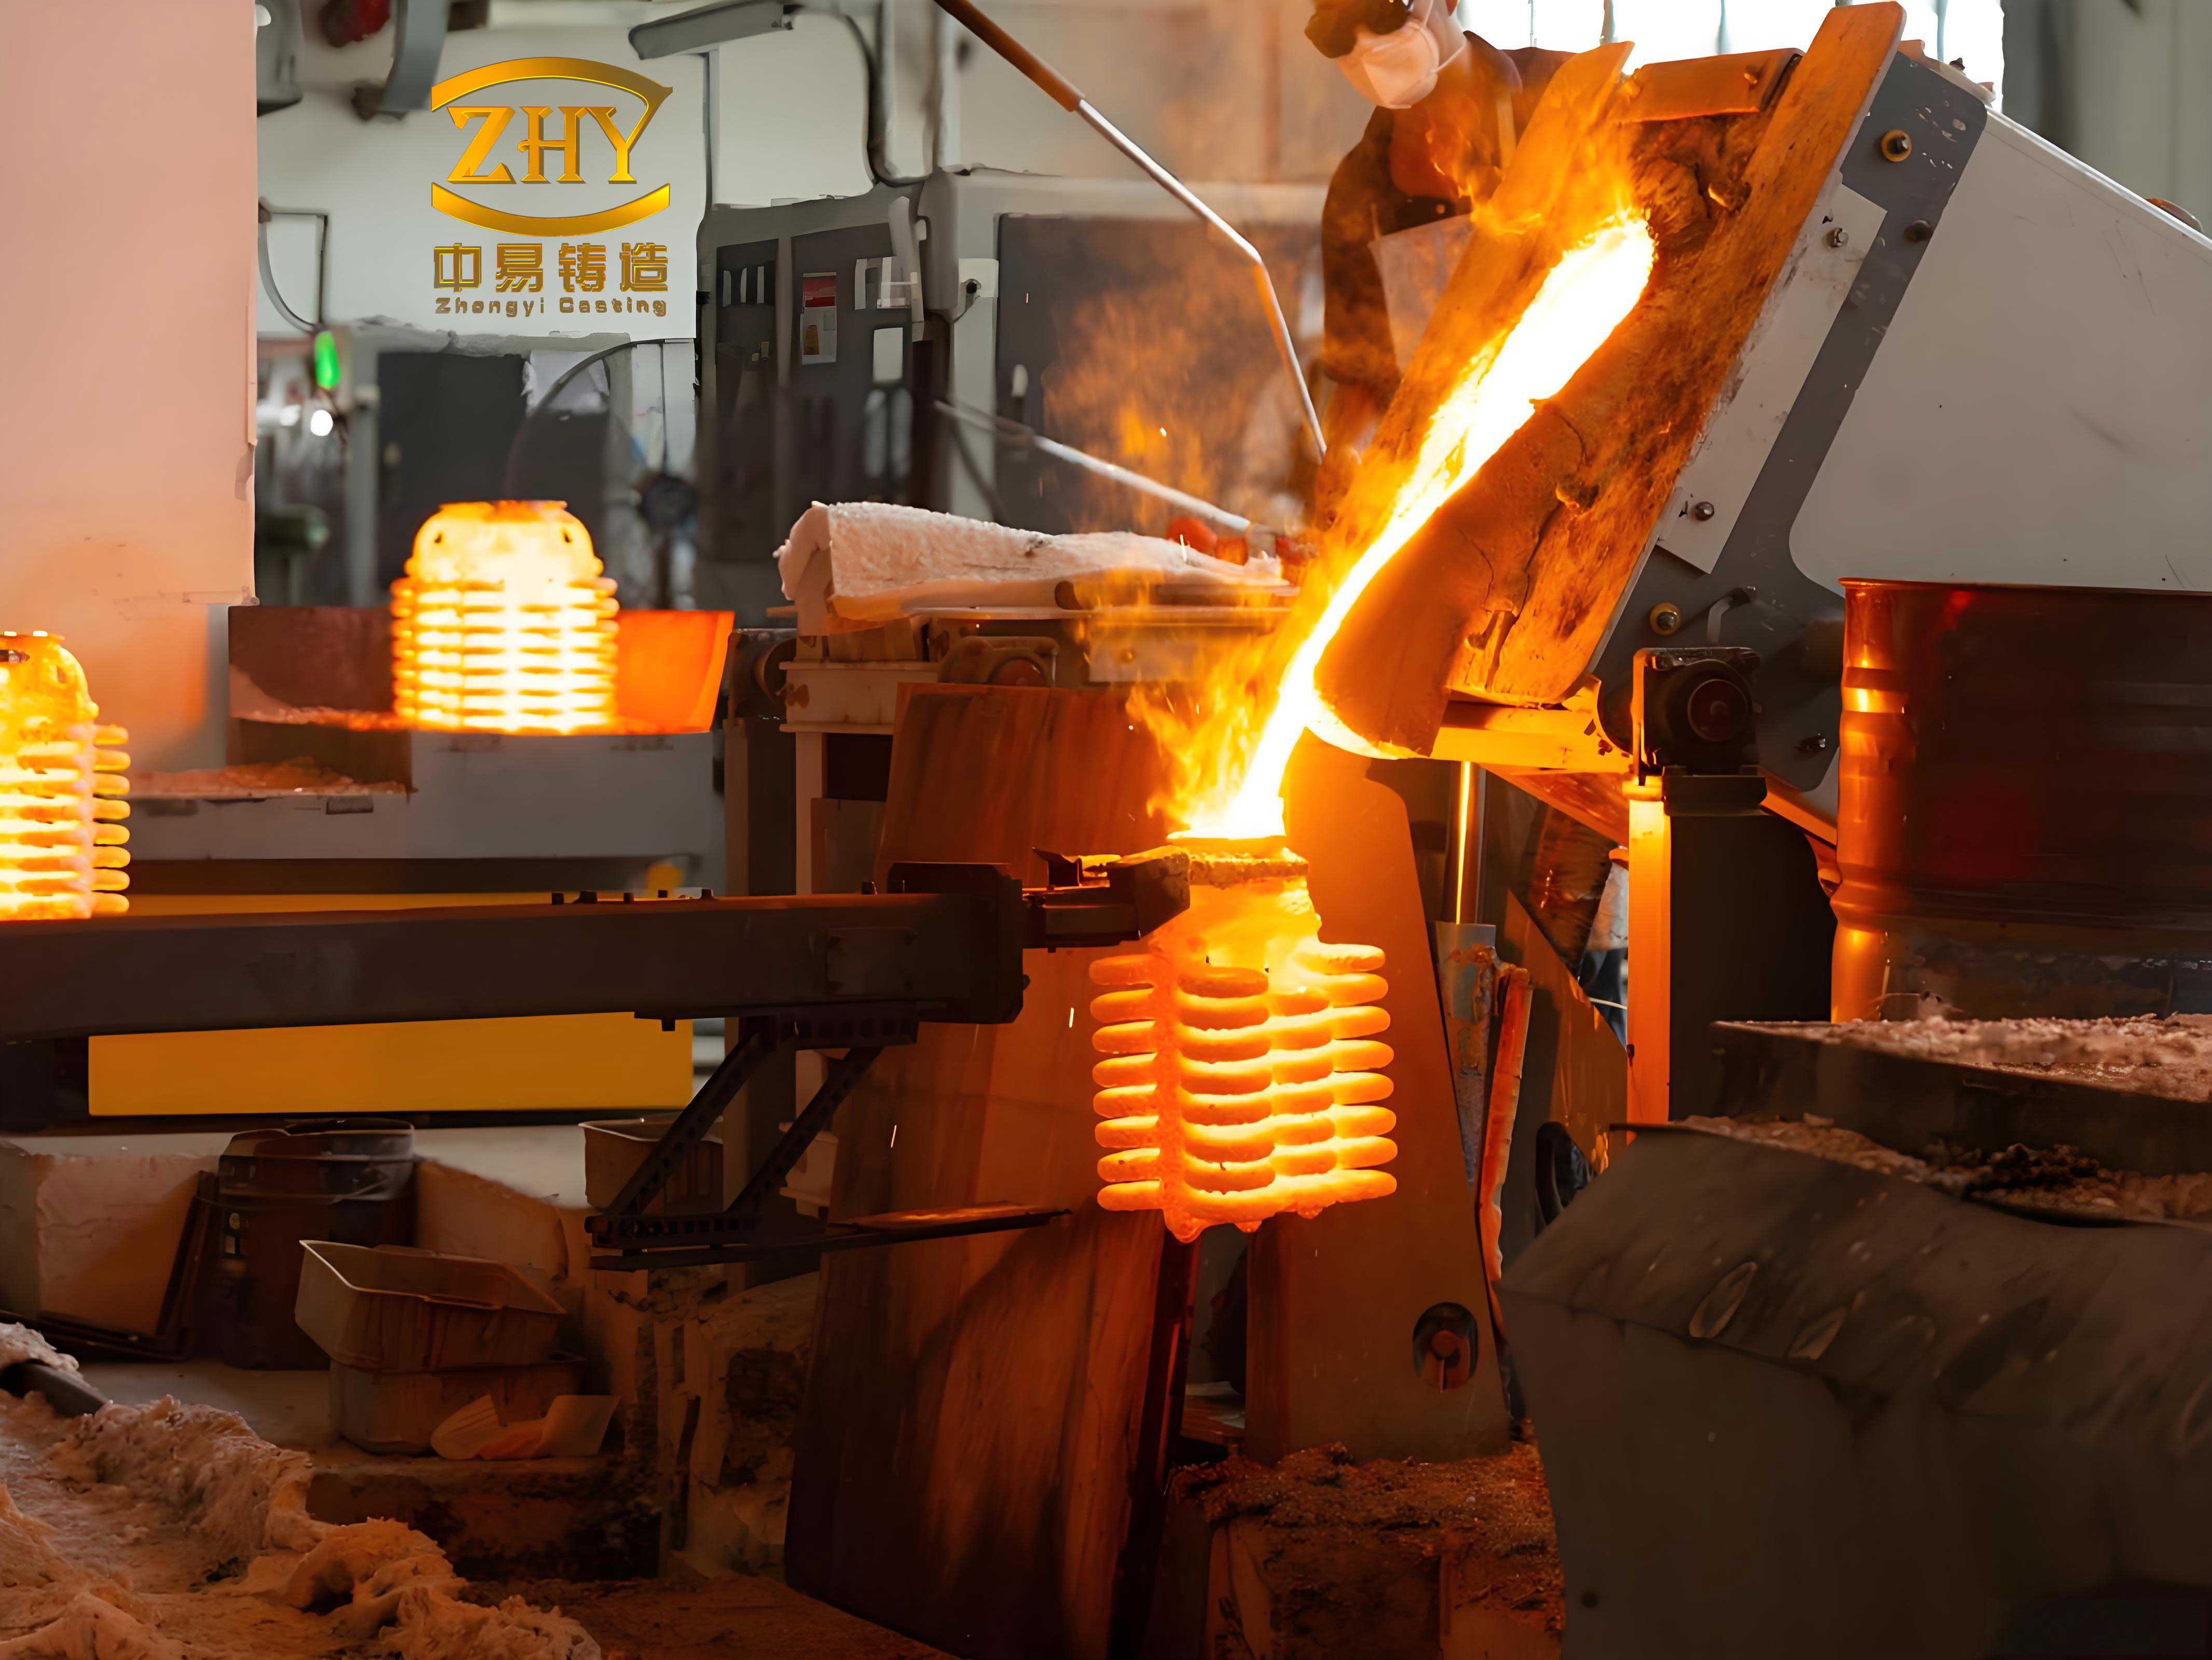
This ensures complete combustion of any organic residues and development of sufficient ceramic bond strength. The pouring procedure was carefully choreographed. The shell was withdrawn from the furnace at a temperature exceeding 1000°C to minimize thermal shock to the metal. The CF8M steel was superheated to a pouring temperature of 1620–1630°C. The pour was conducted steadily over approximately 120 seconds to ensure smooth, turbulence-free filling—a key tenet of sound investment casting practice. Within 30 seconds of the main pour, the riser was topped up with additional molten metal, and exothermic insulating compounds were added to retard solidification in the riser, enhancing its feeding efficiency.
To directly address the core issue of shrinkage at the hub’s hot spot, we implemented a forced cooling strategy post-pouring. The casting, placed on a dedicated steel frame base, was subjected to forced air cooling directed specifically into the internal passages and the thick hub section. This accelerates solidification in the hot spot, reducing the time available for pore formation. The cooling rate, $\frac{dT}{dt}$, in such a scenario can be influenced by convective heat transfer:
$$ q_{conv} = h A (T_{surface} – T_{air}) $$
where $h$ is the convective heat transfer coefficient, $A$ is the surface area exposed to airflow, and $T_{surface} – T_{air}$ is the temperature differential. By increasing $h$ through forced airflow, we elevated $\frac{dT}{dt}$, promoting directional solidification towards the riser. This active cooling measure is a powerful tool in the investment casting of components prone to centerline shrinkage.
5. Process Outcomes and Metallurgical Considerations
Upon shakeout and final cleaning, the sun wheel castings were thoroughly inspected. The results were highly satisfactory: the intricate gear blades showed no measurable distortion, and radiographic and penetrant testing confirmed the absence of shrinkage cavities or porosity in the critical hub and ingate junction areas. The dimensional tolerances and surface finish met all specified requirements, validating the entire investment casting process design.
The success hinges on the integrated control of multiple factors. In investment casting, the solidification sequence is paramount. The Chvorinov’s rule, while simplistic, provides a foundational understanding:
$$ t_s = B \left( \frac{V}{A} \right)^n $$
where $t_s$ is the solidification time, $V/A$ is the modulus, $B$ is a mold constant, and $n$ is an exponent (typically ~2). Our gating design ensured the riser had the largest modulus, solidifying last. Combined with controlled cooling, this created a positive temperature gradient from the casting towards the riser. Furthermore, the quality of the silica sol shell contributed significantly. The high-temperature strength of the fired shell can be related to the binder bonding mechanism, which involves the formation of siloxane bonds (Si-O-Si) during firing. The shell’s permeability, crucial for allowing air displacement during pouring and gas evolution during solidification, is a function of the stucco particle size distribution and layer thickness. Our multi-layer approach with progressively coarser stucco optimized this property.
6. Extended Discussion on Process Optimization
The investment casting of large sun wheels presents ongoing opportunities for optimization. Computer simulation of solidification and stress development could further refine gating and cooling designs. For instance, simulating the temperature field, $T(x,y,z,t)$, using the heat conduction equation with phase change:
$$ \rho c_p \frac{\partial T}{\partial t} = \nabla \cdot (k \nabla T) + \dot{q}_{latent} $$
where $\rho$ is density, $c_p$ is specific heat, $k$ is thermal conductivity, and $\dot{q}_{latent}$ is the latent heat release rate, would allow predictive identification of hot spots. Additionally, the rheology of the silica sol slurries is critical for coating uniformity. The viscosity, $\eta$, often follows a non-Newtonian behavior describable by models like the Herschel-Bulkley equation:
$$ \tau = \tau_0 + K \dot{\gamma}^n $$
where $\tau$ is shear stress, $\tau_0$ is yield stress, $K$ is consistency index, $\dot{\gamma}$ is shear rate, and $n$ is flow index. Controlling these parameters ensures proper coating thickness and defect-free shells. Another aspect is the dewaxing kinetics. The rate of wax removal can be modeled considering pressure-driven flow through the porous shell network, described in simplified form by Darcy’s law:
$$ v = -\frac{\kappa}{\mu} \frac{\Delta P}{L} $$
where $v$ is flow velocity, $\kappa$ is shell permeability, $\mu$ is wax viscosity, $\Delta P$ is pressure drop, and $L$ is flow path length. Our sequential method effectively managed $\Delta P$ and $L$ to prevent shell failure. These scientific principles underpin the art of reliable investment casting.
7. Conclusion
The production of high-integrity sun wheel castings via the investment casting process demands a holistic and meticulously controlled approach. By designing a gating system that promotes directional solidification, implementing a robust silica sol shell-building regimen with precise parameters, innovating the dewaxing step to prevent shell damage, executing a high-temperature shell firing, and complementing the pour with strategic riser feeding and forced cooling, we successfully eliminated shrinkage defects. This case underscores the capability of advanced investment casting to manufacture complex, high-performance components with exceptional quality. The integration of empirical process control with fundamental engineering principles, as illustrated through the tables and formulas presented, provides a replicable framework for tackling similar challenges in precision investment casting.