
In my daily work with large gray iron and ductile iron casting, I treat every component as an integrated thermal, metallurgical, and fluid-flow system. The component is not only a shape poured into sand; it is a sequence of charge preparation, melting, treatment, inoculation, molding, gating, feeding, solidification, cooling, heat treatment, cleaning, and inspection decisions. When the casting is large, every one of those decisions becomes more sensitive because the wall thickness is uneven, the modulus varies widely, the solidification time is long, and the opportunity for gas, shrinkage, and matrix imbalance increases. For ductile iron casting, the difficulties are even more concentrated because the alloy must achieve spheroidal graphite while also resisting shrinkage and maintaining a pearlitic matrix above 80%. I have found that stable production is achieved only when the process window is defined numerically, checked with formulas, and verified against tables of practical limits.
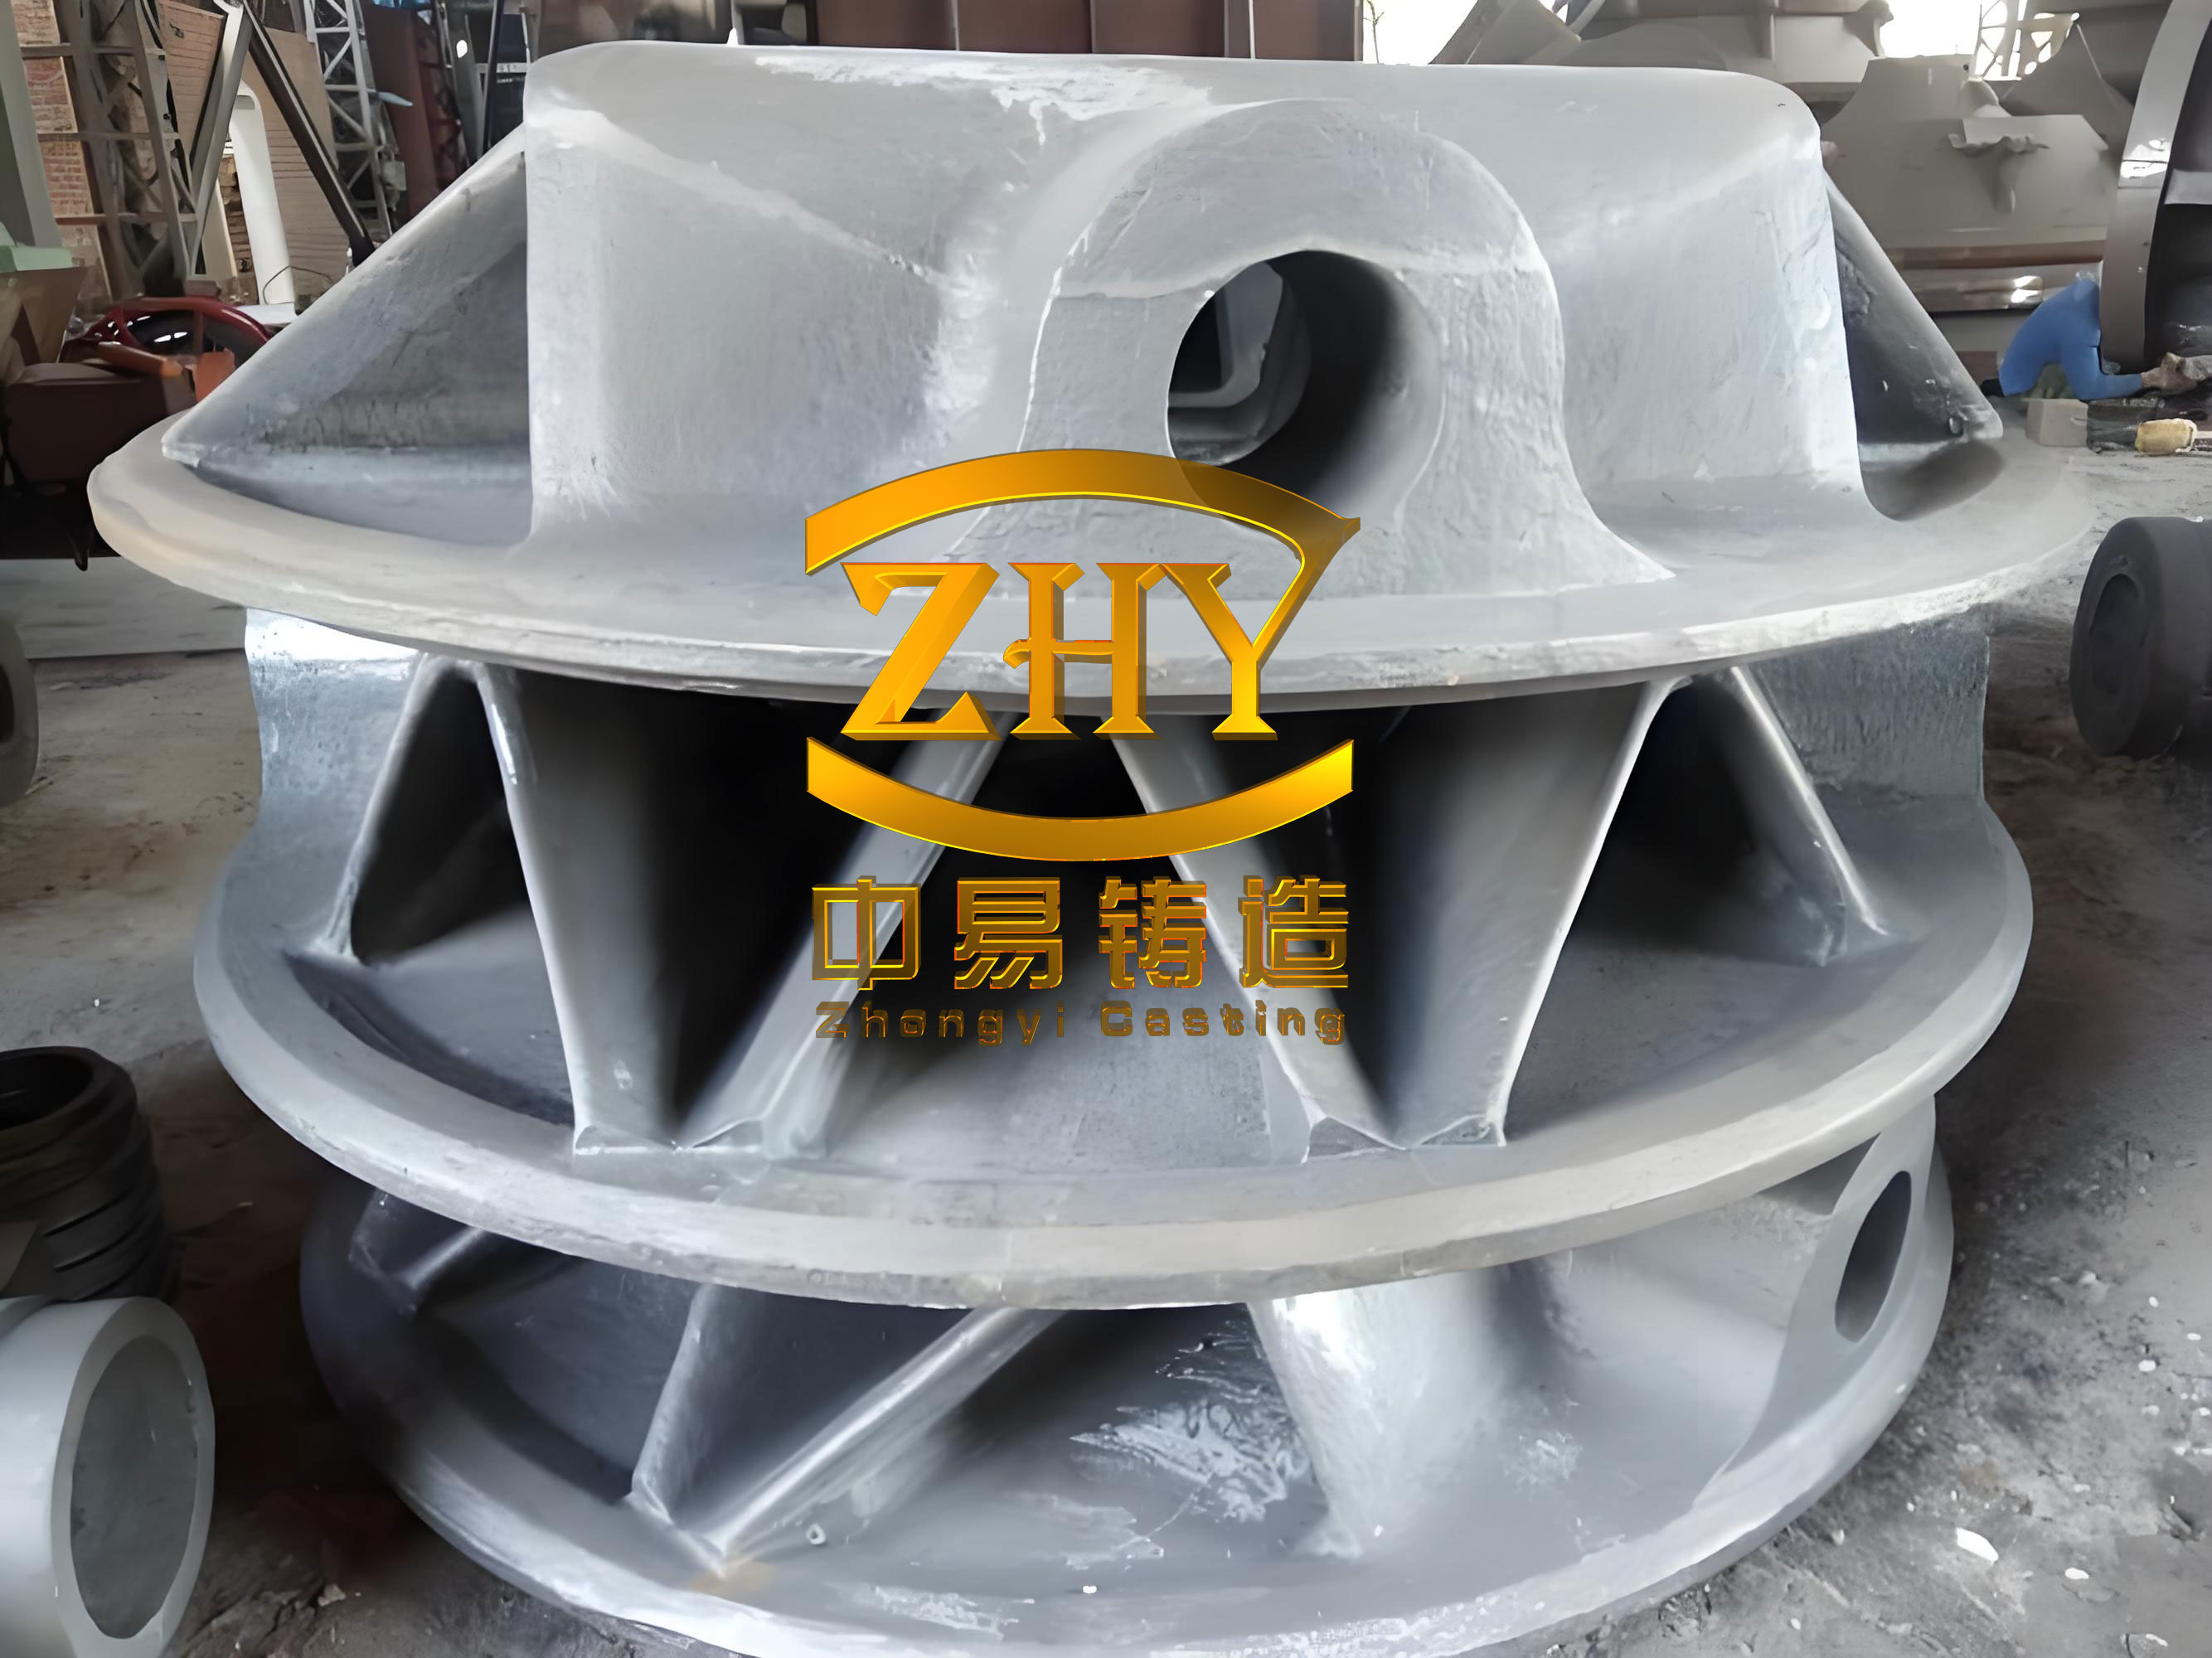
Base material behavior and quality targets. In my experience, HT150 and HT200 gray irons and QT700-2 ductile iron casting behave differently enough that they must be controlled with separate windows. Gray iron contains flake graphite, which gives excellent damping, thermal conductivity, machinability, and low shrinkage, but it also creates stress concentration at graphite flake tips. HT200 is stronger and harder than HT150, so I use it for large bases, housings, machine frames, and load-bearing structural parts. In ductile iron casting, the graphite is spheroidal, so the matrix continuity is much better; tensile strength, elongation, fatigue resistance, and wear resistance increase sharply. QT700-2 requires a predominantly pearlitic matrix, usually with pearlite above 80%, because ferrite lowers strength and hardness. The quality target is therefore not only a tensile test value. I also specify graphite shape, nodule count, nodularity, carbide content, porosity class, and matrix phase fractions.
| Material | Graphite form | Primary advantage | Primary risk in heavy sections | Typical large-part use |
|---|---|---|---|---|
| HT150 gray iron | Flake | Damping, low shrinkage, easy machining | Low strength, coarse flakes, gas porosity | Large covers, non-critical bases |
| HT200 gray iron | Flake | Higher strength and hardness than HT150 | Section sensitivity, pearlite banding, shrinkage | Machine frames, housings, beds |
| QT700-2 ductile iron casting | Spheroidal | High tensile strength, toughness, wear resistance | Shrinkage, nodule degeneration, ferrite formation | Heavy-duty supports, gears, housings |
To describe the chemical condition of the iron, I use the carbon equivalent as a first screening number. For gray iron, a common form is:
$$CE = C + \frac{Si + P}{3}$$
For ductile iron casting, I often use a modified expression because silicon and phosphorus affect graphite expansion and shrinkage differently:
$$CE_{ductile} = C + \frac{Si}{3} + \frac{P}{3}$$
The matrix requirement is measured directly by area fraction. For a target of pearlite above 80%, I use:
$$P_{pearlite} = \frac{A_p}{A_p + A_f + A_c} \times 100\%$$
where \(A_p\) is pearlite area, \(A_f\) is ferrite area, and \(A_c\) is carbide or other carbon-rich phase area. In ductile iron casting, nodularity and nodule count are equally important. I express nodularity as:
$$Nodularity = \frac{N_{VI} + N_{V}}{N_{total}} \times 100\%$$
where \(N_{VI}\) and \(N_{V}\) are nodule counts in the highest shape classes. Nodule count per unit area is:
$$N_A = \frac{N_n}{A}$$
High nodule count refines the matrix and reduces segregation, but excessive magnesium or rare earth can increase shrinkage and dross. I therefore treat graphite shape and matrix fraction as linked targets, not separate inspection items.
| Quality item | HT150 target | HT200 target | QT700-2 ductile iron casting target |
|---|---|---|---|
| Tensile strength | ≥150 MPa | ≥200 MPa | ≥700 MPa |
| Elongation | Low, not primary | Low, not primary | ≥2% |
| Matrix | Pearlite + ferrite, controlled | Pearlite above 70-80% | Pearlite above 80% |
| Graphite | Flake, uniform, no coarse clusters | Flake, uniform, medium size | Spheroidal, nodularity high |
| Porosity | No open gas holes or shrinkage networks | No critical internal shrinkage | No shrinkage cavity in load path |
| Hardness | Consistent with machinability | Stable for wear and support | Uniform through heavy sections |
How defects form in heavy sections. In my defect analysis, gas porosity, shrinkage, and low strength are not independent. A gas hole changes local cooling, a shrinkage cavity changes stress distribution, and a ferrite band changes the local matrix. The root causes often overlap in charge quality, melting, treatment, molding, and pouring. For that reason, I classify defects by mechanism before I adjust a process parameter. Gas porosity is usually divided into invasive gas, evolved gas, and reaction gas. Invasive gas comes from mold and core gas that enters the metal before a skin forms. Evolved gas comes from hydrogen, nitrogen, and oxygen that were dissolved in the liquid iron and are rejected during solidification. Reaction gas comes from chemical reactions among liquid iron, sand, coatings, and slag. In large ductile iron casting, the long filling time and large mold cavity give gas more time and space to collect.
| Gas defect type | Main source | Typical location | Primary control |
|---|---|---|---|
| Invasive gas | Moisture and binder gas from sand or core | Top surface, core interface, blind pockets | Dry sand, low moisture, venting |
| Evolved gas | Hydrogen, nitrogen, oxygen dissolved in iron | Hot spots, thick sections, last freezing zones | Clean charge, degassing, controlled melting |
| Reaction gas | Iron-sand, iron-coating, slag reactions | Gate area, sand-metal interface | Coating control, slag removal, balanced chemistry |
The solubility of gases in liquid iron follows a square-root relation with partial pressure. I use a general form for hydrogen and nitrogen:
$$S_g = K_s \sqrt{p_g}$$
For hydrogen specifically:
$$[H] = K_H \sqrt{p_{H_2}}$$
This means that reducing the partial pressure of hydrogen in the melt environment and reducing moisture in the charge are powerful controls. I also use the Chvorinov relation to estimate solidification time and hot-spot behavior:
$$t_s = B \left(\frac{V}{A}\right)^n$$
The modulus is:
$$M = \frac{V}{A}$$
Where \(M\) is the casting modulus, \(V\) is volume, and \(A\) is heat-transfer surface area. A large modulus means slow cooling, long local solidification time, and a high risk of shrinkage and coarse graphite. For ductile iron casting, slow cooling also increases the chance of ferrite formation and nodule degeneration. Shrinkage is driven by volume change during liquid cooling, solidification, and solid-state cooling. The total volume change can be expressed as:
$$\Delta V = \alpha_V V \Delta T$$
Feeding design must compensate the liquid and solidification contraction before the feeding path closes. I use the riser modulus rule as a starting point:
$$M_r \ge 1.2 M_c$$
For ductile iron casting with an insulating sleeve, I sometimes use:
$$M_r \ge 1.1 M_c$$
The required riser volume is estimated from contraction and feeding efficiency:
$$V_r = \frac{\epsilon V_c}{\eta}$$
where \(\epsilon\) is the volumetric contraction fraction, \(V_c\) is the casting volume, and \(\eta\) is the feeding efficiency.
Raw material control and melt cleanliness. I have learned that no gating or feeding design can fully compensate for a dirty melt. Charge materials must be separated by grade and cleanliness. Rust, oil, grease, paint, moisture, and sand must be kept out of the furnace. Oily scrap decomposes and produces hydrogen and oxidizing gases. Wet ferroalloys and inoculants introduce water vapor directly into the melt. I specify dry storage for silicon, manganese, inoculant, nodulizer, and alloy additions. I also limit the fraction of low-quality returns and ensure that return material is clean and known. Before tapping, I remove slag thoroughly and use a clean ladle. For ductile iron casting, slag and dross control is especially important because magnesium treatment produces reaction products that can become inclusions if they are not removed.
| Input | Rejection or control rule | Reason | My practice |
|---|---|---|---|
| Pig iron | Known chemistry, dry, low rust | Controls carbon, silicon, sulfur, trace elements | Batch verification before charging |
| Steel scrap | No oil, paint, moisture, or mixed alloy | Prevents hydrogen, nitrogen, and tramp elements | Segregate by source |
| Returns | Clean, same family, limited fraction | Avoids composition drift and sand inclusions | Use within validated ratio |
| Ferroalloys | Dry and preheated | Prevents gas from moisture | Preheat before addition |
| Ladle and furnace | Clean lining, no residual slag | Prevents reaction gas and inclusions | Inspect before each heat |
During melting, I control temperature history rather than only final temperature. Long holding at low temperature increases gas absorption. Excessive superheat increases liquid shrinkage and gas solubility. I prefer a controlled melt-up, adequate superheat for treatment and filling, and a stable tapping temperature. For gray iron, I usually target a moderate pouring temperature to reduce shrinkage while maintaining fluidity. For QT700-2 ductile iron casting, I maintain enough temperature for magnesium treatment and inoculation but avoid unnecessary overheating. I also use clean scrap, limited returns, and slag removal to reduce oxygen. Oxygen control is important because oxygen increases slag and reaction gas and lowers mechanical properties.
| Melting parameter | Gray iron HT150/HT200 | QT700-2 ductile iron casting | Reason |
|---|---|---|---|
| Charge cleanliness | High | Very high | Gas and inclusion control |
| Superheat | Controlled, not excessive | Controlled for treatment | Limit gas absorption and shrinkage |
| Holding time | Short as practical | Short before treatment | Prevent gas pickup |
| Slag removal | Thorough | Very thorough | Remove oxides and reaction products |
| Tapping temperature | Stable window | Stable treatment window | Balance fluidity and shrinkage |
Molding sand, core, and venting control. In large castings, the mold and core behave as a gas source as well as a shape. Moisture in green sand, core binder, coating, and repair paste can all generate steam and hydrocarbon gas. I control sand moisture tightly and test it frequently. Permeability must be sufficient for the mold, but too much open porosity can cause metal penetration. I balance moisture, bentonite, carbonaceous additives, and sand grain distribution. For large ductile iron casting, I prefer cores that are fully cured and dry. I avoid excess binder because it increases gas evolution and reduces collapsibility. Venting must be designed, not left to chance. I place vents at high points, blind pockets, core prints, and hot spots. I also increase vent cross-section where gas volume is largest.
| Sand or mold factor | Target direction | Risk if too low | Risk if too high |
|---|---|---|---|
| Moisture | Low and stable | Weak mold, poor surface | Steam gas, blowholes |
| Permeability | Adequate for section | Gas entrapment | Penetration, rough surface |
| Binder content | Minimum for strength | Core collapse, erosion | High gas evolution |
| Venting | Direct and generous | Invasive gas porosity | Mold weakness if poorly placed |
| Coating | Dry, uniform | Burns, metal penetration | Gas from un-dried coating |
I often use a simple gas-risk index for mold-related porosity. If \(m\) is moisture, \(b\) is binder, and \(v\) is venting efficiency, I track a qualitative index:
$$G_{risk} = \frac{m + b}{v}$$
The exact scale is plant-specific, but the meaning is clear: increasing moisture and binder raises gas risk, while increasing venting lowers it. This helps me explain to operators why drying and venting are not secondary tasks.
Gating system optimization to reduce turbulence and gas entrainment. I design gating to fill the mold smoothly, not merely quickly. For large castings, bottom gating and stepped gating reduce free fall and splashing. A high pouring stream can entrain air and oxides. Turbulence can fold the surface film into the metal. I estimate Reynolds number for the gating channel:
$$Re = \frac{\rho v D}{\mu}$$
When \(Re\) is high, flow is more likely to be turbulent. I also calculate gate velocity:
$$v_{gate} = \frac{Q}{A_g}$$
where \(Q\) is volumetric flow rate and \(A_g\) is gate area. I keep the gate velocity within a range that fills the mold without erosion or air entrainment. For ductile iron casting, I pay special attention to the sprue, runner, and ingate because magnesium-treated iron is sensitive to turbulence and oxide film formation. I use a clean, streamlined pouring basin and keep the ladle stream submerged or close to the basin. I avoid interrupted pouring because it can create cold laps, slag entrapment, and gas entrainment.
| Gating feature | My preferred design for large castings | Benefit | Risk to avoid |
|---|---|---|---|
| Pouring basin | Deep, with dam and skim | Traps slag and stabilizes flow | Shallow basin, vortex |
| Sprue | Tapered, streamlined | Reduces air aspiration | Straight rough sprue |
| Runner | Large cross-section, smooth bends | Lower velocity, less turbulence | Sharp corners |
| Ingates | Multiple, balanced, bottom or stepped | Uniform filling, lower superheat loss | Single high-velocity gate |
| Venting | Independent of gating | Removes mold gas | Relying on ingates to vent |
Inoculation practice and its effect on gas and structure. Inoculation controls graphite nucleation and matrix formation. If inoculation is late, weak, or uneven, the iron can form coarse graphite, carbides, and ferrite. In ductile iron casting, inoculation after magnesium treatment is essential to restore nucleation and avoid chill. I use late-stream inoculation or in-mold inoculation to reduce fade. The inoculant must be dry and preheated. Wet inoculant is a direct gas source. If the inoculant is added too early, it can be consumed before it reaches the mold. If the iron is held too long after inoculation, the nucleation effect fades. I model fade qualitatively as:
$$F(t) = F_0 e^{-kt}$$
where \(F_0\) is initial inoculation effect and \(k\) is a fade constant. My target is to fill the mold while \(F(t)\) is still high. For gray iron, inoculation promotes uniform pearlite and controls flake size. For ductile iron casting, it promotes nodule count and reduces carbide. I separate gray iron and ductile iron inoculation strategies because the treatment sequence and magnesium recovery differ.
| Inoculation variable | Gray iron | QT700-2 ductile iron casting | Control objective |
|---|---|---|---|
| Addition stage | Ladle or late stream | Post-magnesium late stream | Minimize fade |
| Inoculant condition | Dry, sized | Dry, preheated | Prevent gas |
| Amount | Based on section and sulfur | Based on treatment and section | Nucleation without excess |
| Holding after addition | Short | Very short | Preserve nuclei |
| Result | Uniform flake and pearlite | Nodularity and pearlite above 80% | Strength and shrinkage balance |
Chemical composition and shrinkage control. In heavy castings, I use chemistry to influence graphite expansion. Carbon and silicon promote graphite formation. In gray iron, moderate carbon equivalent increases graphite expansion and reduces shrinkage, but too high carbon equivalent can coarsen flakes and lower strength. In ductile iron casting, carbon equivalent must be high enough to promote graphite expansion but controlled to avoid graphite flotation and degenerated nodules. Sulfur must be low in ductile iron casting because sulfur consumes magnesium. Phosphorus should be low because it forms low-melting phases and increases hot tearing and shrinkage porosity. Manganese and trace alloys must be balanced. I use the following table as a practical starting point; final values depend on section size, charge, treatment, and molding method.
| Element | HT150 range | HT200 range | QT700-2 ductile iron casting range | Role |
|---|---|---|---|---|
| C | 3.20-3.60% | 3.10-3.50% | 3.40-3.80% | Graphite formation, expansion |
| Si | 1.80-2.40% | 1.70-2.30% | 2.00-2.80% | Graphitization, ferrite control |
| Mn | 0.50-0.90% | 0.60-1.00% | 0.20-0.60% | Pearlite stabilization, sulfur control |
| P | ≤0.15% | ≤0.12% | ≤0.05% | Low-melting phase risk |
| S | ≤0.12% | ≤0.10% | ≤0.02% | Nodularization and shrinkage |
| Mg | Not applicable | Not applicable | 0.03-0.06% | Nodularization |
| Cu | 0-0.30% | 0-0.50% | 0.30-0.80% | Pearlite promotion |
| Sn | 0-0.03% | 0-0.05% | 0.01-0.04% | Pearlite promotion, careful control |
I calculate carbon equivalent before tapping and adjust with charge makeup. A simple control target for ductile iron casting is to keep carbon equivalent in a narrow band around the eutectic so that graphite expansion compensates liquid and solidification contraction. If the carbon equivalent is too low, shrinkage porosity rises. If it is too high, graphite flotation and nodule degeneration can occur in very thick sections. I therefore combine carbon equivalent with section modulus. A thick section needs more graphite expansion but also more feeding, not less.
Solidification sequence, risers, and chills. I do not allow a large casting to solidify randomly. I identify the last freezing zones using modulus and simulation. I place risers where the casting will freeze last. I place chills where I need faster cooling and directional solidification. The goal is a sequence from thin sections toward the riser, so that the riser remains liquid and feeds contraction. In ductile iron casting, the graphite expansion can reduce feeding demand if the mold is rigid and the expansion is used correctly. However, if the mold expands, the graphite expansion is wasted and shrinkage still appears. Therefore, mold rigidity is part of feeding design. I use strong flasks, compacted sand, and adequate clamping. I also use insulating sleeves and exothermic sleeves where the riser must stay liquid longer.
| Feature | Design purpose | Typical rule | My practice |
|---|---|---|---|
| Riser location | Feed last freezing zone | At hot spot or highest modulus | Confirm by simulation and sectioning |
| Riser modulus | Stay liquid after casting | \(M_r \ge 1.2 M_c\) | Use sleeve to reduce size |
| Riser neck | Transmit liquid feed | Short and not prematurely frozen | Increase neck modulus |
| Chill | Promote directional freezing | Place near thin-thick transition | Balance against hot tearing |
| Mold rigidity | Use graphite expansion | High compactness and clamping | Monitor flask and core support |
The feeding distance of a riser depends on the modulus and the alloy. I use a simplified form:
$$L_f = k M$$
where \(L_f\) is feeding distance and \(k\) is an alloy and process factor. For ductile iron casting, \(k\) is often lower than for gray iron because the feeding path can close earlier. For long castings, I use multiple risers or segmented feeding. I also check the riser neck with modulus difference:
$$M_n \ge b M_c$$
where \(M_n\) is neck modulus and \(b\) is a factor close to 0.8-1.0 depending on alloy and sleeve. If the neck freezes before the casting, the riser is isolated and cannot feed.
Pouring temperature and pouring speed. I control pouring temperature and speed as a pair. High temperature increases liquid shrinkage, gas solubility, and mold reaction, but it improves fluidity for thin sections. Low temperature reduces shrinkage but can cause cold shuts, misruns, and poor feeding because viscosity rises. For large gray iron, I prefer a moderate temperature. For ductile iron casting, I maintain a slightly higher temperature to compensate for magnesium treatment and inoculation, but I still avoid excessive superheat. Pouring speed must be steady. A fast pour can erode molds and create turbulence. A slow pour can cause cold laps and temperature loss. I keep the pouring basin full and the stream continuous. I record temperature and time for every large heat.
| Process parameter | Gray iron HT150/HT200 | QT700-2 ductile iron casting | Reason |
|---|---|---|---|
| Pouring temperature | Moderate, section-dependent | Controlled treatment window | Balance fluidity and shrinkage |
| Pouring speed | Steady, moderate | Steady, not turbulent | Avoid cold shut and gas entrainment |
| Pouring continuity | Continuous | Continuous | Prevent slag and gas entrapment |
| Basin level | Full | Full | Prevent vortex |
| Record | Temperature and time | Temperature, time, Mg recovery | Traceability |
Modulus calculation and feeding system improvement. I use modulus calculation to convert a complex casting into hot-spot regions. The modulus \(M=V/A\) is calculated for each section. I then compare casting modulus with riser modulus and chill effect. The Chvorinov equation gives solidification time:
$$t_s = B M^n$$
For many casting conditions, \(n\) is close to 2. Therefore, a section with twice the modulus can take about four times longer to solidify. That is why a thick flange or boss can remain liquid long after a thin wall has frozen. I use this to set riser size and chill placement. For a large casting, I may use a combination of top risers, side risers, and neck-down risers. For ductile iron casting, I often use an insulating sleeve to increase the effective modulus without increasing riser diameter. I also use chill blocks at transition zones to reduce the effective modulus difference. The feeding system is not designed by rule of thumb alone; I verify with simulation, trial cut, ultrasonic testing, and sectioning.
| Hot spot type | Risk | Feeding or cooling method | Verification |
|---|---|---|---|
| Thick flange | Centerline shrinkage | Side riser with sleeve | UT and sectioning |
| Boss on thin wall | Isolated hot spot | Chill and local riser | Thermal analysis |
| Intersection of ribs | Hot tearing and porosity | Rounded fillets, chill | Dye penetrant and UT |
| Long thick bar | Feeding distance too long | Multiple risers or segmented feed | Simulation and X-ray |
| Heavy base | Slow cooling, coarse graphite | Chills and alloy control | Microstructure audit |
Special controls for ductile iron casting shrinkage. In my experience, ductile iron casting has a wider shrinkage risk than gray iron because magnesium treatment changes the solidification path. The graphite expansion can be beneficial, but only if the mold is rigid and the carbon equivalent is in the correct range. I control magnesium addition carefully. Too little magnesium gives poor nodularity. Too much magnesium increases dross, shrinkage, and gas. I control rare earth addition because it affects nodularity and carbide. I keep sulfur low before treatment and control the treatment temperature. After treatment, I minimize holding time because magnesium fades and nodules can degenerate. I use late inoculation to restore nucleation. For heavy sections, I use a combination of riser, chill, and insulating sleeve. I also check the pouring temperature because a high temperature increases liquid contraction. In ductile iron casting, the combination of high carbon equivalent, strong mold, good nodularity, and correct feeding is the most reliable path to soundness.
| Ductile iron casting issue | Root cause | My control action | Measured result |
|---|---|---|---|
| Shrinkage cavity | Insufficient feed or low CE | Increase CE within window, add riser | Reduced UT indications |
| Dispersed porosity | Long freezing, poor nucleation | Late inoculation, chill control | Higher nodule count |
| Graphite flotation | Excess CE in very thick section | Reduce C, control Si | Uniform nodule distribution |
| Dross inclusion | High Mg or turbulent filling | Optimize Mg, gating, slag removal | Lower inclusion rating |
| Ferrite band | Slow cooling or low alloy | Cu/Sn addition, chill | Pearlite above 80% |
Strength improvement and pearlite control above 80%. Strength in large iron castings is not improved by a single expensive alloy. I build it through clean melting, correct chemistry, controlled cooling, and matrix stabilization. In gray iron, strength depends on flake size, flake distribution, and pearlite fraction. In ductile iron casting, strength depends on nodularity, nodule count, matrix, and freedom from defects. QT700-2 requires a pearlitic matrix. Ferrite is soft and lowers tensile strength. Carbide is hard but brittle and harms machinability. I target a matrix that is predominantly pearlite with controlled carbide. The pearlite fraction can be modeled qualitatively by a transformation rate:
$$\frac{dP}{dt} = K (1-P)$$
where \(P\) is pearlite fraction and \(K\) depends on cooling rate and alloy. Faster cooling raises \(K\). Alloying elements such as copper, tin, manganese, and chromium also raise \(K\). However, excessive alloying can increase segregation and shrinkage. I prefer a balanced approach: controlled cooling, moderate copper, very small tin, manganese within limits, and inoculation to avoid chill. For heavy sections, cooling rate is low, so alloying and chills become more important.
| Strength factor | Effect on gray iron | Effect on QT700-2 ductile iron casting | My control |
|---|---|---|---|
| Graphite shape | Flake size and distribution | Nodularity and nodule count | Inoculation, Mg treatment |
| Matrix | Pearlite raises strength | Pearlite above 80% | Alloy and cooling control |
| Cooling rate | Faster cooling refines flakes | Faster cooling refines nodules | Chills and section design |
| Inclusions | Lower strength and machinability | Initiates cracks | Clean melt and filters |
| Porosity | Stress concentration | Reduces fatigue and tensile strength | Gas and shrinkage control |
I use hardness as a rapid indicator of matrix state. For gray iron, tensile strength often correlates with hardness:
$$UTS = a HB + b$$
where \(a\) and \(b\) are empirical constants for the specific iron and section. For ductile iron casting, hardness alone is not enough because nodularity and porosity also affect strength. I therefore combine hardness with microstructure and ultrasonic inspection. When pearlite is below 80%, I check cooling rate, copper and tin content, inoculation, and section thickness. When carbide is too high, I check silicon, inoculation, and cooling. The process window must be wide enough for production but narrow enough for consistency.
| Alloy element | Main effect | Typical addition in QT700-2 ductile iron casting | Risk of excess |
|---|---|---|---|
| Cu | Promotes pearlite, improves strength | 0.30-0.80% | Segregation, reduced ductility |
| Sn | Strong pearlite promoter | 0.01-0.04% | Brittleness, hot tearing |
| Mn | Pearlite stabilizer, sulfur control | 0.20-0.60% | Carbide, segregation |
| Cr | Carbide former, wear resistance | Usually low or avoided | Chill and poor machining |
| Mo | Hardenability | Selected heavy sections | Cost and carbide |
| Ni | Toughness and hardenability | Selected grades | Cost and matrix balance |
Heat treatment and final property adjustment. When as-cast properties cannot meet QT700-2 requirements, I use heat treatment. Normalizing can raise pearlite and strength. Quenching and tempering can produce a tempered martensitic matrix, but it requires careful control to avoid cracking in large castings. For large ductile iron casting, uniform heating and cooling are difficult, so I use gradual heating, controlled austenitizing, and uniform cooling. I also consider stress relief when the casting has complex geometry. For gray iron, stress relief is often more important than phase change because it reduces residual stress and improves dimensional stability. I verify heat treatment with hardness traverses and microstructure samples from critical sections.
| Heat treatment | Purpose | Typical application | Risk |
|---|---|---|---|
| Stress relief | Reduce residual stress | Large gray iron and ductile iron casting | Distortion if heating is uneven |
| Normalizing | Increase pearlite, refine matrix | QT700-2 ductile iron casting | Residual stress, cracking |
| Quenching and tempering | High strength with toughness | Selected heavy-duty parts | Quench cracking, distortion |
| Austempering | Ausferrite matrix | Special ductile iron casting grades | Process control cost |
| Annealing | Improve machinability | Gray iron and ductile iron | Lower strength if over-annealed |
Process capability, inspection, and continuous improvement. I do not rely on final inspection alone. I use process capability indices to judge whether the process is stable. For a critical dimension or property:
$$C_p = \frac{USL – LSL}{6\sigma}$$
$$C_{pk} = \min\left(\frac{USL-\mu}{3\sigma}, \frac{\mu-LSL}{3\sigma}\right)$$
I want \(C_p\) and \(C_{pk}\) above 1.33 for critical characteristics. For tensile strength, pearlite fraction, nodularity, and porosity class, I track the same logic even when the data are attribute-based. I use control charts for carbon equivalent, pouring temperature, inoculation amount, magnesium recovery, sand moisture, and mold hardness. I also use ultrasound and sectioning for shrinkage, and microstructure audits for pearlite above 80%. When a defect appears, I trace it back to the process step and verify the cause with a designed trial. This is how I prevent the same gas porosity, shrinkage, or ferrite band from returning.
| Inspection item | Method | Frequency for large castings | Decision rule |
|---|---|---|---|
| Chemical composition | Spectrometer | Every heat | Within specified window |
| Carbon equivalent | Calculation | Every heat | Target band by section |
| Pouring temperature | Thermocouple | Every pour | Within validated range |
| Microstructure | Metallography | Per batch and critical section | Pearlite above 80% for QT700-2 |
| Nodularity | Image analysis | Ductile iron casting batch | Above specification |
| Porosity and shrinkage | UT, X-ray, sectioning | Critical zones | No rejectable indication |
| Hardness | Brinell | Representative locations | Uniform and within range |
| Sand moisture | Moisture tester | Every shift | Low and stable |
In my own production philosophy, the most important step is to connect the defect mechanism to the process variable. Gas porosity is not solved by a single vent; it is solved by dry charge, clean melt, controlled gas content, dry molds, good venting, and smooth gating. Shrinkage is not solved by a larger riser alone; it is solved by correct carbon equivalent, directional solidification, rigid molds, proper modulus calculation, and controlled pouring. Low strength is not solved by adding alloy blindly; it is solved by graphite control, matrix control, inoculation, cooling rate, and cleanliness. For ductile iron casting, all of these factors interact because magnesium treatment, graphite expansion, and shrinkage occur together.
I also use a defect severity index for internal review. If \(V_s\) is the volume of shrinkage indications and \(V_c\) is the casting volume, then:
$$SDI = \frac{V_s}{V_c} \times 100\%$$
For gas porosity, I use an area or volume fraction from radiography or sectioning. For microstructure, I use pearlite fraction, nodularity, and nodule count. These numbers allow me to compare heats, patterns, and process changes. I do not judge a change by a single casting; I judge it by the mean, standard deviation, and capability index. This is especially important in large castings because the cost of a failed trial is high.
| Defect | Primary process lever | Secondary lever | Verification metric |
|---|---|---|---|
| Invasive gas | Sand moisture and venting | Core drying and coating | Blowhole area fraction |
| Evolved gas | Charge cleanliness and melting | Degassing and temperature | Hydrogen and nitrogen content |
| Reaction gas | Slag removal and coating control | Gating and chemistry | Surface and subsurface porosity |
| Shrinkage cavity | Riser and chill design | Carbon equivalent and pouring | UT indication size |
| Dispersed porosity | Solidification rate and inoculation | Alloy and mold rigidity | Density and sectioning |
| Low strength | Pearlite fraction and nodularity | Inclusions and porosity | Tensile and hardness |
My integrated control window for large gray iron and ductile iron casting. I summarize the production window in one place so that operators and engineers use the same language. The window is not a substitute for judgment, but it prevents drift. For HT150 and HT200, I keep carbon equivalent in a range that gives graphite expansion without coarse flakes. I use moderate pouring temperature, clean sand, adequate venting, and a gating system that fills smoothly. For QT700-2 ductile iron casting, I keep sulfur low, control magnesium and rare earth, use late inoculation, maintain a rigid mold, and design feeding from modulus calculation. I target pearlite above 80% by balancing cooling rate, copper, tin, and section size. I verify with microstructure and mechanical testing.
| Control area | Gray iron HT150/HT200 | QT700-2 ductile iron casting | Common rule |
|---|---|---|---|
| Charge | Clean, sorted, dry | Very clean, low sulfur | No oil, rust, moisture |
| Melting | Stable superheat | Stable treatment temperature | Avoid long low-temperature holding |
| Treatment | Inoculation | Mg treatment plus inoculation | Control fade and reaction |
| Mold | Dry sand, good venting | Rigid mold, dry core, venting | Gas and expansion control |
| Gating | Smooth, low turbulence | Smooth, low turbulence | Prevent air entrainment |
| Feeding | Riser and chill as needed | Modulus-based riser and chill | Directional solidification |
| Matrix | Pearlite control | Pearlite above 80% | Cooling rate and alloy balance |
| Inspection | Hardness and microstructure | UT, nodularity, tensile | Data-driven release |
I have seen that the most successful large-casting processes are not the ones with the most complex equipment. They are the ones with disciplined adherence to a defined window. The charge must be clean. The melt must be treated correctly. The mold must be dry and vented. The gating must be smooth. The feeding must be calculated. The cooling must be controlled. The microstructure must be verified. When these conditions are met, gas porosity falls, shrinkage is reduced, strength becomes stable, and pearlite above 80% becomes a normal result rather than an occasional achievement. In ductile iron casting, this discipline is even more important because the alloy has less tolerance for variation.
For future work, I continue to use simulation for filling and solidification, but I always calibrate simulation with real sectioning and ultrasonic results. I use thermal analysis to check inoculation and magnesium treatment. I use statistical process control to detect drift before defects appear. I use table-based process windows and formula-based checks to train operators and engineers. My goal is not only to produce a conforming large casting, but to produce it repeatedly with low scrap, stable mechanical properties, and predictable microstructure. This is how I approach large gray iron and ductile iron casting production, and it is the method I trust for heavy-section components that must perform safely under load.