
Steel castings play a critical role in heavy-duty industrial applications, particularly in the manufacturing of axle housings for off-highway mining vehicles. The production of large steel castings with complex geometry such as the cast steel axle housing presents significant challenges due to the high risk of shrinkage cavities, porosity, hot tearing, and sand inclusion defects during the solidification process. Traditional trial-and-error approaches in foundry practice are often time-consuming and costly, making them unsuitable for the fast-paced product development cycles of modern manufacturing. The emergence of computer-aided engineering (CAE) techniques, especially numerical simulation software for casting processes, has opened new avenues for foundry engineers to investigate and optimize casting designs before physical trials are conducted.
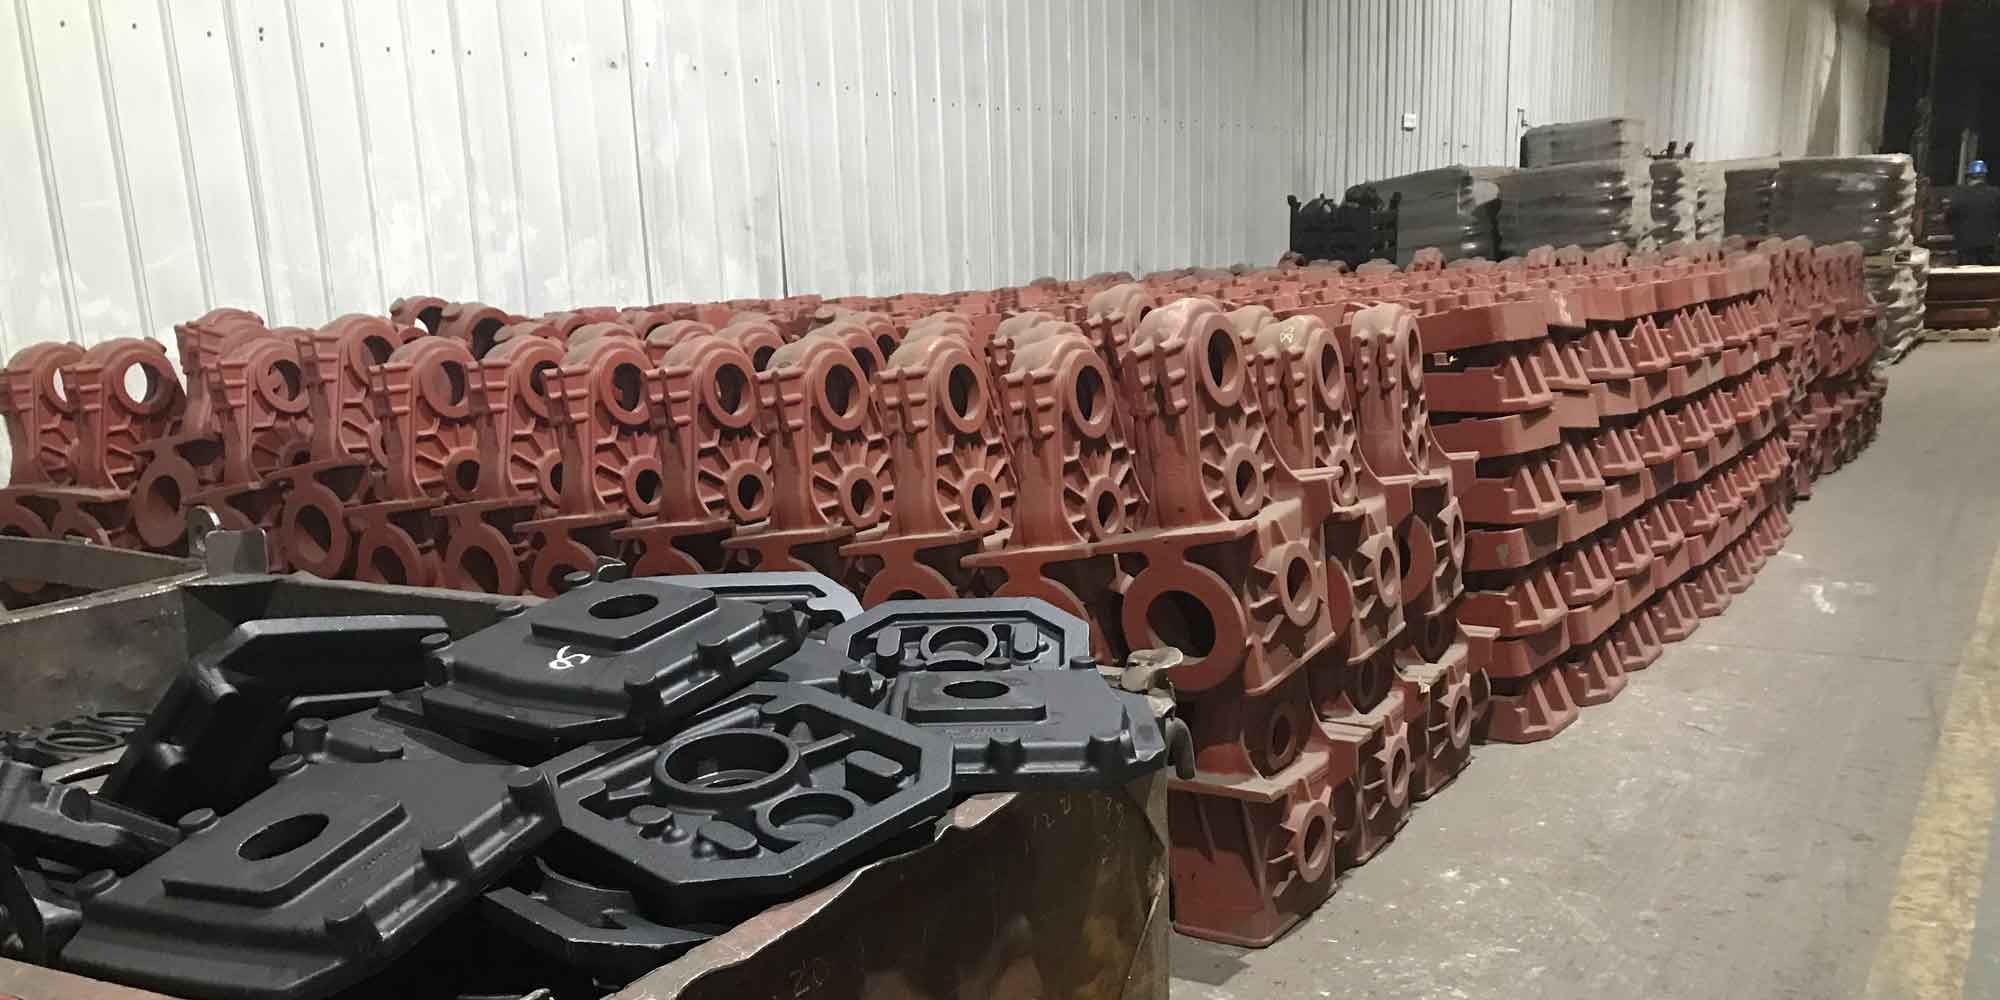
In this research, the focus is placed on a 70-tonne mining dump truck manufactured by a company that requires a highly robust axle housing to endure extreme loads and impact forces. The axle housing under investigation has an overall dimension of approximately 2116 mm × 596 mm × 364 mm, with a total weight of about 553 kg and a nominal wall thickness ranging from 15 mm to as thick as 87 mm. The material designated for this component is SCW550, a low-alloy cast steel widely used for structural parts requiring high strength and toughness. The geometrical complexity of the axle housing, including flanges, spring seats, and an intermediate differential housing section, makes it extremely difficult to achieve sound castings without sophisticated process design. The initial casting process was designed using conventional gating and risering principles, but the outcome was not satisfactory due to prevalent shrinkage defects.
The primary objective of this work is to apply numerical simulation to optimize the casting process of steel castings, specifically the axle housing, and to establish a comprehensive predicting method for shrinkage cavity and porosity. By integrating the three-dimensional CAD software CATIA with the finite element based casting simulation package ProCAST, a digital twin of the casting process was established. This numerical framework allows for the prediction of filling behavior, solidification sequences, temperature distributions, and defect formation mechanisms. Through iterative modifications to the gating system, riser configuration, and core sand materials, an optimized casting process was achieved and subsequently validated by full-scale production trials.
Introduction
The cast steel axle housing is one of the most safety-critical components in heavy mining trucks. It serves as the structural backbone connecting the suspension system, drivetrain, and wheels. During vehicle operation, the axle housing is subjected to repeated dynamic loads, impact forces, and torque fluctuations. Therefore, any internal defects such as shrinkage cavities, porosity, or hot tearing can lead to premature failure and catastrophic results. The foundry industry recognizes that the production of large steel castings is inherently challenging due to the wide solidification temperature range and the high volumetric shrinkage of steel. Without proper riser design and thermal control, shrinkage defects are inevitable.
Traditional casting process design relied heavily on empirical rules, published charts, and the personal experience of foundry engineers. While these approaches provided a reasonable starting point, they often failed to account for the complex interactions between heat transfer, fluid flow, and solidification in intricate geometries. As a result, the initial casting design often produced defective castings that required multiple trial iterations to rectify. This trial-and-error process not only extended the product development timeline but also incurred significant material and energy costs.
The advent of numerical simulation technology has fundamentally transformed the casting industry. By solving the governing equations of fluid dynamics and heat transfer over the entire computational domain, simulation software such as ProCAST can provide detailed insights into the casting process. The technology enables foundry engineers to visualize the filling sequence, identify potential air entrapment, evaluate solidification patterns, and predict the formation of shrinkage defects with remarkable accuracy. The application of such tools in the development of steel castings has become a standard practice in modern foundries.
Literature Review of Casting Simulation and Process Optimization
The numerical simulation of casting processes has evolved significantly since the 1960s. Initially, simulation efforts were limited to simple solidification analysis using analytical methods. With the rapid advancement of computational hardware and numerical algorithms, modern simulation tools are capable of handling complex three-dimensional geometries, non-linear material properties, and multi-physics phenomena. The finite difference method (FDM) and the finite element method (FEM) are the two most prominent numerical techniques used in casting simulation. FDM is widely used in the analysis of flow and heat transfer, while FEM offers better accuracy for stress and deformation predictions.
Contemporary casting simulation software packages, including ProCAST, MAGMASOFT, and AnyCasting, provide integrated environments for modeling filling, solidification, microstructure evolution, and residual stress. These tools have been successfully applied to a wide range of casting processes such as sand casting, investment casting, high-pressure die casting, and low-pressure casting. Among these, sand casting remains the most common method for producing large steel castings due to its flexibility and cost-effectiveness. The application of simulation to sand casting of steel components has been particularly fruitful in reducing defects and improving yield.
In parallel with the development of simulation software, researchers have explored various optimization strategies for casting processes. These strategies can be broadly classified into four categories:
| Category | Approach | Advantages | Limitations |
|---|---|---|---|
| Experimental-based | Physical trials, destructive testing | Direct evidence, high fidelity | Time-consuming, high cost |
| Modern optimization algorithms | Neural networks, genetic algorithms, Taguchi methods | Global search capability, systematic | Need training data, computationally heavy |
| Empirical formulas and theoretical derivation | Chvorinov rule, modulus method, feeding distance formulas | Rapid estimation, simple to use | Limited accuracy for complex shapes |
| Simulation-based optimization | Virtual prototyping, sensitivity analysis | Detailed insight, cost-effective | Requires accurate material data and models |
The simulation-based optimization approach is particularly appealing because it allows for a thorough exploration of the design space without the expense of physical prototyping. By varying parameters such as pouring temperature, gating system geometry, riser size, and mold materials, the designer can systematically evaluate the impact of each factor on the final casting quality. In the context of steel castings, simulation has been widely used to predict and eliminate shrinkage porosity, hot tears, and inclusions.
Prior research has demonstrated the value of numerical simulation in optimizing various cast components. For instance, several investigators have applied simulation to automotive axle housings to reduce shrinkage defects by optimizing riser placement and feeding aids. Others have focused on the influence of core sand materials on the solidification process. It has been observed that the thermophysical properties of the mold and core materials significantly affect the cooling rate and hence the soundness of the casting. Thus, selecting an appropriate core material is a critical aspect of casting process design.
Theoretical Foundation of Casting Simulation and Defect Prediction
The numerical simulation of the casting filling process is based on the principles of fluid mechanics and heat transfer. The governing equations are the continuity equation, the Navier-Stokes equations, and the energy equation. For an incompressible Newtonian fluid, the continuity equation is expressed as follows:
$$ \frac{\partial u}{\partial x} + \frac{\partial v}{\partial y} + \frac{\partial w}{\partial z} = 0 \tag{1} $$
where u, v, w represent the velocity components in the x, y, z directions, respectively. The momentum equations, known as the Navier-Stokes equations, describe the conservation of momentum and are given by:
$$ \rho \left( \frac{\partial u}{\partial t} + u \frac{\partial u}{\partial x} + v \frac{\partial u}{\partial y} + w \frac{\partial u}{\partial z} \right) = -\frac{\partial P}{\partial x} + \rho g_x + \mu \nabla^2 u \tag{2} $$
$$ \rho \left( \frac{\partial v}{\partial t} + u \frac{\partial v}{\partial x} + v \frac{\partial v}{\partial y} + w \frac{\partial v}{\partial z} \right) = -\frac{\partial P}{\partial y} + \rho g_y + \mu \nabla^2 v \tag{3} $$
$$ \rho \left( \frac{\partial w}{\partial t} + u \frac{\partial w}{\partial x} + v \frac{\partial w}{\partial y} + w \frac{\partial w}{\partial z} \right) = -\frac{\partial P}{\partial z} + \rho g_z + \mu \nabla^2 w \tag{4} $$
where ρ is the density of the molten metal, P is the pressure, g is the gravitational acceleration, and μ is the dynamic viscosity. In the context of the casting filling process, the flow is typically turbulent due to the complex geometry of the gating system and the high flow velocities involved. To model turbulent flow accurately, the k-ε two-equation turbulence model is commonly employed. The turbulent kinetic energy k and its dissipation rate ε are governed by the following transport equations:
$$ \frac{\partial}{\partial t} (\rho k) + \frac{\partial}{\partial x_j} (\rho u_j k) = \frac{\partial}{\partial x_j} \left[ \left( \mu + \frac{\mu_t}{\sigma_k} \right) \frac{\partial k}{\partial x_j} \right] + P_k – \rho \varepsilon \tag{5} $$
$$ \frac{\partial}{\partial t} (\rho \varepsilon) + \frac{\partial}{\partial x_j} (\rho u_j \varepsilon) = \frac{\partial}{\partial x_j} \left[ \left( \mu + \frac{\mu_t}{\sigma_\varepsilon} \right) \frac{\partial \varepsilon}{\partial x_j} \right] + \frac{\varepsilon}{k} (C_1 P_k – C_2 \rho \varepsilon) \tag{6} $$
The turbulent eddy viscosity is then computed from k and ε:
$$ \mu_t = C_\mu \rho \frac{k^2}{\varepsilon} \tag{7} $$
The constants used in the k-ε model are presented in the following table:
| C₁ | C₂ | Cμ | σk | σε |
|---|---|---|---|---|
| 1.44 | 1.92 | 0.09 | 1.0 | 1.33 |
In addition to the flow field, the energy equation governs the heat transfer during the filling and solidification processes. The energy conservation equation is expressed in terms of temperature T:
$$ \rho c_p \left( \frac{\partial T}{\partial t} + u \frac{\partial T}{\partial x} + v \frac{\partial T}{\partial y} + w \frac{\partial T}{\partial z} \right) = \frac{\partial}{\partial x} \left( k \frac{\partial T}{\partial x} \right) + \frac{\partial}{\partial y} \left( k \frac{\partial T}{\partial y} \right) + \frac{\partial}{\partial z} \left( k \frac{\partial T}{\partial z} \right) + Q \tag{8} $$
where cp is the specific heat capacity, k is the thermal conductivity, and Q represents the internal heat source, which accounts for the latent heat of solidification. During the solidification process, the latent heat L is released over the solidification temperature range between liquidus T_L and solidus T_S. The fraction of solid f_s at any temperature T follows the lever rule or the Scheil equation, which can be simplified to:
$$ f_s = \sqrt{\frac{T_L – T}{T_L – T_S}} \tag{9} $$
In the context of numerical simulation of steel castings, accurate modeling of the solidification behavior is essential for the reliable prediction of shrinkage defects.
Mechanism and Prediction of Shrinkage Cavity and Porosity in Steel Castings
The formation of shrinkage cavity and porosity in steel castings is a direct consequence of the volumetric contraction that occurs during the cooling and solidification of the molten metal. When molten steel solidifies, it undergoes three distinct stages of contraction: liquid contraction, solidification contraction, and solid contraction. If the contraction is not compensated by additional molten metal from a riser, porosity will form in the last solidifying regions of the casting. The phenomenon can be described by considering a simple solidification model: the molten metal first fills the mold cavity, and after a thin solid skin forms on the mold surface, the interior remains liquid. As cooling continues, the liquid level drops due to volumetric contraction, while the solid shell grows inward. If the riser freezes before the casting, the remaining liquid inside the casting becomes isolated and cannot be fed, resulting in a shrinkage cavity at the final solidification point.
While macro-shrinkage appears as a large, concentrated cavity, micro-shrinkage porosity is characterized by numerous small, dispersed voids located between dendrite arms. These micro-porosities are particularly harmful to the mechanical properties and pressure tightness of steel castings. The prediction of porosity is significantly more complex because it depends on the feeding capability of the interdendritic channels, which in turn is influenced by the solidification morphology, permeability of the mushy zone, and the local temperature gradient. Various criteria have been developed to predict the occurrence of shrinkage defects, including the temperature gradient criterion, the Niyama criterion, and the feeding resistance criterion. Among these, the Niyama criterion is widely used for steel castings. It relates the temperature gradient G and the cooling rate R to the tendency for micro-shrinkage formation:
$$ \frac{G}{\sqrt{R}} < C_{Niyama} \tag{10} $$
The critical value of G/√R is typically in the range of 0.8 to 1.0 for steel castings. A smaller local value of G/√R indicates a higher risk of micro-porosity formation. The Niyama criterion is readily available in commercial simulation software and was adopted in this study to evaluate the shrinkage propensity in the cast steel axle housing.
Numerical Modeling of the Cast Steel Axle Housing
The first step in the simulation-driven optimization of steel castings is the creation of a robust three-dimensional geometric model. In this investigation, the axle housing was modeled using CATIA software based on the detailed engineering drawing of the component. The component exhibits a hollow, drum-like central section, integral flange housings at both ends, spring seats, and several connection plates. The geometry is dominated by free-form surfaces and varying wall thickness, making the meshing operation complex. The complete model comprises the casting, the gating system, and the virtual sand mold. The key dimensions of the axle housing are summarized in the following table:
| Parameter | Value |
|---|---|
| Overall length | 2128 mm |
| Width | 600 mm |
| Height | 380 mm |
| Weight | 553 kg |
| Minimum wall thickness | 15 mm |
| Maximum wall thickness | 87 mm |
Once the CAD model was completed, it was imported into the ProCAST software environment for mesh generation. The finite element mesh was created using the Visual-Mesh module. First, the geometry was checked for errors such as holes, intersecting surfaces, or duplicate faces. Any defects were corrected using the automatic healing tools within Visual-Mesh. A careful compromise between computational accuracy and time was achieved by using refined mesh in thin sections and coarser mesh in bulky regions. The mesh statistics after discretization are presented below:
| Mesh Type | Number of Elements |
|---|---|
| Surface mesh (2D) | 3,056 |
| Volume mesh (3D) | 12,938 |
The virtual sand box was defined using the Virtual Mold functionality available in ProCAST. This approach obviates the need to explicitly model the sand mold geometry, significantly reducing pre-processing effort. The virtual mold automatically encapsulates the casting and gating system and permits simple adjustments to mold dimensions and boundary conditions. A standard mold thickness of 250 mm was adopted for the simulation.
Material Property Modeling of Steel Castings
The material selected for the axle housing is SCW550, a structural cast carbon steel with high strength and toughness. The chemical composition supplied by the foundry is listed in the table below:
| Element | C | Si | Mn | P | S | Mo | Cr | Ni | Fe |
|---|---|---|---|---|---|---|---|---|---|
| Content (wt. %) | 0.20 | 0.50 | 1.00 | 0.03 | 0.03 | 0.05 | 0.20 | 0.50 | Balance |
In the ProCAST material database, the exact thermophysical properties of SCW550 were not available. Therefore, the necessary parameters were established by referencing similar low-carbon steel grades and using the built-in property estimation algorithms. The thermal conductivity of the steel was determined using the Lever rule algorithm. The comparison between the Lever rule and the Scheil model revealed significant differences, as shown by the thermal conductivity curves. The Lever model was chosen because it better conforms to the experimentally measured values for low-carbon steel. The specific heat capacity of the steel in the solid state and liquid state was calculated using the following regression formulas:
$$ C_S = 550 + 9.25 \times 10^{-2} T \tag{11} $$
$$ C_L = 842 \tag{12} $$
where C_S is the specific heat in the solid state (J/kg·°C), C_L is the specific heat in the liquid state (J/kg·°C), and T is the temperature in °C. The effective specific heat method was used to handle the latent heat release during solidification:
$$ C_{eff} = f_s C_S + (1 – f_s) C_L – L_e \frac{\partial f_s}{\partial T} \tag{13} $$
where f_s is the solid fraction and L_e is the latent heat of fusion. The liquidus and solidus temperatures were calculated from empirical relationships based on the alloy composition:
$$ T_L = 1534 – (73C + 12Si + 3Mn + 28P + 40S + 3.5Ni + 1Cr + 7Cu + 3Al) \tag{14} $$
The calculated values were compared with those obtained directly from the ProCAST software. The results are summarized in the next table:
| Property | Formula Calculation | Software Calculation | Difference |
|---|---|---|---|
| Liquidus T_L (°C) | 1506 | 1504 | 2 |
| Solidus T_S (°C) | 1459 | 1457 | 2 |
The excellent agreement between the two methods validated the use of the software-provided values for the simulation. The density of the steel was taken as 7.6 g/cm³ in the solid region and 7.4 g/cm³ in the two-phase region, with its variation with temperature provided by the software database. All these properties were incorporated into the simulation model to ensure accurate representation of the casting process.
Sand Mold and Core Material Properties
The mold material originally used was phenolic resin self-hardening sand, a common choice in steel foundries due to its excellent strength and dimensional stability. The thermal properties of the sand, including thermal conductivity and specific heat capacity, were selected from the ProCAST material database. The thermal conductivity of the sand at room temperature is approximately 0.65 W/(m·K) and increases at elevated temperatures. The density of the sand mold is 1520 kg/m³, and the specific heat capacity varies with temperature.
The heat transfer at the casting-mold interface is a critical parameter in the simulation. The interfacial heat transfer coefficient h governs how effectively the heat is removed from the molten metal to the mold. For compacted sand molds, a value of h = 750 W/(m²·K) was selected for the casting-mold interface, while the outer surfaces of the mold were assumed to transfer heat by natural convection to the ambient air with a heat transfer coefficient of h = 25 W/(m²·K). The standard values of heat transfer coefficients used in the simulation are given below:
| Interface Type | Heat Transfer Coefficient (W/m²·K) |
|---|---|
| Casting-mold interface | 750 |
| Mold-air interface (natural convection) | 25 |
| Riser top-air interface (with insulation) | 10 |
Boundary and Initial Conditions
For the numerical simulation, several boundary and initial conditions must be defined. The molten steel was assumed to enter the sprue at a constant temperature of 1640°C, with a filling rate of 15 kg/s and the gravity vector oriented along the positive Z direction. The initial temperature of the sand mold was set to the ambient value of 25°C. The simulation was terminated when the casting temperature dropped to 700°C, a value well above the solidus temperature, ensuring the entire solidification sequence was captured. The detailed parameter setup is reported below:
| Parameter | Value |
|---|---|
| Pouring temperature | 1640°C |
| Pouring velocity | 15 kg/s |
| Gravity direction | +Z |
| Initial casting temperature | 1640°C |
| Initial mold temperature | 25°C |
| Stop temperature criterion | 700°C |
Simulation Results of the Initial Casting Process
After completing the pre-processing, the numerical simulation of the filling and solidification of the cast steel axle housing was performed using ProCAST. The simulation procedure generated the necessary binary files containing the results of flow, thermal, and porosity calculations. The filling sequence shown in the simulation results demonstrates that the molten steel flowed smoothly through the gating system and gradually filled the mold cavity. The molten steel entered the mold from the gating system, then proceeded into the lower sections of the casting, and eventually rose to fill the upper sections. The overall filling time was in the order of 45 seconds.
The filling simulation revealed that although the flow was generally steady, localized turbulence occurred at the junctions of multiple flow fronts. This turbulence could potentially lead to gas entrapment and inclusions in the final casting. However, the well-designed gating system ensured that most of the entrapped air was expelled through the vents during filling.
The solidification sequence is of utmost importance in determining the soundness of steel castings. The solidification time plot obtained from the simulation shows the distribution of the time from the liquidus temperature to the solidus temperature across the casting. The longer solidification times are represented in red, while shorter times are represented in deep purple. It is evident from the simulation that the last solidifying regions are located at the two end flanges and the central thick section of the axle housing. These are the regions that correspond to thermal hot spots where the local heat conduction is poor, and thus solidification is delayed. The hot spot positions were accurately identified, and the risk of internal shrinkage defects in these regions was confirmed by the porosity criterion.
The predictions of shrinkage cavity and porosity were visualized using the hot spot criterion and the Porosity criterion. The results, as presented in the diagram of shrinkage cavity and porosity, show distinct porosity formations at the two ends of the casting and in the central upper section. The central upper section displayed a noticeable shrinkage tendency, indicating that the gating system was not fully capable of feeding the solidifying steel near the end of solidification. The occurrence of such defects can be attributed to the insufficient number of risers and the inadequate thermal gradient between the casting and the feeding system.
Optimization of the Casting Process for Steel Castings
Based on the analysis of the initial simulation, it was evident that the casting process required substantial modifications to eliminate the shrinkage defects. The optimization strategies were categorized into three progressive schemes, each addressing different aspects of the casting process.
Scheme 1: Addition of Conventional Risers
The first optimization scheme involved the introduction of conventional risers to the casting system. Risers serve as reservoirs of molten metal that can compensate for the volumetric shrinkage during solidification. This approach is widely practiced in the production of steel castings because steel has a high volumetric contraction ratio. The risers were positioned at the two end flanges and near the gating system. The objective was to enhance the feeding capacity of the gating system and to create preferential thermal gradients that would ensure directional solidification from the extremities toward the risers.
The key principles in riser design are summarized as follows:
1. The riser solidification time should exceed the solidification time of the casting section it feeds.
2. The riser must contain sufficient liquid metal to compensate for both the liquid and solidification contraction of the casting.
3. The feeding channel between the riser and the casting must remain open until solidification is complete.
4. The geometric hot spot of the casting should coincide with the riser-casting junction to minimize the need for additional feeding aids.
Upon re-running the simulation with conventional risers, the solidification time diagram was substantially altered. The maximum solidification time region shifted from the internal sections of the casting to the risers themselves. The hot spot comparison chart clearly shows that the risers were effective in moving the hot spots out of the casting. As a consequence, the shrinkage cavity and porosity in the end flanges were greatly reduced. However, the central section of the axle housing, corresponding to the differential housing, still exhibited a moderate level of shrinkage porosity. This suggests that the central thickened areas required additional thermal control measures.
Scheme 2: Application of Insulated Riser Sleeves
To further improve the feeding efficiency and reduce the risks of central shrinkage, the second optimization scheme adopted insulated risers at the two end flanges. Insulated risers, also known as exothermic sleeves or insulating sleeves, are made of materials with very low thermal conductivity and sometimes contain exothermic compounds that release heat upon ignition. These sleeves significantly reduce the heat loss from the riser top and side walls, thereby extending the liquid lifetime of the riser. In industrial practice, insulating sleeves enhance the efficiency of feeding by keeping the riser molten for a longer duration, which allows for more complete feeding of the casting.
The thermophysical properties of the insulating material used for the riser sleeves are characterized as follows. The thermal conductivity is highly temperature-dependent, initially low and increasing gradually as the temperature rises. The density of the insulating material is 500 kg/m³, with a specific heat capacity that follows a distinct curve as a function of temperature. Since direct measurement of the exothermic reaction kinetics is difficult, the energy release was treated as an additional heat source inside the riser region. The simulation results show that the solidification time in the riser area was significantly prolonged, and the hot spot in the end flanges shifted completely into the insulating sleeves. This led to a marked reduction in the internal shrinkage porosity of the casting.
The comparison of the shrinkage porosity distribution between Scheme 1 and Scheme 2 demonstrates that the insulating sleeves were more effective in eliminating the defects at the flange ends. The use of insulating sleeves not only reduces the number of risers needed but also improves the casting yield. Nevertheless, the central section of the casting continued to be a concern, requiring a different approach.
Scheme 3: Reformulation of the Core Sand Material
The persistent central defects in the cast steel axle housing were attributed to the poor collapsibility and high thermal conductivity of the phenolic resin self-hardening sand core. During solidification, the sand core restricts the contraction of the solidifying steel shell, causing tensile stresses and potential hot tearing. The high thermal conductivity of the core also accelerates the cooling rate at the core-casting interface, leading to a less favorable temperature gradient for feeding. To mitigate these effects, a new core material was selected: water glass sand (sodium silicate-bonded sand). This material exhibits superior collapsibility due to its lower high-temperature strength and a lower thermal conductivity, thereby promoting a more uniform cooling process.
| Property | Phenolic Resin Sand | Water Glass Sand |
|---|---|---|
| Density (kg/m³) | 1520 | 1520 |
| Thermal conductivity | Higher | Lower |
| High-temperature collapsibility | Poor | Excellent |
| Core collapsibility | Restrictive | High |
The center core of the axle housing was redesigned to combine both materials: a water glass sand core embedded in the middle region of the phenolic resin core. This hybrid core structure allowed the central sections that suffered from hot spots to have a lower thermal extraction rate and better stress relief. The numerical simulation of this new configuration showed a substantial reduction in the hot spot in the central area. The porosity diagram for Scheme 3, as seen in the shrinkage cavity comparison, exhibits almost complete elimination of internal shrinkage porosity in the axle housing. The simulation results strongly indicated that the combination of insulated risers and the modified core sand material provided the optimal conditions for the production of sound steel castings.
Experimental Verification
The optimized casting process, incorporating the changes outlined in Scheme 3, was transferred to the foundry floor for a full-scale production trial. The mold and cores were manufactured using the production facilities available at the foundry. The molding line consisted of a DS25 continuous sand mixer, vibration tables, and a rollover machine, enabling semi-automated mold production. The sand mixture proportions are given in the following table:
| Component | Ratio/Percentage |
|---|---|
| New silica sand | 5-25% |
| Reclaimed sand | 75-95% |
| Furan resin | 0.3-0.5% |
| Sodium silicate (water glass) | 5-7% |
| Hardener | 0.15-0.25% |
The cores were coated with a zircon-based refractory coating to prevent metal penetration and sand burn-on. The mold cavities were coated using the flow-coating technique with an alumina-based coating. The coating density was controlled within 1.6-1.8 g/ml for flow coating and 1.8-2.1 g/ml for brush application. The cores were dried and assembled, then placed in the mold. The pouring conditions were identical to those used in the simulation, as detailed earlier.
After pouring, solidification, and cooling, the castings were subjected to rigorous inspection. The actual castings were sectioned at various critical locations, precisely where the simulation had predicted potential shrinkage porosity. The cross-sectional cuts of the optimized cast steel axle housing showed a completely sound internal structure. No visible shrinkage cavities or significant porosity were observed. The absence of defects in the castings aligned perfectly with the numerical predictions made by ProCAST. The successful trial validated the accuracy and reliability of the numerical simulation in guiding the process design for steel castings.
The comparison between the initial and optimized processes revealed that the combination of adding risers, using insulating sleeves, and optimizing the core sand materials successfully eliminated the shrinkage defects in the cast steel axle housing. This approach not only improved the quality of the castings but also significantly reduced the development time and avoided the need for multiple physical trials. The economic benefits to the foundry are considerable, including reduced scrap rates, decreased material consumption, and faster time-to-market for new products.
Conclusion and Future Perspectives
This thesis has demonstrated the effectiveness of numerical simulation in guiding the casting process optimization of steel castings, specifically for a large and complex cast steel axle housing. Based on the findings and experiences acquired throughout this investigation, the following conclusions can be drawn:
1. The application of CATIA and ProCAST for modeling and simulation of the casting process of steel castings provides a comprehensive understanding of the filling and solidification behavior. The simulation successfully reproduced the defect formation mechanisms and identified the precise locations of shrinkage cavity and porosity in the initial casting design.
2. The primary deficiencies of the initial casting process were identified as insufficient riser provisions and improper core material selection. The hot spots at the two ends and the central section of the axle housing were the primary origins of internal porosity.
3. The addition of conventional risers to the end flanges and the gating system proved effective in shifting the hot spots from the casting into the risers, significantly reducing the internal shrinkage porosity in the flange regions.
4. The use of insulating riser sleeves further improved the feeding efficiency and eliminated the residual porosity at the end sections. The insulating material effectively prolonged the liquid state of the riser, ensuring complete feeding of the solidifying steel castings.
5. Replacing the middle phenolic resin self-hardening sand core with water glass sand dramatically reduced the shrinkage porosity in the central section of the casting. The water glass sand provided superior high-temperature collapsibility, allowing the solidifying casting to contract freely. Moreover, its lower thermal conductivity contributed to a more favorable solidification pattern. This confirms that core sand selection is of paramount importance in controlling the soundness of steel castings.
6. The simulation results of the optimized casting process were validated by full-scale production trials. The actual castings exhibited no significant shrinkage defects, and the internal quality met the required standards for the mining vehicle axle housing. This successful outcome not only substantiates the accuracy of the numerical model but also confirms the substantial value of casting simulation in reducing development costs and lead times.
Looking forward, several avenues for further improvement are worth consideration. The current simulation only focused on the thermal and porosity prediction. Future studies could incorporate stress analysis to better assess hot tearing tendencies. The database of material properties in the simulation software could be expanded to accommodate all the alloys produced by the company, thereby enabling simulation to be applied to a wider range of products. Additionally, simulation could be used to explore the effects of pouring temperature, chills, and alternative gating designs. The knowledge gained from this research can provide valuable guidance for the development of future steel castings with complex geometries and stringent quality requirements.
Acknowledgements
I wish to express my deepest gratitude to all who have supported and guided me through this demanding yet rewarding journey. The completion of this thesis would not have been possible without the invaluable assistance from my research supervisor, colleagues, and the foundry staff. Their unwavering support and constructive suggestions have greatly contributed to the development of this research. I also deeply appreciate the assistance provided by the technical team during the experimental trials at the foundry. Their expertise and willingness to share knowledge were essential to the success of this work.