
In the production of complex, thin-walled aluminum alloy components like transmission housings and clutch housings, the Lost Foam Casting (LFC) process offers significant advantages in terms of design flexibility and cost-effectiveness for prototyping and low-to-medium volume production. However, the quality of the final shell castings is profoundly influenced by the gating system design. Poor design can lead to defects such as mistuns, shrinkage porosity, and gas porosity, resulting in unacceptably low yield rates. This article details a first-person engineering perspective on diagnosing and solving such quality issues through systematic gating system optimization for a specific aluminum alloy transmission-clutch integrated housing.
The subject component, a ZL101A aluminum alloy integrated transmission and clutch housing, presents a formidable challenge for the LFC process. Its design, originally intended for high-pressure die-casting, features intricate internal and external ribbing, varying wall thicknesses (with a minimum of 4mm), and complex geometries with undercuts. The primary quality requirement is 100% X-ray inspection, with stringent mechanical properties: tensile strength (Rm) ≥ 250 MPa and elongation (A) ≥ 3%. The initial yield rate for sound castings was below 30%, which was economically and logistically unsustainable.
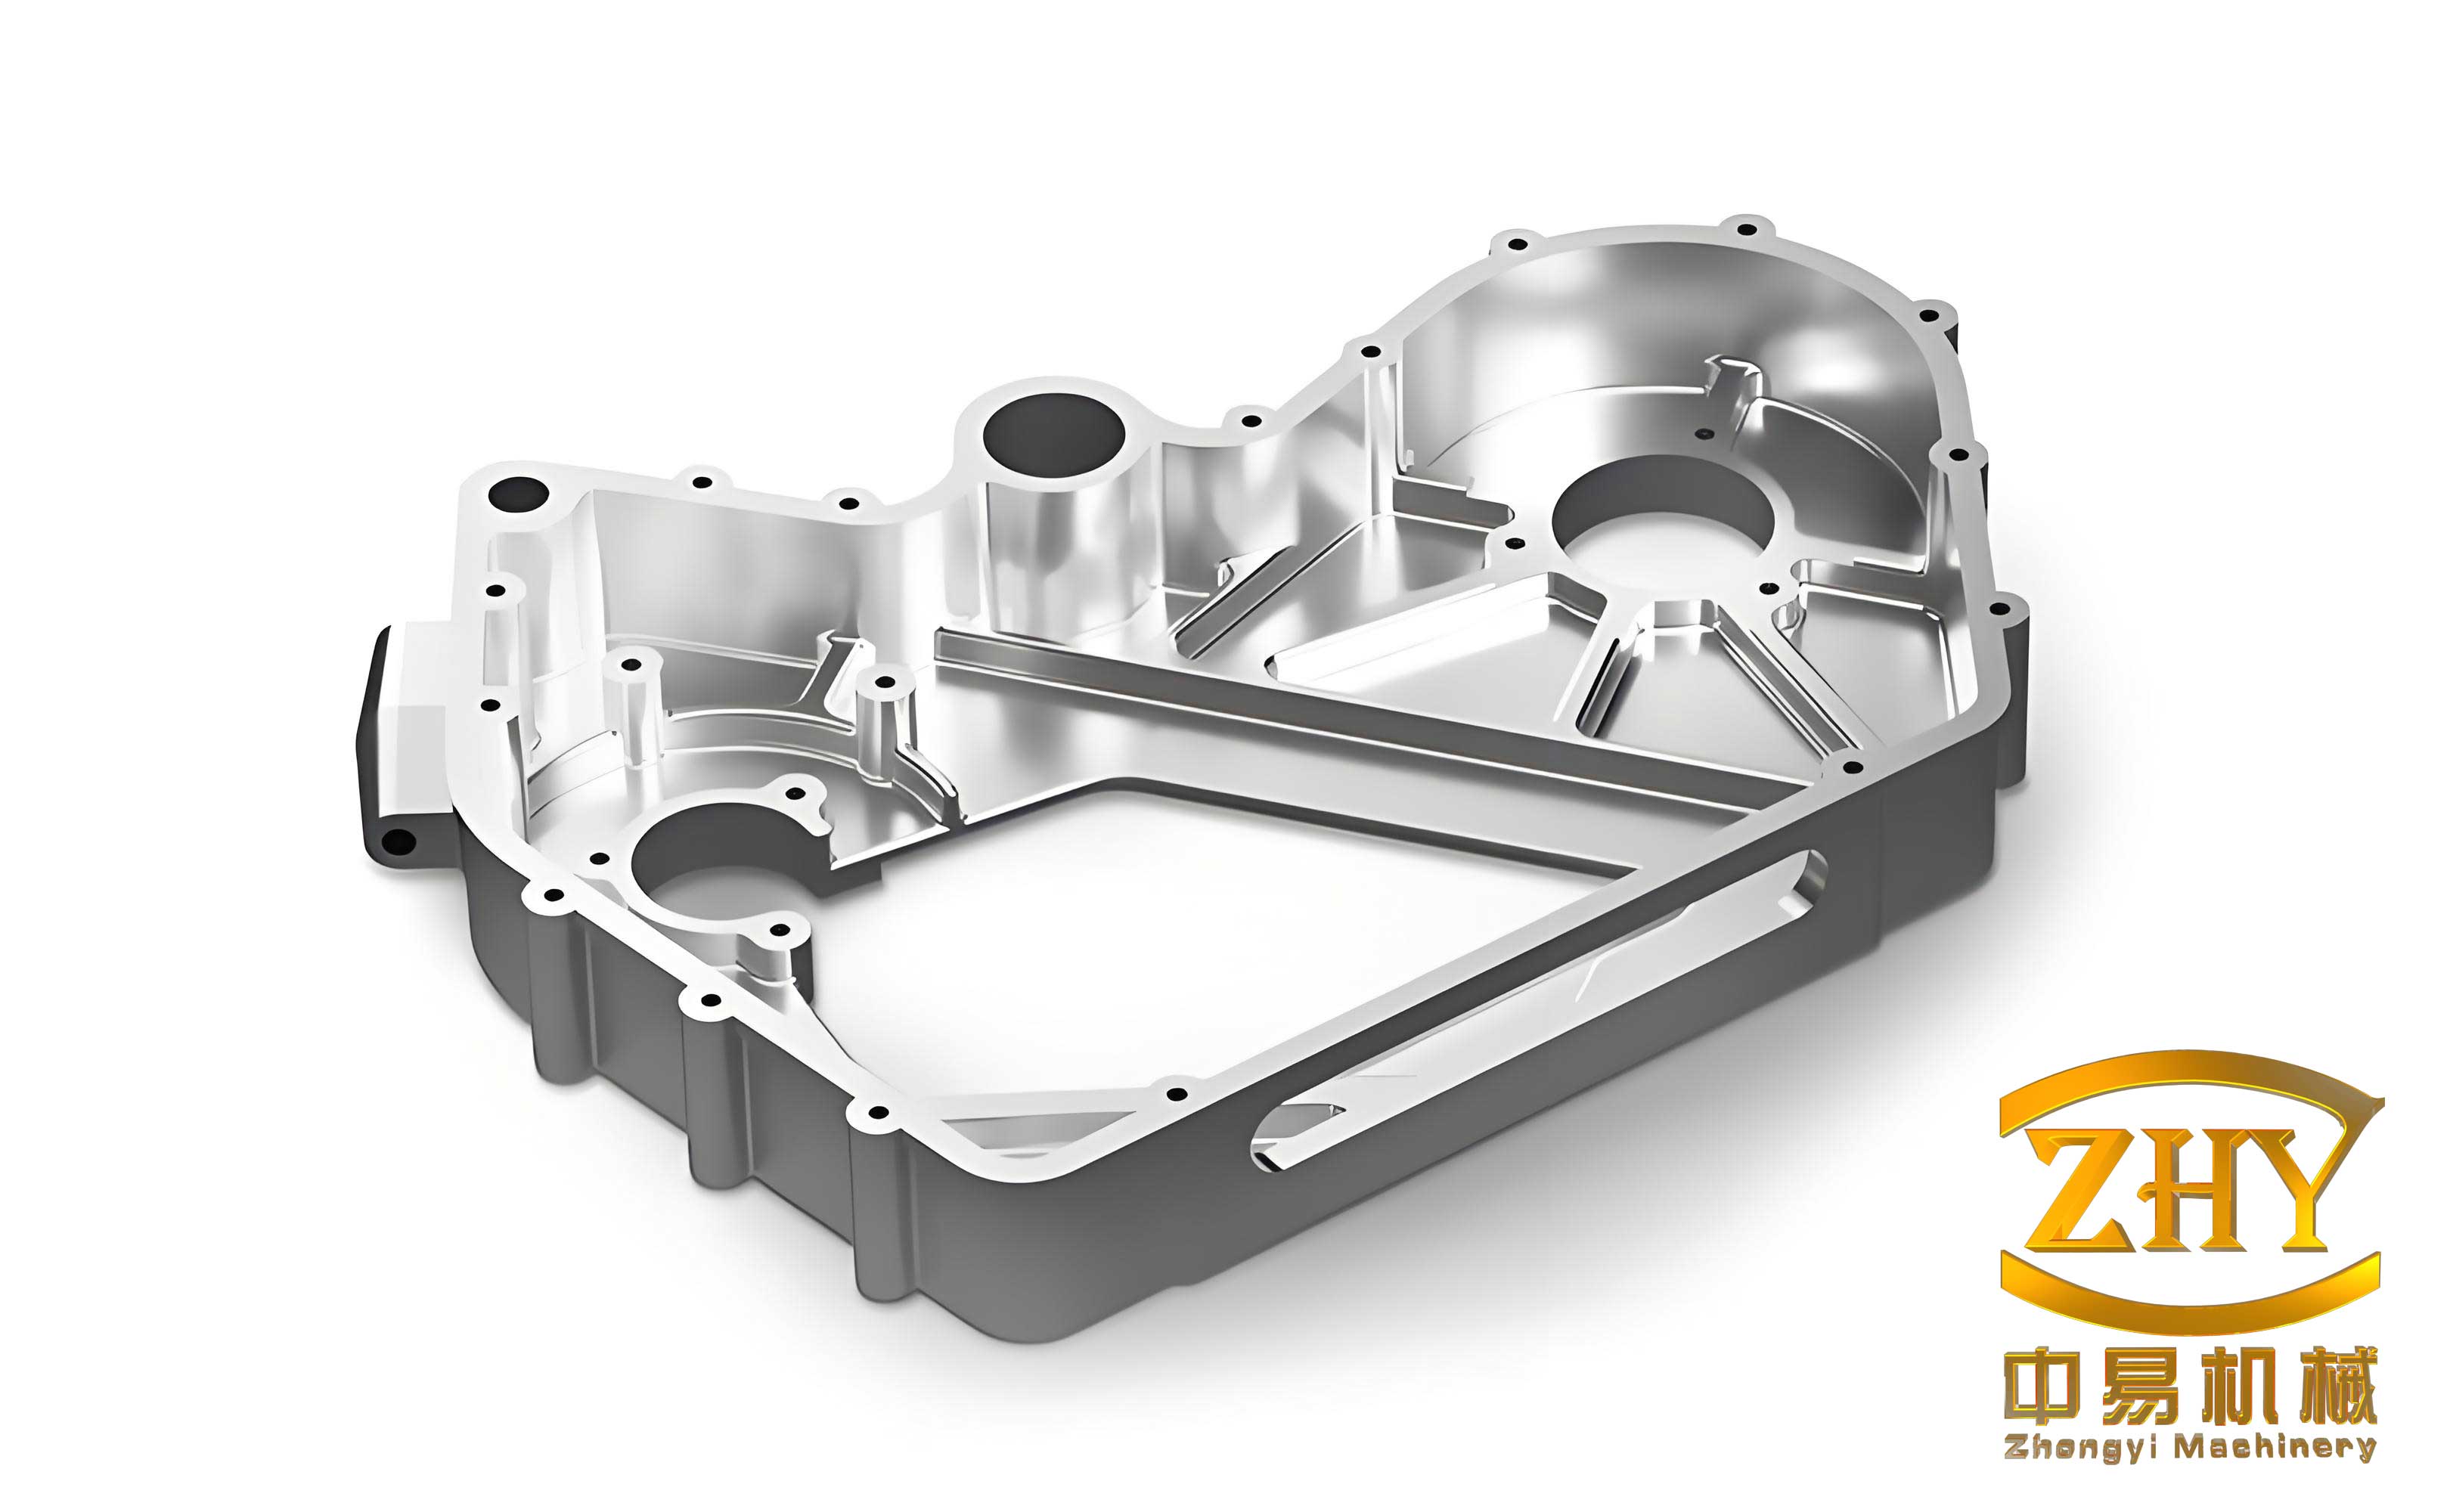
The LFC process for such shell castings involves several critical stages: foam pattern assembly, coating application and drying, sand filling and compaction, and finally, pouring. The interaction between the molten metal and the decomposing foam pattern is central to defect formation. The governing equations for fluid flow and heat transfer during mold filling are described by the Navier-Stokes and energy equations, considering the momentum sink and gas generation from foam degradation:
$$
\rho \left( \frac{\partial \mathbf{u}}{\partial t} + \mathbf{u} \cdot \nabla \mathbf{u} \right) = -\nabla p + \mu \nabla^2 \mathbf{u} + \rho \mathbf{g} + \mathbf{S}
$$
$$
\rho C_p \left( \frac{\partial T}{\partial t} + \mathbf{u} \cdot \nabla T \right) = \nabla \cdot (k \nabla T) + \dot{Q}_{reaction}
$$
Here, $\mathbf{S}$ represents the momentum sink due to the viscous resistance in the porous coating/sand medium and the counter-pressure from foam pyrolysis gases. $\dot{Q}_{reaction}$ accounts for the endothermic heat of foam decomposition. A poorly designed gate can exacerbate back-pressure, leading to mistuns, or create unfavorable thermal gradients, promoting shrinkage.
Two initial gating system designs were implemented and analyzed:
| Gating Scheme | Orientation & Gate Location | Area Ratio (Sprue:Runner:Gate) | Primary Defects Observed | Root Cause Analysis |
|---|---|---|---|---|
| Bottom Gating | Clutch flange down, gates on outer rim. | 2.0 : 1.3 : 1.0 | Shrinkage porosity in thick sections; Mistuns in distant, thin ribs. | Poor thermal gradient for feeding; Metal front loses heat and mobility before filling intricate, remote sections. |
| Step Gating | Clutch flange down, gates at flange and on transmission side window. | Variable | Random, scattered gas porosity. | Turbulent filling and air entrapment; Potential for “foam swallowing” if gate velocity is too high, trapping decomposition gases in the melt. |
The defect formation mechanisms can be further quantified. Shrinkage porosity occurs when liquid feeding is insufficient to compensate for solidification shrinkage. The Niyama criterion, often adapted for shell castings, provides a useful indicator:
$$
G / \sqrt{\dot{R}} \ge C
$$
where $G$ is the temperature gradient, $\dot{R}$ is the cooling rate, and $C$ is a material-dependent constant. Low $G$ values in isolated thermal nodes, often created by improper gating, predict shrinkage susceptibility. Gas porosity, on the other hand, arises when the total gas pressure ($P_{gas}$) from foam decomposition and air entrainment exceeds the local metallostatic pressure ($P_{metal}$) plus the capillary pressure ($P_{\sigma}$) needed to nucleate a pore:
$$
P_{gas} > P_{metal} + P_{\sigma} = \rho g h + \frac{2\sigma}{r}
$$
Where $\rho$ is melt density, $g$ is gravity, $h$ is the melt head, $\sigma$ is surface tension, and $r$ is the pore nucleus radius. Turbulent filling increases $P_{gas}$ by fragmenting and trapping foam decomposition products.
Based on this analysis, a radical redesign of the gating system was undertaken. The core concept was to pivot the casting orientation 180 degrees and utilize a central, top-down gating approach via the main bore of the housing.
Optimized Central Gating System Design:
- Orientation: The casting was inverted, with the clutch flange facing upwards. This positions the massive, thermally demanding flange section near the top, directly under the gates, creating a natural and positive thermal gradient for directional solidification towards the gates.
- Sprue and Runner: A single, sizable rectangular sprue (64mm x 64mm x 350mm) was used to ensure adequate flow rate and heat content.
- Gate Design: Three gates, spaced 120° apart, were connected from the sprue to the central bore of the housing. The gates were designed with a specific profile (32mm wide x 15mm thick) to balance flow velocity and heat transfer. Crucially, two of these gates were strategically aligned to feed directly into the two thick support pillars on the clutch floor, providing direct thermal and mass feeding to these critical, shrinkage-prone zones.
- Connection Geometry: The gates were connected to the sprue via short, cylindrical connectors (φ50mm x 50mm). This design provided ample space for dry sand to flow through and compact effectively behind the pattern’s internal walls, preventing sand collapse and subsequent metal penetration.
- Pattern Reinforcement: To combat distortion during coating and sand filling, wooden anti-deformation braces were applied to the clutch flange, and foam strips reinforced the sprue-pattern assembly.
The filling and solidification dynamics of this optimized system offer clear advantages. The metal enters at the geometric center and flows radially outward and downward into the complex shell castings features. This promotes a more uniform and simultaneous filling of thin sections, reducing the risk of mistuns. The thermal center is now at the top, near the gates. The solidification sequence can be modeled to follow Chvorinov’s rule, where solidification time $t_f$ is proportional to the square of the volume-to-surface-area ratio:
$$
t_f = C \left( \frac{V}{A} \right)^n
$$
In the optimized design, the thickest sections (flange, pillars) have the largest $V/A$ ratio but are now closest to the thermal source (the gates), ensuring they remain liquid longest to feed solidifying thinner sections below, thereby minimizing shrinkage porosity.
The gate area was carefully calculated to control velocity and avoid foam swallowing. The critical velocity $v_{crit}$ to avoid turbulent entrapment can be estimated based on the foam decomposition kinetics and gas permeability of the coating. The actual gate velocity $v_{gate}$ is given by:
$$
v_{gate} = \frac{Q}{A_{gate}}
$$
where $Q$ is the volumetric flow rate. The optimized gate dimensions ensured $v_{gate}$ remained below $v_{crit}$, promoting a smooth, laminar front that allows pyrolysis gases to be evacuated through the coating ahead of the advancing metal.
The implementation of this optimized central gating system yielded transformative results. The incidence of mistuns was virtually eliminated due to the more direct and energetic filling of complex features. Shrinkage porosity in the clutch pillars and flange was significantly reduced, as these areas became the final hot spots fed directly by the gates. Systematic gas porosity was dramatically minimized due to the controlled, quiescent filling mode. Post-production inspection and X-ray testing confirmed that the structural integrity and soundness of the shell castings met all specifications. The yield rate for qualified castings increased from below 30% to over 85%.
This case study underscores a fundamental principle in LFC process design for complex shell castings: the gating system must be engineered not just for filling, but for controlling the entire thermal history of the casting. The central top-gating approach, while counter-intuitive for some casting processes, proved ideal for this integrated housing. It established a favorable thermal gradient for feeding, enabled rapid and uniform filling of thin walls, and facilitated the orderly evacuation of decomposition products. This optimization strategy provides a valuable framework for addressing similar challenges in the lost foam casting of intricate, thin-walled aluminum shell castings, where achieving a high yield of defect-free components is paramount.