
In the field of metal casting, the production of large and complex shell castings, such as cabinet housings, presents significant challenges due to non-uniform wall thicknesses, intricate internal structures, and stringent quality requirements. As an engineer specializing in casting process design, I have encountered a specific case involving a ZL101A aluminum alloy cabinet shell casting, which exhibited high rejection rates due to defects like shrinkage porosity, shrinkage cavities, and dimensional inconsistencies. This article details my first-hand experience in optimizing the casting process for these shell castings through numerical simulation, leading to a substantial improvement in yield and quality. The focus is on leveraging simulation tools like ProCAST to predict and mitigate defects before actual production, thereby reducing costs and enhancing reliability. Throughout this discussion, the term “shell castings” will be emphasized to highlight its relevance in industrial applications.
The cabinet shell casting in question has overall dimensions of approximately 1600 mm × 550 mm × 320 mm, with a rough weight of 95 kg. Its structure is relatively regular, resembling a rectangular box divided into upper and lower cavities, with a thin-walled stepped plane in the middle and numerous internal bosses and reinforcing ribs. The wall thickness varies significantly, ranging from a maximum of 22 mm to a minimum of 8 mm. Such non-uniformity adversely affects metal fluidity during pouring and often leads to localized shrinkage defects. In a production batch of 20 shell castings, 9 were rejected—6 due to shrinkage-related defects and 3 due to dimensional exceeding on the stepped plane—resulting in a mere 55% yield. This prompted a comprehensive review and optimization of the casting process, with numerical simulation at its core.
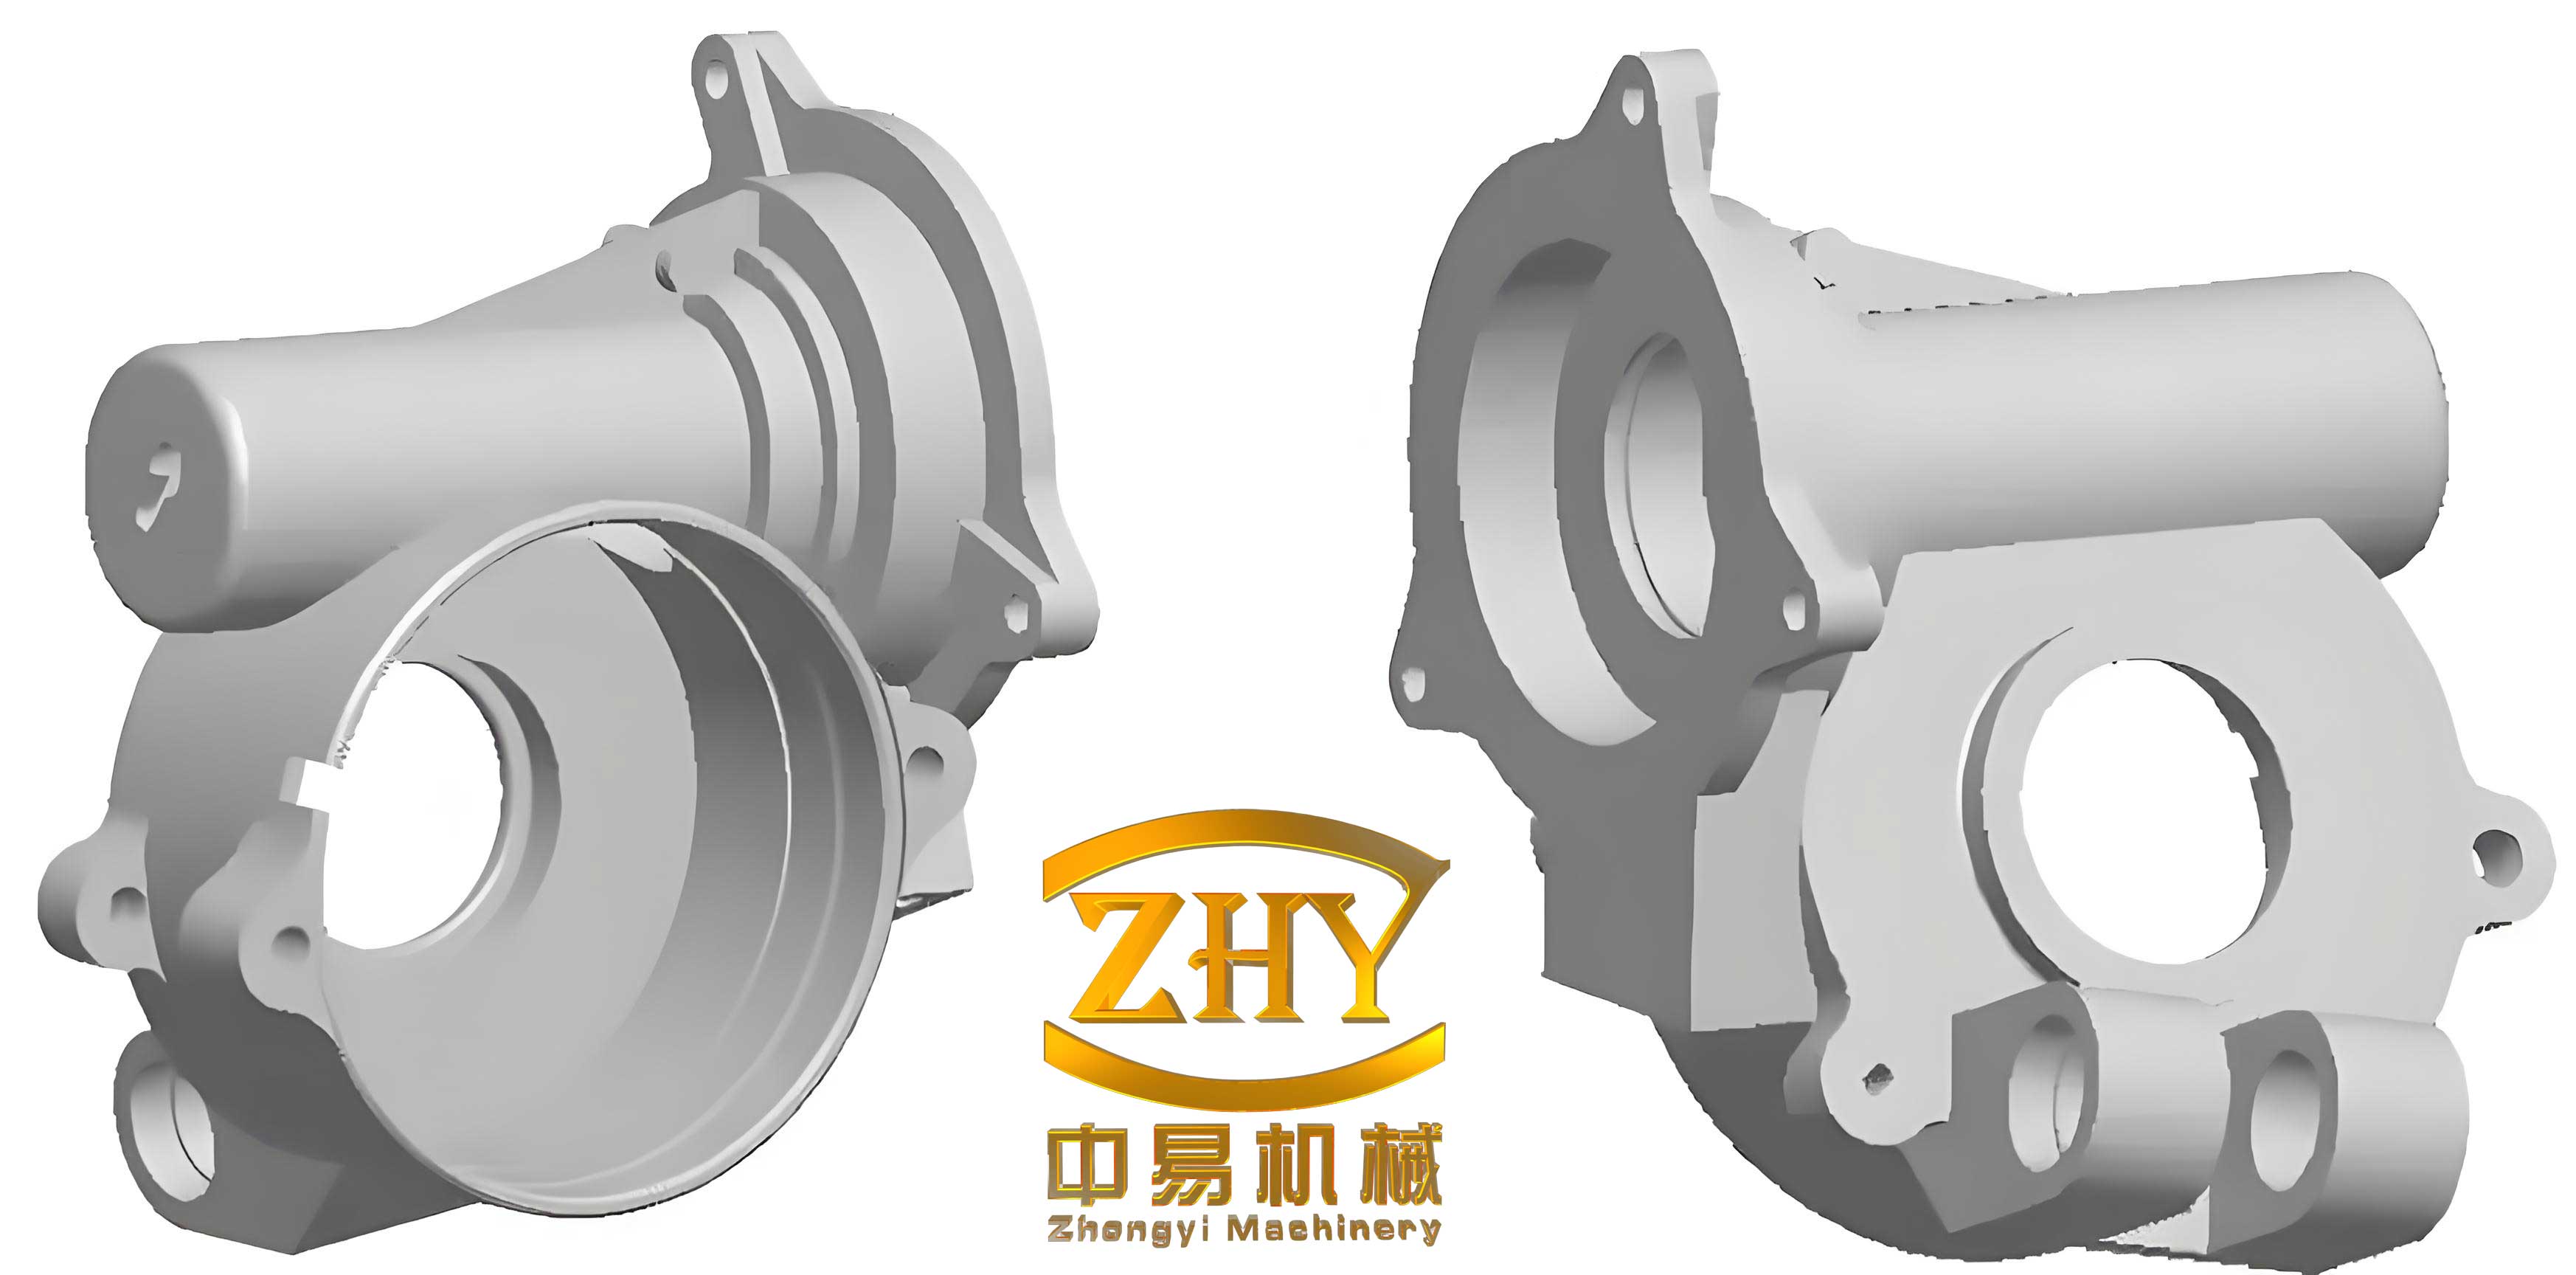
The material for these shell castings is ZL101A aluminum alloy, which must meet specific chemical and mechanical properties as per GB/T 1173-2013. The chemical composition requirements are summarized in Table 1, and the mechanical properties under T6 heat treatment (solution heat treatment plus artificial aging) are listed in Table 2. These shell castings are classified as Class II, requiring high integrity on machined surfaces with no allowed defects like shrinkage holes, cracks, or slag inclusions.
| Element | Specified Range |
|---|---|
| Si | 6.5–7.5 |
| Mg | 0.25–0.45 |
| Ti | 0.08–0.20 |
| Fe (max) | 0.20 |
| Others | As per standard |
| Property | Minimum Value |
|---|---|
| Tensile Strength | 275 MPa |
| Elongation | 2% |
| Hardness (HB) | 80 |
The original casting process employed resin sand gravity casting with a wooden pattern. The parting line was set at the middle stepped plane, resulting in a top and bottom mold arrangement. The sand core assembly consisted of an outer skin core, a top core, and a bottom core, which were difficult to position accurately due to the lack of clear locators and the heavy weight of the cores. The gating system was designed as an open type with top pouring from one side. The sprue, runners, and ingates were placed in the cope, with a filter screen at the ingate to reduce turbulence and slag inclusion. Thirteen risers were installed using the hot-spot circle method—three blind risers on the stepped plane and the rest as open risers. Chills made of the same material as the casting were placed at thick sections like the bottom and internal bosses to promote directional solidification. However, this initial process led to several issues: severe shrinkage porosity in the thin-walled stepped area and the upper side wall (referred to as A-surface), as well as poor dimensional consistency in the stepped plane thickness.
Through analysis, I identified the root causes. First, the stepped plane’s thin wall had inadequate feeding and venting; although risers and chills were used, the area requiring feeding was large with varying thickness, leading to incomplete solidification feeding. This can be explained by the feeding distance formula in casting: $$ L_f = k \sqrt{T} $$ where \( L_f \) is the feeding distance, \( k \) is a material constant, and \( T \) is the wall thickness. For non-uniform shell castings, \( L_f \) may be insufficient, causing shrinkage. Second, the A-surface, located at the top during pouring, acted as a slag and gas collection zone, exacerbating defects. Third, the core positioning inaccuracies led to dimensional variations in the stepped plane thickness, as it was a blind area during molding.
To address these, I optimized the process with a focus on numerical simulation. The key changes included: (1) altering the parting method from top-bottom to left-right parting along the stepped plane, (2) switching from top pouring to bottom pouring to ensure smoother filling, and (3) enhancing feeding with additional risers and chills. The new gating system was designed as an open type with a ratio of sprue area (\( \sum F_s \)), runner area (\( \sum F_r \)), and ingate area (\( \sum F_g \)) as \( 1 : 2.8 : 3.6 \). Thirteen open risers were placed at hot spots, and chills were strategically positioned. The simulation parameters for ProCAST were set: pouring temperature of 720°C, sand mold temperature of 20°C, and air cooling. The filling and solidification processes were simulated to predict defect formation.
The simulation results for the optimized shell castings process revealed significant improvements. During filling, the metal entered from both sides at the bottom, rising steadily without turbulence, as shown by the velocity vectors: $$ \vec{v} = \frac{d\vec{x}}{dt} $$ where \( \vec{v} \) is the fluid velocity. The temperature gradient during solidification indicated that the risers remained hot longest, aiding feeding. The shrinkage porosity prediction showed defects concentrated mainly in the gating system and risers, with minimal defects in critical areas like the A-surface and stepped plane. This aligns with the Chvorinov’s rule for solidification time: $$ t = B \left( \frac{V}{A} \right)^2 $$ where \( t \) is solidification time, \( V \) is volume, \( A \) is surface area, and \( B \) is a mold constant. By adjusting chills, the solidification time in thick sections was reduced, minimizing isolated liquid pockets.
For production validation, the optimized process was implemented. The molding used resin sand with proper strength and compaction. The cores were dried and assembled precisely. Melting was done in a medium-frequency induction furnace, followed by refinement and modification in a resistance holding furnace. The melt was treated with argon degassing to reduce hydrogen content, measured via vacuum density test—acceptable if density exceeded 2.64 g/cm³. After pouring, the shell castings were shaken out after 8 hours, and T6 heat treatment was applied. The resulting castings showed excellent quality: no cracks, shrinkage, or cold shuts, with dimensional accuracy meeting specifications. The stepped plane thickness was consistent, and machined surfaces were defect-free. Chemical and mechanical tests confirmed compliance with standards. The yield improved from 55% to 94%, demonstrating the efficacy of the optimization.
In conclusion, the integration of numerical simulation into the casting process for shell castings proved invaluable. The switch to bottom pouring and left-right parting enhanced filling stability and feeding efficiency. The use of ProCAST allowed for pre-emptive defect identification, reducing trial-and-error costs. Key formulas, such as those for feeding distance and solidification time, guided the design of risers and chills. This approach not only solved immediate quality issues but also provided a framework for optimizing complex shell castings in future projects. The success underscores the importance of simulation-driven design in modern foundry practices for high-integrity shell castings.
To further elaborate on the technical aspects, the heat transfer during solidification of shell castings can be modeled using the Fourier equation: $$ \frac{\partial T}{\partial t} = \alpha \nabla^2 T $$ where \( T \) is temperature, \( t \) is time, and \( \alpha \) is thermal diffusivity. In simulation, this equation is solved numerically to predict temperature fields. Additionally, the Niyama criterion is often used to predict shrinkage porosity: $$ N_y = \frac{G}{\sqrt{\dot{T}}} $$ where \( G \) is temperature gradient and \( \dot{T} \) is cooling rate. For aluminum shell castings, a higher \( N_y \) value indicates lower shrinkage risk. In our optimized process, the simulation showed \( N_y > 1 \) in critical areas, confirming reduced defects.
| Parameter | Original Process | Optimized Process |
|---|---|---|
| Parting Method | Top-Bottom | Left-Right |
| Pouring Method | Top Pouring | Bottom Pouring |
| Gating Ratio (∑F_s:∑F_r:∑F_g) | Not specified | 1:2.8:3.6 |
| Number of Risers | 13 (mixed open/blind) | 13 (all open) |
| Chill Usage | Limited | Enhanced at thick sections |
| Simulation Used | No | Yes (ProCAST) |
| Yield Rate | 55% | 94% |
The economic impact of this optimization for shell castings is substantial. By reducing rejection rates, material and energy savings are achieved. The formula for cost savings can be expressed as: $$ C_{save} = N \cdot (C_{prod} – C_{rej}) $$ where \( C_{save} \) is total savings, \( N \) is number of castings, \( C_{prod} \) is production cost per casting, and \( C_{rej} \) is cost of rejection. For large-scale production of shell castings, this translates to significant financial benefits.
In summary, the journey from a problematic casting process to a robust one highlights the power of numerical simulation. For shell castings, especially those with complex geometries, simulation tools like ProCAST provide insights that are difficult to obtain experimentally. By iterating virtually, we optimized feeding, gating, and cooling, leading to high-quality shell castings. This methodology is now a standard in my work for developing reliable casting processes for various shell castings components.