
The evolution of manufacturing processes for critical components in high-voltage power transmission and distribution systems, such as Three-Station (Tri-Position) enclosures used in Gas-Insulated Switchgear (GIS), represents a significant area of technological advancement. Traditionally, the production of these complex shell castings has heavily relied on aluminum casting techniques, specifically using alloys like ZL101. While effective, traditional casting presents challenges related to process complexity, environmental impact, and inherent material limitations. This analysis delves into a comprehensive comparison between the established casting methodology and an innovative “Cast-to-Weld” manufacturing process. The latter replaces the monolithic casting approach with forming and welding of wrought aluminum alloys, offering a paradigm shift towards efficiency, structural optimization, and sustainable production. The discussion will encompass material science, process mechanics, defect analysis, and a multi-faceted performance evaluation, highlighting the transformative potential of the new method for manufacturing high-integrity shell castings.
Aluminum alloys are indispensable in modern engineering due to their favorable strength-to-weight ratio, corrosion resistance, and good formability. In the power industry, particularly for SF6 gas-insulated metal-enclosed transmission lines, aluminum is the material of choice for outer enclosures. The Tri-Position shell, a central housing unit accommodating multiple switching functions, has historically been manufactured as a single shell castings piece. This approach, however, is increasingly scrutinized under the imperatives of “Carbon Peak” and “Carbon Neutrality” goals, which demand greener, more efficient manufacturing. The novel Cast-to-Weld process emerges as a direct response to these challenges, promising not only enhanced product performance but also alignment with global sustainability trends in industrial production.
1. Traditional Casting Manufacturing Process for Tri-Position Shell Castings
1.1 Material Foundation: ZL101 Cast Aluminum Alloy
The traditional process relies on ZL101 (ZAlSi7Mg), a cast aluminum-silicon alloy. Its composition and mechanical properties are standardized.
Chemical Composition: The primary elements of ZL101, as per GB/T 1173-2013, include Si (~7%), Mg (~0.3%), with controlled limits for impurities like Fe, Cu, and Zn. Silicon enhances fluidity and casting characteristics but can reduce ductility.
Mechanical Properties: The properties vary significantly with heat treatment (T-state). For shell castings requiring pressure integrity, the T5 or T6 tempers are typically targeted.
| Alloy State | Tensile Strength, Rm (MPa) | Elongation, A (%) | Typical Hardness (HBW) |
|---|---|---|---|
| As-Cast (F) | ≥ 155 | ≥ 2 | ~50 |
| T4 (Solutionized) | ≥ 185 | ≥ 4 | ~50 |
| T5 (Artificially Aged) | ≥ 205 | ≥ 2 | ~60 |
| T6 (Solutionized & Aged) | ≥ 225 | ≥ 1 | ~70 |
The strength of ZL101 shell castings can be expressed in relation to its microstructure:
$$ R_m = f(\alpha\text{-Al matrix}, \text{Eutectic Si morphology}, \text{Mg}_2\text{Si precipitates}, \text{Defect density}) $$
where the defect density (porosity, inclusions) is a critical, often process-dependent variable that can severely degrade the theoretical property ceiling.
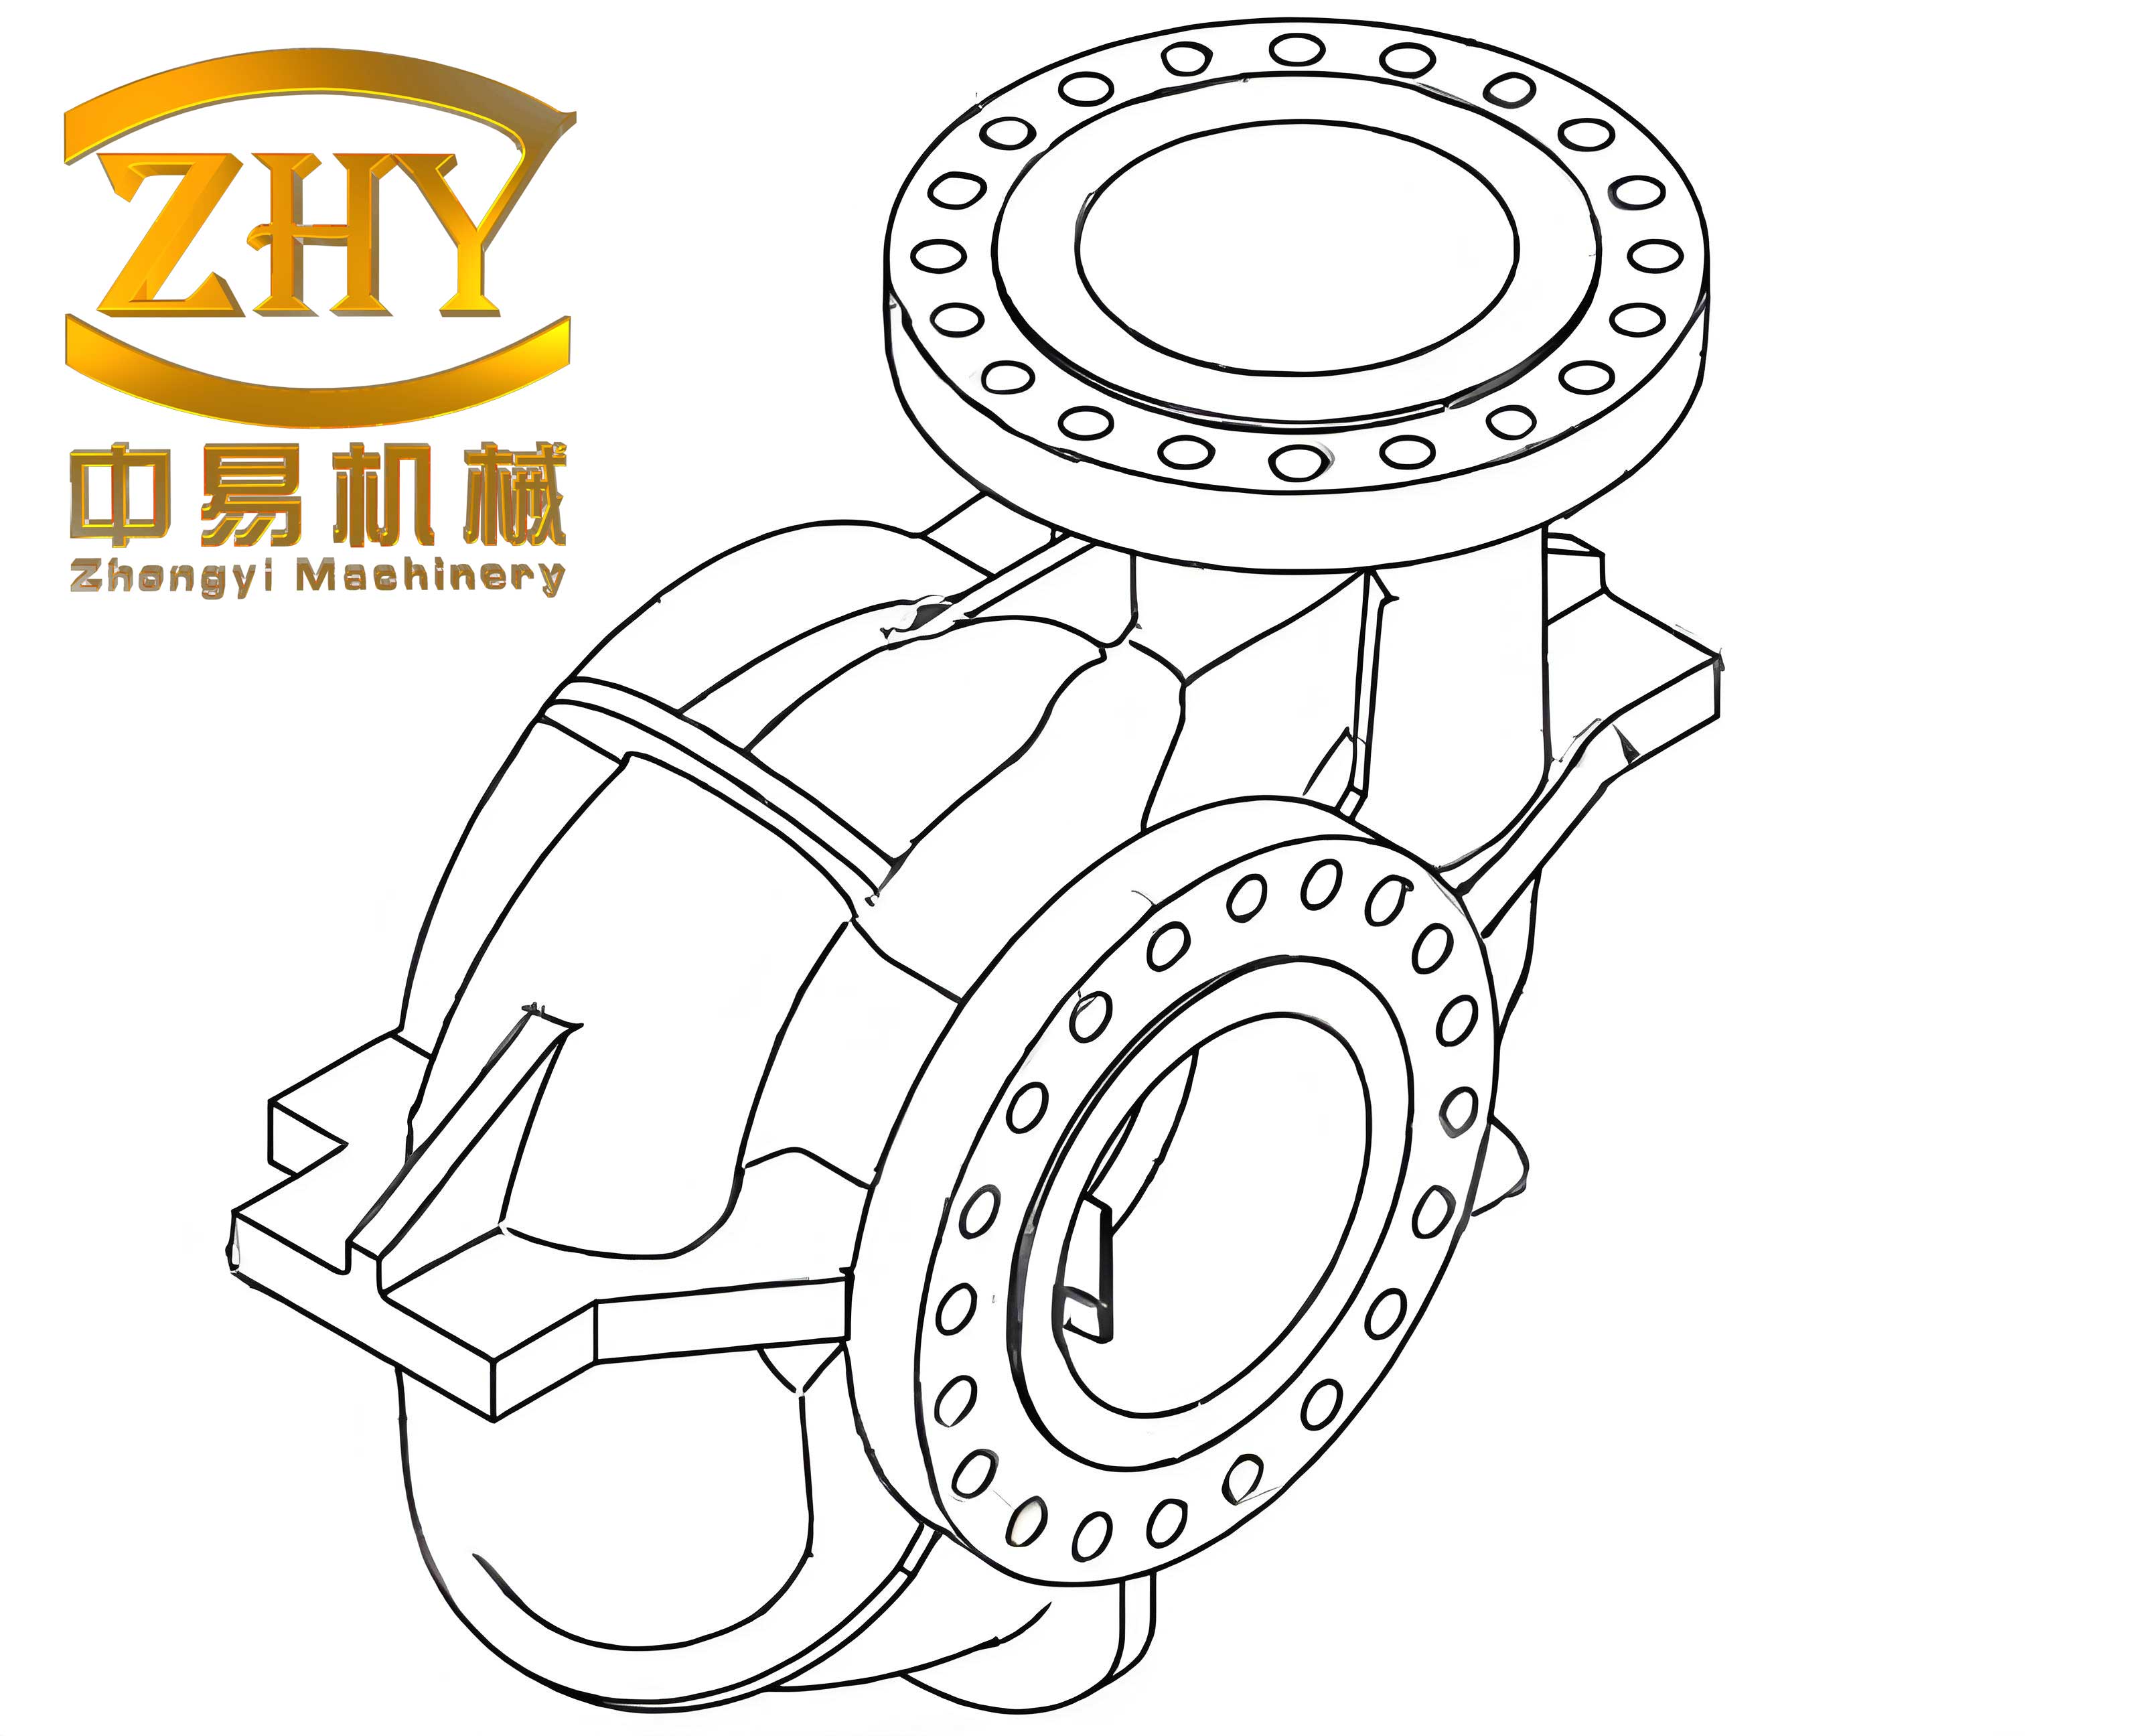
1.2 Casting Process Analysis and Inherent Defects
The manufacturing of a Tri-Position shell castings via traditional methods involves a lengthy, multi-step sequence: raw material preparation, melting, composition adjustment, refining (degassing), modification/grain refinement, pouring, heat treatment (T6), and extensive finishing/machining. Each stage introduces potential variability and defects.
Common Defects in Cast Shell Castings:
The quality of final shell castings is plagued by an array of potential imperfections intrinsic to the solidification process:
| Defect Category | Root Causes | Impact on Shell Performance |
|---|---|---|
| Micro/Macro Segregation | Non-uniform solidification, density differences. | Inhomogeneous mechanical properties, localized weakness. |
| Porosity (Gas & Shrinkage) | Entrapped gas (H₂), inadequate feeding during solidification. | Reduces effective load-bearing area, acts as stress concentrator: $$ \sigma_{local} \approx \sigma_{nominal} \cdot K_t $$ where Kt (stress concentration factor) increases sharply with pore sharpness. Degrades pressure tightness. |
| Inclusions (Oxide, Slag) | Poor melt practice, furnace lining erosion. | Creates brittle points, initiates fatigue cracks, compromises pressure boundary integrity. |
| Hot Tears & Cold Cracks | Thermal stresses exceeding material strength in semi-solid/ solid state. | Catastrophic leaks, significantly reduces fatigue life and fracture toughness. |
| Cold Shuts & Misruns | Low melt temperature, poor fluidity. | Creates planar discontinuities, severe leakage paths. |
Furthermore, the geometric necessities of casting often lead to thick sections, abrupt changes in wall thickness, and non-optimal fillet radii at intersections (e.g., where cylindrical branches meet the main shell). These features are stress concentrators. The localized stress ($\sigma_{max}$) at a sharp corner can be estimated relative to the nominal stress ($\sigma_{nom}$):
$$ \sigma_{max} = K_t \cdot \sigma_{nom} $$
For a sharp re-entrant corner in a shell castings, Kt can be significantly greater than 3, drastically reducing the pressure vessel’s fatigue life. This necessitates over-engineering (thicker walls) in traditionally cast shell castings to compensate for these inherent stress risers and potential defects, increasing weight and material usage.
2. Novel Cast-to-Weld Manufacturing Process
2.1 Material Foundation: 5XXX Series (Al-Mg) Wrought Alloy
The Cast-to-Weld process abandons casting alloys in favor of work-hardenable 5XXX series Al-Mg alloys (e.g., AA5083, AA5456). These are non-heat-treatable and derive strength from solid solution strengthening and strain hardening.
Key Advantages:
– Superior ductility and toughness: Higher elongation (A > 10-15% typically) provides greater damage tolerance.
– Excellent weldability: Low susceptibility to solidification cracking.
– Homogeneous microstructure: Free from casting defects like shrinkage porosity and coarse eutectic silicon.
– Good corrosion resistance, especially to marine atmospheres.
The yield strength ($\sigma_y$) of the base plate is a more reliable and consistent design parameter compared to cast material:
$$ \sigma_{y, base} \geq 125 \text{ MPa (for AA5083-H111/H321)} $$
This consistency allows for more precise and optimized design of the shell castings.
2.2 Process Methodology: Forming and Joining
The core philosophy is to “form and join” rather than “pour and solidify.” The main process flow is significantly streamlined:
- Material Certification & Blanking: Verified wrought plate is cut to computed blank sizes.
- Hot Forming / Press Brake Forming: The plate is heated and formed into hemispherical or semi-cylindrical segments using dedicated dies. Finite Element Analysis (FEA) is critical here to predict thinning and springback. The thickness distribution after forming can be modeled, ensuring minimal deviation from nominal design thickness.
- Edge Preparation: Machining of weld preparation (V or U grooves).
- Subassembly Welding: Automated or manual TIG/MIG welding of longitudinal seams for segment fabrication.
- Final Assembly Welding: Circumferential welding of segments and attachment of forged/wrought flanges.
- Inspection & Testing: Dimensional check, 100% volumetric NDT (Radiography or Ultrasonic Testing), pressure test, and leak test.
The use of formed segments allows for radical improvements in geometry. Sharp intersections are eliminated. The junction between the main shell and a branch can be designed with optimized, large-radius transitions, effectively reducing the stress concentration factor Kt to near 1. This is a fundamental geometric advantage over most shell castings.
2.3 Quality and Defect Analysis
While the Cast-to-Weld process eliminates classic casting defects, it introduces its own set of potential issues, which are generally more predictable and controllable.
| Potential Issue | Control Method | Severity vs. Casting Defects |
|---|---|---|
| Base Metal Flaws (Laminations, Inclusions) | Strict material certification (Mill certs, UT). | Far less frequent and severe than inherent casting porosity/inclusions. |
| Forming Defects (Excessive Thinning, Cracks) | FEA-based die design, controlled heating, and forming parameters. | Predictable and detectable via post-forming inspection. |
| Welding Defects (Porosity, Lack of Fusion, Cracks) | Stringent Welding Procedure Specifications (WPS), qualified welders/robots, post-weld NDT. | Localized to the weld seam; detectable with high reliability via NDT. Not pervasive throughout the component like shrinkage in a shell castings. |
| Distortion | Sequenced welding, fixturing, post-weld machining of flanges if needed. | Manageable process issue, not a material integrity defect. |
The primary performance metric for the weld joint is its efficiency, often expressed as a ratio of the weld metal or Heat-Affected Zone (HAZ) strength to the base metal strength. For 5XXX alloys, properly welded joints can achieve a joint efficiency ($\eta$) close to 1 for tensile strength:
$$ \eta = \frac{R_{m, weld}}{R_{m, base}} \approx 0.9 – 1.0 $$
The design inherently places the welded joints in areas of lower primary membrane stress where possible.
3. Comprehensive Performance Comparison
3.1 Manufacturing Process and Cycle Time
The contrast in process complexity directly impacts lead time, resource allocation, and cost structure.
| Aspect | Traditional Casting Process | Novel Cast-to-Weld Process |
|---|---|---|
| Core Steps | Pattern making, core making, melting, pouring, solidification, shakeout, heat treatment (T6), extensive fettling/grinding, machining. | Material cutting, forming, edge prep, welding, inspection. Minimal machining. |
| Cycle Time | Very long (weeks). Dependent on mold preparation, furnace schedules, and lengthy heat treatment cycles. | Significantly shorter (days). Streamlined, parallelizable steps. |
| Labor & Skill | High labor intensity across multiple skilled trades (molders, melters, heat treaters, fettlers). | Lower labor count, skills focused on forming, welding, and NDT. |
| Material Utilization | Low. Significant material is poured only to be machined away from thick sections. Sprue/runner waste. | High. Near-net-shape forming. Minimal scrap from machining. |
3.2 Environmental Impact and Energy Consumption
This is a pivotal differentiator in the context of carbon neutrality goals. The environmental footprint of producing a shell castings is substantially higher.
Emissions and Waste:
– Casting: Direct CO2 emissions from fossil-fueled furnaces (if used). Emissions of SF6 (a potent GHG) if used for degassing. Generation of foundry sand waste (spent mold material), slag, and dross. Potential VOC emissions from binders.
– Cast-to-Weld: Primary emissions are indirect, from electrical grid power for forming and welding. Very little solid waste (mostly cutting chips). No process-related SF6 or sand waste.
Energy Demand:
The total specific energy ($E_{total}$) per unit mass of finished shell can be approximated as a sum of process energies:
For Casting: $$ E_{total, cast} \approx E_{melt} + E_{heat treat} + E_{machining} $$
For Cast-to-Weld: $$ E_{total, ctow} \approx E_{forming} + E_{welding} $$
Where $E_{melt}$ (the energy to raise Al to ~750°C and provide heat of fusion) is by far the largest single term, making $E_{total, cast} >> E_{total, ctow}$. Furthermore, the lighter weight of the optimized Cast-to-Weld design compounds the lifecycle energy savings.
3.3 Structural and Mechanical Performance
This comparison lies at the heart of the technological shift from shell castings to fabricated structures.
| Performance Metric | Traditional Cast Shell | Cast-to-Weld Shell | Engineering Implication |
|---|---|---|---|
| Design Freedom & Geometry | Limited by draft angles, feed paths. Abrupt thickness changes, small fillets. | High freedom. Smooth, optimized transitions with large radii. | Cast-to-Weld enables optimal stress flow, minimizing peak stresses ($\sigma_{max}$). |
| Stress Concentration (Kt) | High at intersections due to geometry and potential micro-shrinkage. | Low. Deliberately engineered contours. | Higher fatigue life and safety margin against static failure for Cast-to-Weld. |
| Tensile Strength & Ductility | Moderate Rm (200-250 MPa), Low ductility (A ~1-4%). Brittle eutectic Si phase. | Moderate Rm (270-310 MPa for AA5083-H32), High ductility (A > 10%). Tough, ductile fracture. | Cast-to-Weld offers better toughness and damage tolerance. Less prone to catastrophic brittle fracture. |
| Property Consistency & Reliability | Variable throughout casting. Dependent on local solidification conditions. Defects are random and internal. | Highly consistent base metal properties. Defects (welds) are localized, known, and 100% inspectable. | Much higher reliability and predictable performance for Cast-to-Weld. Enables use of lower safety factors. |
| Weight | Higher, due to necessary over-thickness for casting soundness and to compensate for stress raisers. | Lower, due to material optimization and thinner, structurally efficient walls. | Direct savings in material, supporting structure, and handling. |
The fundamental comparison of structural efficiency can be framed by the achievable pressure ($P$) for a given weight ($W$) or material volume. For a cylindrical shell castings, the limiting pressure is often governed by the fatigue strength at a stress concentration or the presence of defects. For the Cast-to-Weld shell, the limit is more predictably the yield strength of the homogeneous plate material at the point of highest membrane stress. This leads to a more efficient design.
4. Conclusion
The comparative analysis unequivocally demonstrates the substantial advantages of the novel Cast-to-Weld manufacturing process over the traditional method for producing Tri-Position shell castings. While traditional casting has served the industry for decades, its drawbacks in terms of process complexity, environmental footprint, geometric limitations, and inherent defect susceptibility are significant. The Cast-to-Weld process, utilizing wrought 5XXX series aluminum alloys, addresses these issues systematically.
It replaces the unpredictable solidification process with controlled forming and welding, resulting in superior and more consistent mechanical properties, notably enhanced ductility and toughness. It enables geometrically optimized designs that minimize stress concentrations, leading to lighter, stronger, and more reliable enclosures. From a manufacturing standpoint, it streamlines production, reduces cycle time, and drastically cuts energy consumption and hazardous waste generation, making it a cornerstone for sustainable, green manufacturing in the power equipment sector.
The transition from monolithic shell castings to fabricated, weld-assembled structures represents a milestone in the evolution of high-voltage enclosure manufacturing. It aligns perfectly with global decarbonization efforts without compromising—and indeed enhancing—technical performance. The future development of this process, including the integration of robotic welding and advanced in-process monitoring, promises further gains in quality, consistency, and cost-effectiveness, solidifying its position as the superior manufacturing paradigm for critical pressure-containing shell castings in the modern electrical grid.