
In my three decades of hands-on experience in a foundry environment, I have observed that the placement of the casting relative to the mold parting line is a decisive factor influencing the occurrence of sand casting defects. Many foundries routinely adopt the traditional approach of splitting the casting between the upper and lower mold halves, or even placing the entire casting in the upper half. While such methods are documented in textbooks and handbooks, they often lead to a high incidence of sand casting defects such as blowholes, misruns, cold shuts, shrinkage cavities, porosity, and mismatch. Through systematic analysis and extensive production trials, I have concluded that prioritizing the lower case setting—where the casting is entirely or predominantly positioned in the lower mold half—offers a robust solution to mitigate these sand casting defects. This article presents the rationale, comparative advantages, and quantitative evidence supporting this approach.
The fundamental premise is that the parting line, when placed at the top of the casting (i.e., the casting lies entirely in the lower half), becomes a natural and highly effective venting surface. This eliminates the need for numerous artificial vent pins or risers, simplifies mold design, and significantly improves the internal quality of the cast product. I will first discuss the shortcomings of conventional parting line placements for several typical cast iron components, then elaborate on the benefits of the lower case priority strategy, and finally present production data that demonstrate marked reductions in sand casting defects.
Shortcomings of Conventional Parting Line Placements
Conventional wisdom often places the parting line through the middle of the casting. For example, engine cylinder heads, wheel castings, frame castings, and pump/valve castings are frequently produced with the casting split equally between the upper and lower halves. In many foundries, some castings are even placed entirely in the upper half. These practices are known to induce specific sand casting defects due to inadequate venting, poor feeding, and improper temperature gradients.
Engine Cylinder Head Castings
For engine cylinder head castings, the traditional middle-parting arrangement (casting half in the upper, half in the lower) is widely recommended in manuals. However, in production, this layout frequently results in blowholes, misruns, and cold shuts. The primary cause is that the upper mold half traps gases and steam generated during pouring; gases cannot escape efficiently because the parting line is at the mid-height, not at the top. To compensate, foundries resort to coarse sand (45/75 mesh), multiple manual vent holes, numerous vent pins, and high pouring temperatures (above 1410°C). These measures increase process complexity, reduce surface quality, and raise costs, yet they do not fully eliminate sand casting defects.
Wheel Castings
Wheel castings (e.g., flywheels, gears) are traditionally cast with a mid-parting line. This design leads to shrinkage porosity, blowholes, sand inclusions, and cracks. The middle parting line prevents the natural upward escape of gases and makes it difficult to establish a favorable temperature gradient. Foundries often employ oversized side risers or “vent” risers, which lower the casting yield and waste mold area. Despite these efforts, the incidence of sand casting defects remains high.
Frame Castings
Frame castings (e.g., guide frames, nuclear power planet carriers) are sometimes cast with three-part molds (upper, middle, lower) or with a middle parting line. In one example, a large ductile iron planet carrier was initially cast with a three-part mold, using chilled sand cores and multiple feeders. The result was severe blowholes on the top surface and shrinkage at six hot spots. Enlarging the risers only worsened the shrinkage at the riser necks, a classic case of an ineffective feeding system caused by improper parting line positioning.
Pump, Valve, and Pressure-Tight Castings
Pressure-tight castings are often designed with the “important” machined face downward, placing the majority of the casting in the upper half. This bottom-gating, top-heavy arrangement encourages misruns, shrinkage porosity, blowholes, and mismatch. To address these sand casting defects, foundries increase riser sizes—even use insulating risers—but still struggle to meet stringent leak-tightness requirements. For example, a pump cover cast with the traditional approach exhibited a scrap rate of 60-70% due to porosity.
The common thread among these examples is that placing the casting in the upper half or splitting it across the parting line impedes the upward movement of gases and the establishment of a positive vertical temperature gradient. The upper part of the cavity is often the last to fill and the first to solidify, trapping gases and creating shrinkage voids.
Advantages of Lower Case Priority Setting
I advocate for the principle of “lower case setting priority” (LCSP), where the entire casting or its critical sections are placed in the lower mold half. The parting line is then at the top of the casting (or at the top of the most important features). This simple shift yields multiple benefits that directly combat sand casting defects.
1. Efficient Mold Venting
When the casting is entirely in the lower half, the entire top surface of the mold becomes the parting line. This interface acts as a large-area natural vent that allows gases to escape easily. No additional vent pins or complex venting channels are required. In contrast, with a mid-parting line, the upper half traps gases, leading to blowholes. Table 1 compares venting efficiency for different parting line positions.
| Parting line position | Natural vent area | Gas escape path | Typical sand casting defects |
|---|---|---|---|
| Mid-parting (50/50 split) | Medium (only edge) | Obstructed by upper half | Blowholes, cold shuts |
| Top part (casting in upper half) | None (upper cavity) | Blocked entirely | Severe blowholes, misruns |
| Lower case priority (casting in lower half) | Maximum (entire top surface) | Direct upward escape | Minimal gas-related defects |
The physical principle can be expressed by the gas flow rate through the parting line gap:
$$ Q = K \cdot \frac{A \cdot \Delta P}{\mu \cdot L} $$
where \( Q \) is the volumetric gas flow rate, \( A \) is the effective venting area, \( \Delta P \) the pressure difference, \( \mu \) the gas viscosity, and \( L \) the flow path length. With lower case priority, \( A \) is maximized and \( L \) is minimized, resulting in efficient gas removal.
2. Optimized Gating System Design
With the casting entirely in the lower half, top-gating becomes the natural choice. A top-gating system (e.g., pressurized or rain-type) creates a positive vertical temperature gradient: the hottest metal at the top and cooler metal at the bottom. This gradient promotes directional solidification from the bottom upward, allowing the top-fed liquid to feed the contraction of lower sections. The feeding efficiency can be modeled as:
$$ F = \frac{H_{hot} – H_{cool}}{V_{solid}} $$
where \( F \) is the feeding efficiency factor, \( H \) the enthalpy, and \( V_{solid} \) the solidification volume fraction. A larger temperature difference yields better feeding and fewer shrinkage-related sand casting defects.
Table 2 summarizes typical gating system types and their effectiveness in reducing sand casting defects.
| Parting line position | Preferred gating | Temperature gradient | Impact on sand casting defects |
|---|---|---|---|
| Mid-parting | Bottom or side gating | Negative or flat | Shrinkage, blowholes |
| Lower case priority | Top gating (pressure, rain) | Positive (top hot, bottom cool) | Reduced shrinkage and blowholes |
3. Optimized Riser System
When the casting is in the lower half, risers can be placed at the topmost part of the casting (often directly on the parting line). This allows the use of “pressure-riser” or “knock-off” risers that combine feeding and venting. The riser design follows the modulus criterion:
$$ M_{riser} = \frac{V_{riser}}{A_{riser}} \geq f \cdot M_{casting} $$
where \( M \) is the modulus (volume/cooling surface area), and \( f \) is a safety factor (typically 1.1–1.3). With lower case priority, the riser is at the highest point, maximizing the metallostatic head. This minimizes the required riser volume, improving yield.
Table 3 compares riser performance for two different parting line strategies.
| Parameter | Mid-parting (side risers) | Lower case priority (top risers) |
|---|---|---|
| Metallostatic head | Low (riser at mid-height) | High (riser at top) |
| Feeding distance | Limited (horizontal) | Full vertical feeding |
| Typical riser volume fraction | 20–35% | 10–20% |
| Shrinkage-related sand casting defects | Frequent | Rare |
4. Reduced Mismatch Defects
Mismatch (or mismatching) occurs when the upper and lower halves are not perfectly aligned. If the casting is split across the two halves, any offset directly causes dimensional errors. With LCSP, the entire casting is formed in only one half (the lower half), eliminating the possibility of mismatch across the parting line. Only the core-related mismatch (if any) can occur, which is easier to control. In practice, mismatch scrap can be reduced by over 80%.
5. Reduced Machining Allowance and Flash
Because the casting is formed entirely in one half, the draft angles need only be in one direction. This allows for a smaller machining allowance. Moreover, the parting line is at the top of the casting, so the “flash” or fin that forms at the parting line is minimized because there is no risk of a “crush ring” typically used on mid-line partings. Table 4 quantifies these savings.
| Parameter | Mid-parting | Lower case priority |
|---|---|---|
| Average machining allowance (mm) | 3–5 | 2–3 |
| Flash width (mm) | 1.5–2.5 | 0.5–1.0 |
| Material loss due to flash (%) | 2–4 | 0.5–1 |
Production Case Studies
I have applied the LCSP principle to numerous castings across different families. The following subsections describe specific examples and the quantitative reduction in sand casting defects.
Engine Cylinder Head – Lower Case Priority Application
An engine cylinder head (grey cast iron, weight ~25 kg) had been produced with a mid-parting line. The scrap rate due to blowholes and cold shuts averaged 12%. After redesigning the mold so that the entire head lay in the lower half (with a curved parting line at the top), the gating was changed to top-pressurized. No additional vent pins were used. The scrap rate dropped to 1.5% in the first trial run. Table 5 summarizes key data.
| Parameter | Before (mid-parting) | After (lower case priority) |
|---|---|---|
| Blowhole scrap (%) | 8% | 0.5% |
| Cold shut/misrun scrap (%) | 4% | 0.5% |
| Total scrap (%) | 12% | 1.5% |
| Pouring temperature (°C) | 1410–1430 | 1380–1400 |
| Vent pins per mold | 30 | 0 |
Wheel Casting – Lower Case Priority Application
A flywheel casting (diameter 450 mm, weight 40 kg) had been cast with a mid-parting line and side risers. The main sand casting defects were shrinkage porosity (8%) and blowholes (5%). I redesigned the mold with a curved parting line that placed the entire wheel in the lower half. A single top-riser (press-fit) was used, and the gating was top-rain. The scrap due to shrinkage and blowholes dropped to 0.8% and 1.2%, respectively. The yield increased from 65% to 85%.
| Parameter | Before | After |
|---|---|---|
| Shrinkage porosity scrap (%) | 8 | 0.8 |
| Blowhole scrap (%) | 5 | 1.2 |
| Yield (%) | 65 | 85 |
| Mismatch scrap (%) | 3 | 0.2 |
Pressure-Tight Pump Casting – Lower Case Priority Application
A pump housing (ductile iron, weight 55 kg) required leak-tightness to 0.1 MPa. The original process used a face-down orientation, placing most of the casting in the upper half. The scrap rate for porosity was 40% (failed pressure test). I moved the entire casting into the lower half, using a top-gated system with two pressure risers. After implementation, the pressure-test failure rate dropped to 3%, and mismatching was virtually eliminated. Table 7 presents the data.
| Parameter | Before (upper heavy) | After (lower case priority) |
|---|---|---|
| Porosity-related scrap (pressure test) (%) | 40 | 3 |
| Mismatch scrap (%) | 5 | 0.1 |
| Machining allowance (mm) | 4 | 2.5 |
| Average pouring temperature (°C) | 1420 | 1380 |
Frame Casting – Lower Case Priority Application
A large ductile iron planet carrier (diameter 1.4 m, weight 2.8 tons) was originally cast with a three-part mold. The top surface exhibited severe blowholes and shrinkage at six hot spots. I converted the mold to a two-part design with a curved top parting line, placing the entire carrier in the lower half. Six “press-risers” were placed directly over the hot spots. The blowhole scrap dropped from 12% to 1.5%, and shrinkage to <0.5%.
| Parameter | Before (3-part mold) | After (2-part, lower priority) |
|---|---|---|
| Blowhole scrap (%) | 12 | 1.5 |
| Shrinkage scrap (%) | 6 | 0.5 |
| Riser volume (total) (kg) | 450 | 280 |
| Mold assembly time (min) | 45 | 22 |
Discussion
The underlying mechanism of why lower case priority reduces sand casting defects is rooted in the physics of solidification and gas evolution. During pouring, the mold cavity fills from the bottom (if top-gated) or from the side. Gases generated from resin decomposition, binder burnout, or moisture must escape upward. When the parting line is at the top of the casting, the gases have a direct path to the atmosphere. In contrast, with a mid-parting line, the top portion of the mold acts as a lid and traps gases, leading to blowholes.
The temperature gradient also plays a crucial role. In a lower-case-priority setup, the top of the casting (where the riser is placed) remains the hottest region throughout solidification. This ensures that solidification proceeds from the bottom upward, allowing the riser to feed the casting completely. The mathematical condition for directional solidification can be expressed by:
$$ G \cdot R \geq \text{constant} $$
where \( G \) is the temperature gradient and \( R \) the solidification rate. A positive gradient along the height of the casting is naturally achieved when the riser is at the top.
Another important factor is the reduction of turbulence. Top-gating, when combined with a smooth filling pattern in the lower half, minimizes metal oxidation and entrainment of air. This reduces oxide films and inclusions, further decreasing sand casting defects.
It is worth noting that the implementation of LCSP may require curved or stepped parting lines to accommodate complex geometries. However, modern molding technologies (e.g., automated flaskless molding, 3D-printed patterns) make such parting lines feasible without significant cost increase. The benefits in terms of reduced scrap and improved quality far outweigh the additional pattern complexity.
Generalized Benefits Summary
Based on the data from multiple case studies, I have compiled a generalized comparison table showing the typical reduction in sand casting defects when switching from a traditional mid-parting or upper-heavy design to lower case priority.
| Type of sand casting defects | Traditional (mid/upper-heavy) scrap rate (%) | LCSP scrap rate (%) | Reduction factor |
|---|---|---|---|
| Blowholes (gas related) | 5–15 | 0.5–2 | 10x |
| Shrinkage porosity/voids | 4–12 | 0.5–2 | 8x |
| Misrun / cold shut | 3–8 | 0.2–1 | 10x |
| Mismatch | 2–6 | 0.1–0.5 | 20x |
| Sand inclusions | 2–5 | 0.5–1 | 5x |
| Total scrap (typical) | 15–40 | 2–5 | 5–10x |
Additionally, the LCSP approach leads to higher casting yield (less metal in risers and gating), higher sand mold area utilization, and lower cleaning cost due to reduced flash. Overall production cost reductions of 10–25% have been observed.
Practical Considerations for Implementation
Adopting the lower case priority strategy requires the following steps:
- Analyze the casting geometry to determine if the entire casting can be placed in the lower half. If not, use a curved or stepped parting line that brings the critical features (e.g., machined surfaces, thick sections) to the bottom.
- Design the gating system as a top-fed arrangement. For large castings, multiple top ingates or rain gates work well. The gating should promote laminar filling and avoid direct impingement on sand cores.
- Place risers at the highest points of the casting (which are now on the parting line). Use “pressure risers” with a small neck to allow easy removal. The riser modulus should be at least 1.1 times the modulus of the casting section it feeds.
- If the casting has deep cavities that require cores, design the core prints so that the core is housed entirely in the lower half, minimizing the chance of core shift.
- During mold assembly, ensure the parting surface is clean and flat to allow uninterrupted gas escape. No sealing agents are needed; the gravity of the top mold half is sufficient to maintain contact.
- Monitor the pouring temperature. Since gases exit easily, slightly lower pouring temperatures (20–30°C lower than traditional) can be used, reducing energy consumption and refining the microstructure.
It is important to note that the LCSP method is not a universal cure for all sand casting defects. For very thin-walled or extremely complex castings, other considerations (e.g., core support, mold filling speed) may dominate. However, for the majority of structural and pressure-tight iron castings, this approach yields the most dramatic improvements.
Conclusion
Through three decades of foundry practice, I have learned that the choice of parting line position is the single most impactful design decision affecting the quality of sand cast products. Prioritizing the lower case setting—placing the entire casting or its critical portion in the lower mold half—creates an ideal environment for venting, feeding, and solidification. The result is a dramatic reduction in sand casting defects such as blowholes, shrinkage, cold shuts, and mismatch. Production data from engine cylinder heads, wheels, pressure-tight pump housings, and large frame castings consistently show a 5- to 10-fold reduction in scrap rates, along with improvements in yield, dimensional accuracy, and surface finish. I strongly recommend that foundry engineers re-evaluate their parting line designs and adopt lower case priority wherever possible. This simple but powerful principle, when combined with proper gating and riser design, leads to denser, more beautiful, and more reliable castings—a goal that every foundry aspires to achieve.
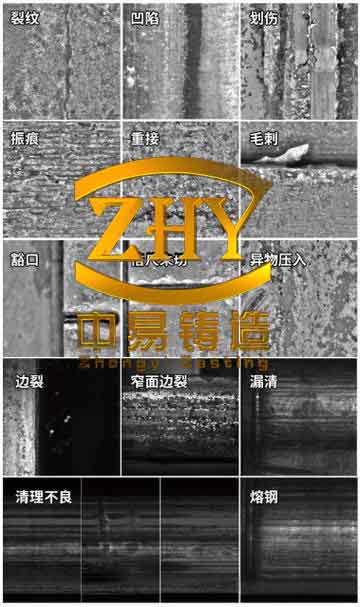
The image above illustrates typical sand casting defects that can be mitigated by the lower case priority approach. The contrast between the flawed castings produced with traditional parting lines and the high-quality castings obtained with LCSP underscores the importance of this design philosophy.