
The pursuit of high performance and reliability in modern aero-engines places stringent demands on every component. Among these, the accessory gearbox housing plays a critical role, serving as the structural backbone for power transmission to auxiliary systems such as fuel and oil pumps. These housings, typically manufactured as large, intricate, thin-walled shell castings, are particularly susceptible to dimensional instability during service. The phenomenon of housing deformation, manifesting as bore misalignment and positional errors, poses a significant threat to gear mesh integrity, leading to accelerated wear and potential system failure. Based on extensive literature and field experience, a primary contributor to this in-service distortion is the release of locked-in residual stresses originating from the casting process. These inherent stresses, if not adequately managed, can redistribute under thermal and mechanical loads during operation, leading to unwanted geometric changes. This work focuses on the front half of such an accessory gearbox housing. We embark on a comprehensive study to characterize the magnitude and distribution of residual stresses within this critical shell casting, employing a synergistic approach of experimental measurement and numerical simulation, followed by the application and validation of an advanced stress-relief optimization technique.
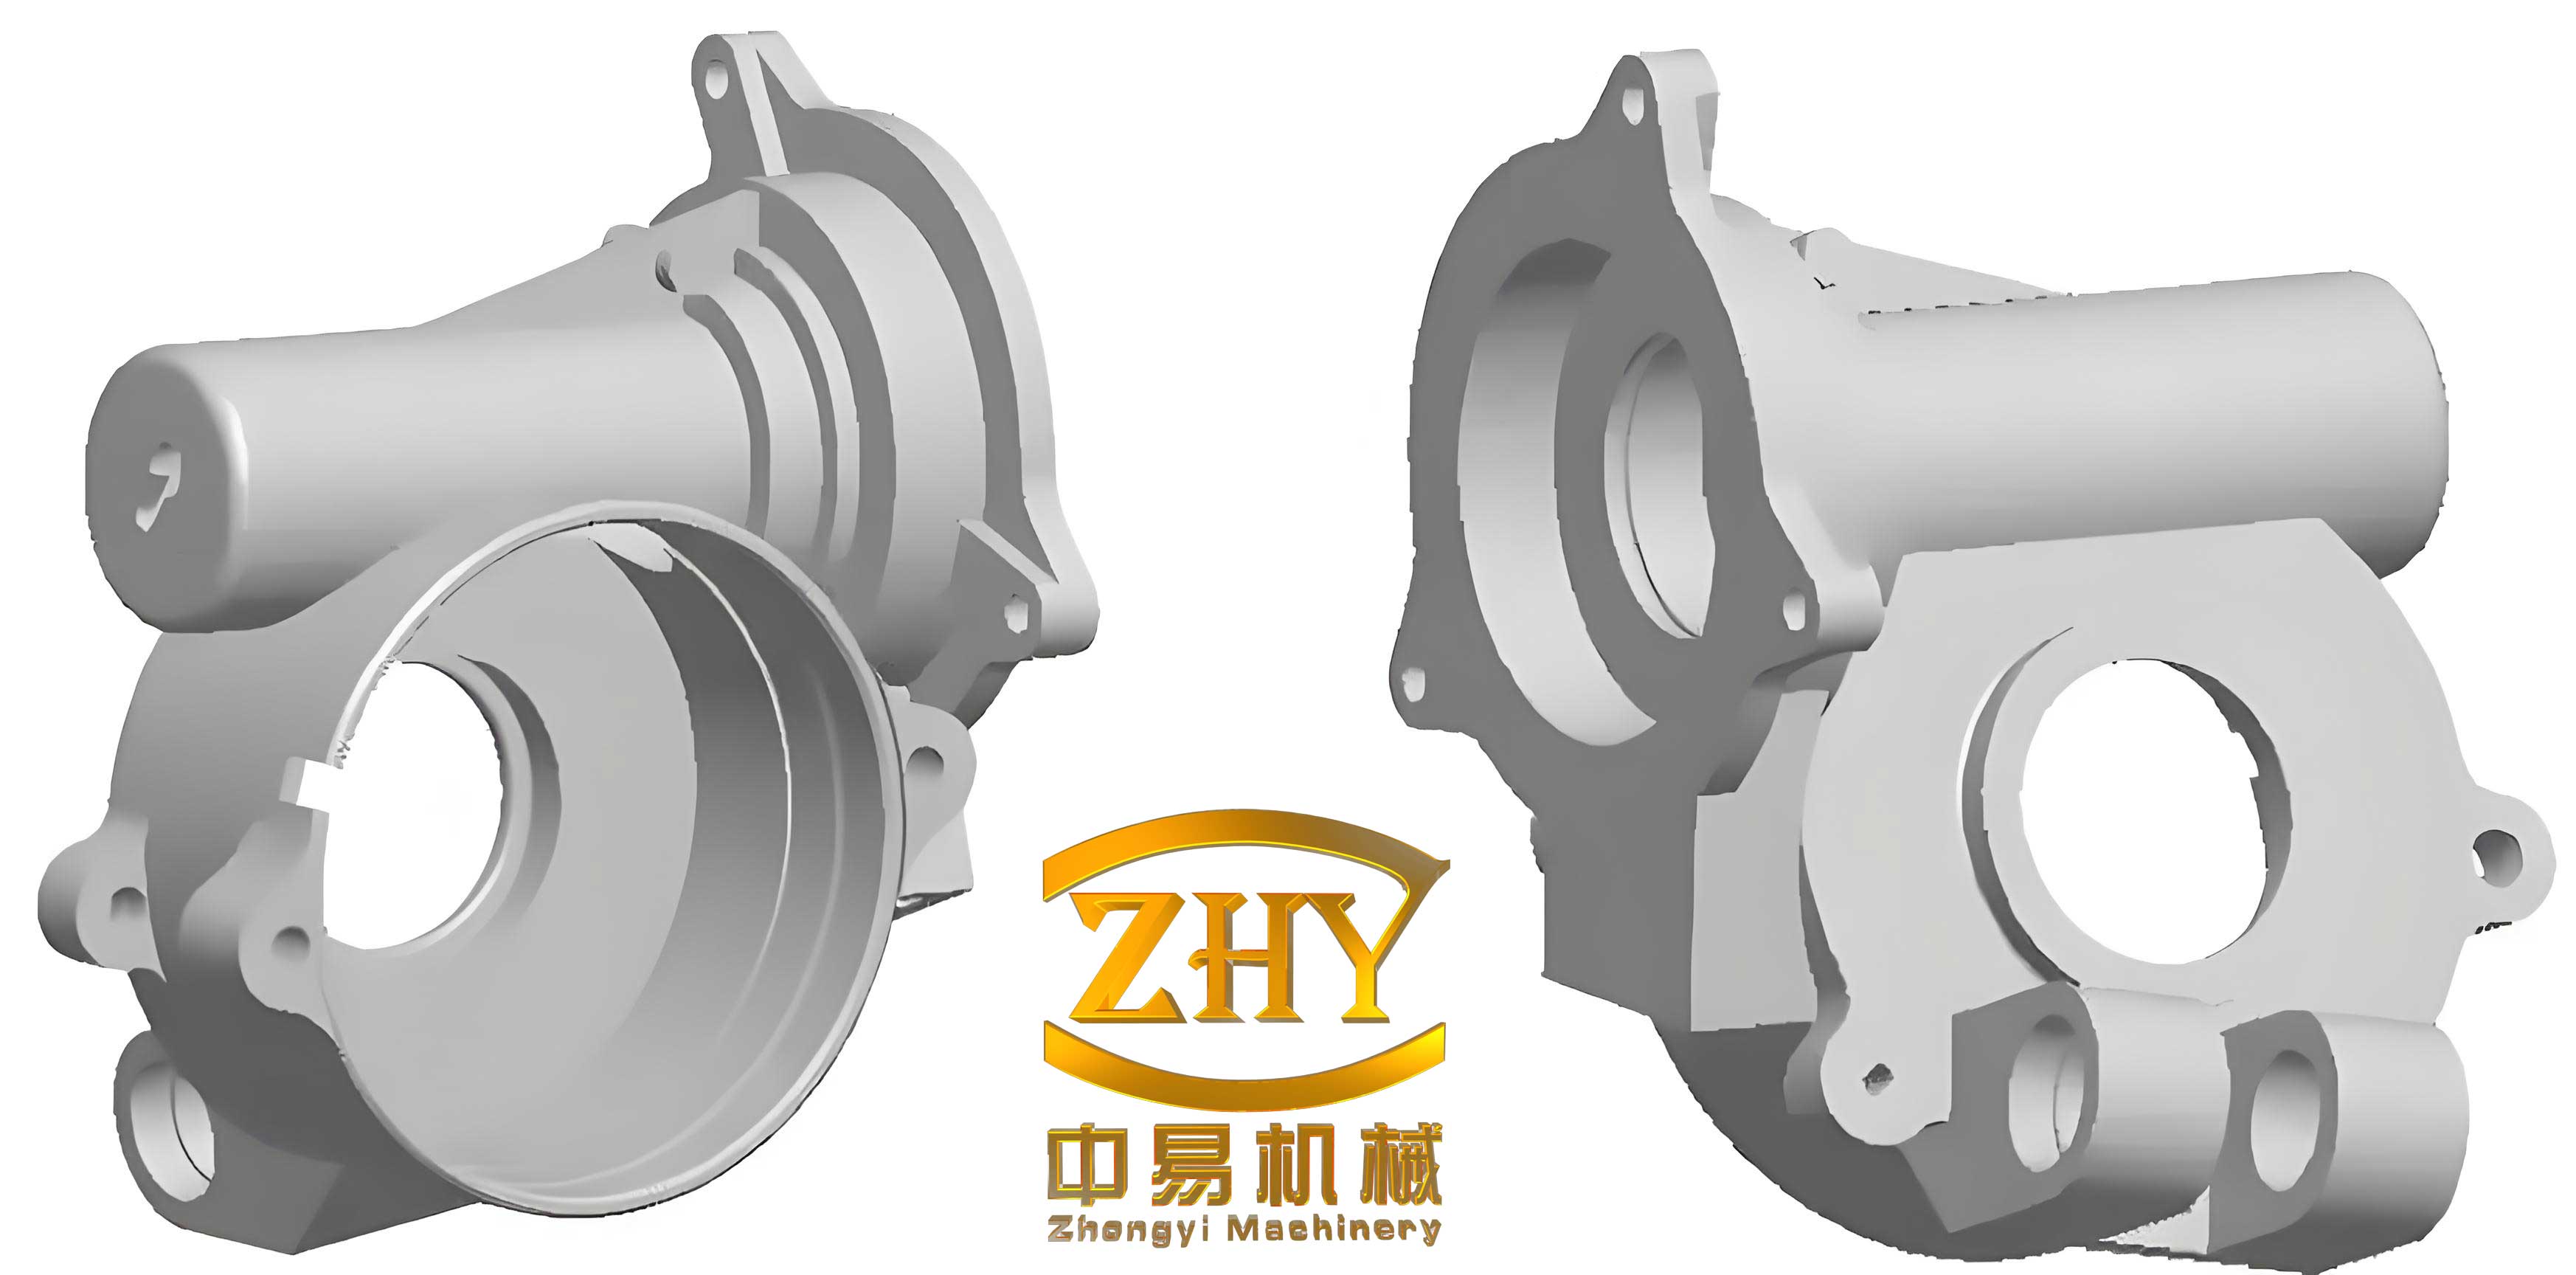
The geometry of the front housing is inherently complex, featuring numerous thin-walled sections, reinforcing ribs, and critical bearing bore surfaces. This complexity, while necessary for functional and weight requirements, makes the casting process a significant source of residual stress. During solidification and cooling, differential thermal contraction between thick and thin sections, hindered by the mold’s geometry (the sand core and mold walls), generates substantial thermal and mechanical stresses. These locked-in stresses, if not quantified and mitigated, become a latent source of distortion. Therefore, the first step in our investigation is to experimentally measure the post-casting residual stress state at key locations on the actual housing.
1. Experimental Characterization of Casting Residual Stress
To obtain a direct, quantitative assessment of the residual stress, we employed the non-destructive X-ray diffraction (XRD) method. This technique is ideal for shell castings as it causes no damage to the finished component. The underlying principle is based on Bragg’s law and the fact that elastic strain within the crystal lattice alters the interplanar spacing (d-spacing) of atomic planes, which in turn shifts the diffraction angle (θ) of a monochromatic X-ray beam. The relationship between the strain and the shift in diffraction angle is given by:
$$ \frac{\Delta d}{d_0} = -\cot \theta_0 \cdot \Delta \theta $$
where \(d_0\) and \(\theta_0\) are the stress-free lattice spacing and diffraction angle, respectively. By measuring the diffraction angle at multiple tilt angles (ψ) relative to the surface normal, the strain in a specific direction can be determined. Using Hooke’s law for the plane-stress condition (valid for surface measurements), the stress \(\sigma_{\phi}\) in direction φ on the surface is calculated as:
$$ \sigma_{\phi} = \frac{E}{(1+\nu)} \cdot \frac{\partial (\ln d_{\phi\psi})}{\partial (\sin^2 \psi)} $$
where \(E\) is Young’s modulus, \(\nu\) is Poisson’s ratio, and \(d_{\phi\psi}\) is the measured lattice spacing. A high-precision, mechanically articulated X-ray stress analyzer was used to ensure accurate positioning and measurement on the complex contours of the housing. Given the critical nature of bearing bores for subsequent assembly and function, and areas prone to stress concentration like sharp corners and section transitions, a total of 36 measurement points were strategically selected across the housing surface. The measured stress values at these points provided the crucial benchmark against which our simulation results would be validated.
2. Numerical Simulation of the Casting Process
While experimental measurement provides accurate data at discrete points, it cannot reveal the full-field residual stress distribution throughout the entire shell casting. Numerical simulation fills this gap, offering insights into stress concentration zones and the overall pattern of residual stress. We developed a coupled thermal-stress finite element model to simulate the entire casting process, including filling, solidification, cooling in the mold, and finally, shakeout and riser removal. The commercial software ANSYS, enhanced with custom material libraries for foundry alloys, served as our simulation platform.
The model encompassed all key components: the aluminum alloy casting, the sand mold and core, the gating system (pouring cup, sprue, runners), and the risers (feeders). A high-fidelity tetrahedral mesh was generated, with local refinement in regions of thin walls and geometric complexity to ensure solution accuracy. The thermophysical and mechanical properties of the alloy (density, specific heat, thermal conductivity, Young’s modulus, yield strength, thermal expansion coefficient) were defined as temperature-dependent functions to capture the material behavior from the liquid state down to room temperature. The critical boundary conditions included the heat transfer coefficients at the metal-mold interface and the mechanical constraints imposed by the sand mold, which restrict the free contraction of the casting.
The simulation proceeded in sequential stages:
1. Filling and Solidification: The initial liquid metal filling was modeled, followed by a fully coupled thermal-stress analysis of solidification and cooling within the mold. The stress evolution during this phase is driven by thermal gradients and the developing mechanical strength of the solidifying metal.
2. Shakeout and Riser Removal: After a simulated cooling period of approximately 10 hours (37,200 seconds), when the casting temperature was near ambient, the mechanical constraint of the sand mold was removed in the simulation. This was followed by a simulated cutting operation to remove the gating system and risers. These steps are critical as they represent significant changes in the boundary conditions, leading to stress redistribution.
The constitutive model for the stress analysis is based on a thermo-elasto-plastic formulation. The total strain increment \(\Delta \varepsilon^{total}\) is decomposed into elastic \(\Delta \varepsilon^{e}\), plastic \(\Delta \varepsilon^{p}\), and thermal \(\Delta \varepsilon^{th}\) components:
$$ \Delta \varepsilon^{total} = \Delta \varepsilon^{e} + \Delta \varepsilon^{p} + \Delta \varepsilon^{th} $$
The stress increment is related to the elastic strain increment by Hooke’s law, while plastic flow is governed by a temperature-dependent yield criterion and flow rule. The simulation solves the equilibrium equations iteratively at each time step:
$$ \int_V \mathbf{B}^T \sigma \, dV = 0 $$
where \(\mathbf{B}\) is the strain-displacement matrix and \(\sigma\) is the Cauchy stress tensor.
| Simulation Stage | Key Physics Modeled | Primary Stress Generation Mechanism |
|---|---|---|
| Filling & Solidification | Fluid flow, Heat transfer, Phase change, Thermo-mechanical stress | Differential cooling & thermal contraction restrained by mold. |
| Cooling in Mold | Heat transfer, Creep (at high T), Thermo-elasto-plastic stress | Continued non-uniform cooling and constraint. |
| Shakeout | Removal of mold/core mechanical constraint | Sudden release of external constraint, leading to stress rebalance. |
| Riser Removal | Material removal simulation (element death) | Additional rebalancing of internal stresses due to changed geometry. |
3. Simulation Results and Correlation with Experiment
The simulation results revealed a highly non-uniform residual stress field within the shell casting. The stress distribution after shakeout and riser removal showed distinct patterns. High tensile stress concentrations, often exceeding 100 MPa, were predicted at several locations:
- Internal corners and sharp geometric transitions where stress naturally concentrates.
- Areas adjacent to thick sections (like mounting bosses) that cool slower than surrounding thin walls.
- Regions that were heavily constrained by the sand core during cooling.
The bulk of the housing exhibited stresses in the range of 0 to 130 MPa, but with significant gradients. This inhomogeneity is a key risk factor for distortion, as any subsequent material removal (machining) or heating in service can trigger an uneven release of these locked-in stresses, leading to geometric changes.
The credibility of the simulation hinges on its ability to match physical reality. Therefore, we directly compared the simulated residual stress values at the 36 measurement points with the experimentally obtained XRD data. The correlation plot showed a promising agreement. The majority of data points clustered around the line of perfect agreement, and crucially, the simulation successfully captured the overall spatial trends of high and low-stress regions across the housing. To quantify the agreement, we calculated the relative deviation between the simulated (\( \sigma_{sim} \)) and experimental mean (\( \bar{\sigma}_{exp} \)) values for each point:
$$ \text{Relative Deviation} = \frac{|\sigma_{sim} – \bar{\sigma}_{exp}|}{\bar{\sigma}_{exp}} \times 100\% $$
A statistical analysis of these deviations confirmed the model’s reliability:
| Relative Deviation Range | Percentage of Measurement Points | Assessment |
|---|---|---|
| 0% – 10% | ~45% | Excellent Agreement |
| 10% – 20% | ~30% | Good Agreement |
| 20% – 30% | ~15% | Acceptable Agreement |
| > 30% | ~10% | Discrepancy (often at complex local features) |
With approximately 75% of points showing a deviation of less than 20%, the simulation model is validated as a reliable tool for predicting the residual stress state in these complex shell castings. The discrepancies are attributed to localized microstructural variations, slight differences between the ideal CAD model and the actual cast part, and the inherent challenges in precisely aligning measurement and simulation points on complex curvature.
4. Optimization: Thermal-Spectral Harmonic Stress Relief
Armed with a validated understanding of the problematic residual stress state, the next objective was to actively reduce and homogenize these stresses before the component enters service. Traditional thermal aging (annealing) can be effective but is time-consuming, energy-intensive, and may adversely affect the material’s temper. We instead applied an advanced mechanical stress relief technique known as Thermal-Spectral Harmonic (TSH) processing. This method combines the benefits of controlled heating with the application of specific vibratory loads.
The underlying principle of TSH processing is to superimpose a dynamic, cyclic mechanical load on the component while it is held at an elevated temperature (below the aging temperature of the alloy). The combined thermal and mechanical energy input reduces the material’s yield strength and provides the driving force for localized micro-plastic deformation in regions of high residual stress. This allows the locked-in elastic strains to be converted into permanent plastic strains, thereby lowering the overall residual stress magnitude and promoting a more uniform distribution. The “spectral” aspect involves using a Fast Fourier Transform (FFT) analysis of the component’s geometry to identify its inherent resonant frequencies. Excitation at these specific harmonic frequencies ensures efficient energy transfer throughout the complex structure of the shell casting, effectively reaching and treating stress concentrations in thin webs and deep cavities that might be shielded in simpler vibratory treatments.
The process can be conceptually related to a dynamic relaxation model. The applied oscillatory stress \(\sigma_{app}(t)\) interacts with the residual stress field \(\sigma_{res}\). When the combined stress in a local region exceeds the thermally reduced yield strength \(\sigma_y(T)\), plastic flow occurs, reducing the local residual stress. The effectiveness can be parameterized by a stress reduction factor.
The front housing was subjected to a tailored TSH cycle. The residual stress was measured again at the same 36 locations using XRD after the treatment. The results demonstrated a clear and significant reduction in stress levels across the board. The quantitative summary is presented below:
| Residual Stress Metric | Before TSH Processing | After TSH Processing | Reduction/Homogenization |
|---|---|---|---|
| Mean Stress (MPa) | 54.7 | 42.6 | 22.2% Decrease |
| Peak Stress (MPa) | 66.6 | 57.9 | 13.1% Decrease |
| Standard Deviation (MPa) | 8.4 | 7.2 | 14.3% Decrease (Improved Homogeneity) |
The reduction in the mean stress by over 22% is particularly noteworthy. This translates directly to a lower driving force for in-service distortion. The decrease in standard deviation indicates a more uniform stress field, further mitigating the risk of uneven distortion. The optimization successfully lowered the stored elastic energy within the shell casting.
5. Discussion and Implications for Distortion Control
This integrated study underscores the critical importance of proactively managing residual stresses in large, thin-walled shell castings for high-precision applications. The simulation revealed that the as-cast state is characterized by a highly non-uniform tensile stress field with localized concentrations that act as latent sources for distortion. The validation of the simulation against experimental data provides engineers with a powerful predictive tool. This tool can be used not only for diagnosis but also for the virtual prototyping of casting processes—optimizing gating and riser design, cooling conditions, and mold stiffness to minimize residual stress formation from the outset.
The successful application of Thermal-Spectral Harmonic processing demonstrates a highly effective post-casting mitigation strategy. The significant reduction in both the magnitude and dispersion of residual stress directly addresses the root cause of the distortion problem. For critical components like accessory gearbox housings, incorporating such a validated stress-relief step into the manufacturing sequence is essential for ensuring dimensional stability throughout the engine’s operational life.
The framework established here—combining advanced non-destructive measurement, predictive multi-physics simulation, and targeted mechanical optimization—forms a robust methodology for the design and manufacture of dimensionally stable cast components. Future work will involve using the validated model to simulate the impact of machining sequences on stress redistribution and final part geometry, enabling a true “first-part-correct” manufacturing approach for complex shell castings.