
In my experience as a foundry engineer, tackling the production of intricate thin-wall aluminum alloy parts through sand casting has been both a challenge and a rewarding endeavor. The specific component in focus is a filter plate, originally fabricated from stainless steel in imported equipment, which we successfully converted to a sand-cast aluminum alloy piece. This transition was driven by the need to maintain overall machine weight and strength while overcoming forming difficulties. The filter plate features numerous solid hemispherical protrusions and has stringent requirements: maximum wall thickness, minimum wall thickness, and a web thickness. Through detailed process analysis, we identified several critical hurdles in sand casting this component, leading to the development of an optimized sand casting methodology that significantly improved outcomes.
The primary difficulties in sand casting such complex thin-wall aluminum alloy parts stem from their geometry and material properties. First, the large contour dimensions combined with thin walls result in rapid cooling rates, which hinder proper mold filling. This often leads to defects like cold shuts and misruns in sand castings. Second, the use of sand molds and cores, especially when green sand and dry cores are involved, generates substantial gases during pouring. These gases can cause issues such as blowholes, gas shrinkage porosity, mold wall movement, and runouts. Third, the non-uniform relative thickness in local areas induces significant casting stresses. The thin walls and complex shape make the sand castings highly prone to deformation, complicating dimensional accuracy. These challenges underscore the importance of meticulous process design in sand casting operations.
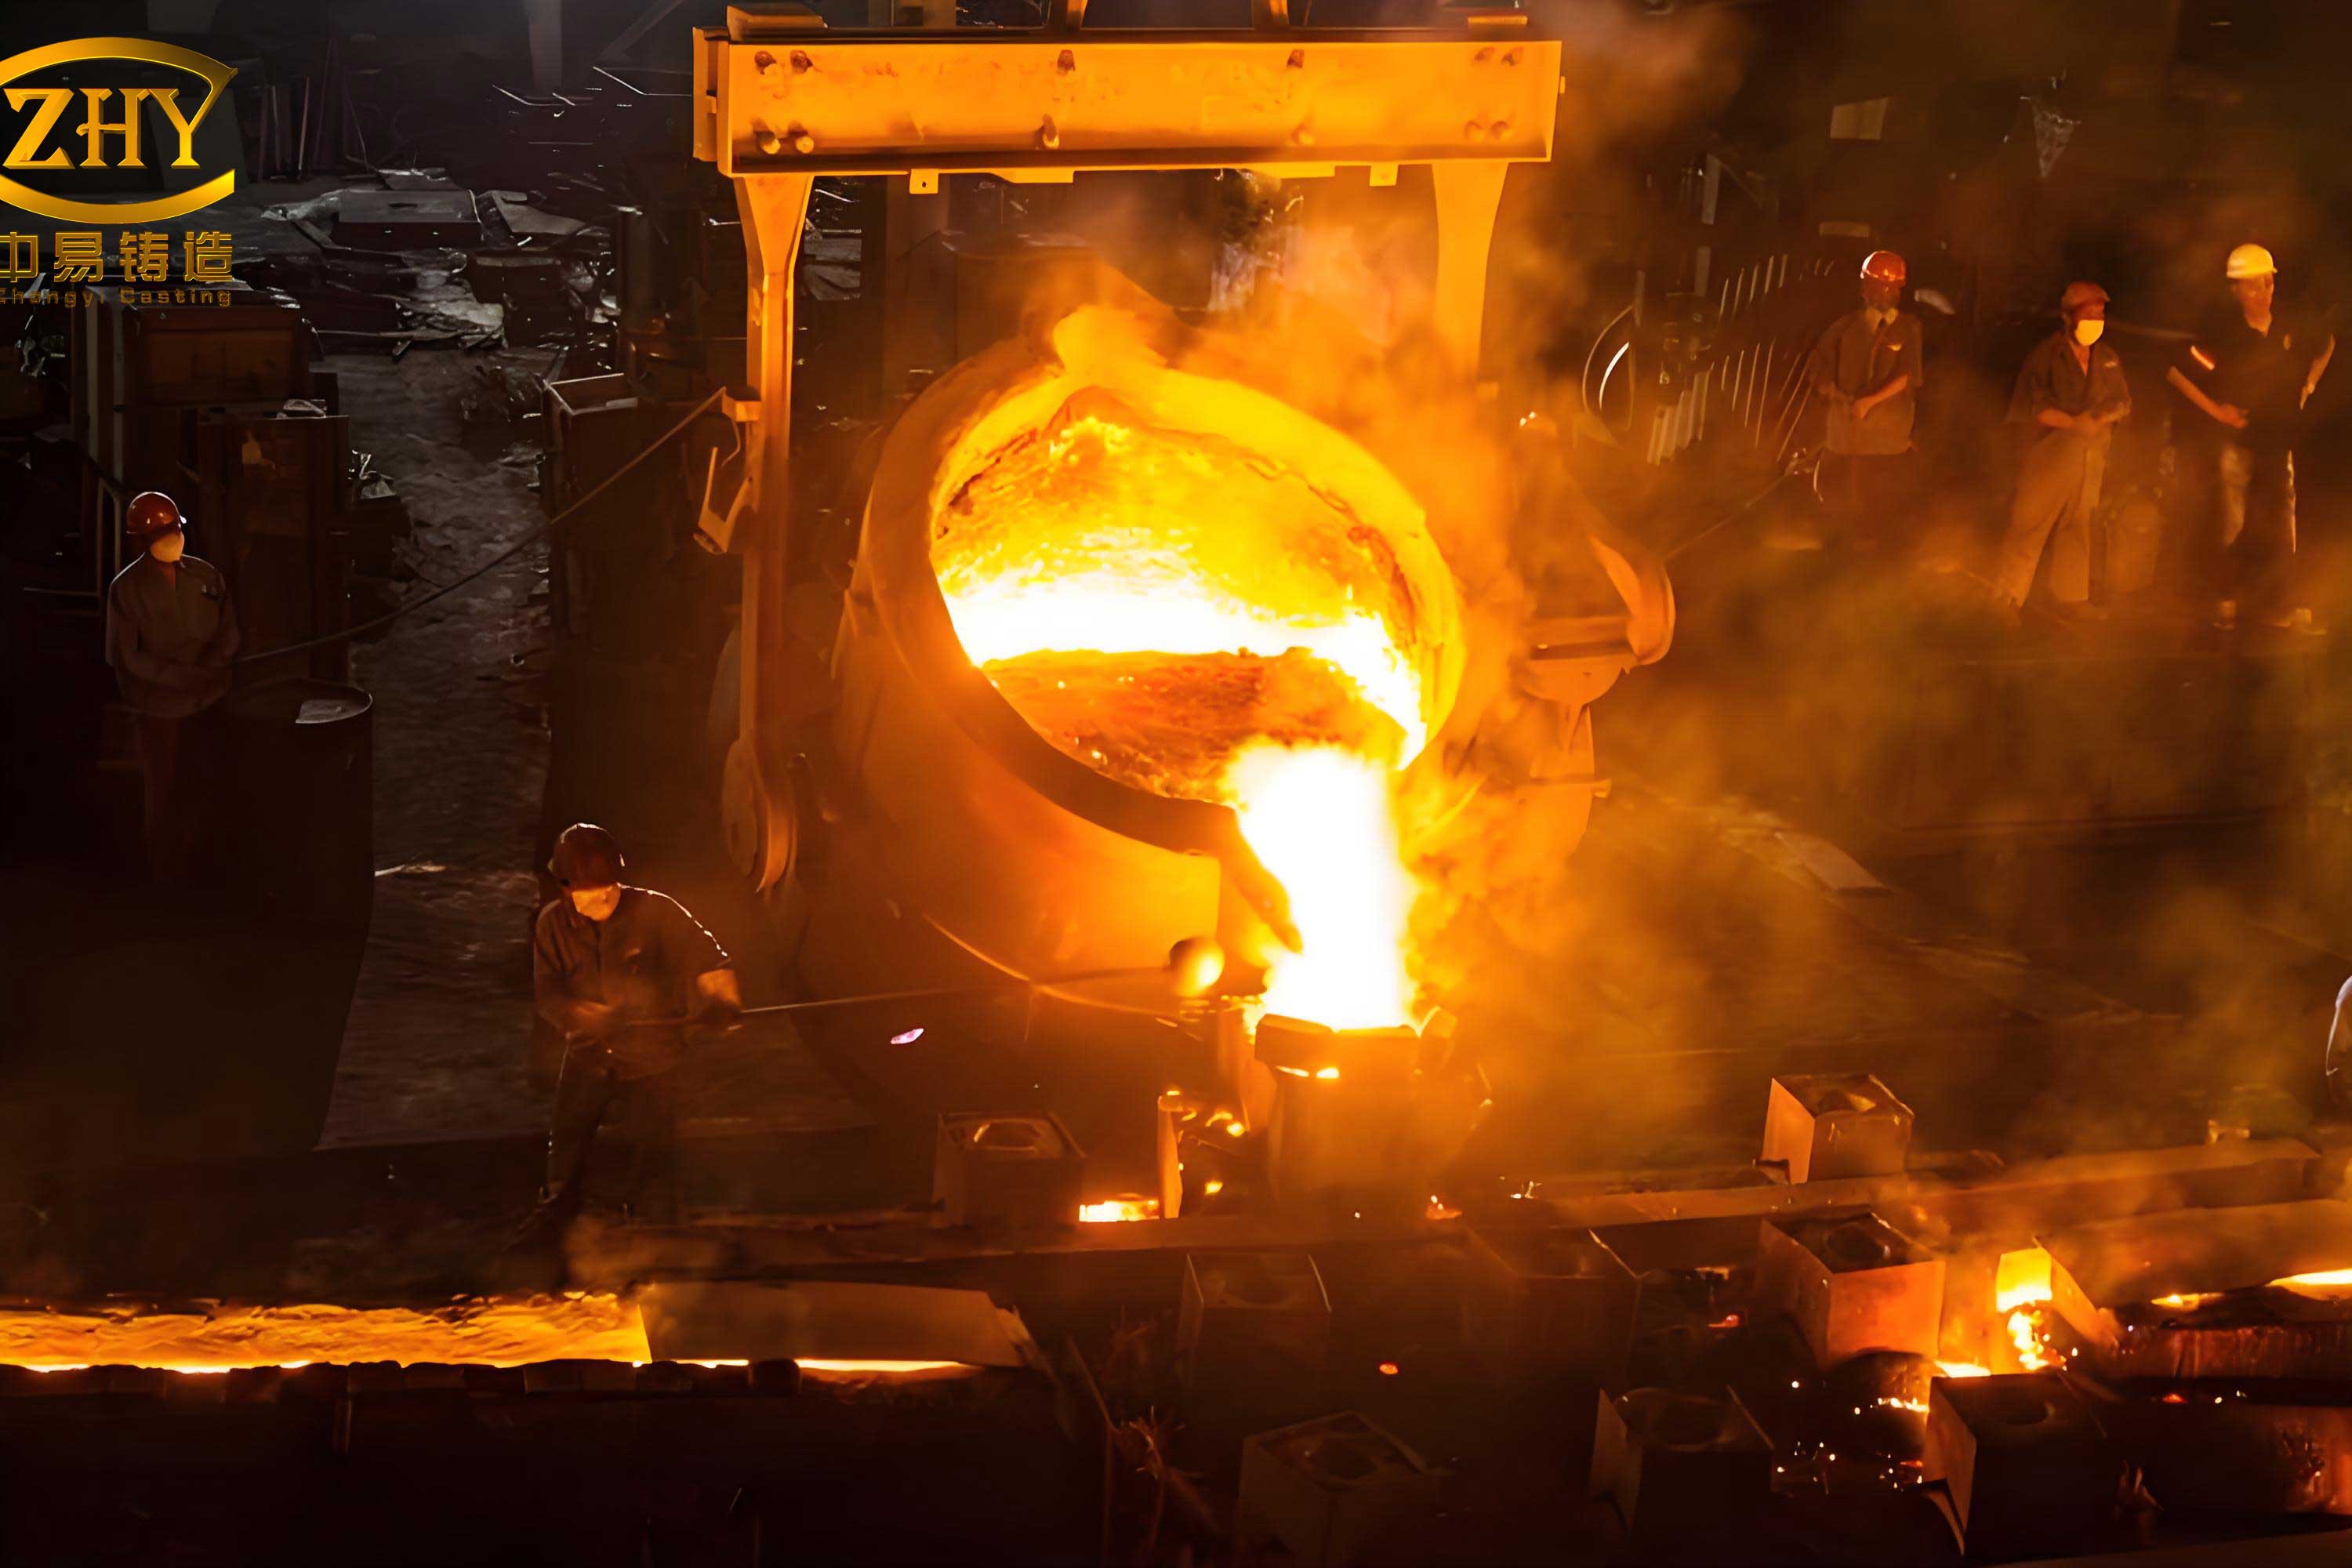
To address these issues, we devised a comprehensive sand casting process scheme. The method employs conventional green sand molds for the cope and drag, combined with dry sand cores. This hybrid approach balances mold strength and gas permeability. The molding assembly involves a flat cope with reserved cavities to facilitate core and mold venting. Cores are suspended within the mold cavity, and multiple vent risers are strategically placed to ensure gas evacuation during pouring. For alignment, a simple wooden pin system is used in the drag, allowing visual inspection to prevent mismatch defects. After closing the mold, weighting is applied to counter buoyancy forces. The mold surfaces are coated with talc powder to enhance surface finish, a common practice in sand castings to reduce metal penetration and improve release.
Crucial to the success of sand castings is the control of pouring parameters. For the aluminum alloy used, the pouring temperature is maintained between 680°C and 720°C. The pouring time is critical and calculated based on the gating system design. We adopted a bottom-gating system with two spruce runners to ensure smooth metal flow and minimize turbulence. The diameter of each spruce is designed to optimize filling, and the pouring time is determined using fluid dynamics principles. The relationship can be expressed through the following formula for flow rate:
$$ Q = A \cdot v $$
where \( Q \) is the volumetric flow rate, \( A \) is the cross-sectional area of the spruce, and \( v \) is the flow velocity. For sand castings, the average pressure head \( H \) influences the velocity, given by Torricelli’s law adapted for foundry applications:
$$ v = C_d \sqrt{2gH} $$
Here, \( C_d \) is the discharge coefficient, and \( g \) is gravitational acceleration. The pouring time \( t \) is then:
$$ t = \frac{V}{Q} = \frac{V}{A \cdot C_d \sqrt{2gH}} $$
where \( V \) is the volume of the casting. In our case, with two spruces, the total flow area doubles, reducing pouring time. We set the pouring time between 8 to 12 seconds to balance mold filling and cooling rates. The table below summarizes key pouring parameters for these sand castings:
| Parameter | Value | Unit |
|---|---|---|
| Pouring Temperature | 680 – 720 | °C |
| Spruce Diameter (each) | 20 | mm |
| Number of Spruces | 2 | – |
| Calculated Pouring Time | 8 – 12 | seconds |
| Average Pressure Head | 150 | mm |
After pouring, the sand castings are allowed to cool in the mold for a specified duration to solidify sufficiently without excessive stress. We cool for approximately 30 minutes before shakeout. Upon removal, the castings are cleaned and inspected for web deformation. If distortion exceeds a tolerance of 0.5 mm across a flat reference plane, corrective straightening is performed using precision tools. This post-casting treatment ensures dimensional stability in thin-wall sand castings.
The economic benefits of this optimized sand casting process are substantial. By adopting sand casting instead of alternative methods like die casting or stamping, we saved significant tooling costs. The initial investment for die casting molds or punch dies would have been prohibitively high, whereas sand casting utilizes reusable patterns and cores. Moreover, the implementation of suspended core techniques replaced earlier methods where cores were placed in the drag, enhancing yield and reducing scrap rates. The table below illustrates the economic impact:
| Aspect | Before Optimization | After Optimization | Improvement |
|---|---|---|---|
| Scrap Rate | 40% – 50% | 5% | Reduction of 35-45 percentage points |
| Tooling Cost Savings | 0 | Approx. 50,000 USD | Significant capital avoidance |
| Labor and Material Efficiency | Low | High | Enhanced productivity |
These improvements highlight the cost-effectiveness of refined sand casting processes for complex components. The reduction in scrap directly translates to lower material waste and rework efforts, making sand castings more sustainable and economical.
From a technical perspective, the gating system plays a pivotal role in determining the quality of sand castings, especially when using resin-bonded sands. Its function is to regulate the temperature field during solidification and modify the solidification mode. For thin-wall high-strength gray iron castings, a stepped or dispersed intermediate injection system with high flow rates is optimal to prevent subsurface gas defects. This principle applies similarly to aluminum sand castings. The low pouring temperature filling into resin sand molds, which have high gas evolution and low permeability, is a primary cause of subsurface porosity in sand castings. Additionally, the coincidence of physical and geometric hot spots, coupled with mold wall movement, leads to shrinkage porosity. Therefore, designing gating systems that promote directional solidification and venting is crucial.
To further elaborate on the science behind sand castings, let’s consider the heat transfer dynamics. The solidification time \( t_s \) for a sand casting can be estimated using Chvorinov’s rule:
$$ t_s = k \left( \frac{V}{A} \right)^n $$
where \( V \) is the volume, \( A \) is the surface area, \( k \) is a constant dependent on mold material and metal properties, and \( n \) is an exponent typically around 2. For thin-wall sand castings, the high surface area-to-volume ratio accelerates cooling, necessitating faster pouring. The modulus \( M = V/A \) is a key parameter; lower modulus indicates faster solidification. The table below compares moduli for different sections of our filter plate sand casting:
| Section | Volume (cm³) | Surface Area (cm²) | Modulus (cm) |
|---|---|---|---|
| Web | 15.2 | 120.5 | 0.126 |
| Hemispherical Protrusion | 0.65 | 3.14 | 0.207 |
| Overall Casting | 250.0 | 800.0 | 0.313 |
This data shows that the web, being thinnest, has the lowest modulus, explaining its susceptibility to cold shuts. To counter this, we increased the pouring temperature slightly within the range to extend fluidity. Moreover, the gating system design ensures that metal enters from the bottom, reducing turbulence and air entrapment, which is vital for defect-free sand castings.
Another critical aspect is the sand properties. In sand castings, the mold sand must have adequate strength, permeability, and refractoriness. We use a blend of silica sand with clay binders for green sand, and resin-bonded sand for cores. The permeability \( P \) is measured in standard units and affects gas escape. It can be quantified as:
$$ P = \frac{C \cdot h \cdot A}{t \cdot \Delta p} $$
where \( C \) is a constant, \( h \) is the sample height, \( A \) is cross-sectional area, \( t \) is time, and \( \Delta p \) is pressure difference. For our sand castings, we maintain permeability above 100 to prevent gas-related defects. Core sands are baked to remove moisture and volatiles, reducing gas evolution. The table summarizes sand mix properties:
| Sand Type | Permeability | Green Strength (kPa) | Moisture Content (%) |
|---|---|---|---|
| Green Sand (Mold) | 110 – 130 | 70 – 90 | 3.5 – 4.5 |
| Resin Sand (Core) | 140 – 160 | >200 (after curing) | < 0.5 |
The success of these sand castings also relies on process monitoring. We implement statistical process control (SPC) to track key variables such as pouring temperature, sand compactness, and cooling time. Control charts help maintain consistency across production batches. For instance, the X-bar chart for pouring temperature ensures it stays within limits, reducing variability in sand casting quality. The formula for calculating control limits is:
$$ \text{UCL} = \bar{X} + A_2 \bar{R}, \quad \text{LCL} = \bar{X} – A_2 \bar{R} $$
where \( \bar{X} \) is the sample mean, \( \bar{R} \) is the average range, and \( A_2 \) is a constant. This systematic approach minimizes defects and enhances repeatability in sand castings.
In terms of metallurgy, the aluminum alloy used is akin to A356, with silicon and magnesium additions for fluidity and strength. The solidification sequence involves the formation of α-Al dendrites and eutectic phases. Rapid cooling in thin sections can lead to finer microstructures, which improve mechanical properties. However, it also increases thermal gradients and stress. We perform heat treatment, such as T6 tempering, to relieve stresses and enhance hardness. The yield strength \( \sigma_y \) of the sand castings after heat treatment can be approximated by:
$$ \sigma_y = \sigma_0 + k \cdot d^{-1/2} $$
where \( \sigma_0 \) is a base strength, \( k \) is a constant, and \( d \) is the grain size. Finer grains from fast cooling in sand castings contribute to higher strength, aligning with our weight and strength requirements.
Looking at broader applications, the principles developed here for thin-wall aluminum sand castings can be extended to other non-ferrous alloys and complex geometries. Sand casting remains a versatile and cost-effective method for low to medium volume production. Innovations like 3D-printed sand molds are emerging, but traditional sand castings still dominate due to their flexibility and low tooling cost. Our experience demonstrates that with careful design, sand castings can achieve precision and quality comparable to more expensive processes.
To conclude, the sand casting of complex thin-wall aluminum alloy components requires a holistic approach addressing design, process, and material factors. Key takeaways include the importance of gating system design in regulating thermal fields, the need for adequate venting to mitigate gas defects, and the management of solidification stresses to prevent deformation. Economic analyses confirm significant savings through process optimization, with scrap rates plummeting from over 40% to just 5%. These outcomes validate sand casting as a viable and efficient manufacturing route for intricate parts. Future work may explore advanced simulation tools to further refine gating and risering designs, pushing the boundaries of what is achievable with sand castings. Ultimately, the journey from stainless steel to aluminum sand castings has not only met technical specifications but also delivered substantial economic benefits, underscoring the enduring relevance of sand casting in modern manufacturing.