
Hydraulic components such as valve bodies, pump casings, and covers represent a category of precision, high-pressure castings. They are characterized by stringent dimensional accuracy requirements and complex internal geometries featuring intricate, often interconnecting, oil galleries and cavities. The internal surfaces of these passages must be free from defects like sand inclusion, burn-on, and oxide scale to ensure reliable performance in hydraulic systems. Traditional production methods, such as those employing green sand molding with resin-bonded cores, often struggle to meet these demands consistently. These conventional processes can result in lower dimensional precision, poor surface finish, difficulties in core removal from internal passages, and relatively high production costs.
The lost foam casting process presents a compelling alternative for manufacturing such components. This method utilizes an expendable foam pattern, which is entirely encapsulated in unbonded sand and vaporized during the pouring of molten metal under a partial vacuum. The absence of parting lines, core boxes, and the need for mold assembly contributes to exceptional dimensional repeatability. Furthermore, the application of a refractory coating directly onto the foam pattern enables the production of castings with superior surface finish. The inherent characteristics of the lost foam casting process—dimensional accuracy, surface quality, and the ability to form complex internal features without cores—make it theoretically ideal for hydraulic parts. However, the specific structural nature of these castings, combined with the unique solidification and formation dynamics of lost foam, introduces distinct challenges that must be systematically addressed to achieve success.
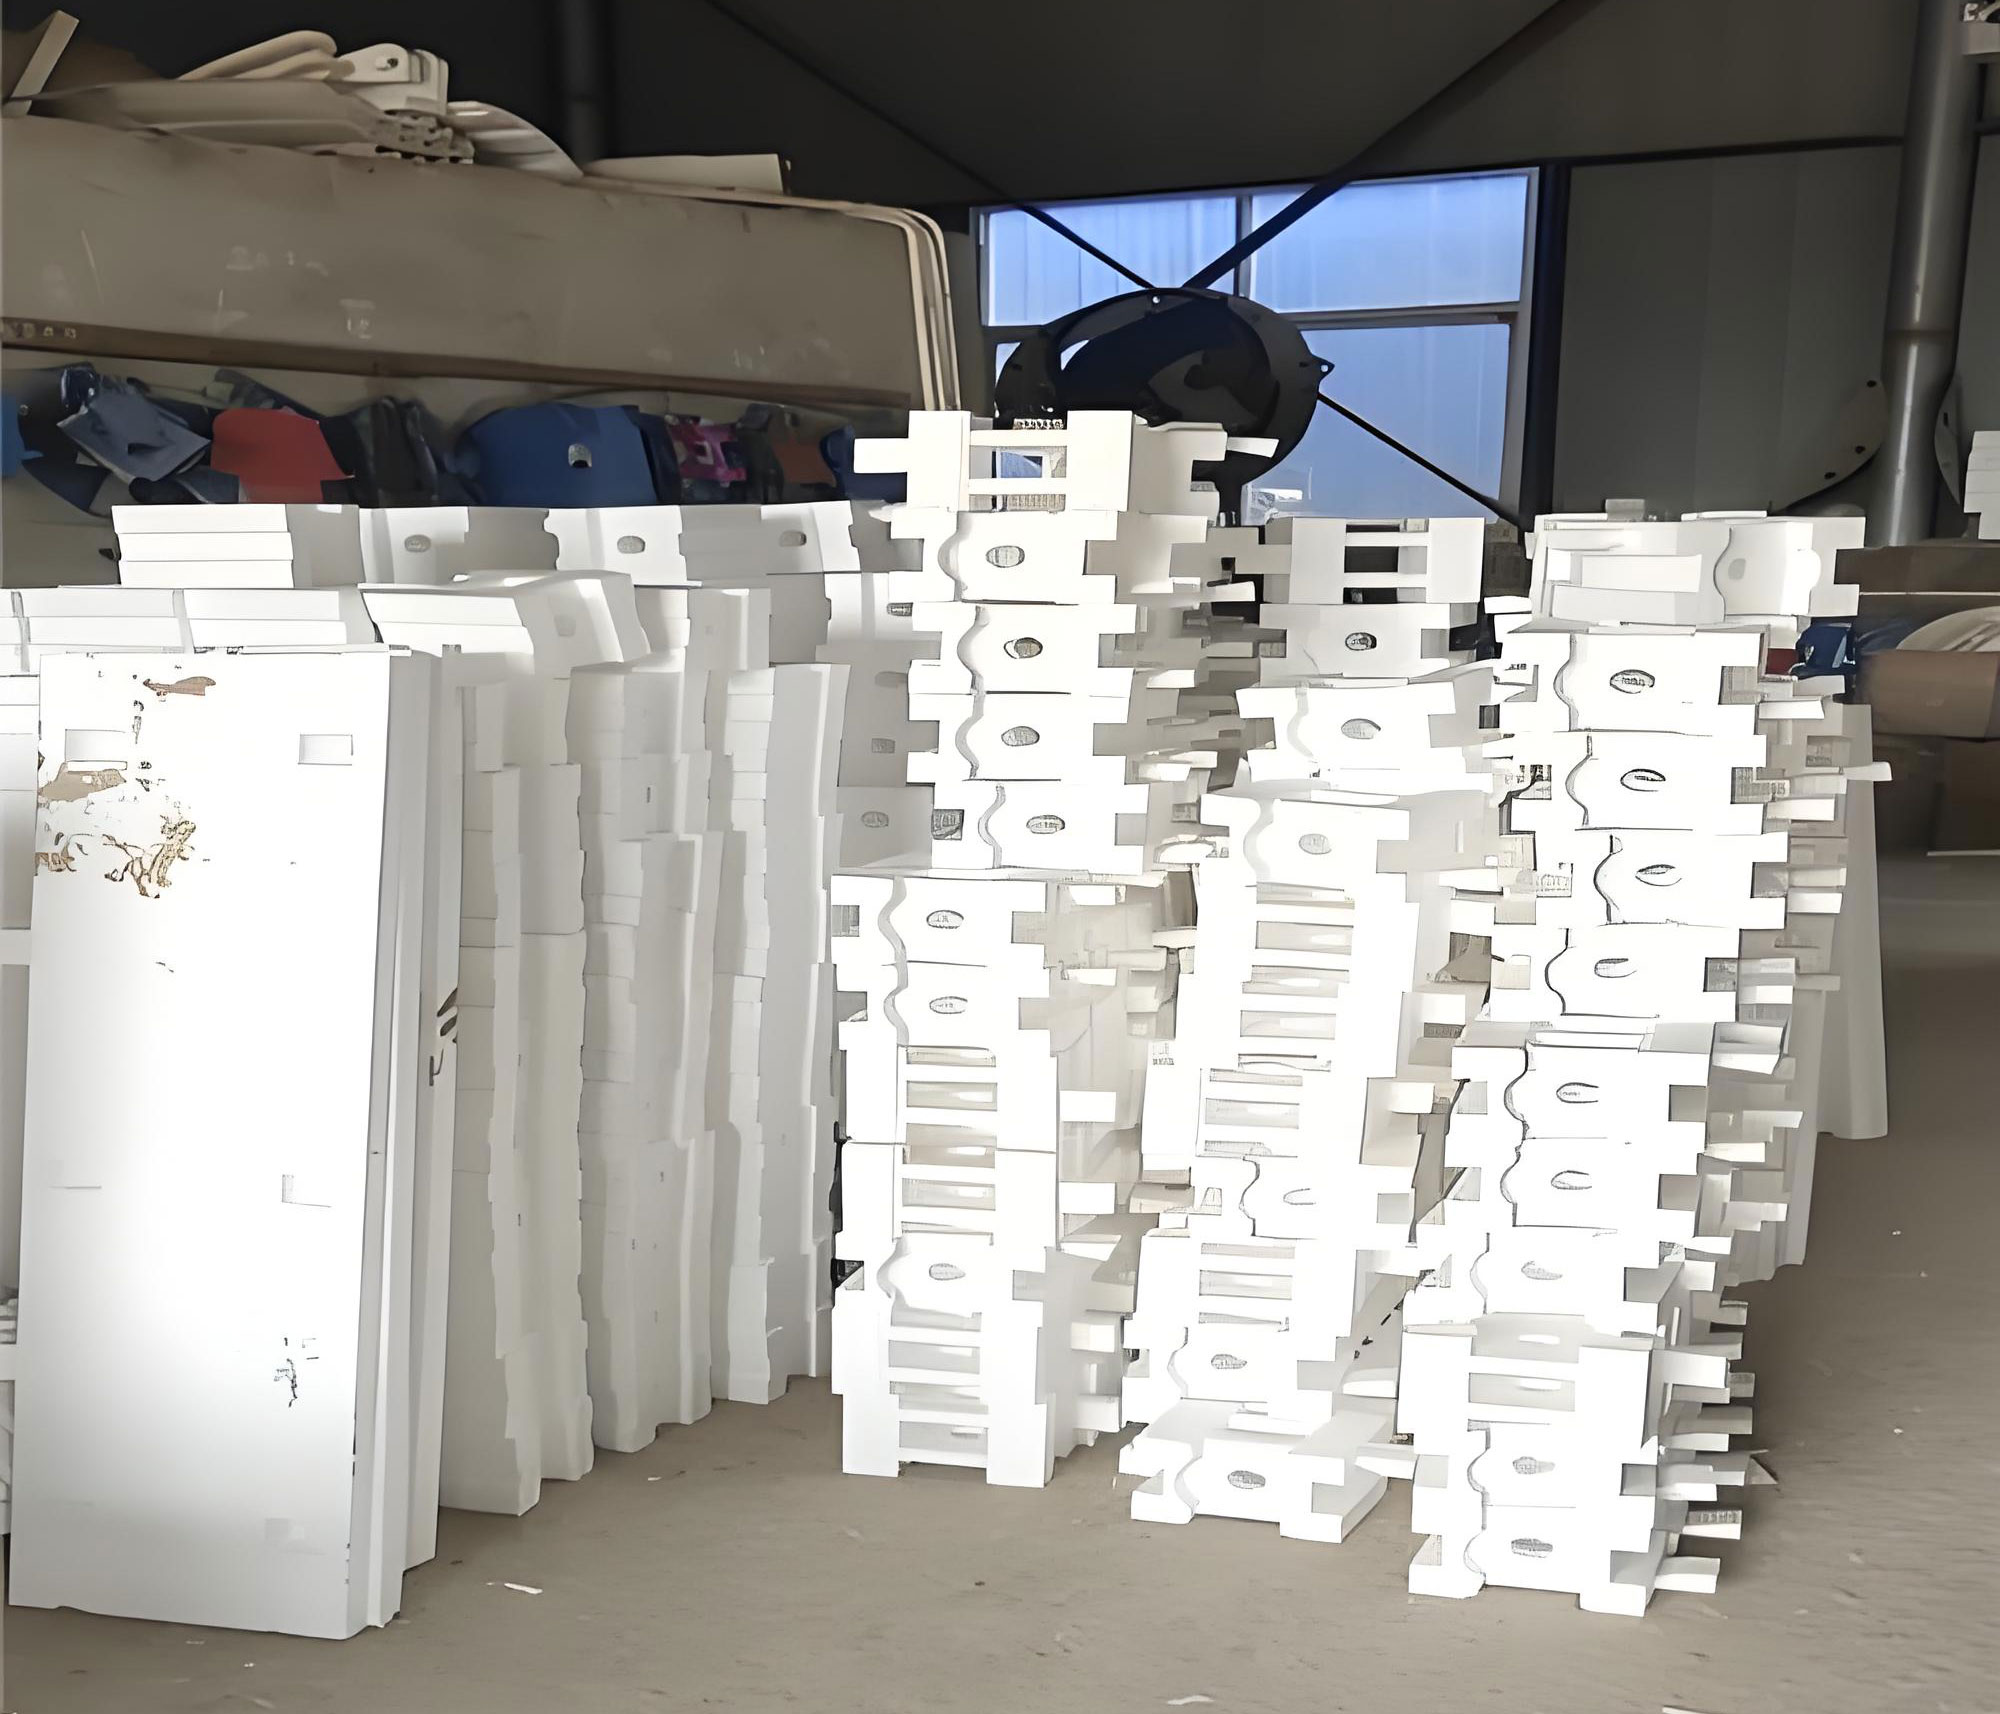
Structural Challenges and Casting Difficulties in Lost Foam
Typical hydraulic components are square or rectangular thick-walled parts with central bore holes. Weights commonly range from 6 to 9 kg, with a nominal wall thickness around 30 mm. The primary complexity arises from the internal network of narrow oil galleries, some of which may be separated by thin septa as slim as 2-3 mm. This extreme variation in section thickness—from 30 mm down to 2-3 mm—poses the first major challenge for the lost foam casting process. It complicates the selection of an appropriate raw foam bead size and final pattern density that can faithfully replicate both the thick sections and the extremely thin features without distortion or poor surface formation.
For thick-section iron castings produced via the lost foam casting process, the high volume-to-surface area (V/S) ratio, or modulus, is a critical factor. A large modulus means a smaller relative surface area through which the thermal degradation products of the foam can escape. Consequently, these gaseous and liquid pyrolysis residues become concentrated. In gray iron castings like HT300, this often manifests as lustrous carbon defects or folds (wrinkles) on the upper surfaces of the casting, where the residues finally coalesce and become entrapped.
Furthermore, the slow solidification inherent to thick sections cast in unbonded sand aggregates allows prolonged contact between the molten iron and the refractory coating, especially within the fine oil passages. Under the influence of the applied vacuum, this can lead to severe mechanical and chemical penetration, resulting in burn-in defects that are extremely difficult to remove. Therefore, a holistic approach optimizing every stage—from pattern material selection and gating design to coating formulation, sand compaction, and pouring parameters—is essential to harness the full potential of the lost foam casting process for high-quality HT300 hydraulic components.
Pattern Material and Bead Selection Strategy
The properties of the expendable foam pattern are fundamental to the success of the lost foam casting process. Two key factors are density and material composition.
Pattern Density and Bead Size: Pattern density directly influences both surface finish and the propensity for carbonaceous defects. A higher density yields a smoother pattern surface and thus a better casting finish, but it increases the mass of carbonaceous residue, elevating the risk of folds and carbon inclusions. Conversely, a lower-density pattern reduces carbon defects but may compromise surface detail. Density is primarily controlled by the size of the original expandable polystyrene (EPS) or copolymer beads. A general rule for the lost foam casting process is that the bead diameter should not exceed one-tenth of the casting’s minimum wall thickness, ensuring at least three beads are present across any thin section.
For a main wall of 30 mm, a bead size of 0.8-1.0 mm is suitable, producing a pattern density of approximately 0.018-0.020 g/cm³. However, for sections as thin as 2-3 mm, a much finer bead in the range of 0.2-0.3 mm is required, resulting in a pattern density of 0.029-0.031 g/cm³. A compromise must be struck. A target pattern density of 0.025-0.027 g/cm³ is often selected, which remains on the higher side for iron casting, necessitating compensatory measures in other process stages to control defects. The relationship can be conceptualized by the following expression for achievable minimum wall thickness ($t_{min}$):
$$ t_{min} \approx n \cdot d_{bead} $$
where $d_{bead}$ is the average expanded bead diameter and $n$ is the minimum number of beads required across a section (typically $n \geq 3$).
Pattern Material Composition: The choice of pattern polymer is critical for controlling carbon defects. Standard expandable polystyrene (EPS) is cost-effective but has a high carbon content (92 wt.%), leading to significant liquid and solid residue during decomposition. Expandable polymethyl methacrylate (EPMMA) has a much lower carbon content (~60 wt.%) and produces less residue, but it generates a larger volume of gas and is more expensive. An effective solution for the lost foam casting process of gray iron is to use a copolymer blend, typically consisting of 70% EPMMA and 30% EPS. This hybrid material reduces the overall carbon load compared to pure EPS while mitigating the high gas generation and cost of pure EPMMA.
| Material | Carbon Content (approx.) | Gas Generation | Liquid Residue | Relative Cost | Suitability for HT300 |
|---|---|---|---|---|---|
| EPS | 92% | Medium | High | Low | Poor (High carbon defect risk) |
| EPMMA | 60% | Very High | Low | High | Good, but high gas & cost |
| EPS/EPMMA Copolymer (30/70) | ~70% | Medium-High | Medium-Low | Medium | Optimal Balance |
Gating System Design Philosophy
Gating design in the lost foam casting process must accommodate the need to remove pattern degradation products. For many castings, a bottom-gating system is preferred as it promotes tranquil mold filling. Initial trials with bottom-gated HT300 hydraulic components, however, resulted in severe folds and carbon inclusions on the top surfaces. The analysis revealed that for these thick-walled castings with relatively high-density patterns, the metal at the end of the pour (reaching the top) had lost significant superheat. This lower temperature caused incomplete foam pyrolysis, generating more viscous liquid and solid residues. The increased viscosity of the cooler metal also hindered the flotation of these residues, trapping them at the top of the casting.
A shift to a top-gating system proved successful. While potentially more turbulent, top-gating ensures that the hottest metal is available at the end of the pour to vaporize the last of the foam pattern thoroughly. The higher temperature at the crown of the mold also keeps the metal fluid for longer, allowing pyrolysis products to float into the pouring cup or riser. Given that the height of typical hydraulic components is less than 150 mm, the potential turbulence from top-gating is manageable and is outweighed by the benefit of reduced carbon defects.
To maximize productivity and yield, the lost foam casting process commonly uses cluster molding, where multiple patterns are attached to a common gating tree. Theoretically, dozens of castings can be poured simultaneously. However, practical limits exist. Pouring an excessive number of thick-section castings like pump bodies in one cluster increases the total mass of foam to be decomposed and the volume of residues to be removed, heightening the risk of defects. Empirical results for HT300 hydraulic parts indicate an optimal cluster size of 20 to 30 patterns, requiring a total pour weight of 300-350 kg of iron. This size aligns well with standard melting furnace capacities, allowing for sequential pouring of multiple clusters from a single melt.
The flow dynamics in such a top-gated cluster can be considered by evaluating the pour time and flow rate. A simplified relation for the required flow rate ($Q$) per pattern cluster to ensure adequate thermal degradation is:
$$ Q = \frac{n \cdot (m_{Fe} + C \cdot m_{foam}) \cdot \Delta H_{req}}{t_{pour} \cdot \Delta T} $$
where $n$ is the number of patterns in the cluster, $m_{Fe}$ is the mass of iron per casting, $m_{foam}$ is the mass of foam per pattern, $C$ is an empirical factor relating foam mass to required additional heat, $\Delta H_{req}$ is the heat required per unit mass, $t_{pour}$ is the target pour time, and $\Delta T$ is the temperature drop deemed acceptable.
Coating Development and Application Protocol
The refractory coating serves as the critical barrier between the vaporizing foam pattern and the solidifying metal. For HT300 hydraulic castings, the coating must possess exceptional refractoriness to withstand prolonged contact with hot iron in thick sections and also promote cooling in thin sections to prevent burn-in.
Coating Formulation: Chromite flour was selected as the primary refractory due to its high fusion point, excellent thermal conductivity (promoting chilling), and low wettability by molten iron, which enhances resistance to metal penetration. To facilitate shakeout, especially from complex internal passages, limestone powder was incorporated as a secondary aggregate. Upon heating to approximately 600°C, limestone (CaCO₃) calcines, releasing CO₂ and contracting in volume, which helps the coating debond from the casting surface. A portion of graphite powder was added to the mix to improve coating blackness (aiding radiative heat transfer) and to reduce overall material cost. The optimized weight ratio for the aggregate blend was determined to be Chromite : Limestone : Graphite = 70 : 15 : 15.
Formulating a stable suspension with dense chromite powder requires a robust binder and suspension system. A composite binder system was used: polyvinyl acetate emulsion (“white glue”) as a low-temperature binder for green strength, and a sulfate-based inorganic binder for high-temperature strength. Suspension was achieved using a synergistic combination of sodium bentonite, sodium carboxymethyl cellulose (CMC), and xanthan gum. Xanthan gum’s stable helical network structure reinforces the continuous network formed by bentonite and CMC, resulting in excellent suspension stability and viscosity control for the lost foam casting process coating.
Application and Drying: Given the relatively small size of hydraulic component patterns, dip coating is the most efficient application method. For general surfaces, two dip coats are applied to achieve a total coating thickness between 0.8 and 2.0 mm. The internal oil galleries and thin septa present a special challenge. To prevent metal penetration in these vulnerable areas, a high-viscosity coating paste is manually injected or brushed to fill these cavities completely, ensuring a robust ceramic barrier is formed. After coating, patterns are dried in a controlled drying chamber at 45-50°C to remove moisture without causing pattern distortion.
| Component | Function | Weight Percentage (%) |
|---|---|---|
| Chromite Flour (70%) + Limestone (15%) + Graphite (15%) | Refractory Aggregate Blend | ~89 |
| Polyvinyl Acetate Emulsion | Low-Temperature Binder | 3.5 |
| Sulfate-based Binder | High-Temperature Binder | 2.0 |
| Sodium Bentonite | Suspension Agent / Plasticizer | 5.0 |
| Sodium Carboxymethyl Cellulose (CMC) | Suspension Agent / Rheology Modifier | 0.5 |
| Xanthan Gum | Suspension Stabilizer / Viscosifier | 0.1 |
| Water + Defoamer | Solvent / Process Aid | Balance |
Molding Sand and Compaction Methodology
Sand Selection: The choice of unbonded sand is crucial for mold fidelity and gas evacuation. Ceramic proppant (often called “beech” or “宝珠” sand) with a grain size of 20-40 mesh is highly recommended for the lost foam casting process of precision components. Its spherical shape provides exceptional flowability, allowing it to fill complex pattern features and thin cavities more effectively than angular silica sand. Under identical vibration, this results in higher and more uniform compaction around delicate pattern features like internal oil gallery cores, minimizing the risk of mold wall movement or collapse. Furthermore, the high intrinsic permeability of rounded-grain sands enhances the evacuation of foam pyrolysis gases through the mold, reducing back-pressure and the associated risk of fold defects.
Pattern Clustering and Compaction: Coated pattern clusters are assembled onto their gating systems and strategically placed in a flask pre-filled with a base layer of sand. Patterns should be oriented so that recesses and blind holes face upwards to facilitate sand filling. Spacing between patterns and from the flask walls should be at least equal to one casting dimension to ensure adequate sand flow and compaction around each unit. Vibration parameters are critical: excessive amplitude can damage thin pattern sections, while insufficient vibration leads to poor sand consolidation. A three-stage vibration sequence is employed:
- After placing the initial base sand, vibrate for 30 seconds to establish a firm foundation.
- Place the pattern cluster and begin sand filling. When the patterns are fully buried, vibrate for 60 seconds to achieve primary consolidation around the patterns.
- After topping off the flask with sand, perform a final compaction vibration for 60 seconds to ensure uniform density throughout the mold.
Low amplitude and relatively high frequency are typically used to protect delicate pattern features while achieving dense packing.
Pouring and Vacuum Process Parameters
The final stage of the lost foam casting process, the pour itself, is governed by temperature and vacuum controls that directly counteract the challenges posed by the pattern material and casting geometry.
Pouring Temperature: For HT300 gray iron, the standard pouring temperature might be in the range of 1380-1420°C for conventional casting. However, in the lost foam casting process, especially for thick sections and patterns with non-zero carbon content, a higher temperature is essential to promote complete gasification of the foam and minimize the formation of heavy, tarry pyrolysis liquids. Raising the pouring temperature to 1440-1480°C provides the necessary superheat. This increases the proportion of foam decomposed into gaseous products (which are more easily drawn through the sand by the vacuum) and reduces the amount of liquid residue, thereby mitigating fold and lustrous carbon defects.
Vacuum Level: Applying a partial vacuum to the sand mold is a defining feature of the lost foam casting process. The vacuum serves multiple functions: it stabilizes the mold, draws pyrolysis gases away from the advancing metal front, and enhances metal fluidity by reducing atmospheric pressure on the melt. For HT300 hydraulic castings, a moderately high vacuum level is beneficial. It assists more forcefully in evacuating the concentrated degradation products from thick sections. An applied vacuum in the range of 0.05 to 0.08 MPa (approximately 380 to 600 mm Hg) is typically optimal. This level is sufficient to ensure clean mold filling and residue evacuation without causing excessive metal penetration into the coating due to the increased pressure differential.
| Process Parameter | Target Value / Range | Primary Function / Rationale |
|---|---|---|
| Pattern Material | EPMMA/EPS Copolymer (70/30) | Balances low carbon residue with manageable gas generation and cost. |
| Pattern Density | 0.025 – 0.027 g/cm³ | Compromise for replicating thin features (2-3 mm) while controlling carbon mass. |
| Gating Style | Top-Gated | Ensures hottest metal at end of pour to fully vaporize foam, reducing folds. |
| Cluster Size | 20 – 30 patterns | Optimizes productivity while limiting total foam mass per pour to control defect risk. |
| Coating Thickness (general) | 0.8 – 2.0 mm | Provides adequate refractory barrier. |
| Coating for Internal Passages | Paste-filled cavities | Prevents metal penetration in vulnerable thin/ intricate areas. |
| Molding Sand | 20-40 Mesh Ceramic Proppant | Superior flowability for filling thin features; high permeability for gas evacuation. |
| Pouring Temperature (HT300) | 1440 – 1480 °C | Enhanced superheat promotes gaseous foam pyrolysis, reduces liquid residue. |
| Applied Vacuum | 0.05 – 0.08 MPa | Effectively evacuates pyrolysis gases without causing excessive metal penetration. |
Practical Outcomes and Defect Analysis
The implementation of the integrated approach outlined above—encompassing copolymer patterns, optimized top-gating, specialized chromite-based coatings, spherical sand, and elevated pour temperatures under controlled vacuum—has been successfully applied to produce various HT300 hydraulic components, including pump bodies, front covers, and rear covers. The castings produced via this refined lost foam casting process exhibit excellent visual and dimensional characteristics.
The surfaces are smooth and clean, with sharply defined edges and corners. Crucially, the complex internal oil galleries are formed without the use of cores, and they are free from burned-in sand or significant veining. Post-casting, the minimal cleanup required is a significant advantage over traditional cored methods. After light machining, the surfaces of the castings are perfectly sound, revealing no subsurface defects such as gas holes or shrinkage associated with the foam degradation process. The dimensional consistency from casting to casting is markedly superior to that achieved with conventional green sand molding, demonstrating the stability and repeatability inherent to a well-controlled lost foam casting process.
The systematic control of parameters directly addresses the primary defect mechanisms:
- Folds/Carbon Defects: Controlled by high pouring temperature (promoting gaseous decomposition), top-gating (hot metal at top), moderate pattern density/low-carbon material (reducing residue source), and sufficient vacuum (evacuating gases).
- Burn-in/Penetration: Controlled by high-refractoriness chromite coating, paste-filling of thin sections, use of low-thermal-expansion ceramic sand, and avoiding excessive vacuum levels.
- Dimensional Inaccuracy: Controlled by robust coating, optimal sand compaction around the stable foam pattern, and the elimination of mold joints and core shifts.
In conclusion, while the production of high-integrity HT300 hydraulic castings presents specific challenges to the lost foam casting process, these challenges can be systematically overcome through a coordinated engineering of materials and parameters. The result is a production method capable of yielding precision castings with excellent surface and internal quality, high dimensional accuracy, and potentially lower total cost compared to traditional core-based methods, validating the lost foam casting process as a viable and superior manufacturing route for such demanding components.