
In the field of modern casting, the lost foam casting process has gained significant traction due to its numerous advantages, including high dimensional accuracy, excellent surface finish, reduced machining allowances, and lower costs. This process eliminates fins and burrs, thereby minimizing cleaning expenses. Its widespread adoption globally underscores its superiority. Initially, the lost foam casting process for gray iron was well-established with mature technology and equipment in many regions. However, driven by the increasing demand for lightweight components, there is a growing trend to replace gray iron parts with aluminum alloy castings. In our company, we have dedicated nearly a decade to mastering the lost foam casting process for aluminum alloys, achieving a remarkable yield rate of over 98%, which positions us at the forefront domestically. Our existing aluminum alloy lost foam casting line incorporates advanced equipment such as an American Fuller line, a German Strikowestofen melting furnace, an American Pyrotek aluminum purification system, and a German ABB robotic pouring system, among other auxiliary devices. Notably, there are no specialized domestic manufacturers for such integrated systems. As part of our strategic planning, we aimed to transform an idle domestic gray iron lost foam casting line into an aluminum alloy production line with minimal investment. This article details the key considerations and modifications involved in this transformation, emphasizing the intricacies of the lost foam casting process.
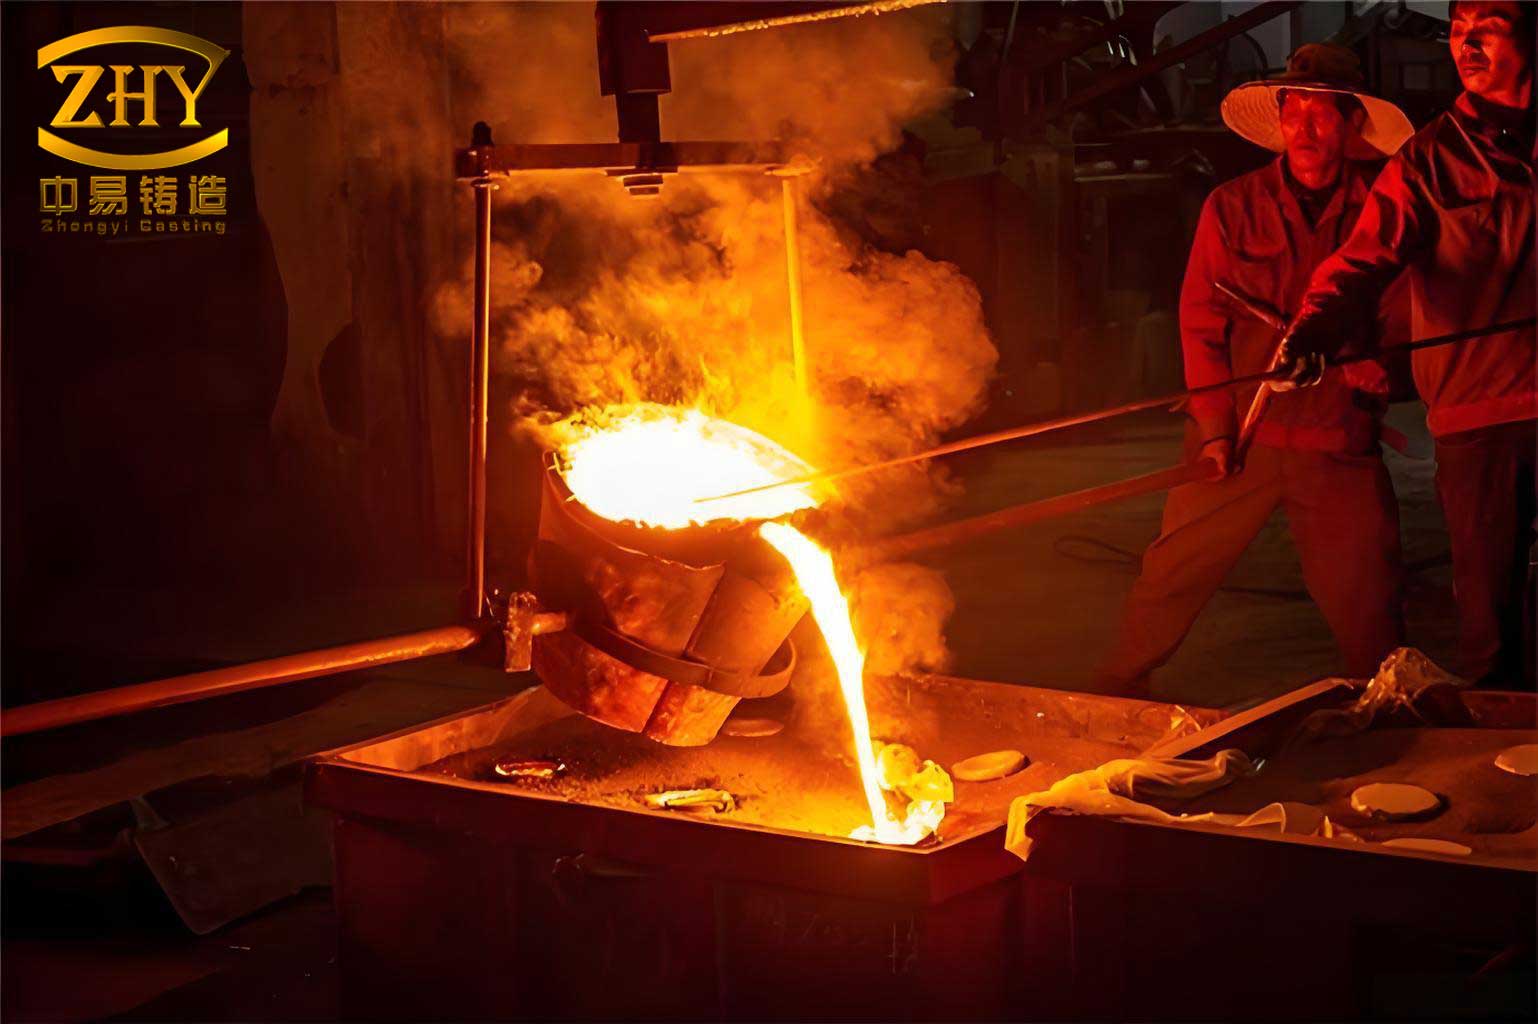
The original gray iron production line consisted of two shared lines, each comprising several critical components. A single line included two medium-frequency induction melting furnaces, one semi-automatic pouring machine, one molding and box-pushing line, two vacuum systems, one mixed sand treatment system, one bag-type dust collector for the melting furnaces, three dust removal systems for the molding line and sand treatment, along with auxiliary equipment like cooling towers, compressed air filters, and casting conveying suspension chains. This setup was optimized for the high-temperature requirements of gray iron casting, where pouring temperatures exceed 1500°C. However, adapting this line for aluminum alloy casting, which involves pouring temperatures around 760°C, necessitated comprehensive modifications across multiple subsystems. The lost foam casting process for aluminum alloys introduces distinct challenges, particularly in melt handling, sand management, and environmental control, which required careful analysis and redesign.
Transitioning from gray iron to aluminum alloy within the lost foam casting process entails addressing fundamental differences in material properties and process parameters. While both utilize the same foundational principle of evaporative pattern casting, the equipment and operational protocols diverge significantly. Based on our experience with an imported American aluminum alloy lost foam casting line and the existing domestic line’s condition, we identified several critical areas requiring modification. These encompass melting equipment, aluminum melt purification, the mold pushing loop system, sand treatment, and ancillary devices. Each area posed unique challenges that impacted product quality, efficiency, and cost-effectiveness. The following sections elaborate on these challenges, our analytical discussions, and the implemented solutions, all centered on optimizing the lost foam casting process for aluminum alloy production.
Melting Equipment Modifications
The melting stage is pivotal in the lost foam casting process, as it directly influences melt quality and subsequent casting integrity. Originally, the line used medium-frequency induction furnaces. In such furnaces, an alternating current through the induction coil generates eddy currents in the metal charge, creating a skin effect where heat is produced within the material itself. This method offers rapid melting and minimal metal loss, making it common in aluminum alloy melting, especially for alloys with higher concentrations of elements like manganese, copper, and zinc. The power efficiency and heating rate can be described by the following formula for eddy current power density:
$$P = \frac{\pi^2 f^2 B^2 d^2}{2\rho}$$
where \(P\) is the power density, \(f\) is the frequency, \(B\) is the magnetic flux density, \(d\) is the thickness of the material, and \(\rho\) is the resistivity. However, for aluminum alloys in the lost foam casting process, medium-frequency furnaces present drawbacks. The “hump” or vortex phenomenon during melting promotes gas entrapment in the aluminum melt, leading to excessive porosity in castings. Additionally, the original tilting mechanism of the furnaces resulted in discontinuous production, requiring transfer to pouring stations, which caused significant temperature drops and inefficiencies.
Moreover, energy consumption comparisons revealed that medium-frequency furnaces are less economical than gas-fired furnaces for aluminum melting in the lost foam casting process. After operating with the existing furnaces for over a month, we observed that casting quality and production efficiency did not meet our standards. Consequently, we decided to replace them with new gas-fired melting and holding furnaces. The thermal efficiency of a gas furnace can be approximated by:
$$\eta = \frac{Q_{\text{melt}}}{Q_{\text{fuel}}} \times 100\%$$
where \(Q_{\text{melt}}\) is the heat absorbed by the aluminum, and \(Q_{\text{fuel}}\) is the heat input from fuel. Gas furnaces provide better temperature stability and reduced gas pickup, crucial for the lost foam casting process. We selected a furnace with a melting capacity of 2 tons per hour and a holding capacity of 4 tons, ensuring continuous supply and minimal temperature fluctuations. The table below summarizes the comparison between the original and new melting systems:
| Aspect | Original Medium-Frequency Furnace | New Gas-Fired Furnace |
|---|---|---|
| Melting Rate | Variable, dependent on charge | 2 tons/hour consistent |
| Temperature Control | Prone to fluctuations | Stable, ±5°C |
| Gas Entrapment | High due to vortex | Low with proper burner design |
| Energy Efficiency | Lower, higher electricity cost | Higher, natural gas cost-effective |
| Continuity | Intermittent, requires transfer | Continuous via launder systems |
| Suitability for Lost Foam Casting Process | Moderate, requires additional purification | High, integrates well with purification |
This shift not only improved melt quality but also enhanced the overall efficiency of the lost foam casting process, reducing defects related to gas porosity.
Aluminum Melt Purification System
Aluminum melt purification is a unique and critical step in the lost foam casting process for aluminum alloys, as it removes dissolved gases and inclusions that can compromise casting integrity. The original gray iron line lacked such equipment, necessitating a complete new installation. Industry practices offer two primary purification workflows, each with implications for the lost foam casting process. The first workflow involves: melting aluminum → tapping into transfer ladles → degassing with a degassing unit → holding in a定量浇注炉 for settling → secondary degassing in the定量炉 → pouring. The second workflow is: melting aluminum → flowing through launders into a holding furnace for refining → settling in the holding furnace → passing through an online degassing unit → filtration box → pouring holding furnace → robotic pouring. Our evaluation focused on parameters like temperature loss, density index, and pouring efficiency within the lost foam casting process.
The first workflow, with multiple transfers via forklifts, led to significant temperature drops, up to 100°C, and increased gas pickup. The density equivalent, a measure of gas content, was higher and unstable. Pouring efficiency was low, at about 4 minutes per piece, due to the limitations of tilting定量炉 structures, which also caused inaccuracies in pouring volume, resulting in aluminum utilization losses of 120-180 kg per 2 tons of melt. In contrast, the second workflow, with integrated launder systems and robotic pouring, minimized temperature loss and offered precise, stable pouring. Robotic pouring allows for constant flow rate pouring, enhancing accuracy. The efficiency gain can be expressed as:
$$E = \frac{N_{\text{castings}}}{t_{\text{cycle}}}$$
where \(E\) is the pouring efficiency, \(N_{\text{castings}}\) is the number of castings per cycle, and \(t_{\text{cycle}}\) is the cycle time. For the lost foam casting process, maintaining melt quality is paramount, so we adopted the second workflow with a Pyrotek purification system. The table below contrasts the two purification methods:
| Parameter | Workflow 1 (Ladle Transfer) | Workflow 2 (Launder & Robotic) |
|---|---|---|
| Temperature Drop | Up to 100°C | Less than 20°C |
| Density Index | High, variable | Low, stable below 0.2 |
| Pouring Efficiency | 4 minutes/casting | 1.5 minutes/casting |
| Aluminum Utilization | Lower, ~90-94% | Higher, ~97-99% |
| Integration with Lost Foam Casting Process | Poor, disrupts continuity | Excellent, seamless flow |
By implementing the advanced purification system, we ensured that the aluminum melt met the stringent requirements of the lost foam casting process, reducing defects like pinholes and inclusions.
Mold Pushing and Loop System Modifications
The mold pushing loop system is essential for transporting sand molds through various stations in the lost foam casting process. Originally, the line used hydraulic cylinders to push boxes, which were then transferred via shuttle cars. This design presented several issues for aluminum alloy casting. First, the relative motion between sand box cars caused wear on the bumpers at both ends. Assuming an average wear of 0.5 mm per bumper, the total length reduction for 38 cars in a single line would be 19 mm. In practice, factors like car deformation and iron slag adhesion led to inconsistent pushing lengths, making it impossible to implement定点浇注 (fixed-point pouring) methods, whether with定量炉 or robotic systems. Second, the hydraulic push system caused severe shaking of the entire line upon stopping, which could disrupt freshly poured, uncured castings in the lost foam casting process, leading to gas entrapment or deformation defects.
To address these, we modified the system by connecting all cars with fixed pins, eliminating gaps and relative movement. This created a closed loop without wear. Hydraulic positioning devices were installed at key stations: molding,定点浇注, and shakeout, ensuring precise positioning after each push. The drive mechanism was upgraded from hydraulic cylinders to servo-driven ball screws. The improved synchronization and control accuracy minimized shaking. The positioning accuracy can be modeled as:
$$\Delta L = \frac{F_{\text{friction}}}{k} + \epsilon$$
where \(\Delta L\) is the positioning error, \(F_{\text{friction}}\) is the frictional force, \(k\) is the system stiffness, and \(\epsilon\) is the control error. With servo control, \(\epsilon\) is reduced significantly. The dual-drive system’s synchronization ensured smooth operation, enhancing the reliability of the lost foam casting process. The modifications are summarized below:
| Feature | Original Hydraulic System | Modified Servo Ball Screw System |
|---|---|---|
| Pushing Mechanism | Hydraulic cylinders with shuttle | Servo motors with ball screws |
| Wear and Tear | High due to relative motion | Negligible, fixed connections |
| Positioning Accuracy | Poor, inconsistent | High, within ±2 mm |
| Shaking upon Stop | Severe, affects castings | Minimal, stable |
| Impact on Lost Foam Casting Process | Negative, causes defects | Positive, improves yield |
These changes enabled precise定点浇注, crucial for the lost foam casting process, and increased product qualification rates by reducing movement-related defects.
Sand Treatment System Overhaul
In the lost foam casting process, sand plays a vital role in supporting the foam pattern and absorbing decomposition products. The transition from gray iron to aluminum alloy significantly alters sand thermal dynamics. Gray iron pouring temperatures exceed 1500°C, resulting in sand temperatures around 300°C at discharge, whereas aluminum alloy pouring at 760°C reduces sand temperatures to below 200°C. The original sand treatment system had excess capacity, leading to high energy consumption and excessively low sand temperatures, which fell outside the optimal range for the lost foam casting process, causing defects like incomplete pattern decomposition. After recalculation, we optimized the system by removing two fluidized bed coolers, reducing capacity to match the lower heat input.
Moreover, the lost foam casting process for aluminum alloys differs from gray iron in that it does not require vacuum systems due to the lower pouring temperature. However, this results in more EPS (expanded polystyrene) residues, which are primarily adsorbed by the sand. Oily coatings on sand grains from these residues impair sand flowability, adversely affecting vibration compaction during molding. This also reduces inter-grain空隙, diminishing adsorption capacity and leading to process issues like反喷 (back spray). To address this, we added an intermittent online sand calciner upstream of the sand cooler. By positioning it after high-temperature sand discharge, we leveraged residual heat for energy savings. The calciner uses direct natural gas heating to reach 600°C, at which most surface contaminants volatilize and are expelled with flue gas, turning sand color from black to white. The sand treatment capacity is 30 tons per hour, and through trials, we determined a calcination rate of 3 tons per hour, or 10% of total flow, suffices for the lost foam casting process. Excessive calcination would raise energy costs. The heat balance for the calciner can be expressed as:
$$Q_{\text{in}} = m_{\text{sand}} \cdot c_p \cdot \Delta T + Q_{\text{loss}}$$
where \(Q_{\text{in}}\) is the heat input from burning natural gas, \(m_{\text{sand}}\) is the sand mass flow rate, \(c_p\) is the specific heat of sand, \(\Delta T\) is the temperature rise, and \(Q_{\text{loss}}\) is heat loss. The table below outlines the sand system modifications:
| Aspect | Original Gray Iron System | Modified Aluminum Alloy System |
|---|---|---|
| Sand Temperature at Discharge | ~300°C | <200°C |
| Cooling Capacity | Overdesigned, 40 tons/hour | Optimized, 30 tons/hour |
| EPS Residue Handling | Minimal, high temp burns off | Significant, requires calcination |
| Calcination Unit | None | 3 tons/hour online calciner |
| Energy Consumption | High due to excess cooling | Lower, targeted calcination |
| Compatibility with Lost Foam Casting Process | Limited for aluminum | Enhanced, maintains sand quality |
These adjustments ensured that the sand system supported the unique demands of the lost foam casting process for aluminum alloys, improving sand reusability and reducing defects.
Other Equipment Adaptations
The shift in the lost foam casting process from gray iron to aluminum alloy also affects auxiliary systems, particularly dust collection. The process generates fumes containing unburned EPS residues, which are viscous and prone to clogging. Originally, bag-type dust collectors were used, but they are unsuitable for aluminum lost foam casting due to residue adhesion. We replaced them with a three-stage wet scrubbing system. However, from experience with our imported line, we learned that carbon steel pipelines in wet scrubbers corrode rapidly—within six months, pipes were compromised, and within a year, the scrubber外壳 failed. To prevent this, we used 304 stainless steel for all pipelines and the scrubber tower, and selected corrosion-resistant nylon pumps for the circulation system. The efficiency of wet scrubbing can be described by the following for particulate removal:
$$\eta = 1 – e^{-k \cdot L \cdot Q}$$
where \(\eta\) is the collection efficiency, \(k\) is a constant dependent on droplet size and particle properties, \(L\) is the liquid-to-gas ratio, and \(Q\) is the gas flow rate. This modification ensured reliable operation and environmental compliance for the lost foam casting process.
Additionally, other auxiliary equipment like cooling towers and compressed air filters were retained but recalibrated for the lower thermal loads and different air quality requirements of aluminum casting. The overall integration of these changes focused on maintaining the continuity and quality of the lost foam casting process. The lost foam casting process, when adapted for aluminum alloys, demands meticulous attention to detail across all subsystems to achieve high yields and efficiency.
Conclusion and Performance Outcomes
After thorough evaluation and collaboration with suppliers, we implemented the transformation. The new setup includes a gas-fired melting and holding furnace from Dongda Sanjian with a melting rate of 2 tons/hour and holding capacity of 4 tons, a Pyrotek aluminum purification system, and a redesigned pushing loop and sand calciner from Beijing Tianzhe Lost Foam Technology Co., Ltd. The revamped line achieves an efficiency of 25 boxes per hour, with only 7 operators per shift and an equipment uptime exceeding 85%. Most importantly, the yield rate for heavy-duty transmission housing castings stabilized above 98%, meeting our stringent standards. This success underscores the feasibility of converting existing gray iron lines for aluminum alloy production within the lost foam casting process framework.
The lost foam casting process, when properly tailored for aluminum alloys, offers immense benefits in lightweight component manufacturing. Our journey highlights that key modifications—such as adopting gas furnaces, implementing advanced purification, upgrading drive systems, optimizing sand treatment, and selecting corrosion-resistant materials—are essential for a successful transition. The lost foam casting process continues to evolve, and these adaptations contribute to its advancement, enabling cost-effective and high-quality aluminum casting production. Future work may focus on further automation and energy savings in the lost foam casting process, but for now, our transformed line serves as a benchmark in the industry.