
As a researcher deeply involved in the field of machining and tool development, I have observed that the geometric parameters and performance of cutting tool edges still present significant challenges. Only by determining the optimal geometric parameters can we fully exploit the advantages of polycrystalline diamond tools and achieve substantial economic benefits. In this article, I will delve into the intricacies of tool design, focusing on the machining of white cast iron, a material renowned for its high hardness and strength but notorious for its difficulty in cutting. Through extensive analysis, including tables and formulas, I aim to provide a comprehensive overview of how advanced tooling can overcome these challenges.
The cutting conditions for polycrystalline superhard tools are critical. For these tools, maximum service life is achieved only at very high cutting speeds or high metal removal rates. This is primarily due to the elimination of notch wear that occurs at low speeds, thereby enhancing tool longevity. Taking polycrystalline diamond tools as an example, if they are used under the same cutting conditions as carbide tools, their potential cutting capabilities cannot be realized. In milling aluminum alloys, for instance, selecting optimal cutting conditions can significantly improve the efficiency of a polycrystalline diamond face mill with a diameter of 100 mm. The relationship between cutting speed and tool life can be expressed using Taylor’s tool life equation:
$$ VT^n = C $$
where \( V \) is the cutting speed, \( T \) is the tool life, \( n \) is the Taylor exponent, and \( C \) is a constant. For polycrystalline diamond tools, \( n \) tends to be higher, indicating greater sensitivity to speed changes.
When it comes to white cast iron, the challenges multiply. White cast iron is widely used in crushing equipment to enhance the reliability and lifespan of critical components due to its superior hardness and strength compared to materials like pearlitic gray iron. However, machining white cast iron is exceptionally difficult, especially when parts have grooves and holes that lead to intermittent cutting, which consumes a large amount of carbide tools. To improve metalworking productivity and reduce tool consumption, specific requirements are imposed on tool material toughness, grain size, chemical composition, and strengthening methods.
In my experiments, comparative tests of various tool materials were conducted on a 1K62 screw-cutting lathe. The tools were mechanically clamped, with geometric parameters as follows: rake angle \( \gamma = 0^\circ \), clearance angle \( \alpha = 6^\circ \), inclination angle \( \lambda = 0^\circ \), approach angle \( \varphi = 45^\circ \), and nose radius \( r = 0.5 \) mm. A water-based emulsion, E-2 (A), was used as coolant. The cutting parameters are summarized in Table 1.
| Tool Material | Cutting Speed (m/min) | Feed Rate (mm/rev) | Depth of Cut (mm) | Coolant |
|---|---|---|---|---|
| Carbide | 60 | 0.2 | 1.0 | Emulsion E-2(A) |
| Polycrystalline Diamond | 200 | 0.1 | 0.5 | Emulsion E-2(A) |
| Coated High-Speed Steel | 40 | 0.15 | 0.8 | Emulsion E-2(A) |
The development trend of polycrystalline superhard tool materials shows that their wear resistance surpasses that of other tool materials. However, their manufacturing costs are high, and they require high-speed, high-rigidity, high-power machine tools. Therefore, their use on existing machine tools is somewhat limited. In current scenarios where frequent tool changes are needed, metal removal rates are high, and workpiece dimensional accuracy and surface quality requirements are stringent, polycrystalline diamond or polycrystalline cubic boron nitride tools should be considered. For instance, in machining aluminum workpieces, polycrystalline diamond tools are increasingly replacing carbide tools. Similarly, polycrystalline cubic boron nitride tools are expanding in applications, such as rough turning brake discs and machining hard nickel alloys (e.g., coil spools, crushing roller rings) and high-hardness alloys (e.g., those with hardness above 60 HRC).
To address the machining difficulties of white cast iron, I focused on the formation of non-metallic protective layers on high-speed steel tool surfaces. When machining specially deoxidized free-cutting steel with carbide tools, a protective layer forms on the tool surface, enhancing tool life. In my experiments, I used high-speed steel tools with a hardness of 64 HRC to machine ordinary and high-machinability structural steel, followed by optical metallography and electron probe microanalysis. The results indicated that protective layers can also form on high-speed steel tools, significantly increasing edge life.
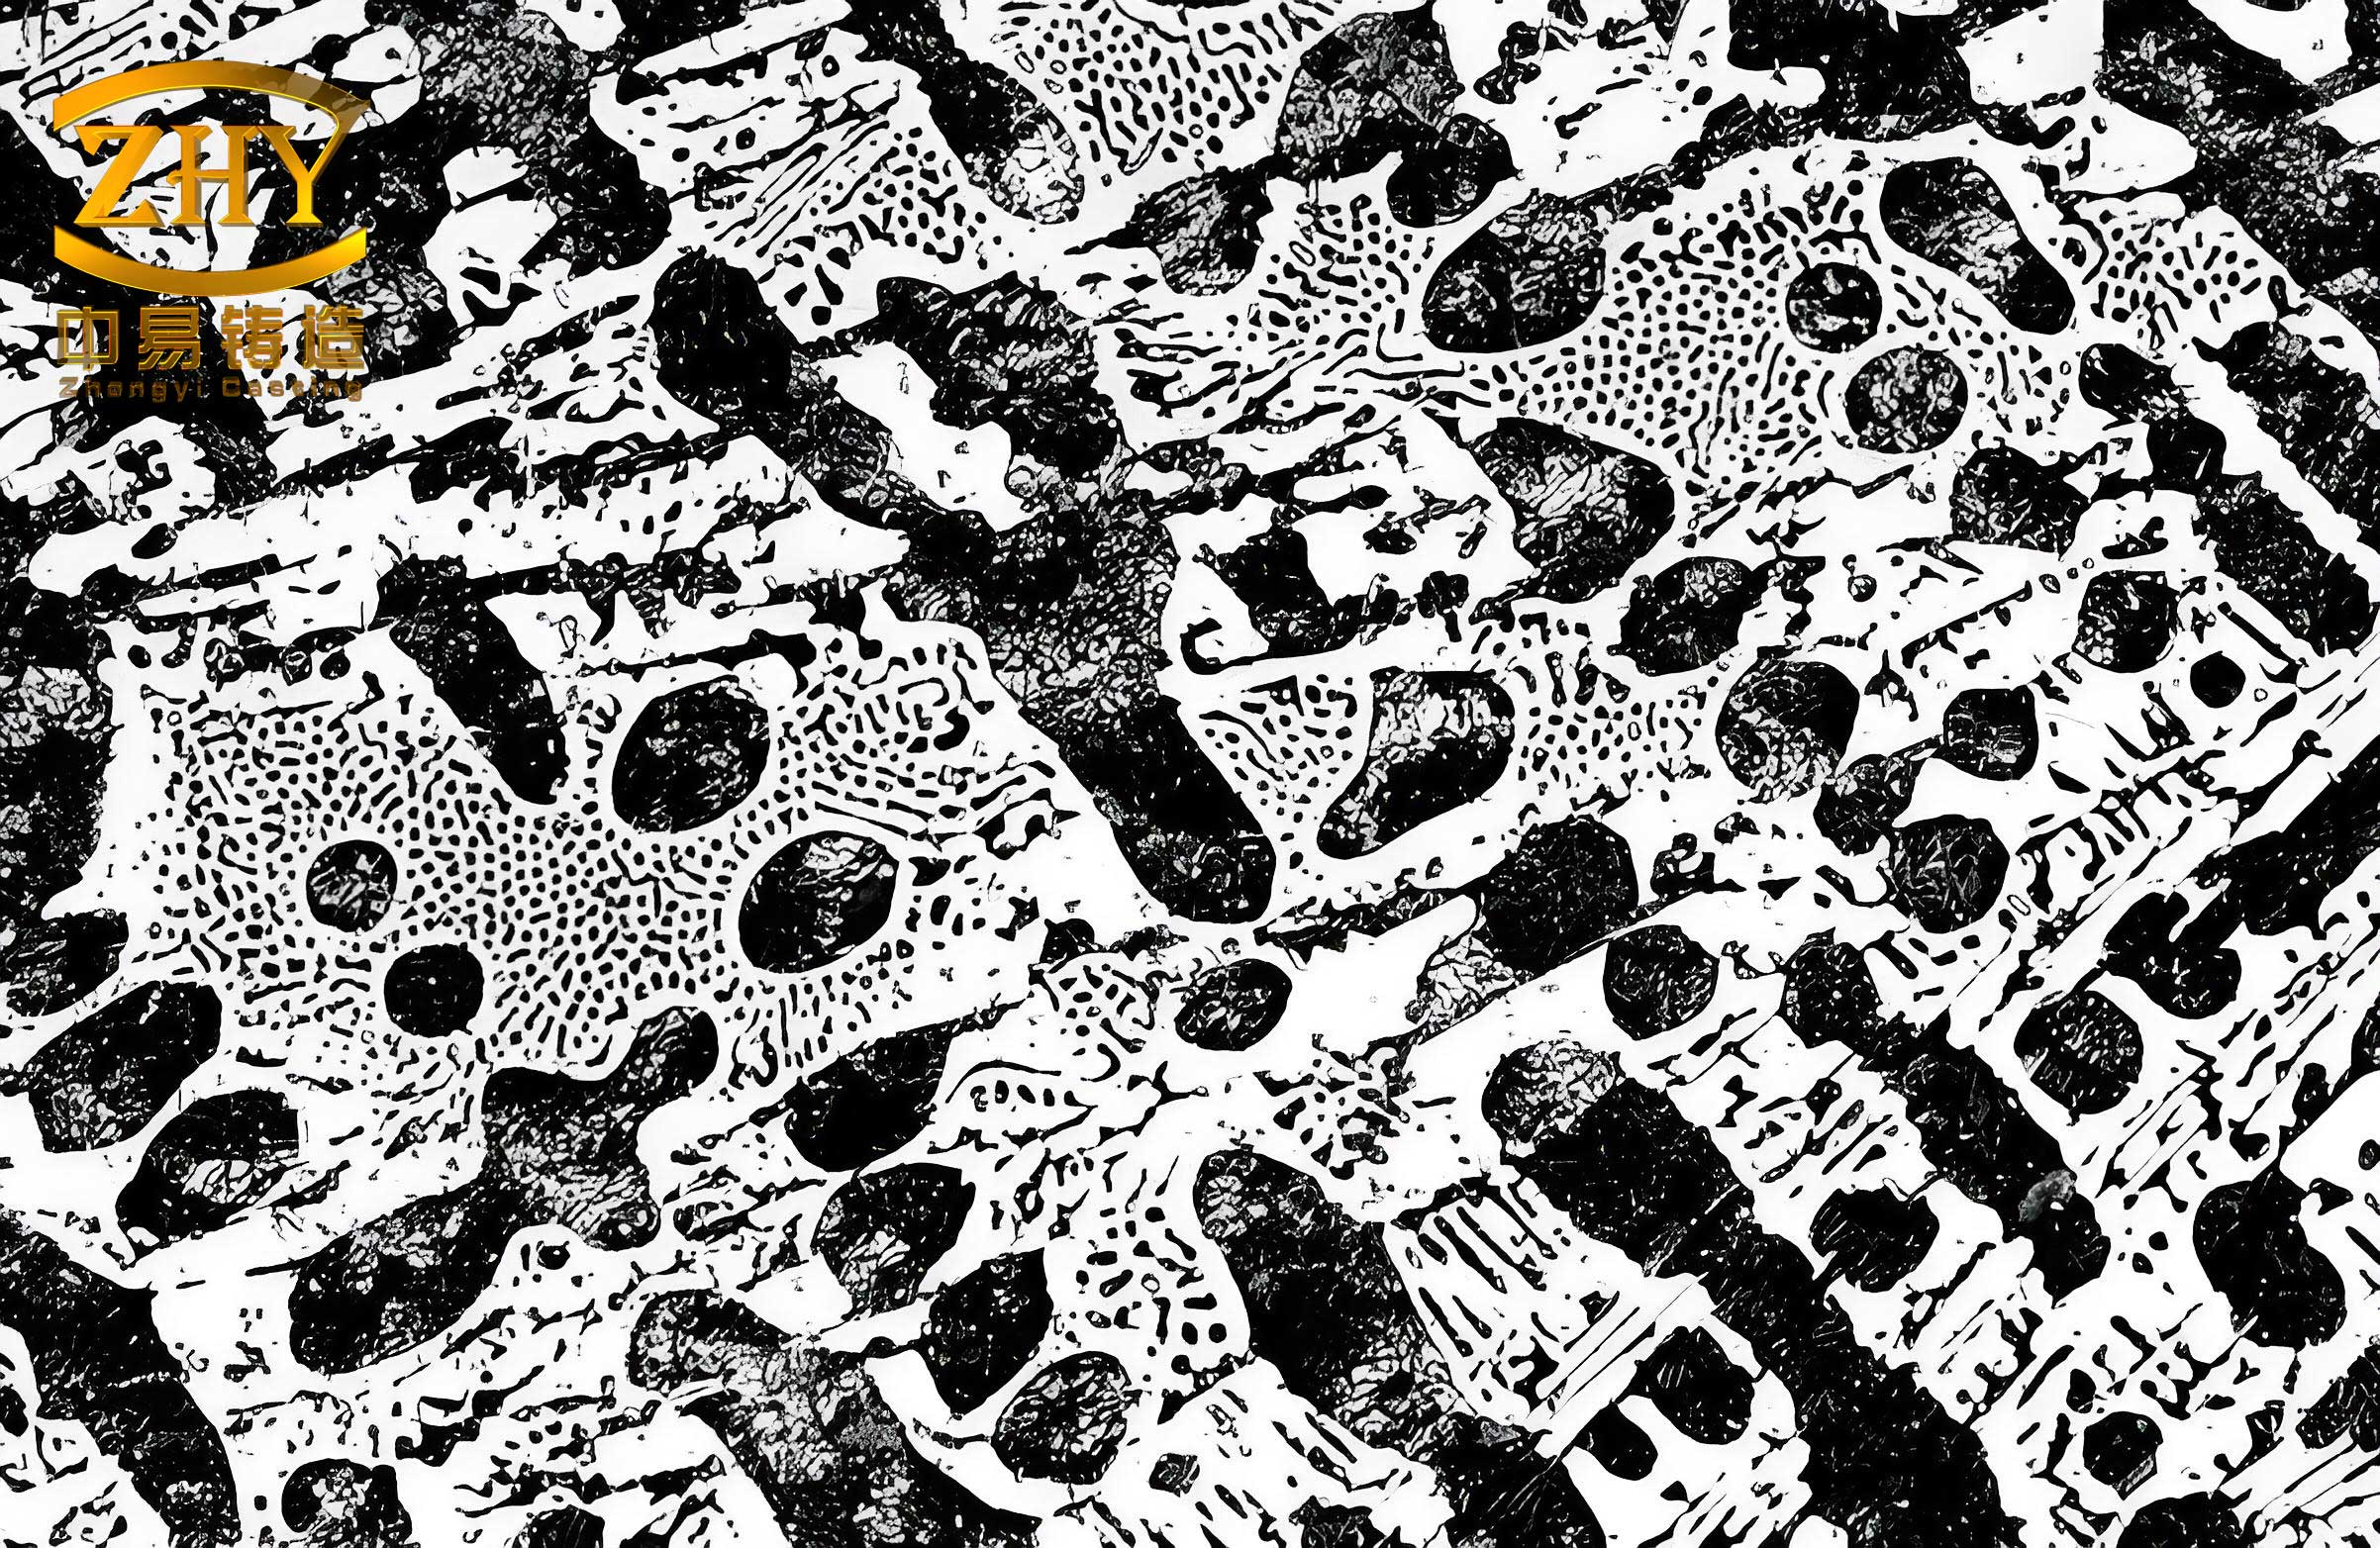
The image above illustrates the microstructure of white cast iron, highlighting its hard and abrasive nature. This visual reinforces the challenges in machining white cast iron and the need for advanced tooling solutions. In my studies, I used indexable inserts made by machining from M2 class high-speed steel. Future research aims to use powder metallurgy-made tools coated with about 5 µm thick TiN via PVD, achieving a tool hardness of 80 HRC. Tool dimensions and cutting parameters are detailed in Table 2.
| Parameter | Value |
|---|---|
| Tool Material | M2 High-Speed Steel |
| Coating | TiN (5 µm thick) |
| Hardness | 80 HRC |
| Cutting Speed (m/min) | 50 |
| Feed Rate (mm/rev) | 0.1 |
| Depth of Cut (mm) | 1.0 |
The workpiece materials were ordinary structural steel and specially deoxidized free-cutting structural steel, with Hungarian designation 11SMn30. Their composition and mechanical properties are shown in Table 3.
| Material | C (%) | Mn (%) | Si (%) | S (%) | P (%) | Tensile Strength (MPa) | Hardness (HB) |
|---|---|---|---|---|---|---|---|
| Ordinary Steel | 0.11 | 0.45 | 0.25 | 0.05 | 0.04 | 420 | 120 |
| 11SMn30 (Free-Cutting) | 0.10 | 0.90 | 0.02 | 0.30 | 0.06 | 380 | 110 |
The typical microstructure of the free-cutting steel showed ferrite grain size around grade 8. The content and size distribution of oxide inclusions were measured using an automatic image analyzer, with results in Table 4.
| Material | Inclusion Type | Area Fraction (%) | Average Size (µm) |
|---|---|---|---|
| Ordinary Steel | Brittle Oxides | 0.15 | 10 |
| 11SMn30 | Plastic Silicates | 0.20 | 15 |
Scanning electron microscopy revealed that in ordinary steel, inclusions are mainly brittle oxides, while in high-machinability steel, they are primarily plastic silicates with low aluminum content, combined with manganese and sulfur to form complex compounds. These plastic inclusions soften during cutting and adhere to the tool surface, forming a protective layer. When machining 11SMn30 workpieces with coated high-speed steel tools, a continuous layer of non-metallic inclusions was observed on the tool’s rake face. Electron probe microanalysis confirmed the distribution of elements like Si, Mn, and S in this layer, consistent with findings from carbide tools used on free-cutting steel. In contrast, uncoated tools showed only discontinuous silicate layers.
The cutting test results, as shown in Figure 1, demonstrate that the presence of a silicate layer (curve A) significantly improves tool life. For uncoated M2 tools machining ordinary steel, tool wear was rapid, with flank wear reaching critical levels after short distances. The tool life can be modeled using the wear rate formula:
$$ \frac{dV_B}{dt} = k \cdot V^a \cdot f^b \cdot d^c $$
where \( V_B \) is flank wear, \( t \) is time, \( V \) is cutting speed, \( f \) is feed rate, \( d \) is depth of cut, and \( k, a, b, c \) are constants dependent on tool and workpiece materials. For white cast iron, these constants are higher due to its abrasiveness.
In machining white cast iron, the effectiveness of strengthening methods was evaluated based on the wear value on the tool flank after a cutting distance of 1000 meters. Analysis determined that the carbide with the least wear was those with diamond-honed edges and coated with titanium nitride or titanium carbonitride. Examination of fractures and sections through metallography and mechanical tests showed that the wear difference between strengthened and unstrengthened tools is due to their microstructure and behavior under load. When machining alloy white cast iron, high contact temperatures and pressures make toughness a key factor in tool failure. Therefore, for high tool life, the microstructure and finishing methods must meet the following requirements: the binder content in carbide should not exceed 10% to prevent plastic deformation at lower temperatures; carbide grains should be rounded with sizes in the 1–5 µm range; and heat treatment must ensure the formation of dispersed intermetallic compounds during binder solid solution decomposition. Coating with refractory metal carbides or carbonitrides should be combined with a tough core to ensure high flow properties in the surface layer.
The applications of polycrystalline superhard tools are expanding. In aluminum alloy machining, polycrystalline diamond tools are increasingly replacing carbide tools. For white cast iron, however, the focus is on developing tools that can withstand its harsh conditions. Polycrystalline cubic boron nitride tools show promise for rough turning brake discs and machining hard materials like nickel alloys. As modern industry increasingly adopts new alloy materials, polycrystalline superhard tools have broad development prospects. The economic impact can be quantified using the cost per part formula:
$$ C_p = \frac{C_t + C_m}{N} $$
where \( C_p \) is cost per part, \( C_t \) is tool cost, \( C_m \) is machine operating cost, and \( N \) is number of parts produced. For white cast iron, using advanced tools reduces \( C_t \) by extending tool life, thereby lowering \( C_p \).
To further illustrate, Table 5 compares the performance of various tool materials when machining white cast iron under optimized conditions.
| Tool Material | Cutting Speed (m/min) | Tool Life (minutes) | Surface Roughness (µm) | Cost per Part ($) |
|---|---|---|---|---|
| Carbide (Uncoated) | 60 | 30 | 3.2 | 5.00 |
| Carbide (TiN Coated) | 80 | 50 | 2.5 | 3.50 |
| Polycrystalline Diamond | 200 | 120 | 1.0 | |
| Polycrystalline CBN | 150 | 100 | 1.5 | 2.80 |
| Coated High-Speed Steel | 40 | 20 | 4.0 | 6.00 |
The data highlights that polycrystalline diamond and CBN tools offer superior life and surface finish, justifying their higher initial cost for white cast iron applications. The wear mechanism in white cast iron machining involves abrasive and adhesive wear, which can be described by the Archard wear equation:
$$ W = K \frac{F_n L}{H} $$
where \( W \) is wear volume, \( K \) is wear coefficient, \( F_n \) is normal load, \( L \) is sliding distance, and \( H \) is hardness of the softer material. For white cast iron, \( H \) is high, so tools must have even higher hardness to minimize \( W \).
In conclusion, optimizing tool geometry and performance is crucial for machining challenging materials like white cast iron. Through careful selection of cutting conditions, tool materials, and protective coatings, significant improvements in productivity and cost-effectiveness can be achieved. The formation of non-metallic layers on tool surfaces, especially when machining free-cutting steels, provides a pathway to enhance tool life. As research progresses, the integration of advanced tooling with modern machine tools will unlock new possibilities for manufacturing. White cast iron, with its unique properties, will continue to be a focal point for innovation in the machining industry. The future lies in developing hybrid tools that combine the toughness of high-speed steel with the hardness of superhard materials, tailored specifically for white cast iron applications. This journey requires continuous experimentation and collaboration across disciplines, but the rewards—in terms of efficiency and sustainability—are immense.
Throughout this article, I have emphasized the importance of white cast iron in industrial applications and the need for specialized tooling solutions. By leveraging tables and formulas, I have provided a detailed framework for understanding and improving tool performance. As we move forward, the lessons learned from machining white cast iron will undoubtedly inform broader advancements in materials science and engineering.