
In my day-to-day foundry engineering work, I have often encountered slag-related defects in ductile iron casting. Slag inclusion is recognized as one of the most harmful and unstable quality problems in foundry production, because it not only creates unacceptable surfaces on components but also degrades the mechanical integrity of the finished part. In this article, I describe the problem-solving process I followed for a heavy diffusion-body ductile iron casting that was suffering from severe slag inclusions. I will explain how I analyzed the defect, how I identified the root cause, and how I solved the problem by redesigning the gating system and introducing ceramic foam filters.
The component in question was a diffusion body for a gas turbine application. It was a medium-to-heavy ductile iron casting with a net weight of approximately 1480 kg and a poured weight of approximately 2000 kg. The material specification was QT400-18, which corresponds to a ferritic ductile iron grade with good ductility and reasonable strength. The production process used a green-sand or chemically bonded sand mold, with the metal poured at 1315–1330 °C and a specified pouring time of 30 ± 5 s.
1. Initial Quality Problem
During production, the foundry experienced a serious period of scrap caused by slag inclusions. The defect rate at its worst reached more than 12%, and several batches were rejected because of the same recurring problem. This was not a minor cosmetic issue. The slag appeared as dark, branched, irregular inclusions in the top section of the casting and along the inner bore wall. In many castings, the inclusions were large enough to be visible after machining. Some castings leaked under pressure testing because the slag networks extended through the wall section, creating porosity and discontinuities.
I started the investigation by examining the defect position and morphology. The slag was concentrated in the upper part of the casting, especially on the top face and the inner wall. I removed samples from the defective areas and prepared them for metallographic observation. The microstructure showed dark, elongated, dendritic inclusions. Some of these inclusions were extremely long, with lengths ranging from 600 μm to more than 1000 μm. The inclusions were not simple round particles; they had a branching shape typical of entrained oxide films and secondary oxidation products.
This observation gave me the first important clue. The shape and distribution of the slag were not typical of primary slag alone. Primary slag generated during spheroidization is often granular and may be trapped near mold surfaces or gates. The dendritic, branched morphology I observed suggested secondary slag formed inside the mold during filling. In other words, the defect was strongly related to the fluid flow behavior of the molten ductile iron.
2. Characterization of Slag Inclusions in Ductile Iron Casting
To solve the problem, I needed to understand the exact nature of the inclusions. I collected samples from defective castings and used optical microscopy to study the inclusion morphology. The inclusions were irregular, branched, and dark in color. In some areas, they appeared as continuous films along grain boundaries; in other areas, they formed clusters of very fine oxides.
I also considered the chemical composition of typical slag in ductile iron casting. The most common constituents are magnesium oxide, silicon dioxide, iron oxide, aluminum oxide, manganese sulfide, and magnesium sulfide. The spheroidization treatment of ductile iron introduces magnesium into the melt, and magnesium is highly reactive. It reacts with oxygen and sulfur to form oxides and sulfides. If these products are not removed before pouring or are generated again during filling, they become slag inclusions in the casting.
For this diffusion-body casting, the metallographic appearance was consistent with a mixture of oxide films and secondary inclusions. The large branched inclusions were particularly important because they suggested that the liquid metal surface had folded over upon itself during mold filling. When the surface oxide film is submerged into the bulk liquid, it does not disappear. The film is entrapped and becomes a two-sided interface in the solidifying metal. This mechanism is sometimes described as bifilm formation. It is extremely harmful in ductile iron casting because it creates a crack-like discontinuity in the matrix.
| Defect Type | Typical Location | Typical Composition | Morphology |
|---|---|---|---|
| Primary slag | Upper surfaces, risers, runner ends | MgO, SiO2, CaS, MgS, Al2O3 | Granular, globular, clustered |
| Secondary slag | Internal cavities, top walls, core surfaces | Complex Fe-Mn-Al-Si oxides, MgO films | Branched, dendritic, film-like, elongated |
3. Mechanism of Slag Formation in Ductile Iron Casting
Slag in ductile iron casting can be divided into two major categories: primary slag and secondary slag. Primary slag is formed before the metal enters the mold cavity. It originates from the metallurgical reactions during melting, spheroidization, inoculation, and holding. This slag is often present on the surface of the ladle or in the pouring stream. Secondary slag is formed during mold filling, as a result of oxidation of the liquid metal surface and the entrainment of oxide films into the liquid metal.
The formation of primary slag is closely related to the chemistry of ductile iron. The magnesium added for spheroidization reacts with oxygen and sulfur according to the following simplified equations:
$$[Mg] + [O] \rightarrow MgO(s)$$
$$[Mg] + [S] \rightarrow MgS(s)$$
These reaction products can rise to the metal surface because they are less dense than the iron melt. If the foundry does not skim the ladle properly, if the pouring basin is poorly designed, or if the gating system does not trap the slag, the inclusions will be carried into the casting.
Secondary slag is more complex. It is generated when the liquid metal surface comes into contact with the air or with oxidizing gases in the mold cavity. A thin solid oxide skin forms at the free surface. If the metal flow is smooth and the surface remains intact, this oxide skin may not enter the metal. However, if the metal is turbulent, if there is a free fall, if there is splashing, or if the stream becomes discontinuous, the oxide film can be folded into the bulk liquid. This produces thin, branched, film-like inclusions that are very difficult to remove once they are inside the casting.
The tendency for film entrainment can be described by the Weber number, which compares the inertia force of the liquid with the surface tension force:
$$We = \frac{\rho v^2 L}{\sigma}$$
where \( \rho \) is the density of liquid ductile iron, \( v \) is the local flow velocity, \( L \) is a characteristic length, and \( \sigma \) is the surface tension. When the Weber number becomes too high, the free surface becomes unstable and oxide films may be folded into the liquid. In practice, it is important to keep the filling velocity below a critical value, especially at the ingates and in the mold cavity.
I also considered the Reynolds number, because turbulent flow promotes the continuous renewal of the free surface and increases the probability of surface oxidation:
$$Re = \frac{\rho v D_h}{\mu}$$
where \( D_h \) is the hydraulic diameter of the flow channel and \( \mu \) is the dynamic viscosity of the melt. Although liquid metal casting is almost always turbulent, excessive velocities generate severe turbulence and worsen the oxide entrainment problem. For this reason, gating system design is one of the most important controls for ductile iron casting quality.
In the defective diffusion-body casting, the large branched inclusions were almost certainly secondary slag. They were generated by the interaction between the liquid ductile iron and the atmosphere during pouring. The gating system allowed the liquid to enter the mold with too much velocity and with a free-fall effect, creating waves, droplets, and folded oxide films. Once these films were submerged, they became trapped in the solidifying casting and appeared as dark, branched inclusions.
4. Analysis of the Original Gating System
After recognizing that the defect was a filling-related secondary slag problem, I focused on the original gating system. The original design was a closed gating system with a sprue-to-runner-to-ingate area ratio of:
$$F_{\text{sprue}} : F_{\text{runner}} : F_{\text{ingate}} = 1 : 2.07 : 0.83$$
This system used a 70 mm diameter ceramic sprue tube. The sprue area was 38.465 cm². The runner consisted of two trapezoidal runners with dimensions 40/60 × 80 mm, giving a total runner area of 80.00 cm². The ingates were eight flat gates with dimensions 38/42 × 10 mm, giving a total ingate area of 32.00 cm². The original gating system was a middle-part gate design, which means that the metal entered the mold cavity at the middle height of the casting.
| Parameter | Original Design | Modified Design |
|---|---|---|
| System type | Closed gating system | Open gating system with filters |
| Area ratio | 1 : 2.07 : 0.83 | 1 : 2.17 : 2.70 |
| Sprue | 70 mm ceramic tube, 38.465 cm² | 60 mm ceramic tube, 28.27 cm² |
| Runner | Two trapezoids 40/60 × 80 mm, 80.00 cm² | Two trapezoids 35/100 × 90 mm, 60.75 cm² |
| Ingate | Eight flat gates 38/42 × 10 mm, 32.00 cm² | Six flat gates 80/90 × 15 mm, 76.50 cm² |
| Choke location | Ingates | Sprue |
| Calculated ingate velocity | Approximately 1.5 m/s or higher | Approximately 1.08 m/s |
The middle-part gating arrangement had an important advantage: it helped the casting feed naturally because the metal entered near the middle of the casting and could promote a good temperature gradient. However, it also had a serious disadvantage. The metal exited from the ingates at a very high velocity. I calculated the flow velocity from the ingate area and the pouring rate. For a poured weight of 2000 kg and a pouring time of about 30 seconds, the mass flow rate is:
$$\dot{m} = \frac{W}{t_f} = \frac{2000 \text{ kg}}{30 \text{ s}} = 66.7 \text{ kg/s}$$
Using the density of liquid ductile iron, approximately 7000 kg/m³, the volumetric flow rate is:
$$Q = \frac{\dot{m}}{\rho} = \frac{66.7}{7000} = 0.00952 \text{ m}^3/\text{s}$$
The original ingate area was 32.00 cm², or 0.0032 m². The corresponding ingate velocity was:
$$v_{\text{ingate}} = \frac{Q}{A_{\text{ingate}}} = \frac{0.00952}{0.0032} = 2.98 \text{ m/s}$$
This is a very high velocity. Even if I include some friction losses and a lower effective metal head, the reality was that the metal entered the mold with a velocity above 1.5 m/s. In ductile iron casting, such a velocity is dangerous because it creates severe turbulence, jetting, and surface film entrainment. In addition, after leaving the middle ingates, the molten iron had to fall into the lower parts of the mold or travel upward along the cavity, generating secondary waves and promoting further oxidation.
The original system also had an unfavorable flow pattern at the ingate. The ingate area was small in relation to the runner area, which is typical of a closed system. This caused the metal to accelerate strongly at the gate. The high kinetic energy of the stream created splashing against the core and the mold wall. The splashed droplets oxidized rapidly and then settled into the liquid pool, becoming inclusions. This explained the location of the slag on the inner wall and upper surface.
5. Gating System Redesign
Once I had identified the root cause, I decided to redesign the gating system completely. The main objectives of the redesign were to reduce the ingate velocity, ensure a smoother and more continuous metal flow, avoid free-fall and splashing, and remove any primary slag before it entered the mold cavity.
I chose an open gating system, also called a pressurized or non-pressurized system depending on terminology. In this system, the sprue is the choke, and the total ingate area is larger than the total runner area, which is larger than the sprue area. The flow area therefore increases as the metal moves downstream. This keeps the metal flowing full in the sprue, reduces the pressure head at the ingates, and allows the velocity to decrease before the metal enters the mold cavity.
The modified gating ratio was selected as:
$$F_{\text{sprue}} : F_{\text{runner}} : F_{\text{ingate}} = 1 : 2.17 : 2.70$$
I selected a 60 mm diameter ceramic sprue tube as the choke element. The sprue cross-sectional area is:
$$A_{\text{sprue}} = \frac{\pi d^2}{4} = \frac{\pi \times 60^2}{4} = 2827 \text{ mm}^2 = 28.27 \text{ cm}^2$$
The runner system was redesigned with two trapezoidal runners having dimensions 35/100 × 90 mm. The total runner area was 60.75 cm². The six ingates were made larger and lower in height, each with dimensions 80/90 × 15 mm. The total ingate area was 76.50 cm². With this arrangement, the choke remained at the sprue, and the downstream sections were no longer the limiting factor.
Using the same pouring rate of 2000 kg in 30 seconds, the volumetric flow rate remains:
$$Q = 0.00952 \text{ m}^3/\text{s}$$
The modified total ingate area is 76.50 cm², or 0.00765 m². Therefore the ingate velocity is:
$$v_{\text{ingate}} = \frac{0.00952}{0.00765} = 1.24 \text{ m/s}$$
With slight differences in actual pouring time and temperature, the actual calculated value was about 1.08 m/s. This represented a significant reduction compared with the original system. The lower velocity reduced the kinetic energy of the entering stream, reduced splashing, and made it easier for the metal to fill the mold without folding over the surface oxide film.
I also considered the need to avoid excessive fall of the metal inside the mold cavity. The ingates were designed to enter the mold in a direction that favored smooth upward filling. By controlling the metal entry point and distributing the metal through multiple large ingates, I reduced the local velocity and prevented the creation of a high-velocity jet impinging against the core.
5.1 Selection of Ceramic Foam Filters
In addition to changing the gating geometry, I added ceramic foam filters to the modified gating system. The filters served two essential functions: they removed primary slag particles from the melt, and they helped to stabilize the flow before the metal entered the ingates.
I selected ceramic foam filters with dimensions of 120 mm × 120 mm × 20 mm. The selection of the number of filters was based on the total poured weight and the practical capacity of each filter. Based on previous foundry experience, a filter of this size can safely pass approximately 400 kg of ductile iron under the given pouring conditions. For a poured weight of 2000 kg, the required number of filters is:
$$n_{\text{filter}} = \frac{W_{\text{poured}}}{W_{\text{filter capacity}}} = \frac{2000}{400} = 5$$
To provide an extra margin of safety and to reduce the risk of premature blockage, I installed six filters in the runner system. The filters were placed at the junction between the upper runner and the lower runner. In this location, the metal had already passed through the initial runner section, so heavy slag droplets had time to float upward. The ceramic foam filter then captured the remaining fine inclusions before the metal reached the ingates.
The filter arrangement also created a desirable pressure drop. The pressure drop helped to reduce the flow velocity and made the metal stream more uniform. In the modified gating system, the total filter area was large enough to avoid acting as a choke. Each filter had a nominal area of 144 cm². With six filters, the total nominal filter area was 864 cm². Even if the open porosity of the ceramic foam was around 80%, the effective open area remained much larger than the sprue choke area, so the filters did not restrict the pouring time.
| Item | Value |
|---|---|
| Filter material | Ceramic foam |
| Filter size | 120 mm × 120 mm × 20 mm |
| Capacity per filter | Approximately 400 kg |
| Number of filters installed | 6 |
| Total nominal filter area | 864 cm² |
| Location | Junction between upper and lower runners |
6. Production Verification
After the redesigned gating system was introduced, I arranged a production trial. The first castings were inspected carefully using visual examination, dye penetrant testing, and metallographic sampling. The results were dramatic. The severe slag inclusions on the top surface and inner wall disappeared. The castings showed a clean as-cast surface, and the internal quality was consistently better than before.
More than one hundred consecutive production castings were made without a single scrap caused by slag inclusion. The defect rate dropped from the unacceptable level of more than 12% to less than 1%. In fact, after the first few verification castings, the slag defect disappeared completely from the critical locations. The castings met all customer acceptance criteria, including pressure tightness, dimensional accuracy, and machinability.
I also repeated the metallographic examination at the same locations that had previously shown severe slag inclusions. The microstructure was clean and free of branched oxide films. No large dendritic inclusions were observed. This confirmed that the gating system modification had eliminated the source of the secondary slag.
| Verification Item | Before Modification | After Modification |
|---|---|---|
| Scrap rate due to slag | Greater than 12% | Less than 1% |
| Inclusion size in critical section | 600 to over 1000 μm, dendritic | No visible branched inclusions |
| Inclusion location | Top face and inner wall | No critical location defects |
| Pressure test | Occasional leaks | No leaks |
| Customer acceptance | Rejected batches | Accepted for mass supply |
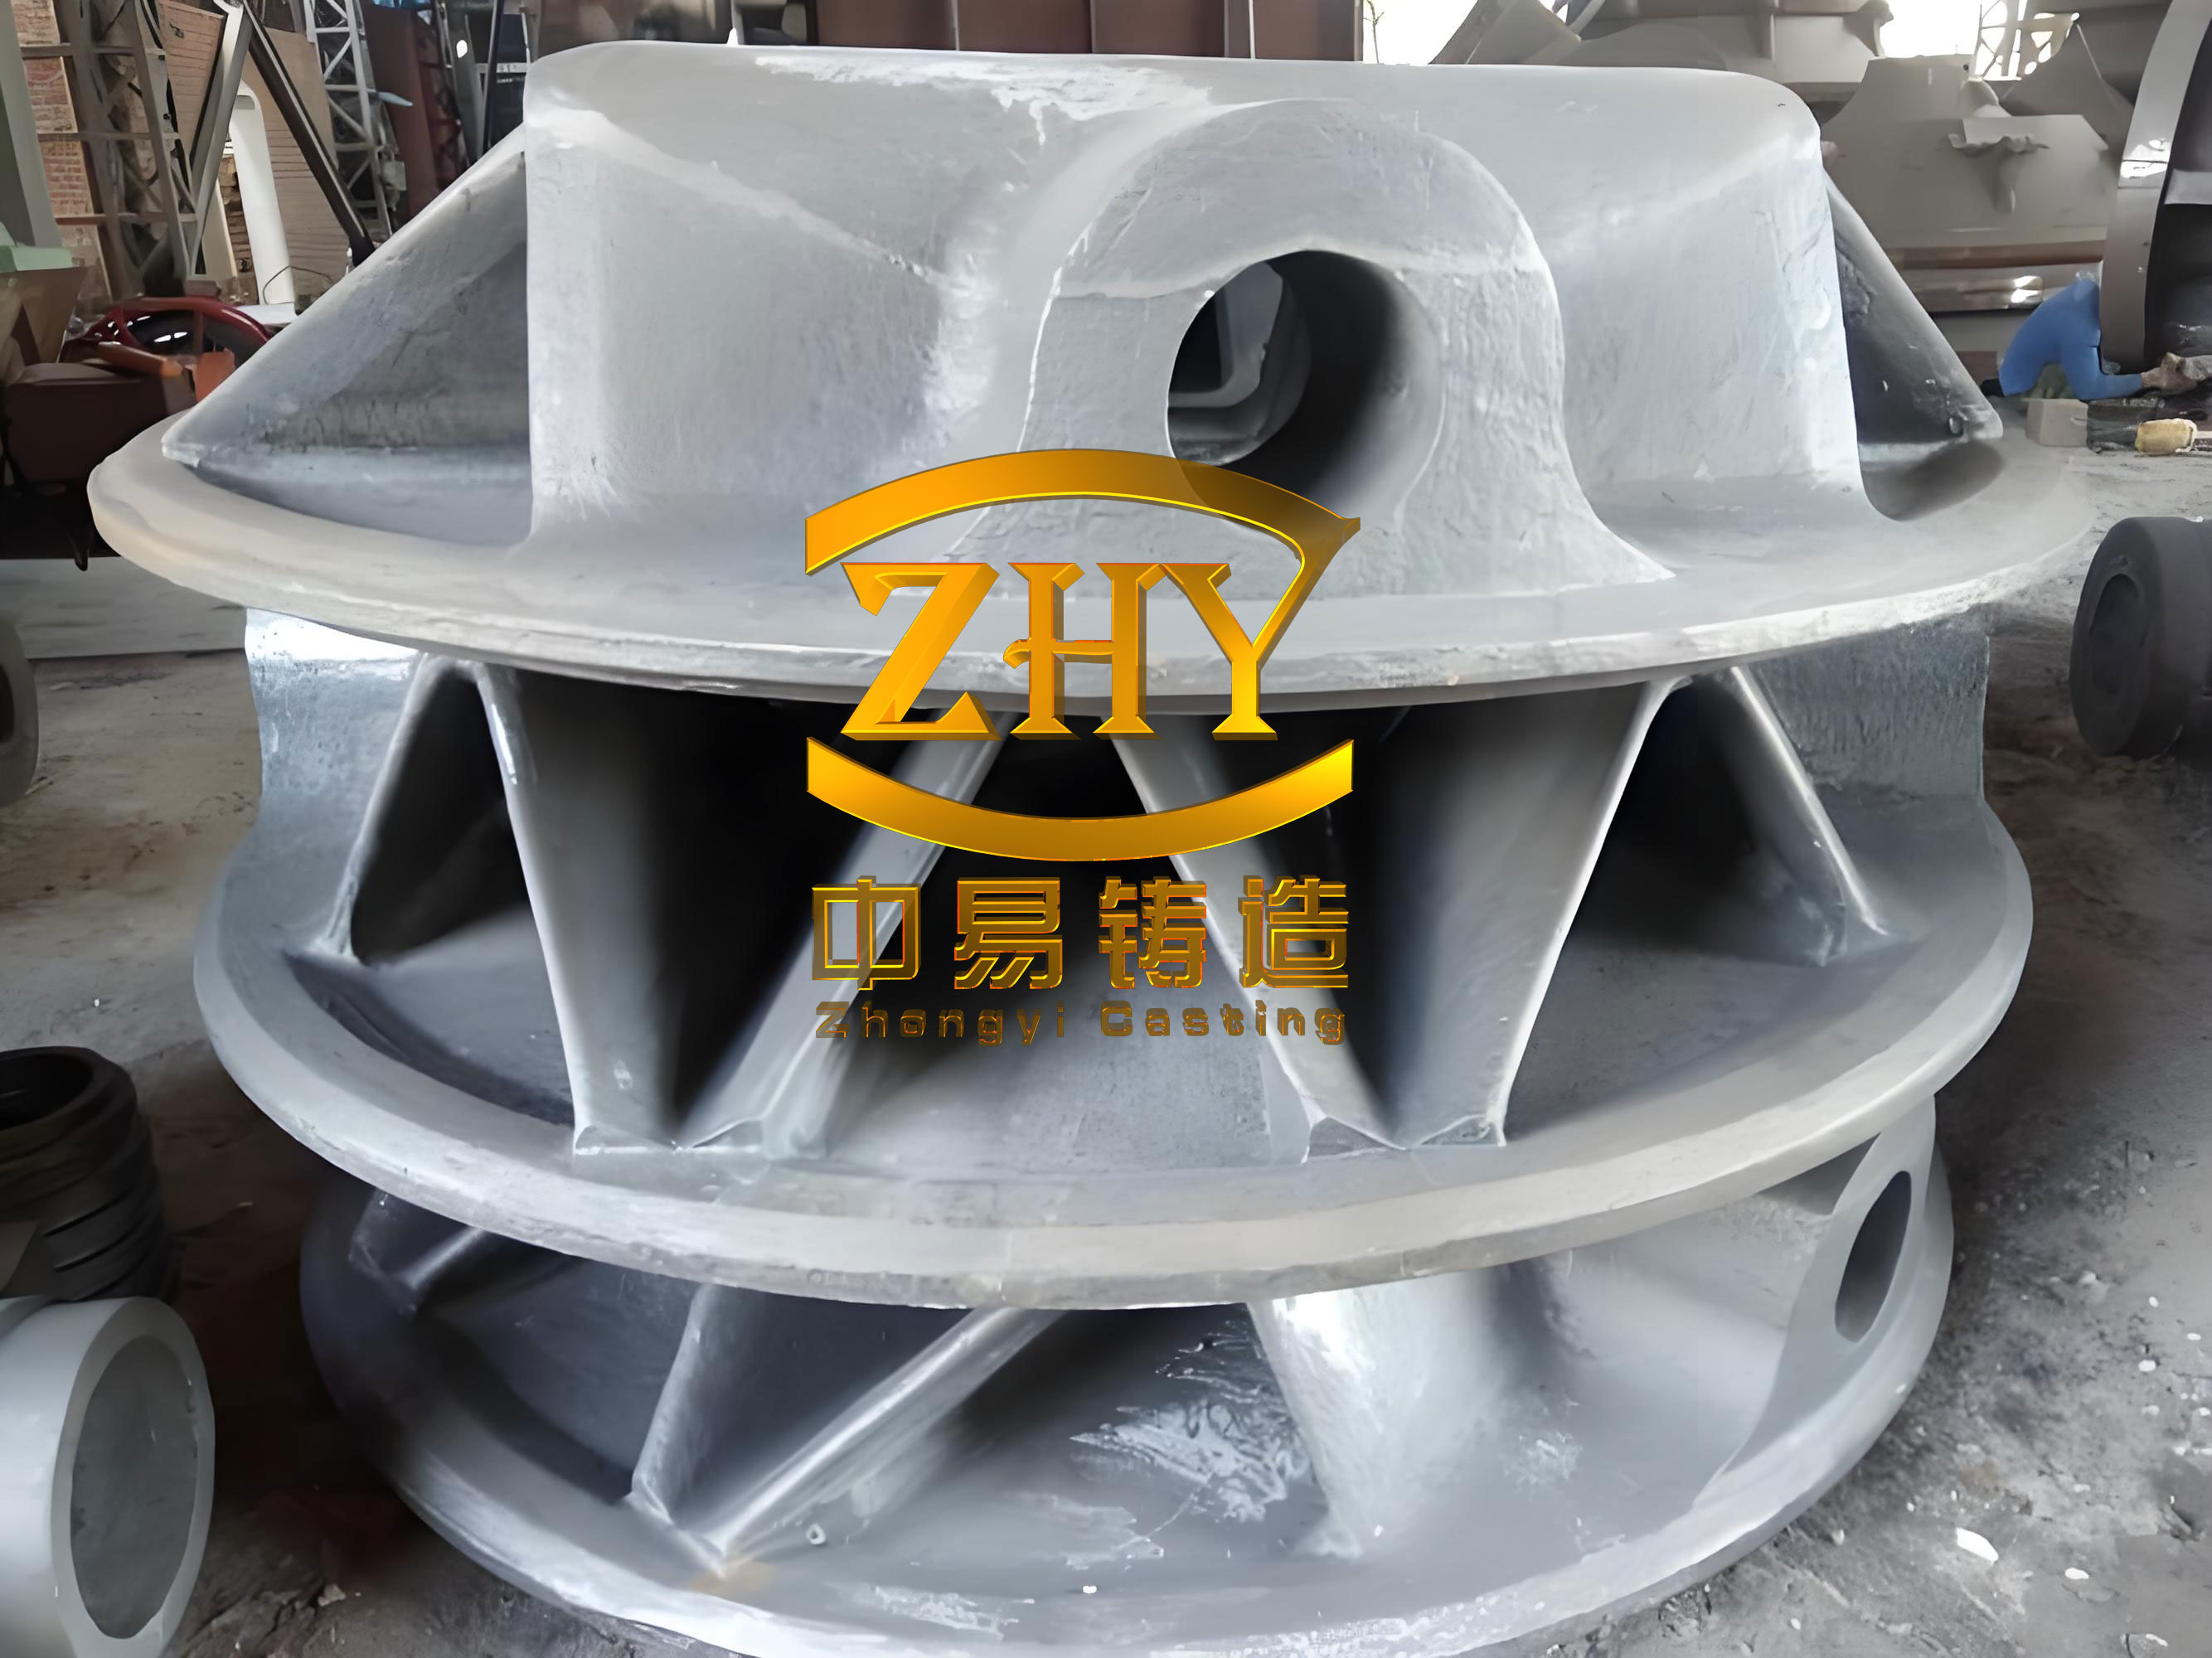
The image below shows a representative ductile iron casting produced after the gating system was modified. The surface is clean, the details are sharp, and the critical openings are free from the slag layers that had previously caused so much trouble.
7. Discussion of the Gating System Formula
One of the key lessons I learned from this ductile iron casting problem is that the gating ratio must be selected according to the actual behavior of the molten metal. A closed gating system can be useful for preventing air aspiration in the sprue, but if the ingates are too small, the velocity becomes excessive. An open gating system, where the sprue is the choke, is generally safer for ductile iron casting because it allows the metal to decelerate as it moves toward the ingates.
In the original closed system, the ingate area was the smallest section. The metal was forced through a narrow opening at high pressure and high speed. This is often suitable for non-oxidizing metals or for small castings, but for heavy ductile iron casting with a large poured weight, it creates severe surface turbulence. The free surface of the metal is repeatedly broken, and each new surface reacts with the mold atmosphere to form a fresh oxide film. When the film becomes folded into the bulk liquid, it remains as a slag inclusion.
The modified open system worked better because the choke area was placed at the sprue. The sprue controlled the metal flow rate, while the large ingates reduced the velocity and allowed the metal to enter the mold cavity gently. The following general formula can be used to estimate the choke area for this type of gating system:
$$A_{\text{choke}} = \frac{W}{\rho t_f v_{\text{choke}}}$$
where \( W \) is the poured weight, \( \rho \) is the density of the liquid ductile iron, \( t_f \) is the pouring time, and \( v_{\text{choke}} \) is the allowed velocity at the choke. By selecting a low velocity at the choke and then opening the runner and ingate areas, I was able to create a filling system that did not damage the liquid metal.
For ductile iron casting, I also paid attention to the pouring time. The pouring time should be short enough to avoid excessive temperature loss and long enough to avoid violent flow. In this case, the casting was designed for a pouring time of 30 ± 5 s. I verified that the modified gating system was capable of completing the pour within this window.
8. Influence of Metal Chemistry and Melt Treatment
Although the gating system was the primary cause of the slag defect, I also reviewed the melt treatment practices for this ductile iron casting. The spheroidization treatment was carried out using a magnesium-containing nodulizer. During spheroidization, the magnesium reacts vigorously with oxygen and sulfur. This reaction produces a large amount of magnesium oxide and magnesium sulfide. If these products are allowed to enter the mold, they can become primary slag inclusions.
The chemistry of the melt has a strong influence on the amount of slag formed in ductile iron casting. High sulfur content, for example, increases the amount of magnesium sulfide formed during spheroidization. Low pouring temperature increases the viscosity of the slag and makes it more difficult for the slag to float out of the liquid metal. Residual magnesium content must be controlled within a suitable range. Excessive magnesium is beneficial for nodularity but can also increase the amount of oxide slag.
I reviewed the target chemistry for the QT400-18 material and ensured that the sulfur content was low enough before spheroidization. I also checked the residual magnesium and rare earth contents after treatment. The target ranges were as follows:
| Element | Target Range | Effect on Ductile Iron Casting |
|---|---|---|
| Carbon | 3.5–3.9% | Promotes graphitization and fluidity |
| Silicon | 1.8–2.3% | Promotes ferrite, affects oxide film |
| Manganese | 0.2–0.5% | Affects pearlite, not a slag driver |
| Phosphorus | Below 0.04% | Reduces brittleness |
| Sulfur | Below 0.02% | Reduces magnesium sulfide slag |
| Residual magnesium | 0.03–0.06% | Required for nodularity |
| Rare earth | 0.01–0.03% | Refines graphite, stabilizes nodulizer |
I also made sure that the spheroidized ductile iron was not held in the ladle for too long before pouring. Holding the treated iron promotes the reversion of magnesium and increases the amount of dross. The pouring temperature was maintained at 1315–1330 °C, which gave the slag a better chance to float and coalesce on the surface of the metal in the gating system. However, because the secondary slag was generated during filling, melt chemistry alone could not solve the problem. The gating system had to be corrected at the same time.
9. Flow Control and Filtering Effects
The role of the ceramic foam filter in this ductile iron casting was not limited to mechanical filtration. It also served as a flow conditioner. When the liquid ductile iron passed through the porous ceramic structure, the large eddies were broken down into smaller eddies, and the velocity profile became more uniform. This reduced the local high-velocity jets that could otherwise travel through the runner and enter the mold cavity.
The filtering effect can be described in terms of the particle capture mechanism. Ceramic foam filters capture inclusions by direct interception, inertial impaction, and surface attraction. In ductile iron casting, the filter also provides a solid surface on which oxides can adhere. The filter becomes coated with a layer of slag, and this layer continues to capture additional inclusions as the metal passes through.
For this diffusion-body casting, I placed the filters in the horizontal runner at the transition between the upper and lower sections. This location was chosen because the runners could be opened to insert the filters and then closed to make the system tight. The filters covered the full cross-section of the runner, so all of the liquid metal had to pass through the porous ceramic foam before reaching the ingates.
One important practical consideration is that the filter area must be large enough to allow the required pouring rate without excessive pressure buildup. If the filter is too small, the metal flow will be restricted, the pouring time will increase, and the metal may cool too much before entering the mold cavity. I calculated the required filter area using the following relationship:
$$A_{\text{filter}} = \frac{W}{\rho t_f v_{\text{filter}}}$$
where \( v_{\text{filter}} \) is the allowed velocity through the filter. In practice, I relied on the measured capacity of the ceramic foam filter and selected six filters to ensure that the effective open area was adequate.
The modification was also beneficial for the temperature distribution of the casting. Because the mold filled more calmly, there was less surface turbulence and less entrainment of cold oxide films. The castings solidified with a more uniform temperature field, which improved the feeding behavior and reduced the risk of shrinkage porosity.
10. Preventive Measures and Process Control
After solving the problem, I introduced several preventive measures to maintain stable production of this ductile iron casting. The first measure was to standardize the gating system design. The open gating ratio, filter size, and filter position were documented as the standard process. No engineer could change the gating system without repeating the design verification.
The second measure was to improve the quality of the ceramic foam filters. I established clear acceptance criteria for the filters, including visual inspection, porosity, and high-temperature resistance. Damaged filters or filters with blocked pores were rejected before use.
The third measure was to train the foundry operators. The operators learned how to place the filters correctly, how to prevent mold sand from entering the gating system, and how to check the runner assembly before closing the mold. Operator awareness was essential because even a perfect gating system can fail if the mold is closed carelessly.
The fourth measure was to inspect the castings systematically after solidification. The locations that had previously shown slag defects were monitored with metallographic sampling and visual examination for the first several production batches. This allowed me to confirm that the problem had been solved and to detect any future variation before it became a major scrap issue.
| Control Point | Control Method | Expected Benefit for Ductile Iron Casting |
|---|---|---|
| Melt chemistry | Spectrometric analysis before and after treatment | Reduces primary slag formation |
| Spheroidization process | Control nodulizer weight, reaction time, skimming | Prevents transfer of ladle slag into mold |
| Pouring temperature | Infrared pyrometer | Maintains fluidity and slag floatability |
| Gating system | Open ratio 1:2.17:2.70 | Reduces ingate velocity and turbulence |
| Filter placement | Six ceramic foam filters in runner | Removes primary slag and stabilizes flow |
| Mold assembly | Inspection of cores, filters, and runner seals | Prevents sand erosion and mold debris entry |
11. Metallurgical Verification
After the modification, I compared the metallurgical quality of the castings produced before and after the gating system redesign. The most important difference was in the inclusion content. Before the modification, the top section of the casting contained large, branched inclusions that were clearly visible at low magnification. After the modification, the same critical section was clean and free from these defects.
I also checked the graphite nodularity of the ductile iron casting. The material still met the QT400-18 specification. The nodularity was above the required minimum, and the ferrite content was consistent with the intended mechanical properties. This confirmed that the reduction in slag did not come at the expense of the metallurgical structure.
The absence of slag inclusions also had a positive effect on the mechanical properties. In previous defective castings, the slag inclusions acted as internal notches and reduced the tensile strength and ductility. After the modification, the tensile test samples showed stable elongation values, and there was no evidence of premature fracture initiated by an oxide film.
For ductile iron casting, the quality of the liquid metal is not judged only by its composition. It is also judged by the cleanliness of the metal and the way it is introduced into the mold. A clean melt can still be ruined by poor gating design. Conversely, a good gating system can compensate for some of the unavoidable dross that is created during spheroidization and pouring.
12. Comparison Between Closed and Open Gating Systems
The experience with this diffusion-body ductile iron casting gave me a clear comparison between closed and open gating systems. I have summarized the main differences in the following table:
| Feature | Closed Gating System | Open Gating System with Filters |
|---|---|---|
| Choke location | Ingates or narrowest downstream section | Sprue or filter |
| Flow velocity at ingates | High, often above 1.5 m/s | Lower, often near 1.0 m/s |
| Turbulence | Severe, especially at gates | Reduced, more stable front |
| Slag removal | Depends on runner geometry | Enhanced by ceramic foam filter |
| Risk of secondary slag | High | Low |
| Suitable for heavy ductile iron casting | Not recommended for large critical castings | Recommended |
This comparison is especially valid for heavy-section ductile iron casting. When the pouring weight exceeds one ton, the volumetric flow rate is high, and the kinetic energy of the metal at the ingates is very large. If the ingates are small, the metal jet can penetrate deep into the mold cavity and create severe surface turbulence. The use of an open gating system with multiple large ingates distributes the metal more evenly and prevents such jetting.
13. Importance of Gating Ratio in Ductile Iron Casting
Gating ratio is a fundamental design parameter in ductile iron casting. It determines where the metal flow is controlled and how the velocity changes along the flow path. The ratio can be expressed as:
$$x : y : z = A_{\text{sprue}} : A_{\text{runner}} : A_{\text{ingate}}$$
In a closed system, the ratio often has a value less than 1 for the last term, meaning the ingate area is the smallest. In an open system, the last term is greater than 1, meaning the ingate area is the largest. For ductile iron casting, I generally prefer an open system for components where slag inclusions are a known risk.
The modified ratio of 1 : 2.17 : 2.70 was chosen based on practical foundry data. The large runner and ingate areas reduced the velocity and also created favorable conditions for slag to float out of the metal. The ceramic foam filters provided additional protection by intercepting slag particles that could not float out naturally.
The theoretical basis for this design can be explained using the continuity equation:
$$Q = A_1 v_1 = A_2 v_2$$
If the cross-sectional area increases from the sprue to the ingates, then the velocity must decrease. This is exactly what I wanted to achieve in this ductile iron casting. The sprue was kept small enough to act as the choke, while the runner and ingates were enlarged to slow down the metal.
Of course, the continuity equation is an idealization. In real foundry practice, there are friction losses, turbulence losses, and local contraction effects. The actual velocity may be somewhat lower than the ideal value. Nevertheless, the equation provides a useful framework for estimating the flow behavior and for comparing different gating designs.
14. Lessons Learned
This problem taught me several lessons about ductile iron casting. The first lesson is that slag inclusions must be analyzed from both a metallurgical and a fluid-flow perspective. It is not enough to assume that all slag comes from dirty melting practice. In this case, the root cause was the gating system, not the melting process.
The second lesson is that casting design must be reviewed before production. If the original gating system had been tested and optimized earlier, the foundry could have avoided the high scrap rate and the lost production time. The cost of modifying a mold pattern and gating system is small compared with the cost of scrapping more than twelve percent of the production.
The third lesson is that filters should be considered as a necessary part of the gating system for critical ductile iron castings. Filters remove inclusions, reduce turbulence, and stabilize the flow. They are especially valuable for heavy castings, where the liquid metal has a long distance to travel and a long time to oxidize.
The fourth lesson is that process stability requires complete documentation. After solving the problem, I wrote down the new gating parameters, the filter specifications, the pouring instructions, and the inspection criteria. This documentation helped the foundry reproduce the successful results in every subsequent batch.
15. Recommendations for Foundry Engineers
For foundry engineers facing similar slag problems in ductile iron casting, I recommend the following steps. First, examine the defect location accurately. Secondary slag tends to appear in the upper surfaces, around cores, and in regions where the metal must change direction. Primary slag tends to appear near gates, runner ends, and riser contacts. The location can tell you which mechanism is dominant.
Second, perform metallographic analysis. A polished sample will reveal whether the inclusions are granular or dendritic. Granular inclusions are more likely to be primary slag. Dendritic and film-like inclusions are more likely to be secondary oxides. This distinction is essential for choosing the right corrective action.
Third, calculate the ingate velocity. For ductile iron casting, an ingate velocity below 1.0 m/s is often preferable for critical sections. Velocities above 1.5 m/s should be avoided unless there is very strong filtering and very careful flow control. If the calculated velocity is too high, enlarge the ingates or change the choke location.
Fourth, use ceramic foam filters. The filters should be large enough and numerous enough to handle the total pour weight. For this diffusion-body casting, I used six filters for a poured weight of 2000 kg. This provided an adequate safety margin and prevented the filters from slowing down the pour.
Fifth, validate the modification with a production trial. Do not change the process based only on calculations. Produce a trial casting, inspect it thoroughly, section it if necessary, and compare the metallography before and after. Only after the trial confirms the improvement should the new design be accepted as the standard.
16. Conclusions
The slag inclusion problem in this diffusion-body ductile iron casting was solved by understanding the root cause and applying a systematic engineering approach. The original closed gating system caused high velocity, turbulence, and oxide film entrainment. The slag defects were located in the top face and inner wall, and metallography showed large branched dendritic inclusions typical of secondary slag.
By changing to an open gating system with a sprue-to-runner-to-ingate ratio of 1 : 2.17 : 2.70, I reduced the ingate velocity from more than 1.5 m/s to approximately 1.08 m/s. I also added six ceramic foam filters to remove primary slag and to stabilize the metal flow. The combination of these changes eliminated the defect.
The production results were outstanding. More than one hundred continuous castings were produced without a single scrap caused by slag inclusion. The defect rate dropped from more than 12% to less than 1%. The castings met all customer requirements and were delivered in serial production.
This experience demonstrates that ductile iron casting requires more than just correct metallurgy. The flow behavior of the liquid metal must be controlled by a rational gating system, appropriate filters, and stable process parameters. When all of these factors are aligned, slag inclusions can be reliably prevented, and the full mechanical potential of ductile iron casting can be achieved.
In the future, I will continue to use this open gating system with ceramic foam filters as the preferred solution for heavy ductile iron casting components where oxide film defects are a concern. The same method can be applied to other castings with similar geometry, weight, and metallurgical requirements.