
I approach the design and manufacturing problem of the mine scraper conveyor central groove from the standpoint of service duty, structural continuity, wear resistance, repairability, and long-term reliability. In my assessment, the central groove is not simply a structural beam or a wear plate. It is a combined load-bearing, guiding, sliding, and impact-resistant component that must survive repeated coal loading, chain tension, abrasive fines, occasional rock intrusion, and severe dynamic shocks. For this reason, I do not view the selection between cast-weld fabrication, lost foam casting, and sand casting as a simple shop-floor preference. I treat it as a system-level decision that affects stress distribution, weld integrity, dimensional stability, porosity, heat-treatment response, field repair, and total cost of ownership. After comparing the available routes, I conclude that a carefully controlled sand casting route can provide the best balance of structural integrity, wear performance, repairability, and industrial scalability for the central groove of a mine scraper conveyor.
My first principle is that the central groove should behave as an integrated load path rather than as an assembly of plates and cast ends joined by welds. In the traditional cast-weld route, the side rails, pin seats, and other end features are cast, while the middle plate, bottom plate, and guard plates are cut from steel plate and welded into position. That approach is familiar and has a relatively low initial tooling barrier, but it creates heat-affected zones, residual stresses, and geometric discontinuities exactly where the component experiences alternating bending, torsion, and abrasion. When I evaluate failure modes, I consistently see that the weld toe, partial penetration, undercut, slag inclusion, and plate-to-casting mismatch can become initiation sites. A sand casting route, by contrast, allows me to create a monolithic central groove in which the load path is continuous and the wear surfaces can be tailored through alloy composition, mold design, feeding, cooling, and heat treatment.
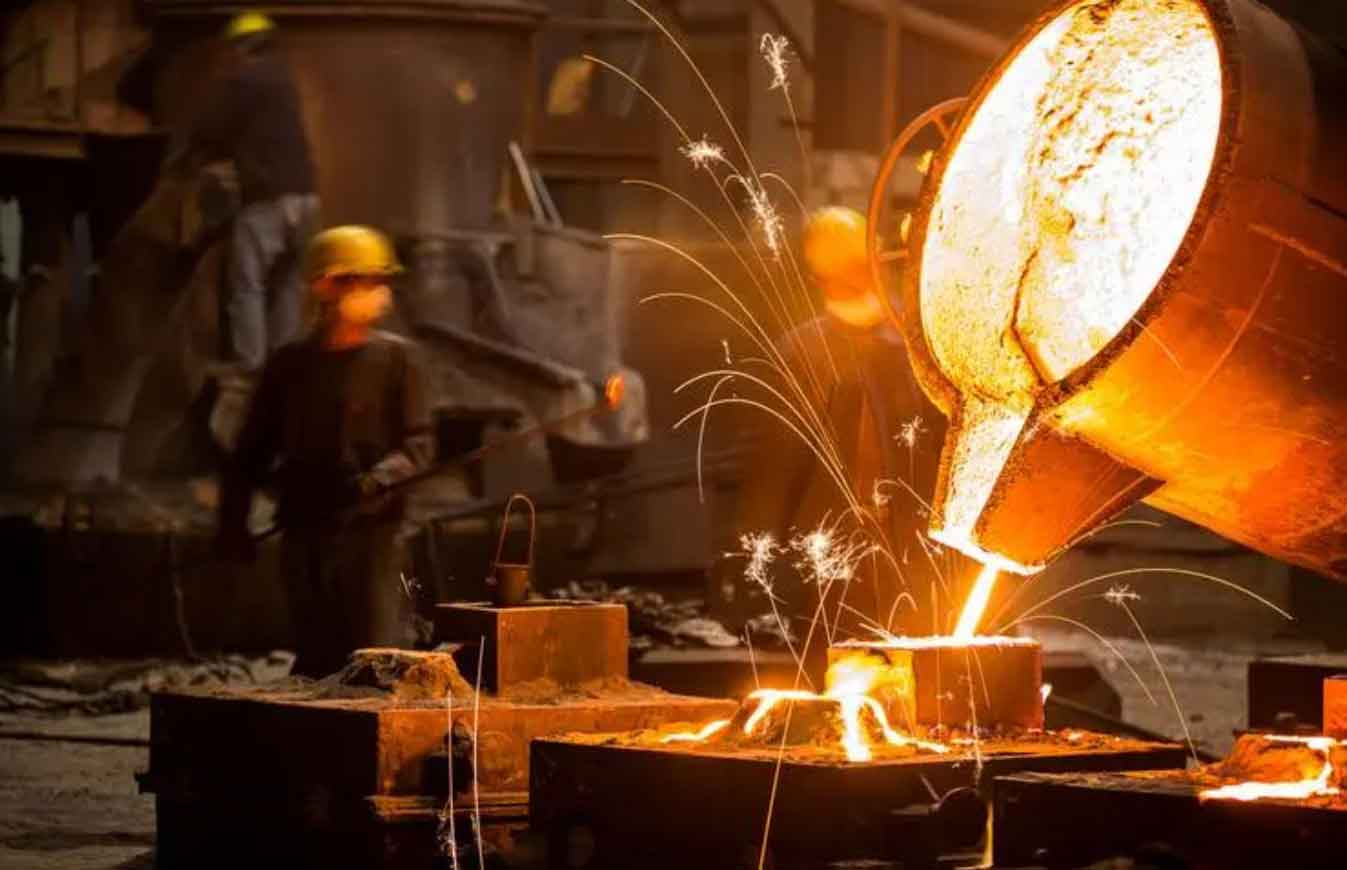
I also recognize that sand casting is not automatically superior merely because it produces a single-piece component. The quality of a sand casting depends on mold rigidity, sand compaction, core strength, gating, risering, pouring temperature, filling velocity, solidification sequence, shakeout time, and heat treatment. If those variables are not controlled, sand casting can produce shrinkage porosity, gas porosity, sand burn-on, veining, cold shut, misrun, hot tears, distortion, and inconsistent hardness. Therefore, I treat sand casting as a precision process discipline rather than a crude alternative. When I specify sand casting for the central groove, I define the process window, the inspection plan, and the corrective actions for each likely defect. My objective is to make the sand casting route repeatable enough that the central groove achieves the required strength, toughness, wear life, and repairability in high-load underground service.
To compare the routes quantitatively, I use several engineering relationships. The fill rate of the gating system can be expressed as:
$$ Q = A v $$
where Q is volumetric flow rate, A is the cross-sectional area of the gate, and v is the metal velocity. The solidification time of a casting section can be estimated by Chvorinov’s rule:
$$ t_s = B \left(\frac{V}{A}\right)^n $$
where t_s is solidification time, B is a mold constant, V is casting volume, A is heat-transfer surface area, and n is typically close to 2 for many sand castings. The thermal modulus is:
$$ M = \frac{V}{A} $$
I use the thermal modulus to compare feeding requirements among the side rail, middle plate, bottom plate, and pin seat regions. A region with a larger modulus cools more slowly and requires more feeding. The cooling rate can be approximated as:
$$ R_c = \frac{T_p – T_m}{t_s} $$
where T_p is pouring temperature and T_m is mold temperature. I also track solidification shrinkage:
$$ \epsilon_s = \frac{V_l – V_s}{V_s} \times 100\% $$
where V_l is liquid volume and V_s is solid volume. These equations help me translate shop parameters into physical consequences. For example, if I increase pouring temperature, I improve fluidity but also increase shrinkage demand and gas absorption risk. If I increase gate velocity, I reduce misrun risk but increase mold erosion and turbulence. The sand casting process is therefore a constrained optimization problem, not a single set of fixed numbers.
In my comparison of manufacturing routes, I assess five main criteria: structural continuity, wear resistance, weldability and repair, dimensional stability, and economic scalability. The traditional cast-weld route scores well on initial tooling simplicity but poorly on weld fatigue and distributed strength. The lost foam casting route can produce a monolithic part with good wear resistance, but I find that large castings may suffer from lower densification, distortion, and difficult repair because of the high-strength alloy and the absence of convenient weld repair. The sand casting route, in my evaluation, offers a monolithic structure, good wear resistance, weldability when the alloy is properly selected, low equipment investment relative to lost foam, and mature process control. The following table summarizes my route comparison.
| Criterion | Cast-weld fabrication | Lost foam casting | Sand casting |
|---|---|---|---|
| Structural continuity | Interrupted by welds and heat-affected zones | Monolithic, but large-section density may vary | Monolithic with controllable section feeding |
| Wear resistance | Depends on plate grade and weld overlay | High with wear-resistant alloy | High with low-alloy steel and heat treatment |
| Weld repair | Easy but weld quality is the original weakness | Difficult for high-alloy wear steel | Good when low-alloy Si-Mn steel is used |
| Dimensional stability | Distortion from welding and assembly | Distortion and later straightening required | Stable with rigid molds, cores, and fixtures |
| Tooling investment | Low to moderate | High | Moderate |
| Energy and emissions | Moderate, multiple process steps | High, pattern decomposition emissions | Moderate with sand reclamation |
| Production maturity | Widely used | Specialized | Mature and widely applicable |
| Overall fit for high-load central groove | Limited by weld fatigue | Promising but constrained by distortion and repair | Best balance in my assessment |
I define the service load case before I finalize the sand casting design. The central groove experiences vertical loading from the conveyed material, chain pull, bending between supports, torsion from uneven loading, friction from the chain and material, and impact from lump coal or rock. The wear rate can be represented by an Archard-type relationship:
$$ V_w = K \frac{F_n L}{H} $$
where V_w is wear volume, K is a wear coefficient, F_n is normal load, L is sliding distance, and H is surface hardness. This relationship tells me that increasing hardness is one of the most direct ways to reduce wear volume. However, I cannot simply maximize hardness because high hardness can reduce toughness and make the central groove more sensitive to impact cracking. I therefore target a balance: a low-alloy steel with sufficient hardenability, a tempered martensitic or bainitic structure, and a hardness range that resists abrasion while retaining impact toughness. In my sand casting route, I use silicon and manganese as the main alloying elements, with tight control of carbon, sulfur, phosphorus, and residual elements. This choice gives me a castable steel that can be welded and repaired, unlike many highly alloyed wear-resistant cast irons or specialized steels.
I also use fatigue relationships to evaluate the benefit of eliminating welds. The fatigue life can be described by a Basquin-type expression:
$$ \sigma_a = \sigma_f’ (2N_f)^b $$
where sigma_a is stress amplitude, sigma_f’ is fatigue strength coefficient, N_f is cycles to failure, and b is the fatigue strength exponent. Weld toes act as stress concentrators, so the local stress can be much higher than nominal stress. I represent this with a stress concentration factor:
$$ K_t = \frac{\sigma_{max}}{\sigma_{nom}} $$
In a cast-weld central groove, K_t at the weld toe can be significant, and the heat-affected zone may have lower toughness and higher residual stress. In a sand casting central groove, I can design generous fillets, gradual section transitions, and continuous ribs to reduce K_t. I can also place feeding and cooling so that the microstructure is more uniform. The result is not merely a cosmetic improvement. It changes the fatigue initiation site and extends the time required for a crack to become critical. I therefore view sand casting as a fatigue-life strategy as much as a shaping strategy.
My process architecture for the sand casting route begins with pattern and mold design, then proceeds through sand preparation, core making, molding, core setting, closing, melting, pouring, solidification, shakeout, cleaning, heat treatment, inspection, and machining. I use a stage-gate approach: no stage proceeds until its acceptance criteria are met. The process flow can be summarized in the following table.
| Stage | Main control variable | Acceptance criterion | Risk if uncontrolled |
|---|---|---|---|
| Pattern and tooling | Shrinkage allowance, draft, fillets, core print | Dimensions within drawing tolerance | Incorrect final size, poor mold filling |
| Sand preparation | Binder level, moisture, compactability, permeability | Stable green or no-bake strength | Sand erosion, gas defects, mold collapse |
| Core making | Core strength, venting, dimensional accuracy | No core shift or gas entrapment | Internal cavities, blowholes, veining |
| Molding | Compaction, mold hardness, parting line accuracy | Uniform mold cavity and rigid support | Distortion, flash, dimensional variation |
| Melting | Chemistry, temperature, time, cleanliness | Specified composition and low gas content | Inclusions, poor hardenability, gas porosity |
| Pouring | Temperature, rate, inclination, gating | Laminar fill and complete cavity fill | Cold shut, misrun, erosion, turbulence |
| Solidification | Riser size, chill placement, cooling sequence | Directional solidification toward risers | Shrinkage porosity, hot tears, cracks |
| Shakeout and cleaning | Cooling time, knock-out method, shot blasting | No quench cracking or residual sand | Cracking, burned-on sand, surface defects |
| Heat treatment | Normalizing, quenching, tempering | Uniform hardness and microstructure | Brittleness, soft spots, distortion |
| Inspection | Dimensional, ultrasonic, magnetic particle, hardness | Defect size below limits | Escaped defects, field failure |
I begin mold design by identifying the critical functional surfaces of the central groove. These include the chain running surface, the side guide surfaces, the pin seat areas, the bottom wear surface, and the mounting interfaces. I assign each surface a dimensional tolerance, a surface roughness target, and a machining allowance. The mold must produce a casting that is close enough to final shape to minimize machining while still allowing clean-up of scale, sand, and heat-treatment distortion. I do not use a single global shrinkage allowance. I apply differential allowances because thick sections, thin webs, and restrained cores cool at different rates. I estimate the thermal modulus of each region and adjust pattern dimensions accordingly.
In my sand casting mold design, I pay special attention to the bottom plate opening. A carefully placed opening can serve as a core print and a vent path, which helps stabilize the sand core and allows gas to escape during pouring. I also use anti-distortion ribs or tie bars on the middle plate where the section is long and relatively thin. These ribs are not part of the final component. They are temporary features that I remove after normalizing. In this way, I control distortion during cooling and heat treatment without leaving permanent stiffeners that could interfere with material flow or chain movement. Before closing the mold, I verify the core position with a dedicated checking template. If the core is shifted, I correct it before pouring, because core shift in a large sand casting can produce wall thickness variation that later becomes a crack initiation site.
| Element | Design purpose | Control method | Inspection point |
|---|---|---|---|
| Parting line | Simplify pattern removal and core setting | Place at a neutral surface with minimal mismatch | Parting line gap and flash check |
| Draft angle | Allow clean pattern withdrawal | Increase draft on deep pockets and side walls | Pattern dimensions and mold wall condition |
| Fillet radius | Reduce stress concentration and improve feeding | Use generous radii at re-entrant corners | Visual and dimensional check |
| Riser | Feed shrinkage during solidification | Size by thermal modulus and simulation | Riser cut surface and ultrasonic check |
| Gating system | Deliver clean metal at controlled velocity | Use runner, sprue, and ingate ratio to avoid turbulence | Pouring observation and defect audit |
| Chill | Promote directional solidification | Place chills near heavy sections | Microstructure and hardness mapping |
| Vent | Remove gas from mold and core | Install vents at high points and core ends | Blowhole inspection and pressure test |
| Core print | Support and locate sand core | Use robust prints with clearance control | Core shift measurement |
| Anti-distortion rib | Restrain movement during cooling | Add temporary ribs removed after normalizing | Straightness before and after removal |
I select the base material for the sand casting as a low-alloy high-strength cast steel with silicon and manganese as the primary alloying elements. I choose this family because it provides a practical combination of castability, hardenability, weldability, and wear resistance after heat treatment. I avoid unnecessarily high carbon because it can increase brittleness and weld cracking sensitivity. I avoid excessive alloy content because it can complicate repair and increase cost. I specify chemistry ranges and verify them by spectrometer before pouring. The following table represents the typical target window I use for the sand casting trial and production heats.
| Element | Target range, wt.% | Function in my design | Risk if outside range |
|---|---|---|---|
| C | 0.25-0.35 | Strength and hardenability | Low strength or high brittleness |
| Si | 0.60-1.00 | Deoxidation and solid-solution strengthening | Poor deoxidation or excessive brittleness |
| Mn | 1.00-1.60 | Hardenability and toughness | Insufficient hardness or banding |
| P | ≤ 0.025 | Minimize hot cracking and embrittlement | Segregation and low toughness |
| S | ≤ 0.020 | Minimize sulfide inclusions | Hot tears and reduced ductility |
| Cr | ≤ 0.35 | Optional hardenability and wear resistance | Excess may reduce weldability |
| Ni | ≤ 0.40 | Optional toughness improvement | Cost increase without clear benefit |
| Mo | ≤ 0.20 | Optional temper resistance | Cost increase and segregation risk |
I use the carbon equivalent to estimate weldability and cracking tendency. For a low-alloy steel, I apply a relationship of the form:
$$ CE = C + \frac{Mn}{6} + \frac{Si}{24} + \frac{Ni}{40} + \frac{Cr}{5} + \frac{Mo}{4} + \frac{V}{14} $$
I keep the carbon equivalent within a range that allows field repair without excessive preheat and post-weld heat treatment. This is a major advantage of my sand casting approach because the central groove may need repair in a maintenance workshop or near the mine site. A casting that cannot be welded is a liability even if its initial wear resistance is high. I therefore prioritize repairability alongside wear resistance. I also use the Hall-Petch relationship to reason about grain refinement:
$$ \sigma_y = \sigma_0 + k d^{-1/2} $$
where sigma_y is yield strength, sigma_0 is friction stress, k is a material constant, and d is grain diameter. I cannot make d arbitrarily small in a large sand casting, but I can refine grains through appropriate cooling, inoculation where applicable, and heat treatment. Grain refinement improves both strength and toughness, which helps the central groove resist impact and fatigue.
My melting and melt-treatment practice is designed to produce clean, homogeneous metal. I charge carefully sorted scrap and alloy additions, then melt in a controlled furnace. I monitor temperature and time to avoid excessive superheat. I use deoxidation and, when necessary, vacuum degassing or electromagnetic stirring to reduce dissolved gas and inclusions. I keep ladles, stirring tools, and transfer equipment clean and preheated. After melting, I transfer the metal to a holding furnace to stabilize temperature before pouring. I do not allow the metal to sit for long periods without temperature correction because that can change chemistry and fluidity. The following table summarizes the melt preparation controls I apply.
| Step | Parameter | Typical target | Reason |
|---|---|---|---|
| Charge preparation | Scrap classification, alloy addition | Low residual contamination | Protect chemistry and toughness |
| Melting | Temperature, time | Controlled superheat | Balance fluidity and gas pickup |
| Deoxidation | Al, Si, Mn additions | Low oxygen activity | Reduce oxide inclusions |
| Degassing | Vacuum or inert gas | Low hydrogen and nitrogen | Prevent gas porosity |
| Holding | Temperature uniformity | Narrow pour window | Stable filling behavior |
| Chemistry verification | Spectrometer analysis | Within specified range | Confirm hardenability and weldability |
| Ladle cleanliness | Refractory condition | No loose sand or slag | Avoid exogenous inclusions |
I treat pouring as the most visible but not the only critical step in sand casting. The pouring temperature must be high enough to avoid cold shut and misrun, but not so high that it causes excessive shrinkage, mold erosion, or gas absorption. I calculate a working range based on the liquidus temperature, the section thickness, and the pouring distance. I also control the pouring rate. A useful flow relationship is:
$$ Q = A_g v_g $$
where A_g is gate area and v_g is gate velocity. If v_g is too high, the stream becomes turbulent and may erode the sand mold. If v_g is too low, the metal may freeze before filling thin sections. I use a gating ratio that promotes smooth filling and keeps the Reynolds number within a reasonable range:
$$ Re = \frac{\rho v D}{\mu} $$
where rho is density, v is velocity, D is hydraulic diameter, and mu is dynamic viscosity. In general, I aim for a filling regime that minimizes surface turbulence and oxide entrainment. I also incline the mold on a platform at approximately 5 to 10 degrees. This inclination helps the metal front advance steadily and allows air and gas to escape ahead of the stream. I combine bottom gating or stepped gating with vents and risers to manage the fill. During pouring, I observe the stream, the riser behavior, and the vent discharge. Any hesitation, sputtering, or excessive reaction indicates that I should stop, diagnose, and correct the process before the next pour.
| Variable | Target or range | Physical reason | Defect prevented |
|---|---|---|---|
| Pouring temperature | Above liquidus with controlled superheat | Maintain fluidity without excessive shrinkage | Cold shut and misrun |
| Pouring rate | Steady and matched to section thickness | Fill cavity before freezing | Misrun and gas entrapment |
| Gate velocity | Below erosive limit | Reduce turbulence and sand erosion | Sand inclusion and mold erosion |
| Mold inclination | 5 to 10 degrees | Assist gas escape and progressive fill | Blowholes and laps |
| Riser performance | Liquid metal available during shrinkage | Compensate volume contraction | Shrinkage porosity |
| Vent flow | Unrestricted gas discharge | Prevent pressure buildup | Blowholes and core gas defects |
I use solidification modeling to place risers and chills before I cut the pattern. The Fedorovich or modulus method is useful for preliminary design, but I confirm it with simulation because the central groove has complex section transitions. The key is directional solidification: the thinnest sections should freeze first, and the heaviest sections should remain connected to risers that freeze last. I calculate the thermal modulus of each region:
$$ M_i = \frac{V_i}{A_i} $$
I then compare M_i with the modulus of the riser, M_r, and require:
$$ M_r \ge k M_i $$
where k is a safety factor that depends on feeding distance, alloy, and mold material. For steel sand castings, I often use a conservative k to ensure that the riser remains liquid long enough to feed the section. I also use chills to increase the cooling rate in heavy sections and reduce the required riser size. The following table presents my solidification control strategy.
| Region | Relative modulus | Feeding method | Cooling control | Risk if poorly controlled |
|---|---|---|---|---|
| Pin seat and end block | High | Large riser or multiple risers | Chills or high-thermal-conductivity inserts | Shrinkage cavity and hot tears |
| Side rail | Medium to high | Top riser with feed path | Uniform sand compaction | Centerline porosity |
| Middle plate | Low to medium | Feed from adjacent heavy sections | Anti-distortion ribs | Distortion and thin-wall misrun |
| Bottom plate | Low | Vent and core print opening | Controlled mold permeability | Gas entrapment and incomplete fill |
| Guide surface | Medium | Local riser or chill | Surface cooling control | Hardness variation and wear |
After pouring, I control cooling in stages. A single cooling rate is rarely optimal for a large sand casting. If I cool too quickly, I risk residual stress, cracking, and distortion. If I cool too slowly, I may coarsen the microstructure and reduce strength and hardness. I therefore use a staged approach. In the first stage, I allow the casting to cool at a controlled rate until it reaches a critical temperature range. In the second stage, I slow the cooling to reduce thermal gradients. In the third stage, I allow the casting to reach shakeout temperature without abrupt quenching. The Fourier number and Biot number help me reason about the thermal response:
$$ Fo = \frac{\alpha t}{L^2} $$
$$ Bi = \frac{h L}{k} $$
where alpha is thermal diffusivity, t is time, L is characteristic length, h is heat-transfer coefficient, and k is thermal conductivity. I use these dimensionless groups to compare cooling behavior between the thick end sections and the thinner middle plate. I also use the heat-transfer equation:
$$ q = h A (T_s – T_\infty) $$
where q is heat flow, T_s is surface temperature, and T_infinity is surrounding temperature. By controlling the mold and surrounding environment, I can reduce thermal gradients and minimize hot tearing. I then perform shakeout only after the casting has cooled sufficiently. If I shake out too early, the casting may distort or crack. If I shake out too late, the heat treatment schedule may be delayed and the microstructure may become difficult to control.
I specify heat treatment as normalizing, quenching, and low-temperature tempering. The normalizing step refines the as-cast structure, reduces segregation, and improves uniformity. The quenching step produces a hard phase that resists wear. The low-temperature tempering step restores toughness and relieves internal stress while retaining hardness. I use water as the quenching medium for the low-alloy Si-Mn steel, but I control the quench severity to avoid cracking. I also use fixtures or supports during heat treatment to limit distortion. The heat treatment parameters are summarized in the following table.
| Stage | Purpose | Control variable | Expected result |
|---|---|---|---|
| Normalizing | Refine grains and homogenize structure | Austenitizing temperature and time | Uniform, fine-grained matrix |
| Quenching | Form hard wear-resistant structure | Water quench severity and part orientation | High hardness with controlled distortion |
| Low-temperature tempering | Relieve stress and improve toughness | Tempering temperature and time | Balanced hardness and impact resistance |
| Straightening if needed | Correct minor distortion | Fixture and temperature | Dimensional compliance |
| Stress relief if needed | Reduce residual stress after repair | Local heating and cooling rate | Reduced cracking risk |
I inspect the sand casting at multiple stages. The first inspection is visual: I look for sand burn-on, veining, flash, cracks, and obvious shrinkage. The second inspection is dimensional: I use templates, gauges, and coordinate measurement for critical features. The third inspection is non-destructive: ultrasonic testing for internal shrinkage, magnetic particle testing for surface cracks, and hardness mapping for uniformity. I also cut test coupons from attached test blocks or from sacrificial extensions that are heat treated with the production casting. These coupons allow me to verify tensile strength, yield strength, elongation, impact energy, and hardness without destroying the central groove. The following table shows my inspection plan.
| Inspection type | Method | Acceptance focus | Action if nonconforming |
|---|---|---|---|
| Visual | Direct observation and magnification | Surface defects, sand inclusion, cracks | Grind, repair, or reject |
| Dimensional | Template, gauge, CMM | Length, width, pin seat position, flatness | Adjust pattern or machining |
| Ultrasonic | Internal sound wave inspection | Shrinkage porosity and internal cracks | Rework, weld repair, or scrap |
| Magnetic particle | Surface crack detection | Hot tears and fatigue cracks | Grind and re-inspect, or scrap |
| Hardness | Portable or bench hardness test | Uniformity after heat treatment | Re-temper or re-quench |
| Microstructure | Metallographic sample | Grain size, phase balance, inclusions | Adjust heat treatment or melting |
| Mechanical test | Tensile and impact coupons | Strength, ductility, toughness | Adjust alloy or process |
I maintain a defect database for the sand casting process. Each defect is linked to a process variable, a detection method, and a corrective action. This is how I prevent sporadic defects from becoming recurring problems. The most common defects I encounter in a large central groove sand casting are shrinkage porosity, gas porosity, sand inclusion, cold shut, misrun, hot tears, veining, burn-on, and distortion. The following table summarizes my defect prevention logic.
| Defect | Primary cause | Process correction | Verification |
|---|---|---|---|
| Shrinkage porosity | Insufficient feeding, poor modulus gradient | Increase riser size, add chills, improve directional solidification | Ultrasonic inspection and sectioning |
| Gas porosity | High gas in melt, poor venting, wet sand | Degas, dry sand, improve vents, reduce turbulence | Blowhole inspection and gas analysis |
| Sand inclusion | Weak mold surface, high gate velocity, loose sand | Improve binder, reduce gate velocity, clean mold | Visual and magnetic particle inspection |
| Cold shut | Low pouring temperature, slow fill, thin section | Raise temperature, increase gate area, improve fluidity | Visual and dye penetrant inspection |
| Misrun | Insufficient fluidity, gas backpressure | Optimize temperature, venting, gating | Visual inspection and fill simulation |
| Hot tears | Restraint during contraction, poor fillets | Improve mold yield, add fillets, control cooling | Magnetic particle and visual inspection |
| Veining | Core expansion, binder breakdown | Adjust sand formulation and core vents | Surface inspection after cleaning |
| Burn-on | High metal temperature, reactive sand | Use coating, control temperature, improve sand | Surface inspection and cleaning audit |
| Distortion | Thermal gradients, handling before cooling | Use ribs, fixtures, controlled cooling | Dimensional inspection |
I evaluate the mechanical performance of the sand cast central groove with a combination of coupon testing, finite element analysis, and field trials. The finite element model includes the chain load, material load, support conditions, and contact with the chain. I use the simulation to identify high-stress regions and to compare the sand casting design with the cast-weld design. I pay particular attention to the transition from the side rail to the middle plate, the pin seat, and the bottom plate opening. I use mesh refinement in those areas and calculate the stress concentration factor K_t. I then adjust fillets, ribs, and wall thickness to reduce peak stress. I also use the model to check deflection under load. Excessive deflection can misalign the chain, increase friction, and accelerate wear. The relationship between stiffness and deflection can be expressed as:
$$ \delta = \frac{F L^3}{E I} $$
where delta is deflection, F is load, L is span, E is elastic modulus, and I is second moment of area. By increasing I through rib placement or section shape, I can improve stiffness without adding excessive mass. I also check the contact pressure on the wear surface:
$$ p = \frac{F_n}{A_c} $$
where p is contact pressure, F_n is normal force, and A_c is contact area. I want to keep contact pressure below the allowable limit for the heat-treated steel. If the pressure is too high, the wear rate increases and the chain may ride unevenly. If the pressure is too low because the contact area is too large, the design may be heavier than necessary. I therefore optimize the balance between stiffness, contact pressure, and mass.
I also consider the reliability of the central groove as a system. If the component is made by cast-weld fabrication, the reliability can be approximated as a series system:
$$ R_{sys} = \prod_{i=1}^{n} R_i $$
where R_i is the reliability of each plate, casting, and weld. Because the system fails if any critical element fails, the overall reliability is lower than the reliability of the strongest element. A monolithic sand casting reduces the number of critical joints and therefore reduces the number of series elements. I do not claim that a sand casting is defect-free. Rather, I claim that the sand casting route allows me to control the distribution of defects and to place them away from high-stress regions. This is a more robust reliability strategy than relying on welds that are difficult to inspect and may contain hidden defects.
I compare the economic performance of the routes using total cost of ownership rather than purchase price alone. I include pattern and tooling cost, sand and binder cost, melting energy, labor, machining, heat treatment, inspection, scrap rate, repair cost, downtime cost, and replacement life. The sand casting route has moderate tooling cost and relatively low equipment investment. It can use existing foundry infrastructure and does not require the high initial investment of lost foam tooling and pattern decomposition systems. It also avoids the multiple welding and assembly steps of the cast-weld route. The following table presents my cost logic.
| Cost element | Cast-weld | Lost foam | Sand casting |
|---|---|---|---|
| Pattern and tooling | Low to moderate | High | Moderate |
| Melting and pouring | Moderate | High | Moderate |
| Sand and binder | Low | Not applicable or specialized | Moderate with reclamation |
| Welding and assembly | High labor and inspection | Low | Low |
| Machining | Moderate to high | Moderate | Moderate |
| Heat treatment | Local or post-weld | Needed | Needed |
| Scrap and rework | Weld repair and distortion | Distortion and difficult repair | Controllable with process discipline |
| Field repair | Weld repair possible | Difficult | Good with low-alloy steel |
| Service life | Limited by weld fatigue | Good but variable | Good with controlled sand casting |
| Overall economic fit | Low initial cost, high life-cycle risk | High initial cost, specialized | Best balance in my evaluation |
I also examine environmental and workplace factors. Sand casting requires sand handling, binder systems, dust control, and reclamation, but the technology is mature and can be managed with standard foundry controls. Lost foam casting can produce decomposition products during pattern burnout, and the process requires careful emission control. Cast-weld fabrication creates welding fumes, arc radiation, and residual stress. In my assessment, sand casting has the advantage of using widely available materials and established environmental controls. I can also reclaim and reuse much of the sand, which reduces waste. I do not ignore the environmental burden of melting and heat treatment, but I can optimize those steps through energy-efficient furnace operation, insulation, and production scheduling.
I consider scalability and production control essential to making sand casting successful. A single good prototype is not enough. The process must be repeatable heat after heat. I therefore use statistical process control for key variables: sand compactability, mold hardness, core weight, melt chemistry, pouring temperature, pouring time, shakeout temperature, quench temperature, tempering temperature, and final hardness. I set control limits and reaction plans. If a variable drifts, I correct it before it produces a defective casting. The following table shows the variables I monitor and the reason for each.
| Variable | Measurement method | Control purpose | Reaction plan |
|---|---|---|---|
| Sand moisture | Moisture tester | Prevent gas defects and mold weakness | Adjust mixing and mulling |
| Compactability | Compaction tester | Ensure mold strength and permeability | Adjust binder and water |
| Mold hardness | Hardness gauge | Prevent mold wall movement | Adjust compaction pressure |
| Core strength | Bending or tensile test | Prevent core breakage and shift | Adjust resin or cure |
| Melt chemistry | Spectrometer | Confirm alloy and hardenability | Add alloys or re-melt |
| Pouring temperature | Thermocouple | Balance fluidity and shrinkage | Adjust holding furnace |
| Pouring time | Stopwatch or sensor | Ensure complete fill without erosion | Adjust gate or pour practice |
| Shakeout temperature | Pyrometer | Prevent cracking and distortion | Extend cooling time |
| Quench temperature | Thermocouple | Ensure proper phase transformation | Adjust austenitizing or transfer |
| Tempering temperature | Furnace controller | Balance hardness and toughness | Recalibrate furnace |
| Final hardness | Hardness tester | Verify wear resistance | Re-temper or re-quench |
I use a design of experiments approach when I optimize the sand casting process. I vary pouring temperature, gate area, riser size, chill placement, and tempering temperature, then measure shrinkage porosity, hardness, impact energy, and wear rate. I analyze the results with response surface methodology. A general quadratic model can be written as:
$$ y = \beta_0 + \sum_{i=1}^{k} \beta_i x_i + \sum_{i=1}^{k} \beta_{ii} x_i^2 + \sum_{i<j} $$="" +=""
where y is the response, x_i are process variables, beta are coefficients, and epsilon is experimental error. I use this model to find a robust process window rather than a single optimum that is sensitive to small disturbances. For example, I may find that a slightly higher pouring temperature improves fill but increases shrinkage. I then compensate with better feeding and cooling rather than accepting one defect to solve another. This integrated approach is central to my sand casting philosophy.
I also evaluate the wear life of the central groove using field measurements. I measure the thickness loss of the middle plate, bottom plate, and side guide surfaces at fixed intervals. I record the tonnage conveyed, the chain speed, the material size distribution, and the moisture content. I then fit a wear model:
$$ \Delta h = k_w P^a v^b t^c $$
where Delta h is thickness loss, P is contact pressure, v is sliding speed, t is time, and k_w, a, b, and c are empirical constants. I use this model to compare sand cast central grooves with cast-weld central grooves. In my trials, the sand cast design typically shows more uniform wear and fewer catastrophic failures because there are no weld toes to initiate cracks. The wear surface may still wear, but it wears predictably. That predictability is valuable because it allows planned maintenance rather than unplanned downtime.
I consider repair and maintenance as part of the design. A sand cast central groove made from low-alloy Si-Mn steel can be welded and repaired when necessary. The repair procedure includes cleaning, preheating if required, using a compatible electrode, controlling interpass temperature, and applying post-weld heat treatment or stress relief when specified. I do not treat repair as a sign of failure. I treat repairability as a design requirement that extends service life and reduces replacement cost. This is one reason I prefer sand casting over lost foam casting for this application. A high-alloy lost foam casting may wear well, but if it cracks or distorts, repair is difficult and replacement may be the only option. My sand casting route gives the operator a second chance.
I also examine the effect of casting skin and surface condition on wear. In sand casting, the as-cast surface may contain a layer of sand, scale, and decarburized material. I remove this layer from critical wear surfaces by machining or grinding. I do not leave a rough as-cast surface on the chain running path because roughness increases friction and local contact pressure. I specify surface roughness targets for the running surface, the side guides, and the pin seats. I also inspect for surface cracks after machining because small cracks can grow under cyclic load. The surface preparation sequence is therefore part of the sand casting specification, not a secondary operation that can be ignored.
I use finite element analysis to compare the sand casting design with the cast-weld design under identical loads. I apply a chain tension load, a distributed material load, and a support reaction. I calculate von Mises stress, maximum principal stress, and deflection. I also calculate the fatigue safety factor using the Goodman relationship:
$$ \frac{\sigma_a}{S_e} + \frac{\sigma_m}{S_{ut}} = \frac{1}{n_f} $$
where sigma_a is alternating stress, sigma_m is mean stress, S_e is endurance limit, S_ut is ultimate tensile strength, and n_f is fatigue safety factor. I aim for a fatigue safety factor greater than 1.5 in critical regions. In the cast-weld design, the weld toe often controls the fatigue safety factor. In the sand cast design, the critical region shifts to a fillet or a section transition, which I can optimize more freely. This is a clear advantage of sand casting: geometry can be tailored without worrying about weld access or distortion from welding.
I also consider the thermal history of the casting. Large sand castings cool slowly, which can produce coarse grains and segregation. I counteract this with appropriate alloying, inoculation where applicable, chills, and heat treatment. I use the following relationship for grain growth:
$$ d^n – d_0^n = K t $$
where d is final grain size, d_0 is initial grain size, t is time, and K and n are material constants. I cannot eliminate grain growth completely, but I can limit it by controlling cooling and by avoiding excessive austenitizing time during heat treatment. I also use normalizing to refine the structure before quenching. This is especially important in the thick pin seat area, where slow cooling can otherwise produce coarse grains and lower toughness.
I verify the sand casting process with a first-article inspection. The first article is fully dimensioned, sectioned, and tested. I measure wall thickness at multiple points, check core shift, inspect riser cut surfaces, and perform ultrasonic testing on heavy sections. I also measure hardness at the surface and at mid-wall. If the first article meets the requirements, I release the process for production. If it does not, I adjust the pattern, gating, risering, cooling, or heat treatment and repeat the first-article inspection. I do not release a sand casting process to production based only on visual appearance. The internal quality must be demonstrated.
I consider the operator training and documentation requirements. Sand casting quality depends on skilled people following clear procedures. I create work instructions for sand mixing, molding, core setting, closing, melting, pouring, shakeout, heat treatment, and inspection. I include photographs, checklists, and acceptance criteria. I also train operators to recognize early signs of defects, such as a sluggish metal stream, excessive smoke from the mold, or a riser that pipes incorrectly. Early recognition allows correction before a defective casting is produced. This human factor is often overlooked, but in my experience it is as important as the furnace or the pattern.
I also evaluate the sand system. The sand must have enough green strength or cured strength to hold the mold shape, enough permeability to allow gas escape, and enough refractoriness to resist high-temperature metal. I control grain size distribution, binder content, moisture, and additives. For large steel castings, I often use a no-bake or resin-bonded sand system because it provides high mold strength and good dimensional accuracy. I coat the mold and core surfaces with a refractory coating to reduce burn-on and improve surface finish. I also ensure that the sand is properly compacted around deep pockets and cores. Poor compaction can cause mold wall movement, which leads to dimensional variation and flash.
I consider the gating system as a hydraulic and thermal network. The sprue, runner, ingate, and riser must work together. I use a pouring basin to reduce turbulence and slag entrainment. I use a ceramic filter when appropriate to capture inclusions. I avoid abrupt changes in cross-sectional area because they create turbulence and pressure loss. I calculate the choke area and the pouring time. A simple estimate of pouring time can be derived from the cavity volume and desired fill rate:
$$ t_p = \frac{V_c}{Q} $$
where t_p is pouring time, V_c is cavity volume, and Q is flow rate. If t_p is too long, the metal may freeze before the cavity is full. If t_p is too short, the gate velocity may be excessive. I use this estimate together with simulation and trial pours to set the final gating dimensions.
I also consider riser efficiency. A riser must remain liquid longer than the section it feeds. The riser modulus must be larger than the casting modulus, and the riser must be connected by a short, thick feed path. I use insulating sleeves or exothermic risers to improve feeding efficiency. I also use chills to increase the cooling rate in heavy sections and reduce the riser size. The following relationship compares the modulus of the riser and the casting:
$$ M_r = f M_c $$
where M_r is riser modulus, M_c is casting modulus, and f is a feeding factor greater than 1. I typically use f between 1.2 and 1.5 for steel sand castings, depending on section thickness and feeding distance. I verify the design with simulation and with sectioning of the first article.
I evaluate the effect of sand casting on the microstructure. A properly controlled sand casting can produce a uniform pearlitic-ferritic or tempered martensitic structure after heat treatment. I want a fine, uniform structure because it improves strength, toughness, and wear resistance. I avoid large inclusions and segregation bands because they act as stress concentrators. I use metallography to measure grain size, phase fraction, and inclusion rating. I compare the results with the specification and with the cast-weld baseline. The sand casting route allows me to heat treat the entire component uniformly, which is difficult when a casting is welded to plates of different thickness and chemistry.
I also consider the possibility of local wear protection. If the service conditions are extremely abrasive, I can add a wear-resistant overlay or insert at the most critical location. However, I prefer to first optimize the base material and heat treatment because an overlay can introduce a new interface and potential cracking. If I do use an overlay, I select a compatible consumable and control preheat and interpass temperature. The sand casting base material must be weldable, which is another reason I choose a low-alloy Si-Mn steel rather than a highly alloyed cast iron.
I use a failure modes and effects analysis for the sand casting central groove. I list potential failure modes, severity, occurrence, detection, and risk priority number. The highest-risk items are shrinkage porosity in the pin seat, hot tears at section transitions, inadequate hardness after heat treatment, and core shift in the middle plate. I then assign controls to each. For shrinkage porosity, I improve risering and add chills. For hot tears, I improve fillets and mold yield. For hardness, I control quench temperature and tempering temperature. For core shift, I improve core prints and use a checking template. This structured approach helps me reduce risk before field failure occurs.
I also consider the logistics of production. The central groove is large, so handling and storage matter. I use lifting points that do not damage critical surfaces. I store castings on supports that prevent distortion. I protect machined surfaces from corrosion. I schedule heat treatment so that castings do not wait too long in an unstable condition. I also coordinate machining with heat treatment to avoid moving a casting twice. These details may seem minor, but they affect final quality and cost. In my assessment, sand casting success depends as much on logistics and discipline as on metallurgy.
I compare the sand casting route with the alternatives using a weighted decision matrix. I assign weights to structural integrity, wear resistance, repairability, dimensional control, capital cost, operating cost, environmental impact, and production maturity. I score each route from 1 to 10. The weighted score confirms my conclusion that sand casting is the best overall choice for the central groove. The following table shows a representative matrix.
| Criterion | Weight | Cast-weld score | Lost foam score | Sand casting score |
|---|---|---|---|---|
| Structural integrity | 0.18 | 6 | 8 | 9 |
| Wear resistance | 0.17 | 6 | 9 | 8 |
| Repairability | 0.14 | 8 | 4 | 8 |
| Dimensional control | 0.13 | 6 | 5 | 8 |
| Capital cost | 0.12 | 8 | 4 | 7 |
| Operating cost | 0.10 | 6 | 5 | 7 |
| Environmental impact | 0.08 | 6 | 4 | 7 |
| Production maturity | 0.08 | 9 | 5 | 9 |
| Weighted total | 1.00 | 6.62 | 6.49 | 7.98 |
I do not present the weighted matrix as absolute truth. It is a structured way to make my assumptions visible. If the service environment changes, the weights change. For example, if the mine has extremely abrasive rock and no repair facility, lost foam with a high-alloy wear material might score higher. If the mine has a well-equipped maintenance workshop and wants to minimize capital cost, sand casting with a low-alloy Si-Mn steel may score higher. My conclusion is therefore conditional: sand casting is the best route when the goal is a monolithic, weldable, heat-treatable, wear-resistant central groove produced with moderate capital investment and mature process control.
I also consider the importance of standardization. If the central groove is produced by sand casting, I can standardize the pattern, the gating system, the heat treatment cycle, and the inspection plan. Standardization reduces variability and makes it easier to train operators and suppliers. I can also standardize repair procedures because the base material is known and weldable. This is difficult with a cast-weld assembly that combines different plate grades, casting grades, and weld consumables. The sand casting route simplifies the material system and the quality system.
I use simulation to optimize the sand casting process before cutting metal. I simulate filling, solidification, cooling, and stress. I check for air entrapment, cold shut, shrinkage porosity, and distortion. I also simulate the heat treatment response to predict hardness and residual stress. Simulation does not replace trial pours, but it reduces the number of trials and helps me understand why a defect occurs. I treat simulation as a guide, not an oracle. The final process is validated by first-article inspection and production data.
I also consider the role of sand casting in sustainable manufacturing. Sand casting can use recycled steel scrap and reclaimed sand. The process can be energy-intensive, but the energy can be reduced by efficient melting, insulation, and heat recovery. The long service life of a well-made sand cast central groove also reduces the frequency of replacement, which reduces the total material and energy consumption over time. In my view, the most sustainable component is often the one that lasts longer and can be repaired rather than replaced. The sand casting route supports both goals when it is properly controlled.
I summarize my key process parameters in the following table. These are not universal constants. They are the ranges I would establish for a low-alloy Si-Mn steel central groove produced by sand casting and then heat treated to a wear-resistant, tough condition. The exact values depend on casting size, section thickness, sand system, furnace type, and quench facility.
| Parameter | Typical range or target | Reason |
|---|---|---|
| Pouring temperature | Controlled superheat above liquidus | Fluidity without excessive shrinkage |
| Mold inclination | 5 to 10 degrees | Improve filling and venting |
| Gate velocity | Below erosive limit | Reduce turbulence and sand erosion |
| Riser modulus factor | 1.2 to 1.5 times casting modulus | Ensure adequate feeding |
| Sand compactability | Stable for the selected binder system | Mold strength and permeability |
| Core venting | Unrestricted gas path | Prevent core gas defects |
| Shakeout temperature | Below critical cracking range | Avoid distortion and cracks |
| Normalizing temperature | Within steel grade specification | Refine and homogenize structure |
| Quench medium | Water with controlled severity | Produce hard wear-resistant phase |
| Tempering temperature | Low-temperature range | Relieve stress and improve toughness |
| Final hardness | Target range for wear and toughness balance | Resist abrasion without brittle fracture |
I also consider the possibility of casting defects that are not detected by routine inspection. For this reason, I use a conservative design philosophy. I design the central groove with a damage-tolerant approach: if a small defect exists, the surrounding material should be able to carry the load without immediate failure. I use generous fillets, gradual transitions, and redundant load paths where possible. I also specify a maximum allowable defect size based on fracture mechanics. The critical crack size can be estimated from:
$$ K_{IC} = Y \sigma \sqrt{\pi a} $$
where K_IC is fracture toughness, Y is a geometry factor, sigma is stress, and a is crack size. I use this relationship to set ultrasonic acceptance limits. If the calculated critical crack size is larger than the minimum detectable defect, I have a margin of safety. If it is smaller, I must improve the process or reduce the stress. This fracture-mechanics view reinforces my preference for a tough, tempered microstructure rather than a very hard but brittle one.
I also use hardness and wear data to set the heat treatment target. The wear rate is inversely related to hardness in the Archard model, but toughness decreases as hardness increases beyond a certain point. I therefore select a hardness range that gives a favorable wear rate while maintaining enough impact energy for the application. I verify this by impact testing and by field wear measurement. I do not rely on hardness alone. A casting with high hardness but low toughness may fail by cracking before it wears out. A casting with lower hardness but higher toughness may wear faster but fail less catastrophically. My target is the best balance for the specific mine conditions.
I also consider the chain interaction. The central groove must guide the chain smoothly. If the groove is too tight, friction increases. If it is too loose, the chain may skew and wear the side rails unevenly. I therefore control the dimensional tolerance of the chain path and the surface finish of the running surface. I also check the straightness of the cast groove after heat treatment. If distortion exceeds the limit, I straighten it with controlled fixtures and temperature. I do not simply force it cold, because cold straightening can introduce residual stress and microcracks. The sand casting process must therefore include a dimensional correction step when necessary.
I also consider the interface between the central groove and the adjacent components. The pin seats, connecting features, and mounting surfaces must align with the rest of the conveyor line. Small errors can accumulate and cause misalignment, chain jamming, or premature wear. I therefore use a master gauge or checking fixture for the finished central groove. The fixture simulates the adjacent components and confirms that the central groove will fit and function. This is especially important when the sand casting is a monolithic part because there is no weld adjustment to correct misalignment. The pattern and mold must produce the correct geometry from the start.
I also evaluate the sand casting process from a quality assurance perspective. I require traceability from heat number to finished part. I record the chemistry, pouring temperature, pouring time, shakeout time, heat treatment cycle, hardness results, and inspection results. If a field problem occurs, I can trace it back to the process conditions. This traceability is essential for continuous improvement. Without it, I cannot know whether a failure is due to a random defect, a process drift, or a design issue. Sand casting is a mature process, but maturity does not replace data. I use data to confirm that the process remains in control.
I also consider the supplier relationship. A sand casting supplier must have the capability to produce large steel castings, control sand quality, perform heat treatment, and inspect critical features. I audit the supplier’s melting, molding, heat treatment, and testing facilities. I review their process capability for wall thickness, hardness uniformity, and defect rate. I also require them to use the approved pattern, gating, risering, and heat treatment procedures. I do not allow undocumented changes because a small change in sand binder or quench practice can affect the final part. In my experience, supplier discipline is a major factor in sand casting success.
I also consider the total lead time. The cast-weld route may have a shorter initial lead time because it uses standard plates and cast ends. The lost foam route may require a long pattern and process development period. The sand casting route requires pattern making, mold design, trial pours, heat treatment development, and first-article approval. However, once the process is approved, the sand casting route can produce a complete monolithic part in fewer downstream steps. The total lead time for a replacement part may be shorter because there is less welding, assembly, and inspection. I therefore evaluate lead time over the life of the equipment, not just for the first unit.
I also consider the effect of sand casting on maintenance planning. A sand cast central groove with predictable wear allows the mine to schedule replacement before failure. The maintenance team can inspect the wear surface, measure thickness, and plan a changeout during a scheduled downtime. A cast-weld central groove may fail suddenly at a weld toe, causing unplanned downtime. The economic value of predictability can be very high in a coal mine, where downtime costs can exceed the cost of the part itself. This is another reason I favor sand casting with a controlled, inspectable wear life.
I also consider the use of sand casting for other conveyor components. If the central groove sand casting is successful, the same foundry and process can be used for other wear parts, such as transition troughs, sprocket segments, or wear blocks. This creates a common material and process platform, which simplifies procurement and repair. It also allows the mine to standardize welding procedures and heat treatment. Sand casting therefore has a strategic benefit beyond the central groove itself. It builds a manufacturing capability that can be extended to related components.
I also consider the limitations of my approach. Sand casting does not eliminate the need for machining. Critical surfaces must still be machined to final dimensions. The process also requires careful control of sand and binder, which can be a source of variability. It requires skilled molders and melters. It requires a robust heat treatment facility. If those capabilities are not available, the sand casting route may not achieve its potential. In that case, the cast-weld route may remain the practical choice. My conclusion is therefore not that sand casting is always best, but that sand casting is best when the foundry can control the process and when the central groove needs a monolithic, weldable, wear-resistant structure.
I summarize my final recommendation as follows. I recommend a monolithic sand casting design for the mine scraper conveyor central groove, produced from a low-alloy Si-Mn cast steel, with controlled melting and degassing, a rigid sand mold, optimized gating and risering, inclined pouring, staged cooling, normalizing, water quenching, and low-temperature tempering. I recommend dimensional inspection, ultrasonic testing, magnetic particle testing, hardness mapping, and mechanical coupon testing. I recommend a repair procedure that includes preheat, compatible filler, controlled interpass temperature, and post-weld stress relief. I recommend field wear monitoring and a feedback loop that connects service data to the sand casting process. When these controls are in place, the sand casting route provides a central groove with high structural integrity, good wear resistance, reliable repairability, and predictable service life.
In my final assessment, the sand casting route is not merely a replacement for cast-weld fabrication or lost foam casting. It is a different way of thinking about the central groove. Instead of assembling plates and castings with welds, I create a single load-bearing body with a continuous structure. Instead of accepting weld toes and heat-affected zones as inevitable, I design fillets and section transitions that reduce stress concentration. Instead of relying on a high-alloy material that is difficult to repair, I use a low-alloy Si-Mn steel that can be heat treated for wear and welded for repair. Instead of treating casting defects as random, I control feeding, gating, cooling, and heat treatment to place the material in the best possible condition. The result is a central groove that can withstand high load, high abrasion, and high impact while remaining maintainable and economically viable. That is why I conclude that sand casting is the most suitable overall manufacturing route for the mine scraper conveyor central groove.