
In my work with lost foam casting for thin-walled shell, housing, and frame components, I have repeatedly observed that the process can deliver accurate dimensions, good repeatability, flexible production, low labor intensity, and low pollution when the pattern cluster, coating, sand filling, vacuum, and pouring system are correctly matched. My focus has been on the defects that most often interrupt stable production in lost foam casting: burning-on, porosity, and sand wash. These defects are not isolated events. They are the result of coupled transport phenomena involving polymer decomposition, gas removal, metal flow, coating permeability, sand compaction, and gate pressure. I studied flywheel housings, connecting-rod rests, and similar castings to identify the mechanisms and to define practical process corrections. The main measures I applied were adjustment of pattern assembly, optimization of the pouring system, placement of exhaust and slag-discharge risers, and rationalization of the inner gate inlet layout. Through small-batch and then large-batch trials, I confirmed that these measures can reduce or eliminate the defects in lost foam casting.
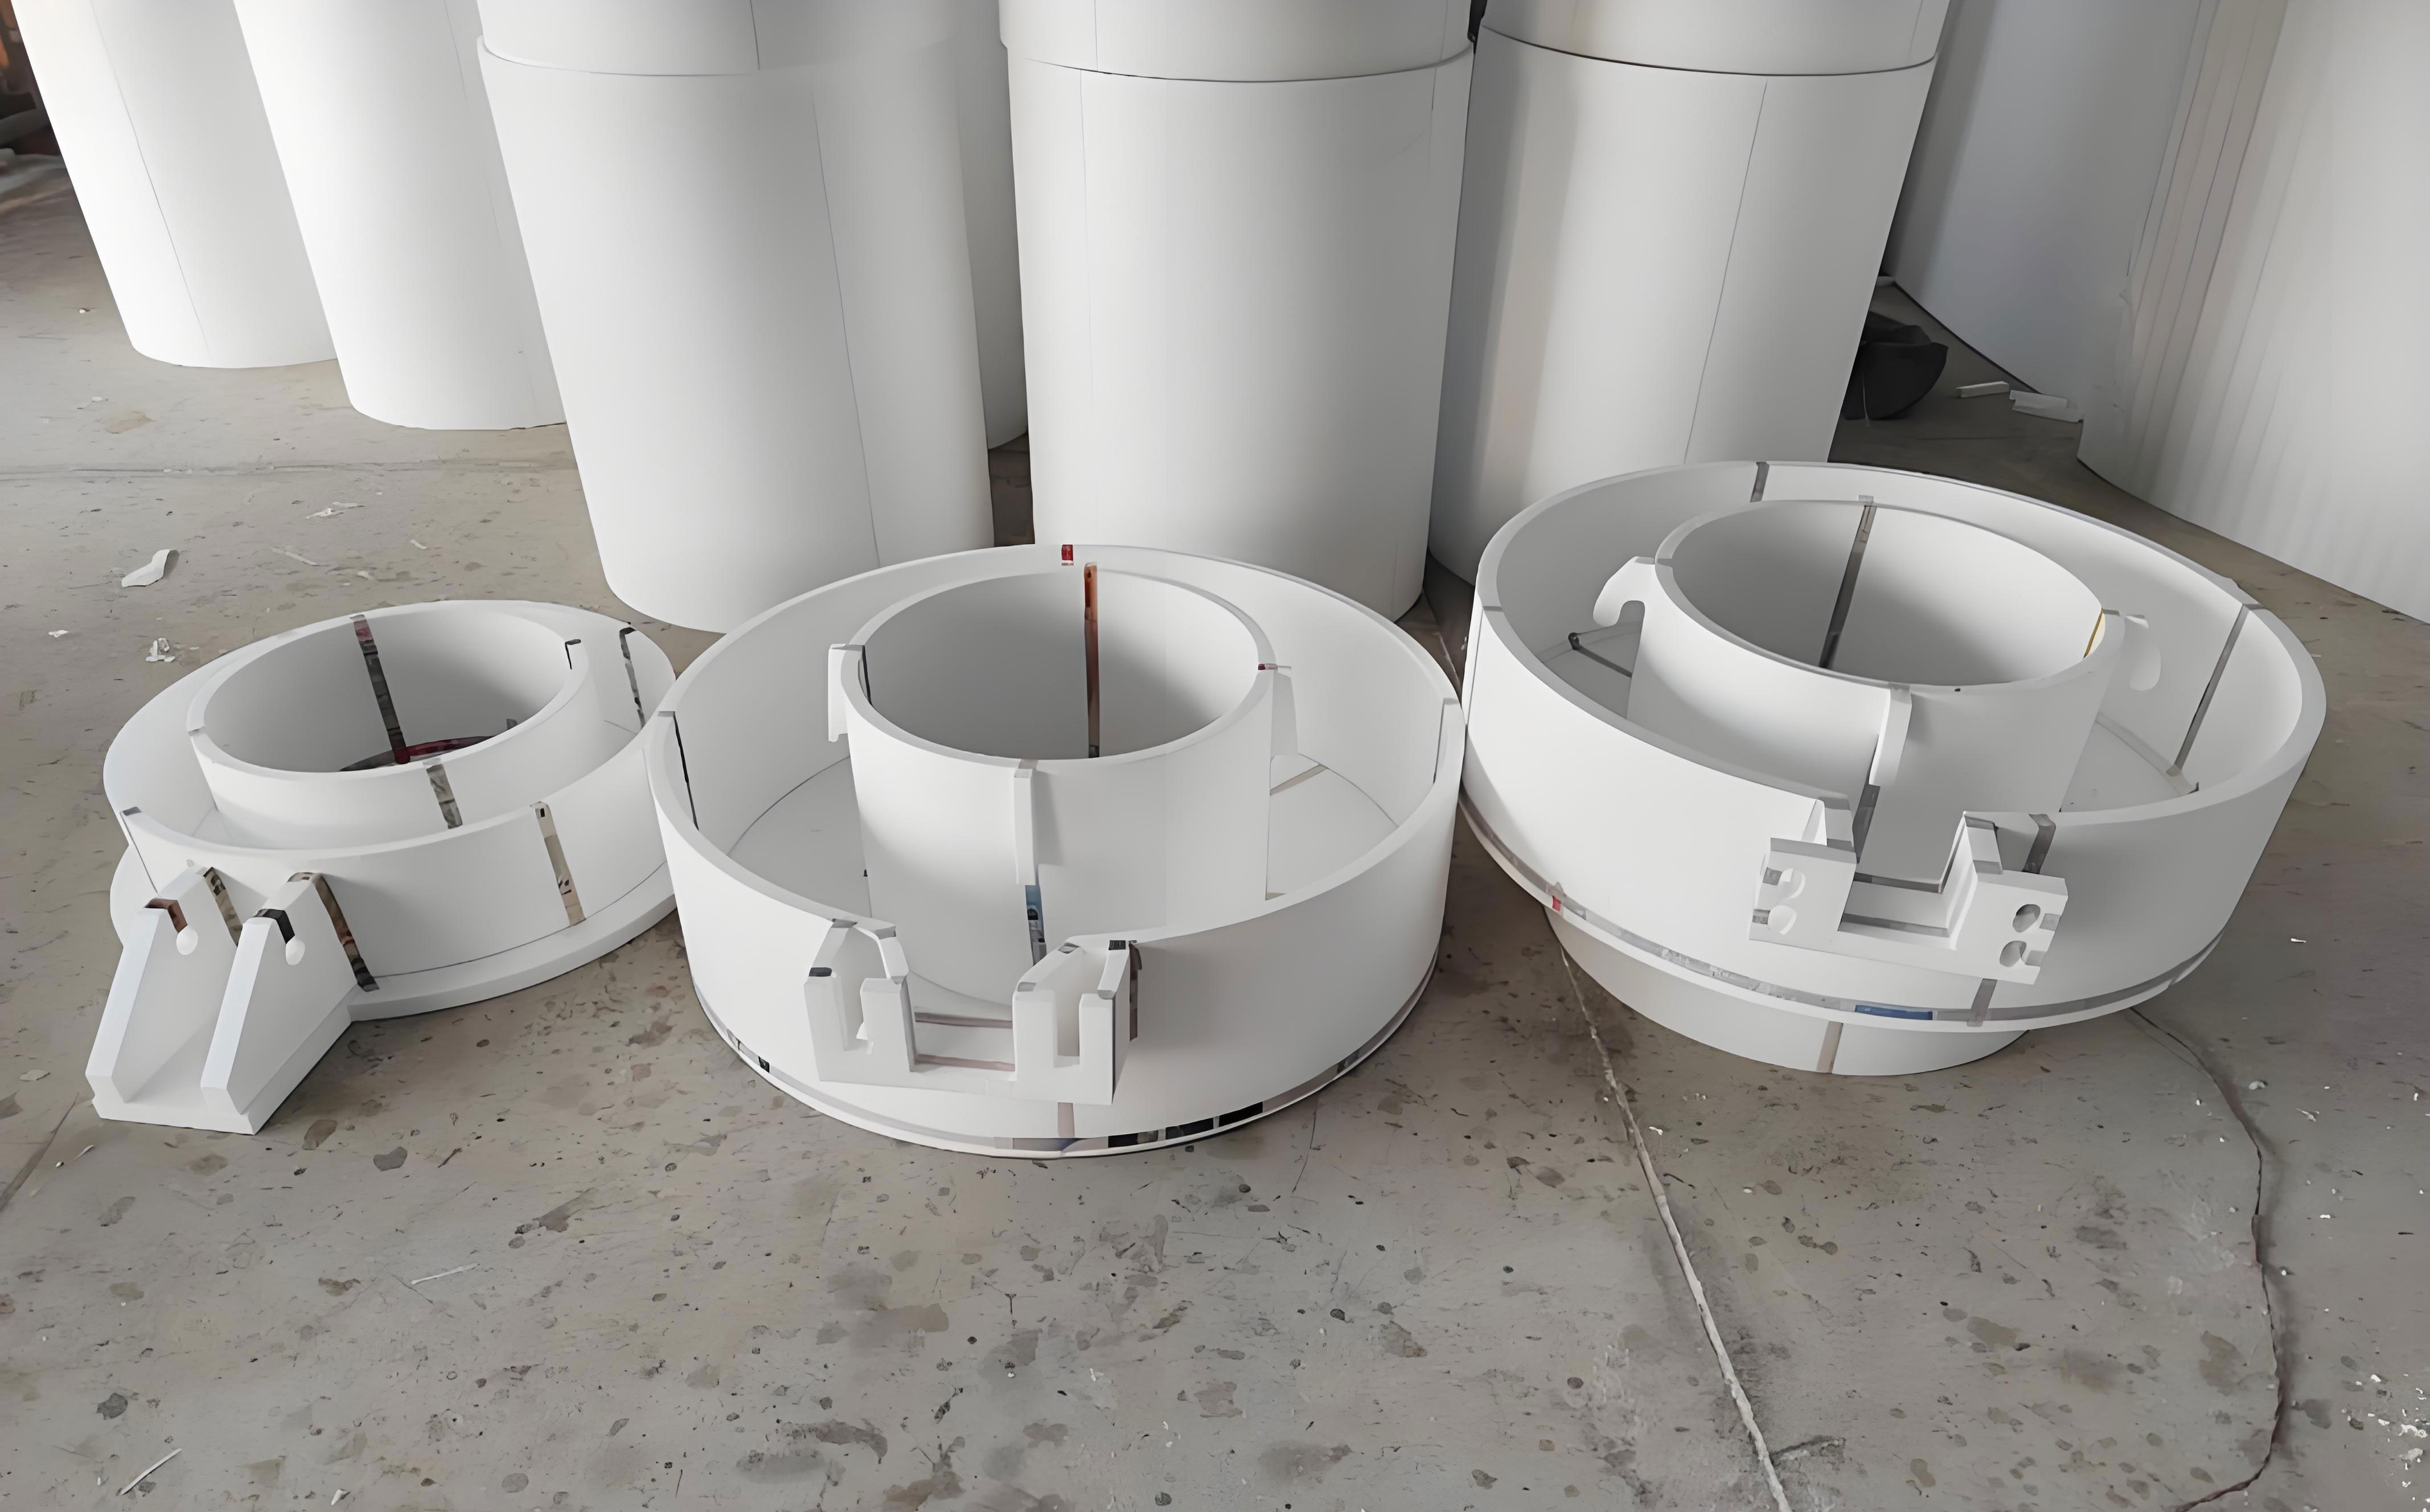
The basic principle of lost foam casting is that a polymer pattern is vaporized and decomposed by the entering molten metal. The decomposition products must escape through the coating, through the dry sand, and through the vacuum system. If gas generation exceeds gas removal, the residual gas and liquid decomposition products become trapped at the metal front or at the casting surface. I express the simplified pressure balance for lost foam casting as follows:
$$ P_{\text{decomp}} + P_{\text{entrained}} = P_{\text{vacuum}} + P_{\text{coating}} + P_{\text{sand}} + P_{\text{escape}} + \Delta P_{\text{residual}} $$
In this expression, \(P_{\text{decomp}}\) is the gas pressure generated by pattern decomposition, \(P_{\text{entrained}}\) is the pressure contribution from air or vapor carried into the mold, \(P_{\text{vacuum}}\) is the negative pressure applied to the sand box, \(P_{\text{coating}}\) is the pressure drop through the coating, \(P_{\text{sand}}\) is the resistance of the compacted sand, \(P_{\text{escape}}\) is the pressure associated with gas escape through vents and permeable paths, and \(\Delta P_{\text{residual}}\) is the residual pressure that can become trapped in the casting. When \(\Delta P_{\text{residual}}\) becomes positive and localized, defects such as porosity, burning-on, and sand wash are more likely to appear. This balance helps me explain why lost foam casting is sensitive to both local geometry and global process settings.
I have found it useful to classify the three main defects by their dominant mechanism, the process variables that control them, and the corrective actions that are most effective in lost foam casting. The matrix below summarizes my experience.
| Defect | Dominant mechanism in lost foam casting | Key process variables | Effective corrective action |
|---|---|---|---|
| Burning-on | Loose or insufficiently compacted sand at local geometry; metal penetrates the sand surface and forms a mechanical mixture | Pattern orientation, gap between patterns, sand fillability, vibration time, coating thickness, pouring temperature | Reorient pattern to improve sand filling; increase pattern spacing; improve compaction; optimize coating |
| Porosity | Incomplete decomposition and removal of pattern gas and residues; gas trapped near the surface or in the last-filled region | Pouring temperature, coating permeability, vacuum level, venting, gate position, metal flow rate | Increase local venting; optimize vacuum; reduce local coating thickness; raise pouring temperature when needed |
| Sand wash | Coating rupture or sand erosion caused by high local metal velocity or pressure; sand enters the mold cavity with the metal | Gate area, gate number, gate position, coating strength, gating ratio, pouring stability | Increase gate number to divide flow; strengthen coating at gates; balance sprue-runner-gate areas |
In lost foam casting, the pouring system is not only a metal delivery network. It is also a gas management system. The polymer pattern must be replaced by metal while the decomposition products are removed. Therefore, I evaluate the gating system using both hydraulic and gas-transport criteria. The flow rate through the gate is given by the continuity equation:
$$ Q = A_{\text{gate}} v_{\text{gate}} $$
where \(Q\) is the volumetric flow rate, \(A_{\text{gate}}\) is the total gate cross-sectional area, and \(v_{\text{gate}}\) is the metal velocity at the gate. If \(v_{\text{gate}}\) becomes too high, the coating can be washed away or broken, and sand wash defects appear. If \(Q\) is too low, the metal front may advance too slowly, and the pattern may not decompose completely, leading to porosity or cold defects. I therefore try to keep both \(Q\) and \(v_{\text{gate}}\) within a stable window for each lost foam casting product.
My first detailed study concerned a flywheel housing with a mass of approximately 22 kg, an overall envelope of about 440 mm by 440 mm by 220 mm, and a wall thickness of about 5 mm. The material was HT250. The existing lost foam casting process used an inner gate with dimensions of 50 mm length, 30 mm height, and 6 mm width. The melting furnace was an electric furnace, the tapping temperature was 1460 to 1470 °C, the pouring temperature was 1430 to 1440 °C, the vacuum level was -0.025 MPa, and no film covering or pressure holding was used. The main defect was burning-on at the upper region of the internal cavity, and the rejection rate reached about 20%. This was a serious loss because the casting had a large surface area, a thin base wall, and a tendency to deform. I inspected the defect and found that the surface had sand grains and a metallic mixture attached to it. After cleaning, the surface showed a metallic luster. This is typical of mechanical burning-on rather than chemical burning-on. The rest of the housing showed no burning-on. Therefore, I concluded that the problem was local sand compaction rather than a global coating or temperature issue.
In the original pattern assembly, the motor hole was placed downward. The top internal corners had angles greater than 90 degrees. During sand filling and vibration, the sand could not easily reach and compact those corners. The sand at the top of the cavity remained loose. When the metal entered, it penetrated the loose sand and formed a mechanical sand-metal mixture. In addition, the gap between two flywheel housings was only 80 mm. That narrow gap reduced the ability of the sand to flow and compact between the two patterns. The combination of poor local geometry and narrow spacing caused the burning-on defect in the lost foam casting.
To solve this, I changed the pattern orientation so that the motor hole faced upward. This allowed the sand to fill the top region more effectively and ensured that sufficient sand was present above the critical cavity. I also increased the distance between two flywheel housings from 80 mm to 120 mm. This larger spacing allowed the sand to flow more freely between the patterns and to achieve better compaction. I kept the coating process, pouring temperature, and vacuum level unchanged so that I could isolate the effect of the assembly changes. After the changes, I ran a small-batch trial and then a large-batch production trial. The burning-on defect was reduced to zero. The key parameters and results are summarized below.
| Parameter or condition | Original process | Improved process |
|---|---|---|
| Material | HT250 | HT250 |
| Casting mass | About 22 kg | About 22 kg |
| Envelope size | About 440 mm × 440 mm × 220 mm | About 440 mm × 440 mm × 220 mm |
| Wall thickness | About 5 mm | About 5 mm |
| Pattern orientation | Motor hole downward | Motor hole upward |
| Pattern spacing | 80 mm | 120 mm |
| Inner gate size | 50 mm × 30 mm × 6 mm | 50 mm × 30 mm × 6 mm |
| Tapping temperature | 1460 to 1470 °C | 1460 to 1470 °C |
| Pouring temperature | 1430 to 1440 °C | 1430 to 1440 °C |
| Vacuum level | -0.025 MPa | -0.025 MPa |
| Burning-on rejection rate | About 20% | 0% |
This result confirmed an important principle in lost foam casting: local sand fillability must be designed into the pattern assembly. A casting may be geometrically feasible but still fail if the sand cannot reach a shadowed or overhanging region. The sand compaction process can be represented qualitatively by a compactness function:
$$ \rho_{\text{comp}} = f(A_{\text{vibration}}, t_{\text{vibration}}, \mu_{\text{sand}}, d_{\text{gap}}, \theta_{\text{local}}) $$
Here \(\rho_{\text{comp}}\) is the local compacted density, \(A_{\text{vibration}}\) is the vibration amplitude, \(t_{\text{vibration}}\) is the vibration time, \(\mu_{\text{sand}}\) is the sand flow resistance, \(d_{\text{gap}}\) is the spacing between patterns, and \(\theta_{\text{local}}\) is the local angle of the cavity. In my flywheel housing case, increasing \(d_{\text{gap}}\) and changing the orientation improved the sand flow into the critical region. This reduced the probability of mechanical burning-on in the lost foam casting.
My second study concerned porosity in a flywheel housing. The defect appeared at the motor hole on the top of the casting. The external surface looked normal, but after machining, smooth pores with oxidized walls were found beneath the surface. This is typical of subsurface porosity in lost foam casting. The original process used a pouring temperature of 1430 to 1440 °C, a vacuum level of -0.025 MPa, no film covering, and no pressure holding. The porosity rejection rate reached about 30%, which was higher than the burning-on rate in the previous case. The location was concentrated at the highest point of the casting, so I suspected that gas accumulated at the last-filled region and could not escape before the metal solidified.
I identified four main influencing factors. First, when the pouring temperature is too low, the polymer pattern does not decompose fully. The gas generation continues while the metal is already solidifying, and the gas becomes trapped as pores. Second, when the local coating is too thick, the coating resistance increases. The gas generated by the pattern cannot pass through the coating quickly enough. Third, when the vacuum level is too low, the gas removal capacity is insufficient, and the decomposition products remain near the metal front. Fourth, the original process lacked a local exhaust path at the top of the flywheel housing. The gas concentrated at the highest point and had no direct route to escape. Any one of these factors can cause porosity, but in this case the lack of local venting appeared to be the dominant factor.
I designed a controlled-variable experiment to separate the effects. I tested four schemes. In scheme 1, I increased the pouring temperature from 1430 to 1440 °C to 1450 to 1460 °C and poured 20 pieces. In scheme 2, I reduced the local coating thickness from 2.0 mm to 0.5 mm and poured 20 pieces. In scheme 3, I increased the vacuum level from -0.025 MPa to -0.045 MPa and poured 20 pieces. In scheme 4, I added an exhaust piece at the motor hole with dimensions of 50 mm length, 30 mm height, and 5 mm width and poured 20 pieces. In each scheme, I kept the other three variables at their original values so that the comparison would be meaningful. The results are shown in the table below.
| Scheme | Process change in lost foam casting | Pieces poured | Pieces with porosity | Porosity rate |
|---|---|---|---|---|
| 1 | Increase pouring temperature to 1450 to 1460 °C | 20 | 4 | 20% |
| 2 | Reduce local coating thickness to 0.5 mm | 20 | 5 | 25% |
| 3 | Increase vacuum to -0.045 MPa | 20 | 3 | 15% |
| 4 | Add exhaust piece of 50 mm × 30 mm × 5 mm at motor hole | 20 | 0 | 0% |
The results showed that increasing the pouring temperature reduced porosity but did not eliminate it. Reducing the coating thickness also helped somewhat, but the improvement was not stable. Increasing the vacuum level gave a moderate improvement. The most effective measure was the addition of a local exhaust piece. This created a direct path for gas and decomposition products to leave the critical region. After the exhaust piece was added, no porosity was found in the 20-piece trial. I then moved to small-batch and large-batch production, and the motor hole porosity remained effectively zero. This confirmed that local venting is a decisive control lever in lost foam casting when gas accumulates at a high point or a last-filled region.
The gas removal process through the coating and sand can be approximated by a Darcy-type relationship:
$$ Q_{\text{vent}} = \frac{k A \Delta P}{\mu L} $$
where \(Q_{\text{vent}}\) is the volumetric venting rate, \(k\) is the permeability of the coating or sand, \(A\) is the effective venting area, \(\Delta P\) is the pressure difference driving the gas, \(\mu\) is the gas viscosity, and \(L\) is the flow path length. In my porosity case, adding an exhaust piece increased \(A\) and reduced \(L\). This increased \(Q_{\text{vent}}\) and reduced the residual gas pressure. The result was a stable elimination of porosity in the lost foam casting. I also noted that vacuum alone cannot compensate for a missing local vent if the gas path is blocked by a thick coating or by a geometric high point. The exhaust piece worked because it changed the local transport geometry, not merely the global vacuum level.
My third study concerned sand wash in a connecting-rod rest. The material was HT200, the mass was about 50 kg, the envelope size was about 572 mm by 380 mm by 348 mm, and the base plate thickness was about 12 mm. The original lost foam casting process used three side inner gates. Each inner gate had dimensions of 60 mm length, 30 mm height, and 6 mm width. The tapping temperature was 1460 to 1470 °C, the pouring temperature was 1430 to 1440 °C, and the vacuum level was -0.03 MPa. No film covering or pressure holding was used. The main defect was sand wash concentrated near the bottom inner gate and at the cavity region where the gate metal entered. The rejection rate was about 20%. The defect appeared as a mixed sand-metal tumor on the surface. This indicated that the coating had been broken or eroded and that sand had entered the cavity with the metal.
I considered three main causes. First, the coating strength at the inner gate may have been too low. The metal flow eroded the coating and exposed the sand. Second, the local pressure or velocity at the inner gate may have been too high. A high local velocity can break the coating even if the coating itself is acceptable. Third, severe metal backflow or splashing during pouring can rupture the coating. However, I observed that the pouring process was stable and that there was no serious backflow. Therefore, I focused on coating strength and gate pressure as the primary factors.
I first increased the coating thickness at the inner gate. The original process used two coating dips, giving a coating thickness of about 1.5 mm. I added one more dip at the inner gate, increasing the local coating thickness to about 2.2 mm. I poured 50 pieces. The sand wash count was 6, giving a rate of 12%. This was an improvement, but not a complete solution. I then changed the gating layout by adding one more bottom inner gate of the same size. This increased the number of bottom gates and divided the metal flow. I poured 50 pieces. The sand wash count was 0. The additional gate reduced the local velocity and pressure at each gate, which protected the coating and reduced sand erosion. The results are summarized below.
| Scheme | Process change in lost foam casting | Pieces poured | Pieces with sand wash | Sand wash rate |
|---|---|---|---|---|
| 1 | Add one coating dip at the inner gate; thickness about 2.2 mm | 50 | 6 | 12% |
| 2 | Add one bottom inner gate of the same size | 50 | 0 | 0% |
After the successful trial, I optimized the final gating system. I used three bottom inner gates and one top inner gate. The individual inner gate cross-section was 60 mm by 8 mm. The sprue was a round pipe with a diameter of 50 mm. The runner cross-section was 50 mm by 40 mm. The total inner gate area was calculated from the number of gates. The gating ratio was then checked against the conventional one-to-one-to-one condition. The relevant formulas are:
$$ A_{\text{sprue}} = \frac{\pi d_{\text{sprue}}^2}{4} $$
$$ A_{\text{runner}} = w_{\text{runner}} h_{\text{runner}} $$
$$ A_{\text{gate,total}} = n w_{\text{gate}} h_{\text{gate}} $$
Using the final dimensions, the sprue area was about 1960 mm², the runner area was 2000 mm², and the total inner gate area was about 1920 mm². The ratio was therefore approximately:
$$ A_{\text{sprue}} : A_{\text{runner}} : A_{\text{gate,total}} = 1960 : 2000 : 1920 \approx 1 : 1.02 : 0.98 $$
This is close to the desired 1:1:1 condition. A balanced gating ratio is important in lost foam casting because it helps control the metal velocity and pressure distribution. When the sprue, runner, and gates are properly proportioned, the metal fills the mold more smoothly, the coating experiences less local impact, and sand wash is less likely to occur. In this connecting-rod rest, the additional bottom gate and the balanced gating ratio solved the sand wash defect completely in the subsequent small-batch and large-batch production trials.
The relationship between gate velocity and local pressure can be expressed through a simplified Bernoulli form:
$$ P_{\text{local}} + \frac{1}{2}\rho v_{\text{gate}}^2 = P_{\text{upstream}} + \frac{1}{2}\rho v_{\text{upstream}}^2 + \Delta P_{\text{loss}} $$
Here \(P_{\text{local}}\) is the local pressure at the gate, \(\rho\) is the metal density, \(v_{\text{gate}}\) is the gate velocity, \(P_{\text{upstream}}\) is the upstream pressure, \(v_{\text{upstream}}\) is the upstream velocity, and \(\Delta P_{\text{loss}}\) is the pressure loss through the gating system. When the number of gates is increased while the total flow rate is kept nearly constant, \(v_{\text{gate}}\) decreases, and the local dynamic pressure is reduced. This protects the coating and reduces sand wash. This principle guided my design change in the lost foam casting of the connecting-rod rest.
Across these three studies, I developed a general procedure for defect control in lost foam casting. The procedure begins with defect identification. I first determine whether the defect is burning-on, porosity, or sand wash. I then examine the location. If the defect is at a top corner or an overhanging region, sand compaction is usually the main concern. If the defect is at a high point or last-filled region, gas removal is usually the main concern. If the defect is at or near a gate, coating strength and gate velocity are usually the main concerns. After identifying the dominant mechanism, I adjust the pattern assembly, the gating system, the coating, the vacuum, and the pouring temperature in a logical sequence.
I also use a controlled-variable approach during process validation. In lost foam casting, many variables interact, so it is easy to make multiple changes at once and then fail to understand which change was effective. In my porosity study, for example, I changed only one variable in each scheme. This allowed me to see that local venting was far more effective than raising the pouring temperature, reducing coating thickness, or increasing vacuum. In my sand wash study, I first increased coating thickness and then added a gate. The gate addition produced the decisive improvement. In my burning-on study, I changed the pattern orientation and spacing together because they were both related to sand fillability. In each case, I confirmed the result with small-batch trials before moving to large-batch production.
The following table summarizes the final process settings and outcomes for the three cases. It shows how different lost foam casting defects require different combinations of process levers.
| Case | Defect | Main original cause | Final corrective measure | Final result |
|---|---|---|---|---|
| Flywheel housing burning-on | Mechanical burning-on at upper internal cavity | Loose sand at top corners; narrow pattern spacing | Motor hole upward; pattern spacing increased from 80 mm to 120 mm | Burning-on reduced to 0% |
| Flywheel housing porosity | Subsurface porosity at motor hole | Gas trapped at top; insufficient local venting | Exhaust piece 50 mm × 30 mm × 5 mm at motor hole | Porosity reduced to 0% |
| Connecting-rod rest sand wash | Sand wash near bottom gate | High local gate velocity; coating rupture | Additional bottom gate; balanced 1:1:1 gating ratio | Sand wash reduced to 0% |
In lost foam casting, the coating is a critical functional layer. It must have enough strength to resist metal erosion, but it must also have enough permeability to allow decomposition gas to escape. These two requirements can conflict. A thick coating may resist sand wash, but it may also trap gas. A thin coating may vent gas well, but it may be eroded by fast metal flow. I therefore treat coating thickness as a local variable rather than a global constant. At gates, I increase coating thickness and strength. At high points and last-filled regions, I reduce coating thickness or add vents. This local approach is more effective than applying a single coating thickness to the entire pattern in lost foam casting.
The vacuum system also plays a dual role in lost foam casting. It helps remove gas and it helps compact the sand. However, increasing the vacuum level alone does not always solve porosity. In my porosity study, increasing the vacuum from -0.025 MPa to -0.045 MPa reduced the porosity rate from 30% to 15%, but it did not eliminate the defect. The exhaust piece eliminated the defect. This shows that gas removal depends on the local path as much as on the global driving pressure. If the gas is trapped behind a thick coating or in a dead-end region, a higher vacuum may not be sufficient. The local vent must be provided in the design of the pattern cluster.
Similarly, increasing the pouring temperature can help decompose the pattern and reduce the viscosity of the metal, but it can also increase gas generation and may cause other defects such as shrinkage or sand penetration. In my porosity study, raising the pouring temperature to 1450 to 1460 °C reduced the porosity rate from 30% to 20%, but it did not eliminate the defect. I therefore consider pouring temperature a secondary adjustment when local venting is inadequate. The primary action should be to improve gas transport through pattern design and gating design in lost foam casting.
The gating system in lost foam casting must also be designed to avoid sand wash. When the metal enters the mold, it must displace the pattern and the decomposition products. If the gate area is too small, the local velocity is high, and the coating can be washed away. If the gate area is too large, the metal may enter too slowly, and the pattern may not decompose completely. I therefore calculate the total gate area and compare it with the sprue and runner areas. A balanced ratio helps maintain a stable metal front. In my connecting-rod rest, the final ratio of approximately 1:1.02:0.98 gave stable filling and eliminated sand wash. I also added a bottom gate to divide the flow. This reduced the local pressure at each gate and protected the coating.
I have also learned that pattern assembly is not only a handling issue. It is a process design issue in lost foam casting. The orientation of the pattern determines how sand fills the cavity. The spacing between patterns determines how sand compacts between them. The position of the motor hole, the location of ribs, and the angle of internal corners all affect sand flow. In the flywheel housing burning-on case, changing the motor hole from downward to upward and increasing the pattern spacing from 80 mm to 120 mm solved the defect. No change in pouring temperature or vacuum was needed. This shows that a geometric process change can be more powerful than a parameter change in lost foam casting.
For process validation, I use a staged approach. I begin with a small batch to confirm that the proposed change produces a measurable improvement. I then increase the batch size gradually. I record the defect rate at each stage and compare it with the baseline. I also record the process parameters to ensure that the validation is repeatable. The table below shows a general validation template that I use for lost foam casting defect reduction.
| Validation stage | Batch size | Objective | Acceptance criterion |
|---|---|---|---|
| Baseline | 20 to 50 pieces | Confirm defect type and rate | Establish current rejection rate |
| Single-variable trial | 10 to 20 pieces per scheme | Identify the dominant process lever | Best scheme shows clear reduction |
| Small-batch confirmation | 50 pieces | Confirm repeatability | Defect rate below target |
| Large-batch production | Several hundred pieces | Verify stability under production conditions | Defect rate remains at or near zero |
In all three cases, the final result was achieved after production and machining. The burning-on, porosity, and sand wash defects were either eliminated or reduced to zero. The improvements were not caused by a single universal parameter. Instead, they came from understanding the specific mechanism of each defect and applying the correct process lever. For burning-on, the lever was sand fillability through pattern orientation and spacing. For porosity, the lever was local gas venting through an exhaust piece. For sand wash, the lever was flow division and gating balance through an additional gate and a 1:1:1 ratio. This mechanism-based approach is central to my work in lost foam casting.
I also want to emphasize the importance of the inner gate inlet layout. The inlet position determines where the metal first contacts the pattern, where the gas is generated most rapidly, and where the coating experiences the highest stress. If the inlet is placed at a thin wall or a sharp corner, the local velocity may be too high, and sand wash or burning-on may occur. If the inlet is placed at a low point, gas may be pushed toward a high point and become trapped. In my work, I moved the inlet layout toward a more balanced configuration. In the flywheel housing, the motor hole was moved upward so that gas could escape more easily. In the connecting-rod rest, the bottom gates were increased to divide the flow. These changes improved both metal flow and gas transport in lost foam casting.
The relationship between gate position and gas transport can be described qualitatively. If the gate is located so that the metal front sweeps the pattern from bottom to top, the decomposition gas is pushed toward the vents. If the gate is located so that the metal front traps gas in a dead-end region, porosity appears. I therefore try to place gates so that the last-filled region coincides with a vent or an exhaust path. This principle is especially important in lost foam casting of thin-walled shell components, where the metal front can advance quickly and the gas can be trapped easily.
The exhaust and slag-discharge risers also play an important role. In lost foam casting, a riser can serve as a gas vent, a slag trap, and a feeding path. When I add a riser at a high point, I create a local path for gas and non-metallic residues to leave the mold. In the flywheel housing porosity case, the exhaust piece at the motor hole acted as a local vent. It was small, but it changed the local pressure balance and allowed the gas to escape. The size and position of the exhaust piece must be matched to the local gas generation rate. If it is too small, it may not provide enough venting. If it is too large, it may affect the casting geometry or create a new defect. I used a 50 mm by 30 mm by 5 mm exhaust piece, and it was effective.
For slag discharge, I have found that a riser placed at the end of the metal flow path can collect decomposition residues and slag. This reduces the risk of slag inclusions in the casting. In lost foam casting, the decomposition residues are often sticky and can adhere to the coating or remain in the metal. A well-placed slag-discharge riser can capture these residues and prevent them from entering the critical sections of the mold. I therefore consider exhaust and slag-discharge risers as part of the gas and residue management system, not merely as feeding aids.
My overall conclusion is that defect control in lost foam casting requires a systematic and mechanism-based approach. I do not rely on a single global parameter such as vacuum or pouring temperature. Instead, I identify the defect type and location, determine the dominant mechanism, and then adjust the pattern assembly, gating system, coating, venting, and vacuum accordingly. I validate each change with controlled trials and staged production. This approach has allowed me to solve burning-on, porosity, and sand wash defects in flywheel housings and connecting-rod rests. It has also improved the stability and repeatability of the lost foam casting process.
The following table summarizes the key process variables and their recommended direction of adjustment for each defect type. I use this table as a practical guide during process design and troubleshooting in lost foam casting.
| Defect | Pattern assembly | Gating system | Coating | Vacuum | Pouring temperature |
|---|---|---|---|---|---|
| Burning-on | Reorient to improve sand fill; increase pattern spacing | Maintain stable filling; avoid high local velocity | Use adequate refractory strength; avoid excessive thickness in shadowed areas | Maintain sufficient sand compaction | Keep within stable range; avoid excessive superheat |
| Porosity | Place high points near vents; avoid dead-end gas traps | Position gates to sweep gas toward vents | Reduce local thickness at high points; maintain permeability | Increase within limits; do not rely on vacuum alone | Increase moderately if decomposition is incomplete |
| Sand wash | Support coating at gates; avoid sharp changes in section | Increase gate number; balance sprue-runner-gate ratio | Increase local coating strength at gates | Maintain stable vacuum; avoid excessive turbulence | Keep within normal range; avoid too low temperature |
In my experience, the most successful lost foam casting projects are those in which the process design is considered from the beginning. The pattern assembly, gating system, coating, venting, and vacuum should be treated as an integrated system. When a defect appears, the first question should be: where is the gas or sand going, and why? The answer usually points to a local geometric or transport problem. By correcting that local problem, I have been able to eliminate defects that initially seemed to require major changes in pouring temperature or vacuum. The three cases described here show that burning-on, porosity, and sand wash can be controlled effectively when the underlying mechanism is understood and the correct process lever is applied.
Finally, I continue to use the same disciplined sequence in every lost foam casting development project: establish the current condition, analyze the cause, formulate a plan, implement countermeasures, and confirm the effect. This sequence prevents random process changes and makes the results repeatable. It also helps transfer successful solutions from one product to another. In lost foam casting, the geometry and the process are closely linked, and the best results come from designing the two together. The measures I have described, including pattern reorientation, pattern spacing adjustment, local exhaust pieces, additional bottom gates, and balanced gating ratios, provide a practical foundation for reducing defects and improving the quality of lost foam casting products.