
In the foundry industry, internal shrinkage porosity and cavities in ductile cast iron castings are common yet challenging issues to resolve. These defects critically impact the mechanical properties and service life of castings, especially for components requiring high densification, such as those used in heavy machinery. Selecting an appropriate feeding process is a prerequisite for mitigating these defects. Typically, feeding risers are placed on the top or side of the casting section needing feeding, but which location yields superior results? Based on practical experience in addressing internal defects in ductile cast iron products, this article explores the differences between top feeding and side feeding processes through a case study. By validating these approaches on the same casting, we demonstrate the efficacy of top feeding over side feeding and draw conclusive insights.
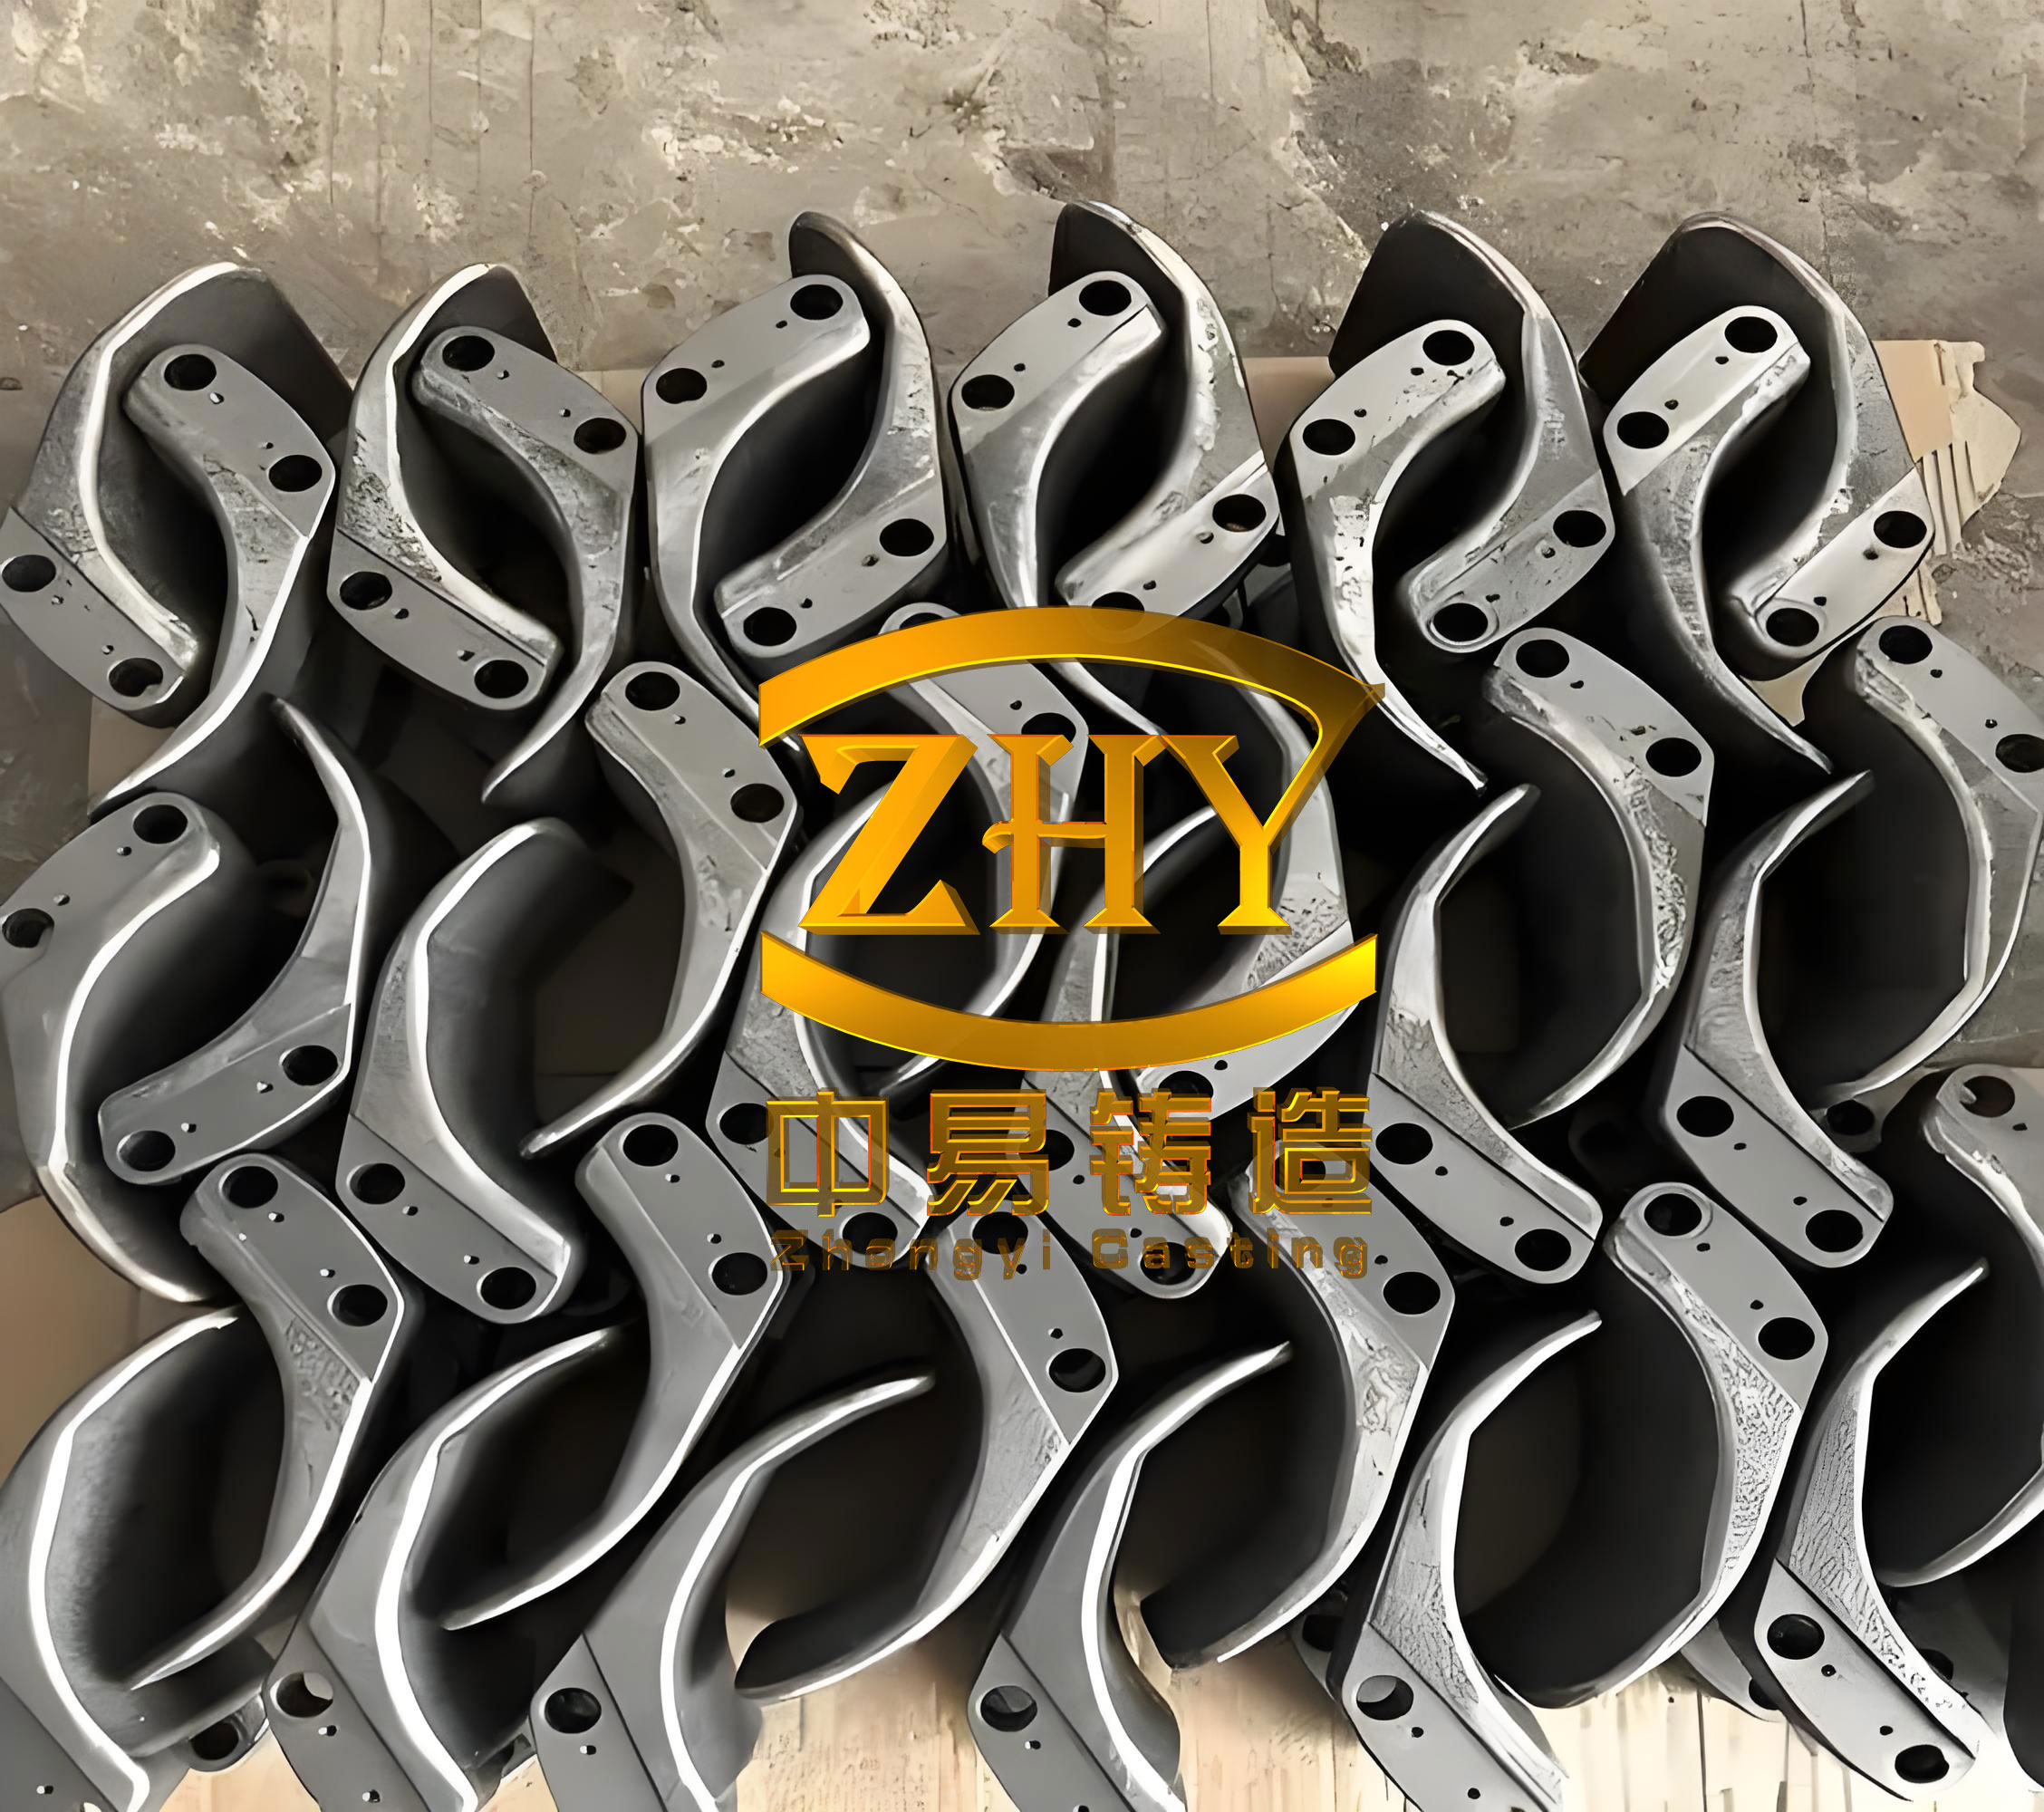
Ductile cast iron, known for its excellent ductility and strength, is widely used in automotive and industrial applications. However, its solidification characteristics, including graphitization expansion and contraction, often lead to shrinkage defects if not properly controlled. The feeding process plays a pivotal role in ensuring sound castings. In our pursuit of expanding into overseas markets and producing high-value-added products, we have developed various steering gear castings made of ductile cast iron, ranging from 15 kg to 250 kg. Each product presents unique challenges, necessitating continuous process optimization. One particular steering gear for a large excavator, with a weight exceeding 81.5 kg, posed significant difficulties due to its thick sections (over 30 mm) and isolated hot spots, the largest having a thermal diameter of approximately 60 mm. The customer demanded high internal densification, with no visible shrinkage defects, adhering to a quality standard above grade 2. This requirement pushed us to refine our feeding strategies.
The causes of shrinkage defects in ductile cast iron castings are multifaceted. Primarily, they stem from the casting design, melting practice, mold and core materials, and process layout. For instance, thick and uneven walls can lead to inadequate thermal feeding, while isolated hot spots disrupt directional solidification. However, altering the casting design is often impractical as it is dictated by functional requirements. Similarly, adjustments in melting processes or sand properties might be constrained by existing production setups, such as large-scale automated molding lines and cupola melting systems. Therefore, process design modifications, particularly in feeding systems, offer the most viable solution. Key aspects include the design of gating systems, riser placement, size, and neck configuration, all of which influence the feeding efficiency. In ductile cast iron, the solidification shrinkage can be modeled using the following formula for volumetric contraction:
$$ \Delta V = V_0 \cdot \beta \cdot (T_{\text{liquidus}} – T_{\text{solidus}}) $$
where \(\Delta V\) is the volume shrinkage, \(V_0\) is the initial volume, \(\beta\) is the coefficient of volumetric shrinkage for ductile cast iron, and \(T_{\text{liquidus}}\) and \(T_{\text{solidus}}\) are the liquidus and solidus temperatures, respectively. For typical ductile cast iron like QT500-7, \(\beta\) ranges from 4% to 6%, necessitating effective riser design to compensate. The riser efficiency \(\eta\) can be expressed as:
$$ \eta = \frac{V_{\text{feeding}}}{V_{\text{riser}}} \times 100\% $$
where \(V_{\text{feeding}}\) is the volume of metal fed to the casting and \(V_{\text{riser}}\) is the riser volume. Exothermic riser sleeves, commonly used for ductile cast iron, can enhance \(\eta\) from around 10% to 50% by insulating the riser and prolonging its liquid state.
Initially, for the large excavator steering gear casting, we employed a side feeding process. An exothermic riser sleeve of size 80/110 mm was embedded in a side core to feed the largest hot spot. The riser neck was formed by the core with a rectangular cross-section of 45 mm × 25 mm. Despite this, evaluation via sectioning (as per the inspection plan) revealed severe shrinkage defects at the hot spot, with a porous area of 37.0 mm × 20.0 mm and a maximum cavity of 8.0 mm × 3.0 mm. To address this, we added a chill plate of dimensions 75 mm × 50 mm × 15 mm adjacent to the hot spot to promote faster cooling and reduce shrinkage tendency. This improvement reduced the defect size to 13.0 mm × 5.0 mm with a maximum cavity of 1.0 mm × 3.0 mm, but it still fell short of the customer’s grade 2 requirement. The limitations of side feeding became apparent, likely due to extended feeding channels and premature solidification of the riser neck.
We then shifted to a top feeding approach. The same exothermic riser sleeve was repositioned directly above the hot spot, embedded in the upper core. The riser neck was shortened to 15 mm and changed to a circular cross-section of 35 mm diameter, which minimizes early freezing compared to a rectangular neck. The modification aimed to streamline the feeding path and enhance riser efficiency. Upon testing, sectioning showed complete elimination of shrinkage defects, meeting the quality standard. This success underscores the superiority of top feeding for difficult-to-feed sections in ductile cast iron castings.
To quantify the differences, we can analyze the feeding effectiveness using theoretical models and empirical data. The feeding distance \(L\) for a riser in ductile cast iron can be estimated using:
$$ L = k \cdot \sqrt{A} $$
where \(A\) is the cross-sectional area of the casting section and \(k\) is a constant dependent on the feeding mode. For side feeding, \(k\) is typically lower due to lateral heat dissipation, whereas for top feeding, \(k\) is higher as gravity aids feeding. Additionally, the solidification time \(t\) of the riser neck is critical and can be approximated by Chvorinov’s rule:
$$ t = B \cdot \left( \frac{V}{A_s} \right)^2 $$
where \(B\) is the mold constant, \(V\) is the volume of the neck, and \(A_s\) is its surface area. A circular neck has a higher volume-to-surface area ratio than a rectangular one, delaying solidification and improving feeding. The following table summarizes the key parameters and outcomes for both feeding processes:
| Parameter | Side Feeding Process | Top Feeding Process |
|---|---|---|
| Riser Type | Exothermic sleeve (80/110 mm) | Exothermic sleeve (80/110 mm) |
| Riser Placement | Embedded in side core | Embedded in top core above hot spot |
| Riser Neck Dimensions | Rectangular: 45 mm × 25 mm | Circular: diameter 35 mm |
| Neck Length | Approx. 40 mm | 15 mm |
| Additional Chill | 75 mm × 50 mm × 15 mm plate used | No chill required |
| Shrinkage Defect Area | 37.0 mm × 20.0 mm (initial), 13.0 mm × 5.0 mm (with chill) | None detected |
| Maximum Cavity Size | 8.0 mm × 3.0 mm (initial), 1.0 mm × 3.0 mm (with chill) | None |
| Feeding Efficiency \(\eta\) | Estimated 30-40% | Estimated 50-60% |
| Solidification Time of Neck | Shorter due to rectangular shape | Longer due to circular shape |
The improvement with top feeding can also be explained through pressure head analysis. In top feeding, the metallostatic pressure \(P\) at the feeding point is given by:
$$ P = \rho g h $$
where \(\rho\) is the density of ductile cast iron (approximately 7100 kg/m³), \(g\) is gravity (9.81 m/s²), and \(h\) is the height of the metal column from the riser to the hot spot. For top feeding, \(h\) is maximized, enhancing feeding force. In contrast, side feeding often results in a lower effective \(h\) due to horizontal pathways. Moreover, the temperature gradient \(\nabla T\) during solidification is more favorable in top feeding, promoting directional solidification toward the riser. This can be expressed as:
$$ \nabla T = \frac{T_{\text{riser}} – T_{\text{casting}}}{\delta} $$
where \(\delta\) is the distance between the riser and the hot spot. With top feeding, \(\delta\) is minimized, increasing \(\nabla T\) and improving feeding.
In our case, the ductile cast iron casting had multiple isolated hot spots, but the largest one at the side ear was critical. The side feeding process, despite using an exothermic riser, suffered from a long feeding path and neck geometry that solidified early, hindering补偿. The addition of chills helped but added complexity. Top feeding, by placing the riser directly above, shortened the path and utilized a circular neck for better longevity. This aligns with principles of directional solidification, where risers should be placed at the top of thick sections to feed downward under gravity. For ductile cast iron, which experiences graphitization expansion, proper feeding is essential to counteract the residual shrinkage after expansion. The expansion pressure \(P_{\text{exp}}\) from graphitization can be estimated as:
$$ P_{\text{exp}} = \alpha E \Delta T $$
where \(\alpha\) is the thermal expansion coefficient, \(E\) is Young’s modulus, and \(\Delta T\) is the temperature drop during graphitization. However, if feeding is inadequate, shrinkage defects still occur.
To further generalize, we can derive a criterion for selecting feeding modes. For a given hot spot diameter \(D\) and casting thickness \(T\), top feeding is preferred when the aspect ratio \(L/D\) (where \(L\) is the feeding distance) exceeds a threshold. Based on our experience with ductile cast iron castings, we propose the following heuristic: if the hot spot is in a thick, isolated region with \(D > 50\) mm, top feeding with an exothermic riser is more effective. The table below compares the applicability of side vs. top feeding for various scenarios in ductile cast iron castings:
| Casting Feature | Side Feeding Suitability | Top Feeding Suitability |
|---|---|---|
| Thin-walled sections (< 20 mm) | High (minimal shrinkage risk) | Low (unnecessary) |
| Thick sections (20-50 mm) with adjacent risers | Moderate | Moderate |
| Isolated hot spots (> 50 mm diameter) | Low (risk of defects) | High (effective feeding) |
| Complex geometries with cores | High (flexible placement) | Moderate (may require core redesign) |
| High densification requirements (grade 2+) | Low (often inadequate) | High (superior results) |
The success of top feeding in this ductile cast iron casting has broader implications. It reduces the need for chills, simplifying production and lowering costs. Moreover, it establishes a process platform for similar high-integrity castings. In foundry practice, side feeding is often favored for its simplicity and ease of implementation, but for critical applications, top feeding should be considered. This is particularly true for ductile cast iron, where the margin for error is small due to stringent quality demands.
In conclusion, through practical validation on a large ductile cast iron steering gear casting, we have demonstrated that top feeding yields better results than side feeding for eliminating shrinkage defects. The key factors include shorter feeding channels, optimized riser neck geometry, and enhanced metallostatic pressure. This approach not only solved the immediate problem but also provided a reliable method for future developments. As the foundry industry evolves, leveraging such insights will be crucial for producing high-quality ductile cast iron components. Continued research into feeding mechanics, perhaps incorporating simulation tools, can further refine these processes. For now, we recommend top feeding for ductile cast iron castings with thick, isolated hot spots and high densification requirements, as it offers a robust solution to a perennial challenge.
To encapsulate, the journey from side to top feeding highlights the importance of iterative process optimization in foundry engineering. Each ductile cast iron casting presents unique challenges, but by understanding the underlying principles of solidification and feeding, we can devise effective strategies. The tables and formulas presented herein serve as a guide for practitioners seeking to enhance their feeding techniques. As we continue to push the boundaries of ductile cast iron applications, such knowledge will be indispensable in achieving sound, reliable castings that meet the ever-increasing demands of industry.