
In my extensive experience with the lost foam casting process, I have observed its growing adoption in metal casting industries, particularly for producing components like crude lead molds used in lead smelting. The lost foam casting process, also known as expendable pattern casting, offers significant advantages in terms of efficiency, surface finish, and dimensional accuracy compared to traditional sand casting. However, due to its unique characteristics, the lost foam casting process is prone to specific defects that can compromise product quality. In this article, I will delve into the common defects encountered in the lost foam casting process for steel castings, such as crude lead molds, and provide detailed preventive measures based on my analysis and practical insights. I will emphasize the importance of rigorous process control and illustrate key points using tables and formulas to enhance understanding.
The lost foam casting process involves using a foam pattern that vaporizes upon contact with molten metal, leaving behind a precise casting. For crude lead molds, which are typically made from low-carbon steel and melted in medium-frequency electric furnaces, the process requires careful attention to avoid defects. The chemical composition of the low-carbon steel used is critical, as shown in Table 1. In my work, I have found that even minor deviations in the lost foam casting process can lead to issues like carbon increase, porosity, and slag inclusion, which I will explore in depth.
| Element | Content (%) |
|---|---|
| C | < 0.2 |
| Si | < 0.5 |
| Mn | 0.3–0.8 |
| S | < 0.03 |
| P | < 0.08 |
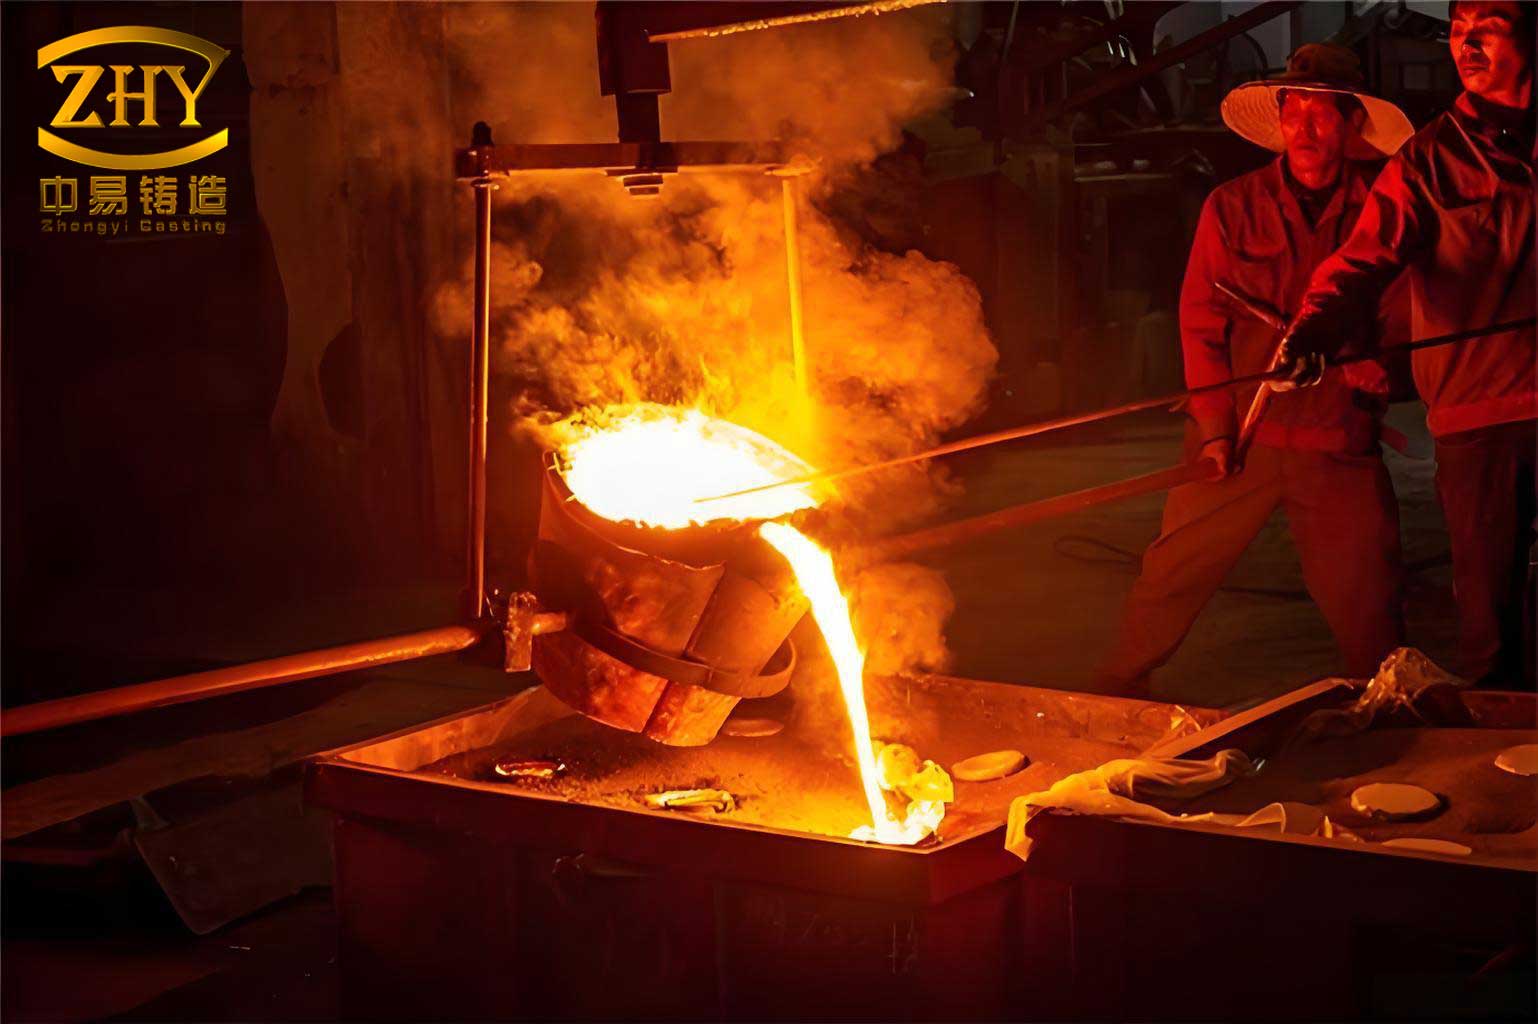
The lost foam casting process relies on a foam pattern that is coated with a refractory coating and embedded in dry sand, followed by vacuum-assisted pouring. A schematic of the process is often illustrated to highlight key stages, such as pattern assembly, coating, and molding. For instance, in the production of crude lead molds, the pattern is typically designed with a gating system to ensure smooth metal flow. To visualize this, I include a reference image that depicts the essential steps in the lost foam casting process, which can aid in understanding the context of the defects discussed.
Now, let me discuss the common defects in the lost foam casting process, starting with carbon increase defects. In the lost foam casting process, the foam pattern, usually made from expanded polystyrene (EPS) or polymethyl methacrylate (PMMA), decomposes upon contact with molten steel, releasing gases and free carbon. This can lead to localized carbon enrichment in the casting, especially at areas like corners, ends of metal flow, or where gases are trapped. From my analysis, the mechanism involves the decomposition of the foam pattern, which primarily consists of carbon and hydrogen. Upon heating, the pattern cracks and decomposes, producing hydrogen and free carbon. The hydrogen may combine with oxygen to form water vapor, but the free carbon can diffuse into the steel surface, causing carburization. The depth of carburization can reach up to 2 mm, increasing the carbon content by about 0.1%, which is detrimental for low-carbon steel applications like crude lead molds.
To quantify this, consider the diffusion of carbon into steel, which can be described by Fick’s laws. The rate of carbon diffusion depends on factors such as temperature and time. For example, the carbon concentration profile can be approximated by:
$$ C(x,t) = C_0 + (C_s – C_0) \cdot \text{erfc}\left(\frac{x}{2\sqrt{Dt}}\right) $$
where \( C(x,t) \) is the carbon concentration at depth \( x \) and time \( t \), \( C_0 \) is the initial carbon content in the steel, \( C_s \) is the surface carbon concentration, \( D \) is the diffusion coefficient, and erfc is the complementary error function. In the lost foam casting process, high temperatures accelerate diffusion, so controlling process parameters is crucial. Based on my observations, preventive measures for carbon increase defects include selecting high-quality foam materials, optimizing pouring techniques, and maintaining appropriate vacuum levels. For instance, using PMMA foam instead of EPS can reduce free carbon generation due to its lower carbon content and higher molecular weight. Additionally, ensuring a pouring temperature above 1550°C and a vacuum holding time of over 20 minutes promotes complete vaporization and gas removal, minimizing carbon pickup. I also recommend adjusting alloying elements like manganese, which can sequester carbon at the gas-metal interface, reducing its migration into the steel. These strategies are essential in the lost foam casting process to maintain the desired low-carbon properties.
Moving on to porosity defects, which are prevalent in the lost foam casting process and can severely affect the service life of castings like crude lead molds. Porosity can manifest as internal voids, surface pinholes, or subsurface bubbles, leading to cracking or difficulties in demolding. In my experience, porosity in the lost foam casting process arises from various sources, which I categorize and address below.
First, porosity caused by the entrapment of foam decomposition products. During pouring in the lost foam casting process, turbulent flow can envelop foam fragments, which then decompose and release gases that cannot escape, forming large, carbon-lined pores. To prevent this, I advocate for a bottom-gating system to ensure laminar flow, as described by the Reynolds number for fluid dynamics:
$$ Re = \frac{\rho v L}{\mu} $$
where \( Re \) is the Reynolds number, \( \rho \) is the density of molten steel, \( v \) is the flow velocity, \( L \) is a characteristic length, and \( \mu \) is the viscosity. Keeping \( Re \) low (typically below 2000 for laminar flow) reduces turbulence. Moreover, increasing pouring temperature and vacuum level enhances foam vaporization and gas evacuation. I have found that a vacuum of 0.045–0.055 MPa is optimal for most applications in the lost foam casting process.
Second, porosity due to inadequate drying of foam patterns or coatings. If the foam pattern retains moisture or the coating is not fully dry, vapor generation during pouring can create gas pockets. This is common when patterns are assembled with adhesives or when environmental humidity is high. The amount of gas produced can be estimated using the ideal gas law:
$$ PV = nRT $$
where \( P \) is pressure, \( V \) is volume, \( n \) is the number of moles of gas, \( R \) is the gas constant, and \( T \) is temperature. To mitigate this, I insist on thorough drying of patterns and coatings, and I minimize the use of adhesives by opting for single-piece foam patterns whenever possible. In the lost foam casting process, proper drying cycles are critical; for example, patterns should be dried at temperatures around 50–60°C for several hours.
Third, porosity from excessive pattern adhesives. Adhesives used to join foam sections have high gas evolution rates, and if overapplied, they can slow decomposition and trap gases. From my trials, using low-gas-emission adhesives and applying them sparingly can significantly reduce porosity. A summary of porosity types and solutions in the lost foam casting process is provided in Table 2.
| Porosity Type | Primary Cause | Preventive Measures |
|---|---|---|
| Entrapped decomposition products | Turbulent metal flow and incomplete vaporization | Use bottom-gating systems; increase pouring temperature and vacuum; improve coating permeability |
| Moisture-related | Wet foam patterns or coatings | Ensure complete drying; control humidity during storage; use dry sand |
| Adhesive-induced | Excessive or high-gas adhesives | Minimize adhesive use; select low-emission adhesives; prefer monolithic patterns |
Another critical defect in the lost foam casting process is slag inclusion and sand sticking, which often appear as surface blemishes or internal inclusions in castings like crude lead molds. These defects can result from the erosion of coatings or the entrainment of sand particles during pouring. In my analysis, slag inclusion in the lost foam casting process is frequently observed at locations such as gating systems, corners, or large flat surfaces, where metal flow is erratic or where vacuum forces draw in loose sand. Sand sticking, on the other hand, occurs when the refractory coating fails to protect the pattern, allowing molten metal to penetrate the sand mold.
The mechanism involves the interaction between molten metal, coating, and sand. For instance, if the coating has low strength or poor adhesion, it can crack under thermal stress, leading to metal infiltration. The probability of sand entrainment can be related to the vacuum pressure and flow dynamics. From my experiments, I have derived that the critical velocity for sand entrainment, \( v_c \), can be expressed as:
$$ v_c = \sqrt{\frac{2 \gamma \cos \theta}{\rho r}} $$
where \( \gamma \) is the surface tension of molten metal, \( \theta \) is the contact angle, \( \rho \) is the density, and \( r \) is the pore radius in the sand. To prevent these defects in the lost foam casting process, I recommend several measures. First, replace foam gating systems with refractory ceramic gating materials to withstand high-temperature erosion. Second, design patterns with generous fillet radii to smooth metal flow and reduce turbulence. Third, use high-strength, permeable coatings that are applied evenly and dried thoroughly. I have found that coatings with alumina-based binders perform well in the lost foam casting process for steel castings. Fourth, control the molding process by layering sand in thin increments and compacting adequately to avoid voids. Fifth, pour soon after molding to prevent sand settling or moisture absorption. Lastly, optimize vacuum levels; excessive vacuum can increase sand ingestion, so I typically maintain a vacuum of 0.045–0.055 MPa, as mentioned earlier. Table 3 summarizes these aspects.
| Defect | Typical Locations | Root Causes | Preventive Measures |
|---|---|---|---|
| Slag inclusion | Gating systems, corners, riser areas | Coating erosion, turbulent flow, high vacuum | Use ceramic gating; improve coating quality; optimize pouring parameters |
| Sand sticking | Large flat surfaces, bottom walls | Coating failure, high metal penetration, inadequate sand compaction | Apply uniform coatings; control sand grain size; ensure proper molding techniques |
Beyond these defects, the lost foam casting process can also exhibit issues like cold shuts, misruns, or surface wrinkles, but in my focus on crude lead molds, the aforementioned defects are most prevalent. To further elaborate on preventive strategies, I emphasize the role of process modeling and simulation. For example, computational fluid dynamics (CFD) can predict metal flow and temperature distribution in the lost foam casting process, helping to design better gating systems. The energy balance during foam decomposition can be modeled using the following equation:
$$ Q = m_f \cdot \Delta H_f + m_c \cdot \Delta H_c $$
where \( Q \) is the total heat required, \( m_f \) is the mass of foam, \( \Delta H_f \) is the heat of decomposition, \( m_c \) is the mass of coating, and \( \Delta H_c \) is the heat absorbed by the coating. This highlights the importance of thermal management in the lost foam casting process.
In my practice, I have also noted that post-casting treatments, such as annealing, are vital for relieving stresses and homogenizing microstructure in castings produced via the lost foam casting process. For low-carbon steel crude lead molds, I recommend an intermediate temperature annealing cycle at around 650–700°C to enhance ductility and reduce cracking tendencies. The kinetics of recrystallization during annealing can be described by the Avrami equation:
$$ X = 1 – \exp(-k t^n) $$
where \( X \) is the fraction transformed, \( k \) is a rate constant, \( t \) is time, and \( n \) is the Avrami exponent. This underscores how material science principles integrate with the lost foam casting process.
To summarize the key insights from my analysis of the lost foam casting process, I present a comprehensive checklist for quality assurance in Table 4. This table encapsulates the critical parameters and actions needed to mitigate defects in the lost foam casting process for steel castings like crude lead molds.
| Aspect | Parameter | Optimal Range | Rationale |
|---|---|---|---|
| Foam Material | Type and density | PMMA foam, low density (20–25 kg/m³) | Reduces free carbon generation and improves vaporization |
| Pouring Temperature | Steel temperature | > 1550°C | Ensures complete foam decomposition and reduces carbon pickup |
| Vacuum Level | Pressure during pouring | 0.045–0.055 MPa | Facilitates gas removal without causing sand entrainment |
| Vacuum Time | Duration after pouring | > 20 minutes | Allows for full degassing and solidification under reduced pressure |
| Coating Quality | Thickness and permeability | 0.5–1.0 mm, high permeability | Prevents metal penetration and allows gas escape |
| Gating Design | System type | Bottom-gating with ceramic components | Promotes laminar flow and reduces turbulence |
| Pattern Drying | Moisture content | < 0.5% | Minimizes vapor generation and porosity |
| Sand Compaction | Layer thickness and vibration | Thin layers (50–100 mm), uniform vibration | Ensures mold integrity and prevents sand movement |
In conclusion, the lost foam casting process is a powerful technique for producing complex castings like crude lead molds, but it demands meticulous control to avoid defects. Through my detailed examination, I have highlighted that carbon increase, porosity, and slag inclusion are major challenges in the lost foam casting process. By implementing the preventive measures discussed—such as selecting appropriate foam materials, optimizing pouring parameters, and ensuring proper coating and molding practices—the quality and durability of castings can be significantly enhanced. The lost foam casting process, when mastered, offers unparalleled efficiency and surface finish, making it indispensable in modern foundries. I encourage continuous monitoring and adaptation of these strategies to suit specific applications, as the lost foam casting process evolves with advancements in materials and technology. Ultimately, success in the lost foam casting process hinges on a deep understanding of its underlying principles and a commitment to precision at every stage.