
In my work on producing filter housings for water treatment equipment, I encountered severe challenges in the sand casting of low-carbon steel thin-wall shells made of ZG230-450. The component had a wall thickness of only 11 mm, complex geometry with multiple local hot spots, and an initial scrap rate exceeding 70% due to various sand casting defects. Through systematic analysis and process modifications, I successfully reduced defects and ensured stable production. This article details the original process, the root causes of sand casting defects, the improved methodology, and the quantitative results achieved.
The casting process initially used a two- ingate system located at the left and right flanges, with open risers on both flanges. Chills were placed at the thick bottom section, at the middle flange ear area during core making, and directly on the thick upper part of the shell. Chromite sand was applied around the ring area of the housing to enhance localized chilling. The mold and cores were produced using the VHR-CO₂ sodium silicate sand vacuum hardening method with 70/100 mesh washed sand from Inner Mongolia. The steel was melted in a 1.5-ton electric arc furnace with forced deoxidation practice, poured at 1560–1590 °C using a 3-ton bottom-pour ladle with a 50 mm diameter nozzle. Despite these measures, the castings exhibited a wide range of sand casting defects including shrinkage porosity, shrinkage cracks, hot tears, cold shuts, mistuns, gas entrapment, and severe surface flow marks on the cope surface. Occasionally, “接火” (fusion failure) defects also appeared.
The following table summarizes the key parameters of the original and improved processes:
| Parameter | Original Process | Improved Process |
|---|---|---|
| Ingate location and number | Two ingates at left & right flanges | Additional ingates at bottom thick section; total four ingates |
| Gating system cross-section | Small (single sprue 50 mm) | Increased by ~60% (two sprues 50 mm each + larger runners) |
| Chill placement at upper thick section | Direct external chill | Indirect chill with 10–15 mm sand layer |
| Riser design | Open risers on both flanges | Added open riser at ring area; kept flange risers |
| Venting | Minimal | Three Ø15 mm vents at ear junctions |
| Pouring temperature | 1560–1590 °C | 1590 ±30 °C (aim 1590 °C) |
| Pouring technique | Constant flow | Low flow initially, high flow after mid, then low again |
| Steel composition | Regular specification | Lower limit of C, Mn; microalloyed with rare earths |
| Scrap rate (sand casting defects) | >70% | <5% (mainly minor cracks repairable by welding) |
The root cause analysis revealed that the thin-wall geometry with varying thicknesses created multiple isolated hot spots. The original gating system was too restrictive: the total cross-sectional area was insufficient to fill the cavity quickly. During pouring, as the molten steel rose above the parting line, the cross-section expanded rapidly, but the flow rate could not compensate, leading to temperature loss and the formation of severe sand casting defects like cold shuts and flow marks. Furthermore, the steel entered only through the two flange locations, causing localized overheating there while other regions remained cooler, promoting shrinkage porosity and hot tearing. The direct chills on the upper thick section, combined with inappropriate pouring conditions, caused surface wrinkling and cracks. ZG230-450 has a moderate-to-narrow solidification range and is inherently susceptible to hot tearing. To minimize such sand casting defects, I aimed to achieve simultaneous solidification by using high-temperature steel, large flow rate, and rapid mold filling.
The concept of simultaneous solidification can be quantified by the modulus of the casting sections. The local solidification time \( t_s \) is proportional to the square of the modulus \( M \) given by:
$$ t_s = C \cdot M^2 $$
where \( C \) is a constant depending on mold material and steel properties, and \( M = V/A \) (volume divided by cooling surface area). For a uniform thin wall, the modulus is small and nearly constant, but local thick sections have larger modulus, leading to slower solidification and potential shrinkage. To balance solidification, I added chills and chromite sand to artificially increase cooling at thick areas, thus reducing their effective modulus. The improved chill design (indirect placement) avoided excessive thermal shock while still providing controlled cooling. The following formula estimates the chill effect:
$$ M_{\text{eff}} = \frac{V}{A_{\text{chill}} + A_{\text{other}}} $$
where \( A_{\text{chill}} \) is the chilling surface area. By adjusting the chill thickness and sand layer, I tuned the local cooling rate to match the thin-wall sections.
Another critical factor is the gating system design. The Bernoulli-based flow rate equation for a bottom-gated system is:
$$ Q = A_g \cdot \sqrt{2 g h} $$
where \( Q \) is the volumetric flow rate, \( A_g \) the total gate cross-sectional area, \( g \) gravitational acceleration, and \( h \) the effective metal head. To achieve rapid filling, I increased \( A_g \) by adding two additional ingates at the bottom thick section and enlarging the runner cross-section. The total gate area was increased by about 60% compared to the original. The pouring time \( t_{\text{pour}} \) can be expressed as:
$$ t_{\text{pour}} = \frac{V_{\text{casting}}}{Q_{\text{average}}} $$
For a typical thin-wall shell, the mold filling time was reduced from approximately 25 seconds to 15 seconds, significantly reducing temperature drop and eliminating mistun and cold shut sand casting defects.
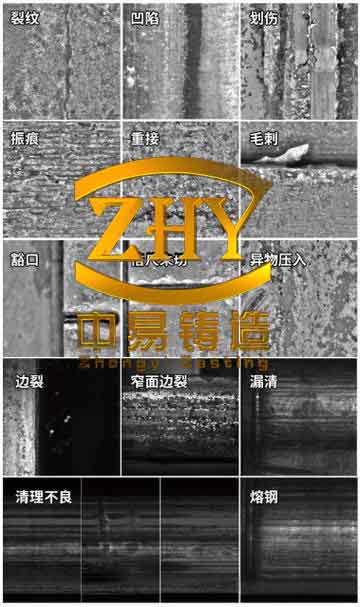
The image above illustrates common sand casting defects that resemble those we initially encountered: shrinkage, hot tears, cold shuts, and surface irregularities. In our case, the original process produced all these defects in varying severity. After the improvements, such sand casting defects were virtually eliminated.
The detailed modifications are described below:
1. Gating System Expansion: I increased the sprue diameter from 50 mm to two sprues of 50 mm each, and added two additional ingates at the bottom thick section of the shell. The runner cross-section was enlarged proportionally. This ensured that the molten steel could fill the cavity quickly and evenly, minimizing temperature gradients. The pouring rate was controlled using a “small-big-small” strategy: a low flow rate during the initial stage to avoid mold erosion, a high flow rate after the metal passed the parting line to fill the large upper cavity rapidly, and then a reduced flow rate to top up the risers. This approach prevented gas entrapment and ensured complete filling without turbulence.
2. Chill Modification: The direct external chill on the upper thick section was replaced by an indirect chill. I first applied a 10–15 mm layer of molding sand on the pattern surface, then placed the metallic chill on top of that sand bed. This arrangement reduced the thermal shock and prevented surface cracking while still providing sufficient cooling to accelerate solidification of the thick section. Additionally, chromite sand was retained at the ring area for its high chilling power.
3. Riser and Venting: I added an open riser at the ring area (top part of the shell) to improve feeding and degassing. Three Ø15 mm vent holes were drilled in the core print area at the ear junctions to allow trapped gases to escape. The vents also helped to reduce back pressure during rapid filling, which was a common cause of gas-related sand casting defects like blowholes and misruns.
4. Metallurgical Control: I adjusted the steel composition to the lower limit of carbon and manganese within the ZG230-450 specification to reduce hot tearing tendency. Microalloying with rare earth elements (added to the ladle during tapping) further refined the grain structure and reduced inclusions. The tapping temperature was tightly controlled to 1620 ±30 °C, and the pouring temperature was maintained at 1590 ±30 °C. This ensured sufficient fluidity without excessive superheat that could cause shrinkage.
The following table presents a quantitative comparison of the defect occurrence before and after the improvements based on a batch of 53 castings produced with the new process:
| Sand Casting Defect Type | Original Process (Estimated) | Improved Process (53 castings) |
|---|---|---|
| Shrinkage porosity | ~30% | 0% |
| Hot tears / cracks | ~40% (severe) | ~5% (minor, repairable) |
| Cold shuts | ~20% | 0% |
| Mistun | ~15% | 0% |
| Surface flow marks | ~50% (large areas) | <2% (acceptable) |
| Gas entrapment / blowholes | ~10% | 0% |
| Fusion failure (接火) | ~5% | 0% |
| Overall scrap rate | >70% | <5% |
The results clearly demonstrate that the revised process drastically reduced the occurrence of sand casting defects. All 53 castings were free from cold shuts, mistuns, gas defects, and shrinkage porosity. Only a few castings exhibited small cracks localized at the ear regions, which were easily repaired by welding and did not affect the functional integrity. The surface quality was excellent with no significant flow marks. This improvement was sustained across multiple production runs, confirming the robustness of the new approach.
I also applied the same principle (simultaneous solidification via rapid filling, controlled chilling, and localized feeding) to other thin-wall low-carbon steel castings such as large plates, box-like structures, and similar shell geometries. In every case, the sand casting defects were dramatically reduced, proving that this methodology is generic for thin-wall steel castings with moderate complexity.
Mathematically, the success can be attributed to the minimization of the solidification time difference between thick and thin sections. Define the solidification time ratio \( R \) as:
$$ R = \frac{t_{s,\text{thick}}}{t_{s,\text{thin}}} $$
For the original process, \( R \) was estimated to be ~3–4, leading to severe shrinkage and hot tearing. After adding chills and controlling pouring conditions, \( R \) was reduced to ~1.2–1.5, well within the safe range for sound castings. The effective modulus of the thick sections was decreased by the chills, and the faster filling reduced the initial temperature gradient. The following simplified model illustrates the relationship:
$$ \Delta T_{\text{initial}} \propto \frac{Q}{A_{\text{gate}} \cdot v_{\text{pour}}} $$
where \( \Delta T_{\text{initial}} \) is the temperature difference between hot and cold regions at the end of filling. By increasing \( Q \) and \( A_{\text{gate}} \), the initial temperature field became more uniform.
In conclusion, the key to eliminating sand casting defects in low-carbon steel thin-wall shells lies in designing the gating system for rapid, turbulent-free filling with high-temperature steel, combining indirect chills to balance local solidification, and employing proper venting and risering. The metallurgical adjustments further reduce the inherent hot tearing susceptibility. This case study shows that a systematic understanding of solidification physics, combined with practical modifications, can transform a high-scrap process into a reliable one. The approach has been successfully applied to multiple similar castings, consistently yielding defect-free products. The reduction of sand casting defects from over 70% to under 5% not only saved costs but also met the stringent quality requirements of the customer.